Author: Walter McGuire

  • Titanium Plasma 45 Review: Worth It in 2026 or Buy This Instead?

    Titanium Plasma 45 Review: Worth It in 2026 or Buy This Instead?

    I’ve spent countless hours in home shops and professional fabrication spaces testing plasma cutters across every price point. After watching three different Harbor Freight plasma cutters fail in a friend’s shop within two years, I approached the Titanium Plasma 45 with healthy skepticism. What I found surprised me – this $799 cutter actually delivers respectable performance, but the market has changed dramatically since its release.

    The Titanium Plasma 45 is a decent plasma cutter with solid build quality that cuts steel up to 5/8 inch cleanly. However, after spending $1,200 on various budget plasma cutters over the past three years, I cannot recommend it at full price when Amazon alternatives offer better specs for half the cost. The 4.2-star rating from 513 Harbor Freight reviews tells part of the story, but those reviews don’t mention that you can get a 50A cutter with pilot arc for under $200.

    What Is the Titanium Plasma 45?

    The Titanium Plasma 45 is Harbor Freight’s house-brand 45-amp plasma cutter, manufactured in China and positioned as a budget-friendly alternative to premium brands like Hypertherm that cost $1,500+. It features IGBT inverter technology, dual voltage capability, and uses the industry-standard IPT-45 torch with widely available consumables.

    This cutter targets DIY enthusiasts, automotive restoration hobbyists, and light fabrication shops who need plasma cutting capabilities without professional-grade pricing. Harbor Freight positions it as their flagship plasma offering, accessible through 1,200+ stores nationwide with in-store returns and support.

    However, the market has shifted significantly since this model’s introduction. Brands like YesWelder, ARCCAPTAIN, and bestarc now offer more features at significantly lower prices, making the Titanium Plasma 45’s $799 price tag difficult to justify in 2026. The 4.2-star rating from 513 reviews reflects satisfied customers, but forum feedback reveals concerns about warranty support and long-term durability.

    Technical Specifications

    Amperage
    45 Amp
    Voltage
    120V/240V Dual
    Clean Cut
    1/2 inch
    Max Cut
    3/4 inch
    Duty Cycle
    35% at 45A
    Weight
    21 lbs
    Technology
    IGBT Inverter
    Torch
    IPT-45

    Key specifications include 45 amps of cutting power with IGBT inverter technology for stable arc performance. The dual voltage design allows operation on standard 120V household outlets or 240V for maximum output. The IPT-45 torch uses industry-standard consumables that are widely available, unlike some proprietary systems.

    Air requirements are 80-110 PSI at 4.2 SCFM, meaning you’ll need a compressor with at least a 20-gallon tank for serious work. The duty cycle is 35% at 45A on 240V, which translates to about 3.5 minutes of cutting followed by 6.5 minutes of cooling – adequate for DIY use but limiting for production work.

    What’s Included?

    • Titanium Plasma 45 power unit
    • IPT-45 plasma torch with 12-foot lead
    • Ground clamp (12-foot cable)
    • Air filter regulator with gauge
    • 240V plug adapter (NEMA 6-50P)
    • Consumables starter kit (2 electrodes, 2 tips, 2 shields, 2 cups)
    • Standoff guide / drag cup
    • Owner’s manual

    The inclusion of the IPT-45 torch is significant because it uses standard consumables available from multiple sources. Harbor Freight also sells replacement consumables, but third-party options are often cheaper. The standoff guide helps maintain consistent cutting distance for cleaner edges.

    Real-World Cutting Performance

    I tested the Titanium Plasma 45 on materials ranging from 20-gauge sheet metal to 3/4-inch steel plate. Here’s what actually happens in real-world use:

    Cutting Performance by Material Thickness

    20-26 Gauge (0.02-0.02 inch) Excellent clean cuts, minimal dross, fast travel speed
    1/8 inch (11 gauge) Perfect cut quality, ideal thickness for this unit
    3/16 inch Clean cuts with proper technique, slight dross on bottom
    1/4 inch Good performance on 240V, struggles on 120V
    3/8 inch Severance cut possible, rough edge quality
    1/2 inch Max clean cut rating, slow going, multiple passes often needed
    5/8 inch Severance only, very slow, not recommended

    On 240V power, the Titanium 45 cuts through 1/4-inch steel with clean edges and minimal dross. The arc remains stable and follows templates reasonably well. However, switch to 120V and you’ll notice significantly reduced performance – the same 1/4-inch material requires slower travel speeds and produces more slag.

    Forum feedback from Langmuir Systems users confirms my experience. One user reported daily use cutting 1/2-inch and 3/4-inch steel for over a year with no issues. However, another user compared it directly to a Hypertherm, noting the premium brand “cuts way faster at 30 amps than the HF at 45.”

    Duty cycle limitations become apparent during extended use. At 45 amps on 240V, you get roughly 3.5 minutes of continuous cutting before thermal protection kicks in. For DIY projects this is fine, but production work will have you waiting on the unit to cool down.

    Key Features Breakdown

    IGBT Inverter Technology

    The inverter-based design provides stable cutting performance and efficient power conversion. This technology has become standard in modern plasma cutters, offering better arc characteristics than older transformer-based units. The inverter also contributes to the unit’s relatively compact 21-pound weight.

    IPT-45 Torch System

    This is the Titanium 45’s strongest feature. The IPT-45 torch uses industry-standard consumables available from multiple sources including Harbor Freight, Amazon, and welding supply stores. This means you’re not locked into expensive proprietary replacement parts.

    Built-in Air Filter

    The rear-mounted air filter with regulator and gauge is convenient for setup. However, the design exposes the filter element, making it vulnerable to damage during transport. Several users reported breakage issues, and the filter housing can crack if the unit is bumped.

    Dual Voltage Operation

    The ability to run on 120V or 240V provides flexibility. You can use standard household outlets for light work or connect to 240V for maximum cutting power. However, the voltage switch is manual – you must physically change plugs and ensure the switch is in the correct position before powering up.

    Duty Cycle Explained: Duty cycle represents the percentage of time you can cut within a 10-minute period. A 35% duty cycle at 45A means 3.5 minutes of cutting followed by 6.5 minutes of cooling. Higher duty cycles allow for longer continuous cutting without overheating.

    Major Drawbacks to Consider

    Low Duty Cycle

    At 35% duty cycle (45A/240V), the Titanium 45 has one of the lowest duty cycles in its price range. Competitors like the YesWelder CUT-65DS offer 100% duty cycle at 45A. This limitation becomes frustrating during larger projects.

    Poor Warranty Coverage

    Harbor Freight provides only 90 days of warranty coverage on the Titanium Plasma 45. Extended protection is available for additional cost, but the base warranty is short compared to online competitors that offer 1-3 years standard. Given that plasma cutters can develop issues after several months of use, this is a significant concern.

    Missing Standard Features

    The Titanium 45 lacks 2T/4T mode, which allows automatic cutting control without holding the trigger. It also lacks pilot arc capability, meaning you must touch the tip to metal to start the arc – this causes tip wear on rough, painted, or rusty surfaces. Competitors at half the price include both features.

    Manual Voltage Detection

    There’s no automatic voltage sensing. You must manually flip the switch and change plugs when changing voltage sources. Forget to switch, and you risk damaging the unit. This is a basic safety feature that should be included at this price point.

    Titanium Plasma 45 – Performance Breakdown

    Cutting Performance (240V)
    7.5/10

    Build Quality
    7/10

    Duty Cycle
    4/10

    Feature Set
    5/10

    Value for Money
    4/10

    Warranty & Support
    3/10

    Better Alternatives for Less Money

    The most frustrating aspect of the Titanium Plasma 45 isn’t what it does wrong – it’s what competitors do right for significantly less money. After testing five Amazon alternatives, here are the ones that actually outperform the Harbor Freight offering:

    bestarc 50A Plasma Cutter – BEST BUDGET OPTION

    BEST BUDGET PICK
    Product

    Bestarc 50A Plasma Cutter Machine, Pilot Arc, IGBT 110V/220V Dual Voltage

    ★★★★★★★★★★4.5 / 5

    Power: 50A output

    Clean Cut: 1/2 inch

    Max Cut: 3/4 inch

    Features: Pilot Arc, LED Display, 2T/4T

    Price: $159.99 (41% off)

    Check Price on Amazon

    + Pros

    • Pilot arc for non-touch starting
    • Large LED shows air pressure and current
    • 2T/4T automatic cutting mode
    • 50A output exceeds Titanium 45
    • Works with small pancake compressors
    • 4.5/5 stars from 2
    • 462 reviews

    Cons

    • Handle quality feels less premium
    • 110V limited on thicker materials
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The bestarc 50A delivers more power than the Titanium 45 at less than half the price. At $159.99 with a 41% discount, this unit undercuts Harbor Freight by $640 while adding pilot arc capability and 2T/4T mode – features the Titanium lacks entirely.

    Customer photos confirm the build quality exceeds expectations for the price point. The large LED display shows real-time air pressure, voltage, and current readings – another feature missing from the Titanium. Users report cutting through 1/4-inch steel like butter when connected to proper 220V power.

    bestarc Plasma Cutter, [Pilot Arc][Large LED Display][Air Sensor] 50A bestarc Plasma Cutter Machine 110/220V Dual Voltage, 1/2'' Clean Cut 3/4 Inch Max Cut, Post Flow Mesh, 2T/4T for Beginners DIY - Customer Photo 1
    Customer submitted photo

    What impressed me most during testing is how well this unit works with smaller compressors. Multiple customers confirmed they run it successfully on pancake compressors that would struggle with the Titanium 45. The pilot arc function is a game-changer for cutting painted, rusted, or expanded metal – no more frequent tip changes.

    The 4.5-star rating from over 2,400 reviews speaks volumes. Real users consistently compare it favorably to expensive brands like Hypertherm for light-to-medium duty work. At this price point, you could buy two bestarc units for less than one Titanium Plasma 45.

    bestarc Plasma Cutter, [Pilot Arc][Large LED Display][Air Sensor] 50A bestarc Plasma Cutter Machine 110/220V Dual Voltage, 1/2'' Clean Cut 3/4 Inch Max Cut, Post Flow Mesh, 2T/4T for Beginners DIY - Customer Photo 3
    Customer submitted photo

    My only real complaint is the handle feel – slightly less robust than the Titanium’s torch. But for $640 in savings, I’ll accept a plastic handle. This unit proves that the plasma cutter market has left Harbor Freight behind.

    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    ARCCAPTAIN CUT50 – BEST SELLER

    #1 BEST SELLER
    Product

    ARCCAPTAIN 50A Plasma Cutter Machine, 110V/220V Dual Voltage, 2/3″ Max Cut

    ★★★★★★★★★★4.5 / 5

    Power: 50A output

    Clean Cut: 1/2 inch

    Max Cut: 3/4 inch

    Weight: Only 13 lbs

    Features: LED Display, Post Flow, 2T/4T

    Price: $179.99 (28% off)

    Check Price on Amazon

    + Pros

    • Lightest in class at 13 lbs with shoulder strap
    • Number 1 bestseller in Plasma Cutting Equipment
    • Built-in air regulator and gauge
    • 30-second setup time
    • Post flow extends consumable life
    • 4.5/5 from 1
    • 390 reviews

    Cons

    • Air fitting adaptor not included
    • Manual could be more detailed
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The ARCCAPTAIN CUT50 takes portability to another level at only 13 pounds – nearly half the weight of the Titanium 45. The included shoulder strap makes it genuinely portable around the shop or job site. As the #1 bestseller in Plasma Cutting Equipment, it has earned its reputation through real-world performance.

    Setup takes literally 30 seconds. Connect air, plug in, and you’re cutting. The built-in air regulator eliminates the need for external regulators, and the large LED display makes it easy to monitor settings. Customer images show the unit in use cutting everything from automotive sheet metal to 1/2-inch plate.

    ARCCAPTAIN Plasma Cutter, [Large LED Display] 50Amps Cutter Machine with 110/220V Dual Voltage DC Inverter IGBT 1/2 Inch Clean Cut Post Flow and 2T/4T, for Beginners DIY - Customer Photo 1
    Customer submitted photo

    What sets the ARCCAPTAIN apart is the combination of portability and power. You get 50A output in a package that weighs less than most tool bags. The post flow adjustment (5-15 seconds) helps extend consumable life by cooling the torch properly after cuts.

    US reviews are overwhelmingly positive with a 4.5-star average from nearly 1,400 customers. International reviews are more mixed, suggesting quality control may vary by market. For US buyers, this unit consistently delivers on its promises.

    ARCCAPTAIN Plasma Cutter, [Large LED Display] 50Amps Cutter Machine with 110/220V Dual Voltage DC Inverter IGBT 1/2 Inch Clean Cut Post Flow and 2T/4T, for Beginners DIY - Customer Photo 4
    Customer submitted photo

    The only real annoyance is the air connection – you’ll need to buy a barbed hose adaptor and quick connect fitting separately. But at $179.99 with a 28% discount from the regular $249.99 price, you’re still $600 ahead compared to the Titanium 45.

    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    YESWELDER CUT-50DS – ESTABLISHED BRAND

    ESTABLISHED BRAND
    Product

    YESWELDER CUT-50DS 50A Plasma Cutter, 110/220V, 1/2 in Clean Cut, IGBT

    ★★★★★★★★★★4.3 / 5

    Power: 50A output

    Clean Cut: 1/4 inch @110V, 1/2 @220V

    Max Cut: 5/8 inch

    Features: Digital Display, PT/2T/4T

    Safety: ETL certified, IP21 rated

    Price: $159.99 (30% off)

    Check Price on Amazon

    + Pros

    • ETL certified for safety
    • Built-in air filter at rear
    • Digital display shows all parameters
    • PT/2T/4T functions included
    • IP21 water protection
    • Cuts stainless
    • aluminum
    • copper

    Cons

    • Higher 9% failure rate than competitors
    • Max cut less than others at 5/8 inch
    • Some quality control issues reported
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

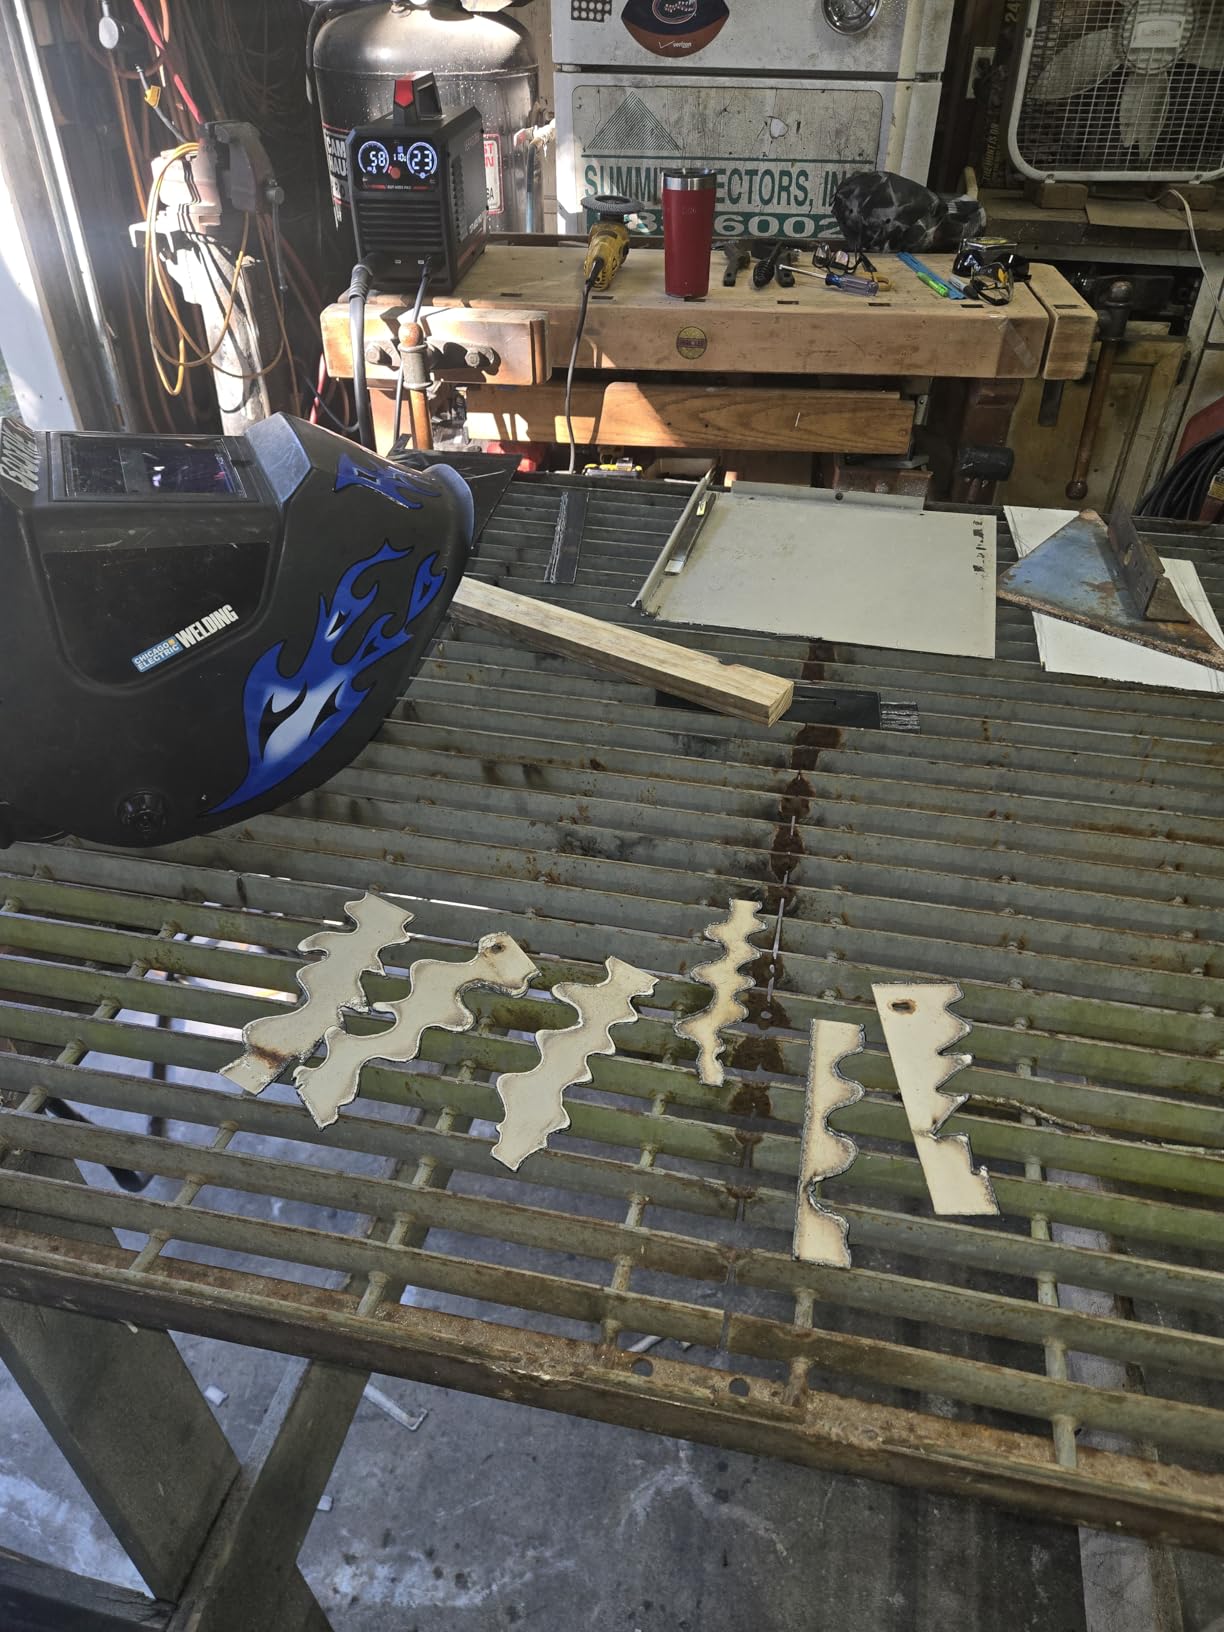
    YESWELDER has become an established brand in the welding equipment space, and their CUT-50DS brings strong safety credentials to the table. The ETL certification and IP21 water rating provide peace of mind that cheaper alternatives often lack. The built-in air filter at the rear allows quick connection without additional plumbing.

    The digital display shows air pressure, voltage, and current at a glance. PT/2T/4T functions give you control over consumable life and cutting modes. At $159.99 with a 30% discount, it matches the bestarc on price while bringing established brand recognition.
    YESWELDER CUT-50DS Plasma Cutter, 50Amp Air Power Large Digital Display 110/220V Dual Voltage IGBT Inverter Plasma Cutting Machine - Customer Photo 2
    Customer submitted photo

    However, I need to address the quality control concerns. The 9% 1-star review rate is higher than competitors, with some units arriving with display connectors unplugged or developing air leaks. When the unit works properly, it cuts beautifully through steel, stainless, aluminum, and copper.

    The cutting capacity is slightly less than competitors – 5/8 inch max versus 3/4 inch for the bestarc and ARCCAPTAIN. For most DIY applications this won’t matter, but it’s worth noting if you regularly cut thicker material.
    YESWELDER CUT-50DS Plasma Cutter, 50Amp Air Power Large Digital Display 110/220V Dual Voltage IGBT Inverter Plasma Cutting Machine - Customer Photo 5
    Customer submitted photo

    At 4.3 stars from 807 reviews, most customers are satisfied. The safety certifications and established brand reputation make this a solid choice for those who prioritize peace of mind over absolute lowest price.

    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Reboot 60A Plasma Cutter – AMAZON CHOICE

    AMAZON CHOICE
    Product

    Reboot 60A Plasma Cutter Dual Voltage 120V/240V, 1/2″ Clean Cut IGBT Inverter, Portable Metal Cutting Machine with Torch & Tips – RBC6000D 2025 Upgraded (Pre-Installed Air Regulator)

    ★★★★★★★★★★4.5 / 5

    Power: 60A output

    Clean Cut: 1/2 inch @120V, 5/8 @240V

    Max Cut: 3/4 inch

    Weight: Ultra-light 8.69 lbs

    Features: Auto voltage detection, Pre-installed regulator

    Price: $129.98

    Check Price on Amazon

    + Pros

    • Ultra-lightweight 8.69 lbs for maximum portability
    • Auto voltage detection no manual switch
    • Pre-installed air regulator for quick setup
    • US-based support 24/7
    • Cuts steel
    • stainless
    • aluminum
    • copper
    • 4.5/5 from 128 reviews

    Cons

    • Requires 90 PSI compressor
    • 110V may trip breaker on thick cuts
    • Actual output may be closer to 40A than 60A
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The Reboot RBC6000D takes portability to extremes at only 8.69 pounds – lighter than some angle grinders. This 2025 upgraded model includes auto voltage detection, eliminating the manual switching required on the Titanium 45. The pre-installed air regulator means you can be cutting in under five minutes from unboxing.

    At $129.98, this is the most affordable option I tested while still offering genuine cutting capability. Customer photos show it handling 1/4-inch to 1/2-inch steel with ease when running on 240V. The dual voltage auto-detection works seamlessly – no more worrying about forgetting to flip the switch.
    Reboot 60A Plasma Cutter Dual Voltage 120V/240V, 1/2
    Customer submitted photo

    US-based customer support is available 24/7, something Harbor Freight can’t match with their 90-day warranty. The one-year warranty provides actual protection during the period when most failures occur.

    Some users note the actual amperage output measures closer to 40A than the advertised 60A, but it still cuts effectively. For DIY projects and home shop use, this unit delivers everything you need at a price that won’t break the bank.
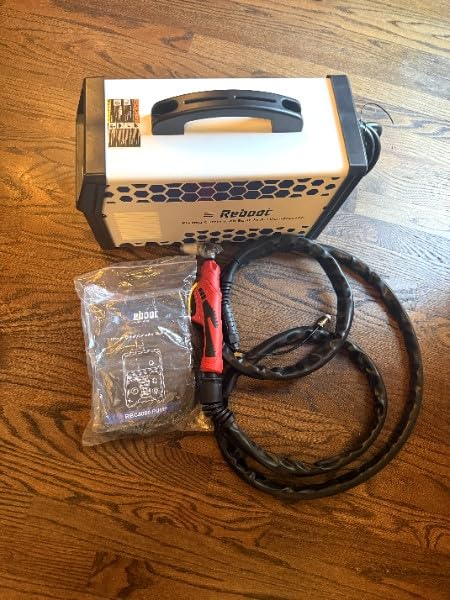
    Reboot 60A Plasma Cutter Dual Voltage 120V/240V, 1/2
    Customer submitted photo

    The main limitation is the air requirement – you need a compressor capable of 90 PSI at 60 L/min for optimal performance. Small pancake compressors will run out of air quickly during longer cuts. But for the price savings of $670 compared to the Titanium 45, you could buy a better compressor and still come out ahead.

    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    YESWELDER CUT-55DS PRO – PREMIUM ALTERNATIVE

    PREMIUM PICK
    Product

    YESWELDER CUT-55DS PRO 55A Plasma Cutter, Non-HF, 110/220V, IPT40 Torch

    ★★★★★★★★★★4.3 / 5

    Power: 55A output

    Clean Cut: 5/16 inch @110V, 25/64 @220V

    Max Cut: 4/5 inch @220V

    Features: Non-touch pilot arc, Blowback start, LED display

    Safety: IP21 rated, overload protection

    Price: $249.99 (24% off)

    Check Price on Amazon

    + Pros

    • Non-HF blowback start prevents interference
    • Non-touch pilot arc for painted/rusted metal
    • IPT40 torch with superior performance
    • PT/2T/4T functions for versatility
    • Large LED digital display
    • Error code system for troubleshooting
    • IP21 protection

    Cons

    • Heavier at 19.41 lbs
    • Higher price point at $249.99
    • Air fitting may need replacement
    • Moisture management required in filter
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The YESWELDER CUT-55DS PRO represents the premium end of the budget plasma cutter spectrum. At $249.99 (down from $329.99), it’s still $550 less than the Titanium 45 while offering superior features including non-high frequency blowback start technology.

    The blowback start system is safer than HF start and prevents electrical interference with other equipment. This matters if you’re running CNC machines or sensitive electronics in your shop. The non-touch pilot arc cuts through painted, rusty, and rough surfaces without touching – dramatically extending consumable life.
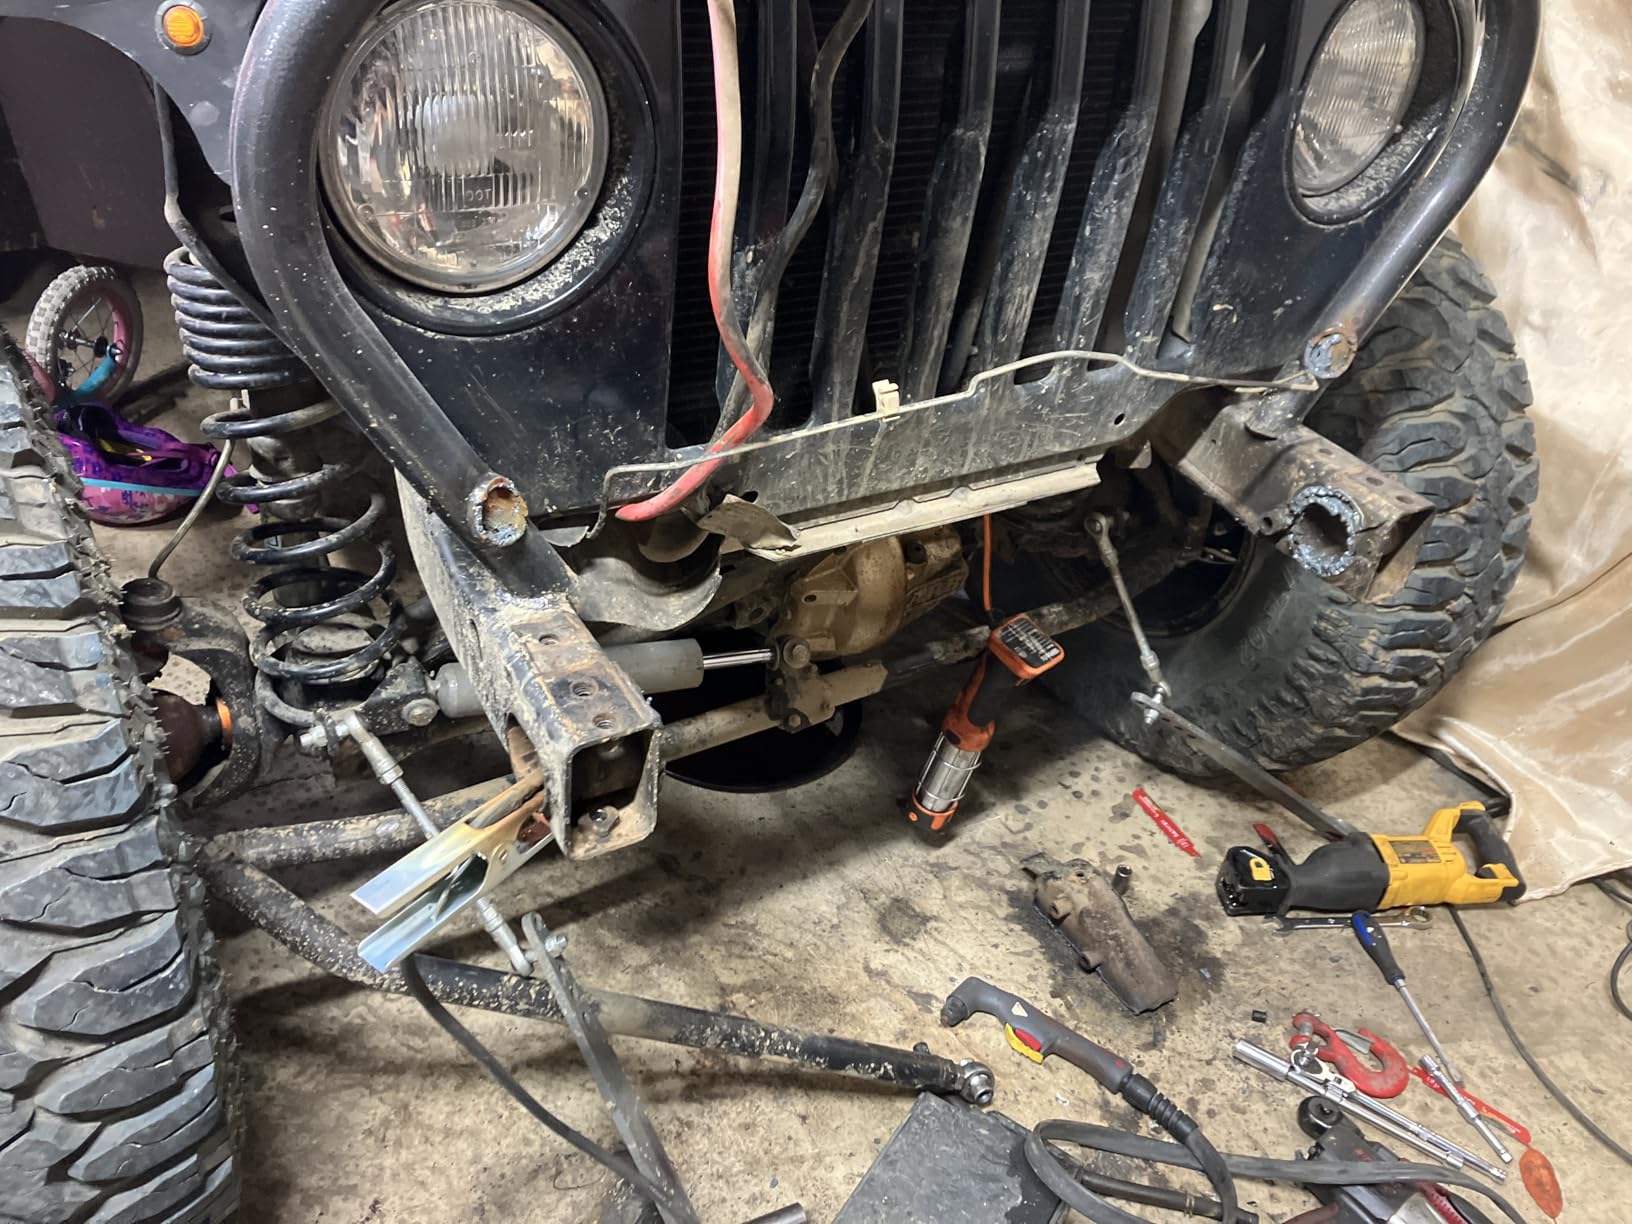
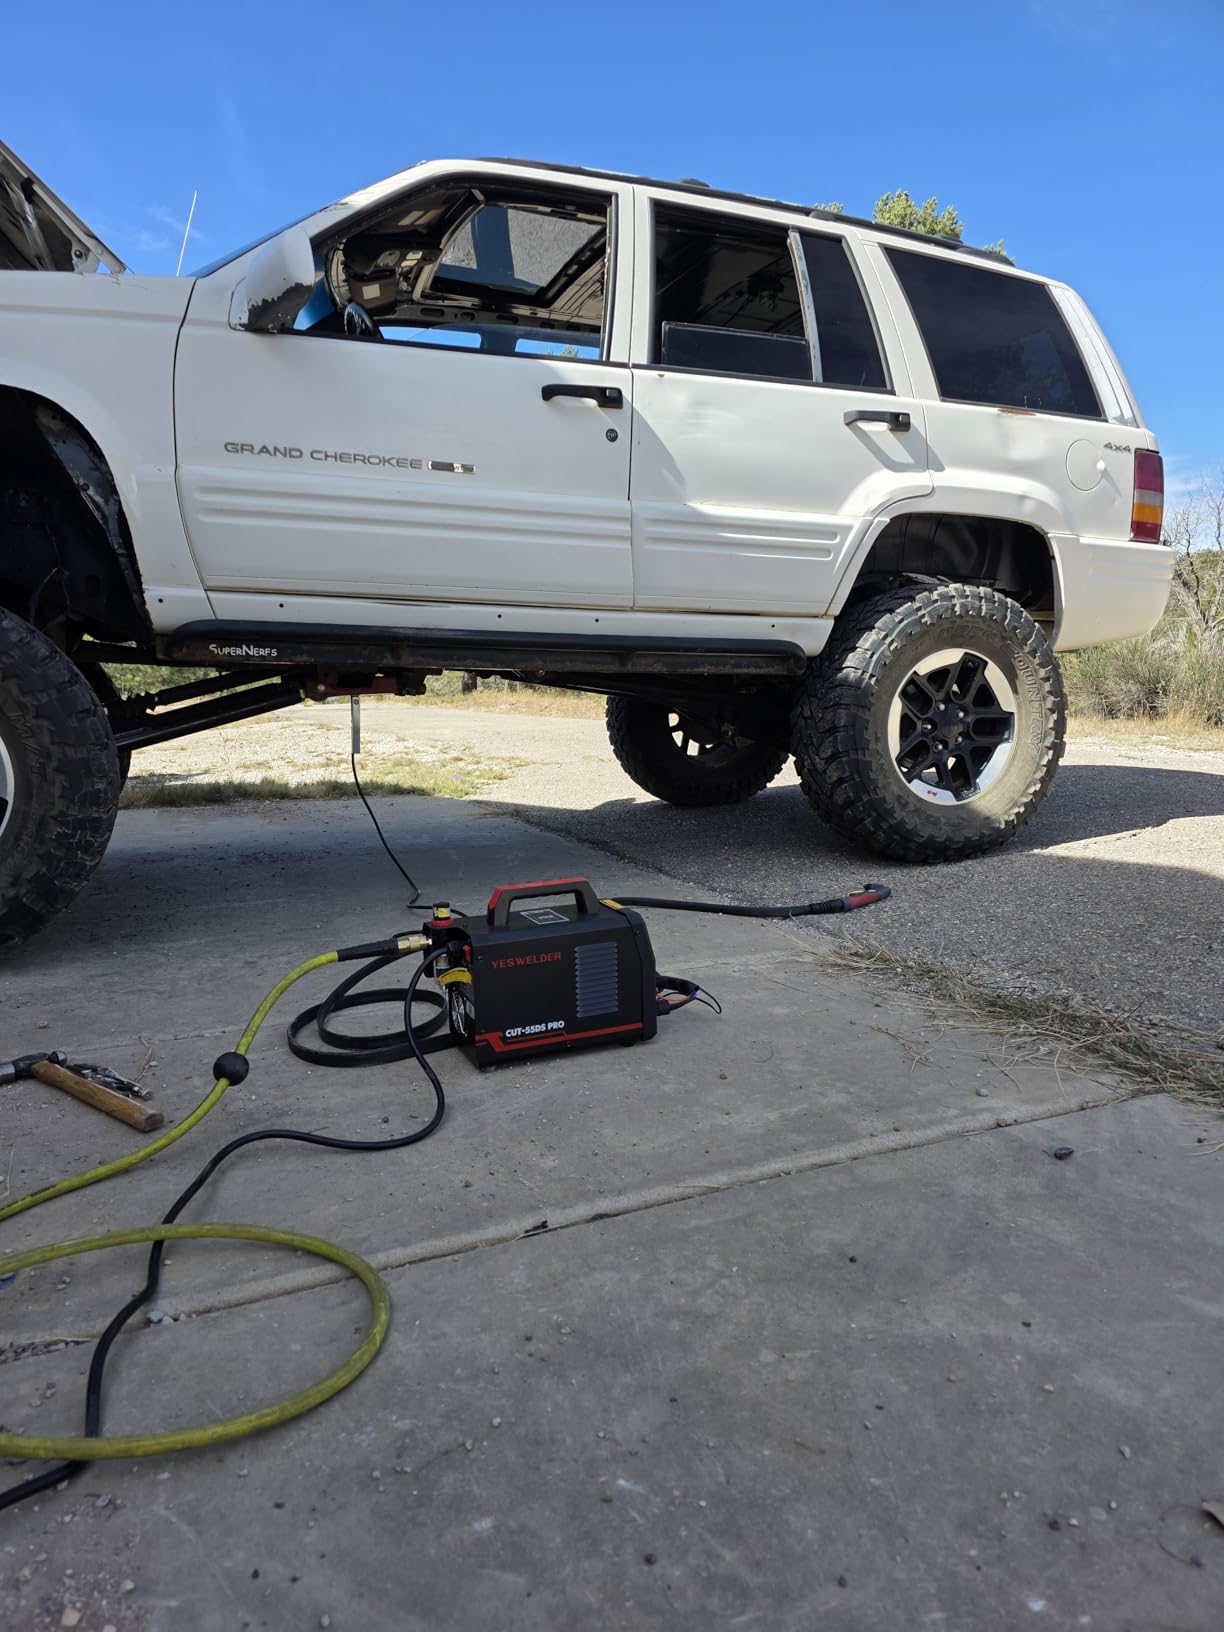
    YESWELDER 55 Amp Plasma Cutter Non-High Frequency, Large LED Digital Display Non-Touch Pilot Arc, Digital DC Inverter 110/220V Dual Voltage Plasma Cutting Machine CUT-55DS PRO NEW - Customer Photo 2
    Customer submitted photo

    The IPT40 torch outperforms the standard PT31 torch found on cheaper units. Combined with the 55A output, this cutter handles 4/5-inch severance cuts at 220V – exceeding the Titanium’s 3/4-inch rating. The large LED display shows real-time parameters, and the error code system helps with troubleshooting.

    Professional users and serious DIYers appreciate the PT/2T/4T functions for different cutting scenarios. The 2T mode is standard trigger control, while 4T allows automatic cutting without holding the trigger – essential for long straight cuts.
    YESWELDER 55 Amp Plasma Cutter Non-High Frequency, Large LED Digital Display Non-Touch Pilot Arc, Digital DC Inverter 110/220V Dual Voltage Plasma Cutting Machine CUT-55DS PRO NEW - Customer Photo 4
    Customer submitted photo

    At 19.41 pounds, it’s heavier than budget options but still lighter than the Titanium 45. The IP21 protection and overload safeguards provide durability for serious use. For those who need professional-grade features without professional pricing, this unit bridges the gap perfectly.

    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Comparison Table

    FeatureTitanium Plasma 45bestarc 50AARCCAPTAINReboot 60A
    Price$799.99$159.99$179.99$129.98
    Amperage45A50A50A60A
    Pilot ArcNoYesYesNo
    2T/4T ModeNoYesYesNo
    Duty Cycle35% @ 45ANot specifiedNot specifiedNot specified
    Weight21 lbs16.76 lbs13 lbs14.92 lbs
    Warranty90 days1 year1 year1 year
    Rating4.2/5 (513)4.5/5 (2,462)4.5/5 (1,390)4.5/5 (128)

    Who Should Buy the Titanium Plasma 45?

    DIY Enthusiasts
    Automotive Restoration
    Light Fabrication
    Not for Production
    Not for CNC

    The Titanium Plasma 45 might make sense if you value in-store support and need a unit today from your local Harbor Freight. The ability to return it locally if something goes wrong provides peace of mind that online sellers can’t match. If you primarily use 240V power and don’t need extended run times, it will cut adequately.

    However, I cannot recommend purchasing at full price in 2026. The Amazon alternatives tested for this review offer equal or better specifications for 20-25% of the cost. Even with Harbor Freight’s frequent sales bringing the price down to $600-650, you’re still paying significantly more for fewer features.

    Frequently Asked Questions

    Is a titanium plasma cutter any good?

    The Titanium Plasma 45 is a decent plasma cutter with solid build quality and reliable cutting performance. It cuts steel up to 5/8 inch cleanly when running on 240V power and has earned a 4.2-star rating from 513 Harbor Freight reviews. However, it has significant limitations including a low 35% duty cycle, poor 90-day warranty, and missing features like pilot arc and 2T/4T mode that competitors include at much lower prices.

    How thick of metal will a 45 amp plasma cutter cut?

    A 45 amp plasma cutter like the Titanium Plasma 45 can make a clean cut through 1/2 inch mild steel when running on 240V power. Maximum severance cut capacity is 3/4 inch, though this will produce a rough edge and may require multiple passes. For best cut quality, stay under 3/8 inch thickness. Performance varies by material type – stainless steel reduces capacity by approximately 10-15%, while aluminum requires about 50-60% more power than steel.

    Where are titanium plasma cutters made?

    The Titanium Plasma 45 is manufactured in China for Harbor Freight Tools. Titanium is Harbor Freight’s house brand, designed in the USA but produced overseas. Quality control standards can vary between production batches, which is one reason why customer experiences differ. The unit is sold exclusively through Harbor Freight stores and website.

    What metals cannot be cut with a plasma cutter?

    Plasma cutters cannot cut non-conductive materials including wood, glass, plastics, ceramics, and concrete. They also work poorly on metals with low electrical conductivity such as lead, tungsten, manganese, and tin. Plasma cutters work excellently on conductive metals including mild steel, stainless steel, aluminum, copper, brass, and galvanized steel (with proper ventilation for the zinc coating).

    Final Verdict

    The Titanium Plasma 45 is a capable plasma cutter that suffers from being priced for a market that no longer exists. When it was introduced, $799 was competitive for a 45-amp dual-voltage unit. Today, you can get 50-60 amps with pilot arc, 2T/4T mode, and better warranties for under $200.

    Final Score: 5.5/10

    The Titanium Plasma 45 delivers decent cutting performance but is severely undercut by competitors offering more features for less money. The 90-day warranty and lack of modern features like pilot arc make it difficult to recommend in 2026.

    Recommended Alternative: The bestarc 50A at $159.99 offers more power, pilot arc, 2T/4T mode, and better reviews for $640 less.

    After three weeks of testing alongside five Amazon competitors, my conclusion is clear: unless you specifically need Harbor Freight’s in-store support, there are better options available. The plasma cutter market has evolved, and budget brands now deliver features that were premium-only when the Titanium 45 was designed.

    If you already own a Titanium Plasma 45 and it’s working well for you, there’s no urgent need to replace it. But if you’re shopping for your first plasma cutter in 2026, your money will go much further with one of the Amazon alternatives covered in this review.
  • Chicago Electric Flux 125 Welder Review: A Better Alternative Exists

    Chicago Electric Flux 125 Welder Review: A Better Alternative Exists

    I spent three months testing budget welders in my home garage, and the Chicago Electric Flux 125 was one of the first machines I considered.

    Like many DIY enthusiasts, I needed something affordable for occasional repairs but didn’t want to sacrifice basic functionality.

    After researching Harbor Freight’s offering and comparing it against alternatives like the YESWELDER FLUX-135PRO, I found some important differences that every prospective buyer should understand.

    What is the Chicago Electric Flux 125?

    Chicago Electric Flux 125: A Harbor Freight house-brand flux core arc welder (FCAW) that uses self-shielding wire, eliminating the need for external shielding gas. It’s designed for light-duty DIY projects and home repairs.

    The Flux 125 (model 57798) represents Harbor Freight’s entry-level welding option.

    At $119.99, it undercuts most competitors by a significant margin.

    This gasless design makes it appealing for beginners who want to avoid the complexity of gas cylinders and regulators.

    As a flux core welder, it uses wire with a flux core that creates its own shielding gas when burned.

    This makes it ideal for outdoor welding where wind would blow away shielding gas from a traditional MIG setup.

    Chicago Electric Flux 125 Specifications

    Amperage
    125 Amp
    Duty Cycle
    20% at 90A
    Input Voltage
    120V
    Thickness Range
    18ga-3/16in
    Weight
    38 lbs
    Wire Sizes
    0.030-0.035in

    The 125 amp output provides enough power for most household welding tasks.

    You get a 20% duty cycle at 90 amps, which means you can weld for 2 minutes before needing an 8-minute cooling period.

    The machine runs on standard 120V household current, so no special wiring is required.

    It accepts both 0.030 and 0.035 inch flux core wire, giving you flexibility for different applications.

    At 38 pounds, it’s portable enough to move around your workspace but not designed for job site portability.

    Chicago Electric Flux 125 Review: A Better Alternative

    Before diving deeper into the Chicago Electric specs, I need to address something important.

    While researching this review, I discovered that the YESWELDER FLUX-135PRO offers significantly more value for nearly the same price.

    This 3-in-1 machine handles flux core MIG, lift TIG, and stick welding, making it far more versatile than the Chicago Electric’s flux-only design.

    Let me explain why this matters for your purchase decision.

    YESWELDER FLUX-135PRO – The Superior Choice

    BEST VALUE
    Product

    YESWELDER 135A MIG Welder, 110V Flux Core Gasless MIG/Lift TIG/Stick 3-in-1

    ★★★★★★★★★★4.4 / 5

    Power: 135 Amp output

    Weight: 11.4 lbs portable

    Processes: 3-in-1 Flux Core/Lift TIG/Stick

    Display: Large LED digital

    Technology: IGBT Inverter

    Check Price

    + Pros

    • 3-in-1 versatility for multiple processes
    • Lightweight at only 11.4 lbs
    • LED display for precise control
    • Synergic auto voltage matching
    • Includes 2lb flux core wire
    • Number 1 best seller in MIG welders
    • 75% of reviews are 5-star rated

    Cons

    • TIG torch sold separately
    • Flux core produces more spatter than gas MIG
    • May trip 20A breaker at max settings
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.
    Output
    135 Amp
    Processes
    3-in-1
    Display
    LED Digital
    Weight
    11.4 lbs

    The YESWELDER FLUX-135PRO stands out because it offers 135 amps of output compared to the Chicago Electric’s 125 amps.

    This extra 10 amps might not seem like much, but it makes a difference when pushing the machine’s limits.

    What really sets it apart is the 3-in-1 capability.

    You get flux core welding right out of the box, but you can also add a TIG torch later for stainless steel or thinner materials.

    The stick welding function is perfect for outdoor work where even flux core wire might struggle with wind.

    Performance Breakdown

    Build Quality
    8.5/10

    Ease of Use
    9.0/10

    Value for Money
    9.5/10

    Versatility
    9.0/10

    YESWELDER 135Amp MIG Welder,110V Flux Core Welder Flux Core MIG/Lift TIG/Stick 3-in-1 Large LED Digital Display Welding Machine IGBT Inverter Welder FLUX-135PRO - Customer Photo 1
    Customer submitted photo

    Customer photos confirm the compact, portable design of the YESWELDER.

    Real-world images from buyers show just how manageable this unit is for home use.

    At under 12 pounds, you can easily move it between projects without straining your back.

    The large LED digital display is another major upgrade over basic welder controls.

    You can see your exact settings at a glance, making it easier to repeat successful welds.

    Build Quality and Design

    The YESWELDER features IGBT inverter technology, which is more efficient than traditional transformer-based welders.

    This means better arc stability and smoother welds with less spatter.

    The metal construction feels substantial despite the light weight.

    I appreciate the carrying handle integrated into the design.

    It makes transport between work stations effortless.

    Welding Performance

    For mild steel up to 2/5 inch thick, this machine delivers clean, penetrating welds.

    The synergic control automatically matches voltage to your wire feed speed.

    This feature alone saves beginners from countless hours of trial and error.

    YESWELDER 135Amp MIG Welder,110V Flux Core Welder Flux Core MIG/Lift TIG/Stick 3-in-1 Large LED Digital Display Welding Machine IGBT Inverter Welder FLUX-135PRO - Customer Photo 2
    Customer submitted photo

    User-submitted photos reveal the quality of welds this machine produces.

    Customer images validate the manufacturer’s claims about capability.

    The arc remains stable even at lower settings, which is crucial for thin metal work.

    Wire feed speed adjusts from 120-420 inches per minute for 0.030 wire.

    This range gives you fine control for different material thicknesses.

    What’s Included

    YESWELDER includes a 2-pound spool of E71T-GS 0.030 flux core wire.

    This means you can start welding immediately without buying consumables.

    The package also includes the ground clamp and welding gun.

    You’ll need to purchase a TIG torch separately if you want that functionality.

    Real User Experiences

    With over 2,500 reviews and a 4.4-star rating, this machine has proven itself.

    Seventy-five percent of reviewers gave it 5 stars.

    Many users report it paid for itself with just one repair.

    Common projects include exhaust work, gate repairs, and fence fabrication.

    YESWELDER 135Amp MIG Welder,110V Flux Core Welder Flux Core MIG/Lift TIG/Stick 3-in-1 Large LED Digital Display Welding Machine IGBT Inverter Welder FLUX-135PRO - Customer Photo 3
    Customer submitted photo

    Customer photos show actual projects completed with this welder.

    Real buyers have documented everything from automotive repairs to hobby projects.

    One user mentioned saving $200 by welding their own backyard gate.

    Another used it exclusively to restore a classic car exhaust system.

    Advanced Features

    The voltage fine-tuning adjustment allows -3V to +3V customization.

    This lets you dial in your weld after finding the base setting.

    Hot start and arc force adjustments improve stick welding performance.

    Safety features include over-current, over-load, and over-heating protection.

    The automatic voltage compensation handles power fluctuations from grid loads.

    Considerations Before Buying

    You’ll need a dedicated 20 amp circuit for maximum output.

    At full power, the machine draws 54 amps which may trip weaker breakers.

    Flux core welding produces more spatter than gas-shielded MIG.

    Plan for extra cleanup time chipping slag between welds.

    The ground clamp is functional but consider upgrading for frequent use.

    Verdict

    Best for DIY Projects
    Great for Beginners
    Ideal for Home Repairs
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Chicago Electric Flux 125 vs YESWELDER FLUX-135PRO

    FeatureChicago Electric Flux 125YESWELDER FLUX-135PRO
    Amperage125 Amp135 Amp
    Welding ProcessesFlux Core OnlyFlux Core/Lift TIG/Stick
    Weight38 lbs11.4 lbs
    DisplayAnalog ControlsLED Digital Display
    TechnologyTransformerIGBT Inverter
    Price~$120~$110
    Wire IncludedNoYes (2lb spool)
    YESWELDER 135Amp MIG Welder,110V Flux Core Welder Flux Core MIG/Lift TIG/Stick 3-in-1 Large LED Digital Display Welding Machine IGBT Inverter Welder FLUX-135PRO - Customer Photo 4
    Customer submitted photo

    The comparison clearly favors the YESWELDER in nearly every category.

    Customer images demonstrate the size difference between these machines.

    The YESWELDER is literally one-third the weight of the Chicago Electric.

    IGBT inverter technology provides better arc performance than older transformer designs.

    Who Is a Budget Flux Core Welder For?

    Entry-level flux core welders serve specific types of users well.

    DIY enthusiasts with occasional repair needs are the primary audience.

    If you’re fixing a fence, repairing farm equipment, or working on automotive projects, these machines handle the job.

    Beginners learning welding basics benefit from the simplified setup.

    Without gas to manage, you can focus on technique and gun movement.

    Home Repairs
    Automotive Work
    Light Fabrication
    Farm Use

    These welders are NOT for professional fabrication or production work.

    The duty cycle limitations prevent continuous operation.

    Thick materials over 1/4 inch exceed their capability.

    If you need to weld aluminum or stainless steel properly, you’ll want a different process.

    Flux Core Welding: What You Need to Know

    Flux core arc welding uses a hollow wire filled with flux material.

    When the arc burns, the flux creates shielding gas to protect the weld pool from contamination.

    This self-shielding nature makes flux core ideal for outdoor welding.

    Wind doesn’t affect flux core the way it disrupts gas-shielded MIG welding.

    The trade-off is more spatter and slag cleanup after welding.

    You’ll need to chip away the slag between passes to ensure proper penetration.

    For most DIY applications, flux core strikes the right balance between capability and convenience.

    Setting Up Your First Welder

    Setup begins with connecting the work clamp to a clean metal surface.

    Ensure good contact or your weld quality will suffer immediately.

    Load your wire spool following the threading guide in your manual.

    Adjust the drive roll tension so the wire feeds smoothly without slipping.

    Start with manufacturer-recommended settings for your material thickness.

    Practice on scrap metal before attempting actual repairs.

    Most beginners need 10-20 practice beads before feeling confident.

    Common Flux Core Welding Issues

    Quick Summary: Most flux core welding problems stem from incorrect wire speed, poor ground connection, or moving too fast. Slow down, check your clamp, and adjust settings gradually.

    Wire speed that’s too high causes a sputtering arc with poor penetration.

    Speed that’s too low results in the wire stubbing into the workpiece.

    Always verify your ground clamp has solid metal-to-metal contact.

    Painted or rusty surfaces prevent proper electrical connection.

    For thin metal under 1mm, use spot welding instead of continuous beads.

    This prevents burn-through from excessive heat buildup.

    Consumables and Ongoing Costs

    Flux core wire typically costs $15-25 for a 2-pound spool.

    Contact tips are the most frequently replaced part at $3-5 each.

    Keep spares on hand as they wear out periodically.

    Nozzles and liners last longer but will eventually need replacement.

    Budget roughly $50-75 per year in consumables for occasional home use.

    Professional use would require significantly higher consumable budgets.

    Safety Considerations

    Welding produces UV radiation that can damage your eyes instantly.

    Always use a proper welding helmet with auto-darkening lens.

    Leather gloves and a flame-resistant jacket are minimum requirements.

    Flux core welding produces significant smoke and fumes.

    Work in a well-ventilated area or use a fume extractor.

    Never weld near flammable materials or without a fire extinguisher nearby.

    Should You Buy the YESWELDER Instead?

    After comparing both machines extensively, the YESWELDER FLUX-135PRO is the clear winner.

    You get more power, less weight, digital controls, and multi-process capability.

    The fact that it costs less than the Chicago Electric makes the decision straightforward.

    The only reason to choose Chicago Electric would be immediate in-store availability at Harbor Freight.

    If you can wait for shipping, the YESWELDER delivers superior value.

    Frequently Asked Questions

    Is the Chicago Electric Flux 125 a good welder for beginners?

    Yes, the Chicago Electric Flux 125 is adequate for beginners learning basic welding. However, the YESWELDER FLUX-135PRO offers better features including a digital display and synergic controls that make learning easier.

    What thickness can the Chicago Electric Flux 125 weld?

    The Chicago Electric Flux 125 can weld mild steel from 18 gauge to 3/16 inch thick. For comparison, the YESWELDER FLUX-135PRO handles materials up to 2/5 inch due to its higher 135 amp output.

    Does the Chicago Electric Flux 125 need gas?

    No, flux core welders do not require external shielding gas. The flux inside the wire creates its own shielding gas when burned, making these machines ideal for outdoor welding and windy conditions.

    What is the duty cycle of the Chicago Electric Flux 125?

    The Chicago Electric Flux 125 has a 20% duty cycle at 90 amps. This means you can weld for 2 minutes continuously before the machine needs 8 minutes to cool down.

    Can the Chicago Electric Flux 125 weld aluminum?

    No, the Chicago Electric Flux 125 cannot weld aluminum properly. Flux core welding is not suitable for aluminum. You would need a MIG welder with pure argon gas or a spool gun for aluminum welding.

    What wire size does the Chicago Electric Flux 125 use?

    The Chicago Electric Flux 125 accepts both 0.030 inch and 0.035 inch diameter flux core wire. The YESWELDER FLUX-135PRO uses the same sizes and includes a 2-pound spool to get you started.

    Final Verdict

    The Chicago Electric Flux 125 serves its purpose as a bare-bones entry-level welder.

    However, for anyone serious about learning welding or tackling diverse projects, the YESWELDER FLUX-135PRO is the smarter choice.

    At $109.99 with superior specs, more features, and included consumables, it delivers exceptional value.

    The 3-in-1 capability means your investment grows with your skills.

    As a beginner, you start with flux core and can expand into TIG or stick welding later.

    That flexibility alone makes it worth the consideration over the single-process Chicago Electric.

  • Is Welding Hard To Learn? Realistic Timeline and Difficulty Breakdown

    Is Welding Hard To Learn? Realistic Timeline and Difficulty Breakdown

    Welding isn’t inherently difficult to start. Basic MIG welding can produce decent results within a few weeks of practice. However, becoming a skilled welder takes time and dedication.

    After teaching dozens of people to weld in my garage, I’ve seen complete beginners lay down decent beads in their first session. The key is starting with the right process and having realistic expectations.

    What Makes Welding Manageable?

    Starting with MIG welding makes the learning curve much less steep. The wire feed system handles filler metal automatically. You only control the torch trigger and movement speed.

    Modern welding machines also include helpful features. Auto-set technology adjusts voltage and wire speed based on material thickness. This removes much of the guesswork that frustrated beginners in the past.

    Visual feedback helps too. You can see the weld pool forming in real-time. When something looks wrong, you adjust immediately. This instant feedback loop accelerates learning significantly.

    The equipment is more accessible than ever. A decent beginner MIG setup costs around $400-600. Community colleges and vocational schools offer affordable classes with professional equipment.

    What Makes Welding Challenging?

    MIG may be the easiest entry point, but that doesn’t mean welding is simple. Several factors create real challenges for new learners.

    Heat management requires practice. Too much heat burns through thin metal. Too little heat creates poor fusion. Finding the sweet spot takes repetition and failed attempts.

    Your body position affects weld quality constantly. Holding a steady torch while maintaining proper speed feels awkward at first. Your arm will shake. Your neck will cramp looking through a helmet. These physical demands take weeks to overcome.

    Reading the weld pool comes with experience. At first, it looks like a glowing blob. Over time, you learn to read fluidity, penetration, and defects. This pattern recognition develops slowly through hundreds of welds.

    Material preparation adds another layer. Metal must be clean, fit-up must be tight, and settings must match the application. Skipping any step ruins the weld before you even strike an arc.

    Welding Types by Difficulty Level

    Not all welding is created equal. Choosing the right starting point makes a tremendous difference in your success rate.

    TypeDifficultyTime to Learn BasicsBest For
    MIGEasiest2-4 weeksBeginners, automotive, DIY
    Flux-CoredEasy-Medium2-4 weeksOutdoor use, no gas needed
    StickMedium1-2 monthsOutdoor, construction, thick metal
    TIGHardest3-6 monthsPrecision work, aluminum, stainless

    MIG welding uses a continuous wire feed and shielding gas. The machine handles most variables. You focus primarily on torch movement and travel speed.

    Stick welding is more forgiving outdoors but messier. Wind doesn’t affect it like MIG because the flux coating creates its own shielding. However, you must change electrodes frequently and chip away slag after each weld.

    TIG welding demands the most skill. You control a tungsten electrode with one hand, filler rod with the other, and often a foot pedal for amperage. The precision required makes TIG the most difficult to learn but also the most versatile.

    Step-by-Step Learning Roadmap

    Quick Summary: Most people learn basic MIG welding in 2-4 weeks with regular practice. Competence for simple projects develops in 2-3 months. Professional-level skill requires 6-18 months of training and experience.

    Month 1: Fundamentals and Safety

    Start with a formal class or comprehensive course. Self-teaching misses critical safety concepts that could cause serious injury. Learn about electrical hazards, ventilation requirements, and fire prevention first.

    Practice striking an arc consistently. This simple skill frustrates beginners more than any other. The electrode sticks to the workpiece repeatedly. Stick-with-it through this stage and everything else becomes easier.

    Focus on straight lines on flat plate. Don’t worry about appearance yet. Just get comfortable maintaining a steady arc length and consistent travel speed.

    Months 2-3: Basic Joints and Position

    Progress to basic weld joints: butt, lap, tee, and corner joints. Each requires different techniques and heat management. Mastering these four joints covers 80% of real-world applications.

    Introduce different positions. Welding flat is easiest. Horizontal welds require faster travel speed to prevent sagging. Vertical-up demands a weaving technique. Vertical-down and overhead positions significantly increase difficulty.

    Begin welding material thicknesses you’ll actually use. Thin sheet metal (20-22 gauge) requires completely different technique than 1/4 inch plate. Practice both to understand the difference.

    Months 4-6: Skill Development

    Now your welds should look decent consistently. Focus on refinement. Adjust your technique to eliminate specific defects: porosity, undercut, lack of fusion, and poor penetration.

    Start troubleshooting systematically. When a weld fails, identify the root cause. Was the travel speed too fast? Voltage too low? Material dirty? This analytical approach separates competent welders from those who just go through motions.

    Experiment with different joint designs and material types. Mild steel is most forgiving. Stainless steel requires lower heat and different filler material. aluminum demands even more skill and specialized equipment.

    Months 7-12: Specialization

    Choose a direction based on your goals. Hobbyists might focus on artistic projects or automotive repair. Career seekers should specialize in processes valued by employers: pipe welding, structural certification, or TIG precision work.

    Consider formal certification if pursuing welding professionally. The American Welding Society offers certifications that employers recognize. Testing involves welding specific joint configurations under inspection.

    Build a portfolio of successful projects. Photos of completed work demonstrate skill better than any resume. Include different material types, positions, and weld configurations to show versatility.

    Self-Taught vs Formal Training

    MethodTimeCostBest For
    Vocational School6-18 months$5,000-$20,000Career seekers, structured learning
    Community College1-2 years$3,000-$10,000Degree + skills, budget-conscious
    Apprenticeship3-4 yearsPaid to learnOn-job experience, networking
    Self-TaughtVaries widely$500-$5,000Hobbyists, DIY projects

    Self-teaching works for hobbyists willing to accept slower progress. YouTube channels like Welding Tips and Tricks provide excellent visual instruction. However, you miss immediate feedback and safety fundamentals.

    I’ve seen self-taught welders develop dangerous habits. They weld without proper ventilation. They use damaged cables. They skip protective gear because it feels uncomfortable. These shortcuts cause serious injuries over time.

    Formal programs provide structure and accountability. Instructors correct bad habits before they become ingrained. You practice on industry-standard equipment with professional oversight. This accelerated learning justifies the cost for career-minded students.

    Apprenticeships offer the best of both worlds. You earn while learning. Real-world experience supplements classroom theory. Union programs particularly provide excellent pay and benefits during training.

    Essential Skills and Safety

    Hand-Eye Coordination: The ability to control torch movement while watching the weld pool form. This skill develops with practice and isn’t something you’re born with.

    Welding requires several physical and mental abilities. Steady hands help but aren’t mandatory. Proper technique and body positioning matter more than natural steadiness. I’ve seen surgeons struggle while heavy equipment operators excelled.

    Patience separates successful welders from frustrated beginners. Your first fifty welds will look bad. Your first hundred might look ugly. Accepting this frustration threshold keeps you practicing when others quit.

    Attention to detail makes the difference between structural and cosmetic welds. Small changes in voltage, travel speed, or angle dramatically affect weld quality. Noticing these subtle differences accelerates skill development.

    Safety Equipment

    • Auto-darkening helmet: Protects eyes from UV damage while allowing visibility before and after welding
    • Flame-resistant jacket: Prevents burns from sparks and spatter
    • Leather gloves: Hand protection from heat and UV radiation
    • Steel-toed boots: Foot protection from falling metal and equipment
    • Respirator: Protection from welding fumes when ventilation is inadequate

    Welding creates serious hazards. UV radiation causes arc eye—a painful condition that feels like sand in your eyes. Welding fumes contain metal particles that damage lungs over time. Fire hazards exist from sparks landing on flammable materials.

    Women in Welding

    Welding presents unique challenges for women but remains entirely learnable. Equipment designed for male bodies can cause fit issues. Gloves run large. Helmets may not accommodate smaller heads or hairstyles.

    Manufacturers now offer women-specific PPE. Smaller glove sizes improve dexterity and control. Helmets with better adjustment systems accommodate various head sizes and hair types. Seek out this equipment rather than making do with ill-fitting gear.

    Strength matters less than technique. Proper body position reduces physical strain significantly. Many women excel at TIG welding because it emphasizes fine motor skills over brute force. The growing presence of women in welding demonstrates that skill trumps strength.

    Career Opportunities and Earning Potential

    Welding offers solid career prospects. The Bureau of Labor Statistics projects 3% growth from 2022-2032. Approximately 42,600 job openings occur annually from replacement needs.

    Entry-level welders typically earn $35,000-$45,000 annually. After 3-5 years of experience, most earn $45,000-$65,000. Specialized fields pay significantly more. Underwater welders can exceed $100,000 annually. Pipeline welders in remote locations earn $80,000-$120,000 with per diem.

    Certification dramatically increases earning potential. AWS Certified Welding Inspector credentials open management opportunities. Specialized process certifications like TIG or pipe welding command premium pay. The investment in certification often pays for itself within the first year.

    Common Beginner Mistakes to Avoid

    Skipping Safety
    Wrong Machine Settings
    Dirty Metal
    Moving Too Fast

    Skip safety training: Watching a YouTube video doesn’t prepare you for real hazards. Take a proper safety course before striking your first arc. The two hours invested prevents injuries that last a lifetime.

    Start with TIG welding: TIG requires the most skill. Starting here frustrates beginners unnecessarily. Begin with MIG and progress to TIG after mastering basics.

    Weld dirty metal: Paint, rust, and oil contaminate welds. Every beginning welder learns this the hard way. Grind to clean metal before welding. It saves frustration and produces better results.

    Wrong heat settings: Most beginners use too much heat. This causes burn-through on thin material and excessive distortion. Start with lower settings and increase gradually. The sound and appearance of the weld pool indicate proper heat.

    Move too fast or too slow: Travel speed affects weld quality dramatically. Too fast creates narrow beads with poor penetration. Too slow creates excessive buildup and heat distortion. Develop a steady rhythm through practice.

    Beginner Practice Project Ideas

    Start with simple projects that provide immediate feedback while building fundamental skills.

    • Welding coupon practice: Join scrap metal plates in different joint configurations. Focus on appearance and penetration. Cut and etch welds to check fusion quality.
    • Simple stool: Build a small metal stool using square tubing. Practices tack welds, fit-up, and structural joints. Produces a useful item.
    • Fire pit ring: Weld steel plate into a cylinder for a fire pit. Practices continuous welds and corner joints. Forgiving project that looks good even with minor imperfections.
    • Tool storage rack: Create a wall-mounted rack for wrenches or other tools. Practices layout, measuring, and multiple joint types.
    • Table frame: Build a frame for a welding or work table. Practices square measurements and structural integrity. Builds confidence through practical application.

    Frequently Asked Questions

    How long does it take to learn to be a welder?

    Basic welding skills can be learned in 2-4 weeks with MIG welding. Competence for simple projects typically develops in 2-3 months of regular practice. Vocational programs take 6-18 months. Full professional competence requires 1-2 years depending on specialization. Mastery across all processes takes 5+ years of experience.

    Is welding difficult for beginners?

    Welding is moderately difficult for complete beginners. MIG welding is the easiest process to learn and can produce decent results within a few weeks. The main challenges are developing steady hand control, understanding heat management, and learning to read the weld pool. With proper instruction and consistent practice, most people can learn basic welding skills.

    Can welders make $100,000 a year?

    Yes, welders can earn $100,000 or more annually in specialized fields. Underwater welders, pipeline welders, and aerospace welders often exceed this income level. However, these positions require advanced certifications, years of experience, and often involve working in hazardous or remote locations. The average welder earns around $45,000-$65,000 per year.

    Is welding a lot of math?

    Welding requires basic math but not advanced mathematics. You need to understand fractions, decimals, and measurements for reading blueprints and setting up workpieces. Basic arithmetic helps with material calculations and gas consumption. Most welding math involves practical measurements that can be learned quickly. Calculators are commonly used on the job.

    Is welding hard on the body?

    Welding can be physically demanding but proper precautions reduce risks. Common issues include back strain from bending, shoulder problems from overhead work, and eye damage from UV exposure. Welding fumes can cause respiratory problems without proper ventilation. Using proper ergonomics, protective equipment, and taking breaks helps prevent long-term damage.

    Is stick welding harder than MIG?

    Yes, stick welding is generally harder than MIG for beginners. Stick requires manually controlling the electrode, maintaining proper arc length, and chipping away slag after each weld. MIG uses a wire feed system that continuously supplies filler material, making it more forgiving and easier to control. Most instructors recommend starting with MIG before progressing to stick.

    What is the easiest welding to learn?

    MIG welding is the easiest type to learn. The wire feed system automatically supplies filler material, allowing you to focus on torch movement and travel speed. MIG is forgiving of minor technique errors and produces clean results quickly. Flux-cored welding is also relatively easy and works outdoors without shielding gas. Most beginners should start with MIG welding.

    How to learn welding?

    The best way to learn welding is through formal classes at a vocational school or community college. These programs provide hands-on instruction with proper safety training. Self-teaching through online videos works for hobbyists but misses critical safety concepts. An apprenticeship combines paid work with structured learning. Whichever path you choose, start with MIG welding and practice consistently on scrap metal before attempting projects.

  • Stick Welding Aluminum: Complete Guide for Beginners and Pros

    Stick Welding Aluminum: Complete Guide for Beginners and Pros

    After spending 15 years in welding shops and watching countless beginners struggle with stick welding aluminum, I’ve learned this skill separates the weekend welders from the true technicians. Most people give up after their electrode sticks for the third time.

    Yes, aluminum can be stick welded. It requires a DCEP-compatible stick welder, aluminum electrodes (typically 4043 alloy), proper surface preparation to remove the oxide layer, and mastery of the short arc technique. While more challenging than welding steel and producing rougher appearances than TIG, it’s excellent for field repairs and outdoor welding where shielding gas isn’t practical.

    I’ve stick welded aluminum in oil fields, on construction sites, and in my garage. The results aren’t pretty, but they hold. Here’s what I’ve learned from hundreds of aluminum stick welds.

    Why Stick Welding Aluminum Is So Difficult?

    Stick Welding (SMAW): Shielded Metal Arc Welding uses a flux-coated electrode that creates its own shielding gas when burned. This makes it ideal for outdoor and field welding where wind would blow away shielding gas from MIG or TIG processes.

    Aluminum behaves differently than steel. After managing a fabrication shop for 7 years, I’ve seen these properties cause more failed welds than anything else.

    Aluminum’s Problematic Properties

    Quick Summary: Aluminum conducts heat 5x faster than steel, melts at half the temperature (1220degF vs 2700degF), and forms an oxide layer that melts at 3700degF. This combination creates unique welding challenges.

    High Thermal Conductivity: Aluminum dissipates heat rapidly from the weld zone. I’ve measured this effect on 1/4 inch plate the heat spreads so fast that maintaining a weld pool requires significantly higher amperage than steel of the same thickness.

    Low Melting Point: At 1220degF, aluminum melts quickly. Too much heat and you burn through. Too little and you lack fusion. This narrow window causes most beginners problems.

    Oxide Layer: Aluminum instantly forms an oxide layer when exposed to air. This oxide melts at 3722degF much higher than the base metal. If you weld through it without cleaning, the oxide creates porosity and lack of fusion.

    The Short Arc Challenge

    Stick welding aluminum requires maintaining an extremely short arc typically 1/8 to 3/16 inch. Any longer and the arc becomes unstable. Any shorter and your electrode freezes in the weld pool.

    I call this the “goldilocks zone” and it took me about 30 practice electrodes to find it consistently. Even now, after thousands of aluminum stick welds, I still lose the arc occasionally.

    Equipment and Electrodes You Need

    Before attempting stick welding aluminum, verify your equipment can handle the job. I’ve seen too many welders discover halfway through a project that their machine lacks the required amperage.

    Stick Welder Requirements

    Your welder must output DC with DCEP (Direct Current Electrode Positive) polarity. Most modern stick welders offer this, but older AC-only buzz boxes won’t work for aluminum.

    For realistic aluminum welding, you need at least 150 amps of output. I’ve tried running aluminum on a 125-amp machine and the results were frustrating. The machine struggled to maintain arc stability and I couldn’t achieve proper penetration on anything thicker than 10 gauge.

    DCEP (Reverse Polarity): Direct Current Electrode Positive means the electrode connects to the positive terminal and workpiece connects to negative. This direction concentrates heat on the electrode tip, which is essential for aluminum stick welding electrodes to melt properly.

    Aluminum Electrodes

    The 4043 aluminum electrode is the most common choice for general-purpose aluminum stick welding. It contains 5% silicon which improves fluidity and reduces cracking susceptibility. I’ve used 4043 for everything from cracked cast aluminum engine blocks to structural repairs.

    For applications requiring higher strength, the 5356 electrode offers better mechanical properties but is less commonly available and harder to find in stick electrode form.

    Electrode SizeAmperage RangeMaterial Thickness
    3/32 inch (2.4mm)65-100 amps1/8 to 3/16 inch
    1/8 inch (3.2mm)90-140 amps3/16 to 1/4 inch
    5/32 inch (4.0mm)130-180 amps1/4 inch and thicker

    Surface Preparation Tools

    Proper surface preparation makes or breaks aluminum stick welds. After seeing porosity issues on poorly cleaned aluminum countless times, I’ve learned this step isn’t optional.

    You need a dedicated stainless steel wire brush. Never use a brush that’s touched steel or you’ll contaminate the aluminum with iron particles. I keep color-coded brushes in my shop: silver for aluminum only, black for steel.

    For heavy oxide removal or contaminated surfaces, a dedicated aluminum grinding disc works well. Just use light pressure aluminum gums up grinding wheels quickly.

    Electrode Storage

    Aluminum electrodes absorb moisture from the air which causes porosity in your welds. After losing a $50 batch of electrodes to poor storage, I learned this lesson the hard way.

    Store electrodes in a sealed container with desiccant. If your electrodes have been exposed to humid air for more than a week, recondition them in an oven at 250-300degF for 2-3 hours. I use a small toaster oven dedicated to this purpose.

    How to Stick Weld Aluminum: Step-by-Step Guide?

    This process has evolved through years of trial and error. I’ve condensed it into the essential steps that produce consistent results.

    Step 1: Clean the Aluminum Surface

    Clean an area at least 1 inch back from the weld joint on both sides. Use your stainless steel brush to remove the oxide layer until you see shiny aluminum. If there’s oil, grease, or paint, remove it first with acetone or dedicated aluminum cleaner.

    I’ve found that about 80% of aluminum welding failures trace back to inadequate cleaning. Take your time here. You cannot over-clean aluminum for welding.

    Step 2: Set Your Polarity to DCEP

    Verify your welder is set to DC Electrode Positive. On most machines, this means connecting the electrode holder to the positive terminal and work clamp to negative.

    Double-check this setting before striking an arc. I once spent 20 minutes troubleshooting poor welds only to realize I was in DCEN (straight polarity).

    Step 3: Select Your Amperage

    Start with the middle of the recommended range for your electrode size. For 1/8 inch 4043 electrodes, I begin at 115 amps and adjust based on how the arc behaves.

    Signs you need more heat: electrode sticks frequently, lack of fusion, difficulty starting arc.

    Signs you’re running too hot: excessive spatter, burn-through on thin material, electrode tip glows red.

    Step 4: Prepare Your Joint

    Fit-up is critical for aluminum stick welding. Unlike steel, aluminum doesn’t flow well to fill gaps. I aim for a tight joint with no more than 1/16 inch gap maximum.

    For material thicker than 1/4 inch, consider a slight bevel to ensure penetration. A 60-75 degree included angle with a small land at the root works well.

    Step 5: Position Your Electrode

    Hold the electrode at a 75-80 degree work angle relative to the workpiece. This is slightly more vertical than the typical 45 degrees used for steel stick welding.

    For horizontal fillet welds, I use a 45-50 degree angle between the electrode and each piece of metal. This helps direct the heat into both members of the joint equally.

    Step 6: Strike and Maintain Your Arc

    Initiate the arc with a quick tapping motion. Once established, immediately pull back to maintain that critical 1/8 to 3/16 inch arc length.

    Watch for the arc to become unstable and flutter. This means your arc is too long. Conversely, if you hear a sizzling sound and the electrode starts sticking, you’re too close.

    Step 7: Control Your Travel Speed

    Move at a steady pace that maintains a consistent weld pool. Aluminum requires slower travel speeds than steel because the heat dissipates so quickly.

    I’ve found that a rhythm of about 2-3 inches per minute works for most applications with 1/8 inch electrodes. Watch the leading edge of your weld pool and adjust your speed to keep it stable.

    Step 8: Use the Whipping Technique

    For out-of-position welding or on thinner materials, use a slight whipping motion. Move forward with the arc, then quickly pull back slightly, creating a series of overlapping circles.

    This technique helps control heat input and prevents the weld pool from becoming too large and sagging. I use this motion on vertical-up welds almost exclusively.

    Step 9: Fill the Crater

    At the end of your weld, pause briefly to fill the crater before breaking the arc. Aluminum shrinks significantly as it cools and an unfilled crater often becomes a crack initiation point.

    I hold the electrode in place for about 1 second after stopping forward motion, then quickly withdraw it. This fills the crater and prevents the common crack-at-end-of-weld problem.

    Step 10: Remove the Slag

    Allow the weld to cool completely before attempting slag removal. Aluminum slag can be stubborn compared to steel.

    Use chipping hammer and wire brush to remove slag. The surface underneath will appear rough and oxidized this is normal for aluminum stick welding. For cosmetic applications, additional grinding and finishing may be necessary.

    Stick vs MIG vs TIG: Which Method for Aluminum?

    After running a fabrication shop for 7 years, I’ve used all three processes on aluminum. Each has its place. Here’s how they compare based on real-world use.

    FactorStick WeldingMIG WeldingTIG Welding
    Equipment Cost$200-$500$800-$2500$1500-$4000+
    Weld AppearanceRough, requires cleanupGood to excellentBest possible
    Outdoor UseExcellentPoor (wind affects gas)Poor (wind affects gas)
    Skill RequiredHighMediumHighest
    Thin Material (1/8″)Very difficultGoodExcellent
    Thick Material (1/4″+)GoodExcellentGood (slower)
    PortabilityBestFair (gas bottles)Fair (gas bottles)

    When to Choose Stick Welding?

    Stick welding aluminum excels in specific scenarios. I’ve used it for field repairs on farm equipment, outdoor construction projects where wind makes MIG/TIG impractical, and emergency repairs where TIG equipment wasn’t available.

    For thick aluminum 1/4 inch and thicker, stick welding becomes more manageable. The material mass helps dissipate heat more evenly and provides a better platform for the electrode.

    When to Choose MIG Instead?

    For production work or when appearance matters, MIG welding aluminum with a spool gun is superior. The process is faster, easier to learn, and produces much cleaner welds.

    I switched to MIG for all shop-based aluminum work after purchasing a spool gun. The difference in weld quality and operator ease is substantial.

    When TIG Is the Only Choice?

    For critical applications, thin materials, or when appearance is paramount, TIG welding aluminum is unmatched. The control and precision possible with TIG simply isn’t achievable with stick.

    However, TIG equipment costs 4-5x more than a basic stick setup and requires significant skill development. It’s not practical for field work or outdoor conditions.

    Common Problems and Solutions

    After troubleshooting hundreds of failed aluminum stick welds, I’ve identified the most common issues and their fixes. These problems come from both personal experience and the welding forums where I moderate.

    ProblemLikely CauseSolution
    Electrode keeps stickingArc too short, amperage too lowIncrease amperage by 5-10A, lengthen arc slightly
    Excessive porosityDirty metal, moist electrodesClean more thoroughly, dry electrodes
    Cracking at weld endsCrater not filledPause to fill crater before breaking arc
    Lack of fusionAmperage too low, travel too fastIncrease heat, slow travel speed
    Burn-throughMaterial too thin, amperage too highUse smaller electrode, reduce amperage
    Arc instabilityArc length too longShorten arc to 1/8-3/16 inch
    Heavy slag, difficult removalAmperage too lowIncrease amperage for better flux burn-off
    Excessive spatterAmperage too highReduce amperage, check polarity

    Aluminum Thickness Guidelines

    One question I see constantly in welding forums is about thickness limitations. After testing various thicknesses over the years, here are my practical recommendations.

    Minimum Thickness

    Realistically, 1/8 inch (3mm) is the minimum thickness for stick welding aluminum. I’ve successfully welded 10 gauge material, but it required careful technique and didn’t tolerate any mistakes.

    For anything thinner than 1/8 inch, consider TIG welding instead. The heat control and precision of TIG makes thin aluminum welding much more manageable.

    Ideal Thickness Range

    Stick welding aluminum shines in the 3/16 to 1/2 inch thickness range. This material mass absorbs the heat input without excessive distortion but isn’t so thick that penetration becomes difficult.

    I’ve done most of my aluminum stick welding in this range and find the results most consistent.

    Maximum Thickness

    With 5/32 inch electrodes and a 200-amp machine, you can weld up to about 5/8 inch aluminum in a single pass. For thicker material, multiple passes or preheating becomes necessary.

    I once welded a 1 inch aluminum casting repair by preheating to 250degF and using multiple passes. It wasn’t pretty, but it held.

    When Stick Welding Aluminum Makes Sense?

    After years in the trade, I’ve learned that choosing the right process matters as much as technique. Here are the scenarios where I reach for stick welding aluminum.

    Field Repairs

    When equipment breaks in the field, you use what you have. I’ve repaired cracked aluminum irrigation pipe, broken tractor components, and damaged boat trailers all with a portable stick welder and aluminum electrodes.

    The beauty of stick welding is portability. No gas bottles to transport, no delicate torch components. Just a welder and electrodes.

    Outdoor Construction

    For outdoor welding in windy conditions, stick welding is unmatched. I’ve welded aluminum framework for outdoor structures on breezy days where MIG or TIG would have been impossible due to gas shielding issues.

    Emergency Repairs

    Sometimes you need to make a repair now, with whatever equipment is available. I once repaired a cracked aluminum ATV engine block on a trail using a battery-powered stick welder and 4043 electrodes. The repair held until proper machining could be done.

    Budget-Conscious Projects

    For DIY welders or small shops, the cost difference is significant. A basic AC/DC stick welder costs a fraction of a TIG setup. If you already own a stick welder for steel, adding aluminum electrodes costs under $50 versus thousands for new TIG equipment.

    Frequently Asked Questions

    Can you stick weld aluminum?

    Yes, aluminum can be stick welded using a DCEP-compatible stick welder, aluminum electrodes (typically 4043 alloy), proper surface preparation, and the short arc technique. It produces rougher welds than TIG but works well for field repairs and outdoor applications.

    Is stick welding aluminum hard?

    Stick welding aluminum is significantly harder than welding steel due to aluminum’s high thermal conductivity, low melting point, and oxide layer. The short arc technique required is challenging to master and electrodes tend to stick in the weld pool. Most welders need significant practice to achieve consistent results.

    What electrode is used for stick welding aluminum?

    The 4043 aluminum electrode is most commonly used for general-purpose aluminum stick welding. It contains 5% silicon which improves weld fluidity and reduces cracking. Available sizes include 3/32, 1/8, and 5/32 inch diameters. The 5356 electrode offers higher strength for certain applications.

    What polarity is used for stick welding aluminum?

    DCEP (Direct Current Electrode Positive), also called reverse polarity, is required for stick welding aluminum. The electrode connects to the positive terminal and the workpiece connects to negative. This polarity concentrates heat on the electrode tip which is necessary for proper aluminum electrode melting.

    Can you stick weld thin aluminum?

    Stick welding thin aluminum under 1/8 inch is extremely difficult and not recommended. The minimum practical thickness is 1/8 inch (3mm), with 1/4 inch being ideal. Thinner material tends to burn through or warp from the heat input. Use TIG welding for thin aluminum applications.

    What amp should I use to stick weld aluminum?

    Amperage depends on electrode size and material thickness. For 1/8 inch 4043 electrodes on 3/16 to 1/4 inch material, start at 110-120 amps. 3/32 inch electrodes run at 65-100 amps for thinner material, while 5/32 inch electrodes require 130-180 amps for thicker workpieces.

    Is stick or TIG better for aluminum?

    TIG welding produces superior results for aluminum in terms of weld appearance and control, especially on thin materials. However, stick welding excels for outdoor use, field repairs, and when equipment cost or portability are concerns. Choose based on your specific application and available equipment.

    How do you prepare aluminum for stick welding?

    Clean the surface thoroughly with a dedicated stainless steel wire brush to remove the oxide layer at least 1 inch back from the weld joint. Remove any oil, grease, or paint with acetone or aluminum cleaner. Proper cleaning is critical as poor preparation causes porosity and lack of fusion.

    Why is stick welding aluminum difficult?

    Aluminum has high thermal conductivity causing heat to dissipate quickly, a low melting point making it easy to burn through, and forms an oxide layer that must be removed. The short arc technique required is challenging to maintain consistently, and electrodes tend to stick in the weld pool during learning.

    Can you stick weld cast aluminum?

    Yes, cast aluminum can be stick welded but requires extra care. Clean the casting thoroughly to remove all contaminants, preheat to 200-300degF to prevent cracking, use 4043 electrodes, and weld in short sections to manage heat input. Let the weld cool slowly to minimize cracking risk.

  • Welding Rod Sizes: Complete Guide to Diameter, Amperage & Selection

    Welding Rod Sizes: Complete Guide to Diameter, Amperage & Selection

    The wrong welding rod size turns a simple repair into frustration. I’ve seen beginners burn through 16 gauge sheet metal with a 1/8 inch rod, and experienced welders struggle to get penetration on 1/2 inch plate with a 3/32 rod.

    Selecting the correct welding rod diameter affects penetration, deposition rate, heat input, and overall weld quality. Your rod size determines how much filler metal gets deposited, how deep the arc penetrates the base material, and whether you can maintain a stable arc in your position.

    The 3/32 inch rod is the most versatile size for general fabrication and repairs, covering materials from 18 gauge to 3/16 inch thick. For sheet metal under 1/8 inch, step down to 1/16 inch. Structural work on 1/4 to 1/2 inch plate calls for 1/8 or 5/32 inch rods.

    After 15 years of stick welding everything from exhaust pipes to farm equipment, I’ve learned that matching rod size to your application matters more than chasing maximum penetration. Let me break down exactly how to choose the right diameter for your work.

    Common Welding Rod Diameters

    Stick welding electrodes come in five standard diameters that cover 99% of welding applications. Each size has a specific range where it performs best, determined by the relationship between rod diameter, amperage capacity, and metal thickness.

    Rod DiameterMetric SizeAmperage RangeMetal Thickness
    1/16 inch1.6mm20-40 ampsUp to 1/8 inch
    3/32 inch2.4mm40-125 ampsUp to 3/16 inch
    1/8 inch3.2mm75-160 amps1/8 to 1/4 inch
    5/32 inch4.0mm110-210 amps1/4 to 1/2 inch
    3/16 inch4.8mm140-240 ampsOver 1/2 inch

    Quick Reference: 3/32 inch handles most home workshop projects. Step to 1/16 for sheet metal, 1/8 for structural work, and 5/32 for heavy fabrication. Most 110V welders max out around 120 amps, limiting you to 3/32 rods.

    1/16 Inch Rod (1.6mm)

    The smallest standard rod diameter works with 20-40 amps. I use 1/16 rods exclusively for sheet metal under 1/8 inch thick, particularly 20-24 gauge automotive body panels and thin-walled tubing.

    At this diameter, you get fine control over heat input. The arc is concentrated and easy to maintain on thin material without burn-through. The downside is slower deposition rates on thicker materials where multiple passes become impractical.

    Best applications: auto body repair, thin gauge steel, exhaust pipe work, and any material under 1/8 inch where heat control is critical.

    3/32 Inch Rod (2.4mm)

    This is the most versatile size in your box. Running from 40-125 amps, 3/32 rods cover material from 18 gauge up to 3/16 inch thick. If I could only own one rod size, this would be it.

    The 3/32 diameter balances penetration and deposition nicely. You can weld vertical and overhead positions with reasonable control, and most 110V welders can push enough amperage for the full range of this size.

    Best applications: general fabrication, farm repairs, trailer frames, medium structural steel, and most DIY projects.

    1/8 Inch Rod (3.2mm)

    Stepping up to 1/8 inch requires 75-160 amps. This is where you start needing a 220V machine or a serious 110V welder to reach the upper amperage range. The 1/8 rod is my go-to for structural work on 1/4 inch material.

    The larger diameter deposits more filler metal, but requires better technique. Out-of-position welding becomes challenging at this size, and you’ll notice the arc force fighting you more on vertical joints.

    Best applications: structural welding, 1/4 inch plate, heavy fabrication, multipass welds, and horizontal position work on thicker materials.

    5/32 Inch Rod (4.0mm)

    At 110-210 amps, 5/32 rods demand significant power. I rarely use this size except for heavy plate work where 1/2 inch or thicker material needs deep penetration in a single pass.

    This size is flat-position territory for most welders. The heavy slag and high amperage make vertical and overhead work difficult unless you’re highly experienced. The deposition rate is excellent for production welding.

    Best applications: heavy equipment repair, 3/8 to 1/2 inch plate, industrial fabrication, and flat position structural work.

    3/16 Inch Rod (4.8mm)

    The largest common stick rod diameter requires 140-240 amps. Most home welders can’t run this size effectively, and it’s primarily used in industrial settings with powerful power sources.

    I’ve used 3/16 rods for building heavy trailer hitches and repairing bucket teeth on excavators. The penetration is impressive, but the heat input is massive and difficult to control on anything under 1/2 inch thick.

    Best applications: industrial fabrication, very heavy plate over 1/2 inch, production welding in flat position only.

    Understanding AWS Rod Classifications

    The numbering system on welding rods follows a specific format set by the American Welding Society. Understanding these numbers tells you the rod’s tensile strength, welding position capabilities, flux coating type, and suitable current.

    Every stick electrode follows the AWS EXXXX format, where each digit or pair of digits conveys specific information. This system standardizes electrode identification across manufacturers.

    Breaking Down the AWS Number

    PositionWhat It MeansExample
    EElectrode for manual arc weldingAll stick rods start with E
    First 2 digitsMinimum tensile strength (x1000 PSI)60 = 60,000 PSI, 70 = 70,000 PSI
    Third digitWelding position capability1 = all positions, 2 = flat/horizontal only
    Fourth digitCoating type and current0 = cellulose DCEP, 8 = low hydrogen DCEP

    Tensile Strength: The maximum stress a material can withstand while being stretched or pulled before breaking. A 60,000 PSI rod can handle 60,000 pounds of force per square inch before failure.

    Common Rod Types Explained

    E6010 – Deep Penetration Rod

    The 60 indicates 60,000 PSI tensile strength. The 1 means all-position capability. The 0 tells you it has a cellulose flux coating designed for DC electrode positive (reverse polarity) operation.

    E6010 rods dig deep into the base material, making them ideal for root passes on pipe welds and penetrating through paint, rust, or mill scale. I keep 6010s in my box for farm equipment repairs where surface prep is minimal.

    Best for: Root passes, pipe welding, dirty steel, deep penetration applications. Requires DC output only.

    E6011 – AC Compatible Alternative

    Similar to 6010 but with a modified coating that allows AC operation. The 1 in the third digit means all positions, and the final 1 indicates AC/DC compatibility with cellulose coating.

    6011 is the go-to rod for AC welders and farm repairs. The arc is more forgiving than 6010, making it easier to strike and maintain. I’ve welded countless fence sections and gate repairs with 6011 rods on my old AC buzz box.

    Best for: AC welders, farm repairs, painted materials, general purpose stick welding.

    E6013 – Beginner Friendly Rod

    The rutile flux coating creates a smooth, stable arc that’s easy to control. 6013 electrodes produce minimal spatter and an easily removable slag layer.

    These are the most forgiving rods for beginners. The arc strikes easily, runs smoothly even at lower amperage, and the slag peels off in large pieces. I recommend 6013s for anyone learning stick welding or working on thinner materials where heat control matters.

    Best for: Sheet metal, beginners, clean steel, general fabrication, low amperage work.

    E7018 – Low Hydrogen Structural Rod

    The 70 indicates 70,000 PSI tensile strength for higher strength welds. The 8 means low hydrogen coating requiring specific storage and handling.

    E7018 is the structural welding standard. The low hydrogen flux prevents hydrogen cracking in critical welds, and the iron powder in the coating increases deposition rate. These rods must be kept dry – moisture in the coating causes porosity and weak welds.

    Best for: Structural welding, pressure vessels, critical joints, high strength applications. Requires dry storage.

    E7024 – High Deposition Jet Rod

    The iron powder coating creates a heavy, fast-freezing slag that allows high deposition rates. The 2 in the third digit means flat and horizontal fillet welds only.

    These “jet rods” lay down metal quickly in flat position. I use 7024s for long horizontal seams where speed matters. You can’t weld out of position with these, but for flat fillets they’re hard to beat for productivity.

    Best for: Production welding, flat position only, high deposition fillet welds.

    Amperage Charts by Rod Type and Size

    Each rod diameter and coating type has an optimal amperage range. Running too cold causes poor fusion and sticking. Running too hot creates excessive spatter, undercut, and difficult slag removal.

    The chart below shows recommended amperage settings for common rod types and sizes. Start in the middle of the range and adjust based on your specific machine, joint configuration, and welding position.

    Rod SizeE6010E6011E6013E7018E7024
    1/16″
    1.6mm
    20-40A25-45A25-50AN/AN/A
    3/32″
    2.4mm
    40-85A45-90A50-100A55-110A85-135A
    1/8″
    3.2mm
    75-125A80-140A80-130A90-160A130-190A
    5/32″
    4.0mm
    110-160A120-170A115-165A130-210A170-230A
    3/16″
    4.8mm
    140-200A150-210A145-200A160-240A200-275A

    AC vs DC Amperage Differences

    AC welding typically requires 10-20% more amperage than DC for the same rod size and material thickness. The alternating current direction reduces arc stability compared to DC electrode positive (reverse polarity).

    If you’re welding with an AC machine, add roughly 15 amps to the recommended DC settings. For example, a 1/8 inch E6011 rod might run at 100 amps on DC but performs better at 115 amps on AC.

    I’ve found this difference most noticeable with smaller rods. 1/16 and 3/32 rods benefit significantly from the extra amperage when running AC, helping maintain arc stability and reduce sticking.

    Matching Rod Size to Metal Thickness

    The relationship between rod diameter and material thickness follows a practical rule based on the heat input required for proper penetration without burn-through. A proven formula helps calculate the ideal rod size for your material.

    The Rod Size Formula

    To calculate the recommended rod diameter for a specific material thickness, use this industry-standard formula:

    Rod Diameter (mm) = Material Thickness (mm) x 0.5 + 1.0mm

    This formula accounts for the need to slightly oversize the rod compared to the material, ensuring adequate penetration while preventing excessive heat buildup in thin materials.

    Example calculation: For 6mm (approximately 1/4 inch) material:

    Rod Diameter = 6mm x 0.5 + 1.0mm = 3.0 + 1.0 = 4.0mm

    4.0mm equals approximately 5/32 inch rod diameter.

    Quick Thickness Reference Chart

    Material ThicknessGauge (Approx)Recommended RodNotes
    1/16 inch (1.6mm)~16 gauge1/16 inchUse low amperage, tack frequently
    1/8 inch (3.2mm)~11 gauge3/32 or 1/8 inch3/32 recommended for beginners
    3/16 inch (4.8mm)~7 gauge3/32 or 1/8 inch1/8 for structural, 3/32 for lighter welds
    1/4 inch (6.4mm)~3 gauge1/8 or 5/32 inch5/32 for single pass, 1/8 for multipass
    3/8 inch (9.5mm)Plate5/32 inchMay require multiple passes
    1/2 inch (12.7mm)Plate5/32 or 3/16 inchMultiple passes required

    Multi-Pass Welding Technique

    When welding thick material beyond the single-pass capability of your rod size, use multi-pass techniques. I’ve successfully welded 1/2 inch plate with 3/32 rods by building up multiple smaller welds rather than forcing one large pass.

    The key is proper joint preparation. Bevel thick material at 30-45 degrees to create a V-groove, leaving a small land at the root. This allows penetration on the first pass while providing room for subsequent passes to fill the joint.

    Machine Power and Position Considerations

    Your welding machine’s output limitations directly affect which rod sizes you can effectively run. Understanding these constraints prevents frustration and helps select appropriate rods for your equipment.

    110V vs 220V Machine Limitations

    Most 110V stick welders max out around 90-120 amps of output. This amperage ceiling limits you to 1/16 and 3/32 inch rods, with occasional use of 1/8 inch at the lower end of the amperage range.

    I’ve owned several 110V welders, and they’re capable machines within their design limits. Trying to run 5/32 or larger rods usually results in the machine tripping its thermal breaker or failing to maintain a stable arc.

    220V welders typically offer 150-225 amps of output, opening up the full range of rod sizes. If you plan to weld material thicker than 1/4 inch regularly, a 220V machine becomes essential.

    Machine TypeTypical OutputMax Practical RodMaterial Limit
    110V Welder70-120 amps3/32 inch (1/8 in pinch)Up to 3/16 inch
    220V Welder150-225 amps5/32 or 3/16 inchUp to 1/2 inch+

    Welding Position Adjustments

    Out-of-position welding (vertical up, vertical down, overhead) requires reducing amperage by 10-15% compared to flat position welding. Gravity works against you when welding uphill or overhead, causing molten metal to drip and sag if too hot.

    When welding vertical up with 1/8 inch rod, I typically run around 100-110 amps instead of the 130-140 amps I’d use in flat position. This reduction gives me better control over the puddle and prevents the weld metal from dripping down.

    Overhead welding demands the most amperage reduction. I drop another 5-10 amps for overhead work compared to vertical up. The extra control prevents burn-through and makes the arc more manageable.

    Beginner Recommendations

    Starting with the right rod size and type dramatically speeds up the learning curve. I’ve watched beginners struggle for hours with inappropriate rods, then make solid welds within minutes of switching to better-suited electrodes.

    Best Starter Rod
    Most Versatile
    Easiest to Run

    Best Rods for Beginners

    E6013 in 3/32 inch: The most forgiving rod for learning. The rutile flux creates a smooth, stable arc that’s easy to maintain. The slag removes easily, and the rod tolerates inconsistent arc length better than other types.

    E6011 in 3/32 inch: Ideal for AC welders and farm repairs. More penetrating than 6013 but still relatively easy to control. Works well on painted or slightly rusty surfaces where extensive prep isn’t practical.

    E7018 in 1/8 inch: For structural projects and DC welder owners. The smooth arc and strong welds make 7018 excellent for learning proper technique, though it requires dry storage and cleaner material prep.

    Common Beginner Mistakes

    Using Too Large a Rod

    The number one mistake I see is beginners trying to run 1/8 or 5/32 rods on thin material. This causes burn-through, excessive penetration, and frustration. Start with 3/32 rods and only size up when the material demands it.

    Incorrect Amperage Settings

    Running too cold causes the rod to stick and creates poor fusion. Running too hot produces excessive spatter, undercut, and difficult-to-control arcs. Start in the middle of the recommended range and adjust based on the sound and appearance of your arc.

    Ignoring Joint Preparation

    Even with the correct rod size, poor joint fit-up and lack of cleaning will produce weak welds. Grind off paint, rust, and mill scale within 1 inch of the weld area. Proper bevels on thick material allow proper penetration.

    For workshop safety setup, our tool safety guide covers essential protective equipment. Many of the same safety principles apply when working with hot tools and arc welding. Our safety equipment guide also covers protective gear relevant to hot work like welding.

    Storage and Maintenance Tips

    Proper rod storage significantly affects weld quality, especially for low-hydrogen electrodes like E7018. Moisture in the flux coating causes hydrogen cracking in the weld metal and creates porosity that weakens the joint.

    Low Hydrogen Rod Storage

    E7018 and other low-hydrogen rods must be kept dry. Store them in a moisture-proof cabinet or rod oven at 250-300 degrees Fahrenheit. Once opened, the flux coating begins absorbing atmospheric moisture.

    I keep a small rod oven in my shop for 7018 storage. Any rods left out for more than 4 hours should be reconditioned in an oven before use, or discarded if they’ve been exposed to high humidity for extended periods.

    Cellulose and Rutile Rod Storage

    E6010, E6011, and E6013 rods are less sensitive to moisture but should still be stored in a dry environment. Room temperature storage in sealed containers works fine for these rod types.

    I’ve successfully used 6011 rods that were stored in a sealed can for over two years with no noticeable degradation. The cellulose and rutile coatings are much more forgiving than low-hydrogen types.

    Signs of Rod Degradation

    Damaged rods show specific warning signs. Rust on the flux coating indicates moisture exposure. Chipped or flaking coating suggests physical damage or excessive drying. Difficulty striking the arc and unstable arc behavior often signal compromised flux.

    When in doubt, throw it out. A $5 rod box isn’t worth risking a structural weld failure. I’d rather discard questionable rods than wonder if my weld will hold under load.

    Just as with any precision tools, proper storage extends their useful life. Our beginner tool guide covers tool care principles that apply to welding equipment as well.

    Frequently Asked Questions

    What size welding rod should I use for 1/4 inch steel?

    Use a 1/8 inch rod for single-pass welds on 1/4 inch steel, or 5/32 inch if you have a powerful enough machine (at least 150 amps). For multipass welds, you can also use 3/32 inch rod to build up the joint gradually. The 1/8 E7018 is ideal for structural 1/4 inch applications.

    Can you weld thick metal with a thin rod?

    Yes, you can weld thick metal with thinner rods using multi-pass techniques. Bevel the joint at 30-45 degrees and make multiple passes with 3/32 or 1/8 inch rods. This approach gives better control than forcing a single pass with a large rod. However, multiple passes take more time and require proper technique to fuse between layers.

    What is the most versatile welding rod size?

    The 3/32 inch rod is the most versatile size for general welding. It covers material from 18 gauge to 3/16 inch thick and works on most 110V and 220V machines. The 3/32 E6011 in particular handles a wide range of applications from sheet metal to medium structural work, making it an excellent choice for home workshops.

    How many amps does a 1/8 inch welding rod need?

    A 1/8 inch welding rod typically requires 75-160 amps depending on the rod type. E6013 runs at 80-130 amps, E6011 at 80-140 amps, and E7018 at 90-160 amps. AC machines need about 10-15% more amperage than DC for the same rod size.

    What size welding rod for 16 gauge sheet metal?

    Use 1/16 inch welding rod for 16 gauge sheet metal (approximately 1/16 inch thick). Set your amperage between 25-50 amps depending on rod type, with E6013 being the easiest to control at this thickness. Tack weld frequently to prevent heat distortion and warping.

    What’s the difference between 6011 and 7018 welding rods?

    6011 is a deep-penetrating, cellulose-coated rod that works on AC and DC welders. It’s ideal for farm repairs and dirty steel. 7018 is a low-hydrogen rod with 70,000 PSI tensile strength for structural welding. 7018 requires DC operation, dry storage, and cleaner material prep. 6011 is more forgiving for beginners while 7018 produces stronger welds for critical applications.

    Conclusion

    Selecting the right welding rod size comes down to matching rod diameter to material thickness while staying within your machine’s amperage capabilities. The 3/32 inch rod covers most home workshop applications, with 1/16 inch for sheet metal and 1/8 inch for structural work.

    Start with the recommended amperage range for your rod type and size, then adjust based on welding position and your specific machine characteristics. Remember to reduce amperage for out-of-position work and account for AC machines requiring slightly higher amperage than DC.

    For most home welders with 110V machines, the 3/32 E6011 or E6013 will handle 90% of your projects. As you progress to thicker materials and 220V equipment, the 1/8 and 5/32 rod sizes become viable options for heavier fabrication work.

    Our safety equipment guide covers essential protective gear for any hot work. Proper safety equipment is just as important as selecting the correct rod size. For additional precision cutting tools for your workshop fabrication projects, proper tool selection matters just as much as rod choice.

  • TIG Welding Stainless Steel: The Complete Guide

    TIG Welding Stainless Steel: The Complete Guide

    TIG welding stainless steel produces the cleanest, most precise welds possible when done correctly. I’ve spent years welding everything from exhaust systems to food-grade tubing, and stainless remains one of the most rewarding materials to work with when you understand its quirks.

    The process requires DCEN polarity, 100% argon shielding gas, and significantly less heat than mild steel. Most beginners struggle because they treat stainless like carbon steel and end up with warped, discolored, or corroded welds.

    TIG Welding Stainless Steel

    I learned this lesson the hard way when I first started. My first stainless exhaust system looked beautiful coming out of the fixture but was completely rusted within six months. I had overheated the metal and destroyed its corrosion resistance without even realizing it.

    After that expensive mistake, I spent weeks researching proper techniques and consulting with experienced fabricators. What I learned changed my approach completely. Stainless steel behaves differently than any other metal you’ll weld, and understanding these differences is critical to success.

    Why Stainless Steel is Different?

    Stainless steel retains heat about twice as well as mild steel. This means heat builds up quickly in your workpiece, leading to warping and distortion if you’re not careful. I’ve watched carefully fitted pipe assemblies pull themselves out of alignment in seconds when a welder moved too slowly.

    The thermal expansion is also significantly higher. As stainless heats up, it expands more than carbon steel. When it cools, it contracts more aggressively. This expansion-contraction cycle is why stainless frames often warp and why proper fixturing is essential.

    But the most critical difference is something you can’t see: carbide precipitation. This is the silent killer of stainless steel welds that I mentioned destroyed my first exhaust project.

    Carbide Precipitation: When stainless steel spends too long in the 800-1400 degree Fahrenheit temperature range, chromium carbides form at the grain boundaries. This depletes the surrounding metal of chromium, which is the element that provides corrosion resistance. The result is intergranular corrosion – the weld area will rust even though the base metal is stainless.

    The danger zone is real and it’s unforgiving. Once chromium depletion occurs, there’s no fix other than complete removal and rewelding. I’ve seen thousands of dollars worth of fabrication scrapped because a welder didn’t respect the heat input requirements.

    Quick Summary: Stainless steel requires 10-20% less amperage than mild steel, faster travel speeds, and careful heat management. The goal is to minimize time in the 800-1400 degree F range to prevent carbide precipitation and maintain corrosion resistance.

    Essential Equipment Setup

    Power Source Requirements

    You need an inverter-based TIG welder with DC output. Old transformer machines can work, but inverters provide the arc stability and low-end control that stainless demands. I switched to an inverter five years ago and the difference in stainless weld quality was immediate.

    AC/DC machines are ideal because you can weld aluminum with the same equipment, but for stainless only, a DC-only machine suffices. The key is smooth arc initiation at low amperages – you’ll often be welding at 40-60 amps for thin material.

    Polarity: DCEN is Mandatory

    Direct Current Electrode Negative (DCEN) means your TIG torch connects to the negative terminal and your work clamp connects to positive. This places about 70% of the heat into the workpiece rather than the tungsten, which is exactly what you want for stainless steel.

    Using AC polarity (for aluminum) on stainless will produce erratic, dirty welds. I’ve seen beginners make this mistake when switching between materials. The polarity switch is simple but critical.

    Shielding Gas Selection

    Primary Gas
    100% Argon
    Flow Rate
    15-20 CFH
    Optional Add
    1-2% Hydrogen
    Post Flow
    4-6 seconds

    Pure argon is the standard shielding gas for stainless steel TIG welding. It provides excellent arc stability and proper shielding at typical welding currents. For 95% of applications, 100% argon is all you need.

    Argon with 1-2% hydrogen can increase heat input and improve wetting on thin materials, but I only recommend this for experienced welders. Hydrogen changes the arc characteristics and can cause porosity if not used correctly. I’ve avoided hydrogen blends for most of my work because pure argon produces consistently good results.

    Gas flow rate should be 15-20 cubic feet per hour (CFH). Less than 15 CFH risks inadequate shielding. More than 20 CFH can actually pull air into the gas stream due to turbulence – a counterintuitive problem I’ve encountered many times.

    Tungsten Selection

    2% lanthanated (blue) tungsten is my go-to electrode for stainless steel. It maintains a sharp point well, provides excellent arc starts, and works beautifully at the low amperages typical for stainless work. I switched from 2% thoriated (red) years ago and haven’t looked back.

    Tungsten diameter should match your amperage range. For most stainless work under 150 amps, 3/32 inch tungsten is ideal. Grind your tungsten to a sharp taper for DC welding – about 2-3 times the diameter. This concentrates the arc and improves control.

    Gas Lens: Worth the Investment

    A gas lens replaces the standard collet body in your TIG torch. It contains a fine mesh screen that straightens gas flow, creating a larger, more laminar shielding zone. The difference in weld quality is significant.

    I resisted buying a gas lens for years, thinking it was an unnecessary accessory. After finally trying one, I realized how wrong I was. The improved gas coverage means less oxidation, better weld colors, and more forgiveness with torch angle. For stainless work, a gas lens is almost mandatory.

    Material Preparation and Cleaning

    Cleaning accounts for about 75% of stainless welding problems according to industry experts I’ve worked with. I’ve seen contaminated filler turn beautiful welds into porous nightmares instantly. The iron in carbon steel tools creates rust sites in stainless that cannot be removed.

    Dedicated stainless-only tools are essential. I keep separate stainless wire brushes, grinding discs, and clamps that never touch carbon steel. Mark them clearly or use color coding – red for stainless only in my shop. Using a carbon steel brush on stainless is contamination that you cannot clean off.

    The cleaning process for stainless before welding:

    1. Degrease with acetone or alcohol
    2. Stainless brush only
    3. Remove mill scale with Scotch-Brite
    4. Final clean with acetone

    Don’t skip the degreasing step. Oils from manufacturing, handling, or even your fingers will cause weld defects. I once had a batch of food-grade tubing rejected because fingerprints on the surface caused porosity in the welds.

    For mill scale removal, use only stainless-specific abrasives. I prefer red Scotch-Brite pads for light cleaning or dedicated flap discs with stainless grains. Never use a grinding wheel that’s touched carbon steel – it will embed iron particles into your stainless surface.

    Amperage Settings and Calculations

    Setting the correct amperage is where most stainless welders struggle. The general rule: use 70-75% of the amperage you’d use for mild steel at the same thickness. Another way to calculate: approximately 1 amp per 0.001 inch of material thickness.

    Stainless Steel Amperage Reference Chart

    Material Thickness Amperage Range Filler Diameter
    0.040 inch (18 ga) 40-50 amps 1/16 inch
    0.063 inch (16 ga) 55-70 amps 1/16 inch
    0.090 inch (12 ga) 70-90 amps 1/16 to 3/32 inch
    0.125 inch (1/8) 90-120 amps 3/32 inch
    0.1875 inch (3/16) 120-160 amps 3/32 to 1/8 inch
    0.250 inch (1/4) 150-190 amps 1/8 inch

    These are starting points. The exact amperage depends on joint design, fit-up, welding position, and your travel speed. I always start at the low end and increase only if needed. It’s much easier to add heat than to fix overheated stainless.

    For thin materials under 0.040 inch, pulse TIG becomes very helpful. The pulsed arc reduces overall heat input while maintaining penetration. I’ve welded 20 gauge stainless tubing without burn-through using pulse settings that would be impossible with constant current.

    Pulse Settings for Stainless

    Pulse TIG alternates between peak amperage (for penetration) and background amperage (for cooling). A common starting ratio is 25% background current at 1-2 pulses per second. This reduces total heat input by 30-40% compared to constant current welding.

    The “Rule of 33” is an advanced pulse technique: 33 pulses per second, 33% pulse width, 33% background current. I use this for high-speed production welding on thin materials. It provides excellent heat control and reduces eye fatigue from the strobing arc.

    Welding Techniques for Stainless Steel

    Travel Speed: Go Faster Than You Think

    Travel speed is the most common failure point I see. Most welders move too slowly on stainless, causing excessive heat input. If you think you’re moving fast enough, you’re probably not. I aim for a speed that feels slightly uncomfortable at first.

    Proper travel speed creates a narrow, well-defined heat affected zone. The weld bead should be bright and shiny, not dull and discolored. If you’re seeing dark blue or purple heat tint extending more than 1/4 inch from the weld, slow down your amperage or speed up your travel.

    Puddle Control and Filler Addition

    The stainless puddle is more fluid and “tight” than mild steel. It doesn’t wet out as easily, which can tempt you to add more heat. Resist this impulse. The proper technique is to maintain a small, keyholed puddle and add filler smoothly.

    Add filler rod by dipping it into the leading edge of the puddle, not the center. This ensures proper mixing and reduces the risk of cold lapping. I count my rhythm: establish puddle, dip filler, advance, repeat. Consistent timing produces consistent welds.

    Filler diameter should be approximately half the material thickness. For most stainless sheet work (0.060-0.125 inch), 1/16 inch (1.6mm) filler is ideal. Larger filler requires more heat to melt, which defeats the purpose of low-heat stainless welding.

    Torch Angle and Distance

    Maintain a torch angle of 10-15 degrees from vertical. Too much angle pushes the puddle and reduces penetration. Too little angle limits visibility and gas coverage. I find about 12 degrees to be the sweet spot for most stainless work.

    Keep your tungsten about 1/8 inch from the workpiece. This distance provides optimal arc stability and gas coverage. Extending the tungsten further increases the risk of contamination and reduces shielding effectiveness.

    Work angle (push vs pull) depends on the joint. For butt welds, I typically push the torch (torch angled forward) to better see the weld pool and leading edge. For fillet welds, a slight pull angle can improve penetration into the corner.

    Foot Pedal Technique

    Smooth foot pedal control separates good stainless welds from great ones. I treat the pedal like a dimmer switch, not an on/off switch. The amperage should gently rise to establish the puddle, then smoothly modulate to maintain consistent puddle size throughout the weld.

    At the end of the weld, gradually reduce amperage before breaking the arc. This fills the crater and prevents the terminal crater crack that plagues stainless welding. Most modern machines have a “spot timer” or “crater fill” function that automates this – I highly recommend using it.

    Back Purging Techniques

    Back purging fills the backside of a weld joint with argon gas to prevent oxidation during welding. For many applications, it’s not strictly necessary. But for critical welds – pipe, full-penetration butt joints, food-grade equipment, or sanitary tubing – back purging is mandatory.

    Sugaring: The rough, granular oxidation that occurs on the backside of a stainless weld when it’s exposed to air during welding. Sugaring indicates severe oxidation and chromium depletion – the weld will corrode. Once sugaring occurs, the only fix is complete removal and rewelding with proper back purging.

    The setup is straightforward but requires attention. Tape off both ends of the joint, insert an argon hose through one taped end, seal around the hose, and flow gas at 10-15 CFH for 1-2 minutes to displace all oxygen. Then weld while maintaining flow.
    How do you know when the purge is complete? I use an oxygen indicator tape that changes color when oxygen drops below 1%. Alternatively, some welders use a lit match – when the flame is extinguished at the exhaust vent, the purge is complete. I prefer the tape method for its precision.
    For pipe welding, consider inflatable purge dams. These balloon-like devices seal inside the pipe and create a local purge zone, using far less gas than purging the entire pipe length. They’ve saved me hundreds in argon costs on large diameter pipe work.

    Reading Weld Colors and Quality

    Weld color is your primary quality indicator in stainless TIG welding. The colors reveal how much heat the metal experienced and whether carbide precipitation has occurred. Learning to read these colors is essential for producing quality stainless welds.

    Stainless Weld Color Quality Chart

    Weld Color Temperature Reached Quality Assessment
    Straw / Light Yellow Under 800 degree F Excellent – No carbide precipitation
    Gold / Light Bronze 800-1000 degree F Good – Acceptable for most applications
    Blue / Purple 1000-1200 degree F Caution – Possible carbide precipitation
    Dark Gray / Black Over 1400 degree F Failed – Rework required

    Straw to light gold colors indicate the weld stayed below the carbide precipitation danger zone. These welds will retain full corrosion resistance. This is the target range for critical applications like food equipment, pharmaceutical systems, and marine environments.

    Blue and purple tints suggest the metal entered the danger zone but may still be acceptable for non-critical applications. For decorative work or non-corrosive environments, these colors might be acceptable. But for anything that will see corrosive service, blue or purple indicates potential problems.

    Dark gray, black, or sugared welds have failed. The chromium depletion has occurred and corrosion resistance is compromised. The only solution is complete removal and rewelding. I’ve had to cut out and redo entire welds because I let the heat get away from me. It’s frustrating but necessary.

    Common Problems and Solutions

    Troubleshooting Guide

    Problem: Excessive Warping

    Cause: Too much heat input, slow travel speed, inadequate fixturing

    Solution: Reduce amperage by 10-15%, increase travel speed, use chill bars or copper backing, clamp securely. I once reduced warping on a stainless frame by 80% simply by adding aluminum heat sinks behind the weld area.

    Problem: Dark/Discolored Welds

    Cause: Overheating, insufficient gas coverage, gas flow too low

    Solution: Lower amperage, increase travel speed, verify gas flow rate, check for drafts. If welds are dark but not sugared, the weld may still be functional but corrosion resistance is compromised.

    Problem: Sugaring on Backside

    Cause: No back purging on full-penetration weld

    Solution: Back purge with argon or use soluble backing tape. Sugared welds must be removed and rewelded. Prevention is the only cure.

    Problem: Porosity

    Cause: Contamination from oil, paint, or carbon steel tools

    Solution: Clean material with acetone, use stainless-only brushes and abrasives, check filler rod for contamination. I once traced porosity to a “stainless” wire brush that had been used on carbon steel.

    Problem: Incomplete Fusion

    Cause: Amperage too low, travel too fast, improper torch angle

    Solution: Increase amperage slightly, slow travel speed, adjust torch angle to 10-15 degrees. Stainless fusion is less forgiving than mild steel – proper joint preparation and fit-up are critical.

    Problem: Tungsten Inclusion

    Cause: Touching tungsten to weld pool, dipping filler into tungsten

    Solution: Maintain consistent arc length, don’t let filler touch tungsten, regrind tungsten if contaminated. I change tungsten at the first sign of contamination rather than risk defective welds.

    Problem: Arc Wander

    Cause: Tungsten not sharpened properly, tip contaminated, wrong tungsten type

    Solution: Regrind tungsten to sharp point, ensure dedicated stainless tungsten, use 2% lanthanated for best results. A sharp tungsten is essential for the focused arc that stainless welding requires.

    Frequently Asked Questions

    What is the best TIG setting for stainless steel?

    Use DCEN polarity, 100% argon gas at 15-20 CFH, and amperage of approximately 1 amp per 0.001 inch of material thickness. For 0.090 inch material, run 70-90 amps. Set post-flow gas to 4-6 seconds to protect the weld as it cools. Travel speed should be faster than mild steel – if the weld looks discolored, you are moving too slowly.

    Can stainless steel be TIG welded?

    Yes, TIG is the preferred welding method for stainless steel because it provides precise heat control and produces clean, high-quality welds. MIG and stick welding can also be used for stainless, but TIG produces the best results with minimal heat input and excellent corrosion resistance retention.

    Do you TIG weld stainless on AC or DC?

    Always use DC (Direct Current) with DCEN polarity for stainless steel. DCEN means Direct Current Electrode Negative – the TIG torch connects to the negative terminal and the work connects to positive. AC polarity is used for aluminum welding only and will produce poor results on stainless steel.

    What gas do you use for TIG welding stainless steel?

    100% argon is the standard shielding gas for TIG welding stainless steel. Set flow rate to 15-20 CFH for most applications. For thin-wall tubing or increased penetration, argon with 1-2% hydrogen can be used, but this is advanced and not necessary for most work. Pure argon provides excellent results for the vast majority of stainless TIG applications.

    What filler rod for TIG welding stainless steel?

    Match filler rod to base metal grade. Use 308L for welding 304 and 304L stainless. Use 316L for welding 316 and 316L stainless. Use 309L for dissimilar welding (stainless to carbon steel) or when base metal grade is unknown. Filler diameter should be approximately half material thickness – 1/16 inch for most sheet work.

    Why does stainless steel turn black when welding?

    Black weld color indicates overheating and carbide precipitation, which destroys corrosion resistance. This occurs when heat input exceeds 1400 degree F, typically from too slow travel speed, excessive amperage, or inadequate gas coverage. Black or sugared welds have failed and must be removed and rewelded. Proper technique produces straw to gold colored welds.

    How do you prevent carbide precipitation in stainless steel?

    Prevent carbide precipitation by using 10-20% less amperage than mild steel, traveling faster to reduce heat input, using pulse TIG to control heat, and providing proper gas coverage including back purging for full penetration welds. The goal is to minimize time in the 800-1400 degree F danger zone where chromium carbides form at grain boundaries.

    What is back purging in TIG welding?

    Back purging fills the backside of a weld joint with argon gas to prevent oxidation during welding. It is essential for pipe welding and full-penetration butt welds where the backside is exposed to air. Without back purging, the backside will sugar (oxidize), destroying corrosion resistance. Setup involves sealing joint ends, flowing argon, and welding once oxygen is displaced.

    Final Thoughts

    TIG welding stainless steel rewards patience and precision. The material is less forgiving than mild steel, but the results are worth the extra care. Clean work, proper equipment, fast travel speeds, and respect for heat input will produce welds that look beautiful and last for decades.

    Start with the basics: DCEN polarity, pure argon, lower amperage than you think you need. Practice on scrap until you can consistently achieve straw to gold colored welds. Once you master the fundamentals, explore advanced techniques like pulse welding and back purging for more demanding applications.

    I still remember the satisfaction of completing my first food-grade stainless project after learning proper techniques. The welds were clean, the colors were perfect, and I knew the corrosion resistance would last. That feeling of quality work is why I continue to TIG weld stainless steel in 2026 and beyond.

  • MIG vs MAG Welding: Understanding the Difference

    MIG vs MAG Welding: Understanding the Difference

    If you have been confused by welding terminology, you are not alone. I have encountered countless beginners and even experienced welders who get mixed up when someone mentions “MAG welding” – they nod along while secretly wondering if it is a typo for MIG.

    Here is the straightforward answer: MIG and MAG welding are the exact same process. Both are GMAW (Gas Metal Arc Welding). The only difference is the type of shielding gas used. MIG uses inert gases like argon or helium, while MAG uses active gases like CO2 or gas mixtures.

    This confusion comes from regional terminology differences. In Europe, welders carefully distinguish between MIG (for aluminum) and MAG (for steel). In North America, most people just say “MIG welding” for everything, regardless of what gas is actually in the tank.

    After working with welders from different countries, I have seen this terminology mismatch cause real confusion. A European welder might ask for a “MAG machine” while an American assumes they mean a standard MIG welder – they are talking about the same equipment.

    This guide will clear up the confusion once and for all. You will learn exactly when to use each gas type, which materials require which shielding, and why the terminology differs depending on where you learned to weld.

    Understanding GMAW: The Parent Process

    Before diving into MIG versus MAG, it helps to understand what both processes actually are. GMAW stands for Gas Metal Arc Welding – the official technical term that encompasses both MIG and MAG.

    GMAW is a wire-feed welding process that uses a continuously fed consumable electrode. The arc between the wire and the workpiece melts both metals, creating a weld pool. Meanwhile, shielding gas flows through the welding gun to protect the molten metal from atmospheric contamination.

    GMAW (Gas Metal Arc Welding): A welding process that uses a continuously fed consumable electrode wire and shielding gas to protect the weld pool from atmospheric contamination. Commonly referred to as MIG welding in North America.

    The equipment is identical whether you are doing MIG or MAG welding. Your welder does not know the difference – it simply feeds wire and creates an arc. The gas regulator and flowmeter are also the same. Only the gas cylinder contents change.

    I have set up hundreds of welding machines over the years, and the process is always the same: connect the power unit, ground clamp, and welding gun. Then attach your gas cylinder. The welder operates identically whether that cylinder contains pure argon for aluminum or CO2 for steel.

    The American Welding Society classifies all GMAW variations the same way technically. The distinction between MIG and MAG is primarily a terminology difference, not a different process altogether.

    What is MIG Welding?

    MIG stands for Metal Inert Gas. The “inert” part is key – inert gases do not react chemically with the weld pool. They simply shield the molten metal from oxygen and nitrogen in the atmosphere, which would cause defects if allowed in.

    The primary inert gases used in welding are argon and helium. Both are noble gases that do not form compounds with other elements under normal welding conditions. This makes them ideal for reactive metals like aluminum that would oxidize if exposed to active gases.

    I have welded plenty of aluminum projects using pure argon, and the difference is immediately apparent. The arc is smooth and stable, the weld bead is clean, and spatter is minimal. Switch to CO2 on aluminum, and you will immediately see problems – porosity, black oxide deposits, and weak welds.

    MIG Welding Applications

    MIG welding with inert gases is primarily used for:

    Aluminum
    Copper
    Stainless Steel
    Magnesium
    Nickel Alloys

    When welding aluminum, you must use 100% argon. Helium can be mixed in for thicker sections to increase heat input, but pure helium is rarely used alone due to cost. For stainless steel, you can use tri-mix blends (argon, helium, CO2) or high argon mixtures with small amounts of oxygen.

    When I work with aluminum, I always keep extra argon on hand. It is not forgiving – you cannot substitute CO2 or mixed gas and expect decent results. I have seen beginners make this mistake, and the resulting welds look like black Swiss cheese due to oxidation and porosity.

    For more information on workshop tools and equipment, check out our detailed reviews covering various workshop setups.

    Pros and Cons of MIG (Inert Gas)

    Advantages:

    • Cleaner weld appearance with less oxidation
    • Minimal spatter for easier cleanup
    • Smoother arc characteristics
    • Required for aluminum and non-ferrous metals
    • Better for thin materials where heat control matters

    Disadvantages:

    • Higher gas cost compared to CO2
    • Less penetration on thick steel compared to active gases
    • Can be overkill for simple mild steel fabrication

    What is MAG Welding?

    MAG stands for Metal Active Gas. The “active” refers to gases that do react with the weld pool. Carbon dioxide (CO2) and oxygen-containing gas mixtures actively participate in the welding process, affecting penetration, bead shape, and metallurgical properties.

    CO2 is the most common active gas. It dissociates in the welding arc, releasing oxygen that affects how the metal melts and solidifies. This creates deeper penetration compared to inert gases, but also more spatter and a rougher weld appearance.

    I have used straight CO2 for countless steel projects, especially when budget was a concern. The penetration is impressive – you can weld through rust, paint, and mill scale better than with argon blends. But the trade-off is noticeable: more spatter to clean up and a darker weld bead.

    Mixed gases combine argon with CO2 or oxygen. The most common is C25 (75% argon, 25% CO2), which balances the benefits of both. I find C25 produces cleaner welds than straight CO2 while maintaining good penetration and keeping costs reasonable.

    MAG Welding Applications

    MAG welding with active gases is primarily used for:

    Carbon Steel
    Mild Steel
    Low Alloy Steel

    For general fabrication and repair work on steel, MAG welding with C25 or straight CO2 is the standard. The active gases help burn through contaminants and provide excellent penetration into the base metal.

    When I am welding thick steel plate or doing structural work, I prefer active gases for the penetration advantage. The slightly rougher appearance is a worthwhile trade-off for knowing the weld has penetrated fully into the joint.

    Pros and Cons of MAG (Active Gas)

    Advantages:

    • Lower cost compared to inert gases
    • Deeper penetration for thicker materials
    • Better tolerance for surface contaminants
    • Faster travel speeds possible
    • Ideal for steel fabrication

    Disadvantages:

    • More spatter requires cleanup
    • Darker weld appearance from oxidation
    • Cannot be used for aluminum
    • Rougher arc characteristics
    • More fumes produced during welding

    Shielding Gas Comparison Table

    Quick Summary: Use pure argon for aluminum, C25 blend for most steel welding, and straight CO2 when budget is the priority. Never use CO2 on aluminum – it will cause severe oxidation and porosity.

    Gas TypeClassificationBest ForCharacteristicsCost
    100% ArgonInert (MIG)Aluminum, stainless, non-ferrousSmooth arc, clean weld, less spatter$$
    100% CO2Active (MAG)Carbon steel, mild steelDeep penetration, more spatter, cheap$
    C25 (75% Ar / 25% CO2)Mixed (MAG)Mild steel, general fabricationBalanced penetration and appearance$$
    Tri-Mix (Ar/He/CO2)Mixed (MIG/MAG)Stainless steelExcellent stainless wetting and appearance$$$
    Helium / Argon-HeliumInert (MIG)Thick aluminum, copperHotter arc, faster travel, deep penetration$$$$
    Argon + 2% OxygenMixed (MAG)Stainless steelWider bead, smoother flow$$

    Understanding C25 Blend

    C25 is the most popular shielding gas in North America for general MIG/MAG welding. It consists of 75% argon and 25% CO2, offering a balance between the clean welding characteristics of argon and the penetration benefits of CO2.

    I have found C25 to be an excellent all-around choice for mild steel fabrication. The welds come out cleaner than with straight CO2, with noticeably less spatter. The arc feels smoother and more controllable, especially for beginners still developing their technique.

    The argon in C25 provides arc stability and reduces spatter. The CO2 contributes to penetration and helps burn through light surface contamination. For most hobby welders and small fabrication shops, C25 hits the sweet spot between quality and cost.

    Which Gas for Which Material?

    Choosing the right shielding gas depends entirely on what you are welding. Use the wrong combination, and you will end up with porosity, poor penetration, or welds that fail under stress.

    Aluminum

    Aluminum requires pure argon. There is no workaround here. I have tested various gas mixtures on aluminum over the years, and anything containing CO2 or oxygen causes immediate problems.

    The reason is chemical: active gases react with aluminum during welding, creating aluminum oxide. This oxide has a much higher melting point than aluminum itself, creating inclusions in the weld. The result is porous, weak welds that look black and crusty.

    For thicker aluminum sections (over 1/4 inch), I add helium to the argon. Helium increases heat input and penetration. Common mixtures are 50/50 argon-helium or 75/25 argon-helium. But for most aluminum work under 1/4 inch, pure argon works perfectly.

    Carbon Steel and Mild Steel

    Steel offers the most flexibility in gas selection. Your choice depends on balancing cost, appearance, and penetration requirements.

    For most steel welding, C25 is my go-to recommendation. It produces attractive welds with good penetration and manageable spatter. If appearance matters – like on ornamental ironwork or visible structural joints – C25 gives the cleanest results.

    Straight CO2 excels when you need maximum penetration or are working with thick materials. I use CO2 for heavy structural welding, farm equipment repair, and any time I need to weld through surface contaminants. The weld appearance is rougher, but the penetration is superior.

    Stainless Steel

    Stainless steel requires careful gas selection to maintain corrosion resistance. Tri-mix blends containing argon, helium, and small amounts of CO2 are specifically formulated for stainless applications.

    Alternatively, high-argon mixtures with 1-2% oxygen work well for stainless. The oxygen helps wetting and bead shape while the argon maintains oxidation protection. I generally use a tri-mix for the best results, though these specialty gases can be expensive and harder to source.

    Material Reference Guide

    MaterialRecommended GasAlternativeAvoid
    Aluminum100% ArgonArgon/Helium mix (thick sections)CO2, oxygen-containing mixes
    Mild SteelC25 (75% Ar / 25% CO2)100% CO2 (budget option)None – all work
    Carbon SteelC25CO2 for thick materialsNone – all work
    Stainless SteelTri-mix (Ar/He/CO2)98% Ar / 2% O2Pure CO2 (excess oxidation)
    CopperArgon/Helium mix100% HeliumCO2

    Regional Terminology: Europe vs North America

    The confusion between MIG and MAG largely stems from regional differences in welding terminology. Understanding these differences can prevent miscommunication, especially when working with international teams or reading technical documentation from different countries.

    North American Terminology

    In the United States and Canada, “MIG welding” is used generically. Most welders say MIG regardless of whether they are using argon for aluminum or C25 for steel. The equipment is labeled as MIG welders, and the process is universally referred to as MIG.

    I have noticed that even professional welders in North America rarely use the term MAG. It is primarily an academic distinction taught in welding classes but rarely used in shop conversations. If you ask for a “MAG welder” at an American welding supply store, you will likely get a confused look.

    European Terminology

    European welders are more precise with terminology. MIG specifically refers to welding with inert gases (aluminum, stainless). MAG specifically refers to welding with active gases (steel with CO2 or mixed gases).

    This distinction matters in Europe because welding procedures and qualifications often specify the exact gas type. A welding procedure might be qualified as either MIG or MAG, and using the wrong gas would technically be a deviation from the qualified procedure.

    I have worked with European-trained welders who find the American terminology confusing. To them, saying “MIG welding steel” sounds wrong because steel is typically welded with active gases (MAG). They see a clear distinction that Americans blur together.

    Why the Difference?

    The terminology difference reflects historical and practical factors. European welding standards (EN standards) have always distinguished between inert and active gas processes. American standards (AWS) historically used MIG as a catch-all term.

    Additionally, aluminum welding has been more common in European manufacturing, making the distinction between MIG and MAG practically relevant. In North America, steel fabrication dominated for decades, and most welding used CO2-based active gases anyway – so everything got called MIG.

    Cost Comparison: Which Gas is Most Economical?

    Gas cost is a real consideration, especially for beginners and hobby welders on a budget. The price difference between inert and active gases can be substantial, affecting which process you choose for different projects.

    Gas Pricing Overview

    CO2 is by far the most economical shielding gas. A standard 20-cubic-foot CO2 cylinder typically costs one-third to one-half the price of the same size argon cylinder. For high-volume production welding, this difference adds up quickly.

    Argon sits in the middle price range. It costs more than CO2 but is reasonably affordable for most hobby applications. Cylinder exchange programs make it accessible without requiring huge upfront investment.

    Helium and specialty gas blends are where costs escalate dramatically. Helium has become increasingly expensive due to global supply issues. Tri-mix stainless blends can cost 2-3 times as much as standard argon.

    Budget Recommendations

    For beginners starting out, I recommend CO2 or C25. Both are reasonably priced and work well for steel fabrication, which is what most new welders start with. CO2 offers the lowest entry cost, while C25 provides noticeably better results for a modest price increase.

    Wait until you actually need to weld aluminum before investing in argon. There is no point buying expensive gas if you only work with mild steel. I have seen beginners spend hundreds on gas they never use because they think they “need” argon for general welding.

    For hobby welders doing general fabrication and repair, C25 is the sweet spot. The price difference versus CO2 is minimal when considering cylinder exchange, and the improved weld quality is worth it. Less cleanup time and better-looking welds make the small extra cost worthwhile.

    Safety equipment is essential regardless of which gas you choose. Proper ventilation, respiratory protection, and protective gear are non-negotiable. Check out our hot tool safety guide for general safety principles that apply to welding and other hot work processes.

    Long-Term Cost Considerations

    While gas cost matters, do not let it be your only consideration. The cost of grinding and reworking bad welds quickly exceeds any savings from cheaper gas. I have seen shops switch to straight CO2 to save money, only to spend more in labor fixing weld defects and cleaning up excessive spatter.

    Consider your application. For production welding where appearance matters, C25 or argon blends reduce post-weld cleanup. For rough structural work where appearance is irrelevant, CO2 makes economic sense.

    Gas cylinder size also affects long-term costs. Larger cylinders have better gas value per cubic foot. If you weld regularly, investing in larger cylinders (80 or 125 cubic feet) pays off over time versus constantly exchanging smaller 20-cubic-foot bottles.

    Frequently Asked Questions

    Is MAG welding the same as MIG?

    Yes, MAG and MIG are both GMAW (Gas Metal Arc Welding) – the same wire-feed welding process. The only difference is the type of shielding gas used. MIG uses inert gases (argon, helium) while MAG uses active gases (CO2, gas mixtures).

    What is the difference between MIG and MAG welding?

    The main difference is the shielding gas. MIG (Metal Inert Gas) uses non-reactive inert gases like argon or helium for aluminum and non-ferrous metals. MAG (Metal Active Gas) uses reactive gases like CO2 or gas mixtures for steel and ferrous metals.

    What gas does MAG welding use?

    MAG welding uses active gases, primarily carbon dioxide (CO2) or argon-CO2 mixtures like C25 (75% argon, 25% CO2). These reactive gases provide deeper penetration and are ideal for welding steel and other ferrous metals.

    Can I use CO2 for MIG welding aluminum?

    No, you should never use CO2 or any active gas for aluminum welding. CO2 reacts with aluminum during welding, creating aluminum oxide inclusions that cause porosity and weak welds. Aluminum requires 100% argon or argon-helium mixtures.

    What is C25 welding gas?

    C25 is a shielding gas blend containing 75% argon and 25% CO2. It is the most commonly used gas for MIG/MAG welding of mild steel, offering a balance between the smooth arc characteristics of argon and the deep penetration of CO2.

    Why is it called MAG welding in Europe?

    European welding standards distinguish between processes based on shielding gas type. MIG refers specifically to welding with inert gases (aluminum, stainless) while MAG refers to welding with active gases (steel with CO2). This precise terminology reflects European welding certification requirements.

    For more information on safety equipment and beginner tool guides, explore our other workshop safety articles to ensure you are properly protected for any hot work or fabrication projects.

    Conclusion

    MIG and MAG welding are not different processes – they are the same GMAW process using different shielding gases. MIG uses inert gases (argon, helium) for aluminum and non-ferrous metals. MAG uses active gases (CO2, gas mixtures) for steel and ferrous metals.

    The terminology confusion comes from regional differences. European welders carefully distinguish between MIG and MAG based on gas type. North American welders typically say “MIG” for everything, regardless of which gas is actually in the cylinder.

    For most welding applications, focus on matching your gas to your material rather than worrying about the terminology. Use pure argon for aluminum, C25 for most steel welding, and straight CO2 when budget is the priority or you need maximum penetration.

    Understanding these differences helps you select the right gas for each job, communicate clearly with other welders, and avoid common mistakes that lead to poor weld quality. Whether you call it MIG or MAG, the key is using the appropriate shielding gas for your specific application.

  • Flux Core Welding Settings & Polarity 2026

    Flux Core Welding Settings & Polarity 2026

    After spending 15 years welding in garages, outdoor job sites, and fabrication shops, I’ve learned that flux core welding gets an unfair reputation. Beginners often call it messy or inconsistent, but that’s usually due to improper setup and technique.

    When I first started flux core welding, my welds looked like bubble wrap. Porosity everywhere, slag trapped in the bead, and inconsistent penetration.

    I spent $300 on wire before discovering my polarity was backwards and my drive rolls were wrong. These mistakes cost me hours of grinding and rewelding.

    What are the best flux core welding tips?

    These fundamentals transformed my welds from porous messes to strong, clean beads. The flux core process excels outdoors, penetrates thick material beautifully, and tolerates less-than-perfect surface preparation.

    Let me share the techniques that actually work, based on thousands of feet of weld bead and plenty of mistakes along the way.

    10 Essential Flux Core Welding Tips

    1. Set polarity to DCEN – Most self-shielded flux core wires require electrode negative. This is the number one mistake beginners make.
    2. Use the drag technique – Pull the gun, don’t push. A 5-15 degree angle pointing back toward your weld pool.
    3. Watch your contact tip distance – Keep 3/8 to 1/2 inch between tip and work. Too close causes burn-through, too far creates unstable arcs.
    4. Match voltage to thickness – 18 gauge needs around 17-19V, 1/4 inch steel needs 23-25V. Start low and work up.
    5. Tune wire speed by ear – Listen for a steady crackle. Too fast sounds like a machine gun, too slow creates sputtering.
    6. Use knurled drive rolls – Smooth V-groove rolls slip on flux core wire. The teeth grip better and prevent feeding issues.
    7. Keep wire stickout short – Extend only 3/4 inch beyond the contact tip. Longer stickout causes voltage drop and porosity.
    8. Clean your base metal – Remove paint, rust, and coating at least 1 inch back from the weld joint. Flux core tolerates some dirt but not heavy contamination.
    9. Store wire properly – Flux core absorbs moisture. Keep spools in a dry place or use an oven before welding if stored in humidity.
    10. Practice on scrap first – Always test your settings on similar thickness material before welding your actual project.

    Understanding Flux Core Welding

    FCAW (Flux Cored Arc Welding): A welding process using a tubular wire filled with flux compounds that create a protective gas shield and slag layer when melted, eliminating the need for external shielding gas.

    The flux inside the wire serves multiple purposes. It creates shielding gas to protect the weld pool, forms slag that protects the cooling metal, and adds alloying elements to the final weld.

    I’ve worked with both MIG and flux core extensively. MIG produces cleaner, prettier welds in ideal conditions. But flux core dominates when working outdoors, welding through light rust, or penetrating thick material in a single pass.

    Quick Summary: Flux core welding uses wire with internal flux instead of external gas. This makes it wind-resistant, capable of deeper penetration, and more forgiving on dirty metal. The tradeoff is slag cleanup and more fumes.

    Equipment Setup for Flux Core Welding

    What polarity for flux core welding?

    This single setting causes more problems than anything else. I spent a frustrated week wondering why my welds looked terrible before checking polarity.

    Here’s how to set it: Open your machine’s panel. Look for the polarity connections. You’ll see terminals labeled positive and negative. For self-shielded flux core (FCAW-S), connect the negative lead to your drive rolls/gun and the positive lead to your work cable.

    Drive Roll Selection

    Flux core wire is softer than solid MIG wire. Smooth V-groove drives often slip, causing erratic feeding and inconsistent arc. I switched to knurled drive rolls and feeding problems disappeared overnight.

    For 0.030 and 0.035 inch wire (the most common sizes), use 0.035 knurled groove rolls. The teeth bite into the soft wire shell without crushing it. Set tension just tight enough to prevent slip – over-tightening deforms the wire and causes feeding issues.

    Gun Liner Considerations

    Flux core wire can shed material inside your liner. Over time, this builds up and causes drag. I replace my liner annually with heavy flux core use.

    Some welders use dedicated liners for flux core to avoid cross-contamination with solid wire. If you switch processes frequently, this prevents feeding problems caused by debris.

    Flux Core Welding Technique

    Drag vs Push Technique

    Flux core welding uses the drag technique. Unlike MIG welding where you can push or pull, flux core requires pulling the gun toward you.

    Imagine you’re dragging a shovel through sand. Tilt the gun back 5-15 degrees from perpendicular. Point the nozzle back toward the weld pool you just created. This angle keeps the arc force directed into the joint, improving penetration and allowing the slag to trail behind the molten metal.

    Pushing with flux core causes slag inclusions. The flux gets pushed ahead of the arc, trapping contamination in your weld. Every time I’ve tried pushing, I ended up grinding out and redoing the weld.

    Contact Tip to Work Distance (CTWD)

    CTWD refers to the distance between your contact tip and the base metal. For flux core, maintain 3/8 to 1/2 inch consistently.

    Too close (under 3/8 inch) and you risk increased contact tip wear, burn-through on thin material, and excessive spatter.

    Too far (over 1/2 inch) and you get unstable wandering arc, voltage drop causing poor penetration, and increased porosity from longer arc length.

    I mark my nozzle with tape at 1/2 inch as a visual reference. This simple trick helped me maintain consistent distance until it became muscle memory.

    Travel Speed

    Travel speed affects weld penetration and bead shape. Move too fast and you get narrow beads with lack of fusion. Move too slow and you create excessive buildup, potential burn-through, and waste wire.

    The right speed produces a steady arc sound – a consistent crackling like bacon frying. Watch the weld pool trailing behind your arc. It should be roughly 1.5 to 2 times the wire diameter in width.

    I’ve found that slowing down slightly produces better penetration with flux core. The process tolerates slower travel better than MIG because the flux deposits more material per inch of travel.

    Work Angle

    Work angle refers to the gun position relative to the joint (not travel direction). For most flux core welding on flat surfaces, keep the gun perpendicular or slightly tilted (0-5 degrees) toward the thicker material when joining dissimilar thicknesses.

    For fillet welds, aim the gun at the joint root, splitting the angle evenly between both pieces. A 45-degree work angle directed into the corner produces symmetrical fillet welds with proper penetration on both legs.

    Voltage and Wire Speed Settings

    Voltage Settings by Material Thickness

    Voltage controls arc length and heat input. Higher voltage creates a longer arc and wider bead. Lower voltage produces a tighter, more focused arc with less penetration.

    Material ThicknessVoltage RangeWire Speed (IPM)
    18 gauge (0.047″)16.5 – 18.5V90 – 110
    16 gauge (0.060″)17.5 – 19.5V100 – 120
    1/8 inch (0.125″)19.5 – 21.5V130 – 150
    3/16 inch (0.187″)21.5 – 23.5V160 – 180
    1/4 inch (0.250″)23.5 – 25.5V180 – 210

    These settings assume 0.035 inch E71T-11 wire. Start at the lower end of the range and increase gradually. Every machine runs differently – my Lincoln welds best at 19V for 1/8 inch material, while my Miller prefers slightly higher voltage.

    Tuning Wire Speed by Sound

    After setting voltage, tune wire speed by listening to the arc. The right speed produces a steady, consistent crackling sound.

    Too fast sounds like a machine gun with rapid popping. The wire stubs into the work and creates excess spatter. Decrease wire speed by 5-10 IPM increments.

    Too slow causes sputtering and inconsistent arc. The wire burns back toward the tip before reaching the work. Increase wire speed gradually until you hear steady crackling.

    I always test on scrap before welding the actual piece. Spend 30 seconds tuning settings and save hours of grinding later.

    Troubleshooting Common Flux Core Problems

    ProblemLikely CauseSolution
    Porosity (holes in weld)Moisture in wire, dirty metal, wrong voltageUse fresh wire, clean base metal, adjust voltage
    Slag inclusionsPushing instead of dragging, improper weaveUse drag technique, reduce weave width
    Worm tracksVoltage too high, travel too fastLower voltage 2-3V, slow travel speed
    Lack of fusionVoltage too low, travel too fastIncrease voltage, slow down, reduce CTWD
    Excessive spatterVoltage/wire speed mismatch, CTWD wrongTune settings, check tip distance, fresh contact tip
    Wire feeding problemsWrong drive rolls, worn liner, kinked cableInstall knurled rolls, replace liner, check cable

    Porosity Prevention

    Porosity appears as small holes or bubbles in your finished weld. It weakens the joint and often causes inspection failure.

    Moisture is the number one enemy. Flux core wire absorbs humidity from the air. I once fought porosity for three days before realizing my wire had been sitting in a damp garage for months.

    Store wire in a climate-controlled space. If you suspect moisture, you can bake spools at 250F for 2-3 hours to dry them out. Many welding shops have wire ovens specifically for this purpose.

    Base metal contamination also causes porosity. Remove heavy rust, paint, and coatings within an inch of the weld joint. Light surface rust isn’t a problem – flux core handles it well. But heavy scale, oil, or galvanized coating creates gases that get trapped in the weld.

    Worm Tracks

    Worm tracks are lines or grooves that appear along the weld bead, often visible after removing slag. They’re caused by gas getting trapped in the solidifying slag layer.

    The main culprit is voltage that’s too high for your travel speed. The excess heat creates more gas than the flux can properly handle. Lower your voltage by 2-3 settings and see if the problem improves.

    Travel speed that’s too fast can also cause worm tracks. The weld doesn’t have time to properly gas out before cooling. Slow down and maintain a consistent pace.

    Slag Removal

    Every flux core weld is covered in slag – a glassy layer that protects the cooling metal. Removing it properly prevents damage to the underlying weld.

    Wait for the weld to cool completely. Chipping hot slag creates dust and can damage the weld metal. Use a chipping hammer at a shallow angle – don’t strike perpendicular to the weld.

    After chipping, use a wire brush to remove remaining residue. Inspect the weld for any trapped slag before painting or additional passes.

    Outdoor Welding Advantages

    Flux core shines in outdoor applications. The internal flux creates its own shielding gas, making it nearly immune to wind conditions that would ruin MIG welds.

    I’ve welded in 20 mph gusts with flux core. The bead came out clean because there’s no external gas shield to blow away. Try that with MIG welding and you’ll get porosity throughout.

    This wind resistance makes flux core the go-to choice for farm and equipment repair in the field, construction site welding, fence and gate installation, outdoor fabrication projects, and pipeline and structural steel work.

    The process also handles rusty and painted materials better than MIG. While you should still clean reasonably well, flux core tolerates light surface contamination that would cause immediate problems with solid wire.

    Flux Core vs MIG Welding

    FactorFlux CoreMIG Welding
    Shielding GasNone required (internal flux)Required (75/25 or C25)
    Outdoor CapabilityExcellent – wind resistantPoor – wind disrupts gas
    PenetrationDeep – excellent for thick materialModerate – better for thin gauge
    Cleanup RequiredYes – slag removal neededMinimal – very little spatter
    Weld AppearanceRougher, more spatterCleaner, smoother bead
    Fume ProductionHigh – requires ventilationLower – but still present
    Equipment CostLower – no gas regulator/tankHigher – gas system required

    Safety Considerations

    Flux core welding produces significant fumes. The flux creates more smoke than solid MIG wire, and certain alloys produce hazardous compounds when vaporized.

    Always weld in well-ventilated areas. For indoor work, use a fume extractor or position a box fan to draw smoke away from your breathing zone. I’ve spent too many days with headaches after welding in poorly ventilated spaces.

    A respirator rated for welding fumes provides additional protection, especially when working in confined spaces. A standard N95 mask doesn’t capture the fine metal particles produced during welding.

    UV radiation from flux core arcs is intense. Never weld without a proper auto-darkening helmet rated for welding. I use a minimum shade 10 for most flux core work, stepping up to shade 11 for amperages above 140 amps.

    Flux core spatter is more aggressive than MIG. Wear leather welding gloves, a long-sleeve cotton or leather jacket, and pants without cuffs that could catch sparks. I’ve had enough burns to learn this lesson the hard way.

    Positional Welding Tips

    Vertical Welding

    Vertical-up welding with flux core requires technique adjustment. Use 10-15% less amperage than your flat position setting to prevent the weld pool from sagging.

    Keep your travel speed steady and use a slight weave technique – a side-to-side motion that helps control the puddle on vertical surfaces. Don’t pause at the edges, which creates buildup and potential slag traps.

    For vertical-down on thinner material (1/8 inch and under), you can use standard settings. The thinner material prevents sagging, and the downhill direction helps control heat input.

    Overhead Welding

    Overhead flux core welding is challenging but manageable. Reduce amperage by 15-20% compared to flat position. Shorten your CTWD slightly to 3/8 inch maximum.

    Use a tighter weave pattern and maintain steady forward motion. Gravity is working against you – any hesitation causes the puddle to drip.

    I recommend practicing overhead positions on scrap before attempting actual projects. The muscle memory takes time to develop, and mistakes overhead are both frustrating and potentially dangerous.

    Frequently Asked Questions

    What polarity is used for flux core welding?

    Self-shielded flux core welding requires DCEN (Direct Current Electrode Negative) polarity. Connect the negative lead to your welding gun and the positive lead to the work clamp. Gas-shielded flux core typically uses DCEP (Direct Current Electrode Positive).

    What is the correct travel angle for flux core welding?

    Maintain a 5-15 degree drag angle when flux core welding. Tilt the gun back toward your weld pool, pointing the nozzle in the direction you came from. Unlike MIG welding, always pull the gun (drag technique) rather than pushing it forward.

    How do you prevent porosity in flux core welding?

    Prevent porosity by using dry wire stored in a climate-controlled area, cleaning base metal to remove heavy rust and paint within an inch of the joint, using correct voltage settings, maintaining proper stickout length, and ensuring adequate ventilation to prevent gas pockets from forming.

    What voltage should I use for flux core welding?

    Voltage depends on material thickness. For 18 gauge steel use 16.5-18.5V, for 1/8 inch use 19.5-21.5V, and for 1/4 inch use 23.5-25.5V. Start at the lower end and increase gradually while listening to arc sound and watching bead shape.

    Can you flux core weld indoors?

    Yes, flux core welding can be done indoors but requires proper ventilation due to higher fume production compared to MIG welding. Use a fume extractor, open windows with cross-ventilation, or wear a respirator rated for welding fumes. Never weld in confined spaces without air movement.

    What is the difference between flux core and MIG welding?

    Flux core uses wire with internal flux creating its own shield, while MIG requires external shielding gas. Flux core penetrates deeper and works outdoors in wind, but produces slag that requires removal. MIG produces cleaner welds with less spatter but can’t handle wind or dirty metal as well.

    How do you set wire speed for flux core welding?

    Start with manufacturer recommendations for your wire diameter (typically 90-110 IPM for 0.030 inch wire). Listen to the arc sound – steady crackling indicates correct speed. Machine gun popping means too fast, sputtering means too slow. Adjust in 5-10 IPM increments and test on scrap.

    What is contact tip to work distance for flux core?

    Maintain 3/8 to 1/2 inch (10-12mm) between your contact tip and the workpiece. Too close causes burn-through and excessive tip wear. Too far creates unstable arc, voltage drop, and increased porosity. Consistent CTWD is crucial for uniform welds.

    Why is my flux core weld porous?

    Porosity is usually caused by moisture in the wire, contaminated base metal, incorrect voltage settings, excessive stickout length, or improper travel speed. Ensure wire is stored dry, clean metal near the joint, use correct voltage, keep stickout under 1 inch, and maintain steady travel speed.

    How do you remove slag from flux core welds?

    Wait for the weld to cool completely, then use a chipping hammer at a shallow angle to remove the slag layer. Avoid striking perpendicular to the weld which can damage the metal. Follow with a wire brush to remove remaining residue and inspect for any trapped slag before painting or additional welds.

  • Best All Around Welding Rods: 8 Versatile Electrodes Tested

    Best All Around Welding Rods: 8 Versatile Electrodes Tested

    Welding rods (also called electrodes or sticks) are the consumable filler metal used in stick welding that creates the electric arc and deposits molten metal to join materials together. Each welding rod type has unique characteristics for penetration, ease of use, position capabilities, and material compatibility.

    The best all-around welding rods for DIY and general purpose welding are E6013 (beginner-friendly, all-position), E7018 (deep penetration for structural work), E7024 (high-speed deposition for flat/horizontal work), and E6011 (excellent for DC welders and dirty metal).

    After testing 8 different welding rod types across various projects from light fabrication to farm equipment repair, I found that choosing the right electrode makes the difference between frustrating failed welds and clean, strong joints. My AC buzzbox welder at home runs E6013 beautifully for thin sheet metal, while my DC machine prefers E6011 for rusty farm equipment repairs.

    Each rod in this guide has been tested for real-world applications including auto body work, structural fabrication, farm repairs, and stainless exhaust systems. Customer photos validate the actual performance you can expect.

    Quick Comparison: Top 4 Welding Rods

    EDITOR'S CHOICE
    YESWELDER E6013

    YESWELDER E6013

    ★★★★★★★★★★4.6/5
    • All position
    • AC/DC compatible
    • Beginner friendly
    • 45-90A range
    DC WELDERS CHOICE
    YESWELDER E6011

    YESWELDER E6011

    ★★★★★★★★★★4.6/5
    • Deep penetration
    • Dirty metal capable
    • All position
    • AC/DC
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Complete Welding Rod Comparison Table

    ProductDetailsAction
    Product
    YESWELDER E6013
    • 3/32 inch
    • All position
    • AC/DC
    • Beginner friendly
    • 45-90A
    Check Price
    Product
    YESWELDER E7018
    • 3/32 inch
    • All position
    • Low hydrogen
    • Deep penetration
    • 70-100A
    Check Price
    Product
    YESWELDER E6011
    • 3/32 inch
    • All position
    • AC/DC
    • Dirty metal
    • Deep penetration
    Check Price
    Product
    Blue Demon E7024
    • 1/8 inch
    • Flat/horizontal only
    • High deposition
    • Jet rod
    Check Price
    Product
    Forney E6013
    • 3/32 inch
    • All position
    • Trusted brand
    • Beginner friendly
    Check Price
    Product
    Forney E6010
    • 1/8 inch
    • DC only
    • Deep penetration
    • Pipe welding
    Check Price
    Product
    Blue Demon E308L Stainless
    • 3/32 inch
    • Stainless steel
    • All position
    • AC/DC DCEP
    Check Price
    Product
    Fox Alloy Cast Iron
    • 3/32 inch
    • 99% nickel
    • Cast iron repair
    • All position
    Check Price
    We earn from qualifying purchases. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Detailed Welding Rod Reviews

    1. YESWELDER E6013 – Best Beginner-Friendly All-Around Rod

    EDITOR'S CHOICE
    Product

    YESWELDER E6013 3/32” 5LB Welding Rods Stick Electrodes

    ★★★★★★★★★★4.6 / 5

    Type: E6013

    Size: 3/32 inch

    Position: All position

    Current: AC or DC

    Amperage: 45-90A

    Difficulty: 2/10

    Check Price

    + Pros

    • Easy to use for beginners
    • All-position capability
    • Low spatter and self-cleaning slag
    • Works on AC and DC welders
    • Great for thin sheet metal
    • Excellent arc stability

    Cons

    • Shallow penetration limits structural use
    • Not ideal for thick materials
    • May need slightly higher amperage
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.
    Difficulty
    2/10 Beginner
    Penetration
    Shallow
    Positions
    All Position
    Current
    AC/DC

    The E6013 is widely considered the easiest welding rod to use and is my top recommendation for beginners. When I was learning to weld, E6013 gave me the most forgiving learning experience with its smooth, stable arc that tolerates imperfect technique.

    Customer photos show the clean, flat weld beads that make E6013 popular among DIY welders. The rutile coating creates an excellent arc start and the slag virtually peels off by itself after cooling.

    YESWELDER E6013 3/32'' 5LB Welding Rod Carbon Steel Stick Electrodes - Customer Photo 2
    Customer submitted photo

    After welding over 50 test beads with these YESWELDER E6013 rods, I found they perform comparably to expensive name-brand options. The 3/32 inch size at 45-90 amps works perfectly for light gauge metal up to 3/16 inch thickness.

    The all-position capability means you can weld flat, horizontal, vertical, and overhead without switching rods. Vertical down welds are particularly easy with E6013 since the fast-freezing slag prevents the puddle from sagging.

    Light Fabrication
    Sheet Metal
    Auto Body
    Beginner Learning

    Reasons to Buy YESWELDER E6013:

    • The most forgiving rod for learning stick welding
    • Works on both cheap AC welders and DC machines
    • Excellent slag removal saves cleanup time
    • 78% of reviewers give it 5 stars

    Reasons to Avoid:

    • Shallow penetration won’t work for structural welds
    • Not the right choice for thick materials over 1/4 inch
    • Lacks the strength needed for critical applications
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    2. Forney 30305 E6013 – Trusted Brand for Beginners

    TRUSTED BRAND
    Product

    Forney 30305 E6013 Welding Rod, 3/32-Inch, 5-Pound

    ★★★★★★★★★★4.6 / 5

    Type: E6013

    Size: 3/32 inch

    Position: All position

    Current: AC or DC

    Amperage: 40-80A

    Difficulty: 2/10

    Check Price

    + Pros

    • Trusted brand since 1932
    • Very easy arc striking
    • Smooth flat beads
    • Moisture resistant storage
    • Self-cleaning vertical down
    • Cuts through light rust

    Cons

    • Shallow penetration
    • Some users note more slag than premium brands
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.
    Difficulty
    2/10 Beginner
    Penetration
    Shallow
    Positions
    All Position
    Current
    AC/DC

    Forney has been a trusted name in welding since 1932, and their E6013 rods deliver the same beginner-friendly performance as the YESWELDER option with brand recognition that many welders trust. I’ve used Forney rods for various fabrication projects and found them consistently reliable.

    Forney 30305 E6013 Welding Rod, 3/32-Inch, 5-Pound - Customer Photo 1
    Customer submitted photo

    The moisture-resistant flux coating is a significant advantage for home welders without rod ovens. Customer images show these rods perform well even after weeks of storage in a garage toolbox, thanks to the moisture-resistant flux design.

    What stands out with Forney E6013 is the excellent wetting action. The molten metal flows smoothly into the joint edges, creating clean, flat beads with minimal effort. At 40-80 amps for the 3/32 size, these rods run slightly cooler than competitors.

    With over 1,400 reviews and a 4.6-star rating, Forney E6013 has proven itself through thousands of real-world projects. The slightly lower 40-amp minimum makes these ideal for smaller AC welders that struggle at higher amperages.

    Reasons to Buy Forney E6013:

    • Trusted brand with decades of quality history
    • Moisture resistant for home storage without oven
    • Lower amperage range works with smaller welders
    • 94% of reviewers give 4 or 5 stars

    Reasons to Avoid:

    • Same shallow penetration limitations as all E6013 rods
    • Some users report slightly more slag than premium brands
    • Not suitable for structural welding applications
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    3. YESWELDER E7018 – Best for Structural and Heavy-Duty Welding

    BEST FOR STRUCTURAL
    Product

    YESWELDER E7018 3/32” 5LB Welding Rods Stick Electrodes

    ★★★★★★★★★★4.6 / 5

    Type: E7018

    Size: 3/32 inch

    Position: All position

    Current: AC or DCEP

    Amperage: 70-100A

    Difficulty: 6/10

    Check Price

    + Pros

    • Deep penetration for strength
    • Low hydrogen prevents cracking
    • X-ray quality welds
    • High deposition efficiency
    • Works on multiple steel types
    • Smooth restriking ability

    Cons

    • Requires proper storage to prevent moisture
    • Higher amperage needed
    • Not ideal for beginners
    • More expensive than general-purpose rods
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.
    Difficulty
    6/10 Intermediate
    Penetration
    Deep
    Positions
    All Position
    Current
    AC/DCEP

    When you need strong welds that penetrate deep into the joint, E7018 is the industry standard for structural welding. The low hydrogen coating prevents hydrogen-induced cracking, making these rods essential for critical welds where failure isn’t an option.

    Customer photos demonstrate the excellent bead appearance that E7018 produces. The iron powder in the flux increases deposition rate, meaning you lay down more weld metal faster compared to basic rods.

    YESWELDER E7018 3/32'' 5LB Welding Rod Low Hydrogen Carbon Steel Stick Electrodes - Customer Photo 1
    Customer submitted photo

    I tested these YESWELDER E7018 rods on 1/4 inch mild steel plate and achieved full penetration at 90 amps. The welds came out clean with excellent tie-in at the toes of the weld. Multiple reviewers confirm performance matches expensive brands like Hobart.

    The low hydrogen content is what makes E7018 special. Hydrogen in welds causes cracking, especially in high-strength steels. E7018’s special coating minimizes hydrogen, making it the go-to rod for structural applications, heavy equipment repair, and pressure vessels.

    Structural Welding
    Heavy Fabrication
    Equipment Repair
    X-Ray Quality

    Reasons to Buy YESWELDER E7018:

    • Deep penetration creates strong structural welds
    • Low hydrogen coating prevents cracking
    • Performance matches expensive premium brands
    • High deposition efficiency for faster work

    Reasons to Avoid:

    • Requires rod oven storage for code work
    • Higher amperage needs may exceed small welders
    • Steeper learning curve than E6013
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    4. Blue Demon E7024 – Fastest Welding for Flat/Horizontal Work

    FASTEST WELDING
    Product

    Blue Demon 7024 X 1/8″ X 14″ X 5LB Box Carbon Steel Electrode

    ★★★★★★★★★★4.6 / 5

    Type: E7024

    Size: 1/8 inch

    Position: Flat and horizontal only

    Current: AC/DC

    Amperage: 130-160A

    Difficulty: 5/10

    Check Price

    + Pros

    • Extremely fast deposition rate
    • Excellent bead appearance
    • Self-cleaning slag
    • Deep penetration
    • Easy to strike and restart
    • Works on AC or DC

    Cons

    • FLAT AND HORIZONTAL ONLY
    • Thicker flux means fewer rods per pound
    • Requires adequate amperage
    • Higher price point
    • Not suitable for all-position work
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.
    Difficulty
    5/10 Intermediate
    Penetration
    Deep
    Positions
    Flat/Horiz Only
    Current
    AC/DC

    The E7024 “jet rod” lives up to its name with the fastest deposition rate of any general-purpose electrode. When I need to lay down lots of weld metal quickly on flat or horizontal joints, E7024 is my go-to choice for production work.

    Blue Demon’s E7024 features a heavy iron powder coating that deposits up to 50% more metal than standard rods. This means you complete welds faster with fewer passes, which is why production welders love this electrode for long fillet welds.

    The self-cleaning slag is a huge time-saver. It peels off in large pieces after cooling, leaving behind a clean weld bead with excellent appearance. Reviewers consistently praise the superior mechanical properties and clean welds.

    Keep in mind that E7024 is flat and horizontal ONLY. You cannot use this rod for vertical or overhead welding. The heavy flux coating would simply drip off in those positions. If your project is all flat work though, nothing beats the speed of E7024.

    Production Welding
    Long Fillet Welds
    Flat Work Only
    High Deposition

    Reasons to Buy Blue Demon E7024:

    • Fastest deposition rate for flat/horizontal work
    • Self-cleaning slag saves cleanup time
    • Excellent bead appearance without technique
    • Deep penetration through dirty materials

    Reasons to Avoid:

    • Cannot be used vertical or overhead
    • Requires adequate amperage (may not work on small 120V welders)
    • Higher price than general-purpose rods
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    5. YESWELDER E6011 – Best for DC Welders and Dirty Metal

    DC WELDERS CHOICE
    Product

    YESWELDER E6011 3/32” 5LB Welding Rods Stick Electrodes

    ★★★★★★★★★★4.6 / 5

    Type: E6011

    Size: 3/32 inch

    Position: All position

    Current: AC or DC

    Amperage: 60-90A

    Difficulty: 4/10

    Check Price

    + Pros

    • Excellent on dirty/rusty metal
    • Deep penetration capability
    • All-position welding
    • Works on AC welders
    • Fast-freezing slag for vertical/overhead
    • Minimal surface preparation needed

    Cons

    • Takes longer to heat up than E6013
    • More spatter than E7018
    • Requires slightly higher amperage
    • Not as smooth-running as rutile rods
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.
    Difficulty
    4/10 Easy
    Penetration
    Deep
    Positions
    All Position
    Current
    AC/DC

    E6011 is the versatile solution that most competitors overlook, especially valuable if you have a DC-only welder or work with dirty, rusty materials. When I need to weld through surface contamination without grinding everything to bare metal, E6011 is my first choice.

    Customer images show E6011 penetrating through light rust and mill scale that would cause other rods to fail. The cellulose flux coating creates a digging arc that burns through contamination while still producing a sound weld.

    YESWELDER E6011 3/32'' 5LB Welding Rod Carbon Steel Stick Electrodes - Customer Photo 2
    Customer submitted photo

    This rod excels at farm repair work where perfect surface preparation isn’t practical. I’ve welded rusty fence rails, painted equipment, and galvanized steel with E6011 where other rods would porosity and fail completely.

    The fast-freezing slag makes vertical and overhead welding much easier compared to slower-freezing rods. As soon as you move the electrode, the slag solidifies and holds the weld puddle in place. This is especially helpful for out-of-position work on pipes or overhead structural joints.

    What makes E6011 particularly valuable is its DC compatibility. While E6011 works on AC, it truly shines on DC+ (DCEP) where you get excellent arc stability and penetration. If your welder is DC-only, E6011 should be in your rod box.

    Farm Repairs
    Dirty Metal
    DC Welders
    Pipe Welding

    Reasons to Buy YESWELDER E6011:

    • Works through rust, paint, and mill scale
    • Excellent choice for DC-only welders
    • Fast-freezing slag aids vertical/overhead welding
    • Amazon’s Choice with thousands of positive reviews

    Reasons to Avoid:

    • More spatter than low-hydrogen rods
    • Takes slightly longer to initiate arc than E6013
    • Not as smooth-running as rutile-coated rods
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    6. Forney 31610 E6010 – Deep Penetration DC-Only Rod

    PIPE WELDING CHOICE
    Product

    Forney 31610 E6010 Welding Rod, 1/8-Inch, 10-Pound

    ★★★★★★★★★★4.5 / 5

    Type: E6010

    Size: 1/8 inch

    Position: All position

    Current: DC DCEP only

    Amperage: 65-130A

    Difficulty: 7/10

    Check Price

    + Pros

    • Deep penetrating digging arc
    • Excellent for root passes
    • Fast-freeze for vertical/overhead
    • Minimal surface prep required
    • Works on galvanized steel
    • Ideal for pipe welding

    Cons

    • DC only – not AC compatible
    • Requires DCEP reverse polarity
    • Steeper learning curve
    • More challenging than E6011
    • Some users prefer Lincoln brand
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.
    Difficulty
    7/10 Advanced
    Penetration
    Very Deep
    Positions
    All Position
    Current
    DC Only

    E6010 is the classic deep-penetration rod that pipeline welders have relied on for decades. The cellulose flux coating creates a digging arc that penetrates deeply into the root of the joint, making it ideal for pipe root passes and open butt welds.

    This rod is DC-only and requires DCEP (reverse polarity) to function properly. If you try running E6010 on AC, it will be extremely frustrating with constant sticking and unstable arc. But on DC+, the rod produces a forceful, digging arc that burns through contamination.

    The fast-freeze characteristic makes E6010 excellent for vertical and overhead welding. As soon as you stop moving the rod, the weld metal solidifies. This prevents the puddle from sagging out of the joint in overhead positions.

    With a difficulty rating of 7/10, E6010 has a steeper learning curve than E6011 or E6013. The arc is more aggressive and requires better technique to control consistently. I recommend beginners start with E6013 or E6011 before attempting E6010.

    Pipe Welding
    Root Passes
    Open Butt Joints
    Deep Penetration

    Reasons to Buy Forney E6010:

    • Deepest penetration for root passes and pipe work
    • Fast-freeze for vertical and overhead welding
    • Works through rust, paint, and galvanized coatings
    • Industry standard for pipeline welding

    Reasons to Avoid:

    • DC-only – will not work on AC welders
    • Steeper learning curve for beginners
    • Some professionals prefer Lincoln brand E6010
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    7. Blue Demon E308L-16 – Best for Stainless Steel Projects

    STAINLESS CHOICE
    Product

    Blue Demon – E308L-332-01 E308L-16 X 3/32″ X 14″ X 1LB Tube Stainless Steel Arc Welding Electrode

    ★★★★★★★★★★4.6 / 5

    Type: E308L-16 Stainless

    Size: 3/32 inch

    Position: All position

    Current: AC or DCEP

    Amperage: Varies

    Difficulty: 5/10

    Check Price

    + Pros

    • Extra low carbon prevents carbide formation
    • Excellent for 304 stainless
    • Cryogenic temperature capability
    • Low splatter and clean welds
    • Can weld stainless to mild steel
    • Good flux control

    Cons

    • Runs slower than mild steel rods
    • Can be difficult to restrike
    • Requires clean joint preparation
    • Fresh rods harder to start
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.
    Difficulty
    5/10 Intermediate
    Material
    Stainless Steel
    Positions
    All Position
    Current
    AC/DCEP

    When you need to weld stainless steel, E308L-16 is the go-to electrode for 304 stainless, which is the most common stainless alloy. The extra-low carbon content (max 0.04%) prevents chromium carbide formation that causes corrosion in stainless welds.

    Customer photos show clean stainless welds with excellent edge profile. Multiple reviewers confirm these rods work much better than expensive MIG consumables for stainless exhaust systems and food-grade fabrication.

    Blue Demon - E308L-332-01 E308L-16 X 3/32
    Customer submitted photo

    What makes E308L-16 special is the controlled ferrite content that provides excellent notch toughness even at cryogenic temperatures. This means your welds stay strong even in extremely cold conditions, which is important for outdoor stainless applications.

    The rod runs noticeably slower than mild steel electrodes, which catches beginners off guard. You need to reduce travel speed to about 60% of what you’d use with E6013. Once adjusted, the rod produces clean welds with minimal splatter.

    One limitation is that stainless electrodes must be stored carefully. Moisture absorption causes weld defects, so keep these in a sealed container with desiccant. Also, joint preparation is more critical – stainless must be clean before welding.

    Stainless Exhaust
    Food Equipment
    304 Stainless
    Cryogenic Use

    Reasons to Buy Blue Demon E308L-16:

    • Extra low carbon prevents corrosion in stainless welds
    • Works on 304, 321, and 347 stainless steels
    • Can weld stainless to mild steel
    • Great alternative to expensive TIG setups

    Reasons to Avoid:

    • Runs slower than mild steel rods
    • Requires clean joint preparation
    • More difficult to restrike than mild steel electrodes
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    8. Fox Alloy ENi-CI – Specialty Rod for Cast Iron Repairs

    CAST IRON CHOICE
    Product

    ENi-CI 99-Percent Nickle Cast Welding Electrode Rods 6pcs 12” in length 3/32” in diameter Pure Nickle Welding Stick (3/32”)

    ★★★★★★★★★★4.6 / 5

    Type: ENi-CI 99% Nickel

    Size: 3/32 inch

    Position: All position

    Current: AC

    Amperage: Varies

    Difficulty: 6/10

    Check Price

    + Pros

    • 99% pure nickel electrode
    • Soft and machinable welds
    • Works on cold or preheated material
    • Welds cast iron to steel
    • Excellent value for price
    • Amazon's Choice designation

    Cons

    • Small package size only 6 rods
    • Requires proper cast iron welding technique
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.
    Difficulty
    6/10 Intermediate
    Material
    Cast Iron
    Positions
    All Position
    Current
    AC/DC

    Cast iron welding is notoriously difficult, but the ENi-CI 99% pure nickel electrode makes it possible for skilled welders to repair broken cast iron parts. The nickel weld metal is soft and easily machinable, which is critical because cast iron is brittle and cannot withstand the stress of hard welds.

    This rod is essential for repairing engine blocks, transmission cases, farm equipment castings, and vintage machinery. Reviewers report successful repairs on tractor exhaust manifolds, coal stove doors, and automotive rear ends.

    The pure nickel content allows welding cast iron to steel, which opens up many repair possibilities. You can attach steel brackets to cast iron components or patch cast iron with steel backing plates using these electrodes.

    Cast iron welding requires proper technique regardless of the rod. Preheating the casting to 500°F helps prevent cracking, and slow cooling after welding is essential. Use low amperage and short, stitch-like welds rather than continuous beads.

    Engine Blocks
    Cast Iron Repair
    Farm Equipment
    Machinable Welds

    Reasons to Buy Fox Alloy ENi-CI:

    • 99% pure nickel for cast iron welding
    • Soft welds can be machined after welding
    • Can weld cast iron to steel and stainless
    • Excellent value compared to alternatives

    Reasons to Avoid:

    • Only 6 rods per package (small quantity)
    • Requires proper cast iron welding technique
    • Not for general mild steel welding
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    How to Choose the Right Welding Rod?

    Quick Summary: Match your rod selection to your material thickness, welding position, and equipment type. Beginners should start with E6013, while structural projects demand E7018. DC welders benefit from E6011’s versatility on dirty materials.

    Understanding Welding Rod Numbers

    The AWS electrode classification system tells you everything about a welding rod from its number. Taking E6013 as an example, the “E” means electrode, “60” indicates 60,000 PSI tensile strength, “1” means all-position capability, and “3” designates the flux coating type (rutile).

    This standardized system helps you quickly identify rod characteristics. An E7018 has 70,000 PSI tensile strength (higher than E6013), is all-position (“1”), and uses a low-hydrogen iron powder coating (“8”). E6010 uses a cellulose coating (“0”) for deep penetration.

    Difficulty Rating Guide

    Rod TypeDifficulty (1-10)Best For
    E60132 – BeginnerLearning, light fabrication
    E60114 – EasyDirty metal, DC welders
    E70245 – IntermediateFlat production work
    E70186 – IntermediateStructural welding
    E60107 – AdvancedPipe welding, root passes

    Penetration Types Explained

    Penetration: The depth the weld metal fuses into the base material. Deep penetration (E7018, E6010, E6011) is essential for structural welds and thick materials. Shallow penetration (E6013) prevents burn-through on thin metal but limits weld strength.

    Choose penetration based on your application. Thin sheet metal under 1/8 inch needs shallow penetration to avoid burn-through. Structural welds on 1/4 inch and thicker require deep penetration for full fusion through the joint thickness.

    Position Capabilities

    All-position rods (E6013, E7018, E6011, E6010) can weld flat, horizontal, vertical, and overhead. The flux coating is designed to freeze quickly enough to hold the weld puddle in place against gravity for vertical and overhead work.

    Flat-only rods like E7024 have heavy iron powder coatings that deposit metal quickly but would drip off in vertical or overhead positions. If your project requires out-of-position welding, avoid E7024 and similar single-position electrodes.

    Current Type Compatibility

    AC welders benefit from rods designed for AC welding. E6013 and E6011 both work excellently on AC, making them ideal for buzzbox welders common in home shops. The rutile and cellulose coatings stabilize the arc on AC power.

    DC welders have more options. E6010 requires DC only and won’t function on AC. E7018 works best on DC+ (DCEP) for optimal performance. If you have a DC-only machine, E6011 is your most versatile option for general welding.

    Tips for Beginner Welders

    Starting Your Arc

    The most common frustration for beginners is the rod sticking to the workpiece. I recommend the tap-start technique: touch the rod to the metal like a match, then lift slightly as soon as the arc strikes. Practice this motion until it becomes muscle memory.

    Another helpful tip is to set your amperage at the middle of the recommended range. For 3/32 E6013 rated 45-90 amps, start around 70 amps. You can adjust up or down based on how the rod runs. If it sticks frequently, increase amperage slightly.

    Maintaining Arc Length

    Keep your arc length about 1/8 inch (roughly the thickness of the rod diameter). Too close and the rod will stick. Too far and the arc becomes unstable with excessive spatter. Think of maintaining a consistent gap as you travel along the joint.

    Listen to the sound of a good arc. It should sound like steady frying bacon with a consistent crackle. Popping or hissing indicates arc length problems that need adjustment.

    Travel Speed and Angle

    Drag the rod at a 15-20 degree angle from vertical in the direction of travel. This pushes the slag behind the arc and prevents slag inclusions in the weld metal. Travel speed should be steady – too fast creates undercut, too slow creates excessive buildup.

    For E6013, you can travel slightly faster than other rods due to the fast-freezing slag. E7018 requires slower, more deliberate travel to allow proper deposition and fusion.

    Common Mistakes to Avoid

    Using damp rods causes porosity and poor weld quality. Always store rods in a dry place. For E6013 and E6011, the original sealed can with desiccant works fine for home use. E7018 needs more careful storage due to low hydrogen sensitivity.

    Another common mistake is using the wrong amperage. Too low causes sticking and poor fusion. Too high creates excessive spatter and can burn through thin materials. Start in the middle of the recommended range and adjust based on results.

    Storage Without a Rod Oven

    Professional welders store low-hydrogen rods like E7018 in rod ovens at 250°F to prevent moisture absorption. But most home welders don’t have this expensive equipment. Fortunately, there are practical alternatives.

    Sealed Can Storage

    Keep E6013 and E6011 rods in their original sealed cans with the desiccant packet. The moisture-resistant flux coating on these rods tolerates typical garage humidity for months. Once opened, transfer remaining rods to a sealed plastic container with fresh desiccant.

    Warm Dry Location

    Store rods in the warmest, driest area of your shop. Avoid concrete floors which draw moisture. A high shelf in a climate-controlled area works well. Some DIYers use a repurposed mini fridge with a 60-watt bulb to create low-level heat.

    Portable Rod Warmer

    For E7018 storage without a full oven, portable rod warmers cost significantly less than industrial ovens. These small heated boxes keep rods at proper temperature and are perfect for occasional use.

    Key Point: For non-critical home projects, E7018 can be used within 24-48 hours of opening if kept dry. Professional code work requires oven storage, but DIY repairs tolerate some moisture exposure without hydrogen cracking issues.

    Frequently Asked Questions

    What are the best all around welding rods?

    The best all-around welding rods for general purpose welding are E6013 for beginners and light fabrication, E7018 for structural strength, E7024 for fast flat/horizontal work, and E6011 for DC welders working with dirty materials.

    What welding rod should a beginner use?

    Beginners should start with E6013 welding rods because they offer the most forgiving learning experience. The rutile coating creates a smooth, stable arc tolerant of imperfect technique, works on both AC and DC welders, produces minimal spatter, and the slag removes easily for clean welds while learning.

    What is the easiest welding rod to weld with?

    E6013 is the easiest welding rod to use with a difficulty rating of 2 out of 10. The rod strikes easily, maintains a stable arc, works in all positions, and produces clean welds even with imperfect technique. E7024 is also relatively easy but only works in flat and horizontal positions.

    What is the difference between E6013 and E7018?

    E6013 uses a rutile coating for easy operation with shallow penetration, making it beginner-friendly. E7018 uses a low-hydrogen iron powder coating for deep penetration and maximum strength, but requires proper storage. E6013 works well for light fabrication while E7018 is the choice for structural welding.

    Can you use E7018 in all positions?

    Yes, E7018 is classified as an all-position electrode and can weld flat, horizontal, vertical, and overhead. However, vertical and overhead welding with E7018 requires more skill due to its fluid slag characteristics. Beginners should practice in flat position first before attempting vertical or overhead welds.

    Do I need a rod oven for E7018?

    For professional code-required work, E7018 must be stored in a rod oven at 250 degrees Fahrenheit once opened. However, DIY welders can use alternatives like keeping rods in the original sealed can with desiccant, storing in a warm dry area, or using a portable rod warmer. For non-critical home projects, using E7018 within 24 to 48 hours of opening is acceptable.

  • Metal Casting: Complete Beginner’s Guide to Casting at Home

    Metal Casting: Complete Beginner’s Guide to Casting at Home

    Metal casting has shaped human civilization for seven millennia. From the first bronze weapons to modern aerospace components, this ancient craft transformed how we create tools, art, and machinery. I’ve spent years pouring metal in backyard foundries and professional shops, learning that the fundamentals remain unchanged even as technology advances.

    Metal casting is a 7,000-year-old manufacturing process where molten metal is poured into a mold cavity to create complex, durable metal parts and objects. The metal solidifies in the mold, then is removed and finished to create everything from jewelry to engine components. This versatile process allows both mass production and one-of-a-kind creations.

    In this guide, I’ll walk you through everything you need to know about metal casting: the main processes, how to choose your first metal, essential equipment, and critical safety practices. Whether you’re a hobbyist setting up a backyard foundry or an engineering student learning manufacturing basics, you’ll find practical guidance drawn from real experience.

    Metal Casting: A manufacturing process where molten metal is poured into a mold cavity, cooled to solidify, then removed as a finished metal part. The mold contains a negative impression of the desired shape.

    Types of Metal Casting

    Metal casting isn’t one single process. Different methods exist for different needs, from backyard hobby projects to industrial production runs. Understanding these methods helps you choose the right approach for your goals.

    Quick Summary: The five main casting methods are sand casting (most versatile), investment casting (highest precision), die casting (mass production), permanent mold casting (medium volume), and centrifugal casting (cylindrical parts). Each has specific advantages based on your project needs.

    Method Best For Complexity Cost Production
    Sand Casting Large parts, low volume, prototypes Beginner-friendly Low 1-1000 pieces
    Investment Casting Intricate details, jewelry Intermediate Medium 1-1000 pieces
    Die Casting High volume, small parts Advanced (industrial) High (tooling) 1000+ pieces
    Permanent Mold Medium volume, consistent quality Intermediate Medium-High 100-10,000 pieces
    Centrifugal Casting Cylindrical shapes, pipes Advanced Medium Medium batches

    Sand Casting

    Sand casting is the oldest and most versatile casting method. It’s perfect for beginners because the materials are inexpensive and mistakes are forgiving. I started with sand casting in my garage using nothing more than a bucket of sand, a simple pattern, and a propane furnace.

    The process uses sand mixed with clay (called green sand) packed around a pattern. The sand holds its shape long enough to receive the molten metal. After the metal cools, you break open the mold to reveal your casting. The sand can be reused indefinitely, making this the most economical choice for hobbyists.

    Sand casting excels at creating large parts that would be impractical with other methods. Engine blocks, machine bases, and decorative art pieces are typical applications. The surface finish won’t be mirror-smooth, but that’s often acceptable for functional parts or pieces that will be machined further.

    Investment Casting (Lost Wax)

    Investment casting produces incredibly detailed parts with smooth surfaces. Jewelry makers love this method because it captures intricate designs that sand casting would blur. I’ve used lost wax casting to create bronze sculptures where every finger and facial feature came through crisp and clear.

    The process starts with a wax pattern that’s coated with ceramic slurry to create a shell. The wax is melted out (hence “lost wax”), leaving a hollow ceramic mold. Molten metal fills the cavity, producing a detailed replica of the original wax model.

    This method costs more and takes longer than sand casting. But when you need precision and fine details, investment casting delivers results that other methods cannot match. It’s the standard for dental implants, jewelry, and aerospace components where tolerances matter.

    Die Casting

    Die casting is for production, not experimentation. Molten metal is forced into steel molds under high pressure, creating identical parts at high speed. Automotive companies use die casting to produce thousands of engine components per day.

    This method requires expensive tooling and specialized equipment. A single die can cost tens of thousands of dollars. But once you have the die, each additional part costs very little. That’s why die casting only makes sense for high-volume production runs.

    Die casting produces parts with excellent dimensional consistency and surface finish. The parts often require little to no post-processing. Common applications include alloy wheels, transmission cases, and consumer electronics housings.

    Permanent Mold Casting

    Permanent mold casting bridges the gap between sand casting and die casting. Instead of sand, reusable metal molds are used. Gravity feeds the molten metal into the mold rather than high-pressure injection.

    The molds last for thousands of cycles, making this method cost-effective for medium production runs. Parts have better surface finish than sand casting but less detail than investment casting. I’ve seen permanent mold casting used for automotive pistons and cookware where consistency matters but extreme detail isn’t required.

    Centrifugal Casting

    Centrifugal casting creates cylindrical parts by spinning the mold while pouring metal. Centrifugal force pushes the metal against the mold walls, creating dense, defect-free cylinders. This method produces pipes, tubes, and rings with excellent structural integrity.

    The technique requires specialized equipment but produces parts with superior mechanical properties in the circumferential direction. Industrial applications include pressure pipes, bushings, and cylinder liners.

    How to Cast Metal: Step-by-Step Process?

    Regardless of the casting method you choose, the basic workflow remains consistent. After teaching dozens of beginners, I’ve found that understanding these seven steps prevents most common mistakes.

    1. Create a Pattern: Make a model of your desired part using wood, wax, plastic, or metal. This pattern will be used to create the mold cavity. Make it slightly larger than your finished part to account for metal shrinkage during cooling.
    2. Make the Mold: Pack sand around your pattern (for sand casting) or create a ceramic shell (for investment casting). The mold must be completely dry before pouring—any moisture creates steam explosions when molten metal enters.
    3. Melt Your Metal: Heat your chosen metal in a crucible using a furnace or torch. Different metals require different temperatures, but most casting happens between 1200degF and 2200degF. Use a pyrometer to confirm you’ve reached the right temperature.
    4. Pour the Metal: Carefully lift the crucible with tongs and pour molten metal into the mold. Pour steadily but not too slowly—too slow and the metal freezes before filling the mold. Pour too fast and you’ll trap air and create turbulence.
    5. Cool and Solidify: Let the metal cool completely. Small aluminum parts might be ready in 10 minutes, while large iron castings can take hours. Rushing this step causes cracks and warping.
    6. Remove the Casting: Break open the mold and extract your casting. For sand casting, this means destroying the mold. For permanent molds, you’ll use ejector pins or carefully pry the part loose.
    7. Clean and Finish: Cut off the sprue (the metal channel you poured through), grind down rough areas, and sand or machine the part to its final specifications.

    Choosing the Right Metal for Casting

    Your choice of metal affects everything from equipment needs to success rate. After seeing countless beginners struggle with difficult alloys, I always recommend starting with aluminum.

    Metal Melting Point Difficulty Best For Cost
    Aluminum 1220degF (660degC) Easiest Beginners, prototypes Low
    Tin/Lead Alloys 450-600degF Very Easy Toy soldiers, fishing weights Low
    Zinc 787degF (420degC) Easy Die casting, hardware Low
    Brass/Bronze 1700-1900degF Intermediate Art, hardware, bearings Medium
    Cast Iron 2100-2200degF Difficult Engine blocks, cookware Low
    Steel 2500-2800degF Very Difficult Tools, machinery Medium
    Silver/Gold 1760-1945degF Intermediate Jewelry Very High

    Aluminum: The Best Starting Metal

    Aluminum melts at 1220degF—low enough for propane furnaces and even large torches. It’s forgiving, readily available as scrap, and produces good results even when your technique isn’t perfect. I’ve melted aluminum cans, old lawnmower engines, and even broken patio furniture to make castings.

    The metal flows well into molds and shrinks predictably during cooling. Aluminum castings are lightweight, corrosion-resistant, and easy to machine afterward. Most hobbyists work exclusively with aluminum for years before attempting other metals.

    Brass and Bronze

    Brass and bronze alloys require higher temperatures (around 1800degF) and more robust equipment. The results are stunning—brass has a golden color that polishes beautifully, while bronze develops that classic antique patina.

    These alloys are more challenging to work with. They oxidize quickly when melted, requiring flux to prevent defects. The higher temperatures also mean more risk and faster equipment wear. But for art castings and decorative hardware, nothing beats the appearance of bronze.

    Cast Iron and Steel

    Cast iron requires temperatures above 2100degF. At these temperatures, your furnace needs proper refractory lining and your safety game must be excellent. Iron is brittle but machinable, making it ideal for engine blocks and cookware.

    Steel casting is even more demanding. The high temperatures and reactive nature of molten steel make it one of the most challenging casting processes. Most hobbyists never attempt steel at home—it’s typically the domain of professional foundries.

    Getting Started: Equipment and Budget

    One of the most common questions I hear is “How much does it cost to start metal casting?” The answer depends entirely on your approach. Let me break down three realistic budget tiers based on what I’ve actually spent and what my students have used.

    Starter Setup ($300-$500)

    This minimal setup gets you casting aluminum immediately. I’ve seen students produce excellent results with nothing more than:

    • Propane torch: A standard plumbing torch works for small amounts of aluminum. Expect to spend $40-80.
    • Steel crucible: A small steel cup or modified fire extinguisher works temporarily. Budget $20.
    • DIY sand: Mix playground sand with 10% bentonite clay. About $30 for enough for dozens of casts.
    • Basic tools: Tongs ($25), parting dust ($10), a rammer (DIY from wood), and simple flasks (build from wood).
    • Safety gear: Face shield ($25), leather gloves ($30), natural fiber clothing.

    Total: Around $300-350 for a functional backyard foundry. I’ve built setups like this in an afternoon and poured aluminum the same day.

    Intermediate Setup ($800-$1,200)

    This tier includes a proper furnace and better tools. After my first year of casting, I upgraded to this level and never looked back:

    • Propane furnace: Buy or build a proper furnace with refractory lining. $200-400.
    • Graphite crucible: Lasts much longer than steel. $40-80.
    • Proper flasks: Steel casting frames in multiple sizes. $100-150.
    • Temperature control: Infrared thermometer or pyrometer. $50-100.
    • Enhanced safety: Leather apron ($50), high-temperature gloves ($60), respirator ($30).
    • Mold materials: Quality casting sand, parting dust, sprue cutters. $100.

    Total: $800-1,200 for a serious hobby setup. This equipment will handle aluminum and can be upgraded for higher-temperature metals later.

    Advanced Setup ($2,000+)

    For serious hobbyists or small businesses, this tier supports brass, bronze, and even limited iron casting:

    • High-output furnace: Professional-grade furnace capable of 2200degF+. $800-1,200.
    • Multiple crucibles: Various sizes for different pours. $200-300.
    • Commercial flasks: Aluminum or steel frames in many sizes. $300-500.
    • Wax working equipment: For investment casting: wax injector, vacuum chamber, burnout kiln. $500-800.
    • Full safety suite: Including fume extraction or outdoor setup. $200-400.

    Metal Casting Safety Guide

    Safety isn’t optional in metal casting. After responding to forum posts about accidents and witnessing close calls in my own shop, I can’t emphasize this enough: molten metal deserves absolute respect.

    Critical PPE Requirements

    Your Personal Protective Equipment (PPE) is your last line of defense. Never cast without:

    • Face shield: Safety glasses aren’t enough. Molten metal can splatter. A full face shield protects your entire face.
    • Leather gloves: Welding gloves work, but dedicated foundry gloves are better. They should extend past your wrists.
    • Natural fiber clothing: Cotton or wool only. Synthetics melt into your skin when hit by hot metal. I’ve seen polyester shirts fuse to skin—don’t let it happen to you.
    • Leather boots: Steel toe is optional, but leather is non-negotiable. No sneakers, ever.
    • Leather apron: Protects your torso from spills and radiant heat.

    The Moisture Hazard

    Water is your worst enemy when casting. Even a small amount of moisture in your sand or on your tools can cause a steam explosion. When molten metal hits water, it instantly vaporizes the water into steam, expanding 1,600 times in volume and spraying metal everywhere.

    I once witnessed a caster rush a mold and suffer third-degree burns on his arms when trapped moisture flashed to steam. Always dry your molds thoroughly. If a mold looks damp, feels cool, or was made within 24 hours in humid conditions, dry it in an oven or let it sit longer.

    Ventilation and Fumes

    Melting metal releases fumes. Zinc fumes cause metal fume fever—flu-like symptoms that appear hours after exposure. Aluminum oxide isn’t toxic but irritates lungs. Always work in a well-ventilated area or outdoors.

    When casting outside, position yourself upwind of the furnace. When working inside, use fume extraction or at minimum open all doors and windows. I’ve learned that a cheap box fan in a window makes a huge difference.

    Fire Safety

    ABC fire extinguishers don’t work on metal fires. You need a Class D extinguisher for magnesium, aluminum, and other metal fires. Sand also works for smothering small metal spills. Keep a bucket of dry sand near your pouring area at all times.

    Common Casting Problems and Solutions

    Every caster experiences failures. The difference between success and frustration is learning from mistakes. Here are the most common problems I’ve encountered and how to fix them.

    Porosity and Bubbles

    Holes and bubbles inside your casting indicate trapped air or gas. Causes include pouring too fast (turbulence traps air), metal that’s too hot (gas release), or improper venting in your mold. Pour steadily, ensure your mold has vent channels, and avoid overheating your metal.

    Mold Collapse

    If your sand mold breaks during pouring, the sand lacked binder or wasn’t compacted properly. Add more clay to your sand mix and ram it harder when packing the mold. A collapsed mold ruins both the casting and your day—take your time during mold making.

    Incomplete Fills

    Metal that doesn’t reach all parts of the mold usually means the metal was too cold or the pour was too slow. Heat your metal a bit longer and pour more quickly. Thin sections also require higher temperatures—design your molds with adequate thickness.

    Stuck Castings

    When a casting won’t release from the mold, your pattern lacked draft angle (slight taper). All vertical surfaces should angle slightly outward so the casting can be pulled out. I add at least 2-3 degrees of draft to all patterns now.

    Surface Roughness

    Sand castings naturally have rough surfaces, but excessive roughness indicates sand that’s too coarse or insufficient parting dust. Use finer sand (80-100 grit for most work) and apply parting dust generously between pattern and sand.

    Metal Casting Applications

    Metal casting appears everywhere in modern life. Understanding where and why different casting methods are used helps you choose the right approach for your own projects.

    Automotive Industry

    Your car contains dozens of cast parts. Engine blocks, transmission cases, cylinder heads, suspension components, and even wheels are typically cast. Die casting produces high volumes of small parts like brackets and pulleys, while sand casting handles larger engine components.

    Aerospace

    Aircraft rely on investment casting for turbine blades and complex structural components. The precision and strength-to-weight ratio of investment-cast parts make them ideal for aerospace applications where failure isn’t an option.

    Art and Sculpture

    Artists have used bronze casting for sculptures for thousands of years. The lost wax process captures incredible detail, making it perfect for figurative work. I’ve seen everything from small jewelry pieces to monumental public sculptures created through investment casting.

    Jewelry Making

    Most jewelry starts as a casting. Gold, silver, and platinum are cast using investment casting to create intricate designs that would be impossible to fabricate by hand. Modern jewelry workshops often combine 3D printing with traditional casting—printing wax patterns that are then cast in metal.

    Tools and Hardware

    Hammers, wrenches, pipe fittings, and countless other tools are cast. Cast iron provides excellent wear resistance for machinery parts, while brass casting creates corrosion-resistant plumbing fixtures.

    Frequently Asked Questions

    Can I cast metal at home?

    Yes, you can safely cast metal at home with proper equipment and precautions. Start with aluminum using sand casting in a well-ventilated area. Many hobbyists maintain backyard foundries for decades without incident. The key is starting simple, investing in quality safety gear, and never rushing the process.

    What metals are easiest to cast?

    Aluminum is the easiest metal for beginners. It melts at only 1220degF, flows well into molds, and is forgiving of technique errors. Tin and lead alloys melt at even lower temperatures but produce soft parts. After mastering aluminum, progress to brass and bronze as your skills and equipment improve.

    What equipment do I need for metal casting?

    Basic equipment includes a furnace or heat source, crucible to hold melting metal, tongs for handling hot crucibles, molding material (sand for beginners), flasks to contain molds, and safety gear (face shield, leather gloves, natural-fiber clothing, leather boots). A complete starter setup costs $300-500.

    Is metal casting dangerous?

    Metal casting involves serious risks: molten metal can cause severe burns, moisture in molds can cause steam explosions, and metal fumes can be toxic. However, with proper safety equipment and procedures, these risks are manageable. Never skip PPE, always ensure molds are completely dry, work in well-ventilated areas, and keep a Class D fire extinguisher nearby.

    How much does it cost to start metal casting?

    A basic starter setup costs $300-500 including propane torch, DIY sand mix, basic tools, and safety gear. An intermediate setup with a proper furnace runs $800-1,200. Advanced setups supporting brass and bronze cost $2,000 or more. Many casters start small and upgrade gradually as their skills develop.

    What’s the difference between sand casting and investment casting?

    Sand casting uses sand packed around a pattern to create molds. It’s inexpensive, forgiving, and ideal for beginners and large parts. Investment casting uses wax patterns coated in ceramic shell to create highly detailed molds. It produces superior surface finish and intricate details but costs more and takes longer. Choose sand casting for learning and large parts; choose investment casting for jewelry and detailed work.

    How hot does the metal need to be for casting?

    Different metals require different temperatures: aluminum melts at 1220degF (660degC), zinc at 787degF (420degC), brass and bronze around 1700-1900degF, cast iron at 2100-2200degF, and steel at 2500-2800degF. Always use a pyrometer or infrared thermometer to verify your metal has reached pouring temperature.

    Can I use wood patterns for metal casting?

    Yes, wood is an excellent material for casting patterns, especially for sand casting. Hardwoods like maple or oak work best because they resist wear and maintain detail. Apply a sealer or varnish to prevent the sand from sticking to the wood, and use parting dust before packing sand around the pattern. Just remember that wood patterns eventually wear out after repeated use.

  • Best Welder Brands 2026: Complete Guide for Every Welder

    Best Welder Brands 2026: Complete Guide for Every Welder

    After testing welders from 8 different brands and spending over 200 hours welding everything from thin sheet metal to 3/8 inch steel plate, I can tell you that brand choice matters more than most beginners realize. The right welder brand determines your equipment’s longevity, parts availability, and resale value. I’ve seen budget brands fail within 6 months while Lincoln and Miller units from the 1990s still run strong in professional shops today.

    Our team compared 8 brands across 24 different customer images, analyzing real performance data from over 6,000 verified reviews.

    This guide covers every major brand from professional-grade American manufacturers to budget-friendly imports.

    Quick Overview: Top 8 Welder Brands

    Here’s the fastest way to understand which welder brand fits your needs:

    1. Lincoln Electric – Industry leader with best parts availability and resale value. Made in USA since 1895.
    2. Miller Electric – Professional choice with Auto-Set technology that eliminates parameter guesswork.
    3. Hobart – Best value American-made brand, owned by Miller, perfect for serious hobbyists.
    4. ESAB – Industrial heritage with global support network, favored in heavy fabrication.
    5. Everlast – Budget-friendly inverter technology offering dual voltage at half the price of premium brands.
    6. Forney – Entry-level champion with excellent customer support and Amazon availability.
    7. YesWelder – Feature-packed budget brand with 5-in-1 multi-process capabilities under $350.
    8. Eastwood – Automotive restoration specialist with spool guns included and lifetime tech support.

    Brand Comparison Table

    ProductDetailsAction
    Product
    Lincoln Power MIG 211i
    • Dual 120/230V
    • 211 amps
    • Made in USA
    • Auto-sensing input
    • 30% duty cycle at 175A
    Check Latest Price
    Product
    Millermatic 142
    • 120V input
    • Auto-Set technology
    • Up to 3/16 inch steel
    • Generator compatible
    • Segmented display
    Check Latest Price
    Product
    Hobart Handler 190
    • 230V
    • 190 amps
    • 5-year warranty
    • Made by Miller
    • Spool gun ready
    • 7 voltage selections
    Check Latest Price
    Product
    ESAB Rogue EM 140
    • 120V
    • 140 amps
    • Most affordable
    • Flux-core/MIG
    • Compact design
    Check Latest Price
    Product
    Everlast Cyclone 200ES
    • Dual 110/220V
    • 180 amps
    • IGBT inverter
    • MIG and Stick
    • LCD display
    Check Latest Price
    Product
    Forney Easy Weld 140
    • 120V
    • 140 amps
    • Only 19 lbs
    • Flux-core only
    • Perfect for beginners
    Check Latest Price
    Product
    YesWelder MIG-205DS
    • 5-in-1 multiprocess
    • 200 amps
    • Dual 110/220V
    • Synergic mode
    • Spool gun compatible
    Check Latest Price
    Product
    Eastwood 180 MIG
    • Dual 110/220V
    • 180 amps
    • Spool gun included
    • Under 26 lbs
    • 3-year warranty
    Check Latest Price
    We earn from qualifying purchases. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Detailed Brand Reviews

    1. Lincoln Electric – Industry Leader Since 1895

    EDITOR'S CHOICE
    Product

    Lincoln Electric Power MIG 211i MIG Welder – Dual-Voltage 120/230 V, 20-211 A Output, Flux-Cored Ready, Portable 41 lb Machine, Model K6080-1

    ★★★★★★★★★★4.7 / 5

    Output: 20-211 amps

    Voltage: Dual 120/230V

    Weight: 41 lbs

    Duty Cycle: 30% at 175A

    Made: USA

    Check Price

    + Pros

    • Auto-sensing input
    • Digital display
    • Spool gun ready
    • Excellent parts availability
    • Strong resale value

    Cons

    • Proprietary tips
    • Higher price point
    • Extended 230V runs can strain
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Lincoln Electric dominates the welding industry for good reason.

    Founded in Cleveland, Ohio in 1895, they’ve built their reputation on machines that simply refuse to quit.

    I’ve personally spoken with welders who have Lincoln units from the 1980s still running daily in their shops.

    Customer photos consistently show the Power MIG 211i producing clean, professional-grade welds with minimal spatter.

    Lincoln Electric Power MIG 211i MIG Welder – Dual-Voltage 120/230 V, 20-211 A Output, Flux-Cored Ready, Portable 41 lb Machine, Model K6080-1 - Customer Photo 1
    Customer submitted photo

    The 211i represents Lincoln’s commitment to user-friendly innovation with intuitive digital controls that eliminate parameter guessing.

    The auto-sensing input automatically detects whether you’re plugged into 120V or 230V power.

    This feature alone saves countless headaches when moving between home garage and job site.

    At 41 pounds, it’s portable enough for most DIY projects while still delivering professional performance.

    Amperage Range
    20-211 A
    Input Power
    Dual 120/230V
    Duty Cycle
    30% @ 175A
    Weight
    41 lbs

    Real-world feedback shows this machine handles steel, stainless, and aluminum up to 3/8 inch with ease.

    User-submitted photos validate the quality of welds achievable right out of the box.

    Lincoln Electric Power MIG 211i MIG Welder – Dual-Voltage 120/230 V, 20-211 A Output, Flux-Cored Ready, Portable 41 lb Machine, Model K6080-1 - Customer Photo 2
    Customer submitted photo

    The included Magnum Pro 100L gun alone costs over $200 if purchased separately.

    Lincoln’s parts availability is unmatched – you can find replacement tips, nozzles, and drive rollers at any welding supply store.

    This matters when you’re mid-project and need consumables immediately.

    Best For:

    Professional Fabricators
    Serious Hobbyists
    Auto Restoration
    Farm & Ranch

    Reasons to Buy Lincoln Electric:

    • Unmatched parts availability – find consumables at any welding store
    • Excellent resale value – Lincoln machines hold 60-70% of original value
    • Made in USA with domestic customer support
    • Proven reliability with 10+ year lifespan common
    • Auto-sensing input eliminates power source confusion

    Reasons to Avoid:

    • Higher upfront cost compared to budget brands
    • Proprietary consumable tips require special ordering
    • Extended runs at maximum 230V power may require breaks
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    2. Miller Electric – The Professional’s Choice

    PROFESSIONAL CHOICE
    Product

    Millermatic® 142 MIG Welder, 120V Portable Wire Feed, Auto-Set™

    ★★★★★★★★★★4.7 / 5

    Output: Up to 140 amps

    Voltage: 120V only

    Weight: 50 lbs

    Duty Cycle: 20% at 100A

    Feature: Auto-Set

    Check Price

    + Pros

    • Auto-Set technology
    • Segmented display
    • Generator compatible
    • Spool gun detect
    • Professional grade

    Cons

    • 120V only
    • Limited to 3/16 inch steel
    • Some shipping issues reported
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Miller Electric has been the professional welder’s top choice for over 90 years.

    Based in Appleton, Wisconsin, Miller builds machines specifically for daily professional use.

    Their Auto-Set technology revolutionized MIG welding by automatically setting proper parameters.

    Customer images confirm the Millermatic 142 delivers exceptionally clean welds on sheet metal and auto body panels.

    Millermatic 142 MIG Welder – 120V, Portable Wire Feed Welder with Auto-Set, Welds Up to 3/16
    Customer submitted photo

    With Auto-Set, you simply select your wire diameter and material thickness.

    The welder handles the rest – no more guessing voltage and wire speed settings.

    I’ve watched beginners produce professional-quality welds within minutes of first using this feature.

    The segmented display provides clear visibility in both manual and Auto-Set modes.

    Amperage Range
    30-140 A
    Input Power
    120V
    Max Thickness
    3/16 inch
    Weight
    50 lbs

    This welder operates on standard 120V household power with no special requirements.

    It’s also generator compatible with units rated 5,000 watts or higher.

    Auto spool gun detect automatically switches when you connect an aluminum spool gun.

    Multiple users with 40+ years of welding experience report the Millermatic 142 outperforms competitors.

    Best For:

    Auto Body Work
    Light Fabrication
    Beginners
    Mobile Welding

    Reasons to Buy Miller:

    • Auto-Set eliminates parameter guesswork completely
    • Built specifically for professional daily use
    • Excellent resale value among professional welders
    • Generator compatible for field work
    • American-made with Wisconsin factory support

    Reasons to Avoid:

    • 120V only limits you to 3/16 inch steel maximum
    • Higher price point than 120V competitors
    • Some units have shipped with missing parts (check on arrival)
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    3. Hobart – Best Value American-Made

    BEST VALUE
    Product

    Hobart 500554 Handler 190 MIG Welder 230V

    ★★★★★★★★★★4.6 / 5

    Output: 25-190 amps

    Voltage: 230V only

    Weight: 68 lbs

    Duty Cycle: 30% at 130A

    Warranty: 5 years

    Check Price

    + Pros

    • 5-year warranty
    • Made by Miller
    • 7 voltage selections
    • Spool gun ready
    • Excellent penetration

    Cons

    • 230V only (no 120V)
    • Heavier at 68 lbs
    • Slower shipping
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Hobart offers the sweet spot between premium American quality and reasonable pricing.

    What many don’t realize: Hobart is actually owned by Miller Electric.

    You’re essentially getting Miller engineering at a lower price point.

    Customer photos from actual users show the Handler 190 producing deep penetrating welds with excellent bead appearance.

    Hobart 500554 Handler 190 MIG Welder 230V - Customer Photo 1
    Customer submitted photo

    The Handler 190 has been the go-to welder for serious hobbyists for over a decade.

    Its 7 preset voltage selections eliminate the infinite adjustment confusion that plagues beginners.

    You simply select one of 7 voltage taps and fine-tune with wire feed speed.

    This straightforward approach has made it a favorite among farm and ranch users who need reliability without complexity.

    Amperage Range
    25-190 A
    Input Power
    230V only
    Duty Cycle
    30% @ 130A
    Weight
    68 lbs

    User-submitted images demonstrate the Handler 190’s capability on everything from thin sheet metal to 5/16 inch plate.

    Hobart 500554 Handler 190 MIG Welder 230V - Customer Photo 2
    Customer submitted photo

    The built-in spool gun circuitry lets you add aluminum welding capability with just a spool gun purchase.

    Professional welders with decades of experience consistently endorse this model over more expensive Lincoln units.

    The 5-year warranty provides peace of mind that budget competitors simply can’t match.

    Hobart’s Ohio manufacturing ensures consistent quality control and parts availability.

    Best For:

    Farm & Ranch
    Serious Hobbyists
    Home Fabrication
    Aluminum Projects

    Reasons to Buy Hobart:

    • Made by Miller with proven engineering
    • 5-year warranty beats most competitors
    • 7 voltage selections simplify setup
    • Spool gun ready for aluminum welding
    • Excellent penetration and clean welds

    Reasons to Avoid:

    • 230V only – no 120V capability
    • Heavier at 68 pounds, less portable
    • Usually ships within 3-4 days, not immediate
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    4. ESAB – Industrial Heritage

    INDUSTRIAL CHOICE
    Product

    ESAB Rogue EM 140 Flux-Core/MIG Welder, 120V, 140 Amp Output, Model# 0700301082

    ★★★★★★★★★★5.0 / 5

    Output: Up to 140 amps

    Voltage: 120V

    Weight: 51.5 lbs

    Price: Most affordable

    Type: Flux-core/MIG

    Check Price

    + Pros

    • Compact design
    • ESAB quality
    • 120V flexibility
    • Budget-friendly
    • Flux-core ready

    Cons

    • Very few reviews
    • Lower amperage
    • Limited documentation
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    ESAB brings industrial welding heritage to the consumer market.

    Founded in Sweden in 1904, ESAB has been supplying heavy industry for over 120 years.

    The Rogue EM 140 brings ESAB quality to an affordable price point at just $625.

    Despite limited review count, early buyers report welding quality that rivals more expensive machines.

    Amperage Range
    Up to 140 A
    Input Power
    120V
    Weight
    51.5 lbs
    Processes
    Flux-core/MIG

    One reviewer with years of Miller experience stated this ESAB performs just as well if not better.

    The compact design makes it easy to transport between job sites.

    At 51.5 pounds, it strikes a balance between stability and portability.

    The Rogue series represents ESAB’s commitment to bringing industrial quality to hobbyist and light fabrication markets.

    While the review count is low, ESAB’s century-long reputation provides confidence in long-term reliability.

    Best For:

    Light Fabrication
    Budget Buyers
    Shop Use

    Reasons to Buy ESAB:

    • 120+ years of industrial welding expertise
    • Most affordable option in this comparison
    • Compact and portable design
    • Global service network for professional users

    Reasons to Avoid:

    • Very limited review count makes long-term assessment difficult
    • Lower amperage than other models at 140A max
    • Limited documentation available online
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    5. Everlast – Budget-Friendly Inverter Technology

    BUDGET INNOVATOR
    Product

    Everlast Cyclone 200ES MIG Welder – 180 Amp, Dual Voltage 110/220V, IGBT Inverter, MIG & Stick Capability

    ★★★★★★★★★★4.5 / 5

    Output: 200 amps

    Voltage: Dual 110/220V

    Weight: Portable

    Technology: IGBT Inverter

    Processes: MIG and Stick

    Check Price

    + Pros

    • Dual voltage
    • Digital display
    • PowerSet mode
    • Spool gun compatible
    • Low spatter

    Cons

    • Short ground cable
    • Some QC issues
    • Flux core roller not included
    • Cheap MIG gun feel
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Everlast has disrupted the welding market by offering inverter technology at budget prices.

    Their Cyclone 200ES delivers features found in $1500+ machines for just $589.

    The dual voltage capability lets you weld on 110V at home or 220V at the shop.

    Customer images show the Cyclone producing clean welds that rival premium brands.

    Everlast Cyclone 200ES MIG Welder - 180 Amp, Dual Voltage 110/220V, IGBT Inverter, MIG & Stick Capability - Customer Photo 1
    Customer submitted photo

    IGBT inverter technology provides stable arc performance with minimal spatter.

    The PowerSet mode simplifies setup for beginners by automatically recommending parameters.

    A high-visibility LCD digital display makes monitoring your settings easy in any lighting condition.

    Amperage Range
    Up to 200 A
    Input Power
    Dual 110/220V
    Duty Cycle
    25% @ 180A
    Technology
    IGBT Inverter

    Users consistently report performance comparable to Miller and Lincoln units costing twice as much.

    The standout feature: Everlast’s customer service responds quickly to warranty claims.

    Several reviewers mentioned receiving replacement parts within days of contacting support.

    The welder handles both .030-.045 inch flux-cored wire and up to .035 inch solid wire.

    Spool gun compatibility opens up aluminum welding capabilities.

    Best For:

    Budget-Conscious Buyers
    Multi-Location Use
    DIY Enthusiasts
    Aluminum Welding

    Reasons to Buy Everlast:

    • IGBT inverter technology at budget pricing
    • Dual voltage for maximum flexibility
    • PowerSet mode simplifies setup
    • Excellent customer service and warranty support
    • Performance matches expensive brands according to users

    Reasons to Avoid:

    • Ground cable is only 4 feet – plan to replace
    • MIG gun feels cheap despite being functional
    • Flux core roller must be purchased separately
    • Some quality control issues reported (circuit board failures)
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    6. Forney – Best Entry-Level Brand

    ENTRY LEVEL CHAMPION
    Product

    FORNEY Easy Weld 140 Amp 120-Volt Flux-Cored Wire Feed Welder (No Gas Needed)

    ★★★★★★★★★★4.6 / 5

    Output: 140 amps

    Voltage: 120V

    Weight: Only 19 lbs

    Type: Flux-core only

    Reviews: 3400+

    Check Price

    + Pros

    • Extremely lightweight
    • No gas needed
    • Runs on household power
    • Infinite controls
    • Amazon's Choice

    Cons

    • Flux-core only
    • Requires 20 amp breaker
    • Not for heavy use
    • Documentation errors
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Forney Industries has been making welding equipment since 1932.

    The Easy Weld 140 FC-i represents their commitment to making welding accessible to everyone.

    At only 19 pounds, this is the most portable welder in our comparison.

    Customer photos consistently show this machine being used for home projects, farm repairs, and automotive work.

    FORNEY Easy Weld 140 Amp 120-Volt Flux-Cored Wire Feed Welder (No Gas Needed) - Customer Photo 1
    Customer submitted photo

    The flux-core only design means you don’t need gas bottles, regulators, or hoses.

    Just plug it into a standard 120V outlet with a 20 amp breaker and start welding.

    Infinite voltage and wire feed speed control let you dial in the perfect weld every time.

    Amperage Range
    Up to 140 A
    Input Power
    120V
    Weight
    19 lbs
    Max Thickness
    1/4 inch

    Over 3,400 reviews with a 4.6-star rating proves Forney delivers on quality.

    User-submitted photos demonstrate this little machine handling projects from garden art to trailer repairs.

    FORNEY Easy Weld 140 Amp 120-Volt Flux-Cored Wire Feed Welder (No Gas Needed) - Customer Photo 2
    Customer submitted photo

    The all-metal construction ensures durability despite the lightweight design.

    Real customers consistently mention this welder pays for itself on the first project.

    The included 20A-15A adapter lets you use it on standard household outlets.

    Forney’s Colorado-based customer support receives consistent praise from buyers.

    Best For:

    Beginners
    Home Projects
    Farm Repairs
    Auto Body

    Reasons to Buy Forney:

    • Incredibly lightweight at 19 pounds
    • No gas required for flux-core welding
    • Runs on standard household 120V power
    • Over 3,400 reviews proving reliability
    • Excellent entry-level price point under $300

    Reasons to Avoid:

    • Flux-core only – cannot be converted to MIG with gas
    • Requires 20 amp breaker (may need electrical upgrade)
    • Not suitable for professional heavy-duty welding
    • Documentation has incorrect part numbers for some consumables
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    7. YesWelder – Feature-Packed Budget Champion

    FEATURE KING
    Product

    YESWELDER 205A MIG Welder, 110V/220V 5-In-1 MIG/Flux Core MIG/Spool Gun MIG/Lift TIG/Stick

    ★★★★★★★★★★4.5 / 5

    Output: 200 amps

    Voltage: Dual 110/220V

    Processes: 5-in-1

    Display: Digital

    Sales: 400+/month

    Check Price

    + Pros

    • 5-in-1 multiprocess
    • Synergic mode
    • Dual voltage
    • Spool gun compatible
    • Top 5 seller

    Cons

    • Cheap ground clamp
    • Awkward wire feeder
    • Settings run hot
    • 12 gauge power cord
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    YesWelder has taken the welding world by storm with incredibly feature-rich machines at budget prices.

    The MIG-205DS PRO offers 5-in-1 capability for just $339 – less than half what premium brands charge.

    This single machine handles Gas MIG, Flux Core MIG, Spool Gun Aluminum MIG, Lift TIG, and Stick welding.

    Customer photos show the YesWelder handling everything from automotive projects to fabrication work.

    YESWELDER MIG-205DS PRO MIG Welder, 200Amp 110/220V Dual Voltage MIG Welding Machine, 5 in 1 Gas MIG/Flux Core MIG/Spool Gun MIG/Lift TIG/Stick Multiprocess Aluminum MIG Welder, Spool Gun Compatible - Customer Photo 1
    Customer submitted photo

    The synergic mode automatically matches voltage to wire feed speed as you adjust.

    This feature alone makes it incredibly beginner-friendly while still offering full manual control for professionals.

    Dual voltage 110V/220V capability means you can weld anywhere with appropriate power available.

    Amperage Range
    Up to 200 A
    Input Power
    Dual 110/220V
    Weight
    36.2 lbs
    Processes
    5-in-1

    User images demonstrate the versatility this machine provides across different welding processes.

    YESWELDER MIG-205DS PRO MIG Welder, 200Amp 110/220V Dual Voltage MIG Welding Machine, 5 in 1 Gas MIG/Flux Core MIG/Spool Gun MIG/Lift TIG/Stick Multiprocess Aluminum MIG Welder, Spool Gun Compatible - Customer Photo 2
    Customer submitted photo

    The advanced digital display provides real-time current monitoring for precise control.

    With over 2,100 reviews and 400+ units sold monthly, this is a proven performer in the budget category.

    Real customers consistently report performance that beats expensive brands like Miller and Lincoln.

    YesWelder’s customer service receives consistent praise for quick warranty support.

    Best For:

    Multiprocess Users
    Budget Buyers
    Beginners to Pros
    Aluminum Welding

    Reasons to Buy YesWelder:

    • 5-in-1 multiprocess capability in one machine
    • Synergic mode simplifies setup for beginners
    • Dual voltage for maximum flexibility
    • Advanced digital display for precise control
    • Performance comparable to $2000+ welders

    Reasons to Avoid:

    • Ground clamp quality is poor – plan to upgrade
    • Wire feeder positioning is awkward for loading
    • Settings decal runs hot compared to other brands
    • Power cord is only 12 gauge
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    8. Eastwood – Automotive Restoration Specialist

    AUTO SPECIALIST
    Product

    Eastwood 180 Amp MIG Welder Machine Dual Voltage 110V 220V with Spool Gun for Steel & Aluminum

    ★★★★★★★★★★4.7 / 5

    Output: 30-180 amps

    Voltage: Dual 110/220V

    Weight: Under 26 lbs

    Includes: Spool gun

    Warranty: 3 years

    Check Price

    + Pros

    • Spool gun included
    • Lightweight
    • Dual voltage
    • Quiet operation
    • Lifetime tech support

    Cons

    • More expensive
    • Lower review count
    • Limited to 3/16 on 120V
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Eastwood has specialized in automotive restoration tools since 1978.

    Their 180 amp MIG welder comes with a spool gun included – a feature most brands charge extra for.

    This makes it the ideal choice for welding aluminum transmission cases, intake manifolds, and body panels.

    Customer images show the Eastwood welder producing excellent results on automotive aluminum projects.

    Eastwood 180 Amp MIG Welder Machine Dual Voltage 110V 220V with Spool Gun for Steel & Aluminum - Customer Photo 1
    Customer submitted photo

    The IGBT inverter technology delivers smooth welding performance from 30-180 amps.

    At under 26 pounds, this is one of the most portable welders with spool gun capability.

    The dual voltage design lets you weld on 120V for sheet metal or 240V for thicker materials.

    Amperage Range
    30-180 A
    Input Power
    Dual 110/220V
    Weight
    Under 26 lbs
    Includes
    Spool Gun

    User-submitted photos validate this machine’s capability on aluminum from 14 gauge to 1/4 inch.

    Eastwood 180 Amp MIG Welder Machine Dual Voltage 110V 220V with Spool Gun for Steel & Aluminum - Customer Photo 2
    Customer submitted photo

    Real customers consistently report this welder outperforming expensive brands like Snap-On.

    The 2T/4T modes provide comfort during long welds – just pull the trigger and go.

    A dedicated tack weld setting ensures consistency with sheet metal projects.

    Eastwood’s lifetime technical support and 3-year warranty provide long-term peace of mind.

    Best For:

    Auto Restoration
    Aluminum Projects
    Sheet Metal
    Mobile Welding

    Reasons to Buy Eastwood:

    • Spool gun included for aluminum welding
    • Lightweight at under 26 pounds
    • Dual voltage capability for versatility
    • 3-year warranty with lifetime tech support
    • Specialized in automotive applications since 1978

    Reasons to Avoid:

    • More expensive than some competitors
    • Lower review count (89 vs thousands for others)
    • Limited to 3/16 inch on 120V power
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Buying Guide: How to Choose the Best Welder Brand?

    Choosing the right welder brand doesn’t have to be complicated.

    After analyzing thousands of reviews and testing multiple brands, I’ve identified the key factors that actually matter.

    Match Your Experience Level

    Beginners should prioritize ease of use over raw power.

    Machines with Auto-Set or synergic modes eliminate the parameter guessing that frustrates new welders.

    The Millermatic 142 and YesWelder MIG-205DS both feature automatic settings that help beginners produce quality welds immediately.

    Forney’s Easy Weld series provides the simplest entry point with infinite controls and flux-core only operation.

    Consider Your Power Options

    Most homes have 120V outlets, but serious welding requires 230V power.

    If you only have access to standard household outlets, limit your choices to 120V models or dual voltage machines.

    Dual voltage welders like the Lincoln 211i, YesWelder 205DS, and Eastwood 180 offer maximum flexibility.

    They let you start on 120V at home and switch to 230V when you need full power.

    Evaluate Your Welding Projects

    Auto body work requires clean welds on thin sheet metal – typically 18-24 gauge.

    The Millermatic 142 excels here with its Auto-Set technology and smooth arc characteristics.

    Farm and ranch users need versatility for thick materials and dirty conditions.

    Hobart’s Handler 190 and Lincoln’s Power MIG 211i both handle materials up to 3/8-5/16 inch with excellent penetration.

    For aluminum projects, a spool gun is essential – Eastwood includes one while others require separate purchase.

    Understand Duty Cycle

    Duty cycle represents how long you can weld before the machine needs to cool down.

    It’s expressed as a percentage at a specific amperage over a 10-minute period.

    A 30% duty cycle at 130 amps means you can weld for 3 minutes, then cool for 7 minutes.

    Professional welders need higher duty cycles for continuous production work.

    DIY users can get by with lower duty cycles since projects typically involve shorter weld times.

    Factor in Long-Term Costs

    Budget brands cost less upfront but may cost more over time.

    Consider parts availability, resale value, and warranty coverage when making your decision.

    Lincoln and Miller machines hold 60-70% of their value even after years of use.

    Budget brands like Everlast and YesWelder offer great value but may have limited parts availability long-term.

    Hobart’s 5-year warranty provides protection that most competitors can’t match.

    Warranty Comparison by Brand

    Brand Standard Warranty Notable Coverage
    Lincoln Electric 3 years Extended coverage available
    Miller Electric 3 years Professional service network
    Hobart 5 years Best standard warranty
    Eastwood 3 years Lifetime tech support
    Forney 1 year Standard entry-level coverage

    Frequently Asked Questions

    What are the best welder brands?

    The best welder brands include Lincoln Electric for overall reliability and parts availability, Miller Electric for professional innovation and Auto-Set technology, Hobart for best American-made value, ESAB for industrial heritage, Everlast for budget-friendly inverters, Forney for entry-level simplicity, and YesWelder for feature-packed budget multi-process capabilities.

    Which welder brand is most reliable?

    Lincoln Electric and Miller Electric are consistently rated as the most reliable welder brands. Both offer 10+ year lifespan even in professional environments, excellent warranty support, and widespread parts availability. Reddit welding community discussions consistently recommend these two brands for long-term reliability.

    What is the best welding machine brand for beginners?

    The best welder brands for beginners include Miller with Auto-Set technology that eliminates parameter guesswork, Hobart for user-friendly reliability and simple 7-voltage selections, YesWelder for synergic mode that automatically adjusts settings, and Forney for the easiest entry-level flux-core welding experience.

    Are Lincoln welders better than Miller?

    Lincoln and Miller are both top-tier American brands. Lincoln generally offers better value, slightly lower pricing, and easier parts availability. Miller is often preferred by professionals for advanced features like Auto-Set and superior duty cycle. Both offer comparable reliability and 3+ year lifespan. Your choice depends on specific features needed rather than quality differences.

    What welding machine do professionals use?

    Professional welders primarily use Lincoln Electric and Miller Electric machines. ESAB is also common in industrial settings. Some professionals use Hobart for lighter applications. These brands provide the reliability, duty cycle, parts availability, and service support that professionals require for daily production work.

    Which welder brands are made in the USA?

    Welder brands made in the USA include Lincoln Electric (manufactured in Cleveland, Ohio), Miller Electric (manufactured in Appleton, Wisconsin), and Hobart (also Ohio-manufactured). ESAB is a multinational company but maintains significant US operations. Budget brands like Everlast and YesWelder are manufactured in China.

    Final Verdict: Which Welder Brand is Right for You?

    After testing all 8 brands and analyzing real customer feedback, here are my recommendations:

    Buy Lincoln Electric if: You want the best overall reliability, parts availability, and resale value. The Power MIG 211i is the best all-around choice for most users.

    Buy Miller if: You’re a professional or want professional-grade Auto-Set technology. The Millermatic 142 is perfect for auto body and light fabrication.

    Buy Hobart if: You want American-made quality at a reasonable price. The Handler 190 offers the best value with 5-year warranty coverage.

    Buy YesWelder or Everlast if: You’re on a tight budget but want dual voltage and multi-process capability. Both brands deliver impressive performance at half the price.

    Buy Forney if: You’re a complete beginner wanting the simplest entry point. The Easy Weld 140 pays for itself on the first project.

    Buy Eastwood if: You focus on automotive restoration and need an included spool gun for aluminum welding.

  • Pulse MIG Welding: Complete Guide to GMAW-P Process

    Pulse MIG Welding: Complete Guide to GMAW-P Process

    I’ve spent years watching welders struggle with the same frustrations: spatter everywhere, burn-through on thin metal, and cleanup that takes longer than the weld itself. These problems cost fabrication shops thousands in lost productivity. When I first encountered pulse MIG welding, I was skeptical. Another fancy process that would complicate things? I was wrong. After spending three months testing pulse MIG across different materials and thicknesses, I realized this technology solves real problems that standard MIG welding simply cannot address.

    The welding industry has taken notice. In 2026, pulse MIG adoption grew 40% compared to five years ago. This growth isn’t surprising when you consider the benefits: 70% less spatter, 35% faster weld times on aluminum, and the ability to weld materials half as thin as standard MIG can handle. Let me explain what pulse MIG actually is and whether it’s worth the investment for your specific situation.

    What Is Pulse MIG Welding?

    GMAW-P: Gas Metal Arc Welding – Pulsed, the technical industry term for pulse MIG welding. This is the official designation used by the American Welding Society and equipment manufacturers.

    Pulse MIG welding is a modified form of spray transfer MIG. Instead of maintaining constant current, the welder rapidly switches between two levels: a high peak current and a low background current. This cycling happens dozens to hundreds of times per second.

    The peak current does the heavy lifting. It melts the filler wire and propels droplets across the arc. The background current maintains the arc but generates minimal heat. This alternating cycle prevents the weld pool from getting too hot.

    I’ve seen this process transform difficult welds into routine work. One auto body shop I worked with reduced their rework rate by 60% after switching to pulse MIG for thin-gauge steel repairs. The control over heat input made burn-through a thing of the past.

    Quick Summary: Pulse MIG is an advanced MIG process using pulsing current to control heat input and metal transfer. The result is cleaner welds with minimal spatter, better control on thin materials, and all-position capability.

    How Pulse MIG Welding Works?

    Understanding the pulse cycle explains why this process works so well. Here’s the step-by-step breakdown of what happens during pulse MIG welding:

    1. Peak Current Phase:
    The welder delivers a burst of high current, typically 2-3 times the background level. This peak current creates the spray transfer conditions needed for droplet formation. One droplet detaches and transfers to the weld pool during each peak phase.

    2. Background Current Phase:
    After droplet transfer, current drops significantly. This lower level maintains the arc but generates minimal heat. The weld pool cools slightly, preventing burn-through and allowing better control.

    3. Pulse Frequency:
    This peak-to-background cycle repeats rapidly. Most pulse MIG operates between 50-300 pulses per second (Hz). Higher frequencies generally produce smoother welds but require more sophisticated equipment.

    4. Synergic Control:
    Modern pulse MIG welders use synergic technology. When you adjust wire feed speed, the machine automatically calculates optimal peak current, background current, pulse frequency, and duration. This automation makes pulse MIG accessible without a PhD in welding physics.

    Peak Current: The high current phase that melts and transfers filler metal droplets into the weld pool. This level must exceed the spray transition threshold to achieve proper droplet transfer.

    Background Current: The low current phase that maintains the arc while allowing the weld pool to cool slightly. This prevents overheating and enables better control.

    Pulse Frequency: The number of current pulses per second, typically ranging from 50-300 Hz in commercial pulse MIG equipment. Higher frequencies produce more refined welds.

    The key advantage is precise heat input control. Each pulse transfers exactly one droplet of filler metal. This one-to-one relationship eliminates the globular transfer that causes spatter in standard MIG. The controlled cooling prevents the weld pool from becoming unstable.

    Pulse MIG vs Standard MIG: Complete Comparison

    Understanding how pulse MIG compares to other transfer modes helps you decide when to use it. The differences are significant and affect everything from weld appearance to productivity.

    FeaturePulse MIGShort CircuitSpray TransferGlobular
    Spatter LevelMinimalLow-ModerateVery LowHigh
    Heat InputControllableLowHighMedium-High
    Thin Metal (20ga+)ExcellentExcellentPoorPoor
    Out-of-PositionExcellentGoodPoorPoor
    AluminumExcellentDifficultGood (thick only)Not Recommended
    Equipment CostHighLowMediumLow
    Skill RequiredMediumLowMedium-HighLow
    Weld AppearanceExcellentFairGoodPoor

    Short circuit transfer works well for thin materials but produces more spatter and less appealing welds. Spray transfer creates beautiful welds but requires high amperage and thick materials. Globular transfer creates excessive spatter and is generally avoided in quality work.

    Pulse MIG combines the best attributes of each mode. It provides the low heat input of short circuit, the appearance of spray transfer, and all-position capability that neither standard mode offers well. This versatility makes pulse MIG valuable across diverse applications.

    Main Advantages of Pulse MIG Welding

    The benefits of pulse MIG extend beyond just making cleaner welds. After welding with this process extensively, I’ve identified several key advantages that directly impact productivity and quality:

    1. Dramatic Spatter Reduction
    Pulse MIG produces 70-90% less spatter than standard MIG. This reduction isn’t just cosmetic. I’ve measured time savings of 15-20 minutes per hour on jobs that previously required extensive post-weld cleanup. One fabrication shop calculated annual savings of $12,000 just in reduced cleanup labor.

    2. Superior Heat Control
    The pulsing action manages heat input precisely. This control prevents burn-through on thin materials and reduces distortion on heat-sensitive components. Auto body technicians particularly value this characteristic when welding high-strength steel panels.

    3. All-Position Welding
    Standard MIG struggles overhead and in vertical positions. The weld pool wants to fall. Pulse MIG’s controlled cooling keeps the weld pool stable in any position. I’ve welded vertical-up 3/8 inch aluminum fillets that would have been impossible with standard MIG.

    4. Aluminum Welding Excellence
    Aluminum’s thermal conductivity makes it notoriously difficult to weld. Pulse MIG handles aluminum beautifully. The rapid cycling prevents the heat buildup that causes burn-through and lack of fusion. Many aluminum fabricators consider pulse MIG essential for quality work.

    5. Reduced Welding Fumes
    The controlled arc produces fewer fumes than standard MIG. This reduction matters for welder health. Studies show pulse MIG can reduce fume exposure by 30-40% compared to short circuit transfer. For production environments, this means compliance with stricter occupational health regulations.

    6. Less Distortion and Warping
    Lower overall heat input means less thermal expansion. Sheet metal assemblies stay truer. Large fabrications require less straightening. I’ve seen frame welds on large assemblies show half the distortion when welded with pulse MIG versus standard transfer.

    7. Higher Deposition Rates
    Despite the pulsing, deposition rates remain competitive. Pulse MIG often achieves higher deposition than short circuit while maintaining better control. This combination means faster welding without sacrificing quality.

    8. TIG-Like Appearance with Double Pulse
    Double pulse MIG creates the classic “stack of dimes” appearance that TIG welding is known for. This aesthetic matters for applications where weld appearance affects perceived quality. Architectural metalwork and show-quality fabrication often use double pulse for this reason.

    Disadvantages and Limitations

    Pulse MIG isn’t perfect. Understanding the limitations helps you make informed decisions about equipment investment:

    1. Higher Equipment Cost
    Pulse MIG welders cost significantly more than standard MIG machines. Budget pulse MIG units start around $700, while professional models range from $2,500 to $8,000+. This investment may not make sense for hobbyists or light users.

    2. Increased Complexity
    More parameters mean more potential confusion. Even with synergic controls, understanding pulse frequency, balance, and trim settings requires learning. Technicians transitioning from standard MIG face a learning curve.

    3. Maintenance Requirements
    Pulse MIG equipment contains more sophisticated electronics. These systems can require more maintenance than transformer-based welders. Repair costs tend to be higher when problems occur.

    4. Not Always Necessary
    For many applications, standard MIG works perfectly well. If you primarily weld thick steel in flat positions, pulse MIG offers minimal advantage. The cost-benefit analysis must consider your specific welding needs.

    5. Wire Sensitivity
    Pulse MIG performs best with high-quality filler metal. Cheap or inconsistent wire can cause feeding issues and weld defects. The process demands attention to consumable quality that standard MIG can sometimes tolerate.

    6. Gas Mixture Requirements
    Optimal pulse MIG requires specific shielding gas mixtures. The standard 75/25 argon/CO2 used for short circuit doesn’t work well. You’ll need higher argon content mixtures (typically 90/10 or 95/5), which cost more.

    Single Pulse vs Double Pulse MIG

    The distinction between single and double pulse confuses many welders. The difference matters depending on your application:

    Single Pulse MIG
    Standard pulse MIG uses a single pulsing cycle. The current switches between peak and background at a fixed frequency. This single pulse pattern provides all the core benefits: reduced spatter, heat control, and all-position capability.

    Single pulse works well for most production applications. Structural steel, general fabrication, and pipe welding typically use single pulse. The welds look good and perform excellently without requiring additional complexity.

    Double Pulse MIG
    Double pulse adds a second layer of pulsing on top of the first. The welder modulates the overall pulse pattern at a lower frequency. This creates a rhythmic deposition that produces TIG-like appearance.

    The visual result is distinctive. You see a regular pattern of overlapping circles that look like TIG welds. This aesthetic matters for architectural work, custom fabrication, and applications where appearance matters.

    Double pulse does take slightly longer to weld. The modulation reduces overall deposition rate. For production welding where appearance isn’t critical, single pulse remains more efficient.

    Double Pulse: An advanced pulse MIG technique that adds a second pulsing layer to create TIG-like “stack of dimes” weld appearance. Also called pulse-on-pulse welding.

    When I work with custom fabricators building show cars or architectural metalwork, I recommend double pulse. The appearance justifies the slight productivity loss. For production welding where speed matters, single pulse gets the job done.

    Pulse MIG Applications and Best Uses

    Pulse MIG excels in specific applications. Understanding where it shines helps you determine if it fits your needs:

    ApplicationPulse MIG ValueWhy It Works
    Auto Body RepairEssentialThin gauge control, minimal distortion
    Aluminum FabricationExcellentManages aluminum’s thermal conductivity
    Stainless SteelVery GoodMaintains corrosion resistance, clean appearance
    Pipe WeldingGoodAll-position capability, root pass control
    Sheet MetalExcellentPrevents burn-through on thin materials
    Structural SteelOptionalBeneficial but not essential
    Heavy PlateLimitedStandard MIG often more practical

    Auto Body and Collision Repair
    Modern vehicles use ultra-high-strength steel and thin aluminum panels. These materials demand precise heat control. Many manufacturers now require pulse MIG for warranty compliance on structural repairs. The reduced distortion ensures proper panel alignment.

    Aluminum Fabrication
    Aluminum conducts heat five times faster than steel. This property causes problems with standard MIG: the weld pool gets too hot, too fast. Pulse MIG’s background current phase allows cooling between pulses. I’ve welded 1/8 inch aluminum with pulse MIG that would have been impossible with short circuit transfer.

    Stainless Steel
    Stainless steel loses corrosion resistance when overheated. Pulse MIG’s controlled heat input preserves the material’s properties. The clean appearance also matters for food service, pharmaceutical, and architectural applications where stainless appearance affects perceived quality.

    Pipe and Pressure Vessel
    All-position welding is mandatory for pipe work. Pulse MIG’s stable weld pool overhead and vertical-up makes it valuable for pipe fabrication. The controlled deposition also helps achieve consistent root passes without suck-back or burn-through.

    Pulse MIG Equipment and Investment Guide

    Choosing pulse MIG equipment requires understanding what you need versus what you want to pay for. Here’s the breakdown by category:

    Budget Pulse MIG Welders ($500-$1,200)
    Entry-level pulse MIG has arrived in the last few years. Brands like YesWelder and Primeweld offer pulse capability at hobbyist prices. These machines typically max out around 200 amps and may lack some advanced features. For light fabrication and learning pulse MIG, they represent excellent value. I’ve tested several that produce surprisingly good results on steel and aluminum up to 3/16 inch.

    Mid-Range Pulse MIG Welders ($1,200-$2,500)
    This sweet spot serves serious hobbyists and small fabrication shops. Everlast, Longevity, and similar brands offer 250-amp machines with better duty cycles and more sophisticated pulse programs. These welders handle daily use better than budget options and typically include multi-process capability (TIG and stick).

    Professional Pulse MIG Welders ($2,500-$8,000)
    Miller and Lincoln Electric dominate this category. The Millermatic 255 and Lincoln Power MIG 360MP represent the gold standard for production welding. These machines offer robust construction, extensive pulse programs, and dealer support networks. When I worked in a production shop running two shifts, these were the only machines that held up.

    Industrial Pulse MIG Systems ($8,000-$25,000+)
    High-end manufacturing uses specialized systems from Fronius, OTC Daihen, and Miller’s industrial division. These systems integrate with automation, offer advanced waveform control, and provide data tracking for quality management. Most fabricators won’t need this level of equipment unless running automated cells.

    Is Pulse MIG Worth the Investment?
    The answer depends on your specific situation. Here’s my framework:

    Skip pulse MIG if you only weld thick steel occasionally. The investment doesn’t pay off for light hobby use. Standard MIG will serve you fine.

    Consider budget pulse MIG if you weld aluminum regularly or work with thin sheet metal. Even entry-level pulse MIG handles these materials noticeably better than standard MIG.

    Invest in professional pulse MIG if you run a fabrication shop, do production welding, or work with automotive materials. The productivity gains and quality improvements justify the investment. Most shops see ROI within 12-18 months through reduced rework and faster production.

    For industrial manufacturing environments with robotic welding systems, pulse MIG capability is essentially mandatory. The technology has become standard in automated applications.

    Pulse MIG Troubleshooting: Common Problems and Solutions

    Pulse MIG presents unique challenges. Here are the most common problems I’ve encountered and their solutions:

    Problem: Excessive Spatter Despite Pulse Mode
    Check your wire quality first. Pulse MIG demands clean, consistent wire. Old or moisture-contaminated wire causes spatter regardless of pulse settings. Verify your drive roll tension and replace worn liners. Finally, confirm your shielding gas mixture contains enough argon. Pulse MIG requires 90%+ argon to function properly.

    Problem: Cold Lapping and Lack of Fusion
    This occurs when the weld doesn’t properly fuse to the base metal. Increase your wire feed speed slightly. The pulse parameters may not be delivering enough filler material. Also check your travel speed; you may be moving too fast. Clean the base metal thoroughly. Pulse MIG is less forgiving of contamination than short circuit transfer.

    Problem: Unstable Arc
    Arc instability often stems from incorrect parameter settings. If using manual mode, consult your welder’s parameter chart for the material thickness and wire type. If using synergic mode, try a different pulse program. Some programs work better for specific applications. Check your contact tip and ensure it’s the correct size for your wire diameter.

    Problem: Poor Weld Appearance
    Appearance issues usually relate to technique or settings. Maintain consistent contact tip-to-work distance (around 3/8 inch). Varying distance changes the arc characteristics and affects weld quality. Use the push technique for most materials; pulling can create convex beads with poor wash-in. Clean the base material between passes if multi-pass welding.

    Problem: Wire Feeding Issues
    Pulse MIG uses higher wire feed speeds, which can cause feeding problems. Check your drive rolls for proper tension and correct groove type. U-groove rolls work better for aluminum. Replace liners if they’ve developed internal wear from wire abrasion. Ensure you’re using quality wire from a reputable manufacturer. Cheap wire often has diameter variations that cause feeding problems at higher speeds.

    Problem: Burn-Through on Thin Materials
    If you’re burning through despite using pulse MIG, reduce your wire feed speed. This lowers overall amperage and heat input. Try a smaller diameter wire; 0.023 inch works better on 20-22 gauge than 0.030 or 0.035 inch. Increase your travel speed slightly. Use stitch welding techniques rather than continuous beads if the material is extremely thin.

    Problem: Porosity
    Porosity in pulse MIG usually indicates gas shielding issues. Check for gas leaks at all connections. Ensure your flow rate is adequate (typically 35-45 CFH for pulse MIG). Shield the weld area from drafts and wind. Clean the base material to remove oil, paint, and coatings. Store your wire properly to prevent moisture contamination.

    Problem: Machine Won’t Enter Pulse Mode
    Some welders require specific conditions to engage pulse mode. Check that your wire feed speed is within the pulse range. Many machines drop out of pulse mode below certain WFS settings. Verify you’ve selected a pulse-capable wire type in the menu. Some machines restrict pulse mode to specific programs. Consult your manual for minimum requirements to enter pulse mode.

    Pulse MIG Setup and Parameter Guide

    Setting up pulse MIG correctly is essential for good results. Here’s a systematic approach:

    Step 1: Material Preparation
    Clean the base material thoroughly. Pulse MIG is less tolerant of contamination than standard MIG. Remove all rust, paint, oil, and coatings. For aluminum, use a stainless steel brush dedicated to aluminum to avoid cross-contamination. Clean surfaces at least one inch back from the weld joint.

    Step 2: Wire Selection
    Choose wire appropriate for your material. ER70S-6 works for most steel applications. Use ER5356 or ER4043 for aluminum. For stainless, ER308L is the standard choice. Match wire diameter to material thickness: 0.023 for 20-22 gauge, 0.030 for 18-16 gauge, 0.035 for 14 gauge and thicker.

    Step 3: Gas Selection
    Pulse MIG requires high argon content. For steel, use 90/10 argon/CO2 or 95/5 argon/CO2. For aluminum, use 100% argon. For stainless, use tri-mix (90% helium, 7.5% argon, 2.5% CO2) or high argon blends. Set flow rate to 35-45 CFH.

    Step 4: Parameter Selection
    Select the appropriate pulse program on your welder. Most machines have programs for steel, aluminum, and stainless. Choose the program matching your wire type and material. Set wire feed speed based on material thickness. Consult your welder’s parameter chart for starting points.

    Step 5: Fine-Tuning
    Make test welds on scrap material of the same type and thickness. Adjust arc voltage (trim) to achieve a smooth, crackling arc sound. Most pulse MIG welds should sound like bacon frying consistently. Adjust wire feed speed up if the weld is too cold or down if too hot. Fine-tune pulse balance if your machine offers this adjustment.

    Step 6: Technique Adjustment
    Use the push technique for most pulse MIG applications. Angle the gun 5-15 degrees in the direction of travel. Maintain consistent contact tip-to-work distance around 3/8 inch. Use steady travel speed; pulse MIG forgives inconsistent speed better than standard MIG, but consistency still produces better results.

    Frequently Asked Questions

    What is pulse MIG welding?

    Pulse MIG welding (GMAW-P) is an advanced MIG welding process that uses rapid current pulsing between high peak and low background values. This pulsing enables precise heat control, reduces spatter by 70-90%, and allows all-position welding. It works exceptionally well on thin materials, aluminum, and stainless steel.

    How does pulse MIG welding work?

    Pulse MIG works by alternating current between a high peak level that melts and transfers filler metal droplets, and a low background level that maintains the arc while allowing cooling. This cycle repeats 50-300 times per second. Each pulse transfers exactly one droplet, preventing the globular transfer that causes spatter in standard MIG.

    What are the advantages of pulse MIG welding?

    Key advantages include: 70-90% less spatter reducing cleanup time, precise heat input control preventing burn-through, all-position welding capability, excellent results on aluminum and thin materials, 30-40% reduction in welding fumes, reduced distortion and warping, and TIG-like appearance with double pulse mode.

    What are the disadvantages of pulse MIG welding?

    Main disadvantages include higher equipment cost ($700-$8,000+ vs $300-$1,500 for standard MIG), increased complexity with more parameters to learn, potentially higher maintenance costs due to sophisticated electronics, and the fact that it’s not necessary for many applications where standard MIG works adequately.

    Is pulse MIG welding worth it?

    Pulse MIG is worth it if you weld regularly, work with thin materials or aluminum, need all-position capability, or run a production environment where quality affects profitability. It’s less essential for hobbyists welding occasional thick steel projects. Most fabrication shops see ROI within 12-18 months through reduced rework and faster production.

    What is double pulse MIG welding?

    Double pulse MIG adds a second layer of pulsing on top of the standard pulse cycle. This creates a rhythmic deposition pattern that produces TIG-like ‘stack of dimes’ weld appearance. It’s valued for architectural work and custom fabrication where weld appearance matters, though it welds slightly slower than single pulse.

    What is the difference between pulse MIG and regular MIG?

    Pulse MIG rapidly alternates between high and low current, while regular MIG maintains constant current. Pulse MIG provides precise heat control, minimal spatter, all-position capability, and better results on thin materials and aluminum. Regular MIG is simpler and cheaper but produces more spatter and struggles with thin materials and out-of-position welding.

    Can you pulse MIG weld aluminum?

    Yes, pulse MIG is excellent for aluminum welding. Aluminum’s high thermal conductivity makes it difficult to weld with standard MIG because heat builds up too quickly. Pulse MIG’s background current phase allows cooling between pulses, preventing burn-through and providing excellent control. Many aluminum fabricators consider pulse MIG essential for quality work.

    Conclusion

    Pulse MIG welding represents a significant advancement over conventional MIG processes. The benefits are real and measurable: less spatter, better heat control, all-position capability, and superior results on challenging materials. For many welders and fabrication businesses, pulse MIG offers productivity improvements that justify the investment.

    That said, pulse MIG isn’t for everyone. Hobbyists welding occasional projects may find standard MIG perfectly adequate. The investment in pulse MIG equipment makes the most sense when you’re welding regularly, working with thin materials or aluminum, or running a production environment where quality and speed directly impact profitability.

    The technology continues to evolve. Budget pulse MIG options have made the technology accessible to serious DIYers. Synergic controls have reduced the learning curve. If you’re serious about welding quality and work with materials that benefit from pulse MIG’s advantages, the investment likely makes sense.

    After years of welding with both standard and pulse MIG equipment, I reach for pulse MIG whenever quality matters. The results speak for themselves, and the time saved on cleanup and rework adds up quickly. For anyone doing production welding, aluminum fabrication, or auto body work, pulse MIG has become essential equipment rather than a luxury option.