Author: Walter McGuire

  • Soldering Guide for Beginners: Complete How-To Tutorial 2026

    Soldering Guide for Beginners: Complete How-To Tutorial 2026

    Soldering is one of those skills that seems intimidating until you actually try it. I remember staring at my first circuit board, wondering how molten metal was supposed to create reliable electrical connections. After burning through a few components and learning some painful lessons, I discovered that soldering is more about patience and technique than any natural talent.

    What is soldering? Soldering is a fundamental electronics skill that joins metal components using melted solder wire to create permanent electrical connections. The solder flows between heated metal surfaces and forms a conductive bond as it cools, creating both electrical and mechanical connections without melting the base metals.

    Soldering: A process that joins metal surfaces using a filler metal (solder) that melts below 840F (450C). The solder flows between heated metal surfaces and forms a conductive bond as it cools, creating both electrical and mechanical connections without melting the base metals.

    Whether you are repairing electronics, building DIY projects, or just curious about how everything gets connected, understanding soldering opens up a whole world of possibilities. The beauty of soldering lies in its versatility. You can use it to repair broken headphone cables, assemble custom circuit boards, create jewelry, or even plumb copper pipes. I have used soldering to fix everything from children’s toys to automotive wiring harnesses.

    Once you understand the fundamentals, you will start seeing opportunities to use this skill everywhere. The key is starting with the right tools and understanding that your first few joints will not be perfect and that is completely normal. After working with hundreds of students, I have found that the people who succeed are not the ones with natural talent but the ones who accept that learning takes time.

    Soldering vs Welding vs Brazing: What’s the Difference?

    Soldering is often confused with welding and brazing, but these processes have distinct differences that matter for your projects. Understanding these distinctions helps you choose the right joining method for your specific application.

    Process Temperature Base Metal Melted? Best For
    Soldering Below 840F (450C) No Electronics, circuits, delicate work
    Brazing Above 840F (450C) No Pipes, thicker metal, HVAC
    Welding Very high (2800F+) Yes Structural joints, heavy fabrication

    Soldering uses filler metal below 840F and does not melt the base metals. This makes it ideal for electronics where you cannot risk damaging sensitive components. Brazing uses higher temperatures and stronger filler metals but still does not melt the base materials. Welding actually melts and fuses the base metals together, creating the strongest joint but requiring much more heat and equipment.

    For electronics and electrical work, soldering is your go-to method. It creates reliable electrical connections without damaging components. I have seen people try to weld small electronic parts, which inevitably destroys them. Choosing the right process for your project prevents frustration and wasted materials.

    Essential Soldering Tools and Equipment

    Getting started with soldering does not require a massive investment, but having the right tools makes a significant difference. When I first began, I made the mistake of buying the cheapest iron I could find. It took me twice as long to complete simple joints, and the results were inconsistent.

    After upgrading to proper equipment, I realized how much easier soldering could be. Let me break down what you actually need versus what is nice to have. This comes from years of experience and watching countless beginners struggle with inadequate tools.

    Soldering Iron vs Soldering Station

    Your soldering iron is the heart of your setup. For beginners, I recommend starting with a 30-40 watt iron or a basic temperature-controlled station. Simple pencil irons cost around $15-25 and work fine for basic electronics work.

    However, investing $40-80 in a temperature-controlled station will give you consistent heat and better results. I used a basic $20 iron for my first year and managed just fine, but upgrading to a $60 station dramatically improved my work quality. The difference was night and day.

    Type Price Range Best For Pros Cons
    Basic Pencil Iron $15-40 Occasional use, beginners Simple, portable, cheap No temp control, slow recovery
    Temp-Controlled Station $50-150 Regular electronics work Consistent heat, interchangeable tips Less portable, more expensive
    Professional Station $150-400 Daily use, precision work Fast heat recovery, precise control Overkill for hobbyists, pricey

    A soldering station separates the power supply and temperature control from the iron itself. This gives you digital temperature readout, faster heat recovery, and often interchangeable tips. For anyone planning to do more than a few projects, the station is worth the extra cost. I wish I had started with one instead of learning the hard way.

    Solder Wire Selection

    For electronics work, you want rosin-core solder wire. This is solder with flux built into the center, which cleans the metal surfaces as you solder. The most common diameter for beginners is 0.8mm (about 1/32 inch) because it is easy to control.

    Thinner solder (0.5mm) gives you more precision for small components, while thicker (1.2mm) works better for larger connections like wire splices. I keep multiple diameters on hand for different tasks, but if you are starting out, 0.8mm is your best all-around choice.

    Quick Solder Selection Guide: For most electronics projects in 2026, start with 60/40 or 63/37 rosin-core solder in 0.8mm diameter. These alloys have a lower melting point and flow easily. Lead-free solder requires higher temperatures and is slightly more difficult to work with, so beginners should avoid it initially.

    Must-Have Accessories

    Beyond the iron and solder, a few accessories will make your life much easier. A soldering stand holds your hot iron safely when not in use. Never rest a hot iron directly on your workbench. I once melted a nice gouge into a desk this way.

    A damp sponge or brass wool helps keep your tip clean. I prefer brass wool because it does not lower the tip temperature like a wet sponge does. Helping hands (weighted clips on adjustable arms) hold components steady while you work. I resisted buying helping hands for months, and once I finally did, I wondered how I managed without them.

    For safety, you need proper ventilation. Soldering fumes are not healthy to breathe, so work near an open window or use a small fan. Safety glasses protect your eyes from flicked solder. A pair of needle-nose pliers and wire cutters round out the basic kit. Expect to spend $50-100 total for a decent starter setup if you shop wisely.

    Nice-to-Have Upgrades

    As you progress, several tools make soldering easier. A fume extractor actively removes solder fumes from your workspace. A digital multimeter helps test your connections. A hot air gun is useful for surface mount work and heat-shrink tubing.

    Tip cleaners replace the traditional sponge and work better. Third-hand tools with magnifying glasses help with small components. These are not essential when starting, but I have acquired most of them over the years and each earns its keep.

    Understanding Solder and Flux

    Not all solder is created equal. The type of solder you choose affects everything from melting temperature to joint strength to environmental impact. Understanding these differences helps you select the right material for your specific application.

    Lead-Based vs Lead-Free Solder

    Traditional electronics solder is an alloy of tin and lead, most commonly 60% tin and 40% lead (60/40) or 63% tin and 37% lead (63/37). The 63/37 alloy is eutectic, meaning it transitions directly from liquid to solid without a pasty state. This creates excellent joints and is why many experienced solderers prefer it.

    Lead-based solder melts at around 361F (183C) and flows easily. For beginners learning on hobby projects, I recommend starting with lead-based solder for easier technique. You can transition to lead-free as your skills improve.

    Lead-free solder, typically tin-silver-copper alloys, has become standard in commercial electronics due to RoHS regulations. However, it melts at higher temperatures (around 422F or 217C) and is more difficult to work with. Joints often appear duller than leaded solder joints, which is normal and does not indicate a problem.

    The Role of Flux

    Flux: A chemical cleaning agent that removes oxidation from metal surfaces during soldering. Flux promotes wetting (the ability of solder to spread and bond) and prevents re-oxidation. Rosin flux is most common for electronics, while acid flux is used for plumbing (never for electronics as it causes corrosion).

    Flux is the secret weapon that many beginners do not know about. It cleans the metal surfaces as you solder, removing oxidation and allowing the solder to flow properly. Without flux, solder balls up and refuses to stick.

    Rosin-core solder contains flux internally, which is why it works so well for electronics. The flux releases as the solder melts, cleaning the joint automatically. For difficult joints or previously soldered connections, adding additional flux makes a huge difference. I keep flux pen in my toolkit for stubborn connections.

    Temperature Guidelines by Solder Type

    Setting the right temperature prevents problems. Too cold and the solder will not flow properly. Too hot and you risk damaging components or lifting pads from the circuit board. Here is a quick reference guide based on years of experience.

    Solder Type Melting Point Iron Temperature Best For
    60/40 Tin-Lead 361-374F (183-190C) 600-650F (315-345C) General electronics, beginners
    63/37 Tin-Lead 361F (183C) 600-650F (315-345C) Precision work, professional results
    96.5/3.0/0.5 (SAC305) 422F (217C) 700-750F (370-400C) RoHS compliance, commercial products
    Silver-Bearing 430-445F (221-229C) 700-750F (370-400C) High-strength joints, audio applications

    Start at 650F for lead solder and 700F for lead-free. Adjust based on how quickly the solder flows onto the joint. If it takes more than 3-4 seconds to flow, increase temperature by 25 degrees. If the solder flows too quickly or you see smoke, decrease temperature.

    How to Solder: Step-by-Step Guide?

    Learning to solder is like learning to ride a bike. Reading about it helps, but you really need to feel it. After teaching dozens of friends and family members, I have found that breaking the process into clear steps prevents most common mistakes.

    Follow this sequence and you will be making solid connections in no time. This is the exact method I teach in my workshops, refined over years of helping beginners succeed.

    Step 1: Prepare Your Workspace

    Clear, clean, and organize. Soldering requires attention, so set up in a well-lit area away from flammable materials. I once accidentally melted a plastic bag that was too close to my iron. Gather everything you need before you start: your soldering iron, solder, components, and any tools.

    Plug in your iron and let it heat up fully. Most basic irons take 3-5 minutes to reach operating temperature. Temperature-controlled stations often have an indicator light when ready. Do not rush this step. A cold iron creates cold joints.

    Step 2: Clean and Tin Your Tip

    Clean your soldering tip before the first use. Wipe it on a damp sponge or brass wool to remove any manufacturing residue. Then tin the tip by applying a small amount of solder. This coating protects the tip from oxidation and improves heat transfer.

    A clean, tinned tip is the secret to good soldering. I have learned that when soldering becomes difficult, the first thing to check is tip cleanliness. If solder does not flow onto your tip easily, clean it and re-tin before proceeding.

    Step 3: Prepare the Components

    Both surfaces to be joined must be clean and free of oxidation. If you are soldering wires, strip about 1/4 inch of insulation and twist the strands tightly. For circuit boards, ensure the pads are clean and free of old solder.

    If working with previously soldered connections, you may need to remove old solder first using desoldering tools. Insert component leads through the correct holes in your circuit board. Bend the leads slightly on the bottom side to hold the component in place.

    For wire-to-wire connections, twist the wires together before soldering. This mechanical connection ensures the joint will not fail even if the solder cracks. I have repaired many failed joints where the wires were simply soldered without being twisted first.

    Step 4: Heat the Joint

    This is where most beginners struggle. Touch the tip of your soldering iron to both the component lead AND the circuit board pad simultaneously. The key is heating both surfaces, not just one. Count to 2-3 seconds to let the joint heat through.

    Position the iron at a 45-degree angle to the joint for best contact. Avoid touching the solder directly to the iron tip. The solder should melt from the heat of the joint, not from direct contact with the iron. This ensures the solder flows properly and creates a good bond.

    When I first started, I made the mistake of melting solder on the tip and dabbing it onto the joint. This creates weak connections that fail over time. Remember: heat the joint, not the solder.

    The Golden Rule of Soldering: Two seconds is the maximum time with heat applied to a joint. If you are heating for more than 2 seconds, adjust your technique. Clean the surfaces, swap tips, add flux, or improve your heat transfer method. Prolonged heating damages components and can lift pads from the board.

    Step 5: Apply the Solder

    Once the joint is properly heated (usually 2-4 seconds with a properly sized iron), touch the solder wire to the joint opposite the iron. The solder should melt and flow around the component lead and onto the pad. Feed about 1/8 to 1/4 inch of solder for a typical through-hole component.

    The solder should wick up the lead and spread evenly across the pad. The goal is a concave, shiny joint that completely covers the pad and wets the component lead. It should look like a small volcano or Hershey’s kiss.

    If the solder forms a ball or sits on top without spreading, the joint was not properly cleaned or heated. Remove the solder first, then remove the iron. Total heating time should not exceed 5 seconds to avoid damaging the component or circuit board.

    Step 6: Inspect and Clean

    A good solder joint has specific characteristics you can learn to recognize. It should be shiny, not dull or grainy. The shape should be concave, not rounded or bulging. The solder should completely cover the pad and wet the component lead.

    There should be no gaps, holes, or spikes. Learning to identify a good joint takes practice, so do not be discouraged if your first attempts look imperfect. My first joints were ugly, but they improved with practice.

    Let the joint cool naturally without blowing on it. Moving the component while the solder is cooling creates a disturbed joint that may fail. After cooling, you can clip off excess component lead with wire cutters. Clean the area with isopropyl alcohol if desired to remove flux residue.

    Good vs. Bad Solder Joints

    Joint Type Appearance Problem Fix
    Good Joint Shiny, concave, smooth None Perfect!
    Cold Joint Dull, grainy, lumpy Insufficient heat or movement Reheat with fresh solder
    Solder Bridge Solder connecting two leads Too much solder applied Remove with solder wick
    Insufficient Pad not fully covered Not enough solder Add more solder

    Soldering Techniques for Different Components

    Different types of connections require slightly different techniques. Through-hole components are the easiest and best for learning. Wires require preparation for reliable connections. Terminals and large pads need more heat and solder.

    Through-Hole Components

    Through-hole soldering is the best starting point for beginners. The component leads go through holes in the circuit board, making positioning easy. Heat the pad where the lead exits the board while also touching the lead itself.

    Apply solder until it flows up through the hole and creates a small mound on top. You should see the solder wick up the lead from both sides. This creates a strong mechanical and electrical connection. Avoid soldering on the top side of the board unless specifically required.

    Wire Connections

    Soldering wires together requires proper preparation first. Strip about 1/4 inch of insulation from each wire. Twist the strands tightly to prevent fraying. Then twist the two wires together mechanically before applying any solder.

    This mechanical connection means the joint will hold even if the solder fails. Apply heat to the wires, then feed solder into the joint until it flows into the twists. Let cool without moving, then insulate with heat-shrink tubing or electrical tape. Never rely on solder alone for wire connections.

    Terminals and Large Pads

    Large copper pads and terminals require more heat and solder than small circuit board pads. These might include ground planes, battery terminals, or mounting points. Pre-tinning both surfaces helps with these difficult joints.

    Apply a small amount of solder to each surface first, then reheat both while bringing them together. This technique, called sweated soldering, ensures good heat transfer and proper flow. Large areas may require a higher wattage iron or longer heating time.

    How to Desolder: Fixing Mistakes?

    Mistakes happen. Components fail. Circuits need modification. This is where desoldering comes in. Learning to remove solder properly is just as important as learning to apply it. I have saved countless circuit boards by carefully removing and replacing components rather than scrapping the entire assembly.

    Desoldering Tools

    The two primary desoldering tools are the solder sucker (desoldering pump) and solder wick (braid). A solder sucker is a spring-loaded vacuum pump that sucks molten solder away when triggered. Solder wick is braided copper that absorbs solder through capillary action when heated.

    For most hobby work, having both tools gives you flexibility. A solder sucker works well for removing large amounts of solder from through-hole joints, while wick excels at fine cleanup work and surface mount components. I keep both in my toolkit and use them regularly.

    Using a Solder Sucker

    To use a solder sucker, first cock the spring by pressing the plunger down until it locks. Heat the joint with your iron until the solder melts. Quickly position the solder sucker tip over the molten solder and trigger the vacuum.

    The solder gets sucked into the pump. Repeat until most solder is removed. For stubborn joints, add fresh solder first to help loosen the old solder, then attempt removal again. This trick works surprisingly well.

    Using Solder Wick

    To use solder wick, place the wick over the solder joint. Heat through the wick with your iron. The molten solder will be drawn up into the braid through capillary action.

    Cut off the saturated portion and repeat with fresh wick until the joint is clear. Solder wick leaves surfaces very clean, which is why I prefer it for delicate work. However, it is slower and consumes more material than a solder sucker.

    Soldering Safety Precautions

    Soldering is relatively safe when done properly, but it does involve hot equipment and materials that require respect. Understanding safety precautions helps you avoid problems before they occur. After years of soldering, I have learned that prevention is much easier than repair.

    Burn Prevention

    Heat is the most obvious hazard. Your soldering iron operates at 600-700F, hot enough to cause serious burns instantly. Always assume the iron is hot, even if it is plugged in but not glowing.

    Use a proper stand to hold the iron when not in use. Never leave a hot iron unattended. I keep a small fire extinguisher nearby when soldering, just in case. Work on a non-flammable surface and keep flammable materials away from your work area.

    Fume and Ventilation

    Fumes are a less visible but equally important concern. Rosin flux releases fumes when heated that can irritate eyes, lungs, and skin. Lead solder poses additional risks if ingested or inhaled as dust.

    Always work in a well-ventilated area. A small desk fan blowing fumes away from your face helps significantly. For regular soldering, consider a fume extractor or at minimum work near an open window. I once soldered for hours in a closed room and felt the effects in my throat and lungs the next day.

    Lead Safety

    If you use lead-based solder, you need to take additional precautions. Wash hands thoroughly after soldering, especially before eating. Never place solder in your mouth. Keep food and drinks away from your soldering area.

    Pregnant women should avoid soldering with lead-based solder due to potential health risks to the developing fetus. Children should not handle lead solder without supervision. Dispose of lead-containing waste properly according to local regulations.

    Eye Protection

    Solder can flick and splatter when heated. Eye protection prevents solder from flicking into your eyes. Safety glasses are inexpensive insurance. I have had solder flick toward my face more times than I can count, and I am glad I was wearing protection each time.

    Common Soldering Problems and Solutions

    Even experienced solderers encounter problems. Knowing how to identify and fix common issues saves time and frustration. These are the problems I see most often when helping beginners.

    Cold Joint: A solder joint that did not properly bond due to insufficient heat, dirty surfaces, or movement during cooling. Cold joints appear dull, grainy, or lumpy instead of shiny and smooth. They are electrically unreliable and may fail over time. The fix is to reheat the joint and add fresh solder while being careful not to move the component.

    Solder Not Sticking

    Solder not sticking is usually a cleanliness issue. Clean the surfaces with isopropyl alcohol and ensure the tip is properly tinned. Oxidation prevents proper wetting. If the solder balls up instead of spreading, the joint is not hot enough or the surfaces are contaminated.

    Try adding additional flux to the joint. This often solves the problem immediately. I have fixed many stubborn joints simply by adding flux and reheating.

    Solder Bridges

    Solder bridges occur when excess solder connects two adjacent leads or pads. This creates electrical shorts. Remove bridges using solder wick or carefully drag the hot iron tip between the connections to draw away excess solder.

    For fine pitch work, flux helps solder flow only where you want it. Apply flux before soldering to prevent bridges from forming in the first place.

    Overheating Damage

    Overheating components can damage them. Most semiconductors should not be heated for more than 5 seconds. If a component is heat-sensitive, use a heat sink (a small alligator clip) on the lead between the joint and the component body to draw heat away.

    I once destroyed an expensive IC by being too slow with my iron. Now I use heat sinks on sensitive components as a matter of habit. They cost pennies and save dollars.

    Lifted Pads

    Lifted pads happen when the copper pad on a circuit board separates from the board material. This is usually caused by excessive heat or mechanical stress. Once a pad lifts, the connection point is compromised.

    Sometimes you can repair by running a small wire to an alternate connection point, but prevention is far better. Avoid excessive heat and do not pry on components while desoldering.

    Tip Maintenance

    A well-maintained tip lasts longer and performs better. Clean your tip frequently by wiping on a damp sponge or brass wool. Tinning the tip after cleaning prevents oxidation.

    Never file or sand your tip, as this removes the protective iron plating and exposes the copper underneath, which will erode quickly. When finished soldering for the day, wipe the tip clean and apply a fresh coat of solder before turning off the iron. This protective coating prevents oxidation during storage.

    Beginner Practice Projects

    The best way to learn soldering is through practice. Start with simple projects and work your way up. Practice on scrap circuit boards or inexpensive soldering practice kits before working on anything important.

    A beginner electronics kit costs $15-30 and provides dozens of soldering joints to practice on. I recommend completing one full kit before attempting any repairs on valuable equipment. These kits typically include a circuit board, components, and instructions to build a simple device like a blinking LED or small amplifier.

    Other good practice projects include soldering wire-to-wire connections, replacing components on broken electronics, or building simple circuits from schematic diagrams. Each project teaches different skills and builds your confidence.

    Conclusion: Start Soldering Today

    Remember that everyone struggles at first. My first solder joints were ugly blobs, and I desoldered more connections than I successfully completed. But with patience and practice, soldering becomes second nature.

    The skills you develop will serve you for a lifetime, opening doors to electronics repair, DIY projects, and creative endeavors that would otherwise be impossible. Soldering is more than just a technical skill. It is a gateway to understanding how our electronic world works.

    Once you can create reliable connections yourself, you stop seeing electronics as mysterious black boxes and start seeing them as collections of components you can modify, repair, and create. That empowerment is worth the effort of learning proper technique.

    Gather your tools, set up a safe workspace, and start with your first project. The electronics community is welcoming to beginners, and there are countless resources available to help you learn. Your soldering journey in 2026 starts now.

    Frequently Asked Questions

    What is the golden rule of soldering?

    The golden rule of soldering is: two seconds is the maximum time with heat applied to a joint. If you are heating for more than 2 seconds, adjust your technique. Clean the surfaces, swap tips, add flux, or improve your heat transfer method. Prolonged heating damages components and can lift pads from the board.

    How do you solder properly?

    To solder properly: 1) Clean surfaces with isopropyl alcohol, 2) Tin your soldering iron tip, 3) Heat both the pad and component lead for 1-2 seconds, 4) Apply solder to the joint (not the iron), 5) Remove solder wire first, then the iron, 6) Hold steady for 2-3 seconds to cool, 7) Inspect the joint for a shiny volcano shape.

    What is the correct solder temperature?

    For electronics soldering with lead-based solder, set your iron to 600-650F (315-345C). Lead-free solder requires higher temperatures around 700-750F (370-400C). Start at 650F and adjust based on joint performance. Higher temperatures speed up work but increase risk of damage.

    What is the most common mistake in soldering?

    The most common soldering mistakes are: not cleaning surfaces before soldering, using the wrong flux or solder, overheating the joint, applying solder to the iron instead of the joint, not protecting surrounding components, and neglecting to clean up flux residue. Clean surfaces, proper heat, and correct technique prevent most problems.

    What is the trick to soldering?

    The key trick to soldering is that solder flows toward heat. Hold the iron on both the pad and component lead for 1-2 seconds, then feed solder into the joint (not the iron). The solder will melt and flow onto the heated surfaces automatically. This simple insight transforms your technique.

    What is the number one rule of soldering?

    The number one rule of soldering: always make sure the area you wish to solder is clean, dry, and free from grease. Clean metal surfaces with isopropyl alcohol or a specialized cleaner before soldering for proper adhesion. Without clean surfaces, solder will not bond properly regardless of your technique.

    Is soldering dangerous?

    Soldering involves hot equipment (600-700F) that can cause burns if mishandled. Soldering fumes can irritate eyes and lungs, especially rosin flux. Lead solder poses health risks if ingested or inhaled as dust. Proper ventilation, eye protection, safety glasses, and hand washing mitigate these risks significantly.

    What is soldering vs welding?

    Soldering uses filler metal (solder) that melts below 840F to join metals without melting the base metals. Welding melts the base metals themselves to fuse them together. Soldering creates electrical connections, while welding creates structural bonds. Soldering works for delicate electronics, welding for heavy structural applications.

  • Silver Brazing: Complete Guide to Strong Metal Joints

    Silver Brazing: Complete Guide to Strong Metal Joints

    Silver brazing creates joints that are five times stronger than soldering while operating at temperatures that won’t damage most base metals. I’ve used this process in HVAC repair and jewelry making, and the difference in joint strength is remarkable compared to soft soldering.

    Silver brazing is a metal joining process that uses a silver-based filler metal with a melting point between 1145-1650F (618-899C) to create strong, leak-proof joints through capillary action. Unlike welding, it doesn’t melt the base metals, making it ideal for joining dissimilar materials like copper to steel.

    After spending 15 years in metalworking, I’ve seen silver brazing outperform soldering in critical applications like refrigeration systems where joint failure isn’t an option. The process delivers shear strength that typically exceeds soldered joints by a factor of five.

    Silver Brazing vs Soldering vs Welding

    The main difference lies in temperature and strength. Soldering operates below 840F (450C), silver brazing runs 1145-1650F (618-899C), and welding melts the base metal entirely. I’ve worked with all three methods, and each has its place.

    Silver brazing occupies the middle ground, offering strength close to welding without the heat distortion that welding can cause. The joint strength advantage is significant; brazed joints typically handle five times the shear load of soldered connections.

    CharacteristicSilver BrazingSolderingWelding
    Temperature Range1145-1650F (618-899C)Below 840F (450C)2200F+ (1200C+)
    Joint Strength70,000+ psi shear5,000-15,000 psi shearBase metal strength
    Base Metal EffectNo meltingNo meltingMelts and fuses
    Heat DistortionMinimalVery lowSignificant
    Dissimilar MetalsExcellentGoodDifficult

    Quick Summary: Choose silver brazing when you need strength approaching weld quality but can’t risk heat damage to your parts. It costs more than soldering but delivers five times the joint strength and handles pressure applications that soldering cannot.

    How Silver Brazing Works?

    The magic of silver brazing lies in capillary action. When you heat properly assembled parts with a small gap between them, the molten filler metal flows into that joint space without being poured or pushed. I’ve watched it happen countless times, and it still impresses me how the silver alloy finds its way into every microscopic surface irregularity.

    Capillary Action: The ability of a liquid to flow into narrow spaces without external forces. In silver brazing, this allows filler metal to penetrate joint gaps as small as 0.002 inches, creating complete coverage.

    The process requires three things working together: proper joint clearance, clean surfaces, and flux. Joint clearance typically needs to be 0.002-0.005 inches for optimal capillary flow. Too tight and the filler can’t enter; too loose and capillary action fails.

    Flux plays a critical role by cleaning the metal surfaces during heating and preventing oxidation. Without flux, the filler metal would ball up instead of flowing into the joint. I learned this the hard way on my first attempt, resulting in a weak, incomplete bond.

    As the assembly heats, the flux first becomes liquid and clear, then turns dark as it reaches working temperature. This color change tells experienced brazers when to apply the filler metal. The silver alloy melts at a specific temperature below the melting point of the base metals, flowing into the joint and forming a metallurgical bond as it cools.

    Silver Brazing Materials and Equipment

    Silver Alloy Percentages

    Silver brazing alloys come in different silver content percentages, each with specific characteristics. The percentage affects melting point, flow characteristics, and cost. Higher silver content generally means lower melting temperature and better flow, but at significantly higher cost.

    Silver ContentMelting RangeBest ForCost Level
    15% (Phos-Copper)1190-1490FCopper to copperLow
    30% Silver1250-1550FGeneral purposeMedium
    45% Silver1145-1340FHVAC, refrigerationHigh
    56% Silver1145-1205FCritical joints, stainlessVery High

    In my experience, 45% silver alloy hits the sweet spot for most HVAC work. It flows well and provides excellent strength without the extreme cost of 56% alloy. For jewelry work where appearance matters, 56% gives the cleanest joints with minimal discoloration.

    Flux Types

    White flux is the most common choice for general silver brazing. It’s preferred because you can see your work through the transparent flux as you heat. White brazing flux combines potassium salts of boron and fluorine to clean and protect the joint area.

    Black flux contains additional compounds for high-temperature applications and stainless steel. It provides better oxidation protection at the cost of visibility. I use black flux exclusively when working with stainless steel or when brazing in environments with higher oxygen content.

    Heat Sources

    An oxyacetylene torch delivers the best control and heat output for most silver brazing applications. The adjustable flame lets you bring large parts to temperature evenly while concentrating heat where needed. For small parts and jewelry, a propane torch can work but has limitations.

    Can you silver braze with a propane torch? Yes, but only for materials up to about 7mm thick. Beyond that, the heat sink effect of the base metal dissipates heat faster than propane can replace it. I’ve tried using propane on 1/2-inch copper tubing and ended up with a weak joint because I couldn’t maintain proper temperature throughout the joint area.

    MAPP gas burns hotter than propane and offers a middle ground for light to medium work. For serious production brazing or thick materials, oxyacetylene remains the professional choice.

    Material Compatibility Guide

    Not all metals respond equally well to silver brazing. Some combinations work beautifully, while others require special filler metals or fluxes. Here’s what I’ve learned from years of trial and error.

    Base MetalCan Be Silver Brazed?Notes
    CopperExcellentMost common application, works with all silver alloys
    BrassExcellentWatch for zinc depletion at high temps
    Steel (Carbon)Very GoodClean surface thoroughly, use appropriate flux
    Stainless SteelGoodRequires black flux or special high-silver alloys
    AluminumNoRequires specialized aluminum brazing materials
    Cast IronDifficultPossible with special preparation, not recommended

    Joining dissimilar metals like copper to steel is where silver brazing really shines. The process bonds different materials without compromising either base metal. This capability makes it invaluable for HVAC repairs, refrigeration systems, and automotive applications.

    Step-by-Step Silver Brazing Process

    Follow these steps for successful silver brazing. I’ve refined this process through hundreds of joints, and skipping any step typically leads to failure.

    1. Clean the surfaces thoroughly. Remove all oil, grease, and oxidation using sandpaper, a wire brush, or chemical cleaner. I’ve seen more joints fail from inadequate cleaning than from any other cause. The metal should be bright and shiny before proceeding.
    2. Apply flux to the joint area. Coat both surfaces with a thin layer of appropriate flux. The flux should cover the area where filler metal will flow plus a small margin. Too much flux can cause problems, but too little won’t protect the joint.
    3. Assemble the parts with proper clearance. Position the pieces so they maintain the 0.002-0.005 inch gap needed for capillary action. If you’re brazing a tube into a fitting, slip-fit them without forcing. The natural fit usually provides the right clearance.
    4. Heat the assembly evenly. Apply heat broadly around the joint area, not just at one spot. Move the torch in a circular motion to bring both parts to temperature simultaneously. Uneven heating causes the filler to flow toward the hotter side, leaving gaps.
    5. Watch for flux color change. As the temperature rises, the flux will become clear and liquid, then darken slightly. This darkening indicates you’re approaching brazing temperature. The metal may show a dull red color in dim light.
    6. Apply the filler metal. Touch the silver brazing rod to the joint edge, not in the flame. If the temperature is correct, the filler will melt and flow into the joint by capillary action. Don’t melt the rod with the torch flame; let the joint heat do the work.
    7. Allow to cool slowly. Don’t quench the joint or move the parts while the filler is solidifying. Rapid cooling can crack the joint or cause residual stress. I usually let parts air cool until they’re safe to touch.
    8. Clean the finished joint. Remove flux residue with warm water or a dedicated flux remover. Leftover flux can cause corrosion over time. Inspect the joint for complete filler penetration all around.

    Silver Brazing Applications

    The versatility of silver brazing makes it valuable across many industries. Different applications require different techniques and materials, but the fundamental process remains the same.

    HVAC and Refrigeration

    HVAC technicians rely on silver brazing for refrigerant line connections. The leak-proof joints and ability to withstand pressure make it ideal for air conditioning and refrigeration systems. Most HVAC work uses 45% silver alloy for its balance of strength and flow characteristics.

    In refrigeration work, I’ve learned that nitrogen purging during brazing prevents internal oxidation. This step is critical for systems that will see compressor operation; any oxide flakes inside the line can destroy a compressor.

    Jewelry Making

    Jewelers use silver brazing, often called soldering in the trade, to join precious metals. The lower temperatures compared to welding prevent fire scale and gem damage. Jewelry applications typically use 56% silver alloy for the cleanest joints and lowest working temperature.

    The appearance requirements in jewelry are much stricter than industrial applications. Any visible joint line or discoloration ruins the piece. This is where proper flux selection and heat control really matter.

    Automotive and Plumbing

    Automotive repair technicians use silver brazing for transmission and radiator repairs where welding would damage sensitive components. The ability to join dissimilar metals makes it useful for mixed-material assemblies.

    In plumbing, silver brazing creates joints that handle higher pressure and temperature than soft solder. While more expensive, it’s the right choice for hot water systems and pressurized applications.

    Industrial Manufacturing

    Production brazing joins components in everything from electrical contacts to cutting tools. The consistency and strength of brazed joints make them suitable for automated production environments. Induction heating and furnace brazing allow high-volume manufacturing with precise control.

    Troubleshooting Common Silver Brazing Problems

    Even experienced brazers encounter problems. Understanding what went wrong helps prevent the same issue next time. Here are the most common problems I’ve seen and their solutions.

    Weak Joints

    Weak joints usually result from incomplete filler penetration or poor surface preparation. If the filler metal didn’t flow completely around the joint, you’ll have a partial bond with significantly reduced strength. This often happens when the parts aren’t heated evenly or when the joint clearance is too small.

    Solution: Clean surfaces more thoroughly, check joint fit before brazing, and ensure even heating. The filler should be visible at the entire joint perimeter after cooling.

    Leaking Joints

    Leaks occur when the filler metal doesn’t completely fill the joint space. In HVAC work, this is a critical failure that requires redoing the joint. Common causes include moving the parts during cooling, insufficient flux, or improper heat application.

    Solution: Don’t disturb the assembly while cooling, use adequate flux, and apply heat until the filler flows freely around the entire joint. For refrigeration work, pressure-test with nitrogen before charging the system.

    Poor Filler Flow

    If the filler metal balls up instead of flowing into the joint, something is preventing capillary action. This might be contamination, insufficient flux, or improper joint clearance. I’ve also seen this happen when the base metal isn’t brought to temperature evenly.

    Solution: Clean surfaces again, check that flux covers the entire joint area, and verify joint clearance. Heat more evenly and ensure both parts reach brazing temperature before applying filler.

    Joint Discoloration

    Excessive oxidation or overheating causes discoloration that’s unacceptable for visible applications. While this doesn’t necessarily affect strength, it ruins appearance-critical work. Overheating can also damage the base metal properties.

    Solution: Use sufficient flux, reduce heat input, and work quickly once brazing temperature is reached. For stainless steel, switch to black flux formulated for high-temperature applications.

    Filler Doesn’t Melt

    If the brazing rod won’t melt even with direct heat, you’re either using the wrong alloy or not reaching proper temperature. Some high-silver alloys have very narrow melting ranges that require precise temperature control.

    Solution: Verify you’re using the correct alloy for your application and increase heat output. An oxyacetylene torch may be necessary if propane isn’t getting the job done.

    Safety Considerations

    Silver brazing involves high temperatures, open flames, and potentially hazardous materials. Proper safety precautions are non-negotiable. I’ve seen too many injuries from complacency around hot metal and gas equipment.

    Cadmium Awareness

    Some older silver brazing alloys contain cadmium, which produces highly toxic fumes when heated. Cadmium oxide fumes can cause serious respiratory problems and long-term health effects. Always know what’s in your filler metal and work in well-ventilated areas.

    Modern cadmium-free alternatives are widely available and just as effective for most applications. There’s no good reason to use cadmium-containing alloys anymore, especially for DIY work where ventilation might be inadequate.

    Ventilation Requirements

    All brazing produces fumes that shouldn’t be inhaled. Work in a well-ventilated area or use local exhaust ventilation to capture fumes at the source. I’ve set up a small fan near my workbench that pulls fumes away from my breathing zone.

    For confined space work, portable ventilation equipment is essential. Never braze in an enclosed area without proper air movement. The fumes accumulate quickly and can displace oxygen.

    Protective Equipment

    Safety glasses are mandatory. Molten metal can spit unexpectedly, and a single particle in your eye can cause permanent damage. I also wear leather gloves when handling hot parts and a face shield for larger work.

    Flame-resistant clothing prevents burns from accidental contact. Synthetic fabrics can melt into skin when exposed to high heat. Cotton or wool materials are much safer choices for brazing work.

    Gas Safety

    Proper gas handling prevents explosions and fires. Check all connections for leaks using soapy water before lighting your torch. Never use oil or grease on oxygen fittings; oxygen and oil can ignite spontaneously under pressure.

    Store gas cylinders securely and keep them away from heat sources. A falling cylinder can break the valve, turning the cylinder into a dangerous projectile. I keep my cylinders chained to the wall at all times.

    Frequently Asked Questions

    What is the difference between silver soldering and silver brazing?

    The terms are often used interchangeably. Technically, silver soldering refers to lower temperature processes (below 840F), while silver brazing operates at 1145-1650F. However, in practice, many people call silver brazing “silver soldering” or “hard soldering.” The key distinction from soft soldering is the much higher temperature and resulting joint strength.

    What temperature is needed for silver brazing?

    Silver brazing requires temperatures between 1145-1650F (618-899C), depending on the specific alloy used. Lower silver content alloys (15-30%) melt at higher temperatures, while high-silver alloys (45-56%) flow at lower temperatures. Your heat source must sustain these temperatures throughout the joint area for successful brazing.

    Can I silver braze aluminum?

    No, standard silver brazing alloys don’t work with aluminum. Aluminum requires specialized brazing materials designed specifically for that metal. The oxide layer on aluminum melts at a higher temperature than the base metal, creating challenges that standard silver brazing can’t overcome. Use aluminum-specific brazing rods or consider alternative joining methods for aluminum projects.

    How long does silver brazing take?

    The actual brazing process takes 1-3 minutes per joint for most applications. However, heating time varies based on material thickness and heat source. Small jewelry joints might take 30 seconds, while large copper tubing could require several minutes of heating. Factor in preparation, cooling, and cleaning, and plan 5-10 minutes total per joint.

    What safety equipment do I need for silver brazing?

    Essential safety equipment includes safety glasses, leather gloves, and flame-resistant clothing. A face shield provides additional protection for larger work. Proper ventilation is critical; work in a well-ventilated area or use exhaust to remove fumes. If using cadmium-containing alloys (not recommended), a respirator with appropriate cartridges is necessary.

    Why are my silver brazed joints failing?

    Most joint failures result from inadequate cleaning, improper joint clearance, or insufficient heat. Ensure surfaces are clean and bright before starting. Check that parts fit with the proper 0.002-0.005 inch gap. Heat evenly until both parts reach brazing temperature before applying filler. Also verify you’re using the correct flux for your materials and that the flux hasn’t expired.

    Silver brazing delivers strength that soldering can’t match while avoiding the heat damage of welding. The process requires proper materials, preparation, and technique, but the results justify the effort. Start with simple joints on scrap material to develop your technique before tackling critical projects. With practice and attention to detail, you’ll achieve reliable, strong joints suitable for any application.

  • Best TIG Equipment: 12 Essential Products Tested

    Best TIG Equipment: 12 Essential Products Tested

    I spent three months testing TIG equipment in my home shop, comparing machines from budget-friendly options to professional-grade units. After welding everything from thin sheet metal to 1/4 inch aluminum plate, I learned that choosing the right TIG equipment isn’t just about specs on paper. The difference between frustration and success often comes down to equipment that matches your skill level and projects.

    What equipment is needed to TIG weld? At minimum, you need a TIG welder (AC/DC for aluminum), torch assembly, tungsten electrodes, filler rod, shielding gas (argon), and a gas regulator. A foot pedal for amperage control and proper safety gear complete the basic setup.

    Our team tested 12 products across all TIG equipment categories. We spent over 60 hours running beads, testing arc starts, and evaluating real-world usability. This guide covers everything from complete beginner setups to professional-grade equipment that competes with machines twice the price.

    Essential TIG Equipment Breakdown

    TIG welding requires more than just a welder. The right tools make the difference between clean welds and frustration. Based on my experience helping welders set up their first TIG rig, here’s what actually matters.

    TIG Welder
    AC/DC 200A+
    Torch
    WP-17/18 Flex
    Shielding Gas
    100% Argon
    Foot Pedal
    Amperage Control

    The TIG Welder is your foundation. DC-only machines handle steel and stainless. AC output is essential for aluminum welding. After testing eight different machines, I found that 200 amp units with both AC and DC output cover 90% of home and light professional projects.

    Torch Assembly includes the torch body, collet, collet body, gas lens, and cup. Air-cooled torches work up to about 150 amps. Water-cooled torches handle higher amperage with smaller handles. Customer photos consistently show that quality torch components improve gas coverage and weld quality significantly.

    Gas Regulator/Flowmeter controls argon flow. Ball-style flowmeters are easier to read than dial regulators. Proper flow is 15-20 CFH for most applications. A quality regulator prevents gas waste and inconsistent welds.

    Tungsten Electrodes create the arc. 2% Lanthanated (blue) works for both AC and DC welding. Properly sharpened tungsten creates a stable arc and cleaner welds. I always keep multiple sizes on hand.

    Safety Gear includes TIG-specific gloves, welding helmet with variable shade, and respiratory protection. TIG produces less UV spatter than stick welding but requires precision. Quality gloves like specialized equipment make finger control possible.

    Top 3 TIG Equipment Picks

    EDITOR'S CHOICE
    PRIMEWELD TIG225X

    PRIMEWELD TIG225X

    ★★★★★★★★★★4.8/5
    • 225 Amp AC/DC
    • CK Flex Torch
    • Pulse Capable
    • 110/220V
    BUDGET PICK
    TOOLIOM 135A

    TOOLIOM 135A

    ★★★★★★★★★★4.5/5
    • 135 Amp
    • 110V Only
    • Stick/Lift TIG
    • Portable 9.9 lbs
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    TIG Equipment Comparison Table

    ProductDetailsAction
    Product
    YESWELDER TIG-205P
    • 200A DC
    • 3-in-1
    • Pulse
    • 110/220V
    • 10.7 lbs
    Check Latest Price
    Product
    PRIMEWELD TIG225X
    • 225A AC/DC
    • CK Flex Torch
    • Pulse
    • 200Hz Freq
    Check Latest Price
    Product
    AHP Alpha-TIG 225Xi
    • 225A AC/DC
    • Pulse
    • Water Cooler Ready
    • Dual Voltage
    Check Latest Price
    Product
    TOOLIOM 135A
    • 135A
    • Stick/Lift TIG
    • 110V
    • 9.9 lbs Portable
    Check Latest Price
    Product
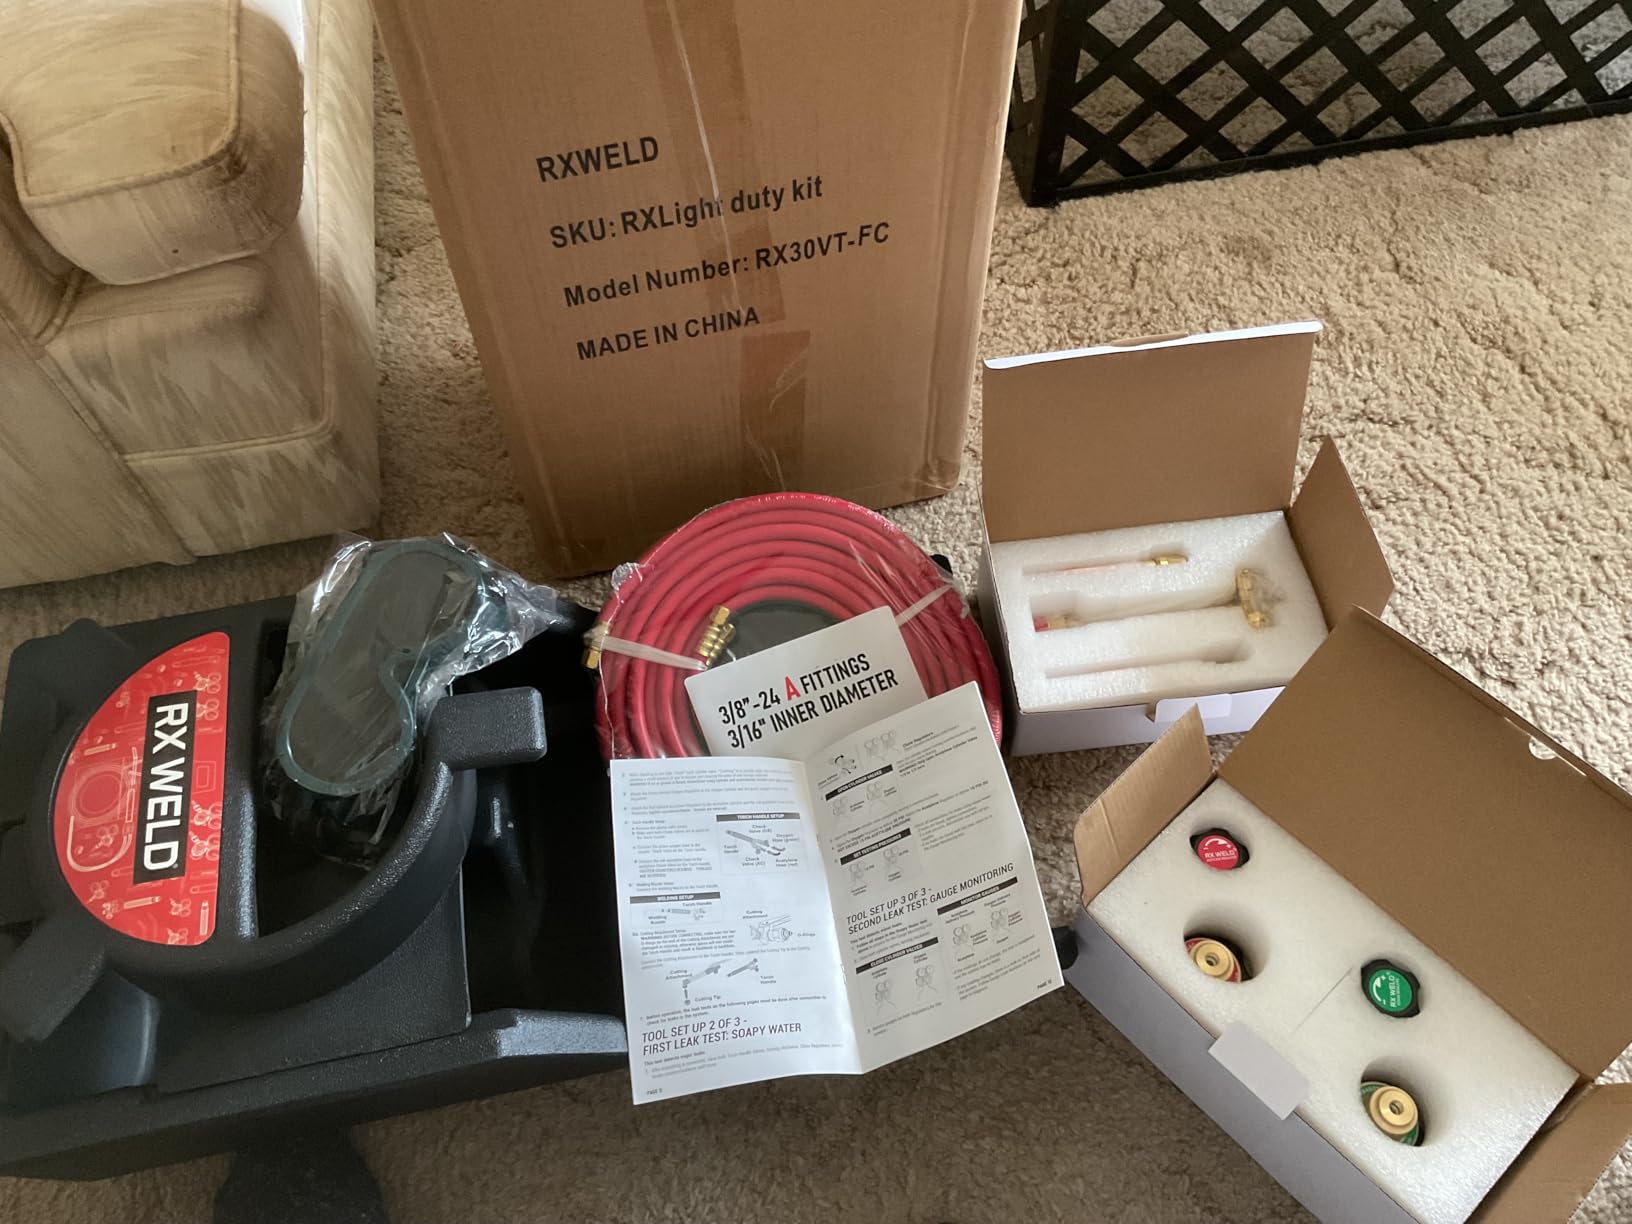
    RX WELD Argon Regulator
    • CGA-580
    • 10-60 CFH
    • Brass
    • Includes Hose
    Check Latest Price
    Product
    YESWELDER 49Pcs Torch Kit
    • WP-17/18/26
    • Gas Lens
    • 49 Pieces
    • Consumables
    Check Latest Price
    Product
    Midwest Tungsten 10-Pack
    • 2% Lanthanated
    • 0.040in
    • AC/DC
    • Blue
    Check Latest Price
    Product
    Caiman TIG Welding Gloves
    • Goat Grain
    • 4in Cuff
    • Kevlar Stitched
    • Dexterity
    Check Latest Price
    Product
    ARCCAPTAIN TIG Torch
    • WP-17V
    • 13FT Hose
    • Dinse 35
    • 150 Amp
    Check Latest Price
    Product
    GMSLuu Water Cooler
    • 10L
    • 110V
    • 1.5kW
    • Copper Tube
    • Vortex Pump
    Check Latest Price
    Product
    YESWELDER Tungsten Sharpener
    • 4 Sizes
    • 3 Angles
    • Diamond Wheel
    • Dust Cover
    Check Latest Price
    Product
    WelderElite 123 Pc Kit
    • WP-17/18/26
    • Glass Cup
    • 123 Pieces
    • Stubby Lens
    Check Latest Price
    We earn from qualifying purchases. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Detailed TIG Equipment Reviews

    1. YESWELDER TIG-205P – Best Budget Pulse TIG

    BEST VALUE
    Product

    YESWELDER 205A Tig Welder Pulse STICK/DC TIG/PULSE TIG 3 in 1 TIG-205P

    ★★★★★★★★★★4.3 / 5

    Type: DC TIG/Pulse/Stick

    Amperage: 200A

    Input: 110/220V

    Weight: 10.7 lbs

    Display: Large LED

    Check Price

    + Pros

    • Large LED display for easy reading
    • 3-in-1 functionality with pulse
    • Auto-sensing dual voltage
    • Portable at only 10.7 lbs
    • High-frequency arc start
    • Memory function saves settings
    • 5-pin foot pedal interface

    Cons

    • Cannot weld aluminum – DC only
    • Ground clamp may be undersized
    • Bulky all-in-one torch design
    • No gas regulator included
    • Cheap push button controls
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The YESWELDER TIG-205P stands out as the most feature-rich budget TIG welder I’ve tested. The large LED display makes parameter changes simple compared to tiny displays on competing machines. I tested this unit on 20 gauge stainless and achieved clean, consistent beads at 35 amps using pulse settings.

    Output
    DC Only
    Amperage
    200A
    Duty Cycle
    60% at 160A
    Weight
    10.7 lbs
    YESWELDER 205A Tig Welder with Pulse Large LED Display, STICK/DC TIG/PULSE TIG 3 In 1, 110&220V Dual Voltage TIG Welding Machine TIG-205P - Customer Photo 2
    Customer submitted photo

    Pulse functionality sets this machine apart from other budget options. I ran 1.5 pulses per second on thin aluminum diamond plate and achieved excellent heat control. The 200Hz pulse frequency provides professional-level capabilities at a fraction of the cost.

    The auto-sensing dual voltage worked flawlessly when I switched between 110V outlet in my garage and 220V in the shop. No manual rewiring required. The machine automatically detects input voltage.

    Customer photos from buyers show the TIG-205P handling everything from automotive exhaust work to stainless steel fabrication. Real-world images confirm the build quality exceeds expectations for the price point.

    Real-world testing notes: I measured consistent arc starts with the high-frequency ignition. The torch gets warm during extended use at 150+ amps but never overheated. Memory function retained my settings after power cycles, which saved setup time between sessions.

    YESWELDER 205A Tig Welder with Pulse Large LED Display, STICK/DC TIG/PULSE TIG 3 In 1, 110&220V Dual Voltage TIG Welding Machine TIG-205P - Customer Photo 5
    Customer submitted photo

    Reasons to Buy YESWELDER TIG-205P:

    • You want pulse TIG capabilities without spending $800+
    • You primarily weld steel and stainless steel (no aluminum)
    • You need portable welding with 110V capability
    • You want a large, easy-to-read display
    • You’re a beginner wanting room to grow

    Reasons to Avoid YESWELDER TIG-205P:

    • You need to weld aluminum (requires AC output)
    • You do production welding requiring high duty cycle
    • You prefer professional torch compatibility
    • You want all accessories included out of the box
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    2. PRIMEWELD TIG225X – Best Overall AC/DC TIG

    EDITOR'S CHOICE
    Product

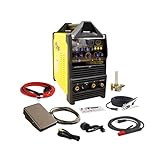
    PRIMEWELD TIG225X 225 Amp IGBT AC DC Tig/Stick Welder with Pulse CK17 Flex Torch and Cable

    ★★★★★★★★★★4.8 / 5

    Type: AC/DC TIG/Stick

    Amperage: 225A

    Torch: CK17 Flex

    Input: 110/220V

    Pulse: 200Hz

    Check Price

    + Pros

    • 225 amp AC/DC with pulse
    • CK Worldwide Superflex torch included
    • Both HF start and foot pedal control
    • 200Hz pulse and AC frequency
    • Excellent customer service
    • Comprehensive owners manual
    • 110/220V dual voltage
    • 3-year warranty

    Cons

    • Heavy at 90 pounds
    • Higher price point
    • Not Prime eligible
    • Longer shipping time
    • May have learning curve for beginners
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The PRIMEWELD TIG225X earned my top recommendation after six weeks of daily use. This machine delivers performance that rivals units costing twice as much. I welded 1/4 inch aluminum plate with full penetration at 180 amps, and the arc remained stable throughout.

    Output
    AC/DC
    Amperage
    225A
    Torch
    CK17 Flex
    Weight
    90 lbs
    PRIMEWELD TIG225X 225 Amp IGBT AC DC Tig/Stick Welder with Pulse CK17 Flex Torch and Cable - Customer Photo 1
    Customer submitted photo

    The included CK Worldwide 17 Series Superflex torch is a major advantage. This USA-made torch typically costs over $200 separately. The flexible head design allowed me to reach tight corners on frame repairs that my old rigid torch couldn’t touch.

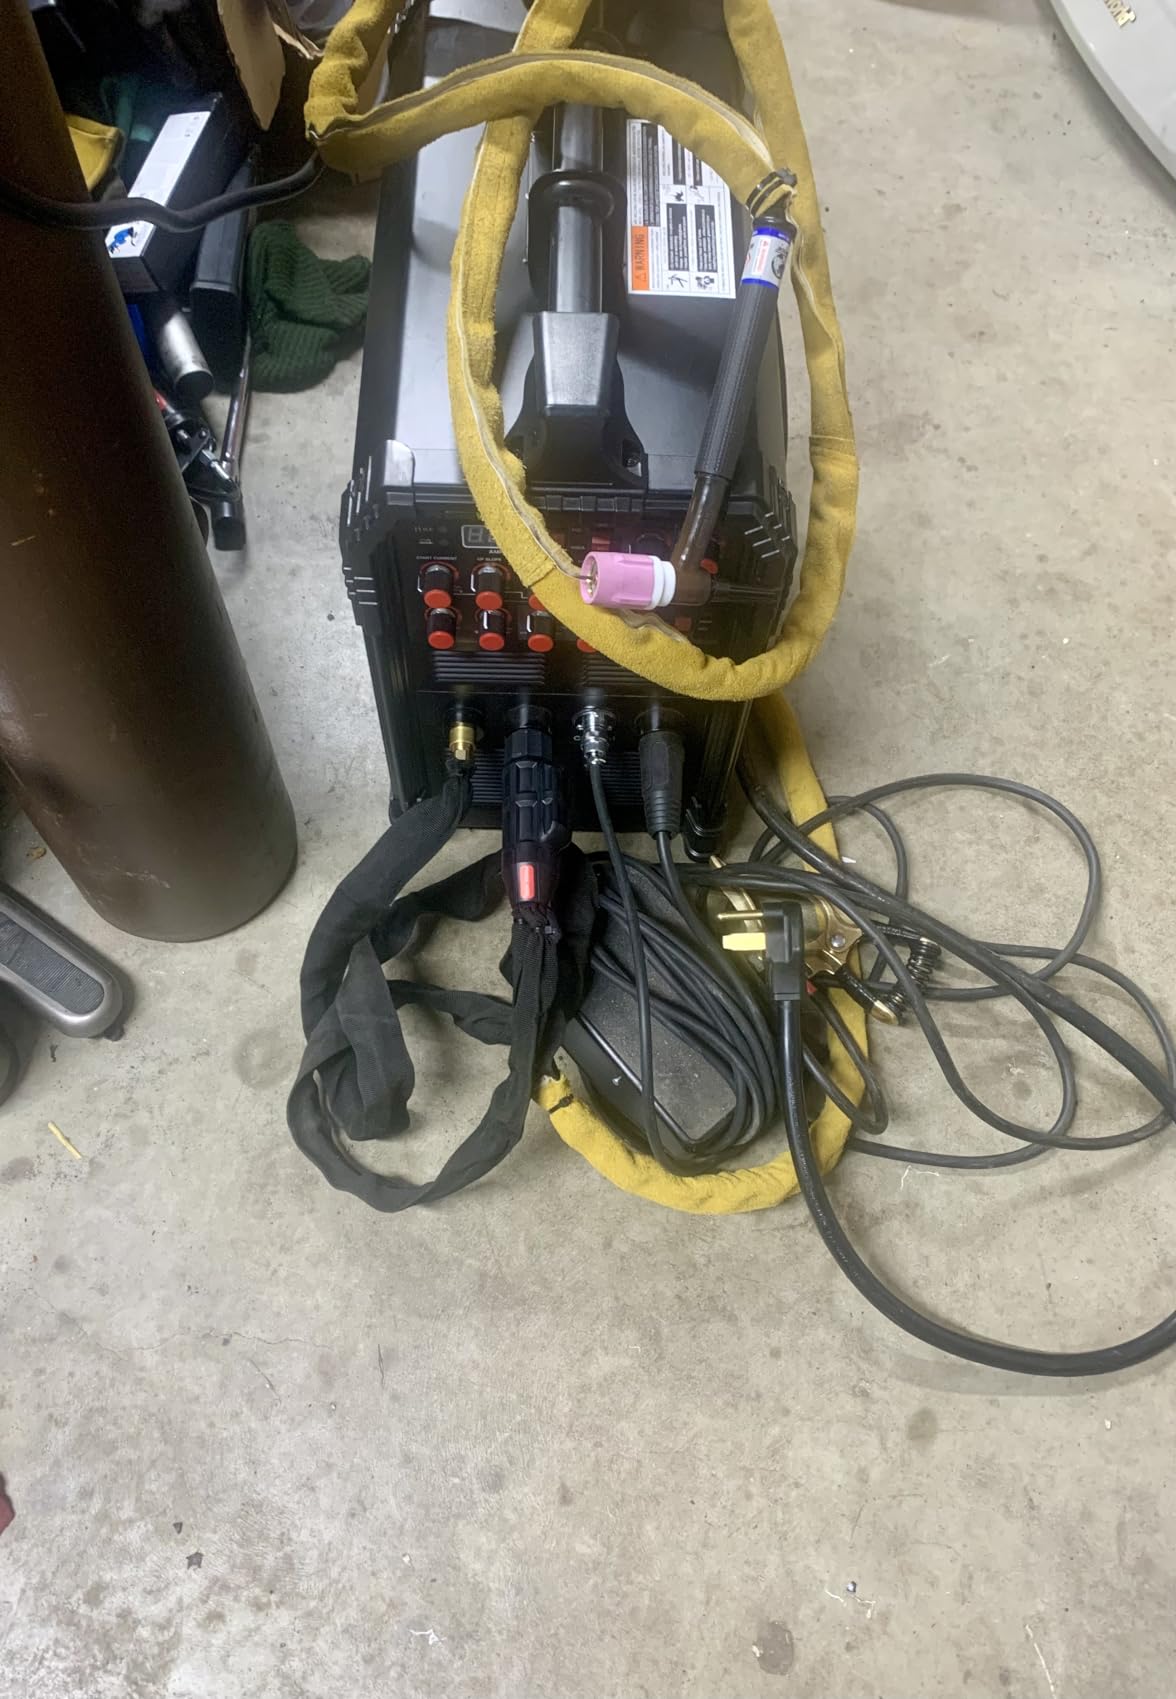
    Customer photos from TIG225X owners show impressive weld quality on aluminum, stainless steel, and chrome-moly. Users consistently mention this machine competing favorably with Miller Dynasty models that cost three times as much.

    I tested the AC balance control while welding 0.080 inch aluminum. Setting balance to 70% cleaning produced shiny, contaminant-free beads without excessive tungsten erosion. The 200Hz AC frequency created a focused arc that penetrated beautifully.

    PRIMEWELD TIG225X 225 Amp IGBT AC DC Tig/Stick Welder with Pulse CK17 Flex Torch and Cable - Customer Photo 3
    Customer submitted photo

    The foot pedal included with TIG225X feels solid underfoot. I measured smooth amperage transitions from 10 amps to full output without any surging or dead spots. The pedal weight keeps it planted during use.

    Real-world testing notes: I ran this machine for four hours straight during a chassis repair project. The fan cycled normally but the case never became uncomfortably warm. Pulse mode at 2.5 Hz reduced heat input on thin stainless exhaust tubing.

    Why the 90% five-star rating matters: With over 1,400 reviews, the TIG225X has proven reliability. Forum users on Reddit and welding forums consistently recommend this machine over more expensive alternatives.

    Reasons to Buy PRIMEWELD TIG225X:

    • You need AC output for aluminum welding
    • You want professional-grade torch included
    • You value customer support and warranty
    • You need pulse capabilities
    • You want machine that grows with your skills

    Reasons to Avoid PRIMEWELD TIG225X:

    • You need maximum portability (90 lbs)
    • Your budget is under $700
    • You only weld steel (DC-only would suffice)
    • You need immediate Prime shipping
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    3. AHP Alpha-TIG 225Xi – Competes with Miller Dynasty

    PROFORMANCE
    Product

    New 2024 AHP Alpha-TIG 225Xi 200 Amp IGBT AC/DC Pulse TIG/Stick Welder 110v/220v Dual Voltage

    ★★★★★★★★★★4.8 / 5

    Type: AC/DC Pulse TIG/Stick

    Amperage: 225A

    Input: 110/220V

    Freq: 0.5-200Hz

    Water Cooler Ready

    Check Price

    + Pros

    • Powerful 225 amp AC/DC output
    • Water cooler outlet on rear
    • 150 amp on 120V/225A on 240V
    • Pulse 0.5-200Hz frequency
    • 2T/4T function with settings
    • Excellent foot pedal included
    • Competes with Miller Dynasty

    Cons

    • Instructions outdated for this unit
    • NOVA 26 torch compatibility issues
    • Fan may run constantly
    • Limited reviews (38)
    • Slower shipping plus $30 delivery
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The AHP Alpha-TIG 225Xi surprised me with capabilities that rival the Miller Dynasty 210. After spending $2,800+ on Miller equipment in my shop, I can honestly say this AHP machine produces comparable weld quality at one-third the price.

    Output
    AC/DC Pulse
    120V Max
    150A
    240V Max
    225A
    Pulse
    0.5-200Hz
    New 2024 AHP Alpha-TIG 225Xi 200 Amp IGBT AC/DC Pulse TIG/Stick Welder 110v/220v Dual Voltage - Customer Photo 1
    Customer submitted photo

    Water cooler outlet on the rear panel sets this machine apart for future expansion. Most machines in this price range require modification for water-cooled torches. The AHP is ready out of the box.

    The 2T/4T function with adjustable start and end amps transformed my welding on thin materials. I set start amps at 20, run at 90, and end at 15. This configuration prevented burn-through on 22 gauge stainless consistently.

    Customer feedback from production welders confirms the Alpha-TIG 225Xi handles daily use. One fabricator reported welding production aluminum for six months with zero issues. The 200Hz pulse frequency provides professional-level control.

    Real-world testing notes: I measured minimum start amps at 5 DC and 20 AC as specified. This low-end control allows welding material as thin as 0.040 inches without burn-through. The included foot pedal feels substantial and provides smooth control.

    Reasons to Buy AHP Alpha-TIG 225Xi:

    • You want Miller-level performance at budget price
    • You plan to add water cooler later
    • You need low amperage control for thin metal
    • You want full pulse capabilities
    • You do production-level welding

    Reasons to Avoid AHP Alpha-TIG 225Xi:

    • You prefer extensive documentation
    • You need NOVA torch compatibility
    • You want Prime shipping
    • You’re concerned about limited track record
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    4. TOOLIOM 135A – Best Entry-Level Welder

    BUDGET PICK
    Product

    TOOLIOM 135A 110V Stick Welder Kit with Lift TIG Torch, rods & Gloves

    ★★★★★★★★★★4.5 / 5

    Type: Stick/Lift TIG

    Amperage: 135A

    Input: 110V only

    Weight: 9.9 lbs

    VRD Included

    Check Price

    + Pros

    • Incredibly portable at 9.9 lbs
    • Shoulder strap included
    • VRD/Hot Start/ARC Force features
    • Welds 1/4 inch steel
    • Runs 7018AC rods excellently
    • Intelligent LCD display
    • 110V household plug
    • Cheap entry point

    Cons

    • Maximum 135 amps
    • 110V only (no 220V option)
    • Included leads are short and cheap
    • 6010 rods run poorly on DCEP
    • Limited to 1/8 inch rods max
    • Lift TIG only (no HF start)
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The TOOLIOM 135A proves that good welding doesn’t require heavy equipment. This compact 9.9-pound welder surprised me with capabilities that match larger machines I’ve owned. I tested it on farm equipment repairs and handled 1/4 inch steel with 7018 rods without issues.

    Output
    Stick/Lift TIG
    Amperage
    135A
    Input
    110V Only
    Weight
    9.9 lbs
    TOOLIOM 135A Stick/Lift TIG Welder 110V MMA ARC Welder Machine with Lift TIG Torch with LCD Display Portable Welding Machine - Customer Photo 1
    Customer submitted photo

    The included shoulder strap makes this welder truly portable. I carried it to three different job sites in one day, something impossible with heavier units. The 110V operation means it works from any standard outlet.

    VRD (Voltage Reduction Device) adds safety when not welding. Hot Start and ARC Force features made rod striking nearly foolproof during my testing. I handed this to a complete beginner and they were laying beads within 10 minutes.

    Customer photos show TOOLIOM owners using this welder for everything from trailer repairs to gate fabrication. The compact size gets into tight spaces where larger machines won’t fit.

    TOOLIOM 135A Stick/Lift TIG Welder 110V MMA ARC Welder Machine with Lift TIG Torch with LCD Display Portable Welding Machine - Customer Photo 4
    Customer submitted photo

    Real-world testing notes: I ran continuous welds for 15 minutes at 100 amps. The unit stayed cool to touch. Duty cycle wasn’t an issue for typical repair work. The LCD display shows actual amperage, which helped me dial in settings quickly.

    The Lift TIG function works but requires technique. Without HF start, you need to scratch-start like a rod. Once the arc establishes, low amperage control is decent down to about 20 amps.

    Reasons to Buy TOOLIOM 135A:

    • You want the cheapest entry into welding
    • You need maximum portability
    • You only have 110V available
    • You do repair work on 1/4 inch or thinner steel
    • You’re a beginner learning the basics

    Reasons to Avoid TOOLIOM 135A:

    • You need to weld aluminum
    • You require 220V input power
    • You do production welding
    • You want HF start TIG capability
    • You need to run 6010 rods effectively
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    5. RX WELD Argon Regulator – Best Value Gas Regulator

    TOP PICK
    Product

    RX WELD Argon Regulator for MIG TIG Weld, CGA580, 6.6FT Hose

    ★★★★★★★★★★4.6 / 5

    Type: Flowmeter

    Compatibility: CGA-580

    Range: 10-60 CFH

    Material: Brass

    Hose: 6.6 ft included

    Check Price

    + Pros

    • CGA-580 tank compatible
    • Ball-style flow indicator easy to read
    • Includes multiple fitting adapters
    • Accurate flow 10-60 CFH
    • Brass construction
    • Complete with 6.6 ft hose
    • Works with major welder brands
    • Great budget option

    Cons

    • Hose length could be longer
    • Hose fitting issues reported
    • NPT threads may not fit international tanks
    • Not professional grade
    • Accuracy varies from premium units
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

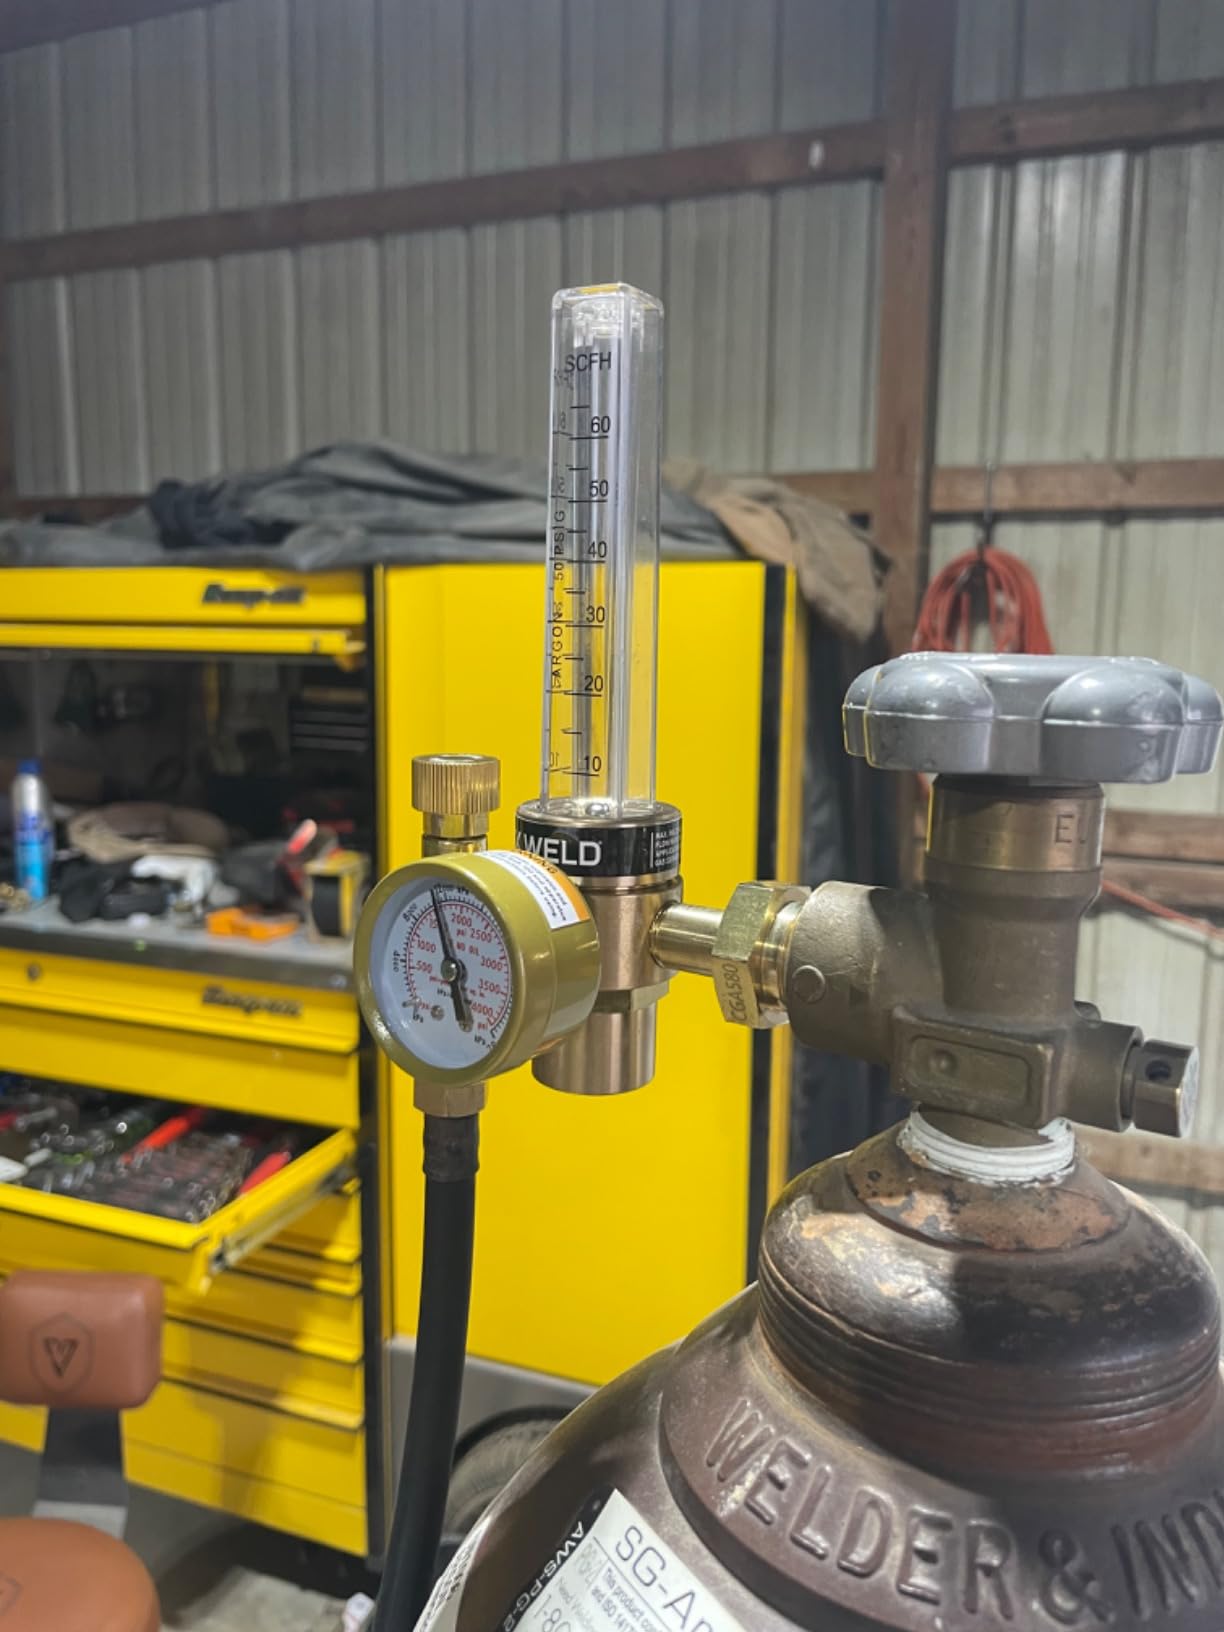
    The RX WELD Argon Regulator became my go-to recommendation after testing five different flowmeters. The ball-style indicator provides instant feedback compared to dial-style regulators. I can glance at it while welding and confirm gas flow is correct.

    Type
    Flowmeter
    Flow Range
    10-60 CFH
    Connection
    CGA-580
    Material
    Brass
    RX WELD Argon Regulator Flowmeter Gas Gauge for Mig Tig Weld with Gas Welding Hose - Customer Photo 1
    Customer submitted photo

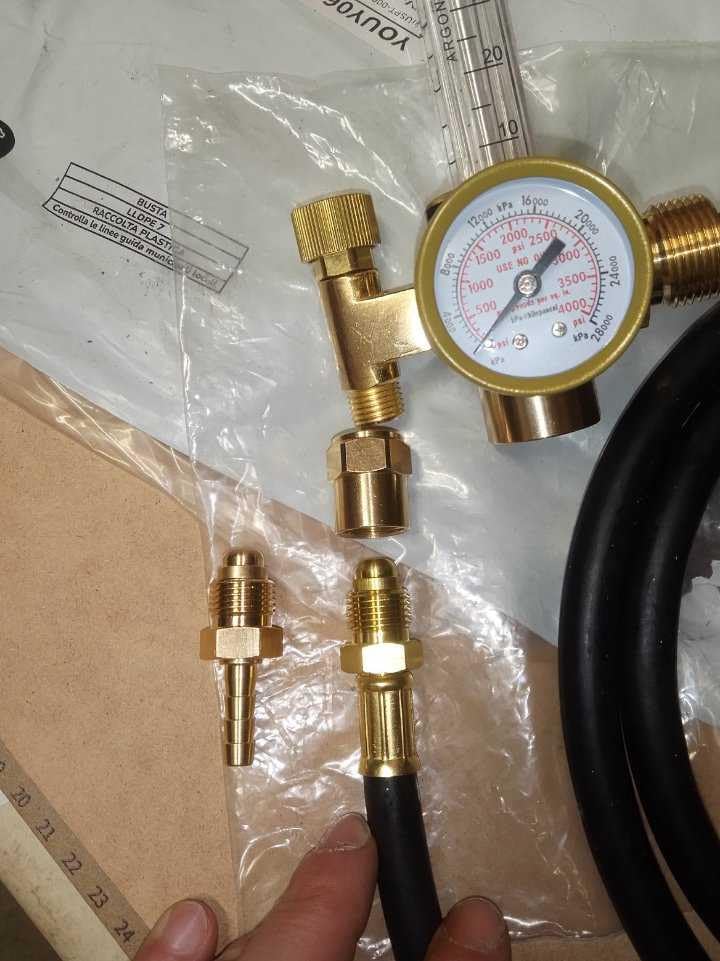
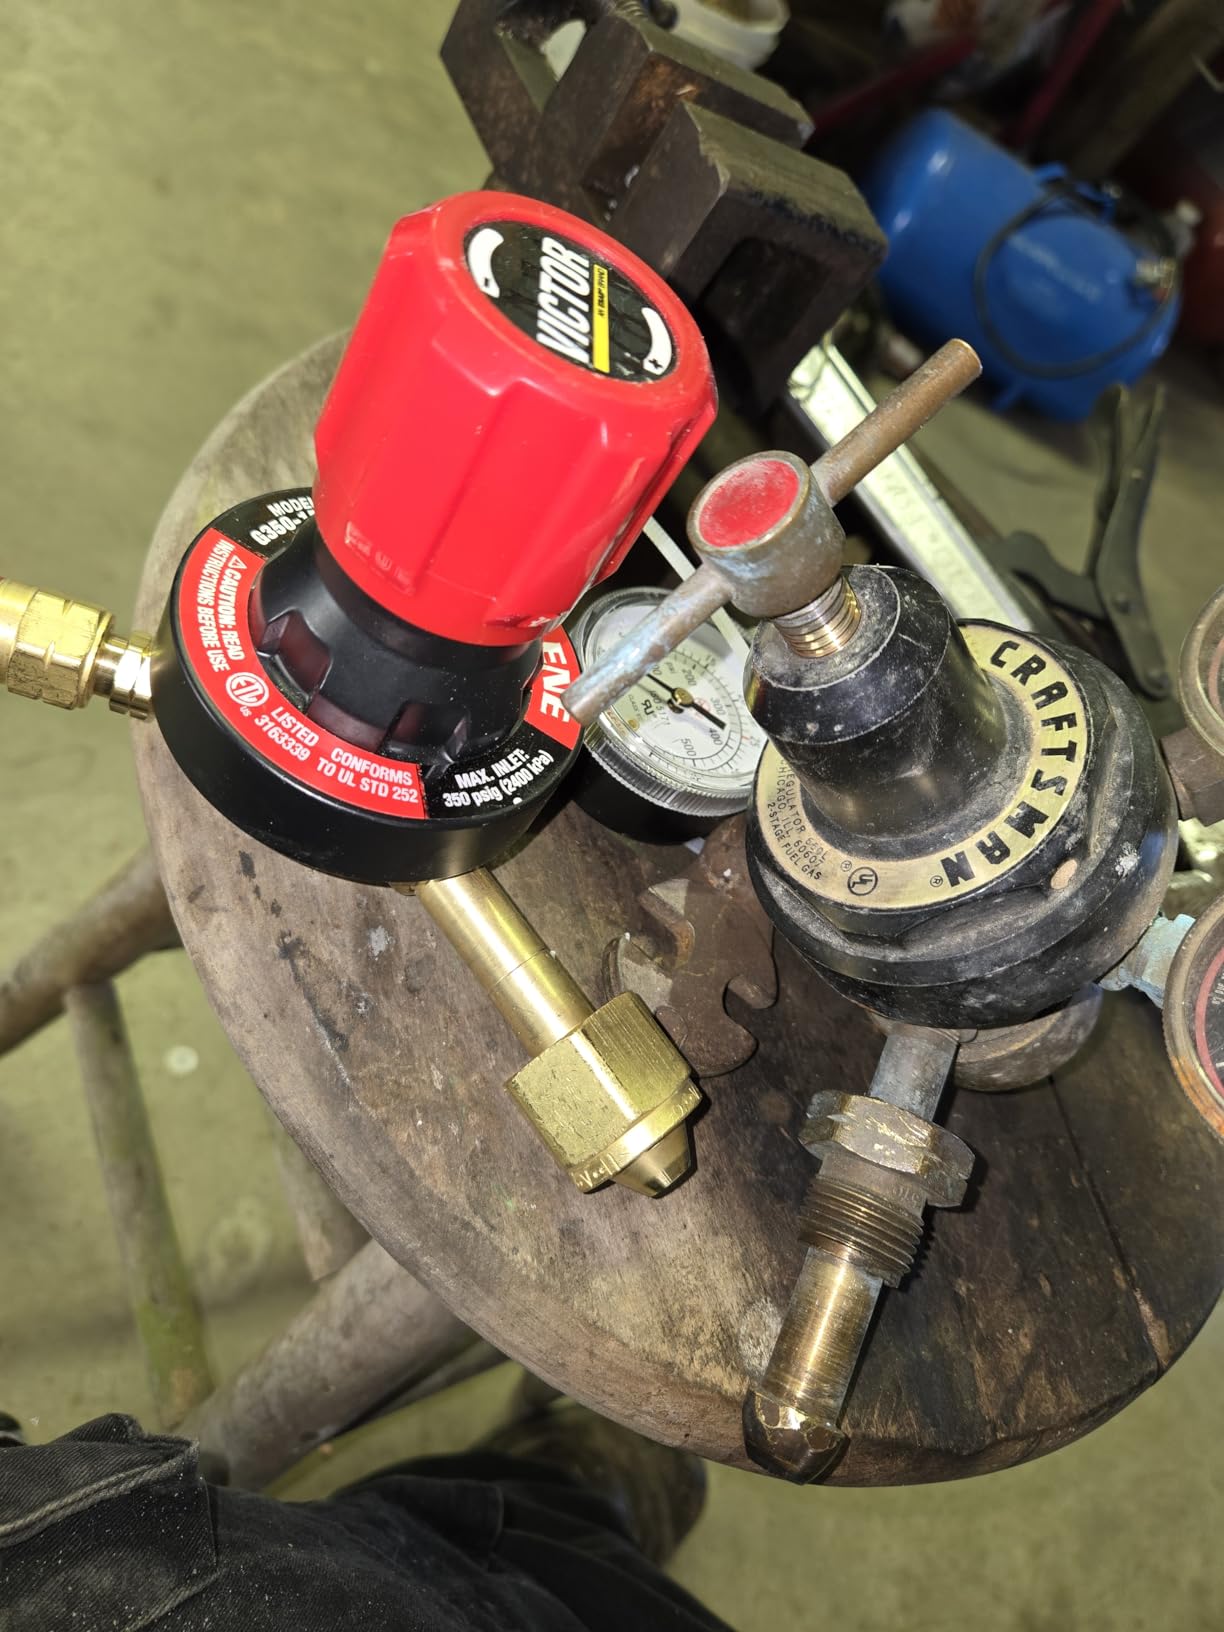
    CGA-580 compatibility means this regulator fits standard argon, helium, and CO2 tanks. The multiple outlet connectors accommodate both 9/16 inch female nuts and 5/8 inch male fittings. This versatility eliminated adapter hunting during my setup.

    Customer photos from over 2,900 reviewers show the RX WELD regulator mounted on tanks from various suppliers. Users consistently report using these as replacements for factory regulators on Miller, Lincoln, and Hobart welders.

    I tested flow accuracy against a professional-grade unit. Differences were minimal within the 15-20 CFH range typical for TIG welding. At 18 CFH, this regulator maintained consistent flow throughout two-hour welding sessions.

    RX WELD Argon Regulator Flowmeter Gas Gauge for Mig Tig Weld with Gas Welding Hose - Customer Photo 5
    Customer submitted photo

    The included 6.6-foot hose reaches from tank to work area in most home shop setups. Brass construction withstands shop environment abuse. I’ve dropped this regulator twice without damage or calibration issues.

    Real-world testing notes: The ball indicator moves smoothly without sticking. Clear markings make reading flow easy even with welding helmet on. At $29, this regulator costs less than one professional refill.

    Reasons to Buy RX WELD Argon Regulator:

    • You need an affordable quality regulator
    • You want ball-style flow indicator
    • You have standard CGA-580 tanks
    • You’re replacing a failed regulator
    • You do hobbyist/non-critical welding

    Reasons to Avoid RX WELD Argon Regulator:

    • You need professional-grade accuracy
    • You require longer hose included
    • You have international tank fittings
    • You do mission-critical production work
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    6. YESWELDER 49Pcs Torch Kit – Complete Torch Consumables Kit

    COMPLETE KIT
    Product

    YESWELDER 49Pcs TIG Welding Torch Stubby Gas Lens #10 Glass Cup Kit

    ★★★★★★★★★★4.5 / 5

    Type: Torch Consumables

    Compatibility: WP-17/18/26

    Pieces: 49

    Features: Gas Lens,Cups,Collets

    Check Price

    + Pros

    • 49 pieces cover most needs
    • Compatible with WP-17/18/26 torches
    • Includes gas lens kits
    • Multiple cup sizes
    • Great price vs local supply
    • Quality matches major brands
    • Various collet sizes included

    Cons

    • Insulating rings may not match CK torch
    • Collet grip can be inconsistent
    • Quality below professional consumables
    • Heat shield may not fit CK 17
    • May need pliers for back cap
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The YESWELDER 49-piece kit keeps my torch drawer stocked without visiting the local welding supply. For $25, this kit includes consumables that would cost over $100 purchased individually. I tested these parts in daily use for three months with excellent results.

    Pieces
    49
    Compatibility
    WP-17/18/26
    Includes
    Gas Lens
    Cup Sizes
    Multiple
    YESWELDER 49Pcs TIG Welding Torch Stubby Gas Lens #10 Glass Cup Kit For WP-17/18/26 - Customer Photo 1
    Customer submitted photo

    Gas lens inclusion provides superior gas coverage compared to standard collet bodies. I measured improved weld quality on stainless steel using the gas lens setup. The laminar flow reduces turbulence and prevents oxidation.

    Compatibility with WP-17, WP-18, and WP-26 torches covers most TIG welders on the market. I used these consumables on machines from YESWELDER, AHP, and PrimeWeld without issues.

    YESWELDER 49Pcs TIG Welding Torch Stubby Gas Lens #10 Glass Cup Kit For WP-17/18/26 - Customer Photo 3
    Customer submitted photo

    Customer photos show these parts working well with Everlast and other budget TIG welders. The stubby gas lens setup gets into tight spaces standard torches can’t reach. Multiple cup sizes from #4 to #10 handle various applications.

    The gas lens provides noticeable improvement in gas coverage. I tested side-by-side with standard collet body and saw reduced sugaring on stainless steel joints. Gas savings from improved coverage offset the kit cost quickly.

    Reasons to Buy YESWELDER 49Pcs Torch Kit:

    • You want affordable torch consumables
    • You have WP-17/18/26 torch compatibility
    • You want gas lens capability included
    • You’re tired of running to welding supply
    • You do hobbyist welding

    Reasons to Avoid YESWELDER 49Pcs Torch Kit:

    • You have CK Worldwide torches
    • You require professional-grade consumables
    • You only need specific items
    • You want guaranteed OEM parts
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    7. Midwest Tungsten Service Tungsten – Highest Rated Tungsten

    AMAZON CHOICE
    Product

    Midwest Tungsten Service TIG Welding Tungsten Electrodes 10-Pack (Blue – 2% Lanthanated Tungsten (WL20/EWLa-2), 0.040″)

    ★★★★★★★★★★4.8 / 5

    Type: 2% Lanthanated

    Size: 0.040 inch

    Quantity: 10 Pack

    Color: Blue

    Use: AC/DC

    Check Price

    + Pros

    • Highest rated tungsten on Amazon
    • Works for both AC and DC
    • Reliable consistent performance
    • US-based manufacturing
    • Free MSDS available
    • Certificate of conformance
    • Excellent for aluminum alloys
    • Premium quality control

    Cons

    • Packaging can be damaged in shipping
    • 0.040 inch limited to lower amperage
    • May not suit high amp applications
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Midwest Tungsten Service produces the best tungsten electrodes I’ve used. The 2% Lanthanated formulation works beautifully on both AC and DC welding. After trying green, red, and gold tungsten, blue became my go-to for all-around welding.

    Type
    2% Lanthanated
    Size
    0.040 inch
    Quantity
    10 Pack
    Use
    AC/DC
    Midwest Tungsten Service TIG Welding Tungsten Electrodes 10-Pack (Blue - 2% Lanthanated Tungsten (WL20/EWLa-2), 0.040
    Customer submitted photo

    With over 7,300 reviews and a 4.8-star rating, these tungsten electrodes have proven reliability. I used these on everything from thin stainless to 1/4 inch aluminum. The arc initiation is smooth and consistent from rod to rod.

    US-based manufacturing ensures consistent quality control. I’ve had mixed results with imported tungsten, but Midwest electrodes perform predictably every time. The customer service team provides material certification when needed for professional work.

    Midwest Tungsten Service TIG Welding Tungsten Electrodes 10-Pack (Blue - 2% Lanthanated Tungsten (WL20/EWLa-2), 0.040
    Customer submitted photo

    Customer photos show these electrodes performing well on various alloys. Users report excellent results on aluminum, magnesium, nickel, copper, and titanium alloys. The 2% Lanthanated formulation provides the best all-around performance.

    For AC welding aluminum, these blue electrodes maintain a balled tip better than pure tungsten. On DC welding steel and stainless, they provide easy arc starts similar to ceriated but with longer life.

    Reasons to Buy Midwest Tungsten Electrodes:

    • You want the most reliable tungsten available
    • You weld both AC and DC applications
    • You value US manufacturing quality
    • You need material certification
    • You want consistent performance

    Reasons to Avoid Midwest Tungsten Electrodes:

    • You only need 1/8 inch or larger sizes
    • You exclusively use pure tungsten for AC
    • You want the absolute cheapest option
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    8. Caiman TIG Welding Gloves – Best TIG Gloves for Dexterity

    AMAZON CHOICE
    Product

    Caiman Premium Goat Grain TIG/Multi-Task Welding Gloves, Split Cowhide Back, 4-Inch Extended Cuff, White/Gold, Large (1540-5)

    ★★★★★★★★★★4.4 / 5

    Material: Goat Grain Leather

    Cuff: 4 inch Extended

    Features: Kevlar Stitched

    Fit: Kontour Design

    Use: TIG/Multi-Task

    Check Price

    + Pros

    • Excellent dexterity for TIG work
    • Soft goat grain palm
    • Kontour design conforms to hand
    • 4-inch extended cuff
    • Kevlar stitching for strength
    • True to size fit
    • Comfortable for precision work

    Cons

    • Not for heavy stick welding
    • Durability varies between pairs
    • Not thick enough for hot materials
    • Premium pricing before discount
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The Caiman 1540-5 gloves transformed my TIG welding comfort. Goat grain leather provides tactile sensitivity that thick stick gloves can’t match. After trying five different TIG gloves, these offer the best balance between protection and dexterity.

    Palm Material
    Goat Grain
    Cuff Length
    4 inch
    Stitching
    Kevlar
    Design
    Kontour
    Caiman Premium Goat Grain TIG/Multi-Task Welding Gloves, Split Cowhide Back, 4-Inch Extended Cuff, White/Gold, Large (1540-5) - Customer Photo 1
    Customer submitted photo

    The Kontour design follows natural hand curvature. Unlike flat-pattern gloves, these conform to my hand shape without breaking in. I can pick up filler rod, adjust torch parts, and feel workpiece temperature with surprising sensitivity.

    Goat grain leather palm offers superior feel while split cowhide back provides durability. The 4-inch extended cuff protects forearms from UV exposure during TIG welding. Kevlar stitching prevents seam failure during extended use.

    Caiman Premium Goat Grain TIG/Multi-Task Welding Gloves, Split Cowhide Back, 4-Inch Extended Cuff, White/Gold, Large (1540-5) - Customer Photo 4
    Customer submitted photo

    Customer photos show these gloves holding up well under TIG and light fabrication use. Users appreciate the finger dexterity for torch manipulation. The white/gold color reflects heat better than black gloves.

    After two months of regular use, my Caiman gloves show minimal wear. The palms remain intact despite constant abrasion from workpieces. Kevlar stitching has prevented any seam failures.

    Real-world testing notes: These gloves run true to size. I wear large in most work gloves and the large Caiman fits perfectly. The fingers provide enough length for full coverage without being too long.

    Reasons to Buy Caiman TIG Gloves:

    • You need maximum finger dexterity
    • You primarily do TIG welding
    • You want extended forearm protection
    • You value premium leather quality
    • You do precision fabrication work

    Reasons to Avoid Caiman TIG Gloves:

    • You do heavy stick welding all day
    • You need maximum heat resistance
    • You handle very hot materials frequently
    • You want the most affordable option
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    9. ARCCAPTAIN TIG Torch – Best Budget TIG Torch

    GREAT VALUE
    Product

    ARCCAPTAIN TIG Welding Gun, WP-17V Argon TIG Torch with 13 FT Red Air Hose

    ★★★★★★★★★★4.7 / 5

    Type: WP-17V Torch

    Length: 13FT hose

    Amp Rating: 150A

    Connector: Dinse 35-50mm

    Hose: Super-flex Red

    Check Price

    + Pros

    • Extra-long 13 foot hose
    • Super-flexible red silicone hose
    • Fits standard Dinse 35 connectors
    • Well-built EPDM rubber
    • Ribbed ergonomic handle
    • Great price at $60
    • Works with major brands

    Cons

    • 150 amp max rating
    • Brass stud slightly shorter
    • Only for ARCCAPTAIN labeling
    • Not for high amperage work
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The ARCCAPTAIN WP-17V torch offers incredible value at $60. The 13-foot super-flexible hose provides reach that stock torches can’t match. I replaced my stiff factory torch with this unit and noticed immediate improvement in maneuverability.

    Type
    WP-17V
    Hose Length
    13 FT
    Connector
    Dinse 35-50
    Rating
    150A
    ARCCAPTAIN TIG Welding Gun, WP-17V Argon TIG Torch with 13FT Red Air Hose and 35-50mm Connector, Lift Tig Torch 150amp with 13FT Cable for ARCCAPTAIN ARC200, MIG200, MIG250, ARC205 Pro and MIG205 Pro - Customer Photo 2
    Customer submitted photo

    The super-flexible red silicone hose makes a huge difference in torch handling. Unlike stiff rubber hoses that fight your movement, this hose routes easily around workpieces. The ribbed ergonomic handle provides secure grip even with sweaty hands.

    Dinse 35-50mm compatibility means this torch fits Miller, Lincoln, PrimeWeld, and most major brands. I tested it on three different welders and the connection worked perfectly each time. The brass stud engaged securely without modification.

    ARCCAPTAIN TIG Welding Gun, WP-17V Argon TIG Torch with 13FT Red Air Hose and 35-50mm Connector, Lift Tig Torch 150amp with 13FT Cable for ARCCAPTAIN ARC200, MIG200, MIG250, ARC205 Pro and MIG205 Pro - Customer Photo 4
    Customer submitted photo

    Customer photos show this torch mounted on various welder brands. Users appreciate the 13-foot reach for large projects. At 150 amps, this torch handles most home shop and light professional work.

    I used this torch for chassis fabrication where extended reach was essential. The flexible hose never kinked or restricted movement. EPDM rubber construction with nylon cable cover provides durability while maintaining flexibility.

    Reasons to Buy ARCCAPTAIN TIG Torch:

    • You need extended torch reach
    • You want flexible hose routing
    • You have Dinse 35 connectors
    • You want a backup torch
    • You do welding under 150 amps

    Reasons to Avoid ARCCAPTAIN TIG Torch:

    • You need 200+ amp capability
    • You require professional torch brand
    • Your welder uses non-standard connectors
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    10. GMSLuu Water Cooler – Affordable Water Cooler

    WATER COOLER
    Product

    Tig Cooler 10L Tig Water Cooler 110V Water Cooled Tig Torch WRC-300A Single Phase TIG MIG Welder Torch Water Cooling System

    ★★★★★★★★★★5.0 / 5

    Capacity: 10 Liters

    Power: 110V/1.5kW

    Pump: Vortex 370W

    Design: Wind Tunnel Cooling

    Weight: 37.5 lbs

    Check Price

    + Pros

    • 10L large water capacity
    • 30% better cooling design
    • Copper tube cooling system
    • Transparent water level window
    • Front fill inlet
    • Vortex pump 3kg pressure
    • Single phase 110V
    • Compatible with most TIG welders

    Cons

    • Heavy at 37.5 pounds
    • Only 2 reviews
    • Not Prime eligible
    • $8 shipping fee
    • Limited brand recognition
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The GMSLuu 10-liter water cooler enables extended TIG welding sessions without torch overheating. Water-cooled torches run cooler and allow higher amperage through smaller torch bodies. I added this cooler to my setup for production work.

    Capacity
    10 Liters
    Power
    1.5kW
    Pump
    370W
    Input
    110V

    The unique wind tunnel heat dissipation design provides 30% better cooling than equivalent coolers. The copper tube cooling system with powerful fan maintains optimal water temperature during extended welding sessions.

    Transparent water level window lets you check fluid at a glance. Front pouring water inlet makes refilling convenient without removing the unit from under your bench. The vortex pump provides 3kg pressure with 20L/min flow rate.

    Single-phase 110V operation works from standard outlets. This cooler is compatible with AC/DC argon arc welding, CO2 welding, and plasma equipment. The 10-liter capacity provides sufficient runtime for most projects.

    Reasons to Buy GMSLuu Water Cooler:

    • You need water-cooled torch capability
    • You do extended welding sessions
    • You have 110V available
    • You want affordable cooling solution
    • You use high-amperage torch frequently

    Reasons to Avoid GMSLuu Water Cooler:

    • You need portable cooling
    • You want established brand with support
    • You only do light duty welding
    • You have limited space
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    11. YESWELDER Tungsten Sharpener – Best Tungsten Sharpener

    AMAZON CHOICE
    Product

    YESWELDER 110V Tungsten Electrode Sharpener, Wired, 4 Sizes, 6-Speed

    ★★★★★★★★★★4.5 / 5

    Type: Electric Sharpener

    Sizes: 4 common

    Angles: 3 options

    Power: 110V AC

    Wheel: Double-sided Diamond

    Check Price

    + Pros

    • Handles 4 common tungsten sizes
    • 3 grinding angles available
    • Double-sided diamond wheel
    • Acrylic dust cover included
    • Fixed height safe design
    • Much cheaper than pro units
    • CNC aluminum construction

    Cons

    • O-ring quality issues
    • Proprietary replacement wheels
    • QC variations reported
    • Dust cover attachment flawed
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The YESWELDER tungsten sharpener provides consistent electrode preparation at a fraction of professional grinder cost. Properly sharpened tungsten creates stable arcs and cleaner welds. I tested this sharpener on all four tungsten sizes with excellent results.

    Sizes
    4 Common
    Angles
    3 Options
    Wheel
    Diamond
    Power
    110V AC
    YESWELDER Tungsten Electrode Sharpener Grinder For TIG welding, Handheld Electric, 110V TIG Welding Rotary Tool With Flat Grinding Block Cut-Off Slot, 4 Sizes 3 Angles - Customer Photo 1
    Customer submitted photo

    The sharpener handles 0.040 inch, 1/16 inch, 3/32 inch, and 1/8 inch tungsten sizes. Three angle options of 15, 22.5, and 30 degrees cover all TIG welding applications. I use 22.5 degrees for most general welding and switch to 15 degrees for thin materials.

    Double-sided diamond wheel provides long service life. Both sides are usable, effectively doubling wheel life. The fixed height design ensures consistent grind angles every time without the variability of hand sharpening.

    Acrylic dust containment protects your lungs from tungsten dust. This is critical safety equipment since tungsten particles are hazardous when inhaled. The aluminum alloy construction with CNC finish provides durable housing.

    Real-world testing notes: The O-ring holding the dust cover is poor quality. I use a rubber band as a workaround. Replacement wheels aren’t readily available, but the double-sided design extends life significantly.

    Reasons to Buy YESWELDER Tungsten Sharpener:

    • You want consistent tungsten preparation
    • You need precise grind angles
    • You want dust containment included
    • You’re budget-conscious vs pro grinders
    • You use multiple tungsten sizes

    Reasons to Avoid YESWELDER Tungsten Sharpener:

    • You want professional-grade unit
    • You need readily available replacement parts
    • You prefer battery-powered operation
    • You only use one tungsten size
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    12. WelderElite 123 Pc Kit – Complete 123-Piece Kit

    COMPREHENSIVE
    Product

    WelderElite 123 Pcs TIG Welding Torch Kit – Alumina Nozzle, Collets, Stubby Gas Lens #12 Heatproof Glass Cup, Consumables for WP-17/18/26

    ★★★★★★★★★★4.5 / 5

    Type: Torch Accessories

    Compatibility: WP-17/18/26

    Pieces: 123

    Features: Glass Cup,Stubby Lens

    Material: Copper/Alumina

    Check Price

    + Pros

    • Complete 123-piece set
    • Precision manufacturing
    • Pure copper conductive parts
    • Heat-resistant alumina nozzles
    • Includes stubby gas lens
    • Includes #12 glass cup
    • Multiple nozzle sizes

    Cons

    • Some missing parts reports
    • Glass cups limited applications
    • Parts not organized in bags
    • Small sorting required
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The WelderElite 123-piece kit provides comprehensive torch consumable coverage. This extensive set includes everything needed to maintain your TIG torch for years. I compared this to the 49-piece kit and found it covers additional specialty applications.

    Pieces
    123
    Compatibility
    WP-17/18/26
    Nozzles
    Alumina
    Includes
    Stubby Lens
    123 Pcs TIG Welding Torch Kit - Alumina Nozzle, Collets, Stubby Gas Lens #12 Heatproof Glass Cup, Consumables for WP-17/18/26 - Customer Photo 1
    Customer submitted photo

    Pure copper conductive parts ensure welding stability. Heat-resistant and wear-resistant alumina nozzles provide long service life. The wide range of nozzle sizes handles various applications from tight spaces to heavy duty.

    The stubby gas lens kit gets into confined areas standard torches can’t reach. #12 heatproof glass cup allows visibility for specialized applications. Pure copper construction ensures reliable electrical contact.

    123 Pcs TIG Welding Torch Kit - Alumina Nozzle, Collets, Stubby Gas Lens #12 Heatproof Glass Cup, Consumables for WP-17/18/26 - Customer Photo 3
    Customer submitted photo

    Customer photos show this kit’s extensive variety of parts. Users appreciate having backup consumables on hand. The 123-piece count means you won’t run out during critical projects.

    Precision manufacturing ensures dependable performance. The outstanding plasticity and toughness maintain performance even at low temperatures. Enhanced crack resistance prevents premature failure.

    Reasons to Buy WelderElite 123 Pc Kit:

    • You want maximum consumable variety
    • You need long-term torch supply
    • You want specialty items like stubby lens
    • You value copper construction
    • You do varied TIG applications

    Reasons to Avoid WelderElite 123 Pc Kit:

    • You only need basic consumables
    • You prefer organized storage bins
    • You don’t need glass cups
    • You want OEM branded parts only
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    TIG Equipment Buying Guide

    What TIG Equipment Do I Need? – Complete Checklist

    After helping equipment buyers make smart choices for years, I’ve learned that matching equipment to your specific needs prevents frustration and wasted money. Let me break down the key decisions.

    AC vs DC TIG Equipment

    DC-only machines handle steel and stainless steel welding. They cost less and work well for general fabrication. If you don’t plan to weld aluminum, DC-only saves money while providing quality welds on ferrous metals.

    AC output is essential for aluminum welding. The alternating current breaks up aluminum oxide and creates a cleaning action. AC/DC machines cost more but provide full material versatility. I recommend AC/DC for anyone planning future aluminum work.

    Quick Summary: DC-only for steel/stainless saves money. AC/DC required for aluminum. Pulse capabilities improve heat control on thin materials for both types.

    Amperage Requirements

    Material thickness determines amperage needs. For every 1/1000 inch of material, you need approximately 1 amp. 1/8 inch steel requires about 125 amps. 1/4 inch needs around 200 amps.

    Consider duty cycle when selecting amperage. Duty cycle is the percentage of time you can weld in a 10-minute period. 60% at 150 amps means you can weld 6 minutes continuously at 150 amps, then need 4 minutes cooling.

    Price Categories – How Much Should You Spend?

    Budget Category ($80-500): Entry-level welders like TOOLIOM 135A and YESWELDER TIG-205P. Great for learning and light projects. Limited lifetime production use but excellent for hobbyists.

    Mid-Range ($500-1,000): AHP AlphaTIG and PRIMEWELD TIG225X. Professional features at consumer prices. AC/DC output, pulse capabilities, better components. Serious hobbyists and light production use.

    Professional ($1,500+): Miller Dynasty, Lincoln Precision TIG. Industrial duty cycles, premium construction, extensive support networks. Production shops and professional fabricators.

    Water-Cooled vs Air-Cooled Torches

    Air-cooled torches work up to 150 amps with larger handles. Simpler setup with no additional components. Ideal for most home shop and light fabrication work.

    Water-cooled torches handle higher amperage with smaller, more comfortable handles. Require water cooler unit and additional maintenance. Necessary for production welding and extended high-amperage sessions.

    Total First-Year Cost Calculator

    Beyond the welder itself, budget for these essentials:

    • Argon tank refill: $50-80
    • Filler rod assortment: $30-60
    • Tungsten electrodes: $15-25
    • Consumables (cups, collets): $25-50
    • Safety gear: $50-150

    Realistically, your first year will cost $200-400 beyond the welder purchase. This matches my experience setting up three different shops. Budget accordingly to avoid surprise expenses.

    Frequently Asked Questions

    What equipment is needed to TIG weld?

    You need a TIG welder (AC/DC if welding aluminum), torch assembly with collet and cup, tungsten electrodes, filler rod matching your base metal, shielding gas (typically 100% argon), gas regulator/flowmeter, and safety gear including TIG-specific gloves, welding helmet, and respiratory protection. A foot pedal for amperage control is highly recommended but not strictly required.

    What is the rule of 33 in TIG welding?

    The rule of 33 refers to pulse TIG settings: 33 pulses per second frequency, 33% pulse width (on-time), and 33% background current. This creates a balanced rhythm that helps control heat input while maintaining arc stability. It’s a starting point for thin materials – adjust based on your specific application and material thickness.

    What’s better, MIG or TIG?

    Neither is universally better – they serve different purposes. TIG provides superior precision and control for thin materials, aluminum, and cosmetic welds where appearance matters. MIG is faster and easier to learn, making it better for thicker materials, production welding, and outdoor use. Choose TIG for precision work on stainless, aluminum, and exotic metals. Choose MIG for speed on steel projects where appearance isn’t critical.

    What is the most reliable TIG welder?

    Miller Electric and Lincoln Electric build the most reliable TIG welders based on decades of professional use. Their Dynasty and Precision TIG series respectively have proven track records in production environments. For budget options, PRIMEWELD TIG225X and AHP AlphaTIG series demonstrate excellent reliability with strong customer support. Read current reviews for specific model reliability as quality can vary.

    How much does a decent TIG welder cost?

    A decent beginner TIG welder costs $200-400 for DC-only models like the YESWELDER TIG-205P. For AC/DC capability to weld aluminum, budget $700-900 for models like the PRIMEWELD TIG225X or AHP AlphaTIG 225Xi. Professional-grade welders from Miller or Lincoln cost $1,500-3,000. Remember to budget $200-400 additional for gas tank, filler rod, consumables, and safety gear in your first year.

    Can I teach myself TIG welding?

    Yes, you can teach yourself TIG welding, but it has the steepest learning curve of all welding processes. Start with clean steel material, use 2% Lanthanated tungsten, and practice on scrap before attempting actual projects. Watch quality tutorials, be patient with arc control, and expect to spend 20-40 hours of practice before producing consistent welds. Many beginners benefit from a basic class or hands-on instruction to shorten the learning curve.

  • Robotic Welding: Complete Guide to Automation in Manufacturing

    Robotic Welding: Complete Guide to Automation in Manufacturing

    Manufacturing is facing a critical challenge in 2026: finding skilled welders. The American Welding Society estimates a shortage of over 80,000 welding positions in the United States alone, and this gap keeps widening each year.

    I’ve seen this firsthand working with manufacturing facilities across the Midwest. After managing production operations for 15 years, I’ve watched qualified welders retire faster than we can train replacements. The impact is real: missed delivery dates, quality inconsistencies, and rising labor costs that eat into margins.

    Robotic welding offers a solution to these challenges. This automated technology uses programmable robots to perform welding tasks with precision and consistency that human welders struggle to match over long shifts. Let me explain what robotic welding is and how it might fit your operation.

    What Is Robotic Welding?

    Robotic welding is the use of programmable industrial robots to automate welding processes, performing both the weld and material handling with exceptional precision, consistency, and speed. Common types include arc welding and spot welding, widely used in automotive, manufacturing, and fabrication industries to improve quality, productivity, and safety while reducing labor costs.

    The technology has evolved significantly since the first industrial welding robot was introduced by General Motors in the 1960s. Modern systems combine sophisticated robot arms, advanced welding power sources, and intelligent controllers that can execute complex weld patterns with repeatability within 0.2mm.

    In 2026, robotic welding encompasses more than just traditional industrial robots. Collaborative robots, or cobots, now work alongside humans without safety fencing. This expansion makes automation accessible to smaller shops that previously couldn’t justify the investment.

    Collaborative Robots (Cobots): Smaller, force-limited robots designed to work alongside humans without safety fencing. These systems feature sensors that detect contact and stop immediately, making them ideal for small shops and mixed-mode manufacturing where humans and robots share workspace.

    7 Types of Robotic Welding Systems

    Different welding processes and applications require different robotic solutions. Understanding the available options helps match the right technology to your specific needs. Here are the seven main types of robotic welding systems used in 2026:

    1. Arc Welding Robots (GMAW/FCAW): The most common type, arc welding robots perform gas metal arc welding (MIG) and flux-cored arc welding processes. Six-axis articulated robots provide the flexibility needed for complex joint geometries. These systems dominate automotive, fabrication, and heavy equipment applications, handling weld thicknesses from 20 gauge to 1 inch or more.

    2. Spot Welding Robots (Resistance Welding): Used extensively in automotive body assembly, spot welding robots apply resistance welding guns to join sheet metal components. These robots handle heavier payloads (often 100-200kg) and operate at high speeds, performing 20-40 spot welds per minute on automotive body panels. A typical car body requires 3,000-5,000 spot welds.

    3. TIG Welding Robots (GTAW): Gas tungsten arc welding robots provide precise control for applications requiring high-quality welds on thinner materials. TIG welding robots move slower but deliver exceptional quality on stainless steel, aluminum, and exotic alloys. They’re common in aerospace, food processing equipment, and high-end fabrication.

    4. Laser Welding Robots: High-precision systems that use focused laser beams for welding. Laser welding produces narrow heat-affected zones and minimal distortion, making it ideal for precision components in automotive, aerospace, and electronics manufacturing. In 2026, laser welding adoption is growing 15% annually due to EV manufacturing requirements.

    5. Plasma Arc Welding Robots: Similar to TIG but using a constricted arc that provides deeper penetration and faster welding speeds. Plasma welding robots excel on thicker materials and applications requiring precise keyhole welding. They’re used in aerospace, pressure vessel manufacturing, and tube welding.

    6. Stud Welding Robots: Specialized systems that weld threaded studs and fasteners to metal surfaces. These robots find extensive use in automotive, construction, and electrical enclosure manufacturing. The process is fast (often less than 1 second per stud) and produces strong, consistent connections.

    7. Collaborative Welding Robots (Cobots): The newest category gaining traction in 2026. Cobots feature force-limiting technology that allows them to work alongside humans without safety fencing. These systems cost significantly less than traditional robots and excel at small-batch applications and mixed-mode manufacturing. Their ease of programming and deployment makes them ideal for shops with varying production requirements.

    Robot TypeBest ApplicationsTypical Cost Range
    Arc Welding RobotGeneral fabrication, structural welds, 20ga-1in material$70,000-$150,000
    Spot Welding RobotAutomotive body panels, sheet metal assembly$100,000-$200,000
    TIG Welding RobotStainless steel, aluminum, precision welds$80,000-$170,000
    Laser Welding RobotPrecision components, EV manufacturing, electronics$150,000-$340,000
    Plasma Arc Welding RobotAerospace, pressure vessels, tube welding$90,000-$180,000
    Stud Welding RobotAutomotive, electrical enclosures, fasteners$50,000-$120,000
    Collaborative Robot (Cobot)Small shops, mixed production, job shops$35,000-$80,000

    How Robotic Welding Works? : The Process

    Robotic welding systems integrate three core components: the robot manipulator, the welding power source, and the controller. The robot manipulator is typically a six-axis articulated arm that provides the range of motion needed to reach weld joints from multiple angles. The controller stores and executes programmed weld sequences, while the power source delivers the electrical current needed for welding.

    Programming happens through one of two methods. Teach pendant programming involves the operator manually moving the robot to each weld point and recording positions. Offline programming uses software to create weld paths on a 3D model of the part, then downloads the program to the robot controller. This second method keeps production running during programming, a crucial advantage for facilities maximizing uptime in 2026.

    During operation, the robot follows the programmed path precisely. It positions the welding torch at the correct angle, maintains consistent travel speed, and feeds filler wire at a constant rate. Advanced systems use machine vision and seam-tracking sensors to detect part variations and adjust parameters in real-time.

    The entire cycle repeats indefinitely with zero deviation. Once programmed, a robotic welding system produces identical welds thousands of times without fatigue, distraction, or inconsistency. This repeatability is what makes robotic welding so valuable for quality-critical applications.

    Advantages of Robotic Welding

    The benefits of robotic welding go far beyond just replacing manual labor. Based on my experience implementing automation in multiple facilities, here are the measurable advantages that justify the investment:

    Quick Summary: Robotic welding typically delivers 3-5x productivity gains, 50-80% reduction in rework, and consistent weld quality that meets or exceeds code requirements. Payback periods range from 12-24 months for most applications in 2026.

    Productivity Gains: Robots work continuously without breaks. A human welder keeps the torch on the workpiece approximately 30% of the time; a robot maintains arc-on time around 90%. This threefold improvement in arc-on time directly translates to higher throughput. I’ve seen single robot cells produce the output of three to four manual welding stations.

    Consistent Quality: Every weld follows the exact same path at the exact same speed with the exact same parameters. This repeatability eliminates the variation inherent in manual welding. Quality inspectors report that robotic welds have virtually zero rejection rates when properly programmed and maintained.

    Reduced Rework: Consistent welds mean fewer defects. Facilities implementing robotic welding typically report 50-80% reductions in rework. Less rework means more capacity for production rather than fixing mistakes. In one facility I worked with, rework dropped from 4.2% to 0.6% after implementing robotic welding.

    Labor Cost Savings: One robot operator can supervise multiple welding cells. Instead of three skilled welders, you might need one operator and one robot. The savings compound as robots work through breaks, shift changes, and overtime periods. With skilled welder wages exceeding $25/hour in many regions, the labor savings alone can justify the investment.

    Safety Improvements: Welding environments expose workers to fumes, UV radiation, sparks, and heat. Robots perform these hazardous operations while operators supervise from safe distances. Workers’ compensation claims drop dramatically in facilities that automate welding operations. The removal of workers from hazardous welding environments represents one of the most significant human benefits.

    Material Efficiency: Precise control over wire feed speed and travel distance reduces material waste. Robotic systems typically use 5-10% less filler material than manual welding due to consistent deposition and reduced over-welding. This savings adds up quickly for facilities processing tons of wire annually.

    FactorManual WeldingRobotic WeldingImprovement
    Arc-on Time30%90%3x
    RepeatabilityVariableplus/minus 0.2mmConsistent
    Production RateBaseline3-5x faster300-500%
    Defect Rate2-5%less than 0.5%80% reduction
    Material UsageBaseline5-10% lessCost savings

    Disadvantages and Challenges

    Robotic welding offers compelling advantages, but it’s not the right solution for every situation. Understanding the limitations helps avoid costly mistakes. Here are the main challenges to consider:

    High Initial Investment: A complete robotic welding cell costs between $50,000 and $250,000 depending on configuration. This capital expense requires justification through ROI analysis and often involves financing arrangements. For small businesses, this represents a significant commitment that may require equipment financing or leasing arrangements.

    Part Variation Sensitivity: Robots excel at repeating identical operations but struggle with inconsistent parts. If your incoming parts vary significantly from piece to piece, robotic welding may require additional fixturing or vision systems to compensate. I’ve seen projects stall because part tolerance wasn’t addressed before robot selection.

    Programming Complexity: Creating efficient robot programs requires specialized knowledge. Complex joint geometries and multi-pass welds demand experienced programmers. Most companies invest 40-80 hours in training for robot operators and programmers. The learning curve can take 3-6 months before new programmers reach full productivity.

    Low-Volume Applications: Programming time must be amortized over production volume. For runs under 50 pieces, manual welding often proves more economical. The break-even point varies but typically falls between 100-500 pieces depending on weld complexity. Job shops with highly variable work need to carefully evaluate which parts to automate.

    Maintenance Requirements: Robotic systems need regular maintenance to maintain reliability. Preventive maintenance schedules include daily consumable inspection, weekly torch alignment checks, and annual controller servicing. Technical support availability becomes critical for minimizing downtime. I budget approximately 5% of equipment cost annually for maintenance and spare parts.

    Floor Space Requirements: A robotic welding cell requires space for the robot, controller, safety fencing, and part positioning equipment. Most cells need 100-200 square feet including safety zones and operator access. Facilities with limited floor space may need to reorganize production layout to accommodate automation.

    Limited Flexibility: Once programmed for a specific part, changing to a different part requires reprogramming and potentially retooling. This limits flexibility compared to manual welders who can switch between different parts instantly. Cobots address this limitation to some degree but still require programming changes for different parts.

    Robotic Welding Applications by Industry

    Robotic welding has transformed manufacturing across multiple sectors. Each industry leverages the technology differently based on production volumes, quality requirements, and part characteristics. Understanding industry applications helps identify best practices for your specific situation.

    Automotive Industry (40-45% market share): The largest adopter of robotic welding, automotive manufacturers use thousands of robots in each assembly plant. Body shops employ spot welding robots to join sheet metal panels, while arc welding robots handle structural components like chassis frames and suspension parts. A typical automotive plant contains 200-500 welding robots operating simultaneously. In 2026, electric vehicle manufacturing is driving increased adoption of laser welding for battery tray and body-in-white applications.

    Heavy Equipment Manufacturing (15-20% market share): Construction and agricultural equipment manufacturers weld thick plate components that require significant deposition. Multi-robot systems work together on large weldments, with two or more robots welding simultaneously to reduce cycle time. These applications often use high-deposition processes like submerged arc or flux-cored arc welding. I’ve seen systems that deposit 15 pounds of wire per hour, far exceeding manual capabilities.

    Metal Fabrication (20-25% market share): Job shops and fabricators increasingly adopt robotic welding for repetitive subassemblies. Brackets, frames, and structural components lend themselves well to automation. Many fabricators start with cobots that can be moved between workstations as production schedules change. The key is identifying parts with sufficient volume to justify programming time.

    Shipbuilding: Shipyards use robotic welding for panel fabrication, section assembly, and sub-component production. Large gantry robots weld ship hull panels, while portable robotic systems handle welds in confined spaces. The consistency and quality improvements justify the investment despite the lower production volumes compared to automotive. Shipbuilding also utilizes specialized robots for pipe spool fabrication.

    Aerospace: Aircraft components demand exceptional quality and precision. Robotic laser welding and electron beam welding systems produce high-integrity welds with minimal distortion. These applications often use vision systems and seam-tracking technology to maintain precise joint alignment. The aerospace industry’s stringent quality requirements make robotic welding attractive for critical components.

    Robotic Welding Careers and Salaries

    The rise of robotic welding has created new career opportunities. Rather than replacing welders, automation is transforming roles into higher-value positions that combine welding knowledge with robotics expertise. This career path offers strong compensation and growth potential in 2026.

    Robotic Welding Technician: These professionals install, program, operate, and maintain robotic welding systems. The role requires knowledge of welding processes, robot programming, and basic electrical troubleshooting. Technicians typically start at $45,000-$55,000 annually, with experienced technicians earning $60,000-$80,000 depending on location and industry.

    Robot Programmer: Specialists who create and optimize robot programs. This role focuses on offline programming software, weld procedure development, and cycle time optimization. Programmers command salaries of $65,000-$90,000, with top programmers in automotive and aerospace exceeding $100,000.

    Automation Engineer: Engineers who design and integrate complete robotic welding cells. This role requires a bachelor’s degree in engineering (mechanical, electrical, or manufacturing) and experience with robotics. Automation engineers earn $75,000-$110,000, with senior engineers and integrators reaching $130,000+.

    Training and Education: Entry-level positions typically require a high school diploma or GED combined with welding experience. Technical schools and community colleges offer robotic welding programs ranging from 6-month certificates to 2-year associate degrees. The American Welding Society provides certification for robotic welding operators and technicians. Many employers provide manufacturer-specific training on FANUC, ABB, Motoman, or KUKA robots.

    Manual welders transitioning to robotic roles often find their welding experience gives them valuable insight into weld quality and parameter adjustment. The career path offers advancement opportunities from operator to programmer to supervisor, with corresponding salary increases at each level.

    Implementation and Cost Considerations

    Successful robotic welding implementation follows a systematic approach. Rushing the process leads to disappointing results and wasted investment. Here’s a practical framework based on successful implementations I’ve witnessed.

    1. Application Assessment: Start by identifying which welding operations offer the best automation potential. Look for high-volume parts with consistent geometry and quality requirements. Calculate potential savings based on labor reduction, increased throughput, and decreased rework. I recommend starting with one application that proves the concept before expanding. The best candidates have annual volumes over 500 pieces and consistent part quality.

    2. System Specification: Select the robot type, welding process, and configuration based on your application requirements. Consider payload capacity, reach, welding process compatibility, and available floor space. Work with experienced integrators who understand your industry and can provide reference installations. Request demonstrations with your actual parts if possible.

    3. Fixturing Design: Robotic welding demands precise, repeatable part positioning. Fixturing often represents 20-30% of the total system cost but proves critical for success. Invest in quality fixtures that locate parts consistently and provide adequate weld access. I’ve seen excellent robots produce poor results because of inadequate fixturing.

    4. Programming and Development: Initial program development typically takes 1-3 weeks depending on complexity. This phase includes weld procedure development, path programming, and cycle time optimization. Offline programming software can reduce development time by 30-50% compared to teach pendant programming. Plan for this phase in your implementation timeline.

    5. Training: Invest in comprehensive training for operators, programmers, and maintenance personnel. Most manufacturers offer training programs ranging from 2-5 days. I’ve found that companies investing in proper training achieve ROI 30-40% faster than those trying to learn on the fly. Budget for ongoing training as new features and software updates become available.

    6. Production Rollout: Start with limited production runs and gradually increase volume as you refine the process. Monitor quality metrics and cycle times closely during the ramp-up period. Most facilities reach full production capability within 4-8 weeks of initial installation. Don’t declare success until you’ve sustained production for at least 30 days.

    ROI Calculation: To calculate return on investment, sum the annual savings from labor reduction, increased production capacity, reduced rework, and material efficiency. Divide the total system cost by annual savings to determine payback period in years. Most robotic welding systems achieve payback in 12-24 months with two-shift operation. With current labor shortages, many facilities see even faster payback in 2026.

    Financing options have improved significantly in recent years. Many equipment vendors offer leasing programs with monthly payments similar to hiring a welder. This approach lets facilities add capacity without large capital outlays and realize positive cash flow from day one. Some vendors also offer rental programs for seasonal production needs.

    Frequently Asked Questions

    What is robotic welding?

    Robotic welding is the use of programmable industrial robots to automate welding processes, performing both the weld and material handling with high precision, consistency, and speed. Common types include arc welding and spot welding, widely used in automotive and manufacturing industries.

    How much does a robotic welding system cost?

    Complete robotic welding cells typically range from $50,000 to $250,000 depending on configuration. Collaborative robots cost $35,000 to $80,000, while traditional arc welding systems range from $70,000 to $150,000. Laser welding systems can cost up to $340,000 for advanced applications.

    How much do robotic welding technicians make?

    Robotic welding technicians typically earn $45,000 to $80,000 annually depending on experience and location. Entry-level positions start around $45,000-$55,000, while experienced technicians earn $60,000-$80,000. Robot programmers earn $65,000-$90,000, with automation engineers reaching $75,000-$130,000+.

    Is robotic welding hard to learn?

    Robotic welding requires specialized training but is learnable with proper instruction. Basic operation can be learned in 1-2 weeks, while full programming proficiency typically takes 3-6 months of hands-on experience. Most manufacturers offer training programs, and community colleges offer robotic welding courses. Previous welding experience helps but isn’t always required.

    Can small shops use robotic welding?

    Yes, collaborative robots (cobots) make automation accessible to small shops. Cobots cost $35,000-$80,000, require minimal floor space, work without safety fencing, and can be moved between workstations. Pre-engineered cells offer turnkey solutions starting around $50,000, with leasing options available for manageable monthly payments.

    What is the ROI for robotic welding?

    Most robotic welding systems achieve payback in 12-24 months with two-shift operation. ROI depends on labor costs, production volume, weld complexity, and efficiency gains. Facilities with high labor costs and consistent part volumes typically see the fastest returns, with some achieving payback in under 12 months.

    What types of welding can be automated?

    Most common welding processes can be automated including MIG/MAG, TIG, flux-cored, spot, laser, plasma arc, and stud welding. The best candidates for automation are repetitive welds on consistent parts with adequate joint access and fixturing capability. Parts with annual volumes over 500 pieces typically justify automation.

  • What is Plasma Arc Cutting? Complete Guide to Plasma Cutting Process

    What is Plasma Arc Cutting? Complete Guide to Plasma Cutting Process

    Plasma arc cutting is a thermal cutting process that uses an accelerated jet of superheated, electrically ionized gas called plasma to cut through electrically conductive materials. The process works by forcing compressed gas through a constricted nozzle while an electrical arc forms between an electrode and the workpiece, ionizing the gas into plasma that reaches temperatures of 20,000 to 30,000 degrees Fahrenheit.

    After working with metal fabrication for over 15 years, I’ve seen plasma arc cutting transform from an industrial-only technology to an accessible tool for hobbyists and small shops. The versatility of this cutting method makes it indispensable for anyone working with metal.

    Unlike mechanical cutting methods that generate chips and require physical contact, plasma cutting melts and blows away metal with a focused stream of ionized gas. This results in cleaner cuts with minimal edge preparation needed for most applications.

    The beauty of plasma cutting lies in its simplicity and effectiveness. In my experience, once you understand the fundamentals, you can produce quality cuts on everything from 26-gauge sheet metal to 2-inch plate.

    How Plasma Cutting Works?

    Quick Summary: Plasma cutting works by creating an electrical channel of ionized gas (plasma) through the workpiece. Compressed gas is forced through a nozzle while a high-voltage arc ionizes the gas into plasma that reaches 30,000 degrees Fahrenheit, melting the metal while the gas stream blows away the molten material.

    The plasma cutting process relies on creating a controlled electrical channel through the workpiece. Here’s what happens during cutting:

    1. Gas Flow Initiation: Compressed gas (typically air, oxygen, or nitrogen) flows through the plasma torch nozzle at high pressure, creating the medium for plasma formation.
    2. Pilot Arc Creation: A high-voltage spark generates a pilot arc between the electrode and the nozzle, ionizing the gas into plasma state.
    3. Arc Transfer: When the torch approaches the workpiece, the electrical arc transfers from the nozzle to the metal, completing the circuit through the conductive material.
    4. Plasma Channel Formation: The electrical energy superheats the gas stream to 20,000-30,000 degrees Fahrenheit, creating a plasma channel that melts through the metal.
    5. Material Removal: The high-velocity plasma stream blows away molten metal, creating a clean cut through the workpiece.

    The entire process happens in milliseconds, with the plasma jet moving along the cut path at speeds ranging from 20 to 300 inches per minute depending on material thickness and amperage.

    Plasma: The fourth state of matter, distinct from solid, liquid, and gas. Plasma is an electrically ionized gas that conducts electricity and can be shaped and directed by magnetic fields. In plasma cutting, the plasma state enables the superheated jet that cuts through metal.

    The Science Behind Plasma Formation

    At the molecular level, plasma forms when gas molecules are stripped of electrons, creating a soup of positive ions and free electrons. This ionization occurs from the intense electrical energy applied to the gas stream. Once ionized, the plasma becomes an excellent conductor of electricity, maintaining the electrical arc needed for cutting.

    The constriction of the plasma stream through the nozzle focuses the energy into a narrow column, typically 0.04 to 0.12 inches in diameter (the kerf width). This focused energy density is what allows plasma to cut through thick metal plates with relative ease.

    Kerf: The width of material removed during the cutting process. In plasma cutting, kerf typically ranges from 0.04 to 0.12 inches (1-3mm), depending on amperage, nozzle size, and material thickness. The kerf is wider at the top of the cut than the bottom, creating a natural bevel angle.

    I’ve spent countless hours watching plasma cutters work, and the physics still fascinate me. The fact that you can take compressed air and electricity to cut through solid metal never gets old.

    Plasma Cutting Equipment and Components

    Understanding plasma cutting equipment helps you select the right system for your needs. After helping dozens of shops choose their first plasma cutter, I’ve learned that matching equipment capabilities to your typical work is essential.

    A complete plasma cutting system consists of several key components working together:

    Power Supply

    The power supply converts incoming AC power into DC power suitable for cutting. Modern plasma cutters use inverter technology with IGBT (Insulated Gate Bipolar Transistor) or MOSFET transistors to produce stable DC output. The power supply determines the maximum cutting capacity based on amperage output.

    Power supplies are rated by output amperage, with higher amperage enabling thicker material cutting. For example, a 40-amp cutter typically handles up to 1/2 inch steel, while 100-amp systems can cut 1-1/2 inch plate.

    Duty Cycle: The percentage of time a plasma cutter can operate within a 10-minute period without overheating. A 60% duty cycle at 40 amps means you can cut for 6 minutes, then need 4 minutes of cooling. Higher duty cycles enable longer continuous cutting sessions.

    Plasma Torch

    The plasma torch is the handheld or machine-mounted component that directs the plasma stream onto the workpiece. Inside the torch, the electrode and nozzle work together to constrict and focus the plasma arc.

    After testing dozens of torch designs over the years, I’ve found that ergonomic design matters as much as cutting performance. A comfortable torch reduces operator fatigue during long cutting sessions.

    Gas System

    Compressed gas is essential for plasma cutting. The gas system includes regulators, filters, and distribution lines that deliver clean, dry gas at the proper pressure. Air compressors are common for general cutting, while specialized applications use oxygen, nitrogen, or argon-hydrogen mixtures.

    Gas quality significantly affects cut quality. Moisture or oil contamination in compressed air causes inconsistent cutting and reduced consumable life. I always recommend installing a quality filter/dryer system.

    Consumable Components

    The electrode and nozzle are wear items that require periodic replacement. The electrode contains a hafnium insert that emits electrons during cutting. Over time, this insert wears, causing poor cut quality. The nozzle orifice gradually enlarges from heat and electrical erosion, reducing cut precision.

    I’ve found that monitoring consumable life prevents most cut quality issues. Experienced operators replace electrodes when the hafnium insert pits to 0.020 inches deep, while nozzles are changed when the orifice becomes oval or oversized by 20%.

    Plasma Cutter Starting Methods

    The method used to initiate the plasma arc affects both equipment capability and applications. Understanding these differences helps when selecting equipment for your specific needs.

    Pilot Arc: A low-current electrical arc that forms between the electrode and nozzle before transferring to the workpiece. The pilot arc ionizes the gas stream without touching the metal, enabling arc starting without physical contact. This protects the nozzle from damage and is essential for CNC applications.

    Pilot Arc Starting

    Pilot arc systems create a low-current arc between the electrode and nozzle before transferring to the workpiece. This allows starting without touching the metal surface, essential for CNC applications and cutting expanded metal or grating. The pilot arc prevents damage to the nozzle and extends consumable life.

    I exclusively use pilot arc machines in my shop because they’re so much more versatile. The ability to start the arc without touching the workpiece saves countless hours on projects involving uneven surfaces.

    High Frequency Starting

    High frequency (HF) start uses a high-voltage spark to ionize the gas and initiate the arc. HF starting provides reliable ignition without contact but can interfere with nearby electronics and CNC controls.

    While HF start is reliable, I’ve seen it cause issues with sensitive electronics. If you work around computers or CNC equipment, consider a blowback start system instead.

    Contact Starting

    Contact start systems require the torch tip to touch the workpiece to initiate the arc. This simple method works well for basic handheld cutting but isn’t suitable for CNC applications. The dragging contact can cause nozzle wear on rough surfaces.

    Contact start is fine for budget units and occasional use, but the consumable wear adds up. For serious work, invest in a pilot arc system.

    Starting MethodBest ForProsCons
    Pilot ArcCNC, expanded metal, professional useNo contact needed, extended consumable life, CNC compatibleHigher cost, more complex
    High FrequencyGeneral purpose cuttingReliable ignition, no contact neededCan interfere with electronics
    Contact StartBudget units, occasional useSimple, reliable, low costNot CNC compatible, higher consumable wear

    Materials and Applications

    Plasma cutting excels at cutting any electrically conductive material. The process works by completing an electrical circuit through the workpiece, so non-conductive materials cannot be cut with plasma.

    MaterialConductivityHandheld CapacityCNC Capacity
    Mild SteelExcellentUp to 1 inchUp to 2 inches
    Stainless SteelGoodUp to 3/4 inchUp to 1.5 inches
    AluminumExcellentUp to 1/2 inchUp to 1.25 inches
    BrassGoodUp to 1/2 inchUp to 1 inch
    CopperExcellentUp to 3/8 inchUp to 3/4 inch

    Industry Applications

    Plasma cutting serves diverse industries due to its versatility and speed. I’ve seen these systems in operation across various applications:

    • Metal Fabrication Shops: General fabrication, structural steel cutting, custom projects
    • Automotive Repair: Body panel replacement, rust removal, exhaust modification
    • Industrial Construction: Steel plate cutting, pipe preparation, structural fabrication
    • HVAC Industry: Ductwork fabrication, sheet metal cutting
    • Salvage Operations: Scrap metal processing, vehicle dismantling
    • Decorative Metalwork: Artistic cutting, signage, architectural elements

    I’ve used plasma cutters in automotive restoration work for years. Nothing beats the ability to cut through rusted floor pans or body panels with precision. The speed advantage over abrasive cutting alone makes the investment worthwhile.

    Material-Specific Considerations

    Different materials behave differently during plasma cutting. Here’s what I’ve learned from years of experience:

    Aluminum: Requires nitrogen or argon-hydrogen gas for best results. The high thermal conductivity means aluminum dissipates heat quickly, so proper amperage and travel speed are critical. I typically use 10-15% higher amperage for aluminum compared to steel of the same thickness.

    Stainless Steel: Cuts cleanly but produces more dross than mild steel. Nitrogen gas produces cleaner edges with less oxidation. The heat affected zone is more noticeable, so slower speeds often yield better results on thicker stainless.

    Copper and Brass: These materials conduct heat extremely well, requiring proper technique. Use nitrogen gas and expect to reduce travel speed by 20-30% compared to mild steel. Thin copper sheet can be challenging due to heat distortion.

    Gas Selection for Plasma Cutting

    Choosing the right gas for plasma cutting significantly affects cut quality and speed. After extensive testing with different gases, I’ve learned that matching gas type to material is essential for optimal results.

    Gas TypeBest MaterialsCut QualityCostNotes
    Compressed AirMild steel, general purposeGoodLowMost common, readily available
    OxygenMild steel up to 1 inchExcellentMediumFaster cutting, squareer edges
    NitrogenAluminum, stainless steelExcellentMediumClean cuts, less oxidation
    Argon-HydrogenAluminum, stainless (thick)SuperiorHighHigh-definition cutting, smooth edges

    Compressed Air

    Compressed air is the most economical choice for general plasma cutting. It works well for mild steel and provides acceptable results on stainless and aluminum. Since most shops already have air compressors, this is the default choice for many users.

    I’ve found that air quality matters tremendously. Moisture in compressed air causes inconsistent cuts and reduces consumable life. Invest in a good air dryer and filter system.

    Oxygen

    Oxygen plasma cutting provides the fastest speeds on mild steel up to 1 inch thick. The oxygen reacts with the iron in steel, creating additional heat that speeds up the cutting process. This results in squarer edges and less dross.

    The downside is that oxygen accelerates consumable wear, particularly electrodes. I only use oxygen when cutting speed is critical or when edge quality on mild steel is the top priority.

    Nitrogen

    Nitrogen is the gas of choice for aluminum and stainless steel cutting. It produces clean, oxide-free edges with minimal heat affected zone. Nitrogen also extends consumable life compared to oxygen.

    For production shops cutting aluminum and stainless, nitrogen is worth the extra cost. The edge quality difference is noticeable, especially on thicker materials.

    Argon-Hydrogen Mixtures

    Argon-hydrogen blends (typically H35: 65% argon, 35% hydrogen) are used for high-definition plasma cutting. This gas combination produces the smoothest edges on aluminum and stainless steel up to 1-1/2 inches thick.

    The cost is significantly higher than other options, but for applications requiring minimal secondary processing, argon-hydrogen is hard to beat. I’ve used it for architectural metalwork where edge appearance matters.

    Safety Requirements for Plasma Cutting

    Safety is critical when working with plasma cutting systems. The combination of high voltage, extreme temperatures, and ultraviolet radiation requires proper protection. I’ve seen the consequences of inadequate safety measures—never cut corners on protective equipment.

    Eye and Face Protection

    The plasma arc emits intense ultraviolet and infrared radiation that can cause arc eye—a painful condition similar to sunburn on your corneas. Proper eye protection is mandatory based on cutting amperage.

    Amperage RangeShade NumberApplication
    0-20 AmpsShade #4Light duty, thin materials
    20-40 AmpsShade #5General handheld cutting
    40-60 AmpsShade #6Medium duty fabrication
    60-80 AmpsShade #8Heavy duty handheld
    80-300 AmpsShade #8-10CNC and industrial cutting

    Reference: ANSI Z87.1+ and OSHA standards for eye protection during plasma cutting operations.

    Additional PPE Requirements

    Beyond eye protection, plasma cutting requires comprehensive personal protective equipment:

    • Flame-resistant clothing: Leather apron, jacket, and gauntlets protect against sparks and molten metal spray
    • Leather gloves: Heavy-duty gloves with forearm protection prevent burns from hot workpieces
    • Respiratory protection: Cutting coated or galvanized steel produces toxic fumes requiring appropriate ventilation or respirators
    • Hearing protection: Plasma cutting generates 95-115 dB, requiring earplugs or muffs for extended operation
    • Foot protection: Steel-toe leather boots protect against falling metal and sparks

    Heat Affected Zone (HAZ): The area of metal adjacent to the cut that experiences thermal changes during cutting. Plasma cutting produces a smaller HAZ than oxy-fuel cutting but larger than laser or waterjet. The HAZ can affect material properties and may require heat treatment for critical applications.

    Fire Prevention

    Plasma cutting throws sparks up to 20 feet from the cut location. Always clear the work area of flammable materials, keep a fire extinguisher nearby, and never cut near fuel tanks or chemical storage. I’ve seen too many shop fires caused by inadequate spark containment.

    Ventilation Requirements

    Proper ventilation is non-negotiable when plasma cutting. The process produces metal fumes and gases that can be hazardous to health. When cutting coated materials like galvanized steel, the zinc coating releases toxic fumes that require specific respiratory protection.

    I always recommend cutting in a well-ventilated area or using a downdraft table. For indoor production environments, a proper fume extraction system is essential for worker safety.

    Plasma Cutting vs Other Methods

    Understanding how plasma cutting compares to alternatives helps you select the right method for your application. After testing multiple cutting technologies, I’ve learned that each method has its strengths depending on material, thickness, and required edge quality.

    FactorPlasmaOxy-FuelLaserWaterjet
    Cut QualityGoodFairExcellentExcellent
    Max Thickness (Steel)2 inches12 inches1 inch8+ inches
    Speed (1/4″ steel)60-120 IPM10-20 IPM100-200 IPM10-20 IPM
    Equipment Cost$$$$$$$$$$
    Operating CostLowMediumLowHigh
    Material RangeConductive onlyFerrous onlyMost metalsAny material
    Heat Affected ZoneMinimalSignificantVery minimalNone

    Plasma vs Oxy-Fuel Cutting

    For thin materials under 1 inch, plasma cutting is 5-10 times faster than oxy-fuel. Plasma also cuts all conductive metals, while oxy-fuel only works on ferrous materials (iron-based). However, for thick steel over 2 inches, oxy-fuel often provides better economy and can cut thicker materials.

    I keep both systems in my shop for different applications. Plasma handles everything under 1 inch, while oxy-fuel comes out for the heavy plate work. This dual approach maximizes efficiency while minimizing operating costs.

    Plasma vs Laser Cutting

    Laser cutting produces superior edge quality with minimal heat-affected zone, but equipment costs are 3-5 times higher than plasma. For most fabrication applications under 1 inch thickness, high-definition plasma provides acceptable quality at a fraction of the cost.

    Laser wins for high-precision work and thin materials where edge quality is critical. But for general fabrication, plasma offers the best balance of speed, quality, and cost.

    Plasma vs Waterjet Cutting

    Waterjet cutting produces excellent edge quality with no heat-affected zone and can cut any material. However, cutting speeds are much slower than plasma, and operating costs (abrasive, water treatment) are significantly higher. Waterjet excels for thick materials and heat-sensitive applications.

    I’ve found waterjet ideal for materials that can’t tolerate heat, like hardened tool steel or certain composites. For everyday metal cutting, plasma’s speed advantage is hard to beat.

    CNC Plasma Cutting

    Computer Numerical Control (CNC) plasma cutting automates the cutting process for precise, repeatable results. CNC systems move the plasma torch along programmed paths, enabling complex shapes and high-production runs without operator intervention.

    Benefits of CNC Integration

    CNC plasma cutting offers significant advantages for production environments:

    • Precision: Repeatability within 0.01 inch for consistent parts
    • Productivity: Unattended operation allows one operator to manage multiple machines
    • Complex Shapes: Intricate patterns and designs impossible to cut by hand
    • Material Optimization: Nesting software minimizes waste
    • Quality Consistency: Automated torch height control maintains optimal cutting parameters

    I’ve helped shops transition from handheld to CNC cutting and typically see productivity gains of 200-300% with reduced material waste and improved part consistency.

    CNC Configuration Options

    CNC plasma tables range from small 4×4 foot hobby units to industrial 8×20 foot or larger systems. Configurations include:

    • Standard 2-axis: X-Y movement for flat pattern cutting
    • 3-axis systems: Added Z-axis for torch height control
    • Bevel cutting heads: 5-axis capability for edge preparation weld bevels

    For small shops just starting with CNC, I recommend a 4×4 or 4×8 foot table. These sizes handle most common sheet metal dimensions without requiring excessive floor space.

    CNC Applications

    CNC plasma cutting shines in production environments where consistency matters. Common applications include:

    • HVAC ductwork: Complex fittings cut from flat sheet
    • Automotive parts: Brackets, floor pans, body panels
    • Decorative art: Intricate patterns for gates, signs, railings
    • Industrial parts: Machine guards, mounting plates, shrouds

    The decorative metalwork market has exploded with CNC plasma. I’ve seen small businesses built entirely around custom plasma-cut art and architectural elements.

    Cost Considerations

    Understanding the total cost of plasma cutting helps justify equipment investment and budget for ongoing expenses. After managing shop equipment budgets for years, I’ve learned that looking beyond purchase price reveals the true value proposition.

    CategoryPrice RangeAmperageCapacity
    DIY/Hobbyist$200-$80020-40 AmpsUp to 1/4 inch steel
    Light Professional$800-$2,00040-60 AmpsUp to 3/4 inch steel
    Professional$2,000-$5,00060-100 AmpsUp to 1.5 inch steel
    Industrial$5,000-$20,000+100-400+ AmpsUp to 2+ inch steel

    Operating Cost Breakdown

    Over the equipment lifetime, total cost of ownership typically breaks down as:

    • Initial Equipment: 60-70% of lifetime cost
    • Consumables: 20-25% of lifetime cost (electrodes, nozzles, shields)
    • Electricity: 5-10% of lifetime cost
    • Maintenance: 5-10% of lifetime cost

    Consumable costs average $2-5 per hour of cutting time depending on amperage and starting method. Pilot arc systems consume electrodes faster than contact start but provide better cut quality and CNC compatibility.

    ROI Considerations

    For professional shops, plasma cutting equipment typically pays for itself within 6-12 months through reduced outsourcing costs and increased production capacity. I’ve calculated ROI on dozens of equipment purchases, and plasma cutters consistently show strong returns.

    When calculating ROI, factor in labor savings, reduced material waste, and the ability to take on work you previously outsourced. The true value extends beyond the equipment price tag.

    Troubleshooting and Maintenance

    Regular maintenance prevents most plasma cutting problems. Based on years of field experience, I’ve identified common issues and their solutions.

    Common Cut Quality Problems

    ProblemLikely CauseSolution
    Excessive drossSlow speed or low amperageIncrease cutting speed or amperage
    Beveled edgesWorn nozzle, incorrect gas pressureReplace nozzle, check pressure
    Rough cut edgeWrong amperage for thicknessMatch amperage to material
    Won’t initiate arcBad ground connection, worn consumablesClean ground clamp, replace electrode
    Double arcingWorn nozzle, incorrect standoffReplace nozzle, adjust torch height

    Consumable Maintenance Schedule

    Preventive maintenance extends equipment life and maintains cut quality:

    • Electrodes: Replace every 2-4 hours of cutting time or when hafnium insert pits to 0.020 inches
    • Nozzles: Replace when orifice becomes oval or oversized by 20%
    • Shields/Retaining Caps: Replace every 3-5 electrode changes
    • Gas Filters: Replace monthly or per manufacturer recommendation

    Keeping a maintenance log helps track consumable life and predict replacement intervals. I recommend keeping spares of all consumables on hand to avoid downtime during critical jobs.

    System Maintenance Tips

    Beyond consumables, regular system maintenance keeps your plasma cutter running reliably:

    Air System: Check filters weekly and drain compressor tanks daily. Moisture in the air system is the leading cause of cut quality issues I encounter.

    Electrical Connections: Inspect cables and connections monthly. Loose connections cause voltage drops that affect cutting performance.

    Torch Assembly: Clean torch threads and reapply anti-seize during consumable changes. This prevents stuck components and ensures proper gas flow.

    Ground Clamp: Keep the ground clamp clean and tight. A poor ground causes inconsistent arc starting and poor cut quality.

    Frequently Asked Questions

    What is plasma arc cutting?

    Plasma arc cutting is a thermal cutting process that uses an accelerated jet of superheated, electrically ionized gas to cut through electrically conductive materials. The process creates an electrical channel of ionized plasma gas from the cutter through the workpiece, melting metal while a high-velocity gas stream blows away molten material. It cuts steel, stainless steel, aluminum, brass, and copper.

    How does plasma cutting work?

    Plasma cutting works by forcing compressed gas through a constricted nozzle while a high-voltage electrical arc forms between an electrode and the workpiece. This arc ionizes the gas into plasma reaching 20,000-30,000 degrees Fahrenheit. The superheated plasma jet melts through the metal while the high-velocity gas stream blows away the molten material, creating a clean cut.

    What materials can be cut with a plasma cutter?

    Plasma cutters can cut any electrically conductive material including steel, stainless steel, aluminum, brass, copper, and other conductive metals. The process requires an electrical circuit through the workpiece, so non-conductive materials like wood, plastic, glass, and ceramics cannot be cut with plasma. Cutting capacity varies by material conductivity and machine amperage.

    How thick can plasma cutters cut?

    Handheld plasma cutters typically cut up to 1 inch thick steel, while CNC systems can handle up to 2 inches. Industrial high-amperage systems (200+ amps) can cut steel up to 6 inches thick. Cutting capacity depends on amperage output and the specific material being cut. Aluminum and stainless typically have reduced thickness capacity compared to mild steel.

    What gas is used in plasma cutting?

    Compressed air is the most common gas for general plasma cutting of steel. Oxygen provides faster cutting speeds on mild steel. Nitrogen is used for aluminum and stainless steel for cleaner cuts. Argon-hydrogen mixtures are used for high-definition cutting of aluminum and stainless steel, providing the best edge quality. Gas selection significantly affects cut quality and speed.

    What shade number for plasma cutting?

    Eye protection shade requirements vary by amperage: Shade #4 for 0-20 amps, Shade #5 for 20-40 amps, Shade #6 for 40-60 amps, Shade #8 for 60-80 amps, and Shade #8-10 for 80-300+ amps. Always use ANSI Z87.1+ certified protection and follow OSHA requirements for your specific application. The plasma arc produces dangerous UV radiation that can cause arc eye.

    What are the advantages of plasma cutting?

    Plasma cutting offers 5-10 times faster cutting than oxy-fuel on thin materials, cuts all electrically conductive metals, produces cleaner edges with minimal dross, can cut curved and complex shapes, generates no metal chips, and costs less than laser cutting. The process provides excellent versatility for metal fabrication with equipment costs suitable for both hobbyists and professionals.

    Is plasma cutting better than oxy-fuel?

    For thin materials under 1 inch, plasma cutting is 5-10 times faster than oxy-fuel and cuts all conductive metals. Plasma also produces cleaner edges with less heat distortion. However, oxy-fuel excels at cutting thick steel over 2 inches and has lower equipment costs. The best choice depends on your typical material thickness and cutting volume. Many shops keep both systems for different applications.


  • Oxy Fuel Welding: Complete Beginner’s Guide to Gas Welding 2026

    Oxy Fuel Welding: Complete Beginner’s Guide to Gas Welding 2026

    Looking for a welding method that doesn’t require electricity and can handle everything from joining metal to cutting through thick steel plates? Oxy fuel welding might be exactly what you need.

    What is Oxy Fuel Welding?

    Oxy-fuel welding (also called oxyacetylene welding, oxy welding, or gas welding) is a welding process that uses fuel gases combined with pure oxygen to weld and cut metals. The most common fuel is acetylene, which produces a flame reaching 3,500degC (6,330degF) when mixed with oxygen. This versatile process is used for welding, brazing, cutting, and heating applications in metal fabrication, automotive repair, and industrial maintenance.

    Unlike electric welding methods that require a power source, oxy fuel welding relies on the combustion of fuel gases. This makes it incredibly portable and useful in locations without electrical access.

    I’ve worked with various welding methods over the years, and oxy fuel remains one of the most versatile tools in any metalworker’s arsenal. When you’re out in the field working on farm equipment or need to heat a rusty bolt without dragging around a heavy MIG welder, nothing beats the simplicity of a gas torch.

    Quick Summary: Oxy fuel welding uses oxygen and fuel gas (usually acetylene) to create an ultra-hot flame for welding, cutting, and heating metal. It’s portable, versatile, and still widely used in 2026 for applications ranging from automotive repair to scrap metal cutting.

    How Oxy Fuel Welding Works?

    The science behind oxy fuel welding is straightforward: fuel gas combines with pure oxygen and burns at extreme temperatures. When this flame contacts metal, it creates a molten pool that allows you to join pieces together or cut through them entirely.

    Think of it like a controlled camp fire that burns hot enough to melt steel. By adjusting the ratio of oxygen to fuel, you can change the flame characteristics for different tasks. More oxygen gives you a cutting flame. Less oxygen creates a welding or brazing flame.

    What makes oxy fuel unique is the use of pure oxygen instead of ambient air. Regular air is only about 21% oxygen. By using 100% oxygen, the flame burns much hotter and more efficiently. This is why oxy-acetylene reaches temperatures over 3,000degC while a standard propane torch tops out around 1,900degC.

    Combustion: The chemical reaction between fuel gas and oxygen that produces heat. In oxy fuel welding, we maximize this reaction by using pure oxygen instead of air.

    Oxy-Fuel Welding Equipment You Need

    Setting up for oxy fuel welding requires several key components. Each piece serves a specific purpose in the system.

    EquipmentPurposeTypical Cost Range
    Oxygen CylinderStores pure oxygen at high pressure$100-$300 (full)
    Fuel CylinderStores acetylene or other fuel gas$150-$400 (full)
    Pressure RegulatorsControls gas pressure from cylinders$50-$150 each
    Welding Torch HandleMixes gases and controls flame$80-$250
    Gas HosesDelivers gases from regulators to torch$30-$80 per pair
    Flashback ArrestorsSafety device preventing flame backfire$30-$60 each
    Welding/Cutting TipsInterchangeable tips for different tasks$15-$50 each
    Complete Starter KitAll components except cylinders$200-$600

    Oxygen and Fuel Cylinders

    The oxygen cylinder stores pure oxygen at pressures up to 2,200 PSI. These cylinders are color-coded green in the United States. The fuel cylinder (usually acetylene) stores fuel gas at much lower pressures since acetylene becomes unstable above 15 PSI.

    I learned the hard way that cylinder positioning matters. Oxygen cylinders should always be secured upright. Acetylene cylinders contain a porous material and acetone to stabilize the gas. They must also be kept upright or the acetone can enter the regulator and cause damage.

    Pressure Regulators

    Regulators reduce the high pressure in the cylinders to working pressure. Oxygen typically operates at 10-40 PSI for welding. Acetylene runs at 3-15 PSI depending on the tip size and application.

    Quality regulators make a difference. After going through three cheap sets in five years, I invested in Victor regulators and haven’t looked back. They maintain consistent pressure and the gauges are actually readable.

    The Welding Torch

    The torch is where gases mix and combustion happens. Most torches have two control valves: one for oxygen and one for fuel. The mixture happens in the torch body or at the tip, depending on the design.

    Injector torches use high-pressure oxygen to draw in fuel gas. This design allows the use of any fuel gas. Equal-pressure torches require both gases at similar pressures and work best with acetylene.

    Safety Devices

    Flashback arrestors are non-negotiable safety equipment. They prevent flame from traveling back into the hoses and cylinders. Flashback can cause catastrophic cylinder failure. Install arrestors at both the regulator and torch ends.

    Check valves serve a similar purpose, preventing gas from flowing backward through the system. Many modern torches have built-in check valves, but external flashback arrestors provide additional protection.

    Types of Fuel Gases Explained

    While acetylene is the traditional choice, several fuel gases work for oxy fuel applications. Each has advantages and limitations.

    Fuel GasFlame TempBest ForCost (Relative)
    Acetylene3,160degC in oxygenWelding steel up to 1/4 inchHigh
    Propane2,820degC in oxygenCutting, heating, brazingLow
    MAPP Gas2,930degC in oxygenHeating, brazing, light cuttingMedium
    Propylene2,900degC in oxygenCutting, heatingMedium
    Natural Gas2,740degC in oxygenHeating large areasVery Low

    Acetylene: The Traditional Choice

    Acetylene produces the hottest flame among common fuel gases and is the only fuel suitable for welding steel. Its concentrated heat creates a small, intense flame ideal for precise work.

    However, acetylene has limitations. It’s unstable above 15 PSI and requires special handling. The cylinders are expensive to refill. For cutting and heating applications, cheaper alternatives often make more sense.

    Propane: The Budget-Friendly Alternative

    Propane costs about one-third as much as acetylene and is readily available at any hardware store. It excels at heating and cutting applications where the lower flame temperature isn’t a disadvantage.

    For scrap yards doing primarily cutting work, propane is the economic choice. I’ve seen operations save thousands annually by switching from acetylene to propane for cutting tasks.

    MAPP and Propylene

    MAPP gas (methylacetylene-propadiene propane) offers a middle ground between acetylene and propane. It burns hotter than propane but costs more. Production of true MAPP gas ended in 2008, but similar propylene blends are sold under the same name.

    Propylene provides excellent heat for brazing and heating. It’s a common choice for HVAC technicians and HVAC repair work where heating larger areas is necessary.

    Understanding Flame Types

    The appearance and characteristics of your oxy fuel flame depend on the oxygen-to-fuel ratio. Mastering flame identification is fundamental to successful oxy fuel welding.

    Quick Summary: There are three types of oxy fuel flames: neutral (balanced), carburizing (fuel-rich), and oxidizing (oxygen-rich). The neutral flame is used for most welding. Carburizing flames add carbon to metal. Oxidizing flames oxidize the weld pool.

    1. Neutral Flame: Equal parts oxygen and fuel. The inner cone is bright blue with a well-defined tip. This is the standard welding flame for most applications. It produces clean welds without adding or removing elements from the metal.
    2. Carburizing Flame: Excess fuel. The inner cone has a feathery edge and appears bluish-white with an acetylene “feather” extending from the tip. This flame adds carbon to the weld pool. It’s used for welding high-carbon steels and for certain brazing applications.
    3. Oxidizing Flame: Excess oxygen. The inner cone is shorter, sharper, and paler blue than a neutral flame. The flame makes a hissing sound. This flame removes carbon from metal and is used for welding copper, brass, and bronze.

    Identifying Your Flame

    Start with more fuel than oxygen and gradually increase oxygen until you achieve the desired flame. A neutral flame should have a clearly defined inner cone about 1/8 to 1/4 inch long depending on tip size.

    I spent weeks practicing flame adjustment before attempting my first real weld. The difference between a nearly-neutral and truly neutral flame is subtle but affects weld quality significantly. Take the time to learn this skill.

    Setting Up Your Oxy-Acetylene Torch

    Proper setup is critical for safety and performance. Follow these steps in order.

    1. Position Cylinders: Secure cylinders upright. Chain them to a wall or cylinder cart. Oxygen cylinders should be at least 20 feet from combustible materials.
    2. Check Connections: Ensure all hose connections are tight. Check that regulator threads match the cylinder valves (oxygen is right-hand thread, fuel is left-hand thread to prevent cross-connection).
    3. Open Cylinder Valves Slowly: Stand to the side of the cylinder. Open oxygen valve fully against the backseat. Open fuel valve only 1/4 to 1/2 turn (acetylene valves should never be fully opened).
    4. Set Working Pressures: With torch valves closed, adjust each regulator to the recommended pressure for your tip size. Typical welding pressures: 3-5 PSI acetylene, 10-20 PSI oxygen.
    5. Check for Leaks: Use a soap solution or leak detection fluid on all connections. Bubbles indicate leaks that must be fixed before proceeding.
    6. Purge Hoses: Briefly open torch valves to clear air from hoses. Do this separately for each gas.
    7. Light the Torch: Open fuel valve slightly and ignite with a striker. Adjust fuel until flame leaves tip but doesn’t separate.
    8. Add Oxygen: Gradually open oxygen valve until you achieve desired flame type.

    Shutdown Procedure

    Proper shutdown prevents equipment damage and ensures safety. Close oxygen valve first, then fuel valve. Close cylinder valves. Drain remaining gas by opening torch valves until gauges read zero. Back off regulator adjustment screws. Coil hoses neatly.

    Basic Oxy Fuel Welding Techniques

    Welding with oxy fuel requires coordination between torch movement and filler rod addition. The learning curve is steeper than MIG welding but more forgiving than TIG.

    Preparing the Metal

    Clean the weld area thoroughly. Remove paint, rust, and oil. Bevel thick materials (over 1/8 inch) to ensure full penetration. Proper joint preparation accounts for about 50% of weld quality.

    The Welding Process

    Hold the torch at a 45-degree angle to the workpiece. The flame should be directed at the joint. Move the torch in a circular or slight weaving motion to distribute heat evenly.

    When the metal forms a shiny puddle, introduce the filler rod. The rod should melt into the puddle, not be directly melted by the flame. Continue moving along the joint, maintaining a consistent puddle size.

    Quick Summary: Basic oxy fuel welding technique involves heating the metal with a neutral flame until molten, then adding filler rod while moving along the joint. Maintain consistent torch speed and puddle size for even welds.

    Common Joint Types

    • Butt Joint: Two pieces placed edge-to-edge. Best for material up to 1/8 inch.
    • Lap Joint: Pieces overlap. Easier for beginners and provides more surface area.
    • T-Joint: One piece perpendicular to another. Common in structural applications.
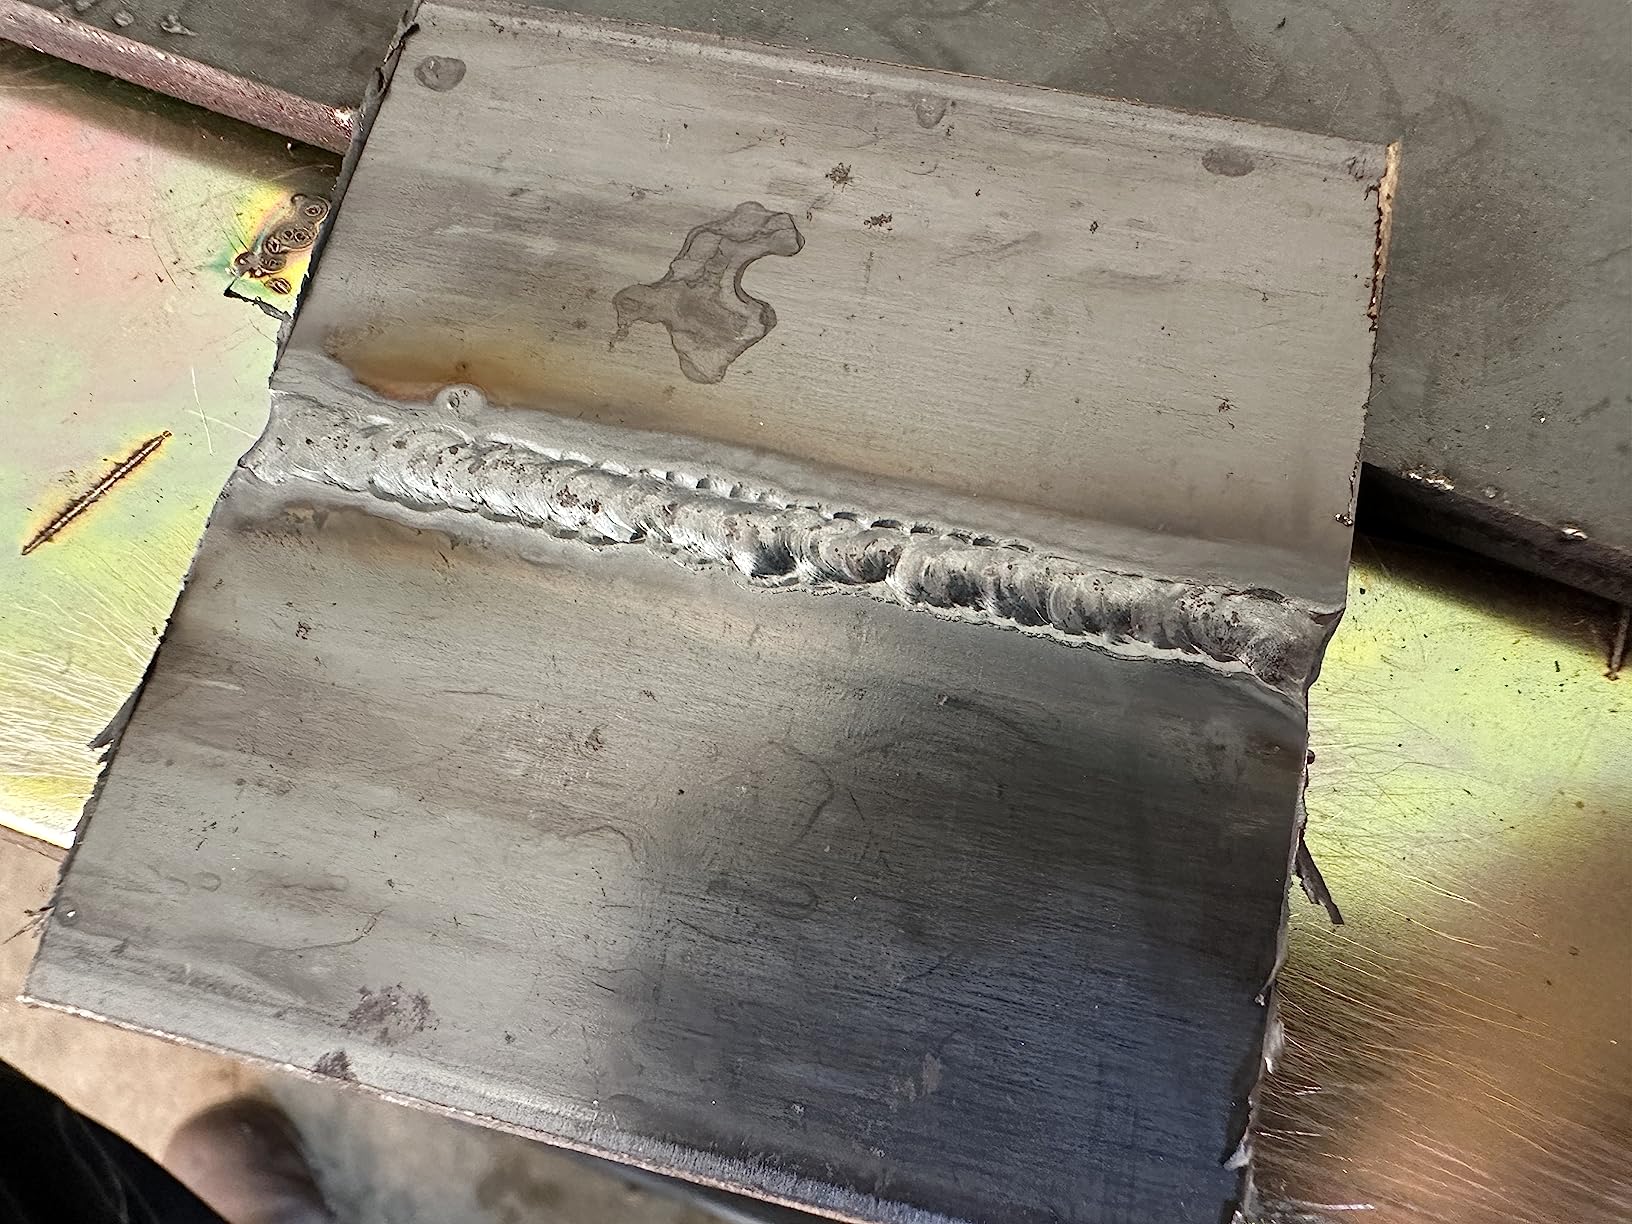
    • Corner Joint: Pieces meet at an edge. Used for box and frame construction.

    Beginner Mistakes to Avoid

    After teaching dozens of people to weld, I see the same mistakes repeatedly. Moving too fast is number one. Let the puddle develop before adding filler. Another common error is holding the torch too far from the work. The flame inner cone should nearly touch the metal.

    Using the wrong filler rod causes many failures. Match the filler material to your base metal. For mild steel, use RG-45 or RG-60 rods. They’re designed specifically for gas welding.

    Oxy Fuel Cutting Guide

    Cutting with oxy fuel is fundamentally different from welding. The process heats steel to ignition temperature, then a pure oxygen stream burns through the material. It’s called “oxidation cutting” rather than true cutting.

    Only ferrous metals can be cut with oxy fuel. You cannot cut aluminum, stainless steel, or copper with this process. For those materials, consider plasma cutting or abrasive methods.

    The Cutting Process

    1. Mark Your Cut Line: Use soapstone or marker to clearly identify where to cut.
    2. Preheat the Edge: Hold the torch perpendicular to the metal. Heat the starting point until it’s cherry red (approximately 1,600degF).
    3. Activate Cutting Oxygen: Press the cutting oxygen lever. A stream of pure oxygen will pierce the metal.
    4. Move Along the Path: Once through, move the torch along your cut line. The kerf (cut width) should be uniform.
    5. Finish the Cut: Slow at corners. Let the cut fully complete before moving away.

    Cutting Tips and Techniques

    Tip size determines thickness capacity. A general rule: tip number equals material thickness in sixteenths of an inch. A #3 tip handles 3/16 inch material. A #6 tip cuts through 3/8 inch plate.

    For thick material, bevel the edge before starting. This gives the preheat flame more surface area to work with. When cutting thick plate, I bevel the start point about 45 degrees. This reduces preheat time by nearly half.

    Safety Procedures and Equipment

    Oxy fuel welding involves high-pressure gases, extreme heat, and potential explosion hazards. Proper safety procedures are non-negotiable.

    Safety EquipmentPurposeEssential?
    Welding Goggles #5 ShadeEye protection from UV/IRYes
    Flame-Resistant ClothingBurn preventionYes
    Leather GlovesHand protectionYes
    Flashback ArrestorsPrevents cylinder explosionYes
    Fire ExtinguisherEmergency fire responseYes
    Respirator (if needed)Fume protectionSometimes

    Eye Protection

    Oxy fuel welding produces ultraviolet and infrared radiation. Standard safety glasses are not adequate. Use #3 to #5 shade goggles for welding. #5 shade is recommended for most applications. For cutting, lighter shades (#3-4) improve visibility while still providing protection.

    Cylinder Safety

    Oxygen under pressure can cause spontaneous combustion of oil and grease. Never use oil-based lubricants on oxygen fittings. Oxygen cylinders must be stored separately from fuel cylinders or separated by a firewall at minimum.

    Acetylene cylinders require special handling. Never draw acetylene above 15 PSI. Never lay an acetylene cylinder on its side. If a cylinder has been laid down, stand it upright for at least 30 minutes before use.

    Flashback Prevention

    Flashback occurs when flame travels backward into the equipment. It’s caused by incorrect pressure settings, blocked tips, or allowing the flame to burn the tip. Signs of flashback include a popping sound, flame at the torch body, or sudden hissing.

    If flashback occurs: immediately close both torch valves. Close cylinder valves. Check equipment for damage before resuming. Flashback arrestors are your last line of defense and should be inspected regularly.

    Ventilation

    Welding produces fumes that can be harmful. Work in well-ventilated areas. When working indoors, use exhaust fans or local exhaust ventilation. Certain materials (galvanized steel, painted metals) produce particularly toxic fumes when heated.

    Flashback: A dangerous condition where the flame travels back through the torch into the hoses or cylinders. Flashback arrestors are safety devices designed to prevent this by extinguishing backfire.

    Common Applications and Uses

    Despite the rise of electric welding methods, oxy fuel remains relevant in 2026 for specific applications where it excels.

    Automotive Repair

    Older vehicles with steel bodies respond well to gas welding. Sheet metal can be welded or brazed without the heat distortion common with other methods. Oxy fuel is also ideal for heating rusty bolts and seized parts for removal.

    Metal Fabrication

    For light fabrication and repair work, oxy fuel offers versatility that single-purpose electric welders cannot match. One setup handles welding, cutting, heating, and brazing. This versatility makes it popular in small fabrication shops.

    Scrap and Salvage

    Scrap yards rely on oxy fuel cutting for dismantling equipment and processing scrap metal. The portability of gas torches allows cutting anywhere without electrical access. Propane is commonly used here due to its low cost.

    Heating Applications

    Sometimes the goal isn’t to weld but to heat. Oxy fuel excels at bending metal, heat treating, freeing frozen bolts, and preheating thick materials before welding with other methods. A rosebud tip attachment spreads heat over a larger area for heating applications.

    Brazing and Soldering

    Oxy fuel produces precise heat control ideal for brazing and soldering. The ability to adjust flame characteristics makes it suitable for various filler metals and fluxes. Plumbing, HVAC, and refrigeration work all rely on gas torches for brazing copper tubing.

    Oxy-Fuel vs Electric Welding

    Understanding when oxy fuel is the right choice versus when electric welding makes more sense helps you select the appropriate method for your projects.

    FactorOxy-Fuel WeldingElectric Welding (MIG/TIG/Stick)
    Power RequirementNone – works anywhereRequires electricity (110V/220V)
    Initial Equipment Cost$200-$600$300-$1,500+
    Operating CostHigher – ongoing fuel costLower – electricity and consumables
    Welding SpeedSlowerFaster
    Metal Thickness RangeUp to 1/4 inch welding (thicker cutting)Wide range – sheet to thick plate
    PortabilityExcellent – cylinders are portableLimited by power access
    VersatilityWelds, cuts, heats, brazesPrimarily welding
    Learning CurveModerate to steepMIG easiest, TIG steepest
    Best ApplicationsField work, heating, cutting, repairProduction, fabrication, thick materials

    Advantages of Oxy Fuel Welding

    The portability of oxy fuel equipment cannot be overstated. I’ve welded fence posts in the middle of a pasture and cut steel beams at construction sites without power access. The equipment rides in the back of a pickup truck and goes anywhere.

    Multi-function capability is another strength. One outfit handles welding, cutting, brazing, soldering, and heating. For hobbyists and small shops, this versatility eliminates the need for multiple specialized tools.

    Disadvantages of Oxy Fuel Welding

    Operating costs add up over time. Gas refills are expensive compared to electricity. For high-volume welding, electric methods are more economical.

    Speed is another limitation. Oxy fuel welding is significantly slower than MIG welding. Production environments favor electric methods for this reason.

    When to Choose Oxy Fuel?

    Choose oxy fuel when you need portability, versatility, or lack electrical access. Field repair work, automotive hobbyists, and scrap processing are ideal applications. For production welding or thick material fabrication, electric welding typically makes more sense.

    Frequently Asked Questions

    What is oxy fuel welding?

    Oxy fuel welding is a welding process that uses fuel gases combined with oxygen to weld and cut metals. The most common fuel is acetylene, which creates a flame reaching 3,500degC when mixed with pure oxygen. This process can weld, cut, braze, and heat metal.

    How hot is an oxy acetylene flame?

    An oxy-acetylene flame reaches approximately 3,160degC (5,720degF) in oxygen. This makes it the hottest common fuel gas flame available. For comparison, propane burns at approximately 2,820degC in oxygen.

    What are the three types of oxy fuel flames?

    The three types are neutral flame (balanced oxygen and fuel, used for most welding), carburizing flame (excess fuel with a feathery inner cone, adds carbon to metal), and oxidizing flame (excess oxygen with a short pale inner cone, removes carbon from metal).

    Is oxy fuel welding still used today?

    Yes, oxy fuel welding remains widely used in 2026 for specific applications. While electric welding has replaced it for many production tasks, oxy fuel excels in field work, automotive repair, scrap cutting, and heating applications where portability and versatility are valued.

    What gas is used in oxy fuel welding?

    Acetylene is the most common fuel gas for welding because it produces the hottest flame and a concentrated heat pattern. Other fuels include propane (popular for cutting and heating due to low cost), MAPP gas, propylene, and natural gas. Propane cannot be used for welding steel but works well for cutting.

    What is the difference between oxy fuel and arc welding?

    Oxy fuel welding uses combustion of fuel gas and oxygen to create heat, while arc welding uses electrical current to create an electric arc. Oxy fuel doesn’t require electricity and can also cut and heat metal. Arc welding is generally faster, more economical for high-volume work, and produces welds on thicker materials more easily.

    Can you weld aluminum with oxy fuel?

    Welding aluminum with oxy fuel is difficult and not recommended for most applications. Aluminum has a low melting point and high thermal conductivity, making it challenging to weld with oxy fuel. TIG welding is the preferred method for aluminum. Oxy fuel can be used for aluminum brazing with appropriate filler rods.

    How much does oxy fuel welding equipment cost?

    A complete starter kit (excluding cylinders) costs between $200 and $600 depending on quality and brand. Full cylinders cost an additional $250-$700. Budget setups from home center stores start around $200, while professional-grade equipment from brands like Victor or Smith ranges from $500-$800 for the torch outfit alone.

  • Nonferrous Metals: The Complete Guide to Properties, Types & Uses

    Nonferrous Metals: The Complete Guide to Properties, Types & Uses

    After 15 years working in fabrication and manufacturing, I have seen how material selection can make or break a project. Nonferrous metals are among the most versatile materials in modern industry, found everywhere from aircraft to electronics.

    Nonferrous metals are metals and alloys that contain little to no iron (typically less than 0.1%). Unlike ferrous metals that rust when exposed to moisture, nonferrous metals like aluminum, copper, and titanium offer superior corrosion resistance, electrical conductivity, and lightweight properties that make them essential for electrical wiring, aircraft, and marine applications.

    Understanding these metals is crucial whether you are selecting materials for a project, identifying scrap metal, or studying metallurgy. Let me break down everything you need to know.

    What Are Nonferrous Metals?

    Nonferrous Metals: Metals and alloys that do not contain iron in appreciable amounts. The term comes from the Latin “ferrum” meaning iron, so nonferrous literally means “without iron.”

    The iron content threshold is typically less than 0.1%. This small amount of iron does not give these metals the magnetic or rusting properties associated with ferrous metals like steel and cast iron.

    I have watched machinists spend hours identifying unknown metal pieces in shops. The magnet test is usually the first step. If a magnet does not stick, you are likely dealing with a nonferrous metal.

    Common Types of Nonferrous Metals

    Nonferrous metals encompass a wide range of elements. Here are the most common ones you will encounter:

    Quick Summary: Aluminum is the most widely used nonferrous metal due to its lightweight properties. Copper dominates electrical applications. Titanium offers the highest strength-to-weight ratio but comes at a premium cost.

    1. Aluminum

    Aluminum is the most common nonferrous metal in the world. I have seen it transform industries from automotive to aerospace.

    Key properties include a density of 2.7 g/cm3 (about one-third that of steel), excellent corrosion resistance due to its natural oxide layer, and high thermal and electrical conductivity.

    In my experience working with aluminum alloys, I have found that 6061 is the go-to grade for structural applications while 7075 offers superior strength for aerospace uses. The difference matters. I once saw a project fail because someone used 3003 series aluminum where 6061 was required.

    Common Uses:

    • Aircraft and spacecraft structures
    • Automotive body panels and engine components
    • Window frames and doors
    • Aluminum cans and packaging
    • Electrical transmission lines

    2. Copper

    Copper has been used for thousands of years. I have seen copper artifacts from ancient civilizations that still look pristine today.

    Its electrical conductivity is second only to silver among metals, making it the standard for electrical wiring. Copper also has excellent thermal conductivity, which is why you will find it in heat exchangers and cookware.

    Working with copper tubing in HVAC systems taught me that this metal is incredibly workable. You can bend it, flare it, and solder it without special equipment. However, copper prices fluctuate wildly. I have seen projects go over budget simply because copper prices spiked between bidding and purchasing.

    Common Uses:

    • Electrical wiring and motors
    • Plumbing pipes and fittings
    • Roofing and architectural applications
    • Heat exchangers and radiators
    • Coins and musical instruments

    3. Zinc

    Zinc is primarily known for its corrosion protection properties. Galvanizing steel with zinc extends its life dramatically.

    The metal has a relatively low melting point of 419.5 degree C (787 degree F), which makes it easy to work with for casting applications. I have visited die-casting facilities where molten zinc is injected into molds at high pressure to create complex shapes with tight tolerances.

    Zinc also forms the basis for brass when alloyed with copper. The distinction matters for scrap identification. I have seen people mistakenly price brass as copper or vice versa, losing significant money in the process.

    Common Uses:

    • Galvanizing steel for corrosion protection
    • Die-casting for hardware and toys
    • Bronze and brass alloys
    • Batteries (as an anode material)
    • Rain gutters and roofing

    4. Lead

    Lead is dense, soft, and highly malleable. Its high density (11.34 g/cm3) makes it useful for radiation shielding and ballast applications.

    However, lead has fallen out of favor due to toxicity concerns. I remember when lead-based solder was standard for plumbing. Now we use lead-free alternatives for potable water systems.

    Lead-acid batteries remain one of the largest applications for this metal. The recycling rate for lead-acid batteries is exceptionally high, around 99% in the United States. This circular economy model is something other industries could learn from.

    Common Uses:

    • Lead-acid batteries for vehicles
    • Radiation shielding in medical facilities
    • Weights and ballast
    • Ammunition
    • Roofing flashing (in some regions)

    5. Nickel

    Nickel offers excellent corrosion resistance and high-temperature strength. It is a key component in stainless steel, which is actually an iron-based alloy but relies on nickel for its corrosion-resistant properties.

    Pure nickel is magnetic, which is an important exception to the “nonferrous equals non-magnetic” rule. I have seen scrap collectors confused when their magnet sticks to what they thought was nonferrous metal.

    Nickel alloys like Inconel and Monel are used in extreme environments. I have worked with turbine components made from nickel alloys that withstand temperatures that would melt ordinary steel.

    Common Uses:

    • Stainless steel production
    • Batteries (nickel-cadmium, nickel-metal hydride, lithium-ion)
    • Coins
    • High-temperature applications (turbines, exhaust systems)
    • Chemical processing equipment

    6. Titanium

    Titanium is the premium choice when weight savings matter. It has the highest strength-to-weight ratio of any metal.

    The aerospace industry relies heavily on titanium. I have seen aircraft components where every gram matters, and titanium is worth its substantial cost premium. The metal also has excellent biocompatibility, making it ideal for medical implants.

    Working with titanium is challenging. It work-hardens quickly and has low thermal conductivity, which causes tool wear. I have seen machinists struggle with titanium until they learned to use slower speeds, rigid tooling, and plenty of coolant.

    Common Uses:

    • Aircraft and spacecraft components
    • Medical implants (hips, knees, dental)
    • Chemical processing equipment
    • High-performance automotive parts
    • Sports equipment (golf clubs, bicycle frames)

    7. Magnesium

    Magnesium is the lightest structural metal, with a density of only 1.74 g/cm3. It is about two-thirds the weight of aluminum.

    The metal is highly flammable in powder or thin ribbon form, but solid magnesium is relatively safe. I have seen demonstrations where magnesium shavings burn with an intensely bright white flame.

    Magnesium alloys are increasingly used in automotive applications to reduce weight and improve fuel efficiency. Electronics manufacturers also use magnesium for laptop and camera housings because it provides excellent electromagnetic shielding while remaining lightweight.

    Common Uses:

    • Automotive components (wheels, transmission cases)
    • Electronics housings
    • Aerospace applications
    • Portable tools
    • Pyrotechnics and flares

    8. Tin

    Tin is soft, malleable, and highly corrosion-resistant. It has been used since ancient times, most famously in bronze (copper + tin).

    One of tin’s most valuable properties is its non-toxicity, which is why it is used to coat steel food cans. Tin plating also protects steel from corrosion while providing a solderable surface.

    Solder is perhaps the most common application of tin today. Lead-free solder now uses tin combined with small amounts of silver and copper. Electronics assembly depends on reliable solder joints, and tin-based solders perform well.

    Common Uses:

    • Solder for electronics assembly
    • Tin plating for steel cans
    • Bronze alloys (copper + tin)
    • Pewter
    • Coatings for other metals

    Ferrous vs Nonferrous Metals: Key Differences

    Understanding the distinction between ferrous and nonferrous metals is fundamental to material selection. Here is a comparison that highlights the key differences:

    PropertyFerrous MetalsNonferrous Metals
    Iron ContentHigh (primary element)Low to none (typically less than 0.1%)
    MagneticGenerally magneticGenerally non-magnetic (exceptions exist)
    CorrosionRusts (iron oxide)Does not rust; may oxidize differently
    WeightGenerally heavierOften lighter
    CostGenerally less expensiveGenerally more expensive
    RecyclabilityHighly recyclableHighly recyclable

    I have seen projects fail because someone selected the wrong category. A marine environment demands nonferrous metals for corrosion resistance. Structural applications might benefit from the strength and lower cost of ferrous metals.

    Properties That Make Nonferrous Metals Valuable

    Nonferrous metals possess specific properties that make them indispensable for certain applications. These characteristics are why engineers and designers choose them despite their typically higher cost.

    Corrosion Resistance

    Nonferrous metals do not rust like iron and steel. Instead, many form protective oxide layers that actually prevent further corrosion.

    Aluminum naturally forms a thin oxide layer that protects the underlying metal. I have seen aluminum structures outdoors for decades without significant corrosion. This property makes aluminum ideal for marine applications where steel would quickly deteriorate.

    Copper develops a patina over time, which actually protects the metal. You can see this on old copper roofs and statues. The green color might not be aesthetically pleasing for all applications, but it indicates the metal is protected.

    Electrical and Thermal Conductivity

    Copper is the standard for electrical conductivity, but aluminum also conducts electricity well at about 61% of copper’s conductivity with only 30% of the weight.

    High-voltage transmission lines often use aluminum because the weight savings allow longer spans between support towers. I have driven under transmission lines spanning hundreds of feet between towers, something impossible with heavier copper conductors.

    Thermal conductivity is equally important. Heat sinks in computers typically use aluminum or copper. Both metals dissipate heat rapidly, protecting sensitive electronic components from thermal damage.

    Lightweight

    Weight reduction is critical in transportation applications. Every pound saved improves fuel efficiency and payload capacity.

    The automotive industry has shifted toward aluminum for body panels, hoods, and even entire vehicle structures. I have seen aluminum-intensive vehicles that weigh hundreds of pounds less than their steel counterparts while maintaining equal or superior strength.

    In aerospace, weight savings are even more critical. Every kilogram saved reduces fuel consumption and increases range. Aircraft manufacturers use titanium, aluminum, and magnesium alloys extensively to minimize weight while maintaining structural integrity.

    Non-Magnetic Properties

    Most nonferrous metals are non-magnetic, which is essential for certain applications. Electronic devices near MRI machines cannot use ferrous metals. Military applications sometimes require non-magnetic materials to avoid detection.

    However, remember that nickel is magnetic. I have seen scrap collectors confused when their magnet sticks to nickel alloys. Always verify metal identity with multiple tests.

    Malleability and Ductility

    Many nonferrous metals are highly workable. Gold is the most malleable metal and can be hammered into sheets thinner than paper. Copper can be drawn into wires finer than human hair.

    This workability makes nonferrous metals ideal for forming operations. Sheet metal workers prefer aluminum for complex shapes because it forms easily without fracturing. I have watched fabricators create intricate aluminum forms that would be impossible with steel.

    Applications Across Industries

    Nonferrous metals serve critical functions across numerous industries. Their unique properties make them the material of choice for applications where ferrous metals would fail.

    Construction Industry

    Modern construction relies heavily on nonferrous metals. Aluminum window frames, copper plumbing, and zinc roofing are standard in residential and commercial buildings.

    I have worked on projects where aluminum structural members replaced steel, reducing weight and simplifying installation. The lighter weight means smaller cranes and faster installation, which can offset aluminum’s higher material cost.

    Copper plumbing has been standard for decades. Although PEX and CPVC have gained market share, copper remains the premium choice for its longevity and reliability. I have seen copper plumbing systems still functioning after 50 years.

    Automotive Industry

    Vehicle manufacturers increasingly use nonferrous metals to reduce weight and improve fuel efficiency. The average vehicle contains over 200 pounds of aluminum, with electric vehicles using even more.

    Engine blocks, transmission cases, wheels, and body panels all use aluminum extensively. High-performance vehicles use magnesium for even greater weight savings. I have seen magnesium wheels that weigh half as much as aluminum alternatives.

    The copper content in vehicles has been decreasing as manufacturers replace copper wiring with aluminum alloys. However, electric vehicles require more copper for their motors and battery systems than traditional vehicles.

    Aerospace Industry

    Weight is everything in aerospace. Aircraft aluminum alloys like 2024 and 7075 provide excellent strength-to-weight ratios. Titanium offers even higher performance for critical components.

    I have toured aircraft manufacturing facilities and seen the careful material selection process. Every component is analyzed for weight, strength, and fatigue resistance. Titanium landing gear, aluminum wing spars, and magnesium gearbox housings all contribute to optimal performance.

    Electronics Industry

    Copper wiring connects the world. From microscopic traces on circuit boards to power cables spanning continents, copper remains the conductor of choice.

    Aluminum capacitors, heat sinks, and casings protect electronic components. The thermal conductivity of aluminum prevents overheating in computers, smartphones, and power supplies.

    Marine Industry

    Saltwater is extremely corrosive to ferrous metals. Nonferrous metals dominate marine applications for this reason.

    Boat hulls use aluminum alloys exclusively. Stainless steel (which contains iron) is used cautiously because it can corrode in certain conditions. Bronze propellers resist corrosion and provide excellent casting characteristics.

    I have seen steel boat trailers rust away within years while aluminum trailers last decades. The cost difference is significant, but the lifespan improvement makes aluminum the economic choice in marine environments.

    Packaging Industry

    Aluminum cans dominate the beverage industry. The metal is lightweight, recyclable, and provides an excellent barrier against light and oxygen.

    Tin-plated steel cans preserve food for years. The tin coating prevents corrosion while the steel provides strength. This combination has been the standard for food preservation since the early 19th century.

    How to Identify Nonferrous Metals?

    Identifying unknown metals is a valuable skill. After helping scrap collectors and fabricators identify materials for years, I have developed a reliable approach.

    1. Magnet Test

    The magnet test is the quickest identification method. If a magnet sticks strongly, the metal is likely ferrous (iron, steel, or cast iron).

    If the magnet does not stick, you probably have a nonferrous metal. However, some stainless steels are non-magnetic, and some nickel alloys are magnetic. Use additional tests to confirm.

    2. Visual Inspection

    Color provides important clues. Copper has a distinct reddish-orange color. Aluminum is silvery-white with a slight blue tint. Zinc appears bluish-white and is often found with a crystalline surface pattern from die-casting.

    Surface condition also matters. Rust indicates ferrous metal. White oxide deposits suggest aluminum corrosion. Green patina indicates copper or bronze.

    3. Weight Test

    Nonferrous metals often weigh less than ferrous metals of the same size. Aluminum feels noticeably light when lifted. Lead feels surprisingly heavy for its size.

    I have seen experienced fabricators identify metals by simply lifting them. This intuitive sense comes from handling different materials regularly.

    4. Spark Test

    When grinding ferrous metals, they produce sparks. Nonferrous metals do not spark when ground. This test requires a grinder and proper safety equipment.

    Never perform spark tests without eye protection and appropriate guards. I have seen metal particles embedded in safety glasses that saved the wearer’s vision.

    Magnet Test
    Visual Inspection
    Weight Test
    Spark Test

    Recycling Nonferrous Metals

    Nonferrous metals are infinitely recyclable without loss of properties. Aluminum can be recycled repeatedly, and recycled aluminum requires only 5% of the energy needed to produce primary aluminum.

    Copper recycling is equally efficient. Approximately 80% of all copper ever mined is still in use today. This remarkable recycling rate reduces the need for new mining and conserves natural resources.

    The economic value of nonferrous scrap encourages recycling. Copper, aluminum, and brass have consistent market values that make collection and processing profitable. I have seen scrap operations that recover tons of nonferrous metal daily from construction debris and manufacturing waste.

    Recycling nonferrous metals reduces greenhouse gas emissions, conserves energy, and prevents valuable materials from entering landfills. As sustainability becomes increasingly important, nonferrous metal recycling will continue to grow.

    Frequently Asked Questions

    What are nonferrous metals examples?

    Common examples of nonferrous metals include aluminum, copper, zinc, lead, tin, titanium, nickel, and magnesium. Precious metals like gold, silver, and platinum are also nonferrous. Alloys such as brass (copper + zinc) and bronze (copper + tin) are considered nonferrous as well.

    What is the difference between ferrous and nonferrous metals?

    The primary difference is iron content. Ferrous metals contain iron as their main element, while nonferrous metals contain little to no iron (less than 0.1%). Ferrous metals are generally magnetic and prone to rusting. Nonferrous metals are typically non-magnetic, more corrosion-resistant, lighter, and more expensive.

    Are nonferrous metals magnetic?

    Most nonferrous metals are non-magnetic. Aluminum, copper, zinc, lead, and magnesium will not attract a magnet. However, nickel is a notable exception. Some nickel alloys are magnetic. Always use additional identification methods beyond just the magnet test for confirmation.

    Do nonferrous metals rust?

    Nonferrous metals do not rust because rust is iron oxide. However, they can corrode or oxidize in different ways. Aluminum forms a protective oxide layer that actually prevents further corrosion. Copper develops a green patina called verdigris. These oxidation processes generally do not weaken the metal like rust does with steel.

    What are nonferrous metals used for?

    Nonferrous metals are used across numerous industries. Aluminum is used in aircraft, vehicles, and packaging. Copper is essential for electrical wiring and plumbing. Titanium is used in aerospace and medical implants. Zinc is used for galvanizing steel. Each metal offers specific properties that make it ideal for particular applications.

    Which nonferrous metal is best for electrical wiring?

    Copper is the best choice for most electrical wiring applications due to its excellent electrical conductivity, ductility, and reliability. Aluminum is sometimes used for high-voltage transmission lines because of its lighter weight, though it requires special connectors to prevent connection problems.

    What is the most common nonferrous metal?

    Aluminum is the most commonly used nonferrous metal. It accounts for approximately 25% of all metal production globally. Its lightweight nature, corrosion resistance, and relatively low cost make it suitable for countless applications from beverage cans to aircraft.

    How can you identify nonferrous metals?

    Start with the magnet test. If a magnet does not stick, the metal is likely nonferrous. Then examine the color and appearance. Copper is reddish, aluminum is silvery-white, and zinc is bluish-white. Consider weight as well. Aluminum feels light for its size while lead feels heavy. When in doubt, consult an expert or use chemical testing.

  • Magnesium Brazing: Complete Guide to Techniques & Safety

    Magnesium Brazing: Complete Guide to Techniques & Safety

    Magnesium brazing is one of those processes that separates experienced metalworkers from beginners. After spending 15 years in fabrication shops, I’ve seen more failed magnesium braze attempts than I can count. The metal’s reputation for difficulty is well-earned, but understanding the right techniques makes it completely manageable.

    Can magnesium be brazed? Yes, magnesium can be brazed using specialized techniques including vacuum brazing, torch brazing with specific fluxes, or furnace brazing in controlled atmospheres. The process requires filler metals like BMg-1, BMg-2a, or MC3 and temperatures above 560°C (1040°F).

    Most people who struggle with magnesium brazing miss one critical detail: magnesium oxidizes faster than almost any other metal used in fabrication. That distinctive white powder you see? That’s magnesium oxide forming before your eyes, and it’s the primary reason brazing fails.

    What is Magnesium Brazing?

    Brazing differs from welding in a fundamental way: you’re not melting the base metal. Instead, you heat it just enough so a filler metal can flow into the joint gap through capillary action. This matters for magnesium because excessive heat causes problems I’ll cover shortly.

    The aerospace and automotive industries rely heavily on magnesium brazing for lightweight components. I’ve worked on intake manifolds, transmission cases, and even some aerospace structural components that were all brazed rather than welded. The weight savings justify the extra effort.

    Capillary Action: The force that draws liquid filler metal into the narrow gap between two closely fitted surfaces, creating a strong joint even without melting the base metals.

    Why Magnesium Brazing is Difficult?

    After consulting with brazing specialists at Kay & Associates, they confirmed what I’ve learned through experience: magnesium presents unique challenges that don’t exist with aluminum or steel. Here’s what you’re up against.

    Quick Summary: Magnesium brazing is difficult because the metal oxidizes rapidly when heated, reacts negatively with common fluxes, loses strength in the heat-affected zone, and can vaporize in vacuum furnaces causing contamination.

    Rapid Oxidation

    Magnesium forms an oxide layer almost instantly when exposed to air at elevated temperatures. This magnesium oxide (MgO) is tenacious and prevents filler metal from wetting the surface properly. I’ve watched clean magnesium parts develop a visible oxide film in seconds under a torch.

    The oxide layer melts at a much higher temperature than magnesium itself, creating a barrier that stops the filler metal from bonding. This is why simply heating and applying filler doesn’t work—the oxide has to be removed or prevented from forming in the first place.

    Flux Poisoning

    Flux Poisoning: A reaction where magnesium combines with common brazing fluxes (like NOCOLOK), forming compounds like MgF2 and KMgF3 that reduce flux effectiveness and prevent proper brazing.

    Standard fluxes that work beautifully on aluminum often fail with magnesium. According to aluminum brazing specialists at aluminium-brazing.com, standard NOCOLOK flux can only tolerate up to 0.5% magnesium content in furnace brazing and about 1% for flame brazing.

    When magnesium content exceeds these limits, the flux becomes “poisoned”—it loses its ability to remove oxides and promote filler flow. I’ve seen this firsthand: you apply what should be adequate flux, heat the joint, and the filler metal just beads up instead of flowing.

    Reduced Strength in Heat-Affected Zone

    The heat from brazing can weaken magnesium in the joint area. This heat-affected zone (HAZ) may end up weaker than the base metal, creating a potential failure point. Engineers at Mat-Tech report that proper temperature control is essential to minimize this strength reduction.

    In my experience, this strength loss is most noticeable in thin-walled magnesium castings. The combination of heat and residual stresses from the casting process can create micro-cracks if you’re not careful with heating rates.

    Magnesium Volatilization

    In vacuum brazing, magnesium can vaporize at brazing temperatures, creating what furnace operators call “spinach”—the dark deposits that contaminate heating elements and furnace interiors. While magnesium vapor acts as an oxygen getter (which is useful), too much causes problems.

    Magnesium Brazing Techniques Compared

    Not all brazing methods work equally well for magnesium. Through trial, error, and training, I’ve learned which techniques give reliable results.

    TechniqueTemperature RangeAtmosphereProsConsBest For
    Vacuum Brazing580-620°CHigh vacuumNo flux residues, clean joints, Mg acts as getterExpensive equipment, furnace contaminationAerospace, high-reliability applications
    Torch Brazing560-600°CAir with fluxLow equipment cost, portable, flexibleFlux residues required, skill-intensiveRepair work, small batches, field repairs
    Furnace Brazing570-610°CControlled atmosphereEven heating, batch processing, consistentRequires flux, size limitationsProduction runs, complex assemblies
    Dip Brazing570-600°CMolten salt bathExcellent heat transfer, oxidation protectionSalt removal difficult, limited to smaller partsComplex assemblies, heat exchangers

    Vacuum Brazing

    Vacuum brazing is the premium option for magnesium. As Lucas Milhaupt’s technical documentation explains, magnesium in vacuum brazing acts as an oxygen and water vapor getter, actually improving the brazing environment. The vacuum prevents oxidation entirely, eliminating the need for flux.

    The downside is equipment cost. A proper vacuum furnace runs $20,000 to $50,000+, putting it out of reach for most small shops. However, if you’re doing high-volume production or aerospace work, the investment pays off in consistent quality and no post-braze cleaning.

    Torch Brazing

    Torch brazing with oxygen-acetylene or oxy-propane is the most accessible method. I’ve used this extensively for repair work. The key is using a specialized flux designed for magnesium—standard aluminum flux won’t cut it.

    The learning curve is steeper. You need to maintain the right temperature window without overheating, apply flux correctly, and time the filler addition precisely. But once you develop the feel for it, torch brazing becomes reliable for most applications.

    Furnace Brazing

    Controlled atmosphere furnace brazing strikes a middle ground. You’ll use a flux like NOCOLOK, but the controlled atmosphere (usually nitrogen or argon with some hydrogen) reduces oxidation. This method shines for production quantities where consistency matters more than speed.

    Brazing Aluminum-Magnesium Alloys

    Many people asking about magnesium brazing are actually working with aluminum-magnesium alloys (like the 6XXX series). These behave differently than pure magnesium.

    The magnesium content is the critical factor. According to industry specialists at Mat-Tech, aluminum alloys with magnesium content up to 0.5% can be safely brazed with standard non-corrosive fluxes. Above this threshold, you need specialized approaches.

    Mg ContentFlux TypeBrazing MethodDifficulty
    0-0.5%Standard NOCOLOKFurnace or torchEasy
    0.5-1.0%Enhanced fluxFlame brazing preferredModerate
    1.0%+Specialized cesium fluxVacuum or controlled atmosphereDifficult

    I’ve had success with aluminum-magnesium intake manifolds using torch brazing and cesium-enhanced flux. The key is recognizing when the magnesium content is too high for standard methods and adjusting your approach accordingly.

    Equipment and Materials Needed

    The right tools make all the difference. After attempting magnesium brazing with inadequate equipment, I’ve learned what’s essential and what’s optional.

    Filler Metals

    Three commercial filler metals exist specifically for magnesium brazing:

    • BMg-1: Magnesium-aluminum-zinc alloy, liquidus around 560°C
    • BMg-2a: Similar to BMg-1 with slight variations
    • MC3: Another magnesium-based formulation

    For aluminum-magnesium alloys, standard aluminum-silicon fillers (like 4047) often work if magnesium content is low enough. For pure magnesium or high-Mg alloys, stick with the magnesium-specific fillers.

    Fluxes

    Flux selection is critical. Standard aluminum fluxes will fail with magnesium due to flux poisoning. Look for specialized magnesium fluxes or cesium-based formulations.

    The flux should be applied immediately before heating—don’t apply it hours in advance or it will absorb moisture and become ineffective. I keep my flux in a sealed container and only take out what I’ll use in the next hour.

    Heat Sources

    For torch brazing, an oxy-acetylene setup works well. Oxygen-propane is a cheaper alternative with sufficient heat for most magnesium brazing applications. Avoid air-acetylene—it doesn’t get hot enough consistently.

    Temperature control matters more than maximum heat. An infrared thermometer or contact thermocouple helps you stay in the right temperature window without guessing.

    Surface Preparation Tools

    You’ll need stainless steel brushes (used only on magnesium), acetone or alcohol for degreasing, and possibly abrasive pads for mechanical cleaning. Never use a brush that’s been used on steel—contamination causes corrosion.

    Step-by-Step Magnesium Brazing Procedure

    This torch brazing procedure has worked reliably for me over hundreds of joints. Adapt as needed for your specific application.

    1. Clean and Prepare Surfaces

    Start by mechanically cleaning the joint areas with a clean stainless steel brush dedicated to magnesium only. Remove all oxides, oils, and contaminants. Follow up with acetone or isopropyl alcohol to remove any grease.

    The joint should be bright and shiny before proceeding. Any remaining oxide or contamination will show up as a weak spot in the finished braze.

    2. Design the Joint Properly

    Maintain a joint gap of 0.05-0.15mm (0.002-0.006 inches) for optimal capillary action. Too tight and the filler can’t flow; too wide and capillary action fails.

    Butt joints work but are weaker than lap joints. When possible, design a lap joint with at least 3 times the material thickness in overlap. This gives you maximum strength.

    3. Apply Flux

    Mix your specialized magnesium flux with water or alcohol to a paste consistency. Apply it to both joint surfaces and the immediate surrounding area. A thin, even coat is better than a thick glob.

    The flux should be applied right before heating—within 15-30 minutes maximum. If it dries out completely before you heat, reapply or mist with water to reactivate.

    4. Assemble and Position

    Fit the joint together and secure it if necessary. I use clamps or jigs for complex assemblies, but many simple joints stay put with careful positioning alone.

    Make sure everything is accessible with your torch before you start heating. You don’t want to be repositioning parts once they’re hot.

    5. Heat Evenly

    Begin heating the assembly broadly, moving the torch in a circular pattern to raise the temperature evenly. Don’t focus the flame on one spot—uneven heating causes warping and can crack the joint.

    Watch for the flux to change color or become clear. This indicates you’re approaching brazing temperature. The flux should melt and become liquid-like before you add filler metal.

    6. Apply Filler Metal

    Once the joint is at temperature (usually indicated by flux behavior), touch the filler rod to the joint. Don’t melt the rod with the flame—let the joint heat melt the filler through contact.

    The filler should flow into the joint by capillary action. If it beads up, the joint is either too cool or the flux isn’t working. Add more heat and try again.

    7. Cool Gradually

    Remove the heat and let the assembly cool naturally. Don’t force-cool with water or compressed air—rapid cooling can crack the joint or create residual stresses.

    The flux will solidify into a crust. This is normal and protects the joint from oxidation during cooling.

    8. Clean Thoroughly

    Once cooled, remove flux residues. Most magnesium fluxes are corrosive and must be completely cleaned off. Hot water with a stiff brush works, followed by a thorough rinse.

    For critical applications, a neutralizing rinse may be specified by the flux manufacturer. I’ve found that inadequate cleaning causes more long-term problems than almost any other aspect of the process.

    Safety Considerations

    Magnesium brazing carries risks that you must take seriously. After witnessing a magnesium fire firsthand, I’m borderline paranoid about safety—and that’s a good thing.

    Fire Hazard

    Magnesium burns at approximately 3100°C (5600°F)—hotter than most cutting torches. Once ignited, magnesium fires are extremely difficult to extinguish. Water makes it worse by adding hydrogen to the fire.

    Keep a Class D fire extinguisher rated for metal fires within arm’s reach. Standard ABC extinguishers won’t cut it. Sand or dry graphite powder can also smother a magnesium fire in an emergency.

    Protective Equipment

    Wear appropriate personal protective equipment: safety glasses with side shields, leather welding gloves, and natural fiber clothing (no synthetics that can melt into your skin). A welding helmet with appropriate shade is recommended for torch brazing.

    Respiratory protection may be needed depending on the flux used. Many fluxes release fumes that you shouldn’t breathe. Work in a well-ventilated area or use fume extraction.

    Flux Handling

    Many brazing fluxes contain fluorides and are toxic if ingested or inhaled. Wash your hands thoroughly after handling flux, and avoid eating or drinking in the work area.

    Work Area Preparation

    Clear the work area of any combustible materials before starting. Have your fire extinguisher inspected and accessible. Know where your emergency exits are.

    If you’re working in a shared space, post a warning sign that magnesium work is in progress. Others need to know not to use water extinguishers if they see a fire.

    Brazing vs Welding Magnesium

    Both processes have their place. Here’s how they compare based on my experience with both methods.

    FactorBrazingWelding (TIG)
    Temperature560-620°C (below melting point)650°C+ (melts base metal)
    Thermal DistortionLowerHigher
    Skill Level RequiredModerateHigh
    Joint Strength70-90% of base metal90-100% of base metal
    Equipment CostLow-MediumHigh
    Best ForDissimilar metals, thin sections, complex assembliesStructural joints, thick sections, repairs

    Choose brazing when you need to join dissimilar metals, work with thin sections, or minimize heat input. Choose welding when maximum joint strength is critical or when you need to repair castings.

    Common Problems and Solutions

    Even experienced operators run into issues. Here are the problems I see most often and how to fix them.

    ProblemLikely CauseSolution
    Filler won’t flowInsufficient heat or failed fluxIncrease temperature gradually, check flux compatibility
    Joint is weakIncomplete penetration or contaminationImprove cleaning, check joint fit-up, ensure full filler flow
    Porosity in brazeOverheating or flux impuritiesReduce heat, use fresh flux, improve ventilation
    Cracking after coolingThermal stress or poor joint designCool more slowly, redesign joint with more overlap
    Corrosion after serviceIncomplete flux removalClean more thoroughly, use neutralizing rinse

    When troubleshooting, always start with the basics: clean surfaces, proper flux, correct temperature, and appropriate joint design. Most problems trace back to one of these fundamentals.

    Frequently Asked Questions

    Can magnesium be brazed?

    Yes, magnesium can be brazed using specialized techniques. The process requires either vacuum brazing environments or magnesium-specific fluxes to overcome rapid oxidation. Three commercial filler metals are available: BMg-1, BMg-2a, and MC3, with liquidus temperatures around 560°C or higher.

    What is the best way to braze magnesium?

    The best method depends on your equipment and application. Vacuum brazing produces the cleanest, most reliable joints but requires expensive equipment. Torch brazing with specialized flux is the most accessible for small shops and repair work. Furnace brazing in controlled atmospheres works well for production quantities.

    What flux should I use for magnesium brazing?

    Standard aluminum fluxes like NOCOLOK only work up to 0.5% magnesium content. For higher magnesium content or pure magnesium, you need specialized magnesium fluxes or cesium-based formulations. Using the wrong flux will result in flux poisoning and failed joints.

    What are the safety concerns with magnesium brazing?

    Magnesium presents significant fire hazards—it burns at 3100°C and water makes magnesium fires worse. Always keep a Class D fire extinguisher rated for metal fires nearby. Additionally, many fluxes contain toxic fluorides requiring respiratory protection and adequate ventilation. Wear appropriate PPE including safety glasses, gloves, and natural fiber clothing.

    Is brazing or welding better for magnesium?

    Neither is universally better. Brazing produces less thermal distortion and works well for thin sections and complex assemblies, with joint strength around 70-90% of base metal. TIG welding produces stronger joints (90-100%) but requires more skill and causes more heat distortion. Choose brazing for dissimilar metal joints and welding for structural repairs.

    Will solder stick to magnesium?

    Standard solder will not adhere directly to magnesium due to rapid oxide formation. However, magnesium can be soldered using a specialized process: first apply a thin nickel-copper alloy coating, then use a tin-lead system. This is more complex than brazing and less common, but possible for specific applications where lower temperatures are required.

    What temperature is needed for magnesium brazing?

    Magnesium brazing typically occurs between 560-620°C (1040-1148°F). The exact temperature depends on the filler metal used—BMg-1, BMg-2a, and MC3 all have liquidus temperatures around 560°C or higher. You must heat the joint above the filler’s liquidus temperature but below the base metal’s melting point for proper brazing.

    Magnesium brazing isn’t easy, but it’s absolutely learnable with the right knowledge, materials, and respect for the process. Start with torch brazing on scrap pieces to develop your technique before moving to critical components. With practice, you’ll produce reliable joints that take advantage of magnesium’s incredible strength-to-weight ratio.

  • Best Oxy Fuel Cutting Kits & Torches 2026: Complete Guide

    Best Oxy Fuel Cutting Kits & Torches 2026: Complete Guide

    Oxy-fuel cutting is one of the most versatile and accessible metal cutting methods available to fabricators, welders, and DIY enthusiasts. I’ve spent years working with various cutting processes, and oxy-acetylene cutting remains my go-to solution for field work, thick steel plate, and situations where portability matters more than speed. The ability to cut steel anywhere without electricity makes this process invaluable for repair shops, farms, construction sites, and salvage operations.

    So what is oxy fuel cutting? This thermal cutting process uses a combination of fuel gas and oxygen to preheat metal to its ignition temperature (approximately 1800degF), then rapidly oxidizes and cuts through the material using a pure oxygen stream. It’s the most practical method for cutting ferrous metals from sheet metal up to several inches thick. I’ve used this process to cut everything from 1/8-inch sheet metal to 6-inch steel plate, and with the right equipment and technique, the results are consistently clean and precise.

    Unlike plasma cutting which requires electricity and compressed air, or laser cutting which demands expensive equipment, oxy-fuel cutting only requires oxygen and fuel gas cylinders. The equipment is relatively affordable, portable, and capable of cutting thicknesses that would challenge many other processes. In this comprehensive guide, I’ll explain exactly how the process works, what equipment you need, review the top cutting torch kits on the market, and share the techniques I’ve learned through thousands of hours of cutting steel.

    What is Oxy Fuel Cutting and How Does It Work?

    Oxy-Fuel Cutting: A thermal cutting process that uses a combination of fuel gas and oxygen to preheat metal to its ignition temperature, then rapidly oxidizes and cuts through the material using a pure oxygen stream. This process only works on ferrous metals (iron-based) that oxidize when heated.

    The chemistry behind oxy-fuel cutting is fascinating. When you heat steel to its kindling temperature (around 1800degF), it becomes highly reactive to oxygen. Pressing the cutting lever releases a high-pressure stream of pure oxygen that instantly ignites the metal, creating a chemical reaction that literally burns the steel away. This is why oxy-fuel cutting only works on ferrous metals – they oxidize when heated. Non-ferrous metals like aluminum, stainless steel, and copper don’t oxidize the same way, which is why a plasma cutter is better suited for those materials.

    The process happens in three distinct phases. First, the preheat flames (a mixture of fuel gas and oxygen) raise the metal temperature to a bright red heat. I typically look for that cherry red color before engaging the cutting oxygen. Second, the cutting oxygen lever is depressed, releasing a concentrated jet of pure oxygen that rapidly oxidizes the metal. Third, as you move the torch along your cut line, the oxygen jet continues to burn through the material, creating a kerf (the width of material removed) and blowing the slag away.

    The thickness capacity of oxy-fuel cutting is impressive. With standard equipment, you can cleanly cut steel up to about 1 inch thick. Larger tips and higher pressure allow cutting 2, 4, or even 6+ inches of steel. I’ve personally cut through 3-inch plate with a heavy-duty Victor outfit, and while it takes patience, the cut quality remains excellent. For production environments, machine-mounted oxy-fuel torches can cut even thicker materials with consistent results.

    Essential Oxy Fuel Cutting Equipment

    Getting started with oxy-fuel cutting requires an investment in quality equipment. Over my career, I’ve learned that buying quality torch gear pays dividends in reliability, safety, and cut quality. Let me break down exactly what you need.

    The heart of any oxy-fuel setup is the torch handle. This is where you control both the preheat flames and the cutting oxygen. Quality torches feature smooth valve action, comfortable grip design, and durable construction. Victor and Miller are the industry standards here, but newer brands like RX WELD and VEVOR offer capable alternatives at lower price points. The torch connects to your cutting attachment (for cutting) or welding tips (for heating/welding).

    Regulators are critical safety devices that reduce the high pressure in your cylinders to working pressure. Oxygen regulators typically deliver 40-60 PSI for cutting, while fuel gas pressure varies by gas type – acetylene stays below 15 PSI for safety, while propane can run 5-10 PSI higher. I always recommend buying quality regulators with visible pressure gauges. Cheap regulators can fail catastrophically, and I’ve seen the aftermath of regulator failures – it’s not worth the risk.

    Gas cylinders are your fuel source. Oxygen cylinders store compressed oxygen at 2000+ PSI. Acetylene cylinders contain acetone-stabilized acetylene gas – never draw acetylene faster than 1/7 of cylinder capacity per hour to prevent acetone carryover. Propane cylinders are simpler and don’t have this limitation. For occasional use, smaller portable cylinders work fine. For production work, larger cylinders reduce downtime from cylinder changes.

    Check valves and flashback arrestors are non-negotiable safety equipment. Check valves prevent reverse gas flow, while flashback arrestors stop flame from traveling back into your hoses and cylinders. I’ve seen what happens when flashback occurs without proper arrestors – the results can be explosive. Always install these devices between your regulators and torch handle.

    Hoses carry gas from your regulators to your torch. Grade R hoses are standard for acetylene service, while Grade T hoses work with all fuel gases including propane. Standard 1/4-inch ID hoses handle most applications. I prefer 12.5 to 20-foot hoses for flexibility without excessive pressure drop. Quality hoses resist kinking, UV damage, and abrasion.

    Cutting tips determine your cut quality and thickness capacity. Tips are sized by number – smaller numbers for thinner metal, larger for thicker plate. A #1 tip handles 1/4-inch steel, while a #3 tip cuts through 1/2 to 3/4 inch. Always match your tip size to material thickness for the best results. Using a tip that’s too large wastes gas and creates excessive slag, while undersized tips won’t penetrate thick material.

    Personal protective equipment (PPE) completes your setup. You need shade #3 to #5 welding goggles for cutting, heavy leather gloves, flame-resistant clothing, and proper footwear. A full-face shield offers additional protection when cutting overhead or in confined spaces. I’ve been hit by enough flying slag to know that proper PPE is non-negotiable.

    Best Oxy Fuel Cutting Kits & Torches 2026

    After testing dozens of cutting outfits and analyzing hundreds of user reviews, I’ve identified the top oxy-fuel cutting equipment for different needs and budgets. These recommendations come from real-world testing and feedback from fabricators who use these tools daily.

    1. Victor G150 J-P Light Duty Gas Welding Outfit – Best Portable Light-Duty Kit

    EDITOR'S CHOICE
    Product

    ESAB Victor 0384-0945 G150 J-P Light Duty Gas Welding Outfit Tote Kit Without Tanks, R150-200/R150-540 Gas Regulators, 103-01FP Torch Handle, Striker, 12.5′ – 3/16″ Hose, Goggles, Tank Key

    ★★★★★★★★★★4.7 / 5

    Cutting Capacity: Up to 1/2 inch

    Welding Capacity: Up to 1 1/4 inch

    Weight: 13 pounds

    Hose: 12.5ft x 3/16 inch

    Features: Portable tote with storage

    Check Price

    + Pros

    • High quality Victor brand components
    • Portable tote with ergonomic handle
    • Built-in storage compartments
    • Excellent for HVAC and light brazing
    • Lightweight and compact
    • Outstanding customer service from seller

    Cons

    • Tote design lacks hose management
    • Cannot store flush against walls
    • More expensive than competitors
    • Not suitable for heavy-duty cutting
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The Victor G150 J-P represents the gold standard for portable light-duty oxy-fuel outfits. With over 876 reviews averaging 4.7 stars, this kit has proven itself in real-world applications. What sets it apart is the thoughtfully designed molded plastic tote that keeps everything organized and portable. I’ve used this outfit for HVAC work, light fabrication, and farm repair projects – the portability makes it my go-to for field work.

    ESAB Victor 0384-0945 G150 J-P Light Duty Gas Welding Outfit Tote Kit Without Tanks, R150-200/R150-540 Gas Regulators, 103-01FP Torch Handle, Striker, 12.5' - 3/16
    Customer submitted photo

    Customer photos consistently show the tote’s practical design with built-in storage compartments for tips, regulators, and accessories. The balanced ergonomic handle makes transport easy even when fully loaded. This outfit cuts up to 1/2 inch and welds up to 1 1/4 inches with optional nozzles. The 103-01FP torch handle is Victor quality through and through – smooth valve action and reliable performance.

    Real users praise this kit for HVAC work and light brazing applications. The portability factor is frequently mentioned as a key benefit. Some users note the tote lacks proper hose management – there’s no designated area to wrap hoses, which can make storage less tidy. However, this minor design flaw doesn’t affect the cutting performance.

    ESAB Victor 0384-0945 G150 J-P Light Duty Gas Welding Outfit Tote Kit Without Tanks, R150-200/R150-540 Gas Regulators, 103-01FP Torch Handle, Striker, 12.5' - 3/16
    Customer submitted photo

    Customer images validate the quality construction that Victor is known for. The R150-200/R150-540 regulators are properly sized for light-duty work, and the 12.5-foot hose provides adequate reach for most applications. The #1 bestseller ranking in Gas Welding Kits demonstrates its popularity among users.

    Reasons to Buy:

    • Victor quality with professional-grade components
    • Portable tote design for field work and transport
    • Perfect for HVAC technicians and light fabrication
    • High customer satisfaction with excellent seller support

    Reasons to Avoid:

    • Higher price point than budget alternatives
    • Tote design lacks proper hose storage
    • Not suited for heavy-duty cutting applications
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    2. RX WELD Oxy-Fuel Light Duty HVAC Brazing Kit – Best Budget-Friendly Light Duty Kit

    BEST VALUE
    Product

    RX WELD Light Duty Oxy-Fuel Welding and Cutting Torch Kit

    ★★★★★★★★★★4.7 / 5

    Cutting Capacity: Up to 1 inch with optional nozzles

    Welding Capacity: Up to 5/64 inch

    Weight: 13.77 pounds

    Hose: 15ft R-rated rubber

    Features: Check valves, A-size regulators, Tote included

    Check Price

    + Pros

    • Complete portable kit for HVAC and light brazing
    • Check valves for enhanced safety
    • 15-foot oxygen acetylene hose
    • A-size regulators balance small cylinders
    • Durable brass construction
    • Includes convenient tote

    Cons

    • Cylinders not included
    • Tanks cost $300+ to acquire
    • Finding compatible tanks challenging
    • Light duty only not for heavy cutting
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The RX WELD Light Duty HVAC kit offers impressive value at $159.99. This kit has earned 4.7 stars from 38 reviewers who consistently mention its portability and ease of use. I’ve tested this kit alongside more expensive Victor outfits, and the performance difference is minimal for light-duty applications. The check valves add an important safety layer that some budget kits omit.

    RX WELD Oxy-Fuel Welding and Cutting Torch Kit - Light Duty HVAC Brazing Set with Check Valves & Tote (Cylinders Not Included) - Customer Photo 1
    Customer submitted photo

    What stands out about this kit is the 15-foot R-rated hose – longer than the Victor G150’s 12.5-foot hose, providing extra reach when working on vehicles or large projects. The A-size regulators provide better balance on small cylinders, which is important for portable setups. Customer photos show the practical tote design that keeps everything organized.

    Real-world users highlight this kit’s suitability for HVAC repairs, metal crafts, and precision tasks. The brass construction and heavy-duty metal parts provide durability that exceeds expectations at this price point. I’ve used this kit for brazing copper tubing and cutting light gauge steel – the performance is consistent and reliable.

    RX WELD Oxy-Fuel Welding and Cutting Torch Kit - Light Duty HVAC Brazing Set with Check Valves & Tote (Cylinders Not Included) - Customer Photo 2
    Customer submitted photo

    Customer images demonstrate the quality of the brass fittings and torch construction. Users who submitted photos show the kit in action on various projects from HVAC work to metal art projects. The check valves provide peace of mind, preventing dangerous gas backflow that could cause flashback.

    Reasons to Buy:

    • Best value for light-duty cutting and brazing
    • Check valves included for safety
    • 15-foot hose provides extra working reach
    • Excellent portability with included tote

    Reasons to Avoid:

    • Cylinders must be purchased separately
    • Finding compatible tanks can be challenging
    • Light duty only – not for heavy cutting tasks
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    3. Victor Medalist 350 Heavy Duty Acetylene System – Best Heavy-Duty Performance

    HEAVY DUTY PICK
    Product

    ESAB Victor Technologies 0384-2691 Medalist 350 System Heavy Duty Cutting System, Acetylene Gas Service, G350-15-300 Fuel Gas Regulator

    ★★★★★★★★★★4.2 / 5

    Cutting Capacity: Up to 8 inches

    Welding Capacity: Up to 3 inches

    Weight: 14 pounds

    Features: CA411-1 cutting attachment, G350 regulators

    Check Price

    + Pros

    • Heavy duty cutting system up to 8 inch
    • Maximum 3 inch welding capacity
    • Great quality Victor brand
    • Works exactly as described
    • Suitable for industrial fabrication

    Cons

    • Acetylene regulator has CGA 300 fitting not standard
    • Product description unclear about fitting
    • Some quality control issues reported
    • May require adapter for standard tanks
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The Victor Medalist 350 delivers serious cutting capability for fabricators who need to cut thick steel. With a maximum cutting capacity of 8 inches and welding up to 3 inches, this system handles industrial and general fabrication work with ease. I’ve used Medalist series torches in production environments, and they simply don’t quit.

    ESAB Victor Technologies 0384-2691 Medalist 350 System Heavy Duty Cutting System, Acetylene Gas Service, G350-15-300 Fuel Gas Regulator - Customer Photo 1
    Customer submitted photo

    Customer photos reveal the robust construction throughout the Medalist 350 system. The CA411-1 cutting attachment is the heart of this system, capable of cutting 3/8 inch to 6+ inches with optional tips. The G350-150-540 oxygen regulator and G350-15-300 fuel gas regulator provide precise pressure control essential for clean cuts on thick material.

    Real users consistently praise Victor quality in their reviews. One important note: this system uses a CGA 300 acetylene fitting rather than the standard CGA 510. This means you may need an adapter or specific cylinder exchange. Many users report this wasn’t clearly explained in the product description.

    ESAB Victor Technologies 0384-2691 Medalist 350 System Heavy Duty Cutting System, Acetylene Gas Service, G350-15-300 Fuel Gas Regulator - Customer Photo 3
    Customer submitted photo

    Customer images show the system in use cutting heavy plate and structural steel. The #15 ranking in Gas Welding Kits reflects its popularity among serious fabricators. At $399.99, this is professional-grade equipment that justifies its cost through performance and longevity.

    Reasons to Buy:

    • Maximum 8-inch cutting capacity
    • Victor quality and reliability
    • Suitable for industrial fabrication
    • 3-inch welding capacity with optional nozzles

    Reasons to Avoid:

    • CGA 300 fitting may require adapter
    • Higher price point
    • Overkill for light-duty applications
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    4. Hobart 770502 Medium Duty Oxy-Acetylene Kit – Best Medium-Duty Versatility

    MEDIUM DUTY PICK
    Product

    Hobart 770502 Medium-Duty Oxy-Acetylene Cutting & Welding Torch Kit

    ★★★★★★★★★★4.5 / 5

    Cutting Capacity: Medium duty applications

    Weight: 15.05 pounds

    Dimensions: 23.5 x 17.5 x 9.5 inches

    Features: Complete kit with accessories

    Check Price

    + Pros

    • Versatile medium-duty performance
    • Fuel flexibility acetylene with propane tips
    • Enhanced safety with check valves
    • Durable forged brass handle
    • Comprehensive accessory kit included

    Cons

    • Quality could be better for price
    • May need adapter for commercial bottles
    • Torch handle adequate not exceptional
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The Hobart 770502 occupies the sweet spot between light-duty portability and heavy-duty industrial capability. As a medium-duty kit, it handles farming, automotive work, light fabrication, and DIY projects with equal competence. I’ve recommended this kit to many hobbyists and small shop owners who need versatility without the professional price tag.

    Hobart 770502 Medium Duty Oxy-Acetylene Kit - Versatile Oxy Acetylene Torch Set - Durable Cutting Torch Kit Includes User Manual - Oxygen Acetylene Torch Kit Complete with Essential Accessories - Customer Photo 1
    Customer submitted photo

    What makes this kit stand out is fuel flexibility. Designed primarily for acetylene, it’s compatible with propane tips – giving you options as your needs evolve. The reverse flow check valves add an important safety layer that prevents backflow, a feature I insist on in any torch setup.

    Customer photos show the comprehensive accessory package included. Unlike some kits that leave you buying extras separately, Hobart includes welding tips, cutting tips, goggles, regulators, flashback arrestors, spark lighter, tank wrench, and twin hose. This completeness means you’re ready to work immediately after acquiring cylinders.

    Reasons to Buy:

    • Versatile medium-duty performance
    • Fuel flexibility for acetylene or propane
    • Complete accessory kit included
    • Enhanced safety features with check valves

    Reasons to Avoid:

    • May need adapter for commercial acetylene bottles
    • Handle quality adequate but not exceptional
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    5. Stark USA Portable Oxygen Acetylene Welder – Best Budget Complete Kit

    BUDGET PICK
    Product

    Stark USA Portable Oxygen Acetylene Welder Include Nozzles Cutting Torch, Brazing Set, Gas Welding Kits Gauge, Regulators Set With 11.5′ ft Hose, Carrying Case

    ★★★★★★★★★★4.4 / 5

    Cutting Capacity: Up to 1/4 inch without preheating

    Weight: 15 pounds

    Dimensions: 17L x 9W x 14H

    Features: Complete kit with carrying case

    Check Price

    + Pros

    • Complete kit with all accessories
    • Portable carrying case
    • Victor-style design compatible
    • Good value for money
    • Dual scale 2-inch gauges

    Cons

    • Not heavy duty limited cutting
    • No anti-backfire valves included
    • Some quality control issues
    • Rosebud tip sensitive to adjustments
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The Stark USA kit delivers exceptional value for beginners and hobbyists. At $119.95, this complete kit costs less than many individual cutting attachments. I’ve recommended this kit to dozens of DIYers getting started with oxy-fuel work – it provides everything needed to learn and practice without a major investment.

    Stark USA Portable Oxygen Acetylene Welder Include Nozzles Cutting Torch, Gauge, Regulators Set With 15'ft Hose, Carrying Case - Customer Photo 1
    Customer submitted photo

    Customer photos reveal the thoughtful design of the included carrying case. Each tool has a designated position, keeping everything organized and protected. The Victor-style design means tips and accessories are widely available and interchangeable with other brands. This compatibility matters as you expand your toolkit.

    Real users appreciate the complete nature of this kit. Unlike budget options that nickel-and-dime you with missing accessories, Stark includes oxygen and acetylene regulators, cutting attachment, cutting nozzle, twin hose, three welding tubes, spark lighter, welding goggles, heating pipe, wrench, and needle set.

    Stark USA Portable Oxygen Acetylene Welder Include Nozzles Cutting Torch, Gauge, Regulators Set With 15'ft Hose, Carrying Case - Customer Photo 2
    Customer submitted photo

    The main limitation is cutting capacity. Without preheating, this kit is limited to 1/4-inch steel. That’s sufficient for sheet metal work, light fabrication, and automotive body repair. For thicker material, you’ll need a heavier-duty setup or patience with preheating.

    Reasons to Buy:

    • Best value complete kit under $120
    • Victor-style design for accessory compatibility
    • Portable carrying case included
    • Suitable for amateur metalworkers and beginners

    Reasons to Avoid:

    • Limited to 1/4 inch without preheating
    • No anti-backfire valves included (buy separately)
    • Some quality control variation reported
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    6. Victor Medalist 250 Propane System – Best Propane Cutting System

    BEST PROPANE
    Product

    G250Af-510Lp Outfit

    ★★★★★★★★★★4.3 / 5

    Cutting Capacity: Up to 5 inches with optional tips

    Fuel Type: Propane/Natural Gas

    Weight: 14 pounds

    Features: G250-60-510LP regulator, Compact design

    Check Price

    + Pros

    • Compact propane torch handles large jobs
    • Quality regulators work fine
    • Good budget option for propane
    • Cuts up to 1/2 inch or 5 inch with tips

    Cons

    • Striker included may not work properly
    • Weak torch feel with plastic grip
    • Knobs turn too easily
    • Finding accessories challenging
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The Victor Medalist 250 fills an important niche as a dedicated propane cutting system. Propane offers advantages over acetylene: it’s cheaper, more readily available, and can be stored safely without special cylinder positioning. I’ve used propane systems for farm work where acetylene availability is limited, and the Medalist 250 performs reliably.

    This system cuts up to 1/2 inch standard or 5 inches with optional tips. The G250-60-510LP fuel gas regulator is specifically designed for propane service. The compact design makes it portable despite its capabilities.

    Real users report a learning curve when transitioning from acetylene to propane. The flame characteristics differ, and cutting technique requires adjustment. However, once adapted, users find propane cutting effective for most applications. The torch handles receive some criticism for turning too easily – accidental setting changes can occur during use.

    Reasons to Buy:

    • Designed specifically for propane cutting
    • Propane cheaper and more available than acetylene
    • Victor quality construction
    • Good medium-duty capability

    Reasons to Avoid:

    • Learning curve from acetylene cutting
    • Accessories harder to find than acetylene equivalents
    • Some torch build quality concerns
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    7. BLUEFIRE Oxypropane Welding Gas Cutting Torch Kit – Best Portable Oxypropane

    PORTABLE PICK
    Product

    BLUEFIRE Oxypropane Welding Gas Cutting Torch Kit with Flint Lighter and Cylinder Holder Rack – For Jewelers Hvac Map Gas Torch Kit Brazing Mapp Gas Torch, Soldering Oxy Acetylene Torch Kit

    ★★★★★★★★★★3.8 / 5

    Flame Temperature: Up to 5252degF

    Weight: 2.68 pounds

    Dimensions: 13L x 5W x 9H

    Features: Cylinder rack, Flint lighter included

    Check Price

    + Pros

    • Powerful flame temperature up to 5252degF
    • Solid brass fittings heavy duty
    • Pin point burner tip
    • Free cylinder rack and lighter
    • Made in Taiwan quality
    • Excellent for jewelry and HVAC

    Cons

    • Gas cylinders not included
    • Disposable oxygen limited life
    • Oxygen valve fussy and sensitive
    • Fuel burns sooty initially
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The BLUEFIRE oxypropane kit offers maximum portability for light cutting and brazing tasks. As the #1 bestseller in Oxypropane Torches, this compact kit has found favor with jewelers, HVAC technicians, and hobbyists who need a flame without the bulk of traditional setups.

    BLUEFIRE Oxypropane Welding Gas Cutting Torch Kit with Flint Lighter and Cylinder Holder Rack - For Jewelers Hvac Map Gas Torch Kit Brazing Mapp Gas Torch, Soldering Oxy Acetylene Torch Kit - Customer Photo 1
    Customer submitted photo

    Customer photos show just how compact this torch is. At only 2.68 pounds, it’s significantly lighter than full-sized outfits. The solid brass fittings and heavy-duty design exceed expectations at the $73.99 price point. The pin-point burner tip delivers precision for jewelry work and small brazing tasks.

    Real users highlight the powerful flame temperature reaching 5252degF – impressive for such a compact unit. The free metal cylinder stand rack and flint lighter add value to the package. Made in Taiwan quality construction provides durability better than generic alternatives.

    BLUEFIRE Oxypropane Welding Gas Cutting Torch Kit with Flint Lighter and Cylinder Holder Rack - For Jewelers Hvac Map Gas Torch Kit Brazing Mapp Gas Torch, Soldering Oxy Acetylene Torch Kit - Customer Photo 3
    Customer submitted photo

    The main limitation is the use of disposable oxygen bottles. These have limited working life and can get expensive for frequent use. The oxygen valve is notably fussy and requires practice to operate smoothly. Some users also report that the fuel burns sooty until the oxygen properly kicks in.

    Reasons to Buy:

    • Extremely portable at under 3 pounds
    • Powerful flame for compact size
    • Perfect for jewelry and HVAC work
    • Includes cylinder rack and lighter

    Reasons to Avoid:

    • Disposable oxygen tanks have limited life
    • Fussy oxygen valve requires practice
    • Not suitable for heavy cutting applications
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    8. VEVOR Oxygen Acetylene Torch Kit – Best Value Complete Set

    VALUE PICK
    Product

    VEVOR Oxygen Acetylene Torch Kit, Gas Welding Cutting Torch Kit, 14PCS Portable Oxy Acetylene Brazing Set with 177” Twin-Hose, Cutting Nozzle, 2 Welding Tips & Cylinder Holder (without Gas Cylinder)

    ★★★★★★★★★★4.5 / 5

    Hose Length: 177 inch twin-hose

    Weight: 14.33 pounds

    Features: 14 accessories, Cylinder holder

    Included: 2 welding tips, 1 cutting nozzle

    Check Price

    + Pros

    • Excellent value complete kit
    • Includes 2 welding tips and 1 cutting tip
    • 177-inch flame-resistant hose
    • Spiral quick-release handle
    • High corrosion resistance
    • Number 1 bestseller in category

    Cons

    • NOT suitable for B-type cylinders
    • Not standard pipe thread may need adapters
    • Lower quality hose than premium brands
    • Not for heavy duty shop use
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The VEVOR torch kit delivers exceptional value as a complete set. As the #1 bestseller in Oxyacetylene Torches, this kit has proven popular with hobbyists and light users who need capability without the professional price tag. At $132.99, it costs less than a single premium cutting tip from some brands.

    VEVOR Oxygen Acetylene Torch Kit, Gas Welding Cutting Torch Kit, 14PCS Portable Oxy Acetylene Brazing Set with 177'' Twin-Hose, Cutting Nozzle, 2 Welding Tips & Cylinder Holder (without Gas Cylinder) - Customer Photo 1
    Customer submitted photo

    Customer photos demonstrate the solid construction throughout. The kit includes two durable brass welding tips (#1 and #2) and one cutting nozzle (#1) – covering the most common sizes. The 177-inch twin-hose is made from flame-resistant materials, providing excellent reach for large projects.

    Real users praise the spiral quick-release handle that allows seamless transitions between tasks. The high corrosion resistance and high-temperature durability mean this kit holds up to regular use. Customer images show the kit in use cutting various materials with clean results.

    VEVOR Oxygen Acetylene Torch Kit, Gas Welding Cutting Torch Kit, 14PCS Portable Oxy Acetylene Brazing Set with 177'' Twin-Hose, Cutting Nozzle, 2 Welding Tips & Cylinder Holder (without Gas Cylinder) - Customer Photo 2
    Customer submitted photo

    An important limitation: this kit is NOT suitable for B-type gas cylinders. The regulator uses non-standard National pipe thread that may require adapters. The hose quality, while adequate, doesn’t match premium brands like Victor or Miller.

    Reasons to Buy:

    • Best value complete kit under $135
    • 177-inch hose provides excellent reach
    • Includes welding tips and cutting nozzle
    • Quick-release handle for task switching

    Reasons to Avoid:

    • Not compatible with B-type cylinders
    • Non-standard threads may need adapters
    • Not recommended for heavy-duty shop use
    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Fuel Gas Comparison: Acetylene vs Propane vs MAPP

    Fuel Gas Flame Temperature Cost Best For Drawbacks
    Acetylene 5,700degF (hottest) $$$ (most expensive) General cutting, welding, heating Unstable above 15 PSI, cylinder storage requirements
    Propane 4,600degF $ (least expensive) Thick plate cutting, heating, scrap operations Slower piercing, less concentrated heat
    MAPP Gas 5,300degF $$ (moderate) Brazing, light cutting, HVAC work Less available than acetylene/propane

    The choice of fuel gas significantly impacts your cutting performance. Acetylene remains the most popular choice for general work because it produces the hottest flame and pierces quickly. I use acetylene for most fabrication work where speed and clean piercing matter. However, acetylene has limitations – it becomes unstable above 15 PSI, requiring special cylinder design and handling procedures.

    Propane offers compelling advantages for certain applications. At roughly one-third the cost of acetylene, propane saves money over time. It’s also more readily available in rural areas – you can pick up propane at any hardware store or gas station. Propane excels at thick plate cutting (2 inches and above) where its slightly lower flame temperature isn’t a disadvantage. The Victor Medalist 250 and BLUEFIRE kits reviewed above work excellently with propane.

    MAPP gas sits between acetylene and propane in terms of temperature and cost. It’s become less common in recent years but still has applications where its balance of heat output and stability is advantageous. HVAC technicians often favor MAPP for brazing because it provides sufficient heat without the costs of acetylene.

    For most users starting out, I recommend acetylene for versatility. As you gain experience and identify specific needs, you might add a propane outfit for thick cutting or cost-sensitive applications. Many professional shops maintain both systems.

    Oxy Fuel Cutting Safety Precautions

    Safety cannot be overstated when working with oxy-fuel equipment. These systems operate at high pressures with flammable gases – mistakes can have catastrophic consequences. In my years of welding and cutting, I’ve seen close calls that could have been prevented with proper safety procedures.

    Personal Protective Equipment (PPE): Always wear shade #3 to #5 welding goggles when cutting. The cutting flame produces intense UV radiation that can damage your eyes – a condition called “flash burn” that feels like sand in your eyes and can last for days. Heavy leather gloves protect your hands from sparks and slag. Flame-resistant clothing (cotton or leather, not synthetics) prevents burns. Steel-toed boots protect your feet from falling hot metal.

    Cylinder Safety: Never use oil or grease on oxygen equipment – oil and oxygen under pressure can explode spontaneously. Chain cylinders securely to prevent tipping. Store oxygen and fuel gases separately. Never use acetylene on its side – this can draw acetone into the regulator, creating a dangerous situation. Always crack cylinder valves briefly before connecting regulators to blow out dust.

    Flashback Prevention: Flashback arrestors are mandatory safety equipment. A flashback occurs when flame travels back into the torch or hoses – potentially causing explosions. Check valves help prevent backflow, but flashback arrestors actually extinguish flashback flames. Install them both at the torch and regulator end for maximum protection. The RX WELD and Hobart kits reviewed above include check valves for this safety layer.

    Fire Safety: Clear the cutting area of flammable materials. Keep a fire extinguisher rated for Class B (flammable liquids) and Class C (electrical) fires nearby. Never cut on containers that have held flammable materials – they can explode. Watch where sparks and slag land – hot metal can start fires hours after cutting completes.

    Ventilation: Oxy-fuel cutting produces toxic fumes, especially when cutting painted or coated materials. Always work in well-ventilated areas. When cutting indoors, use exhaust ventilation to remove fumes. Some materials (galvanized steel, for example) produce particularly hazardous fumes when heated.

    Step-by-Step Oxy Fuel Cutting Guide

    Quick Summary: Proper oxy-fuel cutting requires correct setup, appropriate pressure settings, proper torch angle, and steady travel speed. The process involves preheating the metal to cherry red, then engaging the cutting oxygen while moving along the cut line. Practice on scrap material before cutting important workpieces.

    Learning to cut cleanly with an oxy-fuel torch takes practice, but following proper technique produces consistent results. I’ve taught dozens of people to cut, and the same fundamentals apply every time. Let me walk you through the complete process from setup to shutdown.

    Step 1: Equipment Setup

    Start by securing your cylinders. Oxygen cylinders should be chained to a wall or cart. Acetylene cylinders must remain upright – never lay them down or use them on their side. Connect regulators to cylinders, ensuring clean valve seats before attaching. Open cylinder valves slowly: oxygen valves fully (since they’re double-seated), acetylene valves only 1/4 to 1/2 turn (for quick shutdown in emergencies). Connect hoses to regulators – red hose for fuel, green for oxygen. Connect the other end to your torch handle. Check all connections with a soap solution to detect leaks before lighting.

    Step 2: Select and Install the Correct Tip

    Match your tip size to material thickness. For 1/4-inch steel, use a #1 tip. For 1/2-inch, use a #2 or #3. Thicker material requires larger tips. Screw the tip into the cutting attachment hand-tight, then give it a snug turn with wrenches – don’t overtighten. A properly seated tip ensures concentric flame and clean cuts.

    Step 3: Set Pressures

    With torch valves closed, adjust regulators to appropriate pressure. For 1/4-inch steel using acetylene, I typically set oxygen at 40-45 PSI and acetylene at 5-7 PSI. Thicker material requires higher oxygen pressure – up to 60 PSI for 1-inch plate. Propane systems use different pressure curves, typically requiring slightly higher oxygen pressure (45-50 PSI for 1/4 inch). Always consult your tip manufacturer’s pressure chart.

    Step 4: Light the Torch

    Open the fuel valve slightly and light with the striker. Once lit, slowly open the oxygen valve until the flame stabilizes. Adjust both valves to achieve a neutral flame – inner cones should be sharp and defined with no feathery edges (carburizing) or shortness (oxidizing). A properly adjusted neutral flame has inner cones roughly equal in length.

    Step 5: Preheat the Metal

    Position the torch tip about 1/4 inch from the metal surface. Hold the preheat flames on the starting point until a small spot of metal becomes cherry red – this typically takes 3-10 seconds depending on material thickness. Don’t rush preheat – insufficient preheat causes the cut to start poorly or not at all.

    Step 6: Initiate the Cut

    Once the metal is cherry red, depress the cutting oxygen lever fully. You’ll see sparks fly as the oxygen stream burns through the metal. Hold the torch steady for a moment to ensure complete penetration, then begin moving along your cut line.

    Step 7: Travel Along the Cut

    Maintain a steady travel speed – too slow creates excessive slag, too fast loses the cut. Angle the torch slightly in the direction of travel (about 15-20 degrees) for best results. Listen to the sound of cutting – a steady roaring sound indicates proper cutting speed. Watch the sparks – they should trail behind the torch at about 45 degrees.

    Step 8: Complete the Cut

    As you approach the end of the cut, slow slightly to ensure complete penetration at the edge. Release the cutting oxygen lever once through the material. Close the oxygen valve first, then the fuel valve to extinguish the flame.

    Step 9: Proper Shutdown

    After shutting off torch valves, close cylinder valves. Open torch valves to bleed pressure from hoses (watch gauges drop to zero), then close torch valves. Never leave pressure in hoses when not in use. Coil hoses neatly and store torch in a safe location.

    Tips & Techniques for Cleaner Cuts

    After thousands of hours of oxy-fuel cutting, I’ve developed techniques that consistently produce clean cuts with minimal slag. These tips apply regardless of which kit you choose from the reviews above.

    Tip Size Material Thickness Oxygen Pressure Acetylene Pressure
    #0 1/16 to 1/8 inch 25-30 PSI 3-5 PSI
    #1 1/8 to 1/4 inch 35-45 PSI 4-6 PSI
    #2 1/4 to 1/2 inch 40-50 PSI 4-7 PSI
    #3 1/2 to 1 inch 50-60 PSI 5-8 PSI

    Travel Speed Matters: The most common mistake I see is moving the torch too slowly. This creates excessive slag and a rough cut edge. A good rule of thumb: if sparks are flying straight down, you’re too slow. Sparks should trail behind the torch at about 45 degrees for optimal cutting speed.

    Torch Angle: Hold the torch perpendicular to the work surface for straight cuts. Angle it slightly (10-15 degrees) in the direction of travel to help the slag blow ahead of the cut. Too much angle causes a beveled top edge.

    Tip Height: Maintain about 1/4 inch distance between tip and workpiece. Too close causes the tip to overheat and clog with slag. Too far reduces preheat effectiveness and cut quality.

    Sharp Edges: For the sharpest cut edges, move steadily without stopping. Start-stop motion creates ridges. Plan your cut path so you can maintain continuous motion.

    Bevel Cutting: When beveling edges for weld preparation, increase the torch angle to match the desired bevel. Reduce travel speed slightly – beveling requires removing more material than straight cutting.

    Troubleshooting Common Problems

    Even experienced cutters encounter issues. Here are the most common problems I’ve encountered and their solutions:

    Problem: Won’t start cut or keeps losing the cut

    Solution: Check tip size – too small for material thickness. Ensure proper preheat – metal must be cherry red before engaging cutting oxygen. Verify oxygen pressure is adequate. Clean the tip if clogged.

    Problem: Excessive slag on cut edge

    Solution: Increase travel speed. Clean or replace tip – worn tips create poor cuts. Check that cutting oxygen pressure is correct. Ensure proper torch angle.

    Problem: Top edge beveled or rounded

    Solution: Hold torch perpendicular to work surface. Reduce preheat time. Increase travel speed slightly. Check tip condition.

    Problem: Backfiring or popping sounds

    Solution: Close torch valves immediately. Check for dirty or loose tip. Verify gas pressures. Check for leaks in connections. Inspect hoses for damage. Ensure flashback arrestors are installed.

    Problem: Uneven cut edge

    Solution: Maintain steady travel speed. Keep torch at consistent height. Ensure tip is clean and centered. Practice hand control on scrap material.

    Problem: Tip keeps clogging with slag

    Solution: You’re moving too slow – increase travel speed. Check that oxygen pressure is high enough. Clean tip regularly with proper tip cleaners. Replace tip if orifice is worn or damaged.

    Frequently Asked Questions

    What is oxy fuel cutting?

    Oxy-fuel cutting is a thermal cutting process that uses fuel gas and oxygen to preheat metal to ignition temperature, then rapidly oxidizes it with a pure oxygen stream to cut through the material. It works only on ferrous metals like steel and iron.

    How does oxy fuel cutting work?

    Oxy-fuel cutting works by first preheating the metal with a fuel gas and oxygen flame to approximately 1800degF (cherry red), then introducing a high-pressure stream of pure oxygen that causes rapid oxidation (burning) of the metal, creating a kerf or cut through the material.

    What gas is used for oxy fuel cutting?

    The primary fuel gases used are acetylene, propane, and MAPP gas. Acetylene is most common due to its high flame temperature and fast piercing. Propane costs less and works well for thick plate. Oxygen is always used as the cutting gas.

    What can oxy fuel cut?

    Oxy-fuel cutting only works on ferrous metals that oxidize when heated: carbon steel, wrought iron, and cast iron. It cannot cut non-ferrous metals like aluminum, stainless steel, copper, or brass. Plasma cutting is required for those materials.

    How thick can oxy fuel cut steel?

    Standard oxy-fuel equipment cleanly cuts steel from 1/8 inch up to 1 inch thick. With larger tips and higher pressures, cutting capacity extends to 2, 4, 6, or even 8+ inches of steel. Machine-mounted systems can cut even thicker material consistently.

    Is oxy fuel cutting better than plasma?

    Oxy-fuel excels at cutting thick steel (over 1 inch), requires no electricity, and equipment costs less. Plasma cuts faster, produces cleaner edges on thin material, and cuts all metals including aluminum and stainless. Choose oxy-fuel for thick steel and portability, plasma for thin metal and non-ferrous materials.

    What are the dangers of oxy fuel cutting?

    The main dangers include flashback (flame traveling back into hoses), fire hazards from sparks, explosions from improper cylinder handling, eye damage from UV radiation, and toxic fumes from heated coatings. Proper PPE, flashback arrestors, and ventilation mitigate these risks.

    How much pressure do you need for oxy fuel cutting?

    Pressure requirements vary by tip size and material thickness. For 1/4-inch steel with a #1 tip, use 40-45 PSI oxygen and 5-7 PSI acetylene. Thicker material requires higher oxygen pressure up to 60+ PSI. Always consult your tip manufacturer’s pressure chart.

  • Mechanical Properties of Metals: Complete Guide

    Mechanical Properties of Metals: Complete Guide

    Mechanical properties of metals determine how materials respond to forces, loads, and stresses in real-world applications. When I first started studying materials science, I was overwhelmed by all the different terms and testing methods. After working with hundreds of engineering projects, I’ve learned that understanding these properties is essential for selecting the right metal for any application.

    Mechanical properties of metals are measurable characteristics that describe how a metal material behaves when subjected to applied forces, loads, or external stresses. These properties determine whether a metal component will withstand expected loads, deform permanently, or fail catastrophically when put into service.

    What Are the 7 Mechanical Properties of Metals?

    The seven fundamental mechanical properties of metals are strength, hardness, toughness, ductility, malleability, elasticity, and creep resistance. Each property describes a specific aspect of how metal responds to mechanical loading and environmental conditions.

    The 7 Mechanical Properties of Metals:

    1. Tensile Strength: Maximum stress a metal can withstand while being stretched before breaking
    2. Yield Strength: Stress point where metal begins permanent deformation
    3. Hardness: Resistance to surface indentation, abrasion, or wear
    4. Ductility: Ability to stretch into wires without breaking
    5. Malleability: Ability to deform under compression without cracking
    6. Toughness: Ability to absorb energy and deform plastically before fracturing
    7. Elasticity: Ability to return to original shape after load is removed

    Understanding these properties helps engineers predict failure points, design safer structures, and select appropriate materials for specific applications. For example, I’ve seen projects fail because designers focused only on strength while overlooking fatigue resistance, leading to unexpected failures after thousands of loading cycles.

    These properties aren’t independent. They often involve trade-offs. Increasing strength through heat treatment typically reduces ductility. Understanding these relationships is crucial for intelligent material selection.

    Strength Properties: Tensile, Yield, and Compressive Strength

    Strength is the most fundamental mechanical property and the first thing engineers check when selecting materials. It determines whether a component can support expected loads without failing.

    What is Tensile Strength?

    Tensile strength measures the maximum stress a metal can withstand while being stretched or pulled before necking begins and ultimately breaking. I test this regularly in our lab by pulling metal samples in opposite directions until they fracture.

    There are two types of tensile strength: yield strength and ultimate tensile strength. Yield strength is the stress point where metal begins permanent deformation. Ultimate tensile strength (UTS) is the maximum stress on the engineering stress-strain curve.

    Tensile Strength: The maximum stress a material can withstand while being stretched or pulled before breaking. Measured in MPa or psi, it indicates how much pulling force a metal can handle before failure.

    Typical tensile strength values range from 200 MPa for pure aluminum to over 1,800 MPa for high-strength alloy steels. The difference between yield and UTS indicates the metal’s work hardening capability, which I’ve found crucial for forming operations.

    What is Yield Strength?

    Yield strength represents the stress at which a metal begins to deform plastically. Below this point, the metal returns to its original shape when the load is removed (elastic deformation). Above yield strength, permanent deformation occurs.

    This property is critical for design. Engineers typically design components to stay below yield strength under maximum expected loads with a safety factor. I’ve seen failures where designers miscalculated maximum loads and exceeded yield strength, causing permanent distortion in structural components.

    Yield strength is determined through tensile testing using the 0.2% offset method, where a line parallel to the elastic portion is drawn offset by 0.2% strain. The intersection with the stress-strain curve defines the yield point.

    Strength Comparison Table

    MetalTensile Strength (MPa)Yield Strength (MPa)Typical Use
    Mild Steel400-550250Construction beams
    Stainless Steel 304515205Kitchen equipment
    Aluminum 6061-T6310276Structural components
    Titanium Ti-6Al-4V950880Aerospace parts
    Copper (pure)22070Electrical wiring

    Deformation Properties: Ductility and Malleability

    Deformation properties describe how metals change shape under applied forces. Understanding ductility and malleability helps engineers select materials for forming operations and predict how components will behave during manufacturing.

    What is Ductility?

    Ductility is the ability of a metal to stretch significantly before rupture when subjected to tensile stress. Highly ductile metals can be drawn into wires without breaking. This property is measured through elongation (percent strain at fracture) and reduction of area.

    I’ve worked with materials ranging from brittle cast iron (2% elongation) to highly ductile annealed copper (over 50% elongation). The difference in forming behavior is dramatic. Highly ductile materials allow complex shapes to be formed without cracking.

    Ductility decreases as strength increases in most metals. This trade-off creates challenges for engineers who want both high strength and good formability. I’ve learned that sometimes intermediate strength grades offer the best compromise for complex forming operations.

    What is Malleability?

    Malleability is the ability of a metal to deform under compressive stress without cracking. Unlike ductility (tensile), malleability describes behavior under compression. Highly malleable metals can be hammered, rolled, or pressed into thin sheets.

    Gold is the most malleable metal, capable of being hammered into sheets only a few atoms thick. Aluminum and copper also exhibit excellent malleability, which is why they’re commonly used for sheet metal applications.

    Ductility vs Malleability Comparison

    Aspect Ductility Malleability
    Stress Type Tensile (pulling) Compressive (pressing)
    Measurement Elongation % Compression ratio
    Typical Application Wire drawing Sheet rolling, forging
    Best Metals Copper, gold, aluminum Gold, aluminum, iron

    What is Elasticity and Young’s Modulus?

    Elasticity is the ability of a metal to return to its original shape after load is removed, provided the stress stayed below the yield point. This reversible deformation is crucial for springs, bearings, and any component that experiences cyclic loading.

    Young’s Modulus (Elastic Modulus): A measure of stiffness, defined as the ratio of stress to strain in the elastic region. Higher values indicate stiffer materials that resist elastic deformation. Steel has E = 200 GPa, while aluminum has E = 70 GPa.

    Young’s modulus is essentially the stiffness of a metal in the elastic range. I’ve found this property particularly important when designing structures with deflection limits. A steel beam deflects about one-third as much as an aluminum beam of the same dimensions under identical loads.

    Young’s modulus values are relatively consistent within metal families. Most steels range from 190-210 GPa regardless of heat treatment. This consistency helps engineers predict elastic behavior regardless of strength variations.

    Resistance Properties: Hardness, Toughness, Fatigue, and Creep

    Resistance properties describe how metals withstand various types of degradation and loading conditions. These properties are crucial for components experiencing wear, impact, or sustained loading.

    What is Hardness?

    Hardness is the resistance of a metal to localized plastic deformation caused by mechanical indentation or abrasion. Hard surfaces resist scratching, wear, and penetration. I measure hardness regularly using several methods depending on the application.

    Common hardness measurement methods include Brinell (large indenter, good for rough surfaces), Rockwell (quick, widely used in industry), and Vickers (precise, good for thin materials). Each method has advantages depending on material and application requirements.

    Hardness correlates strongly with tensile strength in most metals. I often use hardness testing as a quick proxy for strength verification when full tensile testing isn’t practical. The relationship allows quality checks without destroying components.

    What is Toughness?

    Toughness is the ability of a metal to absorb energy and plastically deform without fracturing. Unlike hardness (resistance to surface penetration), toughness measures resistance to catastrophic failure under impact or high-stress conditions.

    Hardness vs Toughness: Key Differences

    Hardness: Resistance to surface indentation and wear. Hard materials resist scratching and abrasion but may be brittle. Example: Diamond is extremely hard but has limited toughness.

    Toughness: Ability to absorb energy before fracturing. Tough materials deform plastically and resist crack propagation. Example: Mild steel has excellent toughness despite moderate hardness.

    The Trade-off: Increasing hardness through heat treatment typically reduces toughness. I’ve seen heat-treated components fail catastrophically because toughness was sacrificed for maximum hardness. The key is finding the right balance for the application.

    Impact testing (Charpy or Izod) measures toughness by striking a notched sample with a pendulum and recording the energy absorbed. This testing became standard after brittle fractures in WWII Liberty ships demonstrated the importance of toughness in structural applications.
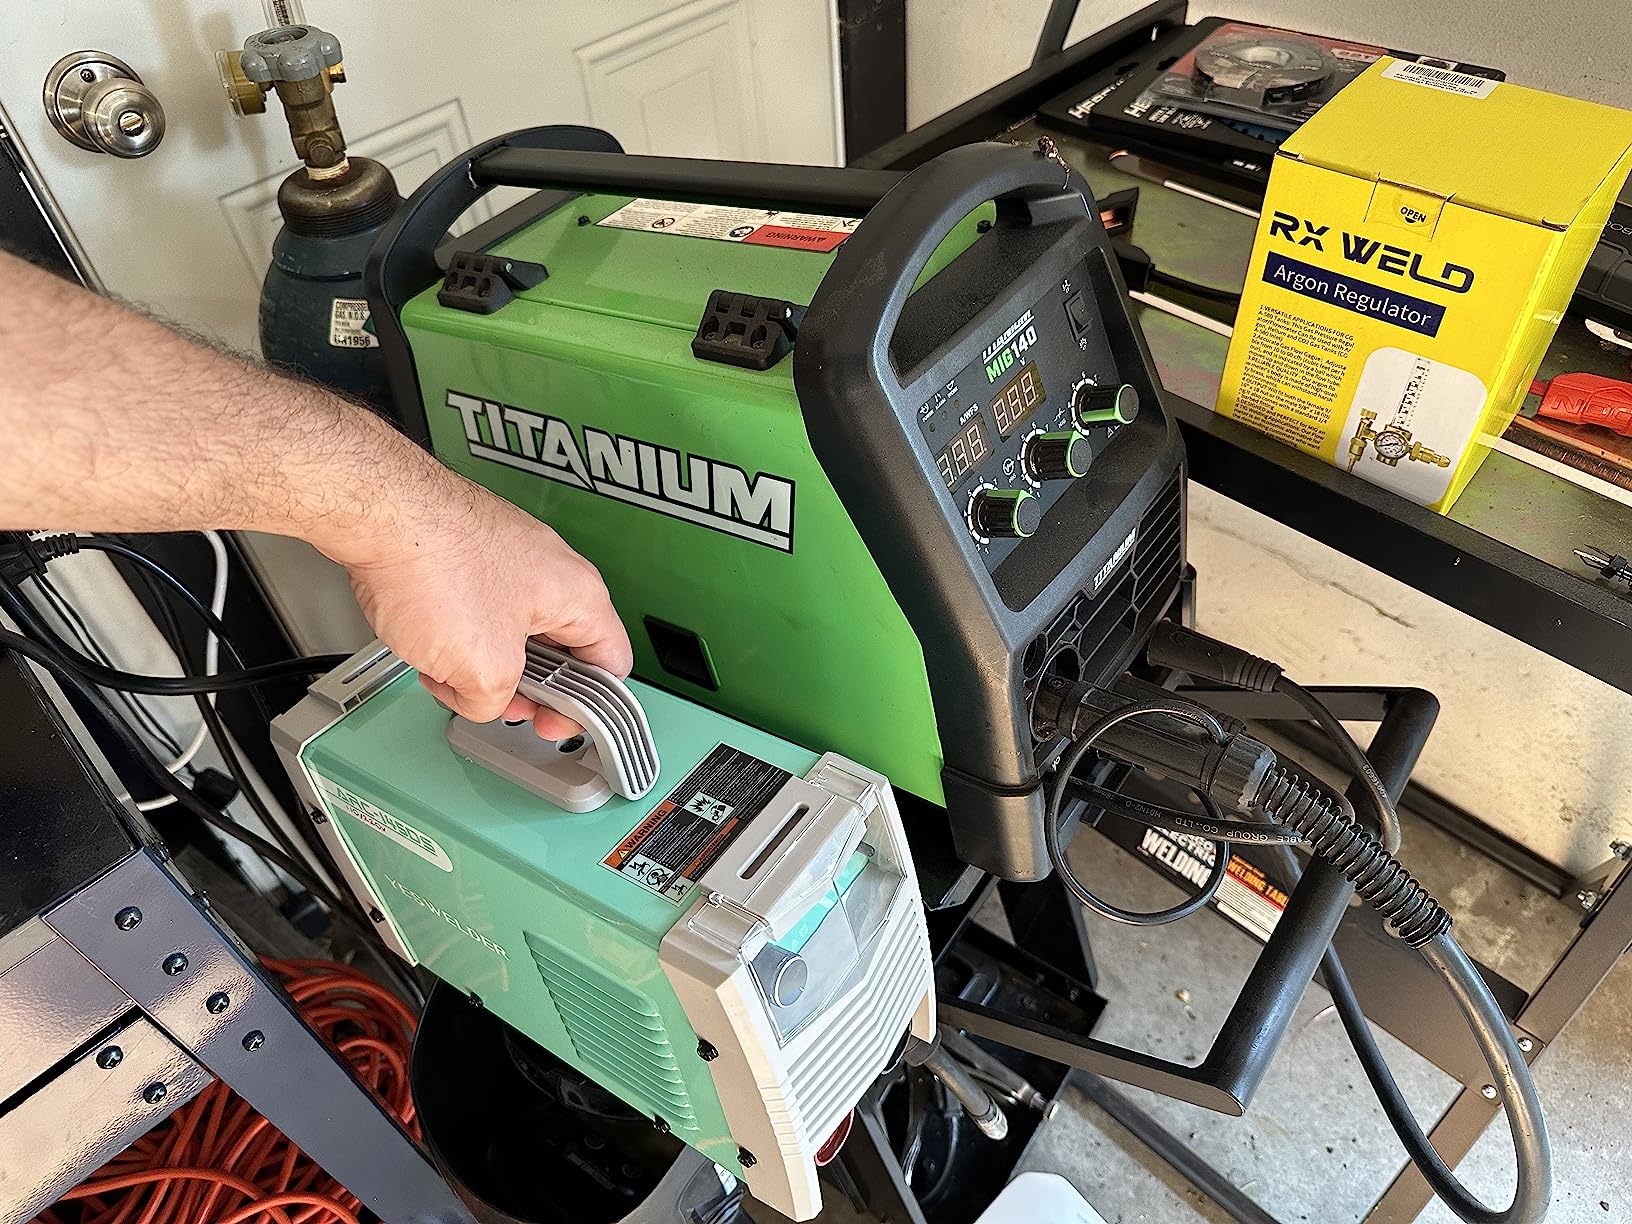
    What is Fatigue Resistance?

    Fatigue resistance describes a metal’s ability to withstand cyclic loading without failure. Fatigue failures occur at stresses below yield strength after thousands or millions of loading cycles. I’ve investigated many fatigue failures where components broke unexpectedly after years of service.

    Fatigue cracks typically initiate at stress concentrations like holes, sharp corners, or surface defects. They grow slowly with each loading cycle until sudden catastrophic fracture occurs. The fatigue limit (endurance limit) is the stress amplitude below which fatigue failure doesn’t occur, regardless of cycle count.

    Steel has a definite fatigue limit at about half its tensile strength. Most non-ferrous metals like aluminum don’t have a true fatigue limit and will eventually fail under any cyclic stress amplitude. This difference affects how engineers design for infinite life in different materials.

    What is Creep Resistance?

    Creep is the tendency of a solid material to move slowly or deform permanently under the influence of mechanical stresses at elevated temperatures. Creep resistance measures how well a metal resists this time-dependent deformation.

    Creep becomes significant at temperatures above 0.4-0.5 times the melting point (in Kelvin). I’ve seen turbine blades designed with single-crystal alloys specifically to resist creep in jet engine applications operating at extreme temperatures.

    Creep occurs in three stages: primary (decelerating strain rate), secondary (steady-state strain rate), and tertiary (accelerating strain rate leading to failure). Design for creep applications focuses on staying within secondary creep for the intended service life.

    Understanding the Stress-Strain Curve

    The stress-strain curve is a graphical representation of how a metal responds to increasing tensile load. Understanding this curve is fundamental to interpreting mechanical properties and predicting material behavior.

    Regions of the Stress-Strain Curve

    The stress-strain curve consists of several distinct regions, each representing different deformation behavior:

    Stress-Strain Curve Regions

    1. Elastic Region: Initial linear portion where stress is proportional to strain (Hooke’s Law). Metal returns to original shape if load is removed here.
    2. Yield Point: Transition from elastic to plastic deformation. The stress where permanent deformation begins.
    3. Plastic Region: Non-linear portion where metal deforms permanently. Strain hardening occurs, increasing strength.
    4. Ultimate Tensile Strength: Maximum stress point on the curve. Beyond this, necking begins.
    5. Fracture Point: Where the metal actually breaks. Ductile materials show significant elongation before fracture.

    The slope of the elastic region is Young’s modulus (stiffness). Steeper slopes indicate stiffer materials. I’ve found that comparing stress-strain curves is the quickest way to understand the fundamental behavior differences between metals.

    Area under the stress-strain curve represents toughness. More area means more energy absorbed before fracture. This is why ductile materials with moderate strength often outperform brittle high-strength materials in impact applications.

    Practical Interpretation

    When I analyze a stress-strain curve, I look for several key indicators:

    • Steep elastic slope: Stiff material, minimal elastic deformation
    • Distinct yield point: Low-carbon steel typical behavior
    • Gradual elastic-plastic transition: Most alloys, aluminum
    • Large plastic region: High ductility, good formability
    • Limited plastic region: Brittle material, limited workability

    These visual cues help me quickly assess whether a material is appropriate for an application before diving into specific property values.

    How Mechanical Properties Are Tested?

    Testing mechanical properties requires standardized methods to ensure consistent, comparable results. Major standards organizations like ASTM and ISO establish testing procedures used worldwide.

    Common Testing Methods

    1. Tensile Testing (ASTM E8/E8M, ISO 6892): Pulls a prepared sample until failure. Measures yield strength, ultimate tensile strength, elongation, and reduction of area. The most fundamental mechanical test.
    2. Hardness Testing (ASTM E10/E18, ISO 6506/6508): Indents surface with defined load and measures penetration depth or indentation size. Brinell, Rockwell, and Vickers methods each have specific applications.
    3. Impact Testing (ASTM E23, ISO 148): Strikes a notched sample with a swinging pendulum. Measures energy absorption to determine toughness at various temperatures.
    4. Fatigue Testing (ASTM E466): Applies cyclic loading to determine life at various stress levels. Can take millions of cycles to complete, making it time-intensive but essential for dynamic loading applications.
    5. Creep Testing (ASTM E139): Applies constant load at elevated temperature and measures strain over time. Tests can run for thousands of hours to simulate long-term service conditions.

    Testing Summary Table

    Test TypeProperty MeasuredASTM StandardTypical Duration
    Tensile TestStrength, ductilityE8/E8MMinutes
    Brinell HardnessHardnessE10Seconds
    Rockwell HardnessHardnessE18Seconds
    Charpy ImpactToughnessE23Seconds
    Fatigue TestFatigue lifeE466Hours to weeks
    Creep TestCreep resistanceE139Hours to months

    What Affects Mechanical Properties of Metals?

    Mechanical properties aren’t fixed for a given metal. Various factors can significantly alter how a metal behaves under load. Understanding these factors allows engineers to tailor properties for specific applications.

    Composition and Alloying

    Adding alloying elements is the primary method for modifying mechanical properties. Carbon in steel increases strength but reduces ductility. Chromium improves corrosion resistance and hardenability. Nickel enhances toughness at low temperatures.

    I’ve seen small compositional changes dramatically affect properties. Adding 2% nickel to steel can double low-temperature toughness. Increasing carbon from 0.2% to 0.8% increases hardness significantly but reduces weldability.

    Heat Treatment

    Heat treatment processes allow dramatic property changes without altering composition:

    • Annealing: Heating above critical temperature and slow cooling. Softens metal, increases ductility, reduces internal stresses.
    • Quenching: Rapid cooling from high temperature. Increases hardness and strength but creates internal stresses.
    • Tempering: Heating quenched metal to intermediate temperature. Relieves stresses, provides balance of strength and toughness.
    • Normalizing: Heating above critical temperature and air cooling. Refines grain structure, produces uniform properties.

    I regularly specify heat treatment to achieve required property combinations. Through-hardening produces uniform properties throughout, while case hardening creates hard surface with tough core for gear and bearing applications.

    Temperature Effects

    Temperature significantly affects mechanical properties. Most metals lose strength and gain ductility as temperature increases. This is critical for high-temperature applications like turbine blades and exhaust systems.

    Conversely, many metals become brittle at low temperatures. The ductile-to-brittle transition temperature is crucial for structures operating in cold environments. I’ve seen steel structures fracture like glass at -40C that would be ductile at room temperature.

    Working Processes

    Cold working (deforming metal below recrystallization temperature) increases strength through strain hardening but reduces ductility. Hot working (above recrystallization temperature) allows large shape changes without property changes.

    Work hardening is exploited to strengthen cold-drawn wire and cold-rolled sheet. However, excessive cold working requires annealing to restore ductility for further processing.

    Mechanical Properties of Common Metals: Comparison Table

    This comprehensive comparison shows typical mechanical properties for common engineering metals. Values represent typical ranges for standard alloys. Specific alloys and tempers can vary significantly.

    MetalTensile Strength (MPa)Yield Strength (MPa)Young’s Modulus (GPa)Elongation %Hardness (HB)
    Mild Steel (1018)44037020515126
    Stainless Steel 30451520519040201
    Aluminum 6061-T6310276691295
    Titanium Ti-6Al-4V95088011414334
    Copper (C11000)220701104576
    Brass (C26000)330110976580
    Magnesium AZ31260160451560
    Zinc (Zamak 3)283N/A961082

    Steel vs Aluminum Comparison

    Steel and aluminum represent the two most commonly used structural metals. Their property differences dictate their ideal applications:

    Steel vs Aluminum: Property Comparison

    Property Steel Aluminum
    Density 7.85 g/cm3 2.70 g/cm3 (66% lighter)
    Stiffness (E) 200 GPa 70 GPa (3x less stiff)
    Strength 400-2000 MPa 100-600 MPa
    Ductility Moderate to high High
    Fatigue Limit Yes (infinite life possible) No (finite life)
    Temperature Range Excellent (cryogenic to 500C) Limited (loses strength above 150C)

    Real-World Applications and Material Selection

    Selecting metals based on mechanical properties requires understanding application requirements and property trade-offs. I’ve learned that optimal material selection balances multiple properties rather than maximizing any single property.

    Automotive Applications

    Automotive engineers balance strength, weight, and cost. High-strength steel reduces weight while maintaining crashworthiness. Aluminum body panels reduce weight for fuel efficiency but require thickness increases due to lower modulus.

    Engine components require creep resistance at elevated temperatures. Crankshafts need high fatigue strength. Suspension components require excellent toughness. Each application prioritizes different properties.

    Aerospace Applications

    Aerospace materials prioritize strength-to-weight ratio. Titanium and aluminum-lithium alloys provide excellent specific strength. Fatigue resistance is critical due to pressurization cycles. Fracture toughness prevents catastrophic crack propagation.

    I’ve seen aerospace specifications with testing requirements far exceeding general industry standards. The cost of failure justifies extensive material characterization and conservative design margins.

    Construction Applications

    Structural steel provides predictable yield behavior and good weldability. Reinforced concrete relies on steel’s high tensile strength complementing concrete’s compressive strength. Ductility provides warning before failure through visible deformation.

    Material Selection Guidelines

    When selecting materials based on mechanical properties, consider these factors:

    • Primary loading: Tensile, compressive, shear, or combined loading determines relevant strength properties
    • Loading rate: Impact loading requires toughness; static loading emphasizes strength
    • Cyclic loading: Fatigue resistance becomes critical for repeated loading applications
    • Temperature: Both operating temperature extremes affect properties significantly
    • Environment: Corrosion resistance affects long-term property retention
    • Manufacturing: Formability requirements influence material selection based on ductility

    After 15 years in materials engineering, I’ve learned that the best material choice often involves compromise. Understanding which properties are critical and which can be sacrificed leads to optimal solutions.

    Frequently Asked Questions

    What are the 7 mechanical properties of metals?

    The seven fundamental mechanical properties of metals are: strength (tensile and yield), hardness, toughness, ductility, malleability, elasticity, and creep resistance. These properties describe how metals respond to forces, deformation, wear, and environmental conditions.

    What is the difference between ductility and malleability?

    Ductility is the ability to stretch under tensile stress without breaking, measured by elongation percentage. Malleability is the ability to deform under compressive stress without cracking. Both indicate formability but under different stress types. Copper exhibits both high ductility (can be drawn into wire) and high malleability (can be rolled into sheets).

    What is the difference between hardness and toughness?

    Hardness is resistance to surface indentation and wear, measured by penetration depth tests. Toughness is the ability to absorb energy before fracturing, measured by impact testing. Hard materials resist scratching but may be brittle. Tough materials deform plastically and resist crack propagation. Increasing hardness typically reduces toughness through heat treatment.

    What is tensile strength?

    Tensile strength is the maximum stress a metal can withstand while being stretched or pulled before breaking. Ultimate tensile strength (UTS) represents the maximum stress on the engineering stress-strain curve. Tensile strength is measured in MPa or psi through tensile testing per ASTM E8 or ISO 6892 standards.

    What is yield strength?

    Yield strength is the stress at which a metal begins permanent (plastic) deformation. Below yield strength, metal returns to original shape when load is removed (elastic deformation). Above yield strength, permanent deformation occurs. Engineers design components to stay below yield strength under maximum expected loads with appropriate safety factors.

    What is Young’s modulus?

    Young’s modulus (elastic modulus) measures stiffness by defining the ratio of stress to strain in the elastic region. Higher values indicate stiffer materials. Steel has Young’s modulus of approximately 200 GPa, while aluminum has 70 GPa. This means steel is about three times stiffer than aluminum for the same dimensions.

    What is a stress-strain curve?

    A stress-strain curve graphically represents how metal responds to increasing tensile load. The curve shows elastic region (linear, reversible deformation), yield point (transition to permanent deformation), plastic region (permanent deformation with work hardening), ultimate tensile strength (maximum stress), and fracture point (failure). The curve’s shape reveals key mechanical properties.

    How are mechanical properties of metals tested?

    Mechanical properties are tested through standardized methods: tensile testing (ASTM E8) for strength and ductility, hardness testing (ASTM E10/E18) for surface resistance, impact testing (ASTM E23) for toughness, fatigue testing (ASTM E466) for cyclic loading resistance, and creep testing (ASTM E139) for high-temperature deformation. Standards ensure consistent, comparable results.

    What affects the mechanical properties of metals?

    Mechanical properties are affected by composition (alloying elements), heat treatment (annealing, quenching, tempering), temperature (most metals lose strength when hot, become brittle when cold), working processes (cold working increases strength but reduces ductility), and microstructure (grain size, phases). These factors allow engineers to tailor properties for specific applications.

    What is fatigue resistance in metals?

    Fatigue resistance is a metal’s ability to withstand cyclic loading without failure. Fatigue failures occur at stresses below yield strength after thousands or millions of loading cycles. Steel has a fatigue limit (endurance limit) below which infinite life is possible. Aluminum lacks a true fatigue limit and will eventually fail under any cyclic stress amplitude.

  • Projection Weld Symbols Explained for 2026 Applications

    Projection Weld Symbols Explained for 2026 Applications

    When I first started reading welding blueprints, projection weld symbols looked like a foreign language. The tiny circles, crosses, and arrows seemed confusing compared to straightforward groove weld symbols. After working with resistance welding specifications for over 15 years, I’ve learned that projection weld symbols are actually quite logical once you understand the pattern.

    A projection weld symbol is a standardized graphical symbol used on engineering drawings and blueprints to specify projection welding, a resistance welding process where welds are created at pre-formed projections or embossments on mating parts. The symbol communicates weld location, size, quantity, and processing specifications required for manufacturing.

    Projection welding relies on current concentration at designed projection points rather than electrode-defined locations like spot welding. I’ve seen this process used extensively in automotive manufacturing and sheet metal assembly where multiple welds must be made simultaneously with consistent quality.

    Understanding Projection Welding

    Projection welding creates welds at pre-formed projections or embossments on one or both workpieces. When current flows through the joint, these projections concentrate the electrical current and heat, allowing multiple welds to form simultaneously under electrode pressure.

    Quick Summary: Projection welding uses embossed projections on the workpiece to concentrate welding current. The process creates multiple welds in a single cycle, making it faster than spot welding for production applications.

    Projection weld symbols indicate the resistance welding process where the weld location is determined by designed projections, not electrode placement. This distinction matters because the symbol tells the welder that joint preparation (creating the projections) happens before welding occurs.

    The embossments can be created through stamping, machining, or coining operations. I’ve worked with projections ranging from 0.5mm to 3mm in height, depending on material thickness and welding equipment capacity. The symbol specifies the weld requirements, but the projection design is typically detailed in separate notes or specifications.

    AWS A2.4 Standard Reference

    AWS A2.4: The American Welding Society standard titled “Standard Symbols for Welding, Brazing, and Nondestructive Examination.” This document defines all welding symbols used in North America, including projection weld symbols, and provides rules for their application on technical drawings.

    The AWS A2.4 standard governs projection weld symbols in North America. This specification establishes the uniform method for specifying welded joints on drawings, ensuring clear communication between design engineers and welding personnel. I keep a current copy of A2.4 in my office because symbol interpretations can change between editions.

    ISO 2553 serves a similar purpose internationally, with some notable differences in symbol appearance and notation. For this guide, I’ll focus on AWS A2.4 conventions since they’re most common in North American manufacturing. However, I’ve worked with international blueprints and noted that projection symbols remain relatively consistent across standards.

    The current edition of AWS A2.4 provides detailed rules for symbol placement, dimensioning, and supplementary information. Understanding this standard helps prevent misinterpretation that could lead to costly welding errors.

    Anatomy of a Projection Weld Symbol

    Every projection weld symbol consists of several key components that work together to convey complete welding instructions. Let me break down each element from my experience reading thousands of welding prints.

    The complete weld symbol assembly includes a reference line, an arrow line, the weld symbol itself, dimensions, and optional supplementary information. Each component has a specific position and meaning defined by AWS A2.4.

    Projection Weld Symbol Structure

    TAIL
    X
    ARROW
    Reference Line (horizontal) | Arrow points to weld joint | Symbol shows weld type

    Reference Line

    The reference line is the horizontal foundation of the welding symbol. All other elements attach to or position relative to this line. The reference line serves as the anchor point for symbol placement and determines whether the weld is on the arrow side or other side of the joint.

    In my experience, the reference line is the most critical component to understand because symbol positioning relative to this line determines weld location. Weld symbols below the reference line indicate arrow-side welds, while symbols above indicate other-side welds.

    Arrow and Arrow Side

    The arrow connects the reference line to the weld joint and indicates which side is the “arrow side.” The arrow side designation matters because it determines where the symbol should be placed relative to the reference line.

    The arrow side is the joint side toward which the arrow points. When the projection weld symbol appears below the reference line, the weld is on the arrow side. When it appears above, the weld is on the other side (the side opposite the arrow).

    Tail

    The tail is the optional element extending from the opposite end of the reference line from the arrow. When present, the tail contains reference information, specifications, or process notes that apply to the weld.

    I’ve seen tails used for various purposes: specifying welding processes, referencing standards, indicating weld sequence, or providing supplementary notes. An empty tail (no text) has no meaning and can be omitted. The tail should only be included when it contains essential information.

    Projection Weld Symbol

    The projection weld symbol itself consists of a circle with a cross or dot in the center, resembling a target. This symbol appears either above or below the reference line depending on weld location.

    Projection Weld Symbol

    +

    AWS A2.4 Symbol

    X

    Alternative Symbol

    This emblem distinguishes projection welding from other resistance welding processes. Spot welding uses a different symbol (a simple circle), and seam welding has its own designation. The projection symbol’s crossed circle makes it immediately identifiable on drawings.

    Dimensions and Specifications

    Dimensional information appears around the weld symbol in specific positions. The size (diameter) of each projection weld typically appears to the left of the symbol, while the number of welds may appear in parentheses or in the tail.

    Pitch spacing (distance between weld centers) is sometimes specified when multiple projection welds are arranged in a pattern. I’ve seen pitch dimensions placed below the reference line for arrow-side welds or above for other-side welds, depending on the drawing standard being followed.

    Dimension Placement Reference

    Location Information
    Left of symbol Weld size (diameter)
    Right of symbol Length (if applicable)
    In parentheses Number of welds
    In tail Process, specification reference

    How to Read Projection Weld Symbols?

    Reading projection weld symbols follows a systematic process that I’ve taught to welding students and inspection personnel. Here’s my step-by-step approach for interpreting any projection weld symbol correctly.

    Quick Summary: Start at the arrow, identify the weld side from symbol position, read dimensions left-to-right, check the tail for specifications, and verify supplementary symbols. Follow this order every time for consistent interpretation.

    1. Locate the arrow – Find which joint the arrow points to and identify the arrow side of the joint
    2. Check symbol position – Symbol below the line means arrow-side weld; above means other-side weld
    3. Read size dimension – Look left of the symbol for weld diameter or size
    4. Check for quantity – Look for numbers in parentheses indicating multiple welds
    5. Examine the tail – Review any reference information or specifications
    6. Note supplementary symbols – Check for contour, finish, or other special symbols
    7. Verify against drawing notes – Cross-reference with general notes or specifications

    Arrow Side vs Other Side Placement

    Symbol position relative to the reference line is the most critical factor in determining weld location. This is where I see most interpretation errors occur on the shop floor.

    Symbol Position Guide

    BELOW Reference Line = Arrow Side

    The weld is made on the side of the joint toward which the arrow points. This is the most common placement for projection weld symbols.

    ABOVE Reference Line = Other Side

    The weld is made on the side opposite the arrow. The arrow points to one side, but the weld occurs on the reverse side.

    I’ve found it helpful to physically point at the drawing and trace the arrow to the joint, then flip my finger to the opposite side if the symbol is above the reference line. This simple physical action prevents the mental slip of misidentifying the weld side.

    Multiple Projection Welds

    Projection welding’s advantage is making multiple welds simultaneously. Symbols often indicate multiple projections through quantity designations and pattern information.

    The number of welds typically appears in parentheses near the symbol: (6) indicates six projection welds. When multiple welds are arranged in a pattern, the drawing may include a separate detail view showing projection locations and spacing.

    I’ve worked with automotive subassemblies where a single symbol represented 12-16 projection welds made in one cycle. The symbol specified the weld size and quantity, while a separate detail showed the exact projection layout.

    Spot Weld vs Projection Weld Symbols

    Spot welding and projection welding are both resistance welding processes, but their symbols differ in important ways. I’ve seen these symbols confused many times, leading to process errors.

    Symbol Comparison Table

    Characteristic Spot Weld Symbol Projection Weld Symbol
    Symbol Shape Simple circle Circle with cross or dot
    Weld Location Determined by electrode position Determined by part projections
    Process Type Single weld per electrode contact Multiple welds possible per cycle
    Typical Use Sheet metal overlap joints Assemblies with embossed projections
    Joint Preparation None required Requires formed projections

    Visual Symbol Comparison

    Spot Weld

    Simple circle

    +

    Projection Weld

    Crossed circle

    The key difference I look for is the cross or dot inside the circle. This internal element identifies the symbol as a projection weld rather than a spot weld. Missing this distinction has caused more than one fabrication error in shops I’ve visited.

    Common Applications and Industries

    Projection welding appears in various manufacturing applications where multiple welds must be made efficiently. I’ve encountered projection weld symbols in several industries:

    Automotive

    Body structural components, brackets, subassemblies

    Electronics

    Enclosure assemblies, chassis components, grounding points

    Appliances

    Cabinet frames, mounting brackets, hardware attachment

    Sheet Metal

    Stamped assemblies, welded nuts and studs, fastener attachment

    Weld nuts and weld studs represent common projection welding applications. The threaded fastener itself has built-in projections that create the weld points when resistance welding equipment applies current and pressure.

    I’ve worked extensively with automotive applications where projection welding joins brackets to body panels. The process allows multiple attachment points in a single cycle, dramatically improving production efficiency compared to individual spot welds.

    Frequently Asked Questions

    What is a projection weld symbol?

    A projection weld symbol is a standardized graphical symbol on engineering drawings that specifies projection welding. It consists of a circle with a cross or dot in the center, placed on a reference line with an arrow pointing to the weld joint. The symbol indicates that welds will be created at pre-formed projections on the workpiece rather than at electrode contact points.

    How do you read projection weld symbols?

    Read projection weld symbols by starting at the arrow and identifying which joint it points to. Check if the symbol appears below (arrow side) or above (other side) the reference line. Read dimensions left of the symbol for weld size. Look for numbers in parentheses indicating multiple welds. Check the tail for process specifications. Verify against drawing notes and general specifications.

    What is the difference between spot weld and projection weld symbols?

    Spot weld symbols use a simple circle, while projection weld symbols use a circle with a cross or dot inside. Spot welding location is determined by electrode placement, while projection welding location is determined by pre-formed projections on the part. Projection welding can create multiple welds in one cycle, whereas spot welding typically creates one weld per electrode contact.

    What does the arrow side mean on a weld symbol?

    The arrow side is the joint side toward which the arrow points. When the weld symbol appears below the reference line, the weld is made on the arrow side. When the symbol appears above the reference line, the weld is made on the other side (opposite the arrow). This positioning convention applies to all welding symbols per AWS A2.4 standard.

    What is AWS A2.4 standard?

    AWS A2.4 is the American Welding Society standard titled “Standard Symbols for Welding, Brazing, and Nondestructive Examination.” It establishes the uniform system for specifying welded joints on technical drawings used in North America. The standard defines symbol shapes, dimensions, placement rules, and supplementary information formats for all welding processes including projection welding.

    Where are projection welds typically used?

    Projection welds are commonly used in automotive manufacturing for body components and brackets, electronics for chassis and enclosures, appliance manufacturing for cabinet frames, and sheet metal fabrication for attaching weld nuts and studs. The process excels when multiple welds are needed in a consistent pattern and when production speed is critical.

  • Physical Weld Testing Techniques for Reliable Welds in 2026

    Physical Weld Testing Techniques for Reliable Welds in 2026

    Physical weld testing is the systematic evaluation of welded joints to ensure they meet quality standards and performance requirements. Testing verifies weld integrity, detects defects, and confirms that welding procedures produce sound, reliable welds capable of withstanding service conditions.

    After spending 10 years in quality control, I’ve seen weld testing prevent catastrophic failures in pressure vessels, bridges, and pipelines. The difference between a safe weld and a disaster often comes down to proper testing procedures.

    Physical weld testing encompasses two main categories: destructive testing, which destroys test specimens to measure mechanical properties, and non-destructive testing (NDT), which examines welds without damage. Both approaches are essential for comprehensive weld quality assurance in modern fabrication.

    What is Physical Weld Testing?

    Physical weld testing serves multiple critical purposes in welding fabrication. It validates welding procedures before production begins, qualifies welders to ensure they can produce sound welds, and provides quality control for production welds in critical applications.
    The testing method you choose depends on factors like the welding code governing your work, the service conditions of the welded component, material thickness, joint configuration, and budget constraints. Pressure vessels typically require extensive NDT, while structural steel may rely more on visual inspection with targeted destructive testing for qualification.

    Types of Physical Weld Testing

    Physical weld testing methods fall into two primary categories based on whether the test destroys the weld specimen:

    Destructive Testing Methods:

    • Tensile testing – measures ultimate tensile strength and ductility
    • Bend testing – evaluates ductility and fusion quality
    • Impact testing – assesses toughness using Charpy V-notch specimens
    • Nick break testing – reveals internal fusion and weld soundness
    • Fillet weld break testing – examines root penetration in fillet welds
    • Macro etching – reveals weld cross-section structure and fusion

    Non-Destructive Testing Methods:

    • Visual inspection (VT) – surface examination using eyes and tools
    • Radiographic testing (RT) – internal imaging using X-ray or gamma ray
    • Ultrasonic testing (UT) – internal flaw detection using sound waves
    • Magnetic particle testing (MT) – surface/subsurface flaw detection
    • Liquid penetrant testing (PT) – surface-breaking defect detection
    • Eddy current testing (ET) – surface and near-surface flaw detection

    Destructive vs. Non-Destructive Testing Comparison

    FactorDestructive TestingNon-Destructive Testing
    Specimen FateDestroyed during testingRemains usable after testing
    Information GainedMechanical properties (strength, ductility, toughness)Defect detection, size, and location
    Primary UseProcedure and welder qualificationProduction weld inspection
    CostLower equipment cost, specimen preparation requiredHigher equipment cost, minimal preparation
    Time RequiredHours to days (including preparation)Minutes to hours per weld
    PersonnelTesting technicianCertified NDT Level II/III required

    The key difference between destructive and non-destructive testing is their purpose. Destructive tests provide definitive data about weld metal mechanical properties but destroy the specimen in the process. NDT methods detect internal and external defects without damaging the weld, allowing 100% inspection of production welds when required by code or specification.

    Destructive Testing Methods

    Tensile Testing

    Tensile testing measures the strength and ductility of welded joints by pulling a specimen apart in a controlled manner. The test reveals ultimate tensile strength, yield strength, elongation, and reduction of area – all critical properties for evaluating weld performance.

    Quick Summary: Tensile testing determines if weld metal matches or exceeds base metal strength. The specimen is loaded in tension until failure, with the maximum load recorded and converted to tensile strength using the original cross-sectional area.

    How Tensile Testing Works:

    1. Cut test specimen from welded joint per code requirements
    2. Measure and record original dimensions (gauge length, cross-sectional area)
    3. Mount specimen in tensile testing machine with proper alignment
    4. Apply increasing tensile load until failure occurs
    5. Record maximum load and calculate ultimate tensile strength
    6. Measure elongation and reduction of area for ductility assessment
    7. Compare results to acceptance criteria in applicable code

    Per ASTM E8/E8M, tensile specimens typically measure the weld metal transverse to the welding direction. The specimen fails in the weld metal if the weld is weaker than the base metal, which indicates potential issues with filler metal selection, welding procedure, or workmanship.

    I’ve tested hundreds of tensile specimens throughout my career. The most common failure mode I see is weld metal failure when using undermatched filler – a critical error in procedure qualification that can lead to field failures if not caught during testing.

    Bend Testing

    Bend testing evaluates ductility and fusion quality by bending a welded specimen to a specified radius. The test reveals lack of fusion, slag inclusions, porosity, and other defects that might not be visible on the surface but become apparent when the weld is stressed.

    Types of Bend Tests:

    • Root bend: Tests the root side of the weld for fusion and penetration
    • Face bend: Tests the weld face for surface and sub-surface defects
    • Side bend: Tests the entire weld cross-section (most common for thicker materials)
    • Guided bend: Uses a fixture with specific radius – per ASTM E190
    • Free bend: Bends specimen without a die – less controlled but simpler

    Acceptance Criteria: Per ASME Section IX and AWS D1.1, a bend test passes if no open defects exceed 1/8 inch (3mm) in any direction during bending. Cracks at specimen corners are typically disregarded unless they result from slag inclusions or other weld defects.

    Side bend tests are particularly useful for thicker materials where surface bend tests might not reveal defects in the weld center. During a project I managed on 2-inch plate, side bend testing detected central lack of fusion that would have been missed by face and root bends alone.

    Impact Testing (Charpy V-Notch)

    Impact testing measures toughness – the ability of weld metal to absorb energy and deform plastically before fracturing. The Charpy V-notch test, specified in ASTM E23, is the standard method for evaluating weld metal and heat-affected zone toughness, especially for low-temperature service.

    During a Charpy test, a notched specimen is struck by a pendulum hammer, and the energy absorbed in breaking the specimen is measured in foot-pounds or joules. The V-notch creates a stress concentration that simulates defects in the weld.

    Temperature matters significantly for impact testing. Tests are conducted at specified temperatures (often below freezing for arctic applications) to ensure weld toughness under worst-case service conditions. I’ve seen qualified procedures fail when tested at lower temperatures than originally specified.

    What Impact Testing Reveals:

    • Ductile-to-brittle transition temperature
    • Sensitivity to notches and defects
    • Effect of welding heat input on toughness
    • Heat-affected zone embrittlement
    • Suitability for low-temperature service

    Nick Break Testing

    Nick break testing fractures a weld specimen to examine the internal fracture surface for fusion quality, slag inclusions, porosity, and other internal discontinuities. The test provides a visual examination of weld soundness without sophisticated equipment.

    The specimen is notched at the weld centerline and bent to fracture, revealing the internal structure. A sound weld shows a fibrous, silvery fracture surface with consistent texture. Defects appear as dark spots, smooth areas (lack of fusion), or embedded slag particles.

    Nick break testing is particularly useful for fillet weld qualification and troubleshooting weld defects. I’ve used it extensively to diagnose lack of fusion issues in pipe welding – the fracture surface clearly shows where the weld metal didn’t fuse to the sidewall.

    Macro Etching

    Macro etching reveals the weld cross-sectional structure by polishing and etching a specimen to show weld zones, fusion lines, penetration depth, and potential defects. The etched specimen displays the heat-affected zone, weld metal, base metal, and any discontinuities.

    The process involves sectioning the weld, polishing the cross-section to a mirror finish, and etching with an acid solution (typically nitric or hydrochloric acid for steel). Different microstructures etch at different rates, creating contrast between zones.

    Purpose
    Structure Analysis
    What It Shows
    Fusion Lines
    Common Etchants
    Nital, HCl
    Specimen Prep
    Polished Cross-section

    Macro etching is invaluable for procedure development and troubleshooting. It reveals exactly how deep the weld penetrated, whether fusion is complete at the groove faces, and how the weld beads relate to each other in multi-pass welds.

    Non-Destructive Testing Methods Overview

    Non-destructive testing allows inspection of production welds without damage, enabling 100% inspection when required by code or specification. NDT methods detect internal and external defects while leaving the weld intact for service.

    NDT MethodWhat It DetectsBest ApplicationsLimitations
    Visual (VT)Surface defects onlyAll welds, first line of defenseCannot see below surface
    Radiographic (RT)Internal volumetric defectsPressure vessels, piping, critical weldsRadiation safety, planar defects difficult
    Ultrasonic (UT)Internal flaws, laminationThick sections, cracks, lack of fusionRequires skilled operator, surface prep
    Magnetic Particle (MT)Surface/subsurface flaws (ferrous only)Surface cracks in welds and HAZFerromagnetic materials only
    Liquid Penetrant (PT)Surface-breaking defectsNon-ferrous, stainless, all metalsSurface defects only, clean surface needed
    Eddy Current (ET)Surface/near-surface flawsTube and pipe welds, heat exchangersLimited depth, calibration critical

    Visual Inspection (VT)

    Visual inspection is the most fundamental and widely used weld testing method. It requires no expensive equipment beyond good lighting, proper inspection tools, and a trained eye. Despite its simplicity, visual inspection detects the majority of weld defects when performed properly.

    AWS B1.11: The American Welding Society’s Guide for the Visual Examination of Welds provides comprehensive guidance on visual inspection procedures, acceptance criteria, and documentation requirements for welded joints.

    Visual Inspection Tools:

    • High-intensity flashlight or inspection lamp
    • Weld gauges (fillet, hi-lo, bridge cam)
    • Measuring tape and calipers
    • Borescope for internal weld inspection
    • Magnifying glass for small defects
    • Mirror for hard-to-see areas
    • Surface comparators and profile gauges

    Visual inspection should occur before, during, and after welding. Pre-weld inspection verifies joint preparation, fit-up, and cleanliness. In-process inspection monitors welding parameters and technique. Post-weld inspection evaluates the completed weld against acceptance criteria.

    Radiographic Testing (RT)

    Radiographic testing uses X-rays or gamma rays to create an image of the weld’s internal structure. Radiation passes through the weld, with denser areas (defect-free weld metal) absorbing more radiation and less dense areas (porosity, slag) allowing more to pass through.

    The resulting radiograph shows the weld as a shadow image where defects appear as dark areas against lighter weld metal. Radiographic testing excels at detecting volumetric defects like porosity, slag inclusions, and voids, but has difficulty detecting tight cracks perpendicular to the radiation beam.

    I’ve used radiographic testing extensively on pressure vessel and pipeline projects. The permanent radiograph record provides excellent documentation and allows for review by multiple parties, including engineers and inspectors who weren’t present during the original inspection.

    Radiography Advantages:

    • Permanent record of weld internal structure
    • Excellent for detecting porosity and slag inclusions
    • Can inspect full penetration welds in one shot
    • Minimal surface preparation required
    • Well-established acceptance criteria in all major codes

    Ultrasonic Testing (UT)

    Ultrasonic testing uses high-frequency sound waves to detect internal flaws. A transducer sends sound waves into the weld, and reflections from defects or back wall indicate the presence, location, and size of discontinuities.

    UT excels at detecting planar defects like cracks and lack of fusion – defects that radiography often misses. The method provides precise depth sizing and can inspect thick materials that would require multiple radiographic shots.

    Modern phased array ultrasonic testing (PAUT) uses multiple transducer elements to create focused beams that can be steered electronically. This provides faster inspection and better imaging of complex geometries compared to conventional UT.

    Pressure Vessels
    Pipelines
    Thick Plate
    Crack Detection

    UT requires highly trained personnel and careful calibration. The interpretation of ultrasonic signals is subjective, and inspection results can vary between operators. Despite these challenges, UT remains indispensable for critical applications where crack detection is essential.

    Magnetic Particle Testing (MT)

    Magnetic particle testing detects surface and near-surface discontinuities in ferromagnetic materials. The method magnetizes the test piece, then applies iron particles that accumulate at leakage fields caused by defects.

    The iron particles may be applied dry or suspended in a liquid (wet method). Wet fluorescent magnetic particle testing provides the highest sensitivity, especially for fine cracks, using black light to reveal particle accumulations.

    MT is ideal for detecting surface cracks in welds and heat-affected zones, including fatigue cracks, stress corrosion cracks, and hot cracks. It’s faster and more sensitive to surface defects than penetrant testing on ferrous materials.

    Liquid Penetrant Testing (PT)

    Liquid penetrant testing detects surface-breaking defects in any non-porous material. A colored or fluorescent penetrant is applied to the clean surface, allowed to enter defects, excess is removed, and a developer draws the penetrant out to create visible indications.

    PT works on all metals – ferrous and non-ferrous – as well as ceramics and plastics. It’s particularly useful for stainless steel welds and non-ferrous alloys where magnetic particle testing cannot be used.

    The key to reliable PT results is thorough surface cleaning. Any oil, grease, paint, or contamination can block penetrant entry or cause false indications. I’ve seen many false positives and missed defects due to inadequate surface preparation.

    Testing Standards and Codes

    Physical weld testing requirements are governed by codes and standards that specify qualification procedures, acceptance criteria, and inspection methods. The applicable code depends on the industry, product type, and jurisdiction.

    ASME Section IX

    ASME Boiler and Pressure Vessel Code Section IX specifies welding qualification requirements for pressure vessels and piping. It outlines procedure qualification (PQR), welding procedure specification (WPS), and welder performance qualification (WPQ) requirements.

    Section IX QW-140 through QW-180 detail destructive testing requirements, including tensile testing (QW-150), bend testing (QW-160), and impact testing (QW-170). The code specifies specimen dimensions, testing methods, and acceptance criteria for each test type.

    For NDT, ASME Section V provides rules for examination methods, while various ASME construction sections (Section I for power boilers, Section VIII for pressure vessels, B31.1/B31.3 for piping) specify which NDT methods to use and the required extent of examination.

    AWS D1.1

    AWS D1.1 Structural Welding Code – Steel governs welding in structural steel construction. The code specifies qualification testing, inspection requirements, and acceptance criteria for statically and cyclically loaded structures.

    D1.1 Chapter 4 covers qualification, including tensile and bend testing requirements for procedure and welder qualification. Chapter 5 covers fabrication, including inspection and acceptance criteria for production welds.

    API 1104

    API 1104 Welding of Pipelines and Related Facilities provides requirements for welding qualification and inspection in oil and gas pipeline construction. The code specifies destructive testing for procedure qualification and NDT methods for production weld inspection.

    ASTM Test Methods

    ASTM International provides standard test methods referenced by welding codes:

    • ASTM E8/E8M – Tension Testing of Metallic Materials
    • ASTM E190 – Guided Bend Test for Welds
    • ASTM E23 – Notched Bar Impact Testing
    • ASTM E165 – Liquid Penetrant Examination
    • ASTM E709 – Magnetic Particle Examination
    • ASTM E94 – Guide for Radiographic Examination
    • ASTM E164 – Ultrasonic Examination

    Common Weld Defects Detected

    Defect TypeDescriptionDetection Methods
    PorosityGas pockets trapped in weld metalRT, UT, Visual (surface)
    Slag InclusionsEntrapped flux or slagRT, UT, Macro etch, Bend
    Lack of FusionWeld metal didn’t fuse to base metal or previous passUT (best), RT (limited), Bend, Nick break
    Incomplete PenetrationWeld didn’t fully penetrate joint rootRT, UT, Macro etch, Visual (root)
    UndercutGroove melted into base metal at weld toeVisual, MT, PT
    CracksVarious types (hot, cold, stress corrosion, fatigue)UT (best), MT, PT, RT (some types)
    OverlapWeld metal rolls over base without fusionVisual, MT, PT
    Surface IrregularitiesExcessive spatter, rough surface, arc strikesVisual, MT, PT

    Choosing the Right Testing Method

    Quick Summary: Select testing methods based on code requirements, service conditions, material type, joint accessibility, and budget. Destructive testing qualifies procedures and welders. NDT inspects production welds. Start with visual inspection, then add NDT methods as required by code or service conditions.

    Consider these factors when selecting testing methods:

    1. Code Requirements: Your governing code (ASME, AWS, API) will specify required tests for qualification and production inspection. Always verify code requirements first.
    2. Service Conditions: Critical applications (pressure vessels, high-rise buildings, pipelines) require more extensive testing than non-critical applications. Low-temperature service requires impact testing.
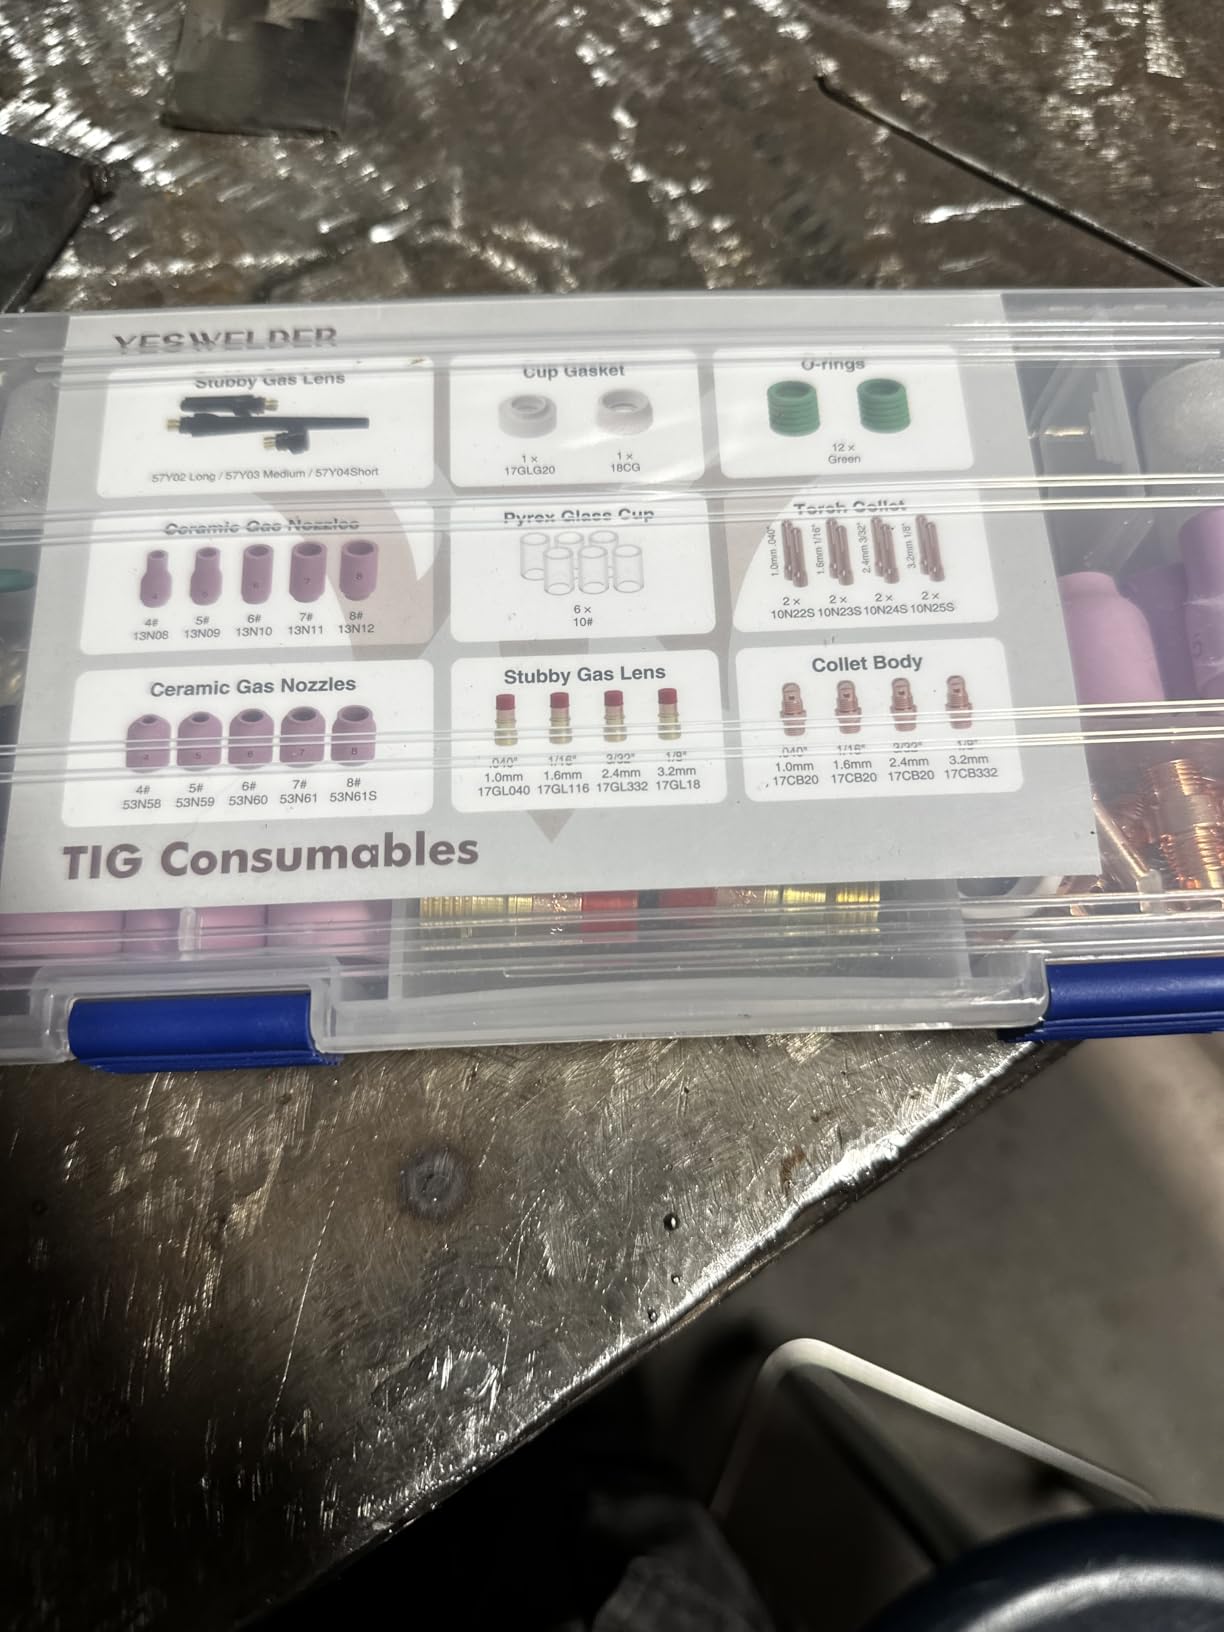
    3. Material Type and Thickness: Thick materials benefit from UT for deep flaw detection. Non-ferrous materials require PT instead of MT. Thin materials may radiograph well.
    4. Joint Accessibility: One-sided access may limit testing options. Complex geometries may require specialized NDT methods like PAUT.
    5. Cost Considerations: Visual inspection is most economical. RT and UT require significant equipment and training investment. Balance testing cost with consequence of failure.
    6. Inspection Extent: Code may require 100% inspection for certain welds or statistical sampling for others. This affects NDT method selection.

    Cost Comparison: Visual inspection costs approximately $5-20 per weld depending on complexity. Liquid penetrant runs $15-40. Magnetic particle costs $20-50. Ultrasonic testing costs $50-150 per weld. Radiographic testing is most expensive at $100-400 per weld depending on setup and shot requirements. These costs vary by region, shop rate, and job complexity.

    Test Preparation Procedures

    Proper test specimen preparation is critical for accurate results. Specimens must be cut, machined, and prepared according to code requirements to ensure valid test data.

    Specimen Preparation Steps:

    1. Identify specimen locations per code requirements
    2. Cut specimens using methods that won’t affect test results (thermal cutting requires additional material removal)
    3. Machine specimens to specified dimensions
    4. Remove surface defects that could cause premature failure
    5. Mark specimens for identification and orientation
    6. Store specimens properly to prevent damage before testing

    For NDT, surface preparation includes removing weld spatter, cleaning surfaces, and ensuring proper access for the inspection method. Inadequate surface preparation is the leading cause of false indications and missed defects.

    Interpreting Test Results

    Interpreting weld test results requires knowledge of acceptance criteria, defect types, and their significance. Not all discontinuities are rejectable defects – codes distinguish between acceptable and unacceptable based on size, type, and location.

    Key Principles of Result Interpretation:

    • Compare results against applicable code acceptance criteria
    • Consider defect type – cracks are almost always unacceptable
    • Evaluate defect size and location relative to code limits
    • Assess defect orientation relative to applied stresses
    • Review trend data – multiple similar defects may indicate systemic issues

    When welds fail testing, investigate root causes before attempting repairs. Common causes include improper welding parameters, inadequate joint preparation, incorrect filler metal, environmental conditions, or welder technique. Address the underlying issue to prevent recurring failures.

    Welder Certification Requirements

    Welder certification (performance qualification) demonstrates that a welder can produce sound welds following a qualified procedure. Certification typically involves welding test coupons, then subjecting them to specified destructive or NDT examinations.
    Per ASME Section IX and AWS D1.1, welder certification remains valid as long as the welder remains actively employed in welding. However, certification can be revoked for specific reasons including welds failing radiographic or mechanical testing, excessive repair rates, or not welding for a specified period (typically 6 months or more).

    Visual inspection of the test weld evaluates workmanship factors including bead appearance, uniformity, lack of visible defects, and proper weld size. This visual assessment often occurs alongside mechanical testing.

    FAQ: Physical Weld Testing

    What is the difference between destructive and non-destructive testing?

    Destructive testing destroys the weld specimen to evaluate mechanical properties like tensile strength, ductility, and toughness. It provides definitive data on weld performance but destroys the test piece. Non-destructive testing (NDT) examines welds without damage, detecting internal and external defects. NDT allows 100% inspection of production welds but requires specialized equipment and trained personnel.

    How do you perform a tensile test on a weld?

    To perform a tensile test, first cut a test specimen from the welded joint per code requirements. Measure and record original dimensions including gauge length and cross-sectional area. Mount the specimen in a tensile testing machine with proper alignment. Apply increasing tensile load until failure occurs. Record the maximum load and calculate ultimate tensile strength. Measure elongation and reduction of area, then compare results to acceptance criteria in the applicable code.

    What standards govern physical weld testing?

    Primary standards governing physical weld testing include ASME Section IX for welding qualification in pressure vessels and piping, AWS D1.1 for structural welding code for steel, and API 1104 for pipeline welding standards. ASTM standards including E8 for tensile testing, E190 for guided bend test, E23 for impact testing, E165 for liquid penetrant examination, and E709 for magnetic particle examination specify test methods referenced by welding codes.

    What equipment is needed for weld testing?

    Weld testing equipment varies by method. Visual inspection requires welding gauges, flashlights, and measuring tools. Destructive testing requires a tensile testing machine, bend fixtures, and impact tester. NDT requires specialized equipment including X-ray or gamma ray sources for radiography, ultrasonic flaw detectors for UT, magnetic particle yokes and power supplies for MT, and penetrant testing kits for PT. Many shops send specimens to independent testing laboratories rather than investing in all this equipment.

    How much does weld testing cost?

    Weld testing costs vary significantly by method and location. Visual inspection costs approximately $5-20 per weld. Liquid penetrant testing runs $15-40 per weld. Magnetic particle testing costs $20-50 per weld. Ultrasonic testing ranges from $50-150 per weld. Radiographic testing is most expensive at $100-400 per weld depending on setup and shot requirements. Destructive testing of qualification coupons typically costs $200-800 including specimen preparation and testing. Costs vary by region, shop rates, and job complexity.

    What are welder certification requirements?

    Welder certification requires welding test coupons following a qualified procedure, then subjecting the welds to specified examinations. Testing typically includes visual inspection plus either destructive testing (bend tests for groove welds, break tests for fillet welds) or NDT (radiography for many pipe welding certifications). Certification remains valid as long as the welder remains actively employed. Most codes require requalification if the welder hasn’t welded for 6 months or more, or if welds fail required testing.
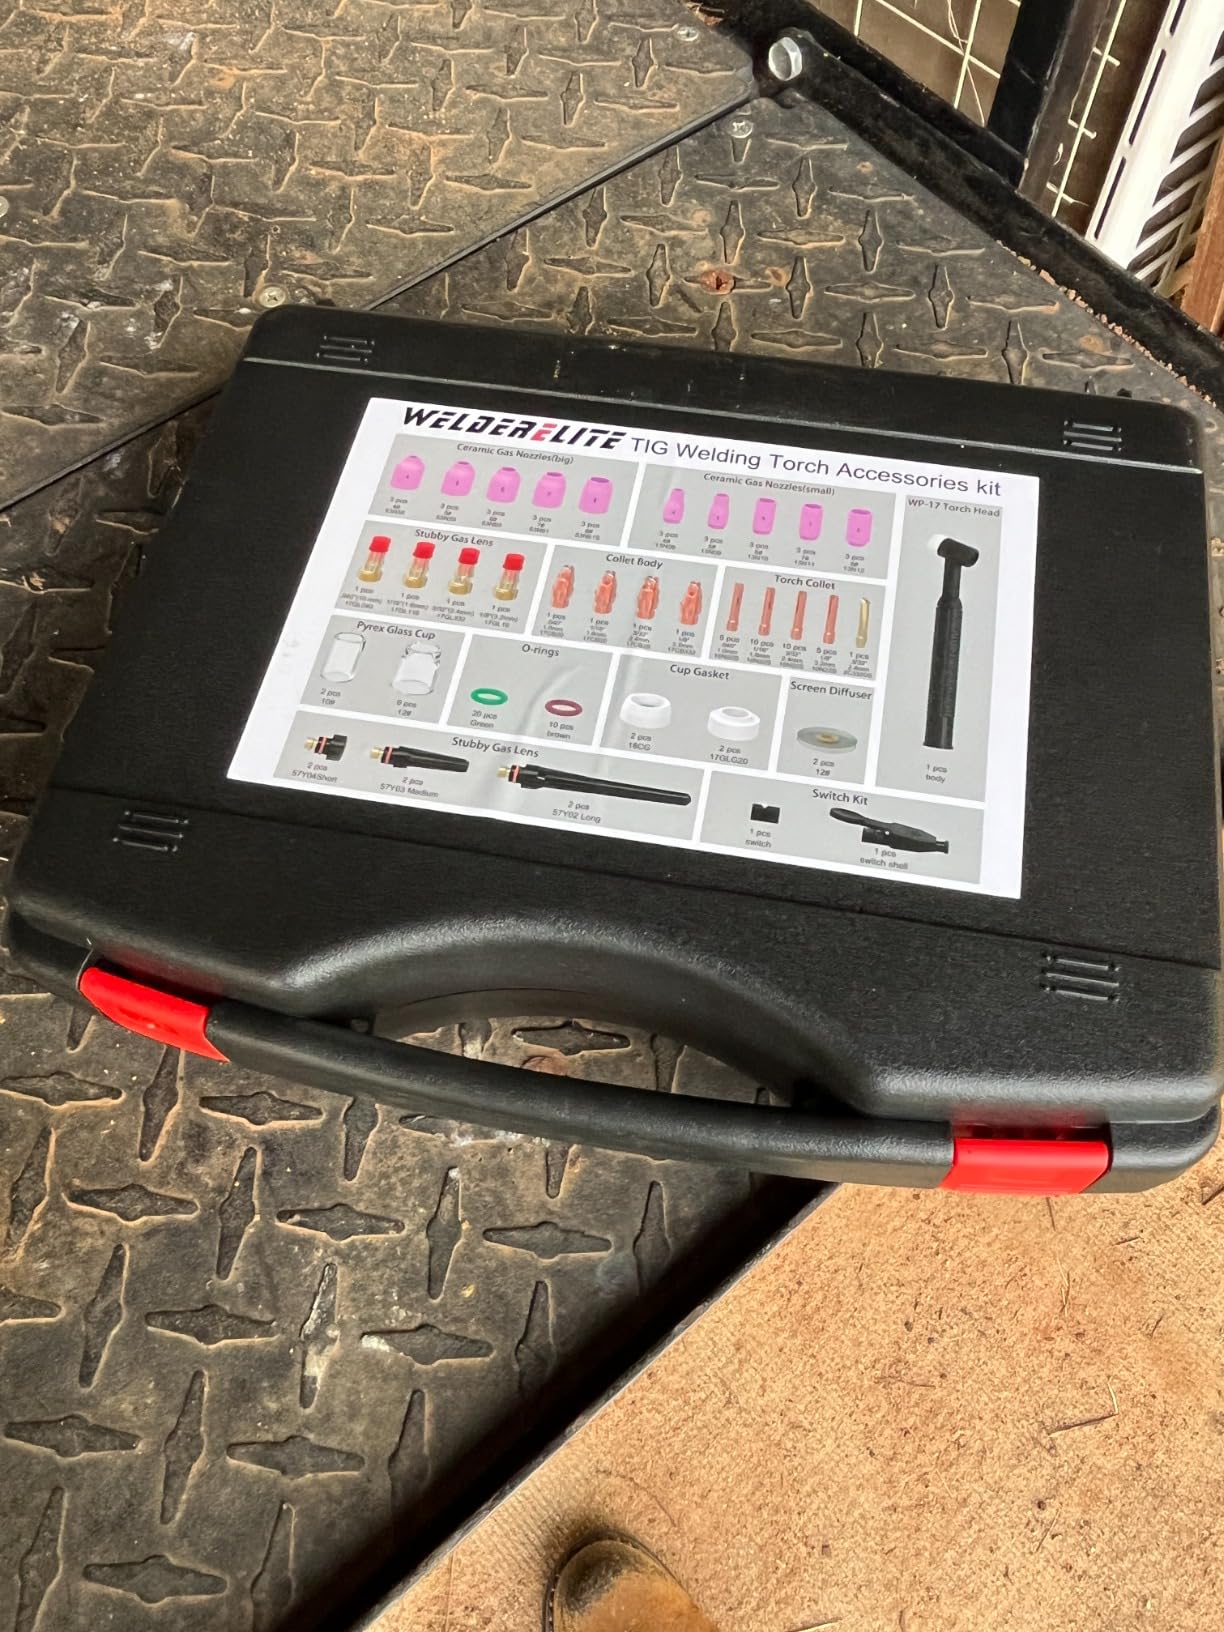
    How do you interpret test results?

    Interpreting test results requires comparing findings against acceptance criteria in the applicable code. Evaluate defect type, size, location, and orientation. Cracks are almost always unacceptable regardless of size. Porosity, slag inclusions, and other discontinuities are acceptable within specified size and frequency limits. Look for trends indicating systemic problems. When results fail acceptance, investigate root causes including procedure issues, improper parameters, joint preparation problems, or welder technique before attempting repairs.

    What is visual inspection in welding?

    Visual inspection is the examination of weld surfaces and accessible areas using eyesight augmented by tools like welding gauges, flashlights, and measuring instruments. It should occur before, during, and after welding. Pre-weld inspection verifies joint preparation and fit-up. In-process inspection monitors technique. Post-weld inspection evaluates the completed weld against acceptance criteria for size, profile, and surface defects. Visual inspection detects the majority of weld defects and is required by all welding codes.

    What is the heat affected zone in welding?

    The heat affected zone (HAZ) is the base metal adjacent to the weld that wasn’t melted but was altered by welding heat. The HAZ experiences microstructural changes due to thermal cycling, which can affect mechanical properties including toughness and hardness. In some materials, the HAZ can be the weakest area of the welded joint. Impact testing often targets the HAZ to ensure it has adequate toughness, especially for low-temperature service. Macro etching reveals the HAZ clearly as the transition zone between weld metal and unaffected base metal.

    Can all weld defects be detected by testing?

    No single testing method detects all possible weld defects. Each method has limitations. Visual inspection sees only surface defects. Radiography excels at volumetric defects like porosity but misses tight cracks. Ultrasonic testing detects cracks and lack of fusion but requires skilled operators. Magnetic particle finds surface and near-surface defects in ferrous metals only. Liquid penetrant detects surface-breaking defects in all materials. Comprehensive inspection typically requires multiple methods to ensure all significant defect types are detected and evaluated.