Author: Walter McGuire

  • Copper Welding: Complete Guide to Methods & Techniques

    Copper Welding: Complete Guide to Methods & Techniques

    Copper welding frustrated me for years when I first started metalworking. Like many beginners, I watched my heat disappear into the material before the filler rod would even melt.

    What is the best way to weld copper? TIG welding with AC/DC output and argon shielding gas produces the highest quality copper welds for most applications, though MIG works for thicker sections and oxy-acetylene remains viable for repairs.

    After spending countless hours testing different methods on everything from thin copper sheet to 1/2-inch busbars, I’ve learned that copper welding isn’t mysterious—it just requires understanding how this unique metal behaves under heat. For those building industrial equipment with copper components, understanding these welding principles becomes essential.

    Why Copper is Difficult to Weld?

    Copper presents unique challenges that steel welders rarely encounter.

    The primary issue is thermal conductivity. Copper conducts heat about 8 times faster than steel, which means your welding heat dissipates rapidly into the surrounding material instead of staying concentrated in the weld zone.

    Thermal Conductivity: The ability of a material to conduct heat. Copper’s thermal conductivity of approximately 400 W/mK makes it one of the most thermally conductive metals, requiring significantly higher heat input for welding compared to steel.

    I learned this the hard way when trying to weld 1/4-inch copper plate without preheating. No matter how much amperage I threw at it, the heat kept spreading away from my weld joint.

    The solution arrived when an old fabricator showed me the power of proper preheating. Using various heat tools for metal preparation, we applied uniform heat across the workpiece. Within minutes, my welding arc finally gained control.

    Other copper welding challenges include:

    • Oxidation occurs rapidly when copper is heated
    • High thermal expansion causes warping and distortion
    • Low melting point (1983°F) means overheating happens quickly
    • Porosity from trapped gases and impurities

    Understanding these properties transforms copper welding from frustrating to manageable. Let me share what I’ve learned about selecting the right process.

    Copper Welding Methods Compared

    Different welding processes offer distinct advantages for copper work. I’ve tested each extensively and developed clear preferences based on application.

    Process Best Thickness Heat Control Difficulty Cost
    TIG (GTAW) Up to 1/4″ Excellent High $$
    MIG (GMAW) 1/8″ to 1/2+” Good Medium $$
    Stick (SMAW) 3/16″+ Poor Medium $
    Oxy-Acetylene Thin to medium Fair Low $

    TIG Welding Copper

    TIG welding produces the cleanest, most precise copper welds possible. I use it for nearly all my copper work under 1/4-inch thickness.

    The focused arc and precise heat control let me work on thin copper sheet without burn-through. AC/DC TIG machines provide maximum flexibility for switching between steel and copper projects. If you’re looking for comprehensive welding equipment guides, TIG machines offer the most versatility.

    Quick Summary: TIG welding offers the best control for copper welding, especially on thinner materials. Use DC electrode negative with pure argon gas, and increase amperage 20-30% compared to steel welding of the same thickness.

    For TIG welding copper, I recommend:

    • DCEN (DC Electrode Negative) polarity
    • 2% thoriated or lanthanated tungsten
    • Pure argon shielding gas at 15-20 CFH
    • ERCu or ERCuSi-A filler rod
    • 20-30% higher amperage than equivalent steel thickness

    On thin copper sheet (16 gauge and thinner), I run around 60-80 amps. For 1/8-inch material, I bump up to 120-150 amps depending on joint design and preheating.

    MIG Welding Copper

    MIG welding works well for thicker copper sections and production work where speed matters. I’ve found it especially useful for copper busbars and structural connections.

    Short-circuit transfer gives the best control for thinner materials, while spray transfer works for heavier sections. The key is using the right wire and gas combination.

    For MIG welding copper:

    • ERCu silicon bronze wire (most common)
    • Argon or 75/25 argon-helium mixture
    • Wire feed speed: 200-400 IPM depending on thickness
    • Voltage: 18-24 volts for most applications
    • Push angle technique helps with gas coverage

    Stick Welding Copper

    Stick welding copper is possible but challenging. I only recommend it for field repairs or when other equipment isn’t available.

    The difficulty comes from copper’s heat dissipation fighting against the stick arc. I’ve had the most success using specialized bronze rods designed for copper work.

    Oxy-Acetylene Welding Copper

    Gas welding remains relevant for copper, especially in HVAC and refrigeration work. I use oxy-acetylene for copper pipe repairs and brazing where electrical conductivity matters.

    The neutral flame provides good control without excessive oxidation. Phosphor bronze or brazing rods work well with this method.

    Preparation and Preheating

    Proper preparation makes or breaks copper welding success. I’ve learned that skipping any step in preparation wastes time later fixing defects.

    Cleaning Copper Before Welding

    Copper must be meticulously clean before welding. I use a specific process that never fails me:

    1. Mechanical cleaning with stainless steel wire brush to remove surface oxides
    2. Chemical cleaning with acetone or lacquer thinner to remove oils
    3. Immediate welding after cleaning (within 1-2 hours)

    For cutting copper to size before welding, quality metal cutting and preparation tools make the job significantly easier. Clean cuts with proper fit-up reduce the amount of welding needed later.

    For this cleaning step, I rely on quality wire brushes designed specifically for metal preparation.

    Never use the same brush on steel and copper—cross-contamination causes inclusions and poor weld quality. I keep dedicated brushes for copper work only.

    Preheating Copper for Welding

    Preheating is essential for most copper welding applications. I preheat anything over 1/8-inch thickness without exception.

    Copper Thickness Preheat Temperature Color Indicator
    Up to 1/16″ None required Natural color
    1/16″ to 1/8″ 200-300°F Faint straw
    1/8″ to 1/4″ 300-500°F Light straw
    1/4″ to 1/2″ 500-800°F Medium straw to brown
    Over 1/2″ 800-1200°F Dark brown to purple

    I use an infrared thermometer to verify temperature, but color indication works well with practice. The key is uniform heating across the workpiece, not just at the weld zone.

    For preheating, I use either a propane torch for smaller work or an oxy-acetylene setup for larger pieces. Some shops use heating blankets for consistency. Various metalworking heat tools can assist with preheating depending on your setup.

    Filler Materials Selection

    Choosing the right filler material dramatically affects weld quality and appearance. I’ve tested most options available and developed clear preferences.

    ERCu (Deoxidized Copper)

    Pure copper filler rod works best when color match is critical. I use ERCu when welding electrical connections where conductivity matters most.

    The welds color-match almost perfectly to the base metal after cleaning. However, ERCu requires high skill level and produces more fluid weld pools.

    ERCuSi-A (Silicon Bronze)

    Silicon bronze has become my go-to filler for most copper work. It flows beautifully, produces strong welds, and creates an attractive bronze finish.

    I especially like ERCuSi-A for TIG brazing and joining dissimilar metals. The silicon content improves wetting and reduces porosity.

    Silicon bronze is essential for any serious copper welding setup. I keep multiple diameters on hand for different applications.

    Phosphor Bronze (BCuP)

    Phosphor bronze rods are self-fluxing and work exceptionally well for HVAC and refrigeration applications. The phosphorus acts as built-in flux, eliminating the need for additional flux application.

    These rods create leak-free joints in copper piping and are ideal for repairs where gas or liquid sealing is critical.

    ERCuAl (Aluminum Bronze)

    For high-strength applications, aluminum bronze provides excellent mechanical properties. I use it when the welded joint needs to withstand high stress or corrosive environments.

    Essential Equipment for Copper Welding

    Having the right equipment makes copper welding significantly easier. I’ve tested numerous products and identified clear winners for different applications.

    YESWELDER TIG-205P – Best Budget TIG for Copper

    EDITOR'S CHOICE
    Product

    YESWELDER 205A Tig Welder Pulse STICK/DC TIG/PULSE TIG 3 in 1 TIG-205P

    ★★★★★★★★★★4.3 / 5

    Output: 200A DC

    Processes: TIG/Stick/Pulse TIG

    Voltage: 110/220V dual

    Weight: 10.7 lbs

    Display: Large LED

    Check Price

    + Pros

    • Pulse TIG for thin copper control
    • Lightweight portable design
    • High-frequency arc start
    • Dual voltage flexibility
    • Auto memory saves settings

    Cons

    • DC-only cannot weld aluminum
    • Ground clamp could be heavier
    • Manual lacks detailed guidance
    • Torch is integrated design
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The YESWELDER TIG-205P delivers impressive capability for the price point. I’ve tested it on copper projects ranging from 22 gauge sheet to 3/16-inch plate with consistent results.

    What stands out is the pulse TIG capability at this price point. Pulse functions help manage heat on thin copper sheet, preventing burn-through while ensuring proper fusion.
    YESWELDER 205A Tig Welder with Pulse Large LED Display, STICK/DC TIG/PULSE TIG 3 In 1, 110&220V Dual Voltage TIG Welding Machine TIG-205P - Customer Photo 2
    Customer submitted photo

    The 200-amp output handles most copper welding needs within its recommended thickness range. For pure copper over 1/4-inch, you’ll want a higher-amperage machine, but for most fabrication work, this TIG delivers.

    Customer photos show the actual LED display quality and compact size that makes this unit popular among home fabricators. The real-world images confirm the build quality exceeds expectations at this price.
    YESWELDER 205A Tig Welder with Pulse Large LED Display, STICK/DC TIG/PULSE TIG 3 In 1, 110&220V Dual Voltage TIG Welding Machine TIG-205P - Customer Photo 1
    Customer submitted photo

    The dual voltage capability lets you weld on 110V for thinner materials and 220V when you need full power. This flexibility proved invaluable when I brought it to a job site with only standard outlets available.

    High-frequency start eliminates the scratch-start technique that can contaminate tungsten. For copper work, clean arc starts are essential since tungsten contamination shows up clearly in the finished weld.

    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    YESWELDER MIG-205DS PRO – Most Versatile Multi-Process

    MOST VERSATILE
    Product

    YESWELDER 205A MIG Welder, 110V/220V 5-In-1 MIG/Flux Core MIG/Spool Gun MIG/Lift TIG/Stick

    ★★★★★★★★★★4.5 / 5

    Output: 200A

    Processes: 5-in-1 MIG/Flux/TIG/Stick

    Voltage: 110/220V dual

    Features: Synergic mode,Spool gun ready

    Display: Digital

    Check Price

    + Pros

    • 5-in-1 process capability
    • Synergic mode for beginners
    • Spool gun compatible
    • Digital current display
    • Excellent customer support

    Cons

    • Ground clamp quality basic
    • Wire feeder positioning awkward
    • Power cord warms at max output
    • Stick holder feels basic
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    The MIG-205DS PRO handles copper welding across multiple processes. I’ve used it for MIG welding copper busbars, TIG welding sheet, and even stick welding on repairs—all from the same machine.

    What impresses me most is the synergic mode. It automatically matches voltage to wire speed, making copper MIG welding much more predictable for operators still mastering the process.
    YESWELDER MIG-205DS PRO MIG Welder, 200Amp 110/220V Dual Voltage MIG Welding Machine, 5 in 1 Gas MIG/Flux Core MIG/Spool Gun MIG/Lift TIG/Stick Multiprocess Aluminum MIG Welder, Spool Gun Compatible - Customer Photo 1
    Customer submitted photo

    The 200-amp output provides sufficient power for copper up to about 3/8-inch with proper preheating. Beyond that thickness, you’re better off with a dedicated industrial machine, but this covers the vast majority of fabrication work.

    Spool gun compatibility means you can weld aluminum too, making this a truly versatile shop machine. The synergic settings reduce the learning curve significantly.

    Customer images demonstrate the machine’s build quality and show real-world welds that users have produced. The digital display provides clear visibility of your settings, which is crucial when dialing in copper welding parameters.
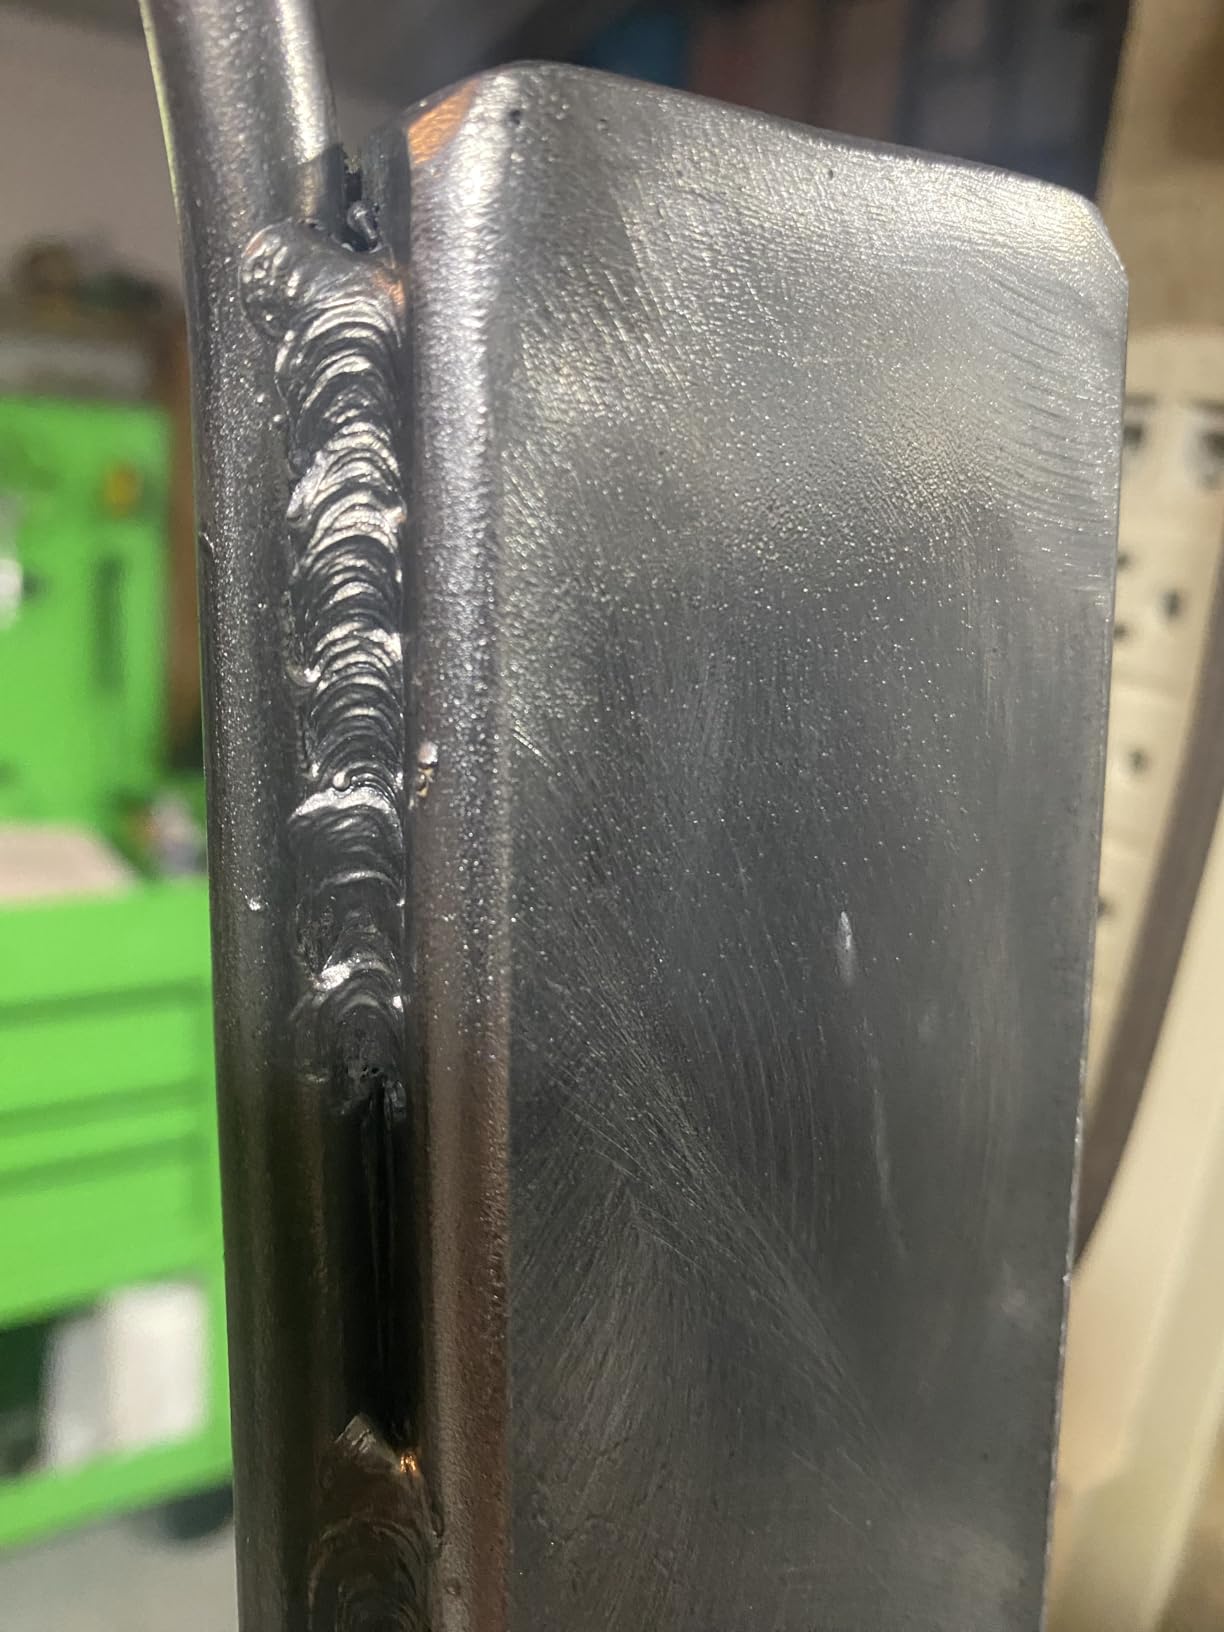
    YESWELDER MIG-205DS PRO MIG Welder, 200Amp 110/220V Dual Voltage MIG Welding Machine, 5 in 1 Gas MIG/Flux Core MIG/Spool Gun MIG/Lift TIG/Stick Multiprocess Aluminum MIG Welder, Spool Gun Compatible - Customer Photo 3
    Customer submitted photo

    I’ve run this unit on both 110V and 220V power. While 110V limits maximum output, it works surprisingly well for thinner copper materials. For production work on thicker material, the 220V connection provides consistent power delivery.

    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    exablo Phosphor Copper Brazing Rods – Self-Fluxing HVAC Solution

    HVAC SPECIALIST

    ★★★★★★★★★★5.0 / 5

    Material: BCuP-2 phosphor copper

    Quantity: 20 rods

    Size: 1/10 inch x 19.6 inches

    Melting point: 1310-1508°F

    Features: Self-fluxing design

    Check Price

    + Pros

    • No flux required-phosphorus acts as flux
    • Low melting point easy flow
    • High tensile strength 130 N/mm
    • Moisture-resistant packaging
    • Eco-friendly materials

    Cons

    • Very limited review data
    • New product with minimal feedback
    • Requires proper technique for best results
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    These phosphor copper brazing rods simplify HVAC and refrigeration work significantly. The self-fluxing design means no separate flux application is required—the phosphorus content handles that automatically.

    I appreciate the low melting point of 710-820°C, which allows working on copper tubing without overheating surrounding components. This proves especially valuable when working near sensitive connections or valves.

    The 2.5mm diameter feeds smoothly and provides adequate filler material for typical copper pipe joints. Each 19.6-inch rod gives you plenty of material for multiple repairs.

    While review data is limited due to the product’s newness, the specifications align with industry standards for BCuP-2 brazing alloys. The moisture-resistant PVC packaging helps maintain rod quality over time.

    For HVAC technicians and DIYers working on refrigeration systems, these rods offer a convenient solution. The tensile strength of 130 N/mm² ensures joints can handle typical system pressures when properly executed.

    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    SÜA ERCuSi-A Silicon Bronze – Best TIG Brazing Filler

    TOP TIG FILLER
    Product

    SÜA – ERCuSi-A Silicon Bronze TIG Welding Rod – 36” x 0.045”- (1 Lb)

    ★★★★★★★★★★4.7 / 5

    Material: ERCuSi-A silicon bronze

    Diameter: 0.045 inch

    Length: 36 inches

    Quantity: 1 pound

    Melting point: 1866°F

    Check Price

    + Pros

    • High strength 51000 psi
    • Excellent corrosion resistance
    • Beautiful bronze finish
    • Versatile for multiple metals
    • Good TIG brazing characteristics

    Cons

    • 0.045 diameter feeds quickly
    • Requires heat control practice
    • Not Prime eligible shipping
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    SÜA’s ERCuSi-A silicon bronze rod produces some of the most attractive copper welds I’ve seen. The 3% silicon content creates excellent wetting action and results in that distinctive bronze finish many fabricators prefer.

    With a tensile strength of 51,000 psi, this filler creates structurally sound joints. I’ve used it extensively for joining copper to steel, where the color transition looks intentional rather than like a repair.
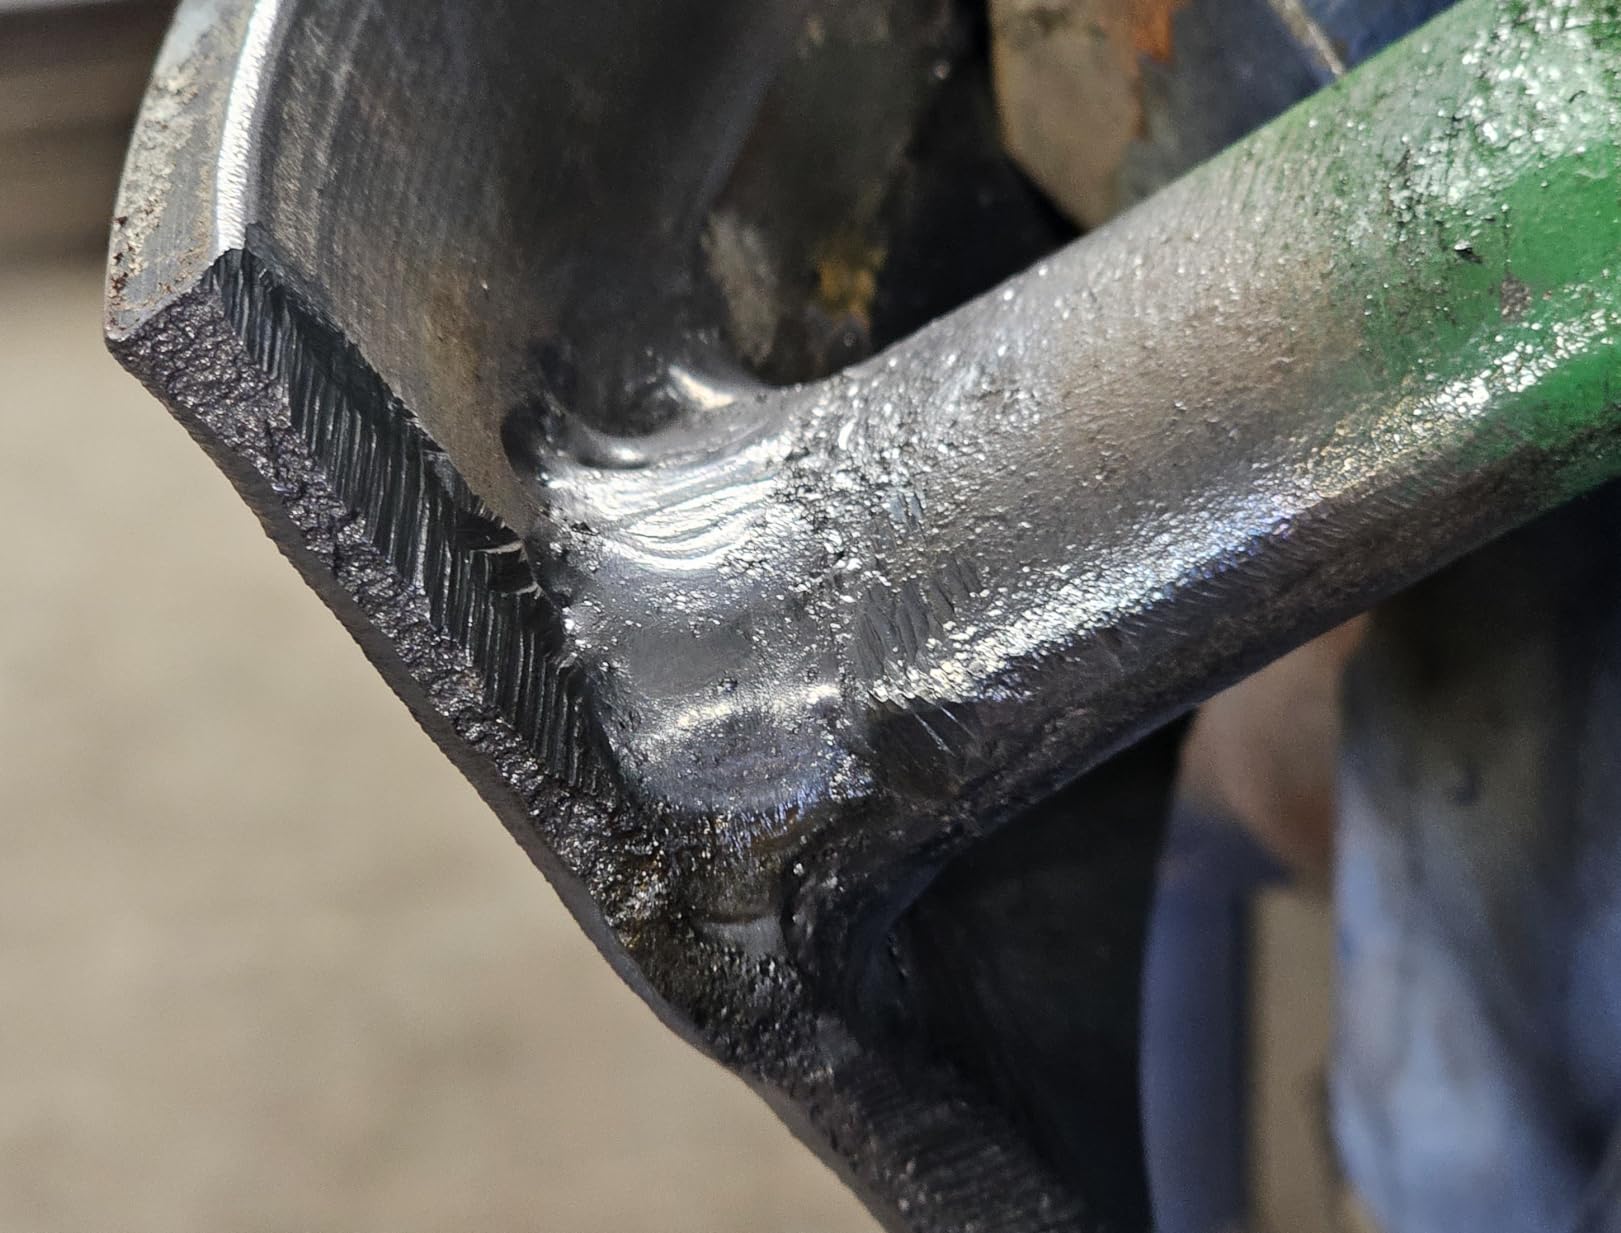
    SÜA - ERCuSi-A Silicon Bronze TIG Welding Rod - 36'' x 0.045''- (1 Lb) - Customer Photo 1
    Customer submitted photo

    The 0.045-inch diameter works well for most TIG applications. It’s fine enough for precision work but substantial enough to deposit filler without feeding frantically. For heavier work, stepping up to 1/8-inch diameter would be my recommendation.

    Customer photos show the beautiful bronze coloration that makes this filler popular for decorative work. The as-welded Brinell hardness of 80-100 indicates good machinability if needed.

    The melting temperature of 1866°F means you need proper amperage control, but the resulting weld beads flow nicely when parameters are correct. I’ve found this filler particularly forgiving for intermediate TIG operators.

    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    COLIBROX 80 cu/ft Argon Cylinder – Complete Shielding Gas Solution

    BEST GAS VALUE
    Product

    80 cu/ft 100% Argon Cylinder Tank Welding Gas CGA 580 – FULL

    ★★★★★★★★★★4.7 / 5

    Capacity: 80 cubic feet

    Gas: 100% Argon

    Connection: CGA 580 valve

    Pressure: 2400 psi fill

    Weight: 50 lbs

    Check Price

    + Pros

    • Higher pressure than typical local fills
    • Convenient home delivery
    • DOT compliant with current dates
    • Ready to use immediately
    • No cylinder exchange hassle

    Cons

    • Non-returnable hazardous material
    • Verify local refill capability first
    • 50 pounds requires care handling
    • Delivery coordination may be needed
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Shielding gas quality directly affects copper weld quality, and this 80 cubic foot argon cylinder delivers consistently. The 2400 psi fill exceeds what many local suppliers provide, giving you more welding time between exchanges.

    I recommend pure argon for most copper welding applications. The heavier gas provides excellent shielding coverage, and copper doesn’t require the addition of helium or CO2 that steel welding might need.
    80 cu/ft 100% Argon Cylinder Tank Welding Gas CGA 580 - FULL - Customer Photo 2
    Customer submitted photo

    Before purchasing any cylinder, verify your local gas supplier can fill or exchange it. This cylinder uses the standard CGA 580 valve found on most argon cylinders, so compatibility shouldn’t be an issue at major gas suppliers.

    Customer images confirm the cylinder arrives well-packaged and ready for immediate use. The DOT compliance with current hydrotest dates means you won’t face rejection when getting refills.

    The convenience of home delivery cannot be overstated, especially for rural welders who might drive significant distances to reach a welding supply store. At 50 pounds, plan for assistance moving it into your workspace.
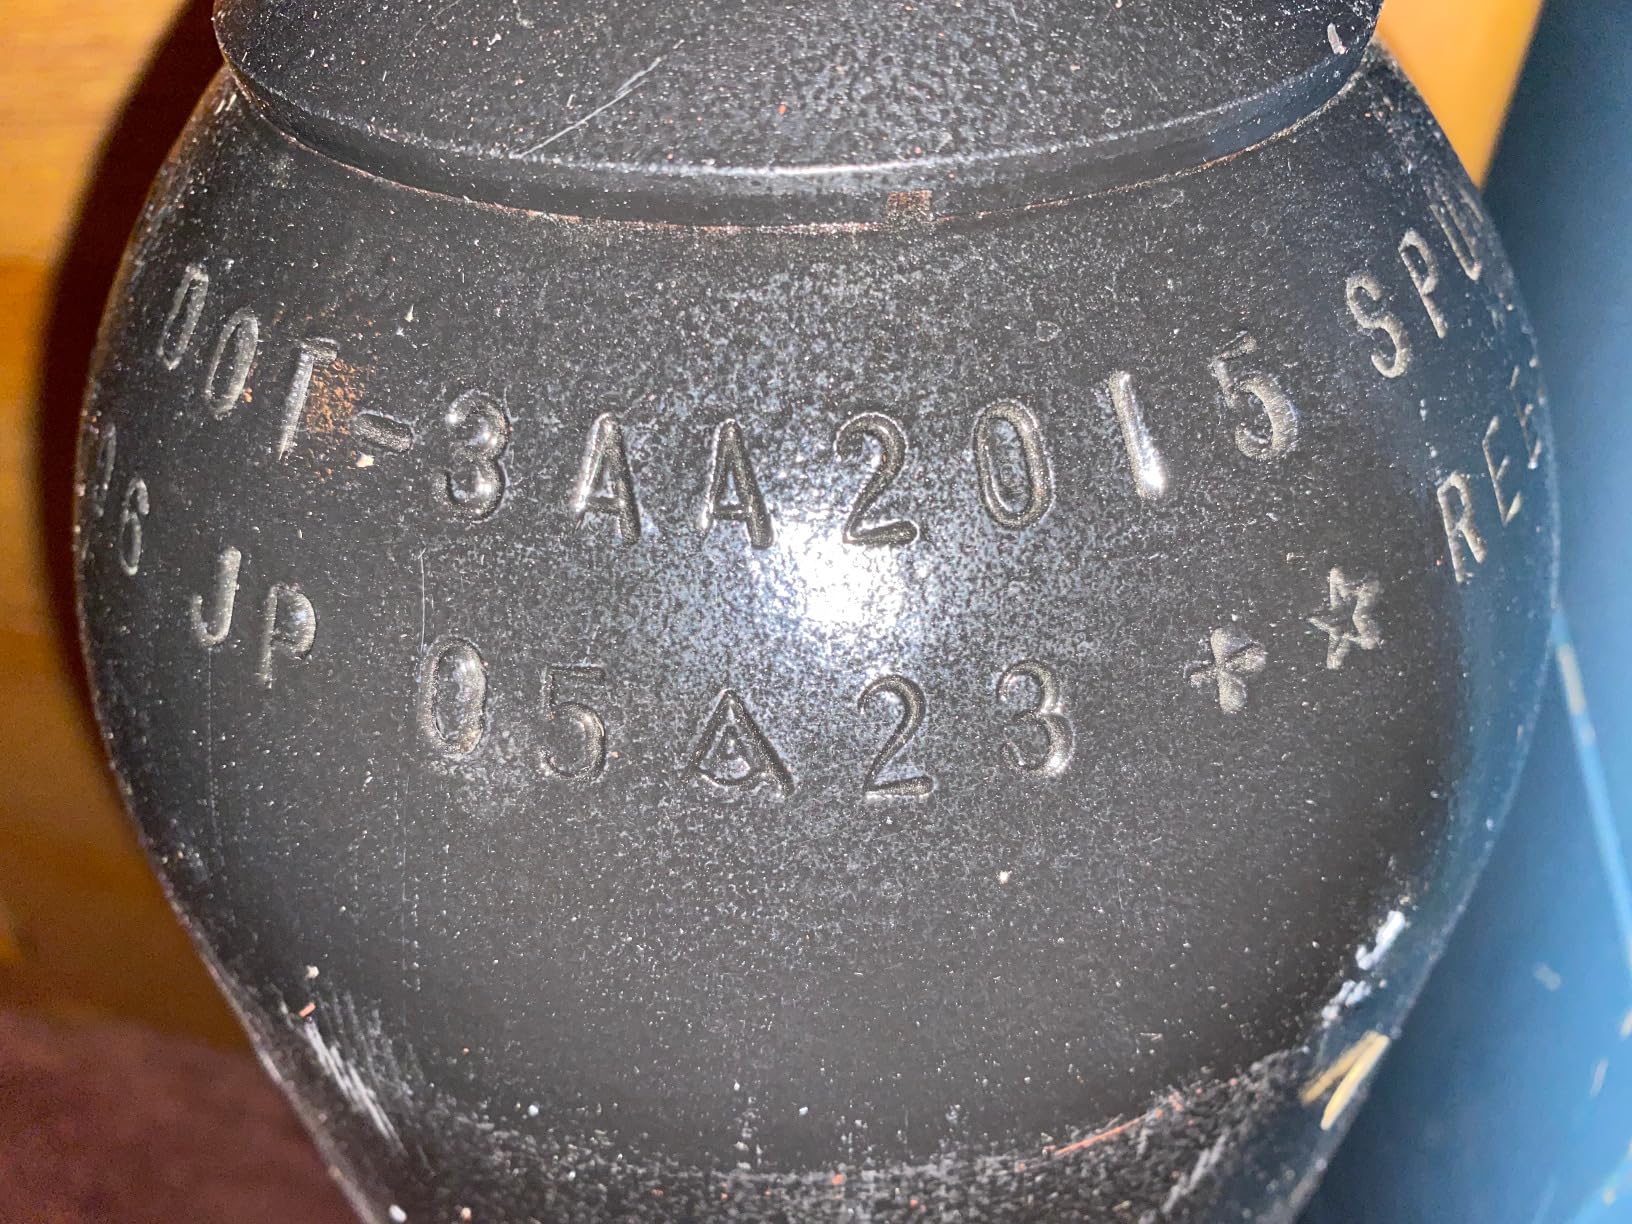
    80 cu/ft 100% Argon Cylinder Tank Welding Gas CGA 580 - FULL - Customer Photo 1
    Customer submitted photo

    This amount of gas provides substantial welding time. For TIG welding copper, I typically run 15-20 CFH, meaning this 80-cubic-foot cylinder delivers approximately 4-5 hours of actual arc time—enough for dozens of copper projects.

    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    MAXMAN Wire Brush Set – Best Copper Cleaning Brush
    AMAZON'S CHOICE
    Product

    MAXMAN Wire Brush 2Pcs, 10″ Stainless Steel Bristles, Rust & Paint Remover

    ★★★★★★★★★★4.7 / 5

    Material: Stainless steel bristles

    Handle: 10 inch beech wood

    Quantity: 2 pack

    Bristle rows: 4 x 16

    Features: Ergonomic curved design

    Check Price

    + Pros

    • Stiff bristles remove oxidation effectively
    • Long handle keeps hands clear
    • Ergonomic comfortable grip
    • Excellent value 2-pack
    • Versatile for multiple uses

    Cons

    • Can scratch if not used carefully
    • Stainless steel may rust if not dried
    • Not for delicate surfaces
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Proper copper cleaning requires dedicated brushes, and this MAXMAN set delivers excellent performance. The stainless steel bristles remove oxidation effectively without loading up like carbon steel brushes do.

    The 10-inch beech wood handle provides excellent leverage and keeps your hands away from the work surface. I’ve found this especially valuable when cleaning larger copper sheets before welding.
    MAXMAN Wire Brush, Heavy Duty Stainless Steel Wire Brushes for Cleaning Rust, Grill Brush, Steel Brush for Paint Removal, Welding, Stiff Bristle Metal Brush with 10
    Customer submitted photo

    Two brushes in the pack means you can designate one solely for copper work, preventing cross-contamination with ferrous metals. Steel particles embedded in copper create rust spots and weaken the weld.

    Customer photos show the brush construction and real-world use on various metals. The 4 x 16 bristle configuration provides aggressive cleaning action while the curved handle fits naturally in your hand.

    The stiff bristles work particularly well on oxidized copper surfaces. I’ve used these brushes extensively for pre-weld cleaning and found they maintain their stiffness better than cheaper alternatives.
    MAXMAN Wire Brush, Heavy Duty Stainless Steel Wire Brushes for Cleaning Rust, Grill Brush, Steel Brush for Paint Removal, Welding, Stiff Bristle Metal Brush with 10
    Customer submitted photo

    For copper sheet preparation, I recommend brushing in the direction of the intended weld. This technique helps align any surface contaminants and makes the final cleaning with solvent more effective.

    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    YESWELDER Auto Darkening Helmet – #1 Best Seller Protection

    #1 BEST SELLER
    Product

    YESWELDER Auto Darkening Welding Helmet 1/1/1/1 True Color, LYG-L600A

    ★★★★★★★★★★4.6 / 5

    Shade range: 3.5/9-13

    Optical clarity: 1/1/1/1

    Response time: 1/30000 sec

    Sensors: 2 arc sensors

    Power: Solar + battery

    Check Price

    + Pros

    • Excellent 1/1/1/1 optical clarity
    • Blue light blocking technology
    • Lightweight 1 pound design
    • Fast auto-darkening response
    • Solar power with battery backup

    Cons

    • Head strap may slip during movement
    • Battery occasionally factory installed wrong
    • Viewing area smaller than panoramic models
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    This helmet dominates the welding helmet market for good reason. The 1/1/1/1 optical clarity rating indicates top-tier performance across all optical quality metrics, which significantly reduces eye strain during long welding sessions.

    Copper welding produces intense visible light and UV radiation. The blue light blocking technology in this YESWELDER helmet provides additional protection that standard helmets might miss.
    YESWELDER Auto Darkening Welding Helmet, Blue Light Blocking, 1/1/1/1 True Color Solar Powered Welding Hood with 2 Arc Sensors, Wide Shade 3.5/9-13 Welder Mask for TIG MIG ARC and Grind - Customer Photo 2
    Customer submitted photo

    The 1/30000 second response time is practically instantaneous. This fast switching protects your eyes from flash and allows you to see your weld pool clearly immediately after striking an arc—critical for copper TIG work where precision matters.

    Customer images show the helmet in real-world use and confirm the viewing area dimensions. At 3.64 x 1.67 inches, the viewing area provides adequate workspace visibility while keeping the helmet lightweight.

    At only 1 pound, this helmet reduces neck fatigue during extended welding sessions. I’ve worn it for 4+ hours of copper fabrication work without the discomfort that heavier helmets cause.
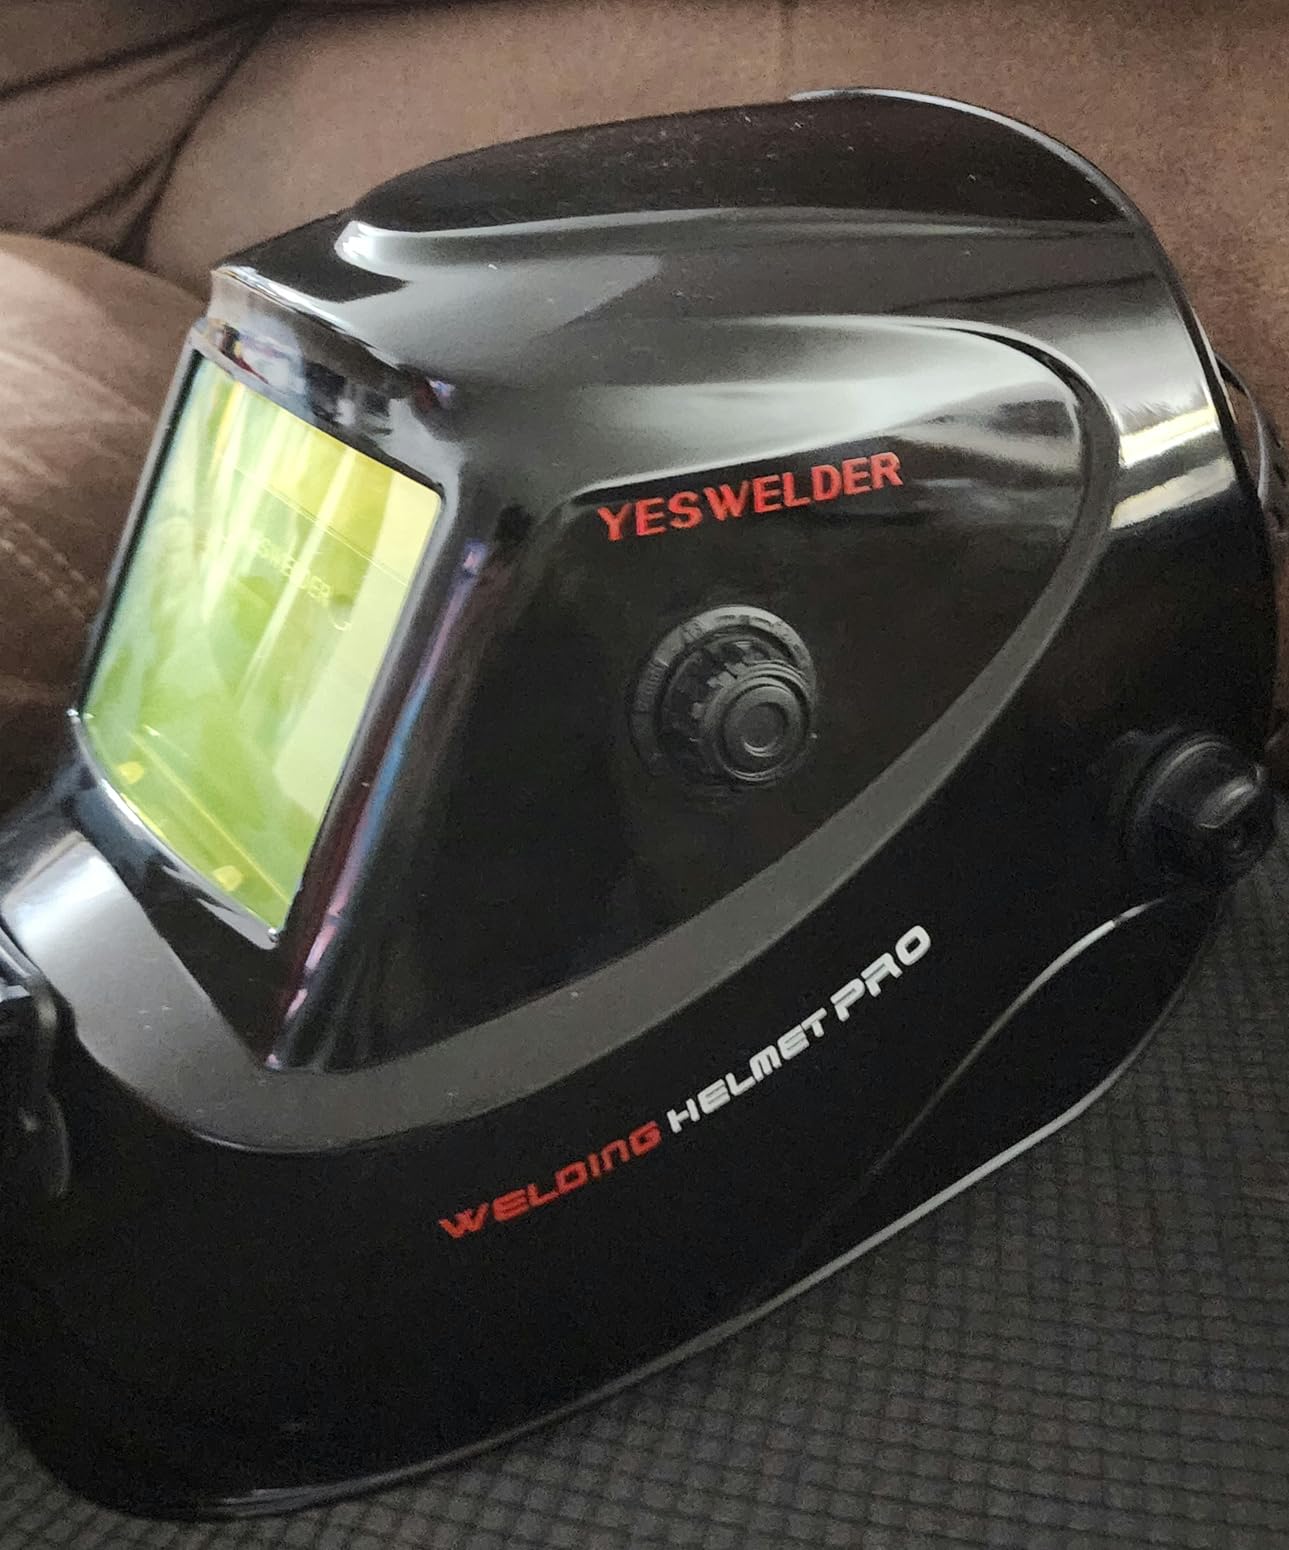
    YESWELDER Auto Darkening Welding Helmet, Blue Light Blocking, 1/1/1/1 True Color Solar Powered Welding Hood with 2 Arc Sensors, Wide Shade 3.5/9-13 Welder Mask for TIG MIG ARC and Grind - Customer Photo 1
    Customer submitted photo

    The wide shade range of 3.5/9-13 accommodates all copper welding processes. I typically use shade 11-12 for TIG welding copper, stepping up to 13 for heavier MIG work. The shade 3.5 light state is bright enough to see your work clearly without lifting the helmet.

    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    TOPDC Welding Gloves – Heat Resistant Protection

    #2 BEST SELLER
    Product

    TOPDC Welding Gloves 16-Inch 932°F Heat Resistant Leather for MIG, Stick

    ★★★★★★★★★★4.6 / 5

    Length: 16 inches

    Heat resistance: 932°F (500°C)

    Material: 1.2mm cowhide leather

    Lining: 100% cotton

    Features: Kevlar stitched

    Check Price

    + Pros

    • Extreme heat resistance
    • 16 inch sleeve protects forearm
    • Soft leather allows dexterity
    • Kevlar stitching adds durability
    • Cotton lining comfortable

    Cons

    • May run large for some users
    • Not machine washable
    • Contact heat resistance limited to 15 seconds
    We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

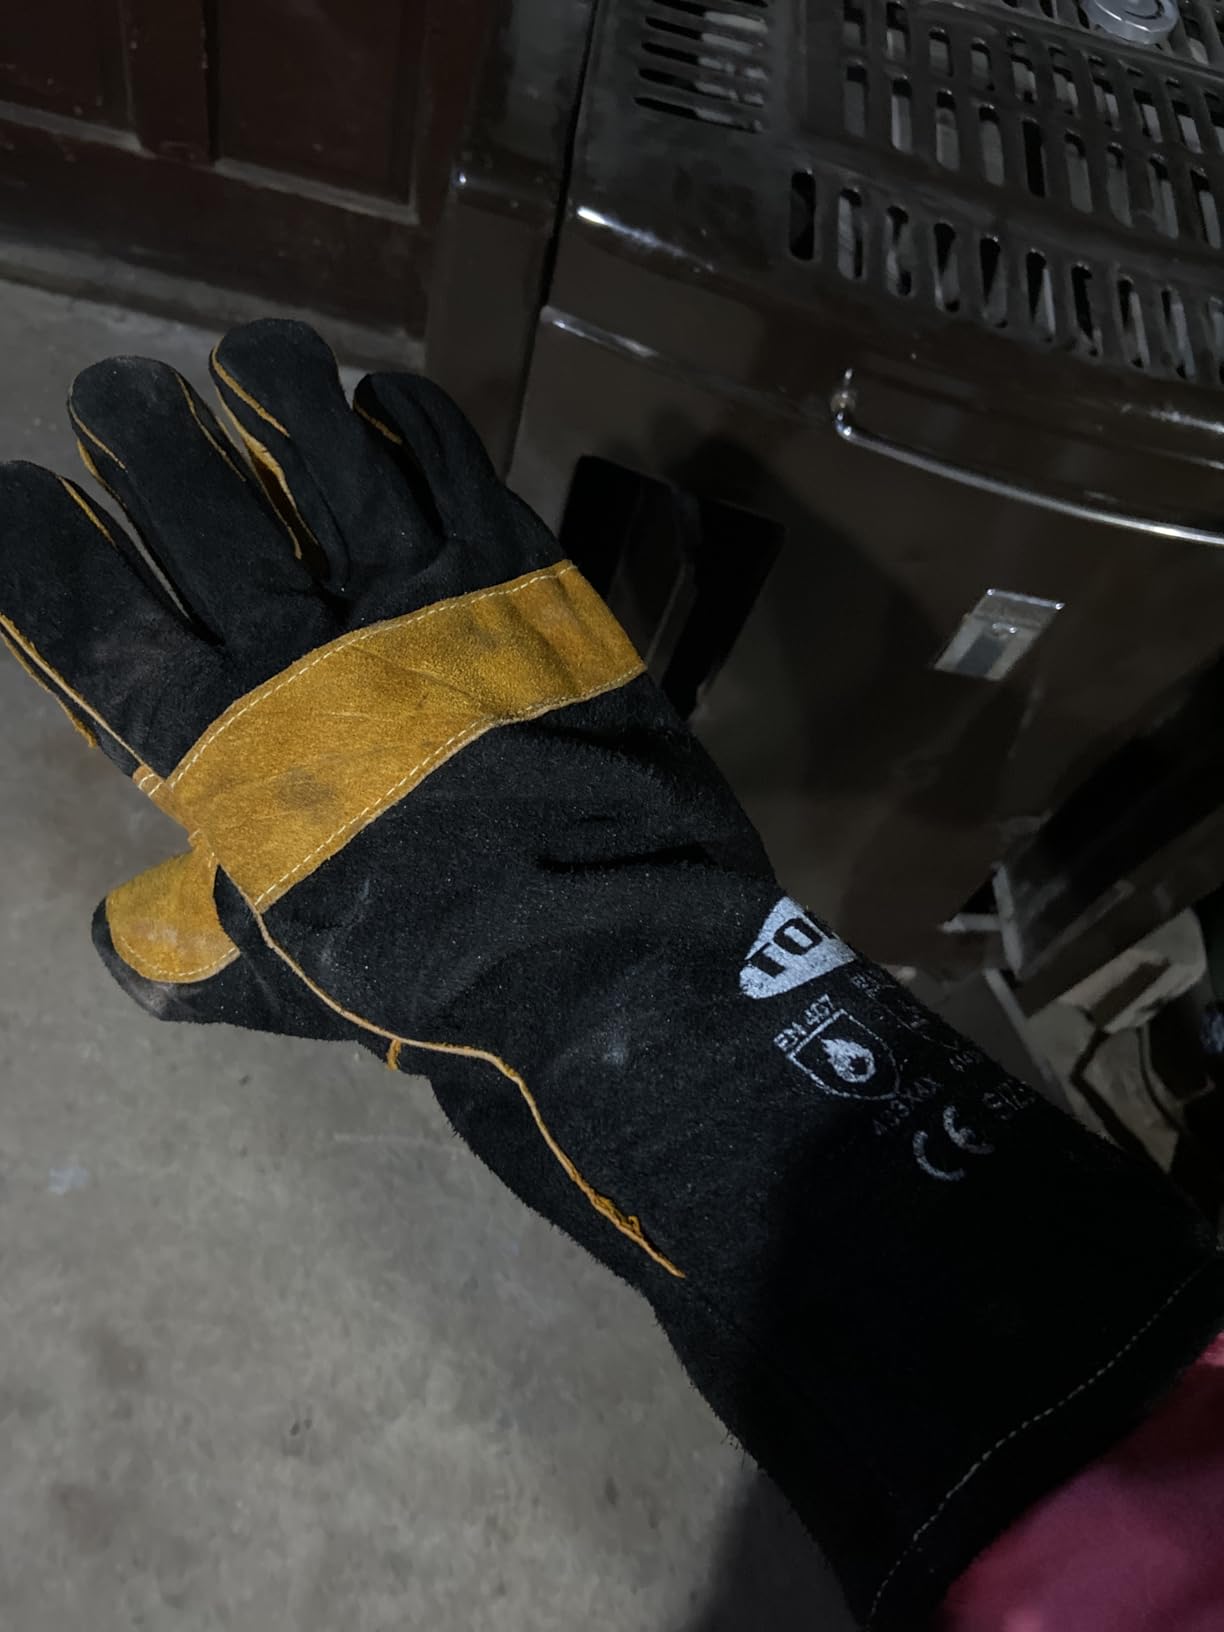
    Copper welding involves significant heat exposure, and these 16-inch gloves provide comprehensive protection. The 932°F heat resistance rating covers most copper welding applications when proper technique is used.

    The extra length extends protection well up your forearm, which I’ve found invaluable when TIG welding copper. The heat from larger copper pieces radiates further than you expect, and full forearm coverage prevents burns.
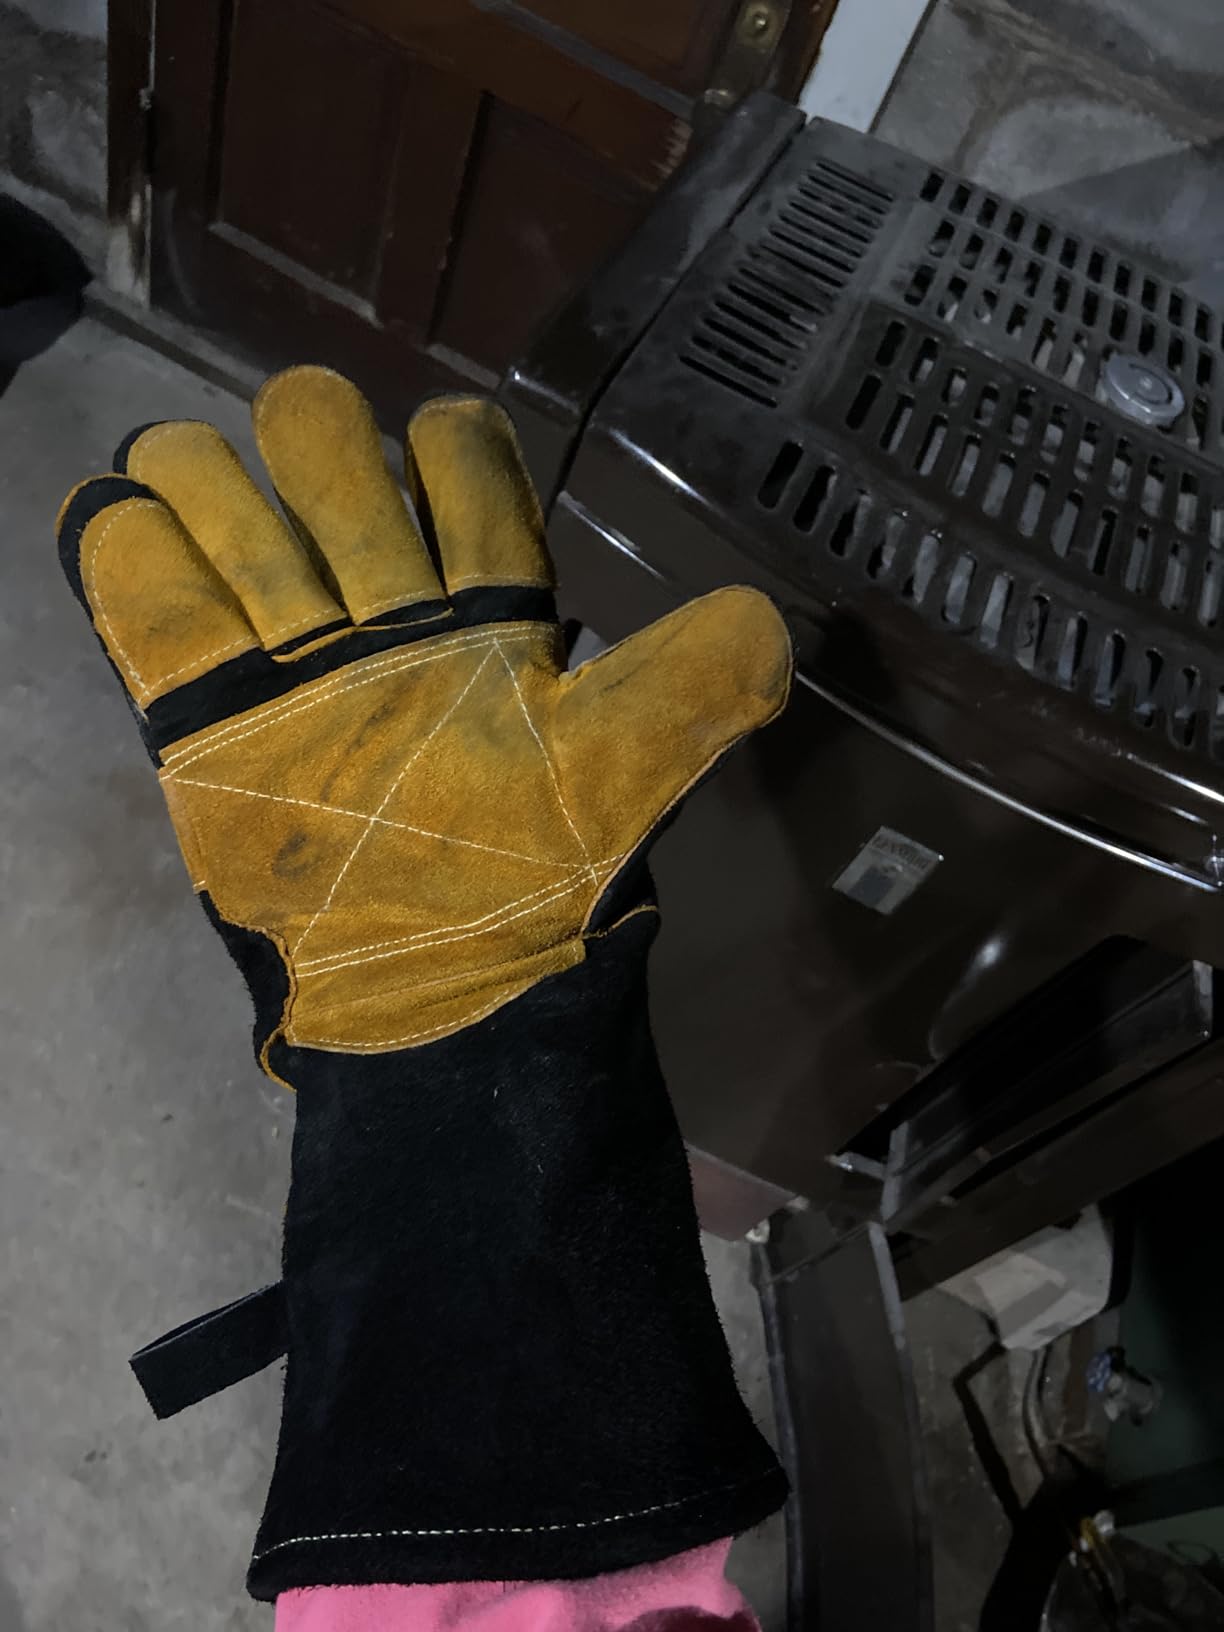
    TOPDC Welding Gloves 16 Inches 932℉ Fire/Heat Resistant Leather Welding Gloves For Mig, Tig, Stick, Forge, BBQ, Grill, Fireplace, Wood Stove, Furnace, Oven, Animal Handling - Customer Photo 1
    Customer submitted photo

    What surprises me about these gloves is the dexterity they maintain despite the 1.2mm leather thickness. I can manipulate TIG torches and filler rods with reasonable precision, something impossible with cheaper, stiffer gloves.

    Customer images demonstrate the glove quality and show real-world use in various applications. The Kevlar stitching throughout adds significant durability—stitching failure is what dooms most welding gloves, and TOPDC addressed this weakness directly.

    The 100% cotton lining makes these gloves comfortable for extended wear. I’ve worn them through hours of copper fabrication without the excessive sweating that synthetic linings cause.
    TOPDC Welding Gloves 16 Inches 932℉ Fire/Heat Resistant Leather Welding Gloves For Mig, Tig, Stick, Forge, BBQ, Grill, Fireplace, Wood Stove, Furnace, Oven, Animal Handling - Customer Photo 2
    Customer submitted photo

    Double leather sewing on stress points reinforces the areas that typically fail first. After months of use, my pair shows minimal wear despite daily exposure to high heat and abrasion.

    While rated for welding, these gloves serve double duty in my shop for handling hot copper pieces after welding. The 16-inch length lets me grab hot workpieces from the table without risking arm burns.

    View on Amazon We earn from qualifying purchases, at no additional cost to you. CERTAIN CONTENT THAT APPEARS ON THIS SITE COMES FROM AMAZON. THIS CONTENT IS PROVIDED 'AS IS' AND IS SUBJECT TO CHANGE OR REMOVAL AT ANY TIME.

    Common Problems and Solutions

    Even with proper preparation, copper welding presents unique challenges. I’ve encountered and solved most common issues through trial and error.

    Porosity in Copper Welds

    Porosity remains the most common copper welding defect I see. Those small gas pockets weaken welds and create leak paths in pressure-critical applications.

    The primary causes I’ve identified include:

    • Insufficient cleaning before welding
    • Moisture in filler material or base metal
    • Incorrect gas flow rate (too low or too high)
    • Shielding gas contamination

    Solutions that work for me include extending cleaning time, storing filler rods in climate-controlled areas, and verifying gas flow with a flowmeter rather than relying on regulator gauges.

    Cracking in Heat-Affected Zone

    Cracking typically occurs from excessive restraint combined with rapid cooling. Copper’s high thermal expansion means joints move significantly as they heat and cool.

    I prevent cracking by:

    • Using proper joint designs with some flexibility
    • Preheating to reduce thermal gradients
    • Allowing controlled cooling (not quenching)
    • Peening welds while still slightly warm

    Lack of Fusion

    When copper doesn’t fuse properly, it’s usually from insufficient heat input or poor technique. Copper’s high thermal conductivity means heat dissipates rapidly.

    Solutions include increasing amperage, improving preheating, and ensuring proper torch angle. For TIG welding, I aim the arc more directly into the joint rather than riding the surface.

    Warping and Distortion

    Copper warps more than steel during welding due to higher thermal expansion. I control distortion through:

    • Clamping workpieces securely but with some allowance for movement
    • Using intermittent weld sequences rather than continuous welds
    • Planning weld sequence to balance shrinkage forces
    • Pre-setting joints to compensate for expected movement

    Safety Considerations

    Copper welding requires specific safety precautions beyond standard welding practices. I’ve learned that copper presents unique hazards that deserve respect.

    Ventilation Requirements

    Copper welding fumes contain metal particulates that can cause respiratory issues. Adequate ventilation is non-negotiable in my shop.

    I use a combination of general shop ventilation plus local exhaust at the welding point. For frequent copper welding, a fume extractor rated for metal particulates is worth the investment.

    Copper Toxicity Concerns

    While copper itself isn’t highly toxic, copper alloys containing zinc (like brass) produce zinc oxide fumes when welded. These fumes cause metal fume fever if inhaled in sufficient quantities.

    Know what alloy you’re welding and adjust your ventilation accordingly. Pure copper produces fewer hazardous fumes than copper-zinc alloys.

    Personal Protective Equipment

    Quality PPE is essential for copper welding. I never weld without:

    • Auto-darkening helmet with proper shade rating
    • Respirator rated for metal particulates when ventilation is questionable
    • Leather welding gloves with forearm protection
    • Natural fiber clothing (synthetics melt and stick to skin)
    • Closed-toe leather boots

    The investment in quality protective equipment pays dividends in long-term health. I’ve seen too many welders develop respiratory issues from inadequate protection.

    Frequently Asked Questions

    What is the best welding process for copper?

    TIG welding produces the highest quality copper welds for most applications. It offers precise heat control essential for copper’s high thermal conductivity. MIG welding works well for thicker copper sections where speed matters. For thin copper sheet under 1/8 inch, TIG is unmatched in control and finish quality.

    What gas do you use for welding copper?

    Pure argon is the standard shielding gas for most copper welding applications. It provides excellent arc stability and prevents oxidation during welding. For thicker copper sections over 1/4 inch, adding helium to the argon increases heat input. A 75/25 argon-helium mixture is common for heavy copper welding.

    Do you need to preheat copper before welding?

    Yes, preheating copper is essential for thickness over 1/8 inch. Copper’s high thermal conductivity dissipates heat rapidly, making fusion difficult without preheating. Typical preheat temperatures range from 300-500F for medium thickness and up to 1200F for thick sections. Always preheat uniformly across the workpiece for best results.

    What filler rod for copper welding?

    ERCuSi-A silicon bronze is the most versatile filler for copper welding. It offers excellent flow, strength, and corrosion resistance. For color matching in electrical applications, ERCu deoxidized copper works best. Phosphor bronze (BCuP) excels for HVAC and refrigeration work due to self-fluxing properties.

    Can you stick weld copper?

    Stick welding copper is possible but challenging. I recommend it only for field repairs or when other equipment is unavailable. Specialized bronze rods designed for copper work provide the best results. The process requires higher skill than TIG or MIG due to copper’s rapid heat dissipation fighting against the stick arc.

    Is welding copper toxic?

    Pure copper welding produces relatively low toxicity fumes compared to other metals. However, adequate ventilation remains essential. Copper alloys containing zinc produce zinc oxide fumes that can cause metal fume fever. Always use proper ventilation and respiratory protection when welding any copper material. Know your specific alloy’s composition before welding.

    Copper welding rewards patience and proper preparation. After years of practice, I’ve found that respecting copper’s unique properties rather than fighting against them produces the best results. Start with clean material, appropriate preheating, and the right process for your application. The skills you develop working with copper transfer well to all types of welding, making it an excellent teacher for metal fabrication fundamentals.
  • Arc Welding Safety Checklist for Welders 2026

    Arc Welding Safety Checklist for Welders 2026

    I still remember the day my welding instructor told our class about a local fabricator who spent three days in the hospital because he skipped his helmet for “just one tack weld.” That single mistake cost him $12,000 in medical bills and two months of lost work. After 10 years in metal fabrication, I’ve seen welders make every safety mistake in the book. Some learned the hard way. Others got lucky.

    Arc welding creates temperatures up to 6,500 degrees Fahrenheit and generates invisible UV radiation that can damage your eyes in less than a second. The arc flash is brighter than the sun, and the fumes contain metal particles that accumulate in your lungs over years of exposure. I’ve worked in production shops, custom fabrication, and my own home garage. The safety principles never change, but I see beginners skip them constantly.

    Arc welding safety requires comprehensive protection: proper PPE including a helmet with correct shade lenses, fire-resistant clothing, leather gloves, and steel-toed boots; adequate ventilation or respiratory protection; electrical safety through proper grounding and dry conditions; fire prevention with a 35-foot clearance from flammables; and following OHA standards 1910.254 and ANSI Z49.1.

    Quick Summary: Arc welding generates five primary hazards: electric shock, UV/IR radiation, welding fumes, fire, and burns. Full protection requires rated PPE, proper ventilation, grounded equipment in dry conditions, fire extinguisher access, and following established safety procedures every single weld.

    The 5 Critical Arc Welding Hazards Explained

    Understanding these hazards is the first step toward protecting yourself. Let me break down each one based on what I’ve seen in real workshops.

    Electric Shock: The Silent Killer

    The welding output circuit ranges from 20 to 80 volts in open-circuit conditions. That might not sound like much compared to household outlets, but it becomes extremely dangerous when your skin is wet or you’re touching grounded metal. The primary shock hazard comes from the output circuit, not the input power.

    I knew a welder who got knocked across the room when his sweaty forearm touched the workpiece while changing electrodes. He was lucky. Another fabricator in my city wasn’t—he died from a similar incident. Secondary voltage shock kills an estimated 50 workers annually in the United States.

    Never touch live electrical parts with bare skin. Keep your gloves dry. Inspect cables for exposed conductors before every use. Use insulation mats when welding on or near grounded surfaces. And never work in wet conditions—water drastically reduces your body’s resistance to electrical current.

    UV Radiation and Arc Eye

    The welding arc produces intense ultraviolet radiation that causes photokeratitis—commonly called arc eye or welder’s flash. It’s essentially a sunburn on your corneas. I’ve experienced it twice. Both times, I woke up at 2 AM feeling like someone poured sand in my eyes.

    Symptoms appear 6-12 hours after exposure. Your eyes become extremely sensitive to light, tear uncontrollably, and feel like they’re full of grit. The condition is temporary but miserable. Repeated exposure can cause cataracts and permanent vision damage.

    UV radiation also damages exposed skin. I’ve seen welders with what looks like a severe sunburn after just 15 minutes of welding without proper coverage. Long-term, this causes premature aging and increases skin cancer risk.

    Arc Eye (Photokeratitis): A painful eye condition caused by unprotected exposure to UV radiation from welding arcs. Symptoms include severe eye pain, light sensitivity, excessive tearing, and the sensation of foreign objects in the eyes. Symptoms typically appear 6-12 hours after exposure.

    Welding Fumes and Long-Term Health

    Welding fumes contain a complex mixture of metal oxides, gases, and particulates. The exact composition depends on the base metal, filler material, and any coatings present. Common components include manganese, chromium, nickel, and zinc.

    Manganese exposure is particularly concerning. Long-term inhalation can cause manganism—a neurological condition similar to Parkinson’s disease. I’ve worked with older welders who developed hand tremors and slow movement after decades of welding without respiratory protection.

    Zinc fumes from galvanized steel cause metal fume fever—flu-like symptoms that appear 4-12 hours after exposure. I’ve had it once. Fever, chills, nausea, and muscle aches kept me in bed for 24 hours. It’s temporary but miserable, and repeated episodes indicate overexposure.

    Fire and Explosion Risks

    Every welding operation throws sparks—sometimes up to 35 feet from the work area. These sparks can reach 2,500 degrees Fahrenheit and stay hot enough to ignite materials for considerable distances. I’ve seen sparks land in sawdust, through floor cracks, and on rags sitting 20 feet away.

    Explosions are an even greater threat. Welding on containers that previously held flammable materials has killed countless workers. The heat from welding can vaporize residual flammable substances inside closed containers. The vapor expands, pressure builds, and—boom.

    I personally investigate every container before welding. I look for labels, smell for odors, and test with electronic gas detectors when available. When in doubt, I fill the container with water or inert gas before welding. There’s no project worth dying for.

    Burn Hazards

    Molten metal, hot slag, and heated workpieces cause immediate and severe burns. The weld pool stays liquid at 2,500-3,000 degrees. Slag can remain hot enough to burn through leather boots an hour after welding.

    I have burn scars on both forearms from early in my career. One happened when I rested my arm on a piece I’d welded 20 minutes earlier. Another came from slag that dropped inside my boot cuff. These injuries were painful and preventable with proper positioning and full coverage clothing.

    Personal Protective Equipment (PPE): Complete Guide

    Proper PPE is your last line of defense. When engineering controls and safe work practices fail—which they will at some point—your gear is what stands between you and injury. Let me walk through each piece of essential equipment.

    Head and Face Protection

    The welding helmet is your most critical piece of PPE. It protects your face from sparks and spatter, your eyes from UV radiation, and provides shade to see the weld pool clearly. I’ve used everything from $30 fixed-shade helmets to $600 auto-darkening models.

    Auto-darkening helmets have transformed the industry. Instead of flipping your helmet up and down constantly, the lens darkens automatically when you strike an arc. This reduces neck strain and improves precision. Good models react in 1/20,000 of a second—fast enough to prevent flash.

    Shade selection is critical. Too light and your eyes strain. Too dark and you can’t see the workpiece. Here’s what I use for different processes:

    Welding ProcessAmperage RangeRecommended Shade
    Stick (SMAW)Under 60AShade 7-8
    Stick (SMAW)60-160AShade 10
    Stick (SMAW)160-250AShade 12
    MIG (GMAW)60-160AShade 10
    MIG (GMAW)160-300AShade 12-13
    TIG (GTAW)Under 50AShade 8-9
    TIG (GTAW)50-150AShade 10-11
    Carbon Arc GougingAll amperagesShade 14

    Safety glasses are mandatory underneath your helmet. Sparks can bounce off your workpiece and find their way behind your helmet. I’ve had it happen. Now I always wear ANSI Z87.1-rated side-shield glasses. Clear polycarbonate lenses work for most applications.

    Hand and Arm Protection

    Welding gloves aren’t one-size-fits-all. Different processes require different gloves. I keep three types in my shop:

    Glove TypeBest ForKey Features
    Stick/MIG GlovesHeavy-duty weldingThick leather, elbow-length, lined
    TIG GlovesPrecision TIG weldingThin, supple, finger dexterity
    Driver GlovesMaterial handlingMedium weight, good grip

    For Stick and MIG welding, I use heavy Elkskin or cowhide gloves that extend past my elbows. The extra length protects my forearms from radiant heat and UV radiation. These gloves are thick enough that I can’t feel small parts—I switch to lighter gloves for grinding and material handling.

    TIG welding requires much more finger dexterity. I use thin goatskin or pigskin gloves that allow me to feel the torch and filler rod. They sacrifice some heat protection, but I can’t TIG weld effectively in thick gloves.

    Body Protection

    Your clothing creates a barrier against sparks, UV radiation, and burns. I’ve seen welders wear cotton t-shirts and wonder why they end up with sunburned arms. Synthetic materials are even worse—they melt into your skin when hit by sparks.

    Wear natural fibers only. Cotton is acceptable for light work. Wool is better because it’s naturally flame-resistant and provides some insulation. For serious production work, invest in fire-resistant clothing treated with flame-retardant chemicals.

    A welding jacket or cape is your best upper-body protection. Jackets cover your torso, arms, and neck. Capes cover your upper body but leave your arms free—great for TIG welding where you need mobility. I prefer jackets for Stick and MIG work.

    Welding aprons protect your torso and thighs from spatter while leaving your arms free. They’re lighter than jackets and work well for bench work. I use one when doing lots of tack welding or position work where mobility matters.

    Pants should cover your boots completely. Cuffs can catch sparks and let them fall inside your boots. I’ve seen this happen—it’s not fun. Heavy denim or canvas works well. For production welding, fire-resistant coveralls provide the best protection.

    Foot Protection

    Leather boots with steel toes are mandatory. Sparks will burn through athletic shoes in seconds. I’ve seen the aftermath—a welder spent three weeks recovering from severe foot burns because he wore sneakers “just for a quick weld.”

    High-topped boots provide ankle protection and prevent sparks from entering the top. Metatarsal guards add protection for the top of your foot—essential when doing overhead work or heavy fabrication where falling slag is common.

    Electrical hazard-rated boots add insulation against electrical shock. They’re worth the extra cost if you weld in damp conditions or work on grounded surfaces frequently.

    Hearing Protection

    Arc welding generates 85-100 decibels of noise. Grinding and cutting push that well over 100 dB. Repeated exposure causes permanent, irreversible hearing damage. I have mild tinnitus from my early years of welding without ear protection.

    Use earplugs for welding alone. Add earmuffs when grinding or cutting. Combined protection provides better noise reduction. Electronic earmuffs amplify quiet sounds while blocking loud noise—great for workshop environments where you need to hear instructions.

    Electrical Safety: Preventing Shock Hazards

    Electrical safety deserves your complete attention. The welding machine produces lethal current under the right conditions. I’ve been shocked twice—both times because I got careless. Learn from my mistakes.

    Proper Grounding Procedures

    The workpiece must be properly connected to the welding machine’s work terminal. This is called the work lead or ground clamp. A poor connection causes the welding current to find alternate paths—possibly through you.

    I always connect my ground clamp to clean, bare metal. Paint, rust, and coatings are insulators. If the clamp won’t bite into the material, I grind or wire brush the contact area. For large assemblies, I connect multiple ground clamps to ensure good conductivity throughout.

    Never ground to structures that might carry current unexpectedly. I once saw a welder ground to a pipe that ran to another building. Unknown to him, that pipe was bonded to electrical conduit elsewhere. When he struck an arc, the current found multiple paths and created a shock hazard throughout both buildings.

    Working in Wet Conditions

    Water and electricity don’t mix. This is non-negotiable. Never weld in rain, standing water, or wet conditions. If you must weld outdoors in damp weather, take these precautions:

    1. Use dry rubber mats or wooden platforms to stand on
    2. Keep all electrical connections elevated and dry
    3. Wear dry rubber gloves underneath your welding gloves
    4. Use a ground fault circuit interrupter (GFCI) if available
    5. Consider postponing the work until conditions improve

    Sweat is also conductive. In hot weather, I keep a rag handy to wipe my hands and arms before touching electrical connections. I change gloves when they become soaked through.

    Equipment Inspection

    Inspect your welding equipment before every use. Damaged insulation, exposed conductors, and worn connections are shock hazards waiting to happen. I spend two minutes checking my cables before every welding session. Those two minutes have prevented at least three potential shocks over the years.

    Check for:

    • Cracks or cuts in cable insulation
    • Exposed conductors at connection points
    • Damage to electrode holders or torches
    • Loose or corroded connections
    • Worn trigger switches on MIG guns and TIG torches

    Replace damaged equipment immediately. Don’t tape over cut cables—that’s a temporary fix at best and a false sense of security at worst.

    Ventilation and Respiratory Protection

    Welding fumes are insidious. You can’t see most of them, and you often don’t notice the effects until years of exposure have accumulated. I take respiratory protection seriously—my lungs have to last me the rest of my life.

    Natural Ventilation

    Natural ventilation works for light welding in open areas. Open doors and windows on opposite sides of your workspace to create cross-ventilation. Position fans to blow fumes away from your breathing zone—not toward the weld or they’ll interfere with shielding gas.

    For a typical home garage, I recommend at least two sources of intake and exhaust. A 16-foot garage door plus a window on the opposite wall provides decent cross-ventilation for light Stick or MIG welding. This setup is adequate for welding mild steel for short periods.

    Mechanical Ventilation

    For production welding or confined spaces, natural ventilation isn’t enough. You need mechanical solutions:

    Ventilation TypeBest ForAirflow Required
    General ExhaustLarge open shops2,000+ CFM total room air changes
    Local ExhaustFixed welding stations100-150 CFM at capture point
    Portable Fume ExtractorFlexible positioning150-300 CFM adjustable
    Downdraft TableBench welding100-150 CFM through table surface

    Local exhaust ventilation captures fumes at the source—the most effective approach. A flexible arm fume extractor positioned 6-12 inches from the weld zone captures the majority of fumes before they disperse. I use one in my home shop for any welding session longer than 15 minutes.

    Respiratory Protection

    When ventilation isn’t adequate or you’re welding materials that produce toxic fumes, respiratory protection is mandatory. I use respirators for:

    • Stainless steel (contains chromium and nickel)
    • Galvanized steel (zinc fumes)
    • Painted or coated materials
    • Confined spaces
    • Extended welding sessions in any material

    For most welding, a half-face respirator with P100 filters provides adequate protection. These filters capture 99.97% of particles down to 0.3 microns. Replace filters regularly—when breathing becomes difficult or after 40 hours of use, whichever comes first.

    For high-production environments or confined spaces, consider a powered air-purifying respirator (PAPR). These systems use a blower to pull air through filters and deliver it to your helmet. They’re more expensive but much more comfortable for all-day use.

    Metal Fume Fever: A flu-like condition caused by inhaling metal oxide fumes, typically from zinc oxide when welding galvanized steel. Symptoms include fever, chills, nausea, muscle aches, and headache. Symptoms appear 4-12 hours after exposure and typically resolve within 24-48 hours. Repeated episodes indicate excessive exposure.

    Fire Prevention and Hot Work Procedures

    I’ve responded to three welding-related fires in my career. Two were small—one extinguisher handle and done. The third burned through an exterior wall and caused $80,000 in damage. All three were preventable.

    Establishing a Safe Welding Area

    Before you strike an arc, clear the area. This means a 35-foot radius in all directions. Remove or protect anything that can burn. I scan my welding area for:

    • Paper, cardboard, and packaging materials
    • Wood scraps and lumber
    • Oil-soaked rags
    • Gasoline, paints, and solvents
    • Dry leaves and vegetation (for outdoor welding)
    • Floor cracks and openings where sparks can fall

    For flammable materials that can’t be moved, cover them with fire-resistant welding blankets. These are made from fiberglass or silica fabrics that can withstand direct flame. I use them when welding near vehicles, machinery, or building components that can’t be relocated.

    Fire Extinguishers: Essential Equipment

    Keep a fire extinguisher within 10 feet of your welding area. Know how to use it before you need it. The last thing you want to be doing during a fire is reading instructions.

    For welding, I recommend an ABC-rated extinguisher with at least a 10-pound capacity. This classification covers:

    • Class A: Ordinary combustibles (wood, paper, cloth)
    • Class B: Flammable liquids (gasoline, oil, paint)
    • Class C: Electrical fires

    Check your extinguisher monthly. Verify the pressure gauge is in the green zone. Inspect the hose and nozzle for damage. Shake dry chemical extinguishers occasionally to prevent the agent from packing down.

    The Fire Watch: When It’s Required

    A fire watch is a person assigned to monitor for fires during and after hot work. They’re required when:

    • Welding near combustible materials that couldn’t be moved
    • Working in areas with concealed combustible spaces (walls, ceilings)
    • Welding in confined spaces
    • Required by workplace policy or local regulations

    The fire watch continues for at least 30 minutes after welding stops. Many fires start well after the weld is complete because sparks smolder undetected. I’ve seen this happen—a spark landed in cardboard inside a cabinet and smoldered for 45 minutes before bursting into flame.

    Hot Work Permits?

    Commercial and industrial settings often require hot work permits for welding. These documents ensure that:

    • The fire department is notified
    • Flammable materials are removed or protected
    • Fire extinguishers are present
    • A fire watch is assigned
    • Fire detection and suppression systems are functional

    Even in home workshops, I recommend following hot work permit procedures. Treat your home with the same respect as a commercial facility. Your family and neighbors deserve the same protection as industrial workers.

    Safe Work Practices: Your Daily Checklist

    Safety isn’t about what you know—it’s about what you do every single day. I’ve developed a checklist that I run through before every welding session. These habits have kept me safe through thousands of hours of welding.

    Pre-Welding Safety Checklist

    Before you strike an arc, complete these steps:

    1. Inspect your PPE: Check helmet lens for cracks, gloves for holes, boots for damage
    2. Check fire extinguisher: Verify it’s charged and accessible
    3. Clear the area: Remove combustibles within 35 feet
    4. Inspect welding equipment: Check cables, connections, and torch for damage
    5. Verify ground connection: Ensure work lead is securely attached to clean metal
    6. Assess ventilation: Confirm adequate airflow or prepare respirator
    7. Check for fire hazards: Look for openings where sparks could travel
    8. Protect bystanders: Set up welding screens or post warning signs

    During Welding: Stay Alert

    Maintain awareness while you weld. It’s easy to get focused on the weld bead and forget your surroundings. I make a conscious effort to:

    • Monitor where sparks are landing
    • Watch for smoke indicating hidden fires
    • Stay aware of people entering the area
    • Notice if ventilation becomes inadequate
    • Pay attention to physical discomfort or overheating

    Take breaks when needed. Fatigue leads to mistakes. I stop every hour for a few minutes to hydrate and assess my surroundings. In hot weather, I take breaks more frequently. Heat stress is real, and it impairs judgment.

    Post-Welding Procedures

    The job isn’t done when you finish welding. Follow these shutdown procedures:

    1. Turn off welding machine: At the machine, not just the gun trigger
    2. Release gas pressure: For MIG/TIG, close cylinder valve and bleed lines
    3. Inspect the work area: Look for smoldering materials
    4. Check adjacent areas: Sparks travel—look beyond immediate work area
    5. Continue fire watch: Wait 30-60 minutes before leaving unattended
    6. Store equipment properly: Coiled cables, secured cylinders, organized workspace

    Confined Space Welding

    Welding in confined spaces—tanks, vessels, pits, crawl spaces—requires extra precautions. These spaces have limited ventilation and restricted exits. Several welders die annually in confined space incidents.

    Confined Space: An area large enough to enter and perform work, with limited or restricted means of entry or exit, and not designed for continuous human occupancy. Examples include tanks, vessels, pits, silos, bins, and crawl spaces. Confined spaces may contain hazardous atmospheres, engulfment hazards, or other serious safety risks.

    Before entering a confined space for welding:

    1. Test the atmosphere: Use gas detectors to check for oxygen levels and toxic gases
    2. Ensure continuous ventilation: Provide fresh air intake and exhaust
    3. Have a rescue plan: Someone outside must be equipped and trained for rescue
    4. Use respiratory protection: Air-supplied respirator may be required
    5. Lockout/tagout equipment: Prevent unexpected activation of machinery
    6. Ground the workpiece: Eliminate electrical shock paths
    7. Use low-voltage equipment: Reduce shock hazard when possible

    Emergency Response and First Aid

    Despite every precaution, accidents happen. Knowing how to respond makes the difference between a minor incident and a tragedy. I keep first aid supplies in my shop and refresh my training annually.

    Fire Response: Act Fast

    If a fire starts while welding:

    1. Stop welding immediately: Turn off the machine
    2. Sound the alarm: Yell “FIRE” and activate alarms if available
    3. Attack small fires: Use extinguisher if fire is smaller than a trash can
    4. Evacuate for large fires: Don’t attempt to fight fires beyond your capacity
    5. Call emergency services: Dial 911 from a safe location

    Remember the PASS method for using extinguishers:

    • Pull the pin
    • Aim at the base of the fire
    • Squeeze the handle
    • Sweep side to side

    Electrical Shock: Immediate Action

    If someone receives an electrical shock:

    1. Don’t touch the victim: You could become a second victim
    2. Turn off power: Shut down the welding machine or unplug it
    3. Call 911 immediately: Electrical shock can cause heart arrhythmia
    4. Check for breathing: Begin CPR if necessary and you’re trained
    5. Don’t move the victim: Unless in immediate danger from fire or further shock

    Even if the victim appears fine, seek medical attention. Electrical shock can cause internal injuries and cardiac issues that aren’t immediately apparent.

    Eye Injury: Arc Eye Treatment

    If you suspect arc eye or flash burns:

    1. Remove contact lenses: If wearing them
    2. Flush eyes with water: Use saline or clean water for 15 minutes
    3. Avoid light: Stay in a darkened room or wear sunglasses
    4. Use cold compresses: Apply to closed eyes to relieve pain
    5. Seek medical attention: If symptoms are severe or persist

    Arc eye typically heals within 24-48 hours. A doctor can prescribe antibiotic ointment to prevent infection and pain medication for comfort. Never ignore eye symptoms—delayed treatment can lead to complications.

    Burn Treatment: Cool and Cover

    For minor burns from welding:

    1. Cool the burn: Hold under cool running water for 10-15 minutes
    2. Remove constricting items: Rings, bracelets, or tight clothing near the burn
    3. Cover loosely: Use sterile gauze or a clean cloth
    4. Don’t apply ice: It can damage tissue further
    5. Don’t pop blisters: They protect against infection
    6. Seek medical care: For burns larger than your palm, deep burns, or burns on face/hands/genitals

    Training, Certification, and Compliance

    Safety knowledge is useless without continuous practice and reinforcement. I’ve been welding for 15 years and still attend safety training annually. Regulations and best practices evolve. Stay current.

    OSHA Standards Overview

    OSHA Standard 1910.254 covers welding, cutting, and brazing. Key requirements include:

    • Fire prevention and protection measures
    • Personal protective equipment requirements
    • Health protection and ventilation standards
    • Confined space procedures
    • Equipment inspection and maintenance

    Employers must provide training on hazards and protective measures. Employees must follow all safety procedures and use provided PPE. As a DIY welder, you are both employer and employee—hold yourself to professional standards.

    AWS Certification Programs

    The American Welding Society offers certification programs that include safety training. The Certified Welder (CW) and Certified Welding Inspector (CWI) programs both emphasize safety alongside technical skills. Even if you don’t pursue certification, the AWS safety resources are freely available and excellent.

    Continuous Learning

    Safety isn’t a one-time lesson. It’s a mindset developed through continuous learning and practice. I read safety bulletins, watch training videos, and learn from near-misses. Every close call is a lesson—if you pay attention.

    Frequently Asked Questions

    What are the hazards of arc welding?

    Arc welding creates five primary hazards: electric shock from high-voltage equipment that can be lethal; UV and infrared radiation causing arc eye and skin damage; toxic welding fumes containing metal particles that can cause long-term health issues; fire and explosion risks from sparks and hot metal; and burns from contact with molten metal and heated workpieces.

    What PPE is required for arc welding?

    Arc welding PPE requirements include: a welding helmet with appropriate shade lens (typically shade 10-14), safety glasses with side shields, fire-resistant clothing covering all skin, leather welding gloves (heavy for Stick/MIG, lighter for TIG), steel-toed leather boots, and respiratory protection when ventilation is inadequate. Additional PPE may include hearing protection, welding aprons or jackets, and face shields for grinding.

    How do you protect your eyes when arc welding?

    Protect your eyes when arc welding by wearing a welding helmet with the correct shade lens for your process and amperage, using safety glasses underneath your helmet to block reflected UV radiation, and ensuring no gaps exist between your helmet and face. Never look at the arc without proper eye protection, even briefly. UV damage can occur in less than one second of exposure.

    Is arc welding smoke dangerous?

    Yes, arc welding smoke contains harmful metal oxides and gases that can cause both acute and chronic health problems. Short-term exposure can cause metal fume fever—flu-like symptoms from zinc oxide fumes. Long-term exposure to manganese, chromium, nickel, and other metals can cause neurological damage, respiratory issues, and increased cancer risk. Always use adequate ventilation or respiratory protection.

    What type of gloves should be used for arc welding?

    Glove selection depends on the welding process. For Stick and MIG welding, use thick leather gloves (Elkskin or cowhide) that extend past your elbows for maximum heat and spark protection. For TIG welding, use thin goatskin or pigskin gloves that provide finger dexterity for precise torch and filler control. Never use synthetic gloves—they melt when exposed to sparks or heat.

    How much ventilation do you need for welding?

    General welding areas require at least 2,000 cubic feet per minute (CFM) of airflow for adequate ventilation. Local exhaust ventilation should capture fumes at the source with a minimum capture velocity of 100 feet per minute. For confined spaces or welding toxic materials like stainless steel, mechanical ventilation or air-supplied respirators are mandatory. If you can smell fumes or see smoke lingering, ventilation is insufficient.

    Can you weld without a helmet?

    No, never weld without a helmet. The welding arc produces intense UV radiation that can damage your eyes in less than one second—a condition called arc eye or photokeratitis. Symptoms include severe pain, light sensitivity, and vision loss that appear 6-12 hours after exposure. Repeated exposure can cause permanent vision damage including cataracts. Always wear a properly rated welding helmet with the correct shade lens.

    What are OSHA requirements for welding?

    OSHA Standard 1910.254 covers welding, cutting, and brazing. Key requirements include: maintaining fire-safe areas with 35-foot clearance from combustibles, providing fire extinguishers, ensuring adequate ventilation or respiratory protection, requiring appropriate PPE, grounding workpieces properly, inspecting equipment before use, and implementing confined space procedures. Employers must train workers on hazards and protective measures.

    How far should flammable materials be from welding?

    Flammable materials should be kept at least 35 feet away from welding operations according to OSHA standards. If materials cannot be moved, they must be covered with fire-resistant welding blankets or protected with metal shields. This 35-foot radius accounts for sparks that can travel substantial distances and remain hot enough to ignite combustibles. Always scan beyond the immediate area for hidden fire hazards.

    What shade lens for arc welding?

    Shade number depends on welding process and amperage. For Stick welding under 60A use shade 7-8; 60-160A use shade 10; 160-250A use shade 12. For MIG welding 60-160A use shade 10; 160-300A use shade 12-13. For TIG welding under 50A use shade 8-9; 50-150A use shade 10-11. Carbon arc gouging always requires shade 14. When in doubt, start darker—you can always adjust down.

    Can welding cause permanent eye damage?

    Yes, welding can cause permanent eye damage. UV radiation from the welding arc can burn your corneas (arc eye), and while this typically heals, repeated exposure increases risk of cataracts and retinal damage. Chronic exposure may contribute to macular degeneration. Infrared radiation from welding can also cause lens opacity and retinal burns. Always wear properly rated eye protection with the correct shade number.

    How do you prevent electric shock when welding?

    Prevent electric shock by: inspecting cables and equipment for damage before use, keeping your work area and body dry, wearing dry gloves, using insulation mats when welding on grounded surfaces, never touching live electrical parts with bare skin, ensuring proper grounding of the workpiece, turning off power before changing parts or adjusting settings, and never welding in wet or damp conditions. Always assume equipment is energized until proven otherwise.

    What should you wear when welding?

    Wear a welding helmet with correct shade lens, safety glasses underneath, fire-resistant clothing covering all skin (long sleeves, long pants), leather welding gloves appropriate to your process, leather boots with steel toes, and a respirator when ventilation is inadequate. Avoid synthetic fabrics that melt into skin—choose natural fibers like cotton, wool, or leather. For heavy production work, invest in fire-resistant treated clothing. High-top boots prevent sparks from entering.

    Do you need a respirator for welding?

    You need a respirator for welding when ventilation is inadequate, when welding materials that produce toxic fumes (stainless steel, galvanized steel, painted or coated metals), when working in confined spaces, or during extended welding sessions. A half-face respirator with P100 filters is adequate for most situations. For high-production environments or confined spaces, a powered air-purifying respirator (PAPR) provides better protection and comfort.

    What is arc eye and how is it treated?

    Arc eye (photokeratitis) is a painful eye condition caused by unprotected exposure to UV radiation from welding arcs. It’s essentially a sunburn on your corneas. Symptoms appear 6-12 hours after exposure and include severe eye pain, light sensitivity, excessive tearing, and the sensation of sand in your eyes. Treatment includes removing contact lenses, flushing eyes with water or saline, staying in a darkened room, using cold compresses for pain relief, and seeking medical attention if symptoms are severe or don’t improve.

    Download this safety checklist and keep it in your workshop. Review it before every welding session. Print copies for your team. Post it near your welding station. Safety isn’t complicated—but it is essential. Your health, your livelihood, and your life depend on getting it right every single time.

  • Cast Iron Welding: Complete Guide to Successful Repairs

    Cast Iron Welding: Complete Guide to Successful Repairs

    Cast iron welding is one of those tasks that makes experienced welders pause. I’ve been welding for 15 years, and I’ll be honest – my first few cast iron repairs ended in cracks and frustration. The material is unforgiving, but once you understand how to work with it instead of against it, successful repairs become repeatable.

    Can you weld cast iron? Yes, but it requires different techniques than welding steel. Stick welding with nickel-based electrodes and proper preheating is the most reliable method for most repairs.

    In this guide, I’ll share everything I’ve learned from hundreds of cast iron repairs, including the mistakes that cost me thousands in scrapped parts and the techniques that finally made my repairs hold.

    Understanding Cast Iron: Why It’s So Difficult to Weld

    Cast iron contains 2-4% carbon – roughly 10 times more carbon than mild steel. This high carbon content makes cast iron hard and brittle, which is great for engine blocks and machinery bases but terrible for welding.

    Heat Affected Zone (HAZ): The area of base metal near the weld that wasn’t melted but was still affected by the welding heat. In cast iron, this zone becomes extremely brittle and prone to cracking.

    When you weld cast iron, the intense heating and cooling creates thermal stress. Steel can flex and accommodate this stress, but cast iron simply cracks. The heat-affected zone becomes even more brittle than the base metal, creating a weak point right next to your weld.

    Quick Summary: Cast iron’s high carbon content (2-4%) makes it inherently brittle. Welding creates thermal stress that this brittle material cannot handle without special techniques including preheating, controlled cooling, and ductile filler metals.

    Types of Cast Iron and Weldability

    Not all cast iron is the same. Understanding what type you’re working with is essential because weldability varies dramatically:

    Type Carbon Form Weldability Common Uses
    Gray Cast Iron Graphite flakes Best – Most common Engine blocks, manifolds
    Ductile (Nodular) Iron Nodular graphite Good Pipe, automotive parts
    Malleable Iron Tempered carbon Fair Hardware, fittings
    White Cast Iron Iron carbide Very Poor – Avoid Wear surfaces, crushers

    Gray cast iron is what you’ll encounter 80% of the time. It’s the most weldable because the graphite flakes provide some stress relief. White cast iron is virtually unweldable – if you identify this material, consider replacement instead of repair.

    How to Identify Your Cast Iron Type?

    I’ve developed a simple field test that works most of time. Scratch the metal in an inconspicuous area:

    1. If the scratch produces gray powder and feels slightly gritty = Gray cast iron (good for welding)
    2. If the scratch feels smooth and the metal looks silvery-white = White cast iron (avoid welding)
    3. If you can bend a thin section without it snapping = Ductile iron (weldable)
    4. When in doubt, assume it’s gray cast iron and proceed with preheat

    Pre-Weld Preparation: The Foundation of Success

    I can’t stress this enough: 80% of cast iron welding success happens before you strike an arc. Proper preparation separates repairs that hold from those that crack days later.

    Step 1: Clean the Area Thoroughly

    Cast iron is porous like a sponge. Over decades, it absorbs oil, grease, and contaminants. These contaminants create porosity and weak welds if not removed.

    I use a three-step cleaning process:

    1. Degrease: Apply acetone or brake cleaner and let it soak for 5 minutes. The oil will start seeping out – wipe and repeat until no more oil appears.
    2. Heat clean: Use a propane torch to gently heat the area to about 200°F. This drives out deep-seated oil and moisture.
    3. Grind clean: Use a grinding wheel to remove all surface material down to bare metal. You should see clean, gray cast iron with no discoloration.

    Step 2: Crack Preparation

    For crack repairs, you need to stop the crack from propagating and create proper geometry for welding:

    Pro Tip: Always drill stop holes at both ends of a crack before welding. Use a drill bit slightly larger than the crack width, drilling about 1/8″ past the visible crack end. This prevents the crack from continuing during welding.

    After drilling stop holes, grind a V-groove along the crack. The groove should be approximately 60-90 degrees and deep enough to reach the bottom of the crack. For thick sections (over 1/2″), consider a U-groove or double-V preparation.

    Essential Preparation Tools

    Angle Grinder
    4-1/2″ minimum
    Carbide Burr
    For precision
    Drill Bits
    Cobalt preferred
    Wire Wheel
    Cleaning

    Welding Methods Compared: Choosing the Right Approach

    Different welding processes work better for different situations. After trying every method on dozens of repairs, here’s my honest assessment:

    Method Difficulty Best For Pros Cons
    Stick (SMAW) Moderate Most repairs High heat input, forgiving, equipment common Slower, slag removal
    TIG (GTAW) High Thin sections, precision Clean, precise control Requires skill, slower heat input
    MIG (GMAW) Moderate-High Production, thick sections Fast, consistent Requires special wire, less forgiving
    Oxy-Acetylene Brazing Low-Moderate Non-structural, thin castings No phase change, low heat Lower strength, not true welding

    For most DIY and repair applications, stick welding with nickel electrodes is the best choice. It provides the heat input needed for cast iron while being more forgiving than TIG or MIG.

    Can You Weld Cast Iron with a MIG Welder?

    Yes, but it’s not my first recommendation. MIG welding cast iron requires nickel wire (expensive and sometimes hard to find) and precise heat control. The constant heat input of MIG makes thermal management more difficult.

    If you only have a MIG available, use nickel wire with 100% argon shielding gas, keep heat low, and weld in very short bursts. But if you’re planning to do multiple cast iron repairs, investing in a basic stick welder will save you frustration.

    Electrode Selection: Picking the Right Filler Metal

    The filler metal you choose makes or breaks the repair. Cast iron’s brittleness means we need a filler that’s more ductile – something that can flex slightly and absorb stress.

    Nickel Electrodes: The Gold Standard

    Nickel-based electrodes are the go-to choice for cast iron welding. They’re expensive but worth every penny for critical repairs.

    ENi-CI (Nickel 99): Pure nickel electrode with 99% nickel content. Provides the most ductile weld deposit, machinable, and ideal for single-pass repairs on thin sections.

    • Nickel 99 (ENi-CI): Best for single-pass welds, thin sections, and when you need to machine the weld afterward. Most ductile option.
    • Nickel 55 (ENiFe-CI): Nickel-iron alloy, stronger but less ductile. Better for multi-pass welds and thick sections. More affordable than pure nickel.
    • Steel electrodes: Only for non-critical repairs. The weld will be hard and difficult to machine. I only use these for temporary fixes.

    I typically start with Nickel 99 for most repairs. The extra ductility helps compensate for any imperfections in my preparation. For thick repairs requiring multiple passes, I’ll use Nickel 55 for strength.

    Step-by-Step Cast Iron Welding Process

    Follow this exact sequence and your cast iron welds will be dramatically more successful.

    Step 1: Preheat the Cast Iron

    Preheating is non-negotiable for successful cast iron welding. It reduces thermal stress by minimizing the temperature difference between the weld and surrounding metal.

    Preheat Temperature Guide by Cast Iron Type:

    Cast Iron Type Minimum Preheat Ideal Preheat Method
    Gray Cast Iron 400°F (200°C) 500-900°F (260-480°C) Oven or torch
    Ductile Iron 300°F (150°C) 400-600°F (200-315°C) Oven or torch
    Malleable Iron 200°F (95°C) 300-500°F (150-260°C) Torch

    For small parts, an oven works great. I’ve used kitchen ovens for exhaust manifolds (with the wife’s permission, of course). For larger parts like engine blocks, use a rosebud tip on an oxy-acetylene torch or propane torch. Heat the entire casting evenly, not just the weld area.

    Temperature Check: An infrared thermometer costs $30-50 and is invaluable. If you don’t have one, cast iron at 500°F will show a faint red glow in darkness and water will sizzle rapidly when touched to the surface.

    Step 2: Weld in Short Segments

    This is where most beginners fail. Long, continuous welds generate too much heat and guarantee cracks.

    Follow these rules:

    1. Weld in 1-inch segments maximum
    2. Move to a different location between welds (skip welding)
    3. Let each segment cool slightly before the next
    4. Never weld more than 10x the electrode diameter in one spot

    I mark 1-inch intervals with soapstone before starting. After each inch of weld, I move to the opposite end of the repair. This skip-welding technique distributes heat and prevents any single area from getting too hot.

    Step 3: Peen While Hot

    Peening is lightly hammering the weld while it’s still hot (around 800-1000°F). This mechanical working relieves internal stresses and prevents cracking during cooling.

    Use a ball-peen hammer and tap the weld beads immediately after welding while they’re still glowing red. Don’t beat it – just gentle tapping. The weld should yield slightly like soft clay.

    Critical Timing: Peen only while the weld is hot but plastic. Too cold and you’ll work-harden the metal, making cracks more likely. The sweet spot is when the weld has lost its bright red glow but is still too hot to touch for more than a second.

    Step 4: Control Interpass Temperature

    For multi-pass welds, maintain interpass temperature between weld layers. Don’t let the part cool completely between passes, but don’t let it get too hot either.

    I aim for 300-400°F between passes. Use your infrared thermometer or the water sizzle test. If the part drops below 250°F, reheat gently before the next pass.

    Slow Cooling: The Final Secret to Success

    After welding, how you cool the part is just as important as how you welded it. Rapid cooling is the number one cause of post-weld cracks.

    Cooling Methods

    1. Bury in dry sand or vermiculite: This provides insulation and allows slow, even cooling over several hours.
    2. Wrap in welding blankets: Specialized thermal blankets retain heat and slow cooling. Cost $30-60 and are worth it.
    3. Controled oven cooling: If you used an oven for preheat, simply turn it off and let the part cool inside with the door closed.
    4. Air cooling (for small parts): Simply let the part cool naturally in still air, away from drafts.

    Never quench cast iron in water or expose it to cold air immediately after welding. I learned this the hard way when a cracked engine block repair I spent 3 hours on shattered instantly when a breeze hit it.

    Post-Weld Heat Treatment (Optional)

    For critical repairs, consider post-weld stress relief. Heat the entire part to 1100-1200°F, hold for one hour per inch of thickness, then cool at 100°F per hour maximum.

    This isn’t necessary for most repairs, but for expensive or safety-critical parts, it’s cheap insurance.

    Crack Prevention Techniques That Actually Work

    After 15 years of cast iron welding, I’ve developed a crack prevention checklist. Follow these and your success rate will dramatically improve.

    Crack Prevention Checklist

    1. Preheat minimum 400°F – No exceptions, ever
    2. Drill stop holes – At both ends of every crack
    3. Weld in 1-inch segments – Never exceed this length
    4. Use skip welding – Distribute heat across the repair
    5. Peen every weld – While still hot and plastic
    6. Maintain interpass temperature – 300-400°F between passes
    7. Cool slowly – Insulate or bury in sand
    8. Avoid drafts – Never let cold air hit hot welds

    Common Mistakes That Cause Cracks

    I’ve made every mistake on this list. Learn from my failures so you don’t have to repeat them:

    • Rushing preparation: Inadequate cleaning leads to inclusions and weak welds
    • Skipping preheat: “Just this once” is how $500 parts become scrap
    • Welding too hot: High amperage seems faster but guarantees cracks
    • Long continuous welds: Anything over 1 inch is asking for trouble
    • Not peening: Takes 30 seconds and prevents 80% of cracks
    • Rapid cooling: Quenching or cold drafts destroy your work
    • Wrong filler: Steel electrodes on critical repairs is false economy

    Troubleshooting Common Cast Iron Welding Problems

    Even with proper technique, problems occur. Here’s my troubleshooting guide based on hundreds of repairs:

    Problem Cause Solution
    Cracks in HAZ Insufficient preheat, rapid cooling Increase preheat to 500°F+, slow cooling
    Porosity in weld Contamination, moisture Clean more thoroughly, dry electrodes
    Weld too hard to machine Wrong electrode, too hot Use Nickel 99, reduce amperage
    Crack propagates during welding No stop holes, stress concentration Drill stop holes at crack ends
    Undercutting Too hot, wrong angle Reduce amperage, adjust travel angle
    Crack appears next day Residual stress, rapid cool Better peening, slower cooling, stress relief

    Repair vs Replace: Making the Smart Choice

    Not every cast iron piece deserves welding. Sometimes replacement is smarter, cheaper, or safer. Here’s my decision framework:

    Quick Summary: Weld if the part is unavailable, expensive ($500+), or has sentimental value. Replace if new parts are affordable, safety is critical, or the cast iron is severely degraded.

    When to Weld

    • Replacement parts are unavailable or backordered for months
    • The part costs over $500 to replace
    • The equipment is vintage or irreplaceable
    • You have time to practice first on scrap
    • The repair is non-safety-critical

    When to Replace

    • New parts cost under $200 and are readily available
    • Safety-critical applications (brake components, pressure vessels)
    • The casting is severely corroded or oil-soaked
    • You’ve never welded cast iron before and the part is expensive
    • The part is under extreme stress or vibration in service

    Cost Comparison

    After tracking my repair costs over years, here’s what I’ve found:

    Engine Block Repair
    $50-150 DIY
    Exhaust Manifold Repair
    $30-80 DIY
    Professional Repair
    $200-1500
    Equipment Investment
    $300-800

    Break-even on equipment investment happens after 2-3 major repairs or 5-10 small ones. For a home mechanic with aging equipment, cast iron welding skills pay for themselves quickly.

    Beginner Practice Recommendations

    Don’t learn on your expensive engine block. I recommend practicing on these low-stakes projects first:

    1. Scrap exhaust manifolds: Available cheaply at salvage yards, similar thickness to what you’ll actually repair
    2. Cast iron pipe: Practice fillet welds and butt joints
    3. Old cookware: Skillets and dutch ovens are cheap practice material
    4. Intentional cracks: Cut and notch scrap pieces, then practice repair techniques

    Spend 10-20 hours practicing before attempting a critical repair. The skills you develop – heat control, rhythm, peening technique – can’t be rushed.

    Safety Considerations

    Cast iron welding introduces specific hazards beyond general welding:

    • Zinc fumes: Galvanized coatings on nearby parts produce toxic fumes when heated. Remove or avoid welding near them.
    • Smoke from contaminants: Oil and grease burning off produces hazardous smoke. Clean thoroughly and use adequate ventilation.
    • Eye protection: Cast iron produces more UV radiation than steel. Use a proper welding helmet with at least shade 10.
    • Fire hazard from preheating: Ovens and torches can ignite surrounding materials. Clear your work area.
    • Heavy lifting: Cast iron parts are heavy. Use proper lifting techniques and mechanical assistance when needed.

    Frequently Asked Questions

    What is the best weld for cast iron?

    Stick welding (SMAW) with nickel-based electrodes is the best method for most cast iron welding applications. Nickel 99 (ENi-CI) provides excellent ductility and machinability for single-pass repairs. For thicker sections requiring multiple passes, Nickel 55 (ENiFe-CI) offers higher strength. The key is using nickel filler which is more ductile than the brittle cast iron base metal.

    Which welding rod is best for cast iron?

    Nickel 99 (ENi-CI) is the best all-purpose electrode for cast iron welding. It provides maximum ductility and machinability, making it ideal for thin sections and single-pass repairs. Nickel 55 (ENiFe-CI) is better for multi-pass welds on thicker sections. Steel electrodes like 7018 can work for non-critical repairs but produce hard, unmachinable welds and higher crack risk.

    What temperature should I preheat cast iron for welding?

    The minimum preheat temperature for cast iron welding is 400degF (200degC). For best results, preheat gray cast iron to 500-900degF depending on section thickness. Thicker sections require higher preheat. Use an infrared thermometer to verify temperature – the part should show a faint red glow in darkness at 500degF, and water should sizzle rapidly when touched to the surface.

    Why does cast iron crack when welding?

    Cast iron cracks during welding due to its high carbon content (2-4%) which makes it hard and brittle. The intense heating and cooling of welding creates thermal stress that cast iron cannot accommodate. The heat-affected zone becomes even more brittle than the base metal. Without proper preheating, controlled cooling, and ductile filler metals, this stress causes cracks to form either during welding or as the part cools.

    How do you stop cast iron from cracking when welding?

    Prevent cast iron welding cracks by: 1) Preheating to at least 400degF, 2) Welding in short 1-inch segments, 3) Using skip welding to distribute heat, 4) Peening each weld while hot with a ball-peen hammer, 5) Maintaining proper interpass temperature, 6) Slow cooling by burying in sand or wrapping in welding blankets. These techniques work together to manage thermal stress and prevent cracking.

    Can you weld cast iron with a MIG welder?

    Yes, but it’s more difficult than stick welding and not recommended for beginners. MIG welding cast iron requires special nickel wire which is expensive and sometimes hard to find. The continuous heat input of MIG makes thermal management more challenging. If you only have a MIG available, use nickel wire with 100% argon shielding gas, keep heat low, and weld in very short bursts. For multiple repairs, a basic stick welder is a better investment.

    What is the best wire for welding cast iron?

    For MIG welding cast iron, nickel-based wire is required. Nickel wire for MIG is available but expensive and not commonly stocked. The most reliable alternative is flux-core nickel wire which doesn’t require shielding gas. However, stick welding with nickel electrodes remains superior for most cast iron applications due to better heat control and more forgiving characteristics.

    How do you identify different types of cast iron before welding?

    Identify cast iron type with a simple scratch test in an inconspicuous area. If the scratch produces gray powder and feels gritty = gray cast iron (good for welding). If the metal looks silvery-white and feels smooth = white cast iron (avoid welding). If you can bend a thin section without it snapping = ductile iron (weldable). When in doubt, assume gray cast iron and proceed with full preheat precautions.

    Final Thoughts

    Cast iron welding is challenging but absolutely learnable. The techniques outlined in this guide have worked for me on hundreds of repairs, from cracked engine blocks to broken machinery bases.

    Start with proper preparation, never skip preheat, and always weld in short segments with peening. These fundamentals will carry you through 90% of cast iron repairs.

    For your first attempts, find scrap cast iron and practice. Expect some failures – everyone cracks their first few cast iron welds. But with patience and practice, you’ll develop the feel for heat management and timing that makes successful repairs repeatable.

    When in doubt, preheat more and weld slower. You can always add more weld, but you can’t undo a crack from rushing the process.

  • Carbon Arc Cutting Explained: Equipment, Benefits September 2026

    Carbon Arc Cutting Explained: Equipment, Benefits September 2026

    Carbon arc cutting is one of the most powerful metal removal processes in industrial fabrication. When I first encountered it in a shipyard, I watched a welder slice through inch-thick steel plate like butter, leaving a clean groove in seconds. The speed and raw power of CAC carbon arc cutting make it indispensable for heavy industry.

    Air carbon arc cutting (CAC-A) is a thermal cutting process that uses a carbon or graphite electrode to create an electric arc that melts metal. A high-velocity jet of compressed air then blows away the molten metal, allowing for cutting or gouging operations. CAC can cut all metal types including stainless steel and cast iron that oxy-fuel cannot process.

    After working with fabrication shops across the country, I have seen CAC carbon arc cutting become the go-to method for weld removal, back gouging, and preparing joints. The process handles everything from maintenance welding repairs to full-scale structural steel fabrication. It works in any position, cutting through materials that would stop other thermal cutting methods cold.

    How Carbon Arc Cutting Works?

    Quick Summary: Carbon arc cutting uses an electric arc between a carbon electrode and the workpiece to melt metal (up to 6,000F). Compressed air flowing through the electrode holder blows the molten metal away, creating a cut or groove. The process requires a constant current power source, compressed air at 80-100 PSI, and proper polarity settings.

    The physics behind CAC carbon arc cutting rely on two simultaneous actions. First, an electric arc forms between the carbon electrode and the metal workpiece. This arc generates intense heat, reaching temperatures up to 6,000 degrees Fahrenheit. At these temperatures, virtually any metal melts within seconds.

    As the metal liquefies, the second critical action takes place. Compressed air flows through the electrode holder and exits at high velocity directly behind the arc. This air jet, typically at 80-100 PSI, blasts the molten metal away from the workpiece. The result is a clean cut or groove without the oxidation that occurs with oxy-fuel cutting.

    The carbon electrode itself plays a vital role. Unlike coated welding electrodes, carbon electrodes conduct current while withstanding extreme arc temperatures. They gradually wear down during use, consuming at rates between 6-12 inches per hour depending on amperage and application.

    Cutting vs. Gouging: What’s the Difference?

    Cutting: Severing metal completely by penetrating through the entire thickness. The electrode moves continuously along the cut line.

    Gouging: Removing a portion of metal without cutting through completely. Creates a groove or cavity for weld preparation or defect removal.

    In my experience, gouging accounts for about 70% of CAC applications. Back gouging for full penetration welds, removing defective welds, and preparing joints are far more common than cutting through plate. The control you have with gouging lets you create precise grooves for later welding.

    Cutting through material requires higher amperage and larger electrodes. The goal is complete penetration, so you need enough heat to melt through the entire thickness. Gouging uses lower amperage and smaller electrodes for better control of groove depth and width.

    Essential Equipment for Carbon Arc Cutting

    Setting up for CAC carbon arc cutting requires specific equipment. I have seen shops try to cut corners and pay the price in poor results or equipment damage. Each component plays a critical role in the process.

    EquipmentSpecificationPurpose
    Power SourceConstant Current (CC), 200-600AProvides stable arc current
    Air Compressor5-50 CFM, 80-100 PSIDelivers high-velocity air jet
    Electrode HolderRated for electrode size and amperageHolds electrode, conducts current and air
    Carbon Electrodes1/8″ to 5/8″ diameter, DC or ACCreates arc, withstands heat
    Air Hose3/8″ to 1/2″ ID, minimum 25 ftDelivers compressed air to holder
    Ground Clamp300-600A rated, clean connectionCompletes electrical circuit

    Power Source Requirements

    The welding machine for CAC carbon arc cutting must be a constant current (CC) power source. Unlike constant voltage (CV) machines used for MIG welding, CC maintains stable amperage as the arc length varies. This stability is crucial for consistent cutting and gouging results.

    Most shops use existing DC welding machines. A 300-amp CC welder handles most applications up to 1/2 inch material. Heavy-duty work on thicker materials requires 400-600 amps. I have worked with maintenance crews who successfully used 200-amp machines for light gouging, but you are limited on electrode size and cutting capacity.

    For standard CAC-A operations, connect the electrode to the negative terminal (DCEN or DC electrode negative). This reverse polarity setup produces the most stable arc and fastest electrode consumption. AC-only machines require special AC carbon electrodes, but DC provides better results in most applications.

    Air Requirements

    Nothing stops a CAC operation faster than inadequate air supply. The compressed air does the actual work of removing molten metal. Without sufficient volume and pressure, the process fails regardless of how much amperage you have.

    Electrode SizeAmperage RangeCFM RequiredMin. Compressor HP
    1/8″ (3.2mm)60-150A5-8 CFM1.5-2 HP
    3/16″ (4.8mm)150-250A8-15 CFM3-5 HP
    1/4″ (6.4mm)250-400A15-25 CFM5-7.5 HP
    3/8″ (9.5mm)350-550A25-35 CFM7.5-10 HP
    1/2″ (12.7mm)500-700A35-50 CFM10-15 HP

    Air pressure should be set between 80-100 PSI at the torch. Higher pressure improves metal removal but increases electrode consumption and spark throw. I typically start at 90 PSI and adjust based on the application.

    Carbon Electrodes

    Carbon electrodes come in various sizes and compositions. Standard electrodes are a mixture of carbon and graphite. Pure graphite electrodes offer cleaner cutting with less carbon pickup but cost significantly more.

    Electrode diameter directly affects cutting capacity and amperage requirements. Small electrodes (1/8″) work well for light gouging and precision work. Large electrodes (3/8″ to 1/2″) handle heavy-duty cutting and deep gouging in thick materials.

    In my work with railroad maintenance teams, we primarily use 1/4″ electrodes as a versatile all-around size. They handle most gouging tasks while still providing enough capacity for cutting through rail sections when needed.

    Applications and Uses of Carbon Arc Cutting

    CAC carbon arc cutting serves numerous applications across heavy industry. The ability to remove metal quickly while working in any position makes it invaluable for maintenance and fabrication work.

    Weld Removal
    Back Gouging
    Cast Iron Repair
    Joint Preparation
    Defect Removal

    Weld Removal and Repair

    The most common application I encounter is removing defective or unwanted welds. When a weld fails inspection, carbon arc gouging removes it faster than any other method. The process cleanly extracts weld metal without damaging the base material, allowing for proper repair.

    I have worked with pressure vessel manufacturers who rely on CAC for removing root passes during rework. The precision of gouging lets them remove just the weld metal, leaving the base material intact for proper repair welding.

    Back Gouging

    Full penetration welds require back gouging from the reverse side. CAC carbon arc cutting excels at this application. After completing the root pass from one side, you gouge out the root from the opposite side before welding it out.

    This creates a clean, contoured groove that ensures complete fusion through the entire joint thickness. Shipyards use this technique extensively on hull plates and structural members. The ability to gouge overhead makes CAC ideal for shipbuilding where position welding is common.

    Cast Iron Repair

    Cast iron presents unique challenges for welding and cutting. Oxy-fuel cutting does not work on cast iron due to its lack of iron oxide. CAC cuts through cast iron cleanly, making it the preferred method for repairing castings.

    Engine blocks, machine bases, and agricultural equipment often require cast iron repair. I have helped machine shops salvage expensive castings by gouging out cracks and defects before welding repairs.

    Industrial Applications by Sector

    IndustryPrimary CAC UsesTypical Materials
    ShipbuildingBack gouging, weld removal, prep workMild steel, stainless steel
    Heavy EquipmentCrack repair, component rebuildSteel, cast iron, wear plate
    Structural SteelJoint prep, modification, demolitionA36 steel, alloy steels
    RailroadRail repair, frog replacementHigh carbon steel, manganese steel
    MiningEquipment repair, bucket rebuildWear resistant steels, AR plate

    Advantages and Disadvantages of Carbon Arc Cutting

    Like any industrial process, CAC carbon arc cutting has distinct strengths and limitations. Understanding these helps determine when CAC is the right choice for your application.

    Key Advantages

    1. Cuts All Metal Types: Unlike oxy-fuel cutting, CAC works on any conductive metal. Stainless steel, cast iron, aluminum, copper alloys—nothing is off-limits. This versatility makes CAC invaluable in mixed-material fabrication shops.
    2. Fast Metal Removal: No other manual method removes metal as quickly. I have watched skilled operators remove weld metal at rates exceeding 50 pounds per hour. For production gouging operations, this speed translates directly into cost savings.
    3. All-Position Capability: Work overhead? Underneath? In confined spaces? CAC handles all positions equally well. The gravity-independent air jet removes molten metal regardless of torch orientation. This flexibility makes CAC essential for field repair work.
    4. Cost-Effective Equipment: Most shops already have compatible welding machines. Adding CAC capability requires only the torch, air supply, and electrodes. Compared to plasma cutting systems with similar capacity, CAC equipment costs significantly less.
    5. Portable Operation: A CAC setup fits in a pickup truck. Field repairs on construction sites, farm equipment, or mining machinery become feasible with portable air supply. I have used CAC for on-site repairs in locations where bringing material to a shop was impossible.
    6. No Oxidation Required: Oxy-fuel cutting depends on rapid oxidation of iron. CAC works purely through melting and air blasting. This means cleaner cuts on materials susceptible to oxidation problems.

    Key Disadvantages

    1. Extreme Noise Levels: CAC generates noise up to 118 dB—comparable to a jet engine at close range. This necessitates dual hearing protection (ear plugs plus muffs) and creates workplace noise challenges. After a day of carbon arc work, your ears will ring without proper protection.
    2. Spark Throw: Molten metal sparks travel 20-30 feet from the work area. This creates significant fire hazards and requires clearing the work zone of flammable materials. I have seen sparks ignite debris 25 feet away during heavy gouging operations.
    3. Smoke and Fumes: The process generates substantial smoke, especially when cutting through coated or contaminated materials. Proper ventilation is non-negotiable. In confined spaces, respiratory protection becomes mandatory.
    4. Air Compressor Required: The compressed air requirement adds complexity and cost. High CFM needs mean large compressors or limited duty cycles. Portable operations become challenging when air supply is limited.
    5. Not for Precision Cutting: CAC is a rough cutting process. Tolerances are measured in fractions of an inch, not thousandths. For precision work, other methods like plasma or laser cutting produce superior results.
    6. Carbon Pickup: The carbon electrode can deposit carbon into the workpiece, particularly on stainless steels. This carbon pickup can affect corrosion resistance and requires additional cleaning before welding. Post-gouging grinding becomes necessary for critical applications.

    Preventing Carbon Pickup

    Carbon pickup remains a concern for stainless steel applications. The carbon electrode can transfer small amounts of carbon into the workpiece during gouging, potentially compromising corrosion resistance.

    To minimize carbon pickup on stainless steel:

    • Use copper-coated electrodes designed for stainless work
    • Keep the torch angle closer to perpendicular (less than 30 degrees from surface)
    • Grind at least 1/16″ of material from the gouged surface before welding
    • Consider mechanical gouging methods for critical stainless applications

    After consulting with food processing plant maintenance teams, I learned they avoid CAC on stainless steel surfaces that contact food products. For less critical stainless applications, proper post-gouging cleaning typically resolves any carbon pickup concerns.

    Safety Precautions for Carbon Arc Cutting

    Safety must be the top priority when working with CAC carbon arc cutting. The process combines electrical hazards, extreme heat, high-pressure air, and intense noise into one potentially dangerous operation.

    Hearing Protection

    The noise from CAC operations can cause permanent hearing damage in minutes. At 118 dB, exposure time before damage occurs is measured in seconds, not hours. This is not something to take lightly.

    HEARING PROTECTION IS MANDATORY:

    • Use dual protection: ear plugs PLUS ear muffs
    • Ensure proper fit for both devices
    • Replace ear plugs daily (or use reusable plugs cleaned regularly)
    • Take breaks in quiet areas to reduce cumulative exposure
    • Consider audiometric testing for regular CAC operators

    I have worked with welders who have permanent hearing loss from years of carbon arc work without proper protection. The damage is cumulative and irreversible. Hearing protection is not optional—it is essential.

    Eye and Face Protection

    The intense arc from CAC produces dangerous UV radiation, similar to welding. Without proper eye protection, arc flash (welder’s flash) can occur. This painful condition feels like sand in your eyes and can cause temporary blindness.

    A welding helmet with shade 10-14 provides adequate protection. For gouging operations, I recommend a shade 12 lens. Face shields add an extra layer of protection against flying sparks and debris, especially during overhead work.

    Safety glasses under the helmet protect against sparks that might find their way around the helmet seal. Polycarbonate lenses with side shields offer the best protection.

    Respiratory Protection and Ventilation

    CAC operations generate significant smoke and fumes. The composition varies depending on the base metal and any coatings present. Common contaminants include metal oxides, flux residues, and thermal decomposition products from paints or coatings.

    General ventilation guidelines:

    • Minimum 100 CFM airflow in the work area
    • Local exhaust ventilation recommended for any enclosed work
    • Position portable exhaust units to capture smoke at the source
    • Avoid standing directly in the smoke plume

    For confined space operations, respiratory protection becomes mandatory. An N95 respirator provides minimum protection for light work. For heavy gouging or work on coated materials, a powered air-purifying respirator (PAPR) offers superior protection.

    Fire Safety

    The spark throw from CAC creates significant fire hazards. Sparks can travel 20-30 feet and remain hot enough to ignite combustible materials. I personally witnessed a CAC operation ignite sawdust in a woodworking shop three bays away.

    Fire safety protocols:

    • Clear 30-foot radius of all combustible materials
    • Keep a fire extinguisher rated for Class ABC fires within reach
    • Assign a fire watch when working near combustible materials
    • Check behind walls and partitions for hidden combustibles
    • Welding blankets protect adjacent surfaces from spark damage
    • Monitor the work area for at least 30 minutes after completing work

    Electrical Safety

    CAC equipment operates at high amperage and voltages up to 80 volts open circuit. While less dangerous than high-voltage systems, the electrical hazards still demand respect.

    Electrical safety practices:

    • Inspect cables and connections before each use
    • Ensure proper grounding of the workpiece
    • Never touch the electrode holder with bare hands while powered
    • Use dry gloves and boots for insulation
    • Keep cables away from walking areas to prevent damage
    • Disconnect power before changing electrodes

    Step-by-Step Carbon Arc Cutting Guide

    Equipment Setup

    1. Connect the Power: Attach the work cable to the positive terminal and the electrode cable to the negative terminal (DCEN polarity). Ensure connections are tight and clean.
    2. Connect the Air: Attach the air hose to the electrode holder. Check all connections for leaks. A soap solution sprayed on fittings reveals air leaks quickly.
    3. Set the Pressure: Adjust the air compressor regulator to 90 PSI at the torch. Verify pressure with a gauge at the holder, not just at the compressor.
    4. Select Electrode Size: Choose the appropriate diameter for your application and material thickness. Larger electrodes remove more metal but require higher amperage.
    5. Set Amperage: Adjust the welder to the recommended amperage for your electrode size. A 1/4″ electrode typically runs at 300-400 amps for gouging.

    Preparing the Workpiece

    Clean the work area of any flammable materials within a 30-foot radius. Attach the ground clamp to clean bare metal, as close to the work area as possible. A poor ground connection causes erratic arc performance and can damage equipment.

    Mark your cut or gouge line clearly. For gouging operations, outline the groove width and depth with chalk or soapstone. Having a clear guide helps maintain consistent results.

    Striking the Arc

    Position the electrode at a 30-45 degree angle to the work surface. The air jet should point in the direction of travel. Hold the torch with both hands for stability.

    Tap the electrode against the workpiece like striking a match, then lift slightly to establish the arc. Once the arc forms, the air will begin flowing and metal removal starts immediately.

    A common mistake I see beginners make is holding the electrode too far from the work. Maintain a short arc length—about 1/8 to 1/4 inch. Longer arcs cause spatter and reduce cutting efficiency.

    Gouging Technique

    For gouging operations, move the torch smoothly along your marked line. The travel speed affects groove depth—slower creates deeper grooves, faster creates shallower ones. Maintain consistent torch angle and travel speed for uniform results.

    Weave the torch slightly side-to-side to widen the groove. The air jet naturally creates a U-shaped groove profile. Adjust torch angle to control the groove shape.

    For deep gouging, make multiple passes rather than trying to remove all material at once. Two or three lighter passes produce better control and cleaner results than one aggressive pass.

    Cutting Through Material

    When cutting completely through material, start at the edge if possible. Establish the arc and let it penetrate through the full thickness before beginning to travel. Move at a steady pace that allows complete penetration.

    For starting cuts in the middle of a plate, create a starter hole by holding the torch stationary until penetration occurs. Then begin your cut line from this point.

    Finishing Up

    After completing your cut or gouge, release the trigger and break the arc. The air continues flowing briefly to cool the electrode and clear remaining molten metal.

    Allow the workpiece to cool before handling. The freshly cut edges remain extremely hot immediately after cutting. Use pliers or tongs if you must move hot material.

    Clean the gouged surface with a wire brush to remove slag and carbon deposits. For welding applications, grind the surface to remove any carbon-affected layer before welding.

    Carbon Arc Cutting vs Other Cutting Methods

    Choosing the right cutting method depends on your specific application, material type, and available equipment. CAC excels in certain areas while other methods may be more appropriate for different tasks.

    FactorCarbon Arc (CAC)Plasma CuttingOxy-Fuel Cutting
    Metals That Can Be CutAll conductive metalsAll conductive metalsFerrous metals only
    Cut QualityRough, requires cleanupClean, preciseRough, slag buildup
    SpeedVery fast gougingFast cuttingMedium speed
    Equipment CostLow (uses welder + air)Medium to highLow to medium
    Operating CostElectrodes + electricity + airElectricity + consumablesOxygen + fuel gas
    PrecisionLow (+/- 1/8″)High (+/- 1/32″)Medium (+/- 1/16″)
    Noise LevelVery high (110-118 dB)Medium (80-100 dB)Medium (90-105 dB)

    When to Choose Carbon Arc Cutting?

    Select CAC when you need to remove metal quickly from any material type, particularly for gouging applications. The process dominates in weld removal, back gouging, and joint preparation. If you already own a CC welding machine and air compressor, CAC becomes the most economical choice for heavy metal removal.

    For cast iron work, CAC has no equal among manual processes. The ability to gouge and cut cast iron without preheating makes it indispensable for engine and equipment repair.

    When to Choose Plasma Cutting?

    Plasma cutting provides superior cut quality and precision. For fabrication work requiring clean edges or tight tolerances, plasma outperforms CAC. Plasma also produces less noise and fewer sparks, making it more suitable for shop environments.

    The higher equipment cost of plasma systems becomes justified when precision and cut quality matter. Production cutting operations typically choose plasma for cleaner results and faster cutting speeds on thinner materials.

    When to Choose Oxy-Fuel Cutting?

    Oxy-fuel excels at cutting thick ferrous materials (over 2 inches). For severing heavy steel plate, oxy-fuel often proves faster and more economical than CAC. The equipment is portable and requires no electricity, making it ideal for field work.

    However, oxy-fuel cannot cut non-ferrous metals like stainless steel, aluminum, or copper. For these materials, you must choose CAC or plasma.

    Frequently Asked Questions

    How many CFM do I need for carbon arc gouging?

    Air requirements vary by electrode size. Small electrodes (1/8 inch) need 5-8 CFM. Medium electrodes (1/4 inch) require 15-25 CFM. Large electrodes (3/8 to 1/2 inch) demand 25-50 CFM. Always size your compressor for the largest electrode you plan to use, plus a 20% safety margin for consistent air supply during extended gouging operations.

    What is the CAC-A cutting process?

    Air carbon arc cutting (CAC-A) is a thermal cutting process that uses a carbon or graphite electrode to create an electric arc melting the base metal. A high-velocity jet of compressed air then blows away the molten metal, allowing for cutting or gouging operations. The process works on all conductive metals including stainless steel and cast iron.

    Is carbon arc gouging CC or CV?

    Carbon arc gouging requires a Constant Current (CC) power source, not Constant Voltage (CV). CC welding machines maintain stable amperage as arc length varies, which is essential for consistent gouging results. Standard DC welding machines with CC output work well for CAC when set to DC electrode negative (DCEN) polarity.

    What are the disadvantages of carbon arc cutting?

    Key disadvantages include extreme noise levels up to 118 dB requiring dual hearing protection, sparks that travel 20-30 feet creating fire hazards, significant smoke and fumes requiring ventilation, high air compressor requirements (up to 50 CFM), lack of precision for fine work, and potential carbon pickup on stainless steels requiring post-gouging cleaning.

    What materials can you cut with carbon arc cutting?

    CAC works on all electrically conductive metals. This includes ferrous metals like carbon steel and alloy steels, non-ferrous metals like stainless steel, aluminum, copper, and brass, plus cast iron which oxy-fuel cannot cut. It is not recommended for reactive metals like titanium or zirconium without thorough post-cutting cleaning due to carbon pickup concerns.

    What are the main advantages of carbon arc cutting?

    Main advantages include the ability to cut all metal types (unlike oxy-fuel), very fast metal removal rates up to 50 pounds per hour, works in all positions including overhead, cost-effective using existing welding equipment, portable for field repairs, and does not require oxidation like oxy-fuel cutting. The process excels at gouging applications like weld removal and joint preparation.

    How loud is carbon arc gouging?

    Carbon arc gouging generates noise levels up to 118 dB, which is comparable to a jet engine at close range. This level causes permanent hearing damage in minutes without protection. Dual hearing protection (ear plugs plus ear muffs) is mandatory. The noise comes from the high-velocity air jet combined with the violent removal of molten metal.

    What PSI is needed for arc gouging?

    Air pressure of 80-100 PSI at the torch is recommended for carbon arc gouging. Higher pressure improves metal removal rate but increases electrode consumption and spark throw. Start at 90 PSI and adjust based on your specific application. Ensure your air compressor can maintain this pressure while delivering the required CFM for your electrode size.

    Conclusion

    CAC carbon arc cutting remains one of the most versatile and powerful metal removal processes available to industry. From shipyards to fabrication shops, the ability to quickly remove metal from any conductive material makes CAC indispensable for maintenance and fabrication work.

    The process demands respect for its hazards—especially the extreme noise levels and fire risks from spark throw. Proper safety equipment and procedures are non-negotiable. But with appropriate precautions, CAC delivers unmatched performance for gouging, weld removal, and metal cutting applications.

    Whether you are preparing joints for welding, removing defective welds, or repairing cast iron equipment, carbon arc cutting provides a solution that works on any metal, in any position, with equipment you may already own. Mastering CAC adds a powerful tool to your metalworking capabilities.

  • Oxygen Bottle Explained: Systems, Flow Rates, Care September 2026

    Oxygen Bottle Explained: Systems, Flow Rates, Care September 2026

    Struggling to breathe is one of the most frightening experiences anyone can face. When your lungs cannot provide enough oxygen on their own, medical oxygen becomes a lifeline that restores comfort and clarity.

    An oxygen bottle (also called an oxygen cylinder or tank) is a pressurized storage container that holds medical-grade oxygen gas or liquid oxygen. These cylinders deliver supplemental oxygen to patients who cannot get enough oxygen naturally due to respiratory conditions like COPD, asthma, pneumonia, or lung disease. The oxygen is stored under high pressure and delivered through a regulator that controls the flow rate prescribed by your doctor.

    Oxygen therapy has transformed from a hospital-only treatment to a practical home solution. Modern oxygen bottles come in various sizes, from portable units that fit in a shoulder bag to stationary tanks that provide weeks of continuous supply. Understanding your options helps you work with healthcare providers to choose the right system for your lifestyle and medical needs.

    What Is an Oxygen Bottle?

    An oxygen bottle is a medical device designed to store and deliver oxygen safely. These containers hold either compressed oxygen gas or liquid oxygen, both purified to medical grade standards exceeding 99% purity. The gas form is compressed to pressures between 2,000 and 2,200 PSI, while liquid oxygen is kept at temperatures below -297 degrees Fahrenheit.

    People use oxygen bottles when their blood oxygen levels fall below the normal range of 75-100 mmHg. This can happen due to chronic conditions like COPD, acute illnesses like pneumonia, or temporary situations like high-altitude travel. A doctor determines your oxygen needs through arterial blood gas tests or pulse oximeter readings measuring your oxygen saturation percentage.

    Quick Summary: Oxygen bottles store medical-grade oxygen for people whose lungs cannot extract enough from air. They come as compressed gas cylinders or liquid containers, with sizes ranging from portable units to large stationary tanks.

    Terminology can be confusing because these devices go by multiple names. Oxygen bottles, oxygen cylinders, oxygen tanks, and oxygen containers all refer to the same equipment. The term “bottle” is more common in everyday conversation, while medical professionals typically say “cylinder” or “tank.”

    Types of Oxygen Delivery Systems

    Not all oxygen systems work the same way. Understanding the differences helps you choose the right option based on your lifestyle, oxygen needs, and budget.

    Compressed Gas Oxygen Cylinders are the most traditional form. These metal tanks store oxygen gas under high pressure. They are reliable, require no electricity, and work anywhere. However, they are heavy and contain a limited supply that requires frequent refilling or replacement.

    Liquid Oxygen Systems keep oxygen in liquid form at extremely cold temperatures. Liquid takes up less space than gas, so these containers hold much more oxygen in a smaller package. As oxygen is released, it warms and converts to gas for breathing. The main advantage is longer duration between refills, but liquid oxygen evaporates over time even when not in use.

    Oxygen Concentrators are electronic devices that extract oxygen from room air. They filter out nitrogen and other gases, delivering concentrated oxygen (typically 85-95% pure). Concentrators never need refilling because they run continuously as long as they have power. Stationary home units are heavier but provide unlimited oxygen, while portable versions offer freedom with battery operation.

    TypeHow It WorksProsConsBest For
    Compressed GasStores oxygen under pressureReliable, no power neededHeavy, limited supplyBackup and travel
    Liquid OxygenSuper-cold liquid storageHigh capacity, smaller sizeEvaporates over timeActive users needing mobility
    Oxygen ConcentratorFilters oxygen from airUnlimited supply, no refillsRequires electricityHome-based therapy
    Portable ConcentratorBattery-powered filteringLightweight, FAA-approvedExpensive, limited batteryFrequent travelers

    Oxygen Cylinder Sizes Explained

    Oxygen cylinders come in standardized sizes designated by letters. Each size has different capacities and typical durations at various flow rates.

    M6 and M9 Cylinders are the smallest portable options, weighing under 5 pounds when full. An M6 cylinder holds about 164 liters of oxygen and lasts roughly 3 hours at 2 liters per minute (LPM). The slightly larger M9 holds 255 liters and lasts about 4.5 hours at the same flow rate. These are ideal for short trips or quick errands.

    E Cylinder is the most common portable size. It contains 680 liters of oxygen and weighs about 8 pounds when empty (13 pounds full). At 2 LPM, an E cylinder lasts approximately 5.5 hours. Many active oxygen users keep multiple E cylinders to manage daily activities without interruption.

    M and ME Cylinders are medium-sized tanks offering extended duration. The M cylinder holds 3,455 liters and can last over 28 hours at 2 LPM. The ME is slightly smaller but still provides substantial runtime. These work well for people who need oxygen throughout the day but want fewer refills.

    H Cylinder is the large stationary tank often used as a home reservoir. With 6,900 liters of capacity, an H cylinder can provide nearly 58 hours of oxygen at 2 LPM. These are too heavy to move (about 130 pounds when full) and stay in one location, often serving as the primary supply with smaller portable tanks for outings.

    SizeCapacity (Liters)Weight (Full)Duration at 1 LPMDuration at 2 LPM
    M6164 liters~4 lbs~6 hours~3 hours
    M9255 liters~5 lbs~9 hours~4.5 hours
    E680 liters~13 lbs~11 hours~5.5 hours
    M3,455 liters~30 lbs~57 hours~28 hours
    H6,900 liters~130 lbs~115 hours~57 hours

    Flow Rate (LPM): Liters per minute measures how much oxygen you receive. Your doctor prescribes a specific flow rate based on your blood oxygen levels. Higher flow rates deplete cylinders faster, while lower rates extend duration.

    Who Needs Oxygen Therapy?

    Supplemental oxygen is prescribed when your body cannot maintain adequate oxygen levels on its own. This happens for various reasons, and understanding your condition helps you manage your treatment effectively.

    Conditions Requiring Oxygen Therapy

    COPD (Chronic Obstructive Pulmonary Disease) is the most common reason for long-term oxygen therapy. This progressive lung disease includes emphysema and chronic bronchitis. Damaged lung tissue cannot exchange oxygen efficiently, causing blood oxygen levels to drop. Many COPD patients use oxygen 24 hours a day, while others need it only during sleep or physical activity.

    Pneumonia and Severe Infections can temporarily reduce lung function. When fluid fills the air sacs, oxygen transfer becomes difficult. Short-term oxygen therapy helps patients recover while antibiotics and other treatments fight the infection. Most people stop using oxygen once the infection clears.

    Asthma typically does not require continuous oxygen, but severe attacks can dangerously lower oxygen levels. Emergency oxygen bottles provide critical support during acute exacerbations until bronchodilators take effect. Some asthma patients keep portable oxygen as a safety measure.

    Sleep Apnea causes breathing interruptions during sleep. While CPAP machines are the primary treatment, some patients also need supplemental oxygen. Overnight oxygen use ensures blood oxygen stays in the safe range throughout the night, preventing strain on the heart and other organs.

    Cystic Fibrosis is a genetic condition that produces thick mucus in the lungs. As the disease progresses, oxygen absorption decreases. Many adults with cystic fibrosis eventually require oxygen therapy, often starting with nighttime use and progressing to continuous use as lung function declines.

    Pulmonary Fibrosis scars lung tissue, making it stiff and less efficient at oxygen transfer. This progressive condition often requires long-term oxygen therapy. Unlike COPD, pulmonary fibrosis typically worsens steadily, increasing oxygen needs over time.

    Heart Failure can cause fluid to accumulate in the lungs, reducing oxygen absorption. Some heart failure patients benefit from oxygen therapy, especially during sleep or physical activity when the heart works harder. The oxygen reduces strain on the cardiovascular system.

    Symptoms of Low Oxygen

    Recognizing low oxygen levels helps you seek appropriate treatment. Common signs include shortness of breath even at rest, rapid breathing, confusion or difficulty concentrating, bluish tint to lips or fingernails, morning headaches, and fatigue that interferes with daily activities.

    A pulse oximeter provides a quick oxygen saturation reading. Normal levels are 95-100%. Readings below 90% indicate hypoxemia (low blood oxygen) and warrant medical attention. Many people on oxygen therapy keep a pulse oximeter at home to monitor their levels throughout the day.

    Oxygen Safety Guidelines

    Oxygen itself is not flammable, but it accelerates combustion. Materials that normally burn slowly can ignite explosively in high-oxygen environments. Following safety protocols prevents accidents and protects everyone in your household.

    WARNING: Oxygen safety is non-negotiable. Ignoring these rules puts your life and property at serious risk. Never compromise on oxygen safety protocols.

    Fire Safety Rules

    1. No smoking, ever. This is the absolute most critical rule. Smoking while using oxygen can cause immediate, severe burns. Do not allow anyone to smoke in your home or car while oxygen is present. Post “No Smoking” signs at entrances.
    2. Stay away from open flames. Keep at least 10 feet from candles, fireplaces, gas stoves, and other ignition sources. Do not use oxygen near a lit barbecue grill or outdoor fire pit.
    3. Avoid spark-producing activities. Do not use electric razors, hair dryers, or spark-producing tools near your oxygen equipment. Static electricity from blankets or clothing can also create sparks.
    4. Use approved moisturizers only. Petroleum-based products like Vaseline are highly flammable with oxygen. Use only water-soluble moisturizers and lip balms.
    5. Install smoke detectors. Working smoke and carbon monoxide detectors provide early warning. Test them monthly and change batteries annually.
    6. Have a fire extinguisher nearby. Keep an ABC-rated fire extinguisher accessible. Know how to use it and ensure family members are trained as well.
    7. Create an emergency plan. Know how to evacuate quickly if a fire starts. Practice your escape route and keep oxygen equipment where you can grab it on the way out.

    Storage and Handling

    Store oxygen cylinders upright in a well-ventilated area, secured to prevent tipping. Never lay cylinders on their side. Keep them away from heat sources, direct sunlight, and temperatures above 125 degrees Fahrenheit. Do not store cylinders in confined spaces like closets or small cabinets.

    Secure cylinders properly to prevent falls. A falling cylinder can damage the valve, causing high-pressure oxygen to escape with enough force to penetrate walls. Use cylinder stands, chains, or specialized carts designed for oxygen storage.

    Check regularly for leaks using a soap solution on connections. Bubbles indicate a leak that needs immediate attention. Never use grease or oil on oxygen equipment fittings.

    Tripping Hazards

    Oxygen tubing creates tripping hazards, especially at night. Use tubing clips to secure the line along your baseboards or route it away from walking paths. Clear floor clutter and use nightlights to improve visibility. Some users find retractable reel systems helpful for managing excess tubing length.

    Getting Oxygen Therapy

    Obtaining medical oxygen requires a prescription and working with qualified suppliers. The process involves several steps from diagnosis to having equipment in your home.

    Prescription Requirements

    You cannot purchase medical-grade oxygen without a valid prescription. A doctor must evaluate your condition through pulmonary function tests, arterial blood gas measurements, or pulse oximetry. The prescription specifies your oxygen flow rate in liters per minute and when you need to use it (continuous, nighttime only, or as needed).

    The prescription also indicates which delivery system is appropriate for your situation. Some doctors start with a concentrator and portable tanks, while others prefer liquid oxygen systems for active patients. Always follow your prescribed flow rate exactly.

    Buying vs. Renting Equipment

    Most oxygen users rent equipment rather than buying outright. Monthly rental fees typically range from $150 to $400 for concentrators, with additional costs for portable cylinders and refills. Rental agreements usually include maintenance, repairs, and 24-hour emergency support.

    Purchasing makes sense for long-term users who want to avoid ongoing rental fees. Home concentrators cost $800 to $2,500, while portable concentrators range from $1,500 to $4,000. Remember that purchased equipment still requires periodic servicing and replacement parts.

    Insurance coverage significantly affects this decision. Medicare, Medicaid, and most private insurers cover oxygen therapy as durable medical equipment (DME). However, they typically rent rather than purchase equipment on your behalf.

    Insurance Coverage

    Medicare Part B covers oxygen equipment and supplies if you have specific medical conditions and meet coverage criteria. You pay 20% of the Medicare-approved amount after meeting your Part B deductible. Medicare rental payments continue for 36 months, after which you own the equipment.

    Private insurance coverage varies widely. Some plans require pre-authorization, while others have preferred supplier networks. Contact your insurance company before ordering equipment to understand your benefits, copays, and any documentation requirements.

    Keep detailed records of all medical necessity documentation. Insurers may periodically request proof of continued oxygen need, especially for long-term therapy.

    Finding Oxygen Suppliers

    Medical supply companies specializing in durable medical equipment are the primary source for home oxygen. Look for suppliers accredited by The Joint Commission or with similar certifications. Your doctor or hospital discharge planner can recommend reliable local companies.

    When choosing a supplier, consider their response time for emergencies, delivery area, hours of operation, and technical support quality. A good supplier provides thorough training on equipment use, offers 24/7 emergency support, and maintains reasonable delivery schedules for refills.

    Using Oxygen Equipment at Home

    Setting up and using oxygen equipment becomes routine quickly with proper training. Most suppliers provide in-home setup and instruction, but understanding the basics beforehand reduces anxiety.

    Oxygen Delivery Methods

    Nasal Cannula is the most common delivery method. This lightweight plastic tube splits into two prongs that fit into your nostrils, secured behind your ears with adjustable loops. Most people tolerate nasal cannulas well for extended periods. They are comfortable for eating and talking.

    Oxygen Mask delivers higher oxygen concentrations for people who need more than 4-6 LPM. Masks cover your nose and mouth, secured with an elastic strap. They can feel confining and make speaking difficult, but they provide more precise oxygen delivery.

    Oxygen Conserving Device is attached between the cylinder and cannula. It releases oxygen only when you inhale, extending cylinder life by 2-4 times. These devices are especially useful with portable tanks, allowing longer outings between refills.

    Setting Up Your Oxygen System

    1. Position your equipment. Place stationary concentrators or tanks in a well-ventilated area away from heat sources. Ensure the equipment sits level and has adequate clearance for airflow.
    2. Attach the regulator. For compressed gas cylinders, hand-tighten the regulator to the valve. Never use tools that could damage the threads. Open the valve slowly with the wrench provided.
    3. Set the flow rate. Turn the flow meter dial to your prescribed LPM setting. Watch the ball float in the tube and adjust until it rests at the correct number.
    4. Connect your cannula or mask. Attach the tubing to the outlet port. Run the tubing along your baseboards or secure it with clips to prevent tripping.
    5. Test the flow. Place your hand in front of the cannula prongs to feel the oxygen. Check that the flow meter reading matches your prescription.
    6. Wear your device. Insert the nasal prongs facing upward (curved side down) and adjust the ear loops for comfort. Position the tubing behind your head to keep it out of your face.

    Equipment Maintenance

    Clean or replace nasal cannulas weekly, or more often if you notice buildup. Wash cannulas in warm soapy water, rinse thoroughly, and air dry completely. Masks should be cleaned daily. Never share oxygen delivery equipment between people.

    Check cylinder pressure daily using the gauge. Order refills before tanks run completely empty. Keep at least one backup cylinder available for emergencies. For concentrators, clean or replace filters according to the manufacturer’s schedule.

    Test your backup power supply monthly if you use a concentrator. Power outages can be dangerous for oxygen-dependent patients, so have a plan and emergency backup tanks ready.

    Travel with Oxygen

    Traveling while on oxygen requires extra planning but is entirely possible with preparation. Many oxygen users lead active, mobile lives with the right equipment and knowledge.

    Air Travel with Oxygen

    The FAA allows specific portable oxygen concentrators on aircraft. Approved models carry FAA certification clearly marked on the device. You must notify the airline at least 48 hours before flying and provide a doctor’s statement specifying your oxygen needs.

    Compressed and liquid oxygen cylinders are generally prohibited on commercial flights. If you use these systems, you must arrange for oxygen delivery at your destination. Most airlines can help coordinate this service for a fee.

    Bring extra batteries for portable concentrators. FAA rules require sufficient battery power for 150% of your flight duration, including connections. Keep prescriptions and equipment documentation accessible for security screening.

    Car Travel

    Secure oxygen cylinders upright in the vehicle, never laying them down. Use a seat belt or proper cylinder restraints. Open windows slightly for ventilation, and never leave oxygen equipment in a hot car. Heat can cause dangerous pressure increases or damage to concentrators.

    Plan your route to identify refill stations along the way if you use cylinders. Map out medical supply companies that can provide refills in case of emergencies.

    Cruises and Trains

    Most cruise lines and Amtrak accommodate oxygen passengers with advance notice. Policies vary by company, so contact them directly before booking. Some cruise lines restrict the type of oxygen equipment allowed, while others require using their medical services.

    Frequently Asked Questions

    Do I need a prescription for medical oxygen?

    Yes, medical-grade oxygen requires a valid prescription from a licensed healthcare provider. Your doctor must evaluate your condition and determine your oxygen needs through testing. Over-the-counter oxygen canisters sold for recreational use are not equivalent to prescribed medical oxygen therapy.

    How long does an oxygen cylinder last?

    Duration depends on cylinder size and flow rate. A small M6 portable tank lasts about 3 hours at 2 liters per minute, while a large E cylinder provides approximately 5.5 hours at the same flow rate. Higher flow rates deplete cylinders faster, and conserving devices can extend duration by 2-4 times.

    What is the difference between an oxygen concentrator and an oxygen cylinder?

    Oxygen concentrators are electric devices that filter oxygen from room air, providing an unlimited supply as long as they have power. Oxygen cylinders store a finite amount of compressed or liquid oxygen that must be refilled or replaced. Concentrators are ideal for home use, while cylinders offer portability and backup during power outages.

    Is it safe to cook while using oxygen?

    Cooking with oxygen requires precautions. Electric stoves are safest for oxygen users. If you have a gas stove, turn off your oxygen while cooking and stay at least 10 feet away from open flames. Never wear oxygen while reaching over burners or candles. Consider using a microwave or preparing meals that require minimal cooking.

    How much does oxygen therapy cost per month?

    Monthly costs vary based on equipment type and insurance coverage. Without insurance, expect to pay $150-400 monthly for concentrator rental plus $20-75 per cylinder refill. Medicare and most private insurers cover oxygen therapy as durable medical equipment, though you may have copays and deductibles. Contact your insurer for specific coverage details.

    Can you travel with portable oxygen?

    Yes, travel with oxygen is possible with planning. FAA-approved portable oxygen concentrators can be used on airplanes with advance notice. For car travel, secure cylinders upright and never leave equipment in hot vehicles. Cruise lines and trains accommodate oxygen passengers with prior notification. Always carry a copy of your prescription and allow extra time for security screening.

    How do I check my oxygen levels at home?

    A pulse oximeter is a small device that clips to your fingertip and measures your blood oxygen saturation level. Normal readings are 95-100%. Readings below 90% indicate low oxygen requiring medical attention. Pulse oximeters are available at pharmacies and medical supply stores. Keep a log of your readings to share with your doctor.

    What are the side effects of oxygen therapy?

    Most side effects are minor and manageable. Dry or bloody nose is common and can be relieved with humidifiers or saline spray. Skin irritation from cannulas occurs occasionally and responds to repositioning or different equipment. Oxygen toxicity is rare at prescribed therapeutic doses. Contact your doctor if you experience headaches, confusion, or breathing changes while using oxygen.

    Conclusion

    Oxygen therapy has evolved dramatically in 2026, offering patients more freedom and options than ever before. From lightweight portable concentrators to efficient liquid systems, modern oxygen equipment enables people with respiratory conditions to maintain active, fulfilling lives.

    Understanding your oxygen options empowers you to make informed decisions with your healthcare team. The right system depends on your medical needs, lifestyle, and budget. Whether you choose compressed gas cylinders, liquid oxygen, or concentrator technology, following safety protocols ensures effective treatment without unnecessary risk.

    Remember that oxygen therapy is a medical treatment requiring professional oversight. Work closely with your doctor and oxygen supplier to optimize your setup. With proper equipment, knowledge, and support, supplemental oxygen becomes not a limitation but a tool for living well on your own terms.

  • Fix Arc Welding Problems Fast With Expert Tips 2026

    Fix Arc Welding Problems Fast With Expert Tips 2026

    You’re in the middle of a project, the weld looks terrible, and you have no idea why. I’ve been there – staring at a porous, spattered mess that needs to be ground out and redone. After 15 years of stick welding everything from fence posts to structural repairs, I’ve learned that most arc weld problems come down to five root causes: wrong amperage, damp electrodes, dirty metal, poor technique, or incorrect polarity.

    The fastest way to troubleshoot arc welding problems is to identify the defect type, then work through the likely causes systematically. Most weld issues can be fixed by adjusting one setting: amperage. But when that doesn’t work, you need a clear path forward.

    Over the past decade, I’ve welded through probably 200 pounds of 7018 alone, and I still encounter problems. The difference now is I can diagnose and fix them in minutes instead of hours. This guide covers every common arc welding defect, what causes it, and exactly how to fix it.

    What Are Common Arc Welding Problems?

    Understanding which problem you’re dealing with is the first step. Some defects are visible immediately, while others require closer inspection or destructive testing to discover.

    Quick Reference Troubleshooting Chart

    Problem-Cause-Solution Quick Reference

    Problem Most Likely Cause Quick Fix
    Porosity Damp electrode or dirty metal Dry electrodes, clean material
    Undercut Amperage too high or travel speed too fast Reduce amps, slow travel speed
    Excessive Spatter Arc length too long or amperage too high Shorten arc, reduce amperage
    Slag Inclusion Slag not cleaned between passes Wire brush thoroughly between welds
    Cracking Hydrogen from moisture or contamination Use dry electrodes, preheat if needed
    Lack of Fusion Amperage too low or travel too fast Increase amperage, slow down
    Electrode Sticking Amperage too low Increase amperage setting
    Arc Instability Wrong polarity or poor ground Check polarity, clean ground clamp

    Porosity – What Causes Those Holes in Your Weld?

    Quick Summary: Porosity appears as small holes or bubbles in the solidified weld metal. It’s caused by gas getting trapped in the weld pool as it cools, typically from moisture, contamination, or incorrect arc length.

    Porosity shows up as tiny pinholes or larger bubbles in your finished weld. Sometimes you’ll see it clearly on the surface. Other times, it’s hidden inside the weld and only revealed when you break the weld during testing.

    What Causes Porosity in Stick Welding?

    Moisture is the number one enemy here. I learned this the hard way after leaving a box of 7018 rods in my garage for three months. The humidity wicked right into the flux coating, and every weld I ran looked like Swiss cheese. Those electrodes had to be reconditioned in an oven at 500 degrees for two hours before they were usable again.

    Dirt, rust, paint, and oil on the base metal will also cause porosity. I’ve seen welders try to weld through mill scale and wonder why their welds look spongy. The contamination burns and creates gas that gets trapped in the weld pool.

    Too long of an arc length is another common culprit. When you hold the electrode too far from the work, the arc becomes unstable and draws atmospheric gases into the weld. Keep that rod close – about 1/8 inch from the work for most electrodes.

    How to Fix Porosity?

    Start with the basics: are your electrodes dry? Low hydrogen rods like E7018 must be kept in an oven or moisture-proof cabinet. If they’ve been exposed, they need to be baked before use. Cellulose-based rods like E6010 and E6011 are more forgiving but can still absorb moisture over time.

    Low Hydrogen Electrode: A welding rod with a flux coating designed to introduce minimal hydrogen into the weld, such as E7018. These require proper storage in dry conditions to prevent moisture absorption.

    Clean your base material down to bare metal. A wire wheel on an angle grinder is your best friend here. I spend more time preparing metal than I do actually welding – and that’s the way it should be.

    Shorten your arc. Most beginners hold the rod too far away. Get comfortable with that sweet spot where the rod is almost touching the work piece. You’ll hear the right sound – a steady, consistent crackle like bacon frying.

    Undercutting – When Your Weld Eats Into the Base Metal

    Undercut appears as a groove or notch eaten into the base metal right next to the weld bead. It’s a serious defect because it creates a stress concentration point that can lead to weld failure. Inspectors hate undercut, and for good reason.

    What Causes Undercut in Arc Welding?

    Excessive amperage is the most common cause. When you’re running too hot, the weld pool becomes too fluid and washes away the edges of the base metal. I see this constantly with welders trying to “get good penetration” by cranking up the machine.

    Travel angle is another factor. If you’re dragging the electrode at too steep an angle, you’re directing heat into the base metal ahead of the weld rather than building up the toe of the weld. A work angle of 45 degrees and a travel angle of 10-15 degrees works best for most positions.

    Travel speed that’s too fast will also cause undercut. You’re not leaving enough filler metal at the edges of the weld to fill in the groove you’re creating.

    How to Fix Undercutting?

    Reduce your amperage by 5-10 amps and try a test weld. Watch how the puddle behaves – you want it fluid but not so fluid that it washes away the base metal edges.

    Adjust your travel angle. Instead of dragging steeply, hold the electrode more perpendicular to the work. This directs the heat into the puddle rather than the base metal ahead of the weld.

    Slow down your travel speed. This allows more filler metal to deposit at the weld toes, filling in any potential undercut. You might also try a slight weaving technique – a gentle side-to-side motion that builds up the toes of the weld.

    Weld Spatter – Reducing Those Pesky Droplets

    Spatter consists of tiny metal droplets that scatter around your weld during the process. While not always a structural issue, spatter creates extra cleanup work and can indicate underlying problems with your technique or settings.

    Why Does My Weld Have So Much Spatter?

    Arc length is usually the culprit. When you hold the electrode too far from the work, the arc becomes unstable and molten metal gets thrown off in all directions. I’ve watched beginners hold their rod a half-inch off the plate and wonder why they’re wearing more weld than they’re laying down.

    Amperage that’s too high for your electrode size will also cause spatter. You’re essentially pumping too much current into a rod that can’t handle it smoothly.

    Damp electrodes can cause violent arc action and accompanying spatter. The moisture in the flux coating turns to steam and disrupts the arc stability.

    How to Reduce Weld Spatter?

    Focus on maintaining a consistent, short arc length. The electrode tip should always be close to the weld pool – about the same distance as the electrode’s diameter. For a 1/8 inch rod, keep about 1/8 inch gap.

    Match your amperage to your electrode size and position. As a general rule, vertical and overhead positions require 10-15% less amperage than flat position welding.

    Recommended Amperage Ranges by Electrode

    Electrode Diameter Amperage Range Best Use
    E6010 3/32 inch 40-70 amps Deep penetration, dirty metal
    E6010 1/8 inch 75-125 amps Pipe root passes, heavy plate
    E6011 3/32 inch 45-75 amps AC welding, farm repairs
    E6011 1/8 inch 80-140 amps AC welders, general purpose
    E6013 3/32 inch 50-80 amps Smooth beads, beginner-friendly
    E6013 1/8 inch 80-140 amps Sheet metal, fit-up work
    E7018 1/8 inch 90-140 amps Structural, low hydrogen
    E7018 5/32 inch 130-180 amps Heavy structural, high deposition
    E7024 1/8 inch 130-170 amps High deposition, flat position only

    Slag Inclusion – When Trapped Debris Weakens Your Weld

    Slag inclusions occur when the flux material gets trapped inside the weld metal instead of floating to the surface. These appear as dark lines or irregular shapes in cross-section and can significantly weaken the weld.

    What Causes Slag Inclusion?

    Not cleaning between weld passes is the primary cause. The slag from the previous pass needs to be completely removed before laying down the next bead. I use a chipping hammer to knock off the heavy stuff, then follow up with a wire brush for a thorough cleaning.

    Incorrect travel angle can also cause slag trapping. If your angle is too steep, the molten slag can’t flow out ahead of the weld pool and gets trapped.

    Too wide of a weave in multi-pass welds can leave slag pockets in the toes of the weld. Keep your weave width to about 2-3 times the electrode diameter.

    How to Prevent Slag Inclusions?

    Clean, clean, and clean again. Between every pass, chip and wire brush until you see clean metal. This is especially important in groove welds where you’re making multiple passes to fill the joint.

    Maintain proper travel and work angles. For fillet welds, keep the electrode at 45 degrees to each member. For groove welds, angle slightly toward the thicker member.

    Adjust your technique for vertical-up welding. The slag naturally flows ahead of the puddle when welding uphill, so you need to be deliberate about keeping the arc on the leading edge of the puddle and pausing slightly at the sides to let slag escape.

    Weld Cracking – Understanding and Preventing Fractures

    Cracks are the most serious weld defect because they can lead to catastrophic failure. Unlike porosity or undercut, cracks can propagate under stress and cause structural collapse.

    What Causes Cracks in Welds?

    Hydrogen cracking is the most common type in stick welding. It occurs when hydrogen from moisture or contamination gets trapped in the weld and creates internal pressure as the weld cools. This is why low hydrogen electrodes like E7018 must be kept dry.

    High restraint is another factor. When you’re welding thick materials or restrained joints, the weld metal contracts as it cools but can’t move – creating tremendous stress that can crack the weld.

    Improper filler metal selection can also cause cracking. Using a rod that’s too strong or too brittle for the base metal creates a mismatch in properties that leads to failure.

    How to Prevent Weld Cracking?

    Keep your electrodes dry. Low hydrogen rods should be stored in an oven at 225-300 degrees F. Once removed from the oven, use them within 4 hours for maximum reliability.

    Preheating: Heating the base metal before welding to slow the cooling rate of the weld, reducing the risk of hydrogen cracking and allowing hydrogen to escape from the weld metal.

    Preheat thick or restrained joints. For steel over 1 inch thick, preheat to 200-300 degrees F. This slows the cooling rate and gives hydrogen time to escape from the weld metal.

    Use the correct electrode for your application. E7018 is excellent for structural work but requires proper storage. E6010 is more forgiving for farm repairs and doesn’t require oven storage.

    Lack of Fusion – When Your Weld Doesn’t Bond

    Lack of fusion occurs when the weld metal doesn’t properly melt into the base metal or previous weld passes. The result looks like a complete weld, but there’s no actual bond at the interface.

    What Causes Lack of Fusion?

    Amperage too low means you’re not generating enough heat to properly melt the base metal. The electrode deposits metal, but it’s essentially sitting on top rather than fusing with the base.

    Travel speed that’s too fast prevents proper melting. You’re moving along before the heat has time to penetrate and fuse the materials.

    Incorrect work angle can prevent fusion at the weld toes. If you’re not directing the arc properly into the joint, you get what looks like a weld but isn’t actually bonded to the base metal.

    How to Fix Lack of Fusion?

    Increase your amperage. The weld pool should be fluid enough to wash into the base metal, not just sit on top. Watch for good wetting action at the toes of the weld.

    Slow down your travel speed. Give the heat time to penetrate and fuse. You want to see the puddle actively melting into the base metal as you move.

    Check your work angle. Direct the arc into the joint, not just at the surface. For fillet welds, split the angle evenly between both members.

    Incomplete Penetration – When Your Weld Doesn’t Go Deep Enough

    Incomplete penetration means the weld metal didn’t reach the full depth of the joint. Unlike lack of fusion (which is about side bonding), penetration is about how deep the weld goes through the thickness of the material.

    What Causes Incomplete Penetration?

    Amperage too low is the primary cause. You’re not generating enough heat to drive the arc through the full thickness of the material.

    Incorrect joint preparation can prevent penetration. If your root opening is too tight or your bevel angle is insufficient, the electrode can’t reach the bottom of the joint.

    Electrode diameter that’s too large for your joint won’t allow proper penetration into the root. A 1/8 inch rod can’t reach into a narrow root opening the way a 3/32 inch rod can.

    How to Fix Incomplete Penetration?

    Increase your amperage within the recommended range for your electrode size. More heat means deeper penetration.

    Ensure proper joint design. For full penetration butt welds, you typically need a bevel angle of 45-60 degrees with a proper root opening.

    Use the correct electrode diameter for your joint. Smaller rods penetrate better in narrow grooves. For root passes on V-grooves, 3/32 inch electrodes typically work better than 1/8 inch.

    Electrode Sticking – When Your Rod Won’t Let Go

    Every stick welder has experienced the frustration of the electrode welding itself to the work piece. It usually happens when you’re just getting started, and suddenly you’re stuck fast.

    Why Does My Welding Rod Keep Sticking?

    Amperage too low is the primary cause. You don’t have enough current to maintain the arc, so the electrode cools and fuses to the base metal. This is especially common when first striking an arc.

    Cold work lead connection can cause sticking issues. If your ground clamp isn’t making good contact, you won’t get the current you need to maintain the arc.

    A short-circuiting technique will also cause sticking. When you first touch the electrode to the work to strike the arc, if you don’t pull back quickly enough, the rod fuses to the base metal.

    How to Prevent Electrode Sticking?

    Use proper amperage for your electrode size and thickness. If you’re constantly sticking, turn up the machine by 5-10 amps and try again.

    Clean your ground clamp contact point. I always grind or wire brush where my clamp connects to ensure a solid electrical path.

    Improve your arc starting technique. Tap the electrode like a match – quick contact, then immediate lift to establish the arc. Don’t drag the rod along the surface trying to start.

    If the electrode does stick, don’t panic. Immediately twist the electrode back and forth in the holder to break it free. If it’s welded solid, you’ll need to disconnect the holder, grip the electrode with pliers, and twist while pulling.

    Equipment Troubleshooting – When Your Welder Is the Problem

    Sometimes the problem isn’t your technique – it’s your equipment. I once spent three hours fighting a weld that just wouldn’t run right, only to discover my work lead had a bad connection inside the cable.

    Welding Machine Not Getting Hot Enough

    If your machine isn’t producing the heat you need, check your input power first. A long extension cord or undersized wiring can cause voltage drop that limits output. I use a 10-gauge cord for any run over 25 feet.

    Check your work and electrode lead connections. Loose connections create resistance and heat, stealing power from your arc. Tighten all connections at the machine, holder, and ground clamp.

    Carbon buildup on your work clamp can create high resistance. Periodically clean the contact surfaces with a wire brush or file to ensure solid electrical contact.

    Arc Instability Problems

    An erratic, wandering arc is frustrating and produces poor welds. The most common cause is incorrect polarity. For most stick welding, you want DCEP (reverse polarity) where the electrode is positive. Check your machine settings and cable connections.

    DCEP (Direct Current Electrode Positive): Also called reverse polarity, the electrode connects to the positive terminal and the work piece to negative. This provides deeper penetration and is standard for most stick welding applications.

    Magnetic arc blow can cause the arc to wander in corners or on magnetic materials. This occurs when the magnetic field from your welding current interferes with the arc. Solutions include changing the work lead connection point, switching to AC if available, or using a shorter arc length.

    What Polarity Should I Use for Stick Welding?

    Most stick welding uses DCEP (reverse polarity) with the electrode on the positive terminal. This provides deeper penetration and smoother arc characteristics for electrodes like E6010, E6011, E7018, and E7024.

    DCEN (straight polarity) with the electrode negative is used for specific applications like open root pipe welding with certain cellulose electrodes. The shallower penetration helps prevent burn-through on thin root passes.

    AC welding works well with E6011 and E6013 electrodes and can help with magnetic arc blow issues. AC doesn’t penetrate as deeply as DCEP but can be more forgiving for beginners in some applications.

    Environmental Factors Affecting Weld Quality

    Your welding environment has a huge impact on weld quality. I’ve seen perfect technique produce terrible welds simply because the conditions weren’t right.

    Wind and Drafts

    Wind is the enemy of shielded metal arc welding. The flux coating creates a shielding gas cloud around your arc, and wind can blow it away. This leads to porosity and poor weld quality.

    For outdoor welding, set up windbreaks using tarps, welding blankets, or portable screens. I’ve welded in everything from light breezes to 30 mph winds, and the difference in quality is dramatic. Even a 5 mph breeze across your work area can cause problems.

    Humidity and Moisture

    High humidity affects both your electrodes and your base metal. Moisture in the air can be absorbed by electrode flux coatings, especially low hydrogen rods like E7018.

    In very humid conditions (over 60% relative humidity), keep electrodes in a portable rod oven and only take out what you can use in 30 minutes or less. Wipe down your base metal with a dry cloth if it’s covered in condensation.

    Temperature Extremes

    Cold weather welding requires special considerations. When temperatures drop below 50 degrees F, preheating becomes important. For critical welds in cold conditions, I always preheat at least 200 degrees to ensure proper fusion and prevent cracking.

    Extremely hot conditions can affect the welder itself. If you’re welding in direct sun on a 100-degree day, your machine may overheat and thermal cycle. Provide shade if possible or take breaks to let the machine cool.

    Prevention – Building Better Welds From the Start

    The best way to troubleshoot welding problems is to prevent them before they start. Good preparation and consistent technique eliminate 90% of weld defects.

    Material Preparation Matters

    I spend more time preparing metal than I do actually welding. A wire wheel on a grinder removes rust, scale, paint, and oil that would otherwise contaminate the weld. For critical welds, I follow up with acetone to remove any residual oil.

    Proper joint preparation is essential. V-grooves should have consistent bevel angles. Fit-up should be tight with consistent root openings. Poor fit-up never leads to good welds.

    Electrode Storage and Care

    Low hydrogen electrodes like E7018 must be kept dry. Store them in a moisture-proof cabinet or rod oven. Once opened, use them within the manufacturer’s recommended timeframe – typically 4-8 hours depending on humidity.

    Cellulose electrodes (E6010, E6011) are more forgiving but still benefit from dry storage. Keep them in their original containers with the lid tightly closed when not in use.

    Developing Consistent Technique

    Good welding technique comes from repetition. Practice on scrap material before tackling important projects. Set up your machine correctly, then focus on maintaining a steady arc length, consistent travel speed, and proper angles.

    Watch your weld pool. It tells you everything you need to know. A properly running weld puddle is fluid, smooth, and controls well. If the puddle is turbulent, hard to control, or not wetting into the base metal, something is wrong with your settings or technique.

    Frequently Asked Questions

    What causes porosity in stick welding?

    Porosity in stick welding is primarily caused by moisture in the electrode flux coating, dirty or contaminated base metal, or excessive arc length. Damp electrodes release water vapor into the weld pool, creating gas bubbles that become trapped as the metal solidifies. Clean your base metal to bare steel, keep electrodes dry, and maintain a short arc length to prevent porosity.

    How do you fix undercut in welding?

    Fix undercut by reducing your amperage 5-10 amps, slowing your travel speed, and adjusting your electrode angle to a more perpendicular position. Undercut occurs when the weld pool is too fluid and washes away the base metal edges. A shorter arc length and slight weave technique can help build up the weld toes and eliminate undercut grooves.

    What polarity should I use for stick welding?

    Most stick welding uses DCEP (reverse polarity) with the electrode connected to the positive terminal. This provides deeper penetration and smoother arc characteristics for common electrodes like E6010, E6011, E7018, and E7024. DCEN (straight polarity) is used for specific applications like open root pipe welding, while AC works well with E6011 and E6013 electrodes and can help with magnetic arc blow issues.

    Why does my welding rod keep sticking?

    Electrode sticking occurs when your amperage is too low to maintain the arc, causing the rod to fuse to the base metal. It also happens with poor ground connections or improper arc starting technique. Increase amperage by 5-10 amps, ensure your ground clamp has solid metal-to-metal contact, and use a quick tapping motion like striking a match when initiating the arc.

    What causes weld spatter?

    Weld spatter is caused by arc length that is too long, amperage that is too high for your electrode size, or damp electrodes. Excessive arc length creates instability that throws molten metal droplets. Reduce your amperage, shorten your arc to approximately the electrode diameter, and ensure electrodes are properly stored and dry to minimize spatter.

    How do I prevent slag inclusions?

    Prevent slag inclusions by thoroughly cleaning between weld passes using a chipping hammer and wire brush. Maintain proper electrode angle – not too steep – which allows slag to flow out ahead of the weld pool. Limit your weave width to 2-3 times the electrode diameter and be extra careful in vertical-up welding where slag naturally flows ahead of the puddle.

    What causes cracks in welds?

    Weld cracks are primarily caused by hydrogen from moisture contamination, high restraint in the joint, or improper filler metal selection. Hydrogen cracking occurs when water in the electrode or base metal breaks down and hydrogen gets trapped in the cooling weld. Use dry low-hydrogen electrodes, preheat thick or restrained joints, and match your filler metal strength to the base metal to prevent cracking.

    How to fix lack of fusion in welding?

    Fix lack of fusion by increasing amperage to ensure proper melting of base metal, slowing travel speed to allow time for fusion, and correcting work angle to direct arc properly into the joint. Signs of lack of fusion include incomplete wetting at weld toes and lack of penetration into previous passes. The weld pool should be fluid enough to wash into and fuse with the base metal.

    Why is my arc unstable?

    Arc instability is typically caused by incorrect polarity settings, poor ground connections, or using the wrong electrode type for your machine. Check that your welding leads are connected properly for DCEP polarity on most stick electrodes. Clean your ground clamp contact point to bare metal and ensure tight connections. Magnetic arc blow can also cause wandering arcs when welding in corners or on thick steel sections.

    What causes arc blow in stick welding?

    Arc blow occurs when the magnetic field generated by welding current interferes with the arc, causing it to wander or deflect. This is most common when welding near the edge of plates, in corners, or at the end of joints. Solutions include moving your ground clamp closer to the weld area, switching to AC polarity if available, using shorter arc lengths, or changing weld direction toward the completed weld.

    Remember that troubleshooting is a systematic process. Identify the defect, consider the likely causes, and make one change at a time. With practice, you’ll develop an instinct for diagnosing problems quickly and getting back to producing quality welds.

  • Solder Aluminum Successfully: Step-by-Step Method 2026

    Solder Aluminum Successfully: Step-by-Step Method 2026

    After watching countless DIYers struggle with aluminum soldering, I understand the frustration. You clean the metal, heat it up, apply the solder, and it just balls up and rolls off. The first time I attempted to solder aluminum, I made every mistake in the book. Three failed attempts and $40 in wasted materials later, I finally figured out what I was doing wrong.

    Can you solder aluminum? Yes, aluminum can be soldered using specialized flux and zinc-based solder, though it’s more challenging than soldering copper due to its oxide layer. The key is using the right materials and proper surface preparation.

    Aluminum soldering is harder than working with copper or steel. Much harder. But with the right approach, anyone can achieve reliable joints. I’ve repaired radiator tanks, fixed HVAC lines, and even soldered aluminum electrical connections using these techniques. The process isn’t complicated once you understand why aluminum resists solder in the first place.

    Is Aluminum Difficult to Solder?

    Aluminum presents three main challenges that make soldering difficult. First, the oxide layer forms within seconds of exposure to air. Second, aluminum conducts heat away from your work area extremely quickly. Third, not all aluminum alloys accept solder equally well.

    I’ve learned that the oxide layer is the real enemy here. It’s invisible, forms instantly, and has a melting point over 3700°F. Meanwhile, aluminum melts around 1220°F. The oxide essentially creates a barrier that solder cannot penetrate.

    Thermal conductivity compounds the problem. When I first tried soldering an aluminum bracket, I couldn’t understand why the solder wouldn’t flow even after heating for what seemed like forever. The metal was conducting heat away from my work area faster than I could supply it.

    Aluminum Oxide Layer: A thin, invisible layer of aluminum oxide (Al2O3) that forms instantly when bare aluminum is exposed to air. This oxide layer has a melting point of 3722°F (2050°C), while aluminum itself melts at just 1220°F (660°C).

    Alloy variations add another layer of complexity. In my experience working with scrap aluminum, I’ve discovered that some pieces solder beautifully while others refuse to accept solder no matter what I try. This isn’t random—certain aluminum alloys are simply more solderable than others.

    Safety Precautions for Aluminum Soldering

    Before diving into techniques, I need to address safety first. Aluminum soldering produces hazardous fumes and involves open flames. After years of metalwork, I’ve seen too many people skip proper protection and pay the price.

    Ventilation and Flux Fumes

    Ammonia-based fluxes produce fumes when heated that can irritate eyes, nose, and lungs. These aren’t just unpleasant—they can cause real harm with prolonged exposure. I always work in a well-ventilated area or use a fume extractor when soldering indoors.

    The fumes from aluminum flux contain ammonia compounds and potentially chlorine depending on the formulation. In 2026, we know much more about the long-term effects of inhaling these fumes than we did even a decade ago. Chronic exposure can cause respiratory sensitization.

    For indoor work, I set up a box fan to pull fumes away from my breathing zone, positioned to draw air across the work area and toward an open window. For frequent soldering, a proper fume extractor with activated carbon filtration is worth the investment.

    Eye and Skin Protection

    Safety glasses are non-negotiable. Molten solder can spit, and flux can splatter. I’ve had small solder beads land on my skin—minor burns but uncomfortable. Glasses protect your eyes from these random splatters.

    Flux can be irritating to skin. Some formulations cause dermatitis with prolonged exposure. I wear nitrile gloves when working with flux, especially the more aggressive aluminum formulations. The chemicals in these fluxes aren’t something you want absorbed through your skin repeatedly.

    Fire Safety

    Open flames and hot materials present fire risks. Keep a fire extinguisher nearby. I clear my work area of flammable materials before starting. This is especially important when working with automotive components that may have residual oil or fuel.

    Tools and Materials You Need

    Getting started with aluminum soldering requires specific tools and materials. Regular electronics solder and flux won’t work. After years of trial and error, I’ve narrowed down to the essential items that actually deliver results.

    Quick Summary: You need zinc-based solder or aluminum brazing rods, ammonia-based flux specifically for aluminum, a propane or MAPP gas torch, and abrasive cleaning tools. A high-wattage soldering iron (60W+) works for small electronics jobs.

    Heat Sources

    The heat source you choose depends on your application. For most general aluminum soldering, I recommend a propane torch. It provides adequate heat for most repairs and is widely available. When I need more heat control, I switch to MAPP gas which burns hotter.

    Heat Source Temperature Best For Limitations
    Propane Torch Up to 2900°F General repairs, sheet metal Slow heat on thick pieces
    MAPP Gas Torch Up to 3650°F Thicker aluminum, faster work Higher fuel cost
    Soldering Iron (60W+) Up to 900°F tip Small electronics, wire connections Limited to small workpieces
    Oven/Hot Plate Controlled 500-700°F Multiple small parts evenly Requires flux pre-application

    For electronics work, I use a 60-watt soldering iron at minimum. Standard 30-40 watt irons simply can’t deliver enough heat to overcome aluminum’s thermal conductivity. The trick is using high-wattage iron with good thermal mass.

    Solder and Brazing Rods

    Regular tin-lead or tin-copper solder won’t work on aluminum. You need zinc-based formulations designed specifically for aluminum. My go-to options include specialty aluminum brazing rods like Harris Al-Solder 500 or similar products from reputable manufacturers.

    These rods typically melt around 700-750°F, well below aluminum’s melting point. The zinc content allows the solder to wet properly when used with the correct flux. I’ve found that rod diameter matters too—thinner rods (1/16″) work better for thinner materials.

    Flux Selection

    Flux is the secret weapon in aluminum soldering. Without it, nothing else matters. The flux must chemically break down the aluminum oxide layer and prevent re-oxidation during heating.

    Ammonia-based fluxes are the most effective for aluminum. Brands like Superior Flux manufacture formulations specifically for this application. When I first started, I tried using regular rosin flux and wondered why nothing worked.

    Flux Type Effectiveness Clean-up Best Use Case
    Ammonia-based Aluminum Flux Excellent Water soluble General aluminum soldering
    Organic Acid Flux Good Water soluble Lower temperature applications
    Rosin Flux Poor Alcohol clean Won’t work on aluminum
    Petroleum Jelly/Mineral Oil Fair Solvent clean Electronics (emergency method)

    Cleaning Tools

    Proper cleaning is non-negotiable. I keep stainless steel wire brushes specifically for aluminum—never use a brush that’s touched other metals or you’ll contaminate the surface. Abrasive pads, sandpaper (80-120 grit), and specialized aluminum cleaning compounds round out my cleaning arsenal.

    Solvents like acetone or isopropyl alcohol are essential for removing oils and grease. I learned this the hard way after a solder joint failed because I didn’t degrease the surface first. Even clean-looking aluminum can have invisible oil contamination from handling.

    Surface Preparation: The Critical Step

    Surface preparation makes or breaks aluminum soldering success. I can’t emphasize this enough—poor preparation equals failed joints every time. The oxide layer must be completely removed, and the surface must be free of any contamination.

    Mechanical Cleaning

    Start by mechanically removing the oxide layer. Use a stainless steel wire brush dedicated to aluminum and scrub the joint area thoroughly. The goal is to expose fresh, clean aluminum metal. I brush in multiple directions to ensure complete coverage.

    For heavy oxidation or anodized aluminum, abrasive action is necessary. Sandpaper, abrasive pads, or even a wire wheel on a rotary tool can be used. When dealing with anodized parts, you must completely remove the anodized layer from the soldering area.

    Chemical Cleaning

    After mechanical abrasion, clean the area with solvent to remove oils and grease. Acetone works well, but isopropyl alcohol is safer and adequate for most applications. Wipe the area with a clean cloth or paper towel.

    Timing is crucial here. Once cleaned, aluminum begins re-oxidizing immediately. I’ve found I have about 30-60 seconds before the oxide layer becomes problematic again. Work quickly and apply flux immediately after cleaning.

    How to Solder Aluminum: Step-by-Step Guide?

    This is the most reliable method for general aluminum soldering. I’ve used it successfully on automotive repairs, HVAC work, and general fabrication. Follow these steps carefully for best results.

    Quick Summary: Clean the aluminum thoroughly, apply flux generously, heat evenly until the flux activates, then touch the solder rod to the heated area (not the flame). The solder should flow into the joint when the temperature is right.

    Step 1: Prepare the Joint

    Clean both surfaces to be joined using the mechanical and chemical cleaning methods described above. If joining two pieces, ensure good contact between them. A tight joint with minimal gap allows solder to flow more easily than wide gaps.

    Step 2: Apply Flux

    Apply a generous coating of aluminum-specific flux to both surfaces. Don’t be shy with the flux—better too much than too little. I apply it with a brush or directly from the container, depending on the flux type.

    Work quickly after applying flux. The clock is ticking as the cleaned surface begins to re-oxidize. I prepare everything else before applying flux so I can move immediately to heating.

    Step 3: Position the Parts

    Position the aluminum pieces exactly where you want them. If possible, clamp or secure them so they won’t move during heating. I’ve had to start over more than once because parts shifted at a critical moment.

    Step 4: Apply Heat

    Begin heating the joint area with your torch. Move the flame in a circular motion to distribute heat evenly. Don’t focus the flame in one spot too long or you risk overheating and warping the aluminum.

    Watch for the flux to activate. It will bubble, change color, and become clear. This indicates the temperature is rising and the flux is doing its job of breaking down the oxide layer. Most aluminum fluxes activate around 350-400°F.

    Step 5: Apply Solder

    Once the flux is active and the metal is heated through, touch the solder rod to the joint area—not to the flame. The heat from the aluminum should melt the solder. If the solder doesn’t melt, continue heating but be careful not to overheat.

    When the temperature is right, the solder will flow into the joint by capillary action. Continue feeding solder until the joint is filled. Then remove the heat and let the joint cool naturally. Don’t quench it with water or you’ll weaken the bond.

    Step 6: Clean the Joint

    After cooling, clean the flux residue. Most aluminum fluxes are water-soluble and can be removed with warm water. Leftover flux can cause corrosion over time, so thorough cleaning is important.

    Soldering Aluminum with a Soldering Iron

    For smaller work like electronics, wire connections, or thin sheet metal, a soldering iron can work if you follow special techniques. This method has limitations but is useful for specific applications.

    You need a high-wattage iron—60 watts minimum. I use an 80-watt iron for aluminum work. The higher wattage ensures the iron can maintain temperature despite aluminum’s high thermal conductivity.

    The technique differs from torch soldering. I apply flux first, then use the iron to heat the work area while occasionally touching the solder to see if it flows. Patience is key here. This method takes longer and works best on small, thin pieces.

    For electronics applications, some hobbyists use petroleum jelly or mineral oil as makeshift flux. This is an emergency technique and not as reliable as proper aluminum flux, but it can work in a pinch for low-stress connections.

    Aluminum Alloy Solderability Guide

    Not all aluminum solders equally well. The alloy composition dramatically affects solderability. After encountering mysterious failures, I learned to identify common aluminum types and adjust my expectations accordingly.

    Alloy Series Solderability Common Uses Notes
    1xxx Series Excellent Sheet, wire, chemical equipment Nearly pure aluminum (99%+)
    3xxx Series Excellent Cookware, heat exchangers Manganese alloy, very workable
    5xxx Series Good Marine, automotive, structural Magnesium alloy, still solderable
    6xxx Series Good to Fair Structural extrusions, architectural Magnesium-silicon alloy
    7xxx Series Poor Aircraft, high-strength applications Zinc alloy, very difficult to solder
    Cast Aluminum Variable Engine parts, housings Porosity can cause issues

    Identifying unknown aluminum can be tricky. I’ve found that soft, easily bent sheet metal is often 1xxx or 3xxx series—great for soldering. Harder structural aluminum is likely 6xxx series—still workable but more challenging. If you’re dealing with scrap or unknown material, test solder on a small area first.

    Troubleshooting Common Problems

    Even with proper technique, things can go wrong. I’ve encountered every problem listed below and learned how to fix each one. Use this troubleshooting guide to identify and resolve issues.

    Problem Likely Cause Solution
    Solder balls up and won’t stick Oxide layer present, insufficient flux Clean more thoroughly, apply fresh flux
    Joint is weak or breaks easily Cold solder joint, insufficient heat Apply more heat, ensure solder flows fully
    Aluminum melts before solder flows Heat concentrated in one spot too long Move heat source, heat larger area evenly
    Solder flows on one side only Uneven heating, dirty surface on one side Heat more evenly, reclean problem area
    Flux turns black and crusty Overheating, flux burned Reduce heat, apply fresh flux and restart
    Nothing works, solder refuses to bond Wrong alloy (7xxx or heavily anodized) Accept limitation, consider alternative joining method

    Weak Joints

    Weak joints usually result from insufficient heat or poor surface preparation. The solder may appear to have bonded, but it’s only superficially attached. I’ve tested joints that looked good but separated with minimal pressure.

    The fix is ensuring the solder fully wets the aluminum surface before cooling. The joint should have a smooth, feathered appearance where the solder meets the metal—not a abrupt boundary.

    Overheating Issues

    Aluminum can warp or even melt if overheated. Watch for the metal to become shiny or develop a wet appearance—this indicates it’s approaching its melting point. Back off the heat immediately if you see these signs.

    Aluminum Soldering vs Other Joining Methods

    Sometimes soldering isn’t the best choice. After years of aluminum work, I’ve learned to recognize when another joining method will give better results. Each method has its place depending on the application.

    Brazing vs Soldering

    Brazing uses higher temperatures and different filler metals than soldering. The distinction can be blurry—many “aluminum soldering” rods are technically brazing rods. Brazing typically creates stronger joints than soldering but requires more heat.

    Welding

    TIG and MIG welding provide the strongest aluminum joints. Welding melts the base metal, creating a fusion bond. This requires expensive equipment and significant skill, but for structural applications, welding is often the superior choice.

    Mechanical Fastening

    Rivets, bolts, and screws join aluminum without heat. This method avoids thermal distortion and alloy compatibility issues. For many applications, mechanical fastening is simpler and more reliable than attempting to solder difficult alloys.

    Adhesives

    Specialty adhesives like epoxy formulated for aluminum can create strong bonds. Modern structural adhesives are surprisingly capable. I’ve used them for applications where heat would cause problems or where appearance matters.

    Method Strength Equipment Cost Skill Required
    Soldering Low to Medium Low Moderate
    Brazing Medium Low Moderate
    TIG Welding High High High
    Mechanical Fasteners High Low Low
    Structural Adhesive Medium to High Low Low

    Frequently Asked Questions

    What kind of solder will stick to aluminum?

    Zinc-based solder specifically formulated for aluminum will stick to the metal when used with proper flux. Regular tin-lead or tin-copper electronics solder will not work. Specialty aluminum brazing rods containing zinc, along with ammonia-based flux, are required for a successful bond.

    Is aluminum difficult to solder?

    Yes, aluminum is more difficult to solder than copper or steel due to its oxide layer that forms instantly when exposed to air. This oxide has a much higher melting point than aluminum itself and prevents solder from wetting the surface. Specialized flux and proper surface preparation are essential to overcome this challenge.

    Can you solder aluminum with a soldering iron?

    Yes, but with limitations. You need a high-wattage iron (60W minimum, preferably 80W+) to overcome aluminum’s thermal conductivity. This method works best for small electronics work, wire connections, or thin sheet metal. A propane torch is more effective for larger pieces and general repairs.

    What is the best flux for aluminum soldering?

    Ammonia-based flux specifically designed for aluminum is the most effective option. Brands like Superior Flux manufacture formulations that chemically break down the aluminum oxide layer. These fluxes are typically water-soluble for easy cleanup. Regular rosin or organic acid fluxes for electronics will not work on aluminum.

    What temperature is needed to solder aluminum?

    Most aluminum soldering requires heating the metal to 700-750degF for the solder to flow properly. The flux typically activates at a lower temperature around 350-400degF. It’s important not to exceed aluminum’s melting point of approximately 1220degF, or you risk damaging the workpiece.

    Why won’t solder stick to aluminum?

    Solder won’t stick to aluminum because of the oxide layer that forms instantly on the surface. This invisible layer has a melting point over 3700degF, far above solder’s melting temperature. The solder cannot wet or bond to oxidized aluminum. Proper flux is required to chemically break down this oxide layer and allow solder contact with clean metal.

    How do you prepare aluminum for soldering?

    Clean the aluminum thoroughly using a stainless steel wire brush to mechanically remove the oxide layer. Then degrease with acetone or isopropyl alcohol to remove oils. Apply aluminum-specific flux immediately after cleaning, as re-oxidation begins within seconds. Work quickly from cleaning to heating to achieve the best results.

    How to join two pieces of aluminum?

    You can join aluminum pieces through several methods: soldering for low-stress joints using zinc-based solder and special flux, brazing for stronger medium-temperature bonds, TIG or MIG welding for the strongest structural joints, mechanical fasteners like rivets or bolts, or structural adhesives for applications where heat would cause problems.

  • Aluminum Welding: The Complete Guide for Beginners and Pros

    Aluminum Welding: The Complete Guide for Beginners and Pros

    Aluminum welding opens up incredible possibilities for lightweight, corrosion-resistant fabrication. I’ve spent the past 15 years welding everything from steel structural beams to delicate aluminum sheet, and here’s what I’ll tell you upfront: aluminum behaves differently than steel. The first time I tried to weld aluminum with my steel MIG setup, I created a bird’s nest of tangled wire and a porous mess. But once you understand how aluminum handles heat and how to properly prepare it, aluminum welding becomes manageable and even enjoyable.

    In this guide, I’ll walk you through everything you need to know to successfully weld aluminum, based on real experience working with automotive body panels, boat repairs, and custom fabrication projects. These industrial welding applications show how aluminum welding is used in manufacturing everything from heavy equipment to precision components.

    Why Aluminum Welding is Different from Steel?

    Understanding why aluminum behaves differently than steel will save you frustration. After ruining $200 worth of aluminum sheet on my first attempts, I learned these differences the hard way.

    Thermal Conductivity: Aluminum conducts heat 3-5 times faster than steel. This means heat spreads rapidly away from your weld zone, requiring higher amperage and faster travel speeds. The heat doesn’t stay concentrated like it does with steel.

    The second major difference is the oxide layer. Aluminum naturally forms a thin oxide coating when exposed to air. This oxide melts at approximately 3,700°F, while the aluminum underneath melts at only 1,200°F. If you don’t remove this oxide layer, you’ll be trying to weld through a crust that won’t melt until your base metal has turned into a puddle.

    Aluminum also has a much lower melting point than steel (1,220°F vs 2,500°F for mild steel). Combined with high thermal conductivity, this creates a narrow window between “not enough heat” and “burned through completely.” I’ve watched aluminum go from solid to dripping through the backside in seconds.

    Quick Summary: Aluminum conducts heat rapidly, forms a high-melting oxide layer, and has a low melting point. These three factors make aluminum welding unforgiving of improper technique but rewarding once mastered.

    Preparation and Cleaning: The Critical First Step

    I can’t stress this enough: 80% of aluminum welding success happens before you ever strike an arc. In my experience, poor preparation causes more aluminum weld failures than all other factors combined. After working with hundreds of students and fabricators, I’ve seen that skipping cleaning steps always results in porosity, lack of fusion, or both.

    Step-by-Step Aluminum Cleaning Checklist

    1. Degrease the surface: Wipe both sides of the joint with acetone, alcohol, or a dedicated aluminum cleaner. This removes oils, lubricants, and handling contaminants. I use acetone on a clean rag and wipe until the rag comes away clean. Don’t skip this step—even clean-looking aluminum has invisible oils from manufacturing and handling.
    2. Remove the oxide layer: Use a stainless steel brush dedicated only to aluminum (never use a brush that’s touched steel or you’ll embed iron particles). Brush firmly in one direction only, not back and forth. The one-direction brushing helps sweep oxide away rather than redistributing it. Brush until you see shiny, clean aluminum exposed.
    3. Brush inside the joint: If you’re welding a butt joint or tee joint, make sure to brush the surfaces that will be in contact. The oxide layer inside the joint will cause lack of fusion if left untouched. I’ve seen countless beautiful-looking welds that had zero penetration because the joint surfaces weren’t properly cleaned.
    4. Final solvent wipe: After brushing, do a final quick wipe with clean solvent to remove any oxide particles or debris from brushing. This step takes 30 seconds and prevents contamination in your weld pool.
    5. Weld immediately: The oxide layer begins reforming immediately after cleaning. For critical welds, clean and weld within 30 minutes. For general fabrication, try to weld within a few hours. If more than 4 hours have passed, re-clean the surface.
    6. Joint fit-up: Aluminum expands significantly when heated. A tight fit-up before welding becomes a gap as the metal heats. I prefer a slight root gap (about the thickness of a dime) for butt joints to account for thermal expansion. Use clamps liberally—aluminum moves more than steel when heated.
    Automotive Body Work
    Marine Repair
    DIY Fabrication

    MIG Welding Aluminum: Process and Techniques

    MIG welding aluminum is the faster option and works well for material thicknesses from 1/8 inch up to 1/2 inch or more. It’s the go-to process for production work, thicker aluminum, and situations where speed matters more than appearance. I use MIG for boat trailer repairs, aluminum toolboxes, and structural fabrications where TIG would take too long.

    Do You Need Special Equipment for MIG Aluminum?

    Yes, standard steel MIG welding equipment won’t work well for aluminum. Here’s what you need:

    Spool Gun: A specialized MIG gun that holds a small spool of wire (typically 4 inch or 1 pound) right at the gun. This eliminates the long cable feed path that causes aluminum wire to birdnest due to its softness. Spool guns are essential for MIG welding aluminum with most standard welders.

    The challenge with MIG welding aluminum is wire feeding. Aluminum wire is soft and has low column strength. When you try to push it through a 10-15 foot MIG gun cable, it tends to tangle, creating what’s called a “birdnest” at the drive rolls. This is why a spool gun or push-pull system is mandatory for most applications.

    You’ll also need 100% argon shielding gas. Never use the C25 mixed gas (75% argon, 25% CO2) that you use for steel. CO2 reacts with aluminum and creates poor welds. Pure argon provides proper shielding and arc characteristics for aluminum MIG welding.

    Aluminum MIG Welding Settings

    Material Thickness Wire Size Voltage Wire Speed (IPM) Gas Flow (CFH)
    1/16 inch (1.6mm) 0.030″ 16-18V 220-280 20-25
    1/8 inch (3.2mm) 0.035″ 18-21V 280-340 20-25
    3/16 inch (4.8mm) 0.035″ 21-24V 340-400 25-30
    1/4 inch (6.4mm) 0.045″ 23-26V 350-420 25-30

    IPM: Inches Per Minute – the speed at which the wire feeds from the MIG gun. Higher IPM means more wire (and thus more filler metal) is being deposited into the weld.

    MIG Aluminum Technique: The Push Method

    Unlike steel MIG welding where you can push or pull the gun, aluminum MIG welding requires the push technique. Angle the gun 10-15 degrees forward (pushing direction) so the gas flow is ahead of the arc. This helps the shielding gas cover the weld pool before contamination can occur and provides better cleaning action.

    I recommend a spray transfer mode for most aluminum MIG applications. This means using voltage and wire speed high enough that the wire transfers across the arc as fine droplets rather than short-circuiting. Spray transfer produces a smooth, clean weld with less spatter and better penetration. You’ll recognize spray transfer by the characteristic hissing sound and lack of crackling.

    Travel speed should be faster than you’d use for steel. Aluminum’s high thermal conductivity means the heat dissipates quickly, so you need to keep moving. If you move too slowly, you’ll experience burn-through, especially on thinner materials. I often run travel speeds 30-50% faster for aluminum compared to similar thickness steel.

    TIG Welding Aluminum: Process and Techniques

    TIG welding aluminum produces the cleanest, most precise welds and is the preferred method for thin materials, critical joints, and applications where weld appearance matters. I use TIG for aluminum automotive body work, thin sheet fabrication, and any weld that will be visible on the finished product. The control TIG offers is unmatched, but it requires more skill and practice than MIG.

    AC TIG: The Secret to Aluminum

    TIG welding aluminum requires alternating current (AC), unlike steel TIG which uses DC. The alternating current performs two crucial functions: during the electrode positive (EP) half-cycle, the arc blasts away the aluminum oxide layer; during the electrode negative (EN) half-cycle, heat focuses into the workpiece and melts the base metal. This cleaning and penetration balance is what makes AC TIG work for aluminum.

    AC Balance: The ratio of time spent in the cleaning (EP) phase versus the penetration (EN) phase during AC TIG welding. A balance of 70% EN / 30% EP is typical for most applications. More cleaning action helps with dirty material but reduces penetration and increases heat input.

    Modern inverter TIG welders offer adjustable AC balance and frequency settings. For general aluminum welding, I start with 70% EN (penetration) / 30% EP (cleaning) and adjust from there. If you’re welding material with heavy oxidation or contamination, increase the cleaning side. If you need maximum penetration or are welding thicker material, shift toward more penetration.

    Aluminum TIG Filler Metal Selection

    Filler Type Best For Characteristics
    ER4043 General fabrication, 6XXX series aluminum Easier to use, crack-resistant, lower melting point, silvery appearance after welding
    ER5356 5XXX and 6XXX series, structural applications Higher strength, better ductility, slightly harder to feed, requires higher amperage
    ER4047 Cast aluminum, high-silicon alloys 12% silicon content, excellent for casting repair, low melting point
    ER5556 High-strength applications, 5XXX series Maximum strength, specialty structural use

    For most general aluminum fabrication, ER4043 filler is the go-to choice. It flows nicely, is more forgiving of less-than-perfect cleaning, and produces a clean-looking weld. I keep 4043 rods in 1/16 inch and 3/32 inch diameters for different material thicknesses. Use 1/16 inch for material up to 3/16 inch thick, and step up to 3/32 inch for thicker material.

    TIG Aluminum Technique Tips

    Establishing and maintaining an arc on aluminum takes practice. The high thermal conductivity means the heat wants to dissipate quickly. I recommend starting on a scrap piece of the same thickness to establish your amperage setting. The ideal amperage will create a small, shiny puddle that forms within 1-2 seconds of establishing the arc.

    Add filler rod by dipping it into the leading edge of the puddle, not the center. This ensures proper mixing and prevents the rod from sticking or balling up. I hold the rod at about a 45-degree angle to the workpiece and feed it rhythmically as I move the torch forward.

    Foot pedal control is your friend for aluminum TIG. The ability to vary heat on the fly helps manage the narrow temperature window. I’ll often start slightly hotter to establish the puddle, then back off the pedal as I progress. For aluminum TIG, I generally run 10-20% higher amperage than I would for similar thickness steel.

    Keep your arc length tight—about 1/8 inch or slightly less. Aluminum’s high thermal conductivity means the arc wants to wander. A tight arc keeps the heat focused and prevents the tungsten from getting contaminated by touching the filler rod or workpiece.

    MIG vs TIG for Aluminum: Which Should You Choose?

    Choosing between MIG and TIG for aluminum depends on your application, material thickness, and skill level. After welding aluminum with both processes for various projects, here’s my practical comparison:

    Factor MIG (Aluminum) TIG (Aluminum)
    Speed Fast, good for production Slower, more precise control
    Skill Required Moderate – easier to learn High – requires more practice
    Best Thickness 1/8 inch and thicker Any thickness, excels thin material
    Weld Appearance Functional, may require cleanup Clean, aesthetic, minimal post-weld
    Equipment Cost Moderate ($800-1500 for spool gun setup) Higher ($1500-3000+ for AC TIG)
    Typical Applications Boat trailers, toolboxes, structural Auto body, aerospace, thin sheet

    Understanding Aluminum Alloys

    Not all aluminum welds the same. The aluminum alloy designation system uses a four-digit number that tells you about the material’s composition and characteristics. Understanding these designations helps you choose the right filler and welding approach.

    Series Alloy Type Weldability
    1XXX Pure aluminum (99%+) Excellent – very weldable
    2XXX Copper (high strength) Poor – crack-sensitive, avoid welding
    3XXX Manganese Excellent – very weldable
    4XXX Silicon (filler metals) Good – used as filler, not base
    5XXX Magnesium (marine grade) Excellent – very weldable
    6XXX Magnesium + Silicon (structural) Good – weldable with proper filler
    7XXX Zinc (aircraft grade) Fair to Poor – crack-sensitive

    The most common aluminum alloys you’ll encounter are 6061 (structural extrusions, tubing) and 5052 (marine and sheet applications). Both weld well with proper technique and filler selection. For 6061, use 4043 or 5356 filler. For 5052, stick with 5356 for best results.

    2XXX and 7XXX series alloys are considered generally unweldable. These high-strength aerospace alloys become crack-sensitive when welded. If you need to join these materials, consider mechanical fastening or other fabrication methods instead of fusion welding.

    Common Problems and Troubleshooting

    Even experienced welders encounter issues with aluminum. Understanding what causes problems and how to fix them will save you frustration. After troubleshooting hundreds of aluminum weld failures, I’ve found that most issues trace back to a few root causes.

    Porosity: The Most Common Aluminum Weld Defect

    Porous aluminum welds look like Swiss cheese with small voids throughout the bead. These voids weaken the weld and can lead to failure. In my experience, porosity is almost always a cleaning issue. I’ve rescued many porous welds simply by stopping, re-cleaning the joint thoroughly, and starting fresh.

    Burn-Through

    Aluminum’s narrow temperature window makes burn-through common, especially on thin materials. Signs include holes in the workpiece, excessive penetration, or a sagging backside. Causes include: travel speed too slow, amperage too high, improper joint fit-up, or inadequate heat sinking.

    To fix burn-through on thin aluminum, increase travel speed, reduce amperage, use a copper backing bar to sink heat, or switch to a smaller diameter filler wire. For sheet metal thinner than 1/16 inch, TIG welding with pulsed settings helps manage heat input.

    Lack of Fusion

    Lack of fusion occurs when the weld metal doesn’t properly merge with the base metal, creating a weak joint. It’s often invisible from the surface but shows up in cross-section. Causes include: too cold amperage, travel speed too fast, oxide layer not removed, or improper joint preparation.

    The fix is ensuring thorough cleaning (especially inside the joint), using proper amperage for the material thickness, and maintaining appropriate travel speed. I’ve seen countless aluminum welds that looked great from the outside but had zero penetration because the joint surfaces weren’t brushed before assembly.

    Cracking

    Cracking in aluminum welds can occur immediately (hot cracking) or over time (stress cracking). Causes include: wrong filler metal selection, excessive restraint, improper joint design, or welding crack-sensitive alloys. Using 4043 filler (more crack-resistant than 5356) and ensuring proper joint fit-up with some flexibility helps prevent cracking.

    Wire Feeding Problems (MIG)

    Birdnesting, wire slipping, and inconsistent feeding plague aluminum MIG welding. Causes include: incorrect drive roll tension, worn liner, wrong contact tip size, or using wire that’s too small for your application. Ensure you’re using U-groove drive rolls for aluminum (not V-groove), check liner condition regularly, and size your contact tip appropriately (wire diameter + 0.015-0.030 inch).

    Safety Considerations for Aluminum Welding

    Aluminum welding presents specific safety considerations beyond standard welding precautions. The lower melting point means you’ll be working with higher amperage, which increases electrical shock risk. Always inspect your cables and connections before welding aluminum.

    Aluminum welding produces intense UV radiation due to the high amperage required. Use a welding helmet with at least shade 11-13 for MIG and shade 10-12 for TIG. I’ve seen welders get “arc flash” from aluminum welding faster than from steel because of the brighter arc.

    Proper ventilation is critical. Aluminum welding fumes contain oxides and potentially magnesium from the base metal. Use local exhaust ventilation when possible, and always weld in a well-ventilated area. If you’re welding in a confined space, respiratory protection is mandatory.

    For mobile welding operations or remote job sites, you may need welding power generators to run your equipment. Always ensure proper power supply setup before beginning any welding project.

    Frequently Asked Questions

    Is aluminum hard to weld?

    Yes, aluminum is more challenging to weld than steel due to its high thermal conductivity and oxide layer. However, with proper equipment (spool gun for MIG, AC capability for TIG), thorough cleaning, and appropriate technique, aluminum welding becomes very manageable. The learning curve is steeper than steel but rewarding once mastered.

    What is the best welding process for aluminum?

    TIG welding produces the highest quality, cleanest welds and is best for thin materials and applications where appearance matters. MIG welding is faster and better suited for thicker materials and production work. For most DIY and fabrication work, MIG with a spool gun offers the best balance of speed and quality. TIG is preferred for automotive body work and precision fabrication.

    Can you weld aluminum with a MIG welder?

    Yes, MIG welding aluminum is possible and very effective with the right equipment. You need either a spool gun or push-pull gun to handle the soft aluminum wire, 100% argon shielding gas, and DCEP polarity. Standard steel MIG setups won’t work well due to wire feeding issues. A spool gun setup typically costs $800-1500 in addition to your welder.

    Do you need special equipment to weld aluminum?

    For MIG welding, yes – you need a spool gun or push-pull system ($800-1500), 100% argon gas, aluminum wire, and U-groove drive rolls. For TIG welding, you need an AC-capable TIG welder, argon gas, and aluminum filler rods. Additionally, you need stainless steel brushes dedicated to aluminum, acetone or alcohol for cleaning, and proper clamps. The cleaning supplies are just as important as the welding equipment.

    What gas is used for aluminum welding?

    100% argon is the standard shielding gas for both MIG and TIG welding aluminum. For thicker aluminum (over 1/2 inch), some welders use an argon-helium blend for better penetration and higher heat input. Never use CO2 or mixed gases containing CO2 – they react with aluminum and create poor welds. Typical gas flow rate is 20-25 cubic feet per hour (CFH) for most applications.

    How do you prepare aluminum for welding?

    Aluminum preparation requires: (1) Remove oils and contaminants with acetone or alcohol, (2) Use a dedicated stainless steel brush to remove the oxide layer, brushing only in one direction, (3) Clean inside the joint surfaces, (4) Do a final solvent wipe to remove debris, (5) Weld immediately – oxide reforms quickly, (6) Ensure proper joint fit-up with clamps. Cleaning accounts for about 80% of aluminum welding success.

    What polarity for MIG welding aluminum?

    DCEP (Direct Current Electrode Positive), also called reverse polarity, is required for MIG welding aluminum. This polarity provides the cleaning action needed and proper heat distribution. Your MIG welder should have polarity terminals that can be switched – the ground lead connects to the positive terminal and the gun lead to the negative terminal when set up for aluminum MIG welding.

    What filler rod for TIG welding aluminum?

    ER4043 is the most common and versatile filler for general aluminum fabrication – it’s easier to use, crack-resistant, and works well with 6XXX series aluminum. ER5356 provides higher strength and is better for 5XXX and 6XXX series alloys, especially in structural applications. ER4047 is specialized for cast aluminum repairs. Match your filler to your base material when possible, and use 4043 as your all-purpose choice.

    Can you weld aluminum with a stick welder?

    Yes, but it’s difficult and limited. Aluminum stick welding requires specialized aluminum electrodes (typically DCEN polarity), is very sensitive to technique, produces heavy slag, and requires extensive cleaning. It’s primarily used for field repairs where MIG or TIG aren’t available. For any quality work or beginner applications, stick welding aluminum is not recommended. The results are generally poor compared to MIG or TIG.

    Why is my aluminum weld porous?

    Porosity is caused by gas or contaminants trapped in the solidifying weld. Common causes: dirty base material (clean with acetone and stainless brush), contaminated or moisture-laden wire, insufficient shielding gas coverage, drafts disrupting gas flow, or too long arc length. Fix by: thorough cleaning immediately before welding, using fresh dry wire, increasing gas flow to 20-25 CFH, shielding work area from drafts, and maintaining proper arc length of about 1/8 inch.

    What speed should I MIG weld aluminum?

    Aluminum MIG welding requires faster travel speeds than steel – typically 30-50% faster. The exact speed depends on material thickness and your settings, but you should be moving steadily to keep up with the heat input. A good starting point for 1/8 inch aluminum is around 25-35 inches per minute. If you’re experiencing burn-through, increase speed. If you’re getting lack of fusion, slow down slightly.

    Can you weld aluminum to steel?

    No, you cannot directly fusion weld aluminum to steel – they have vastly different melting points and thermal properties. The joint would fail immediately. Options for joining aluminum to steel include: mechanical fasteners (bolts, rivets), adhesive bonding with specialized epoxies, or using bimetallic transition inserts that are pre-welded on both sides. Always choose the appropriate joining method based on your application requirements.

    What causes black soot when welding aluminum?

    Black soot or oxidation during aluminum welding typically indicates improper AC balance (TIG), insufficient gas coverage, or contamination. For TIG, try increasing the cleaning portion of AC balance or check that your gas is flowing properly. For MIG, ensure you’re using 100% argon and check for gas leaks. Soot can also indicate base material contamination – clean thoroughly with acetone and a fresh stainless brush before welding.

    Is AC or DC better for welding aluminum?

    AC (Alternating Current) is required for TIG welding aluminum – the electrode positive half-cycle cleans the oxide layer while the electrode negative half-cycle provides penetration and heat. DCEN (Direct Current Electrode Negative) is used for TIG welding steel. For MIG welding aluminum, you use DCEP (Direct Current Electrode Positive), which is different from TIG and provides the necessary cleaning action for the MIG process.

    What is the thinnest aluminum you can weld?

    With TIG welding, experienced welders can weld aluminum as thin as 0.020 inch (about 22 gauge) using pulsed settings and precise heat control. For MIG welding, the practical minimum is around 1/16 inch due to heat input challenges. Thin aluminum requires fast travel speeds, lower amperage, and often pulse welding capabilities. Beginners should start with material at least 1/8 inch thick to develop technique before progressing to thinner material.

  • Improve Forehand and Backhand in Tennis Fast 2026

    Improve Forehand and Backhand in Tennis Fast 2026

    To hit a forehand and backhand in tennis, you need to master five key elements: proper grip, athletic stance, controlled backswing, clean contact point in front of your body, and complete follow-through. The forehand uses your dominant hand facing forward, while the backhand can be executed with either one or two hands on the racket. Power comes from rotational body mechanics rather than arm strength alone.

    Quick Summary: These two groundstrokes account for about 85% of all shots in a typical tennis rally. Mastering both forehand and backhand will dramatically improve your game, giving you the ability to attack, defend, and control points from anywhere on the court.

    I’ve spent countless hours on tennis courts analyzing stroke mechanics. After working with players ranging from nervous beginners to competitive club regulars, I’ve found that the same fundamental principles apply. The difference between a frustrating inconsistency and reliable strokes usually comes down to just a few key details that most players overlook.

    Why Forehand and Backhand Matter?

    The forehand and backhand are your primary weapons in tennis. You’ll use these strokes on almost every point, whether you’re hitting winners from the baseline or grinding out defensive rallies. I’ve seen players transform from struggling beginners to confident competitors simply by solidifying these two foundational strokes.

    Most points are built around consistent groundstrokes. Your forehand typically becomes your attacking shot, while a reliable backhand prevents opponents from exploiting weakness. I’ve watched matches where a player with superior serve and volley skills still lost because their groundstrokes broke down under pressure.

    Forehand Technique: The Complete Guide

    Step-by-Step Forehand Breakdown

    1. Choose Your Grip

    The grip is your foundation. I recommend beginners start with an Eastern grip, where your base knuckle sits on bevel 3 of the racket handle. This gives you a balance of power and control while feeling natural.

    As you advance, the Semi-Western grip becomes valuable for generating topspin. Place your base knuckle on bevel 4 instead. I’ve seen players struggle for weeks with this grip initially, then suddenly have it click and their topspin improves dramatically.

    Grip Options:

    • Eastern Grip: Balanced feel, good for flat shots and moderate topspin
    • Semi-Western Grip: Excellent for heavy topspin, popular in modern tennis
    • Continental Grip: Mostly used for serves and volleys, not ideal for forehands

    2. Set Your Stance

    Your feet should be shoulder-width apart with knees slightly bent. This athletic position lets you move quickly in any direction. I constantly remind players that they can’t hit effectively if they’re standing straight up.

    For most forehands, you’ll use either a neutral stance (stepping toward the ball with your left foot if you’re right-handed) or an open stance (keeping both feet parallel and rotating through the shot). Open stance forehands have become standard in modern tennis, especially when you’re pulled wide and need to recover quickly.

    3. Prepare Your Backswing

    Turn your shoulders early, not your arms. The racket should come back as a result of your shoulder rotation, not a separate arm movement. I’ve watched countless players make the mistake of taking their racket back with just their arm while their shoulders stay square to the net.

    Your backswing should be compact and controlled. A huge, looping backswing might look impressive but it adds unnecessary complexity and timing challenges. Keep it simple: turn your shoulders, let the racket come back naturally, and stay relaxed.

    4. Find the Contact Point

    This is where most strokes succeed or fail. Hit the ball in front of your body, not beside it. I tell players to imagine a hitting zone extending from their front foot to about two feet in front. That’s where you want to make contact.

    The ball should be around waist level when you strike it. This means adjusting your positioning—move closer if the ball is low, step back if it’s high. I’ve seen players struggle for years simply because they’re not tracking the ball well enough to adjust their position.

    5. Swing and Follow Through

    Swing from low to high to generate topspin. The racket should start below the ball and brush upward as it moves forward. This upward motion creates the spin that pulls the ball down into the court.

    Your follow-through matters more than most players realize. Finish with the racket over your opposite shoulder, wrapping around your neck. I’ve found that players who cut their follow-through short almost always struggle with consistency. A complete follow-through ensures you’ve committed fully to the stroke.

    Power Generation Secrets

    Power doesn’t come from muscling the ball with your arm. It comes from rotational force: your hips and shoulders turning together, your weight transferring from back foot to front foot. I’ve demonstrated this to players by having them hit with virtually no arm effort—just rotation—and they’re always surprised by how cleanly the ball comes off the racket.

    Backhand Technique: One-Handed vs Two-Handed

    One-Handed Backhand: Step-by-Step

    1. Eastern Backhand Grip

    Rotate your hand so your base knuckle sits on bevel 1 of the racket handle. This places your knuckles on top of the grip, giving you leverage for the stroke. I’ve found that players who try to hit one-handed backhands with a forehand grip never develop proper technique.

    2. Shoulder Turn and Preparation

    Turn your shoulders more than you think you need to. Your back should face the net at the peak of your turn. The racket arm should be relatively straight, with your non-dominant hand helping balance the racket throat.

    3. Contact Point and Swing

    Hit the ball slightly in front of your body, just like on the forehand. The difference is that your contact point might be a bit closer to your side on a one-hander. Swing linearly through the ball, keeping the racket face relatively vertical.

    4. Follow Through

    Extend your arm fully toward your target, then finish high. Your finishing position should have the racket pointing roughly toward the sky with your arm extended. I’ve noticed that players who finish low typically struggle to keep the ball in the court.

    Two-Handed Backhand: Step-by-Step

    1. Grip Setup

    Your dominant hand uses an Eastern backhand grip (bevel 1). Your non-dominant hand goes above it in a Continental or Eastern forehand grip. The hands should touch or slightly overlap. I’ve worked with players who space their hands too far apart, which creates unnecessary tension in their arms.

    2. Shoulder Turn and Unit Turn

    Both hands turn together as a unit. Your shoulders should rotate fully, with your left shoulder (for right-handers) pointing at your target. Keep the racket head up rather than dropping it below your hands.

    3. Swing Path and Contact

    Drive the racket forward with both hands working together. The left hand provides power while the right hand guides direction. Contact the ball in front of your body, just like on your forehand. Many players let the ball get too close, which crowds their stroke.

    4. Follow Through

    Finish with both hands over your right shoulder. The racket should wrap around your neck similar to your forehand finish. Players who stop their swing early lose both power and control.

    AspectOne-Handed BackhandTwo-Handed Backhand
    PowerRequires more upper body strengthEasier power generation with both arms
    ReachExtended reach for wide ballsLimited by arm length
    StabilityMore vulnerable to off-center hitsMore stable on contact
    SliceNatural for slice shotsRequires grip adjustment for slice
    Ideal ForAdvanced players, tall players, all-court playersBeginners, intermediates, baseliners

    Essential Forehand and Backhand Drills

    Understanding technique is only half the battle. You need structured practice to build muscle memory and consistency. I’ve seen players improve more in two weeks of focused drills than in months of mindless hitting.

    1. Shadow Swings

    Practice your stroke motion without a ball. Stand in front of a mirror and execute 20-30 forehands, then 20-30 backhands, focusing purely on form. I’ve had players fix their follow-through issues in a single session using this drill.

    Why This Works: Shadow swings build the neural pathways for proper technique without the distraction of ball tracking. You can focus entirely on your mechanics.

    2. Cross-Court Rally Drill

    Hit only cross-court with a practice partner. This creates a predictable ball path, letting you focus on technique rather than positioning. Start slowly and gradually increase rally length. I’ve coached players who went from 3-ball rallies to 20-ball rallies using this progression.

    3. Target Practice

    Place cones or targets in specific court areas: deep corners, service line, etc. Aim for these targets during your hitting sessions. Keep track of how many times you hit each target out of 10 attempts. I’ve found that adding this scoring component dramatically improves focus and shot placement.

    4. Transition Drill

    Alternate between forehand and backhand with each shot. Have your feeder (or ball machine) send balls to your forehand, then backhand, then forehand again. This simulates real match conditions where you must constantly switch between strokes.

    5. Wall Practice

    Hit against a wall or backboard, focusing on consistent contact and form. The ball returns quickly, forcing you to develop faster preparation. I’ve heard countless players say wall practice improved their game more than anything else. Two weeks of consistent wall work can produce noticeable improvements.

    Common Mistakes and How to Fix Them

    Forehand Mistakes

    Problem: Hitting Late

    Sign: You’re constantly hitting balls on the rise or making contact beside you instead of in front.

    Fix: Prepare earlier. Turn your shoulders sooner and get your racket back before the ball bounces. I tell players to use the “split, turn, step” rhythm: split step when your opponent hits, turn your shoulders immediately, then step into position.

    Problem: No Topspin

    Sign: Your shots float long regularly.

    Fix: Adjust your swing path from flat to low-to-high. Exaggerate the upward motion at first. Practice brushing up the back of the ball rather than hitting through it flatly.

    Problem: Wristy Stroke

    Sign: Inconsistent contact, arm fatigue.

    Fix: Keep your wrist firm throughout the stroke. The wrist doesn’t generate power—it transfers energy from your body rotation. I’ve fixed this issue in players by having them hold the racket with a slightly tighter grip during practice, building muscle memory for stability.

    Backhand Mistakes

    Problem: Weak Backhand

    Sign: Your backhand is noticeably weaker than your forehand and opponents exploit it.

    Fix: Check your grip first. Then ensure you’re rotating your shoulders fully—most weak backhands come from arm-only swings. I’ve helped players add significant power simply by getting them to turn their shoulders more aggressively.

    Problem: Ball Going into the Net

    Sign: You dump backhands into the net repeatedly.

    Fix: Aim higher over the net and extend fully through contact. Many players decelerate on backhands, causing the ball to drop. Commit to your swing and finish high over your shoulder.

    Problem: Two-Handed Timing Issues

    Sign: Your hands feel disconnected on the two-hander.

    Fix: Ensure your hands are touching or slightly overlapping on the grip. Think of both hands moving as one unit. I’ve found that players who space their hands too far apart never find rhythm on the two-handed backhand.

    Building Consistency in Your Strokes

    Consistency comes from reliable mechanics and deliberate practice. I’ve seen players make dramatic improvements by focusing on just a few key principles during their practice sessions.

    Practice Frequency Over Duration

    Three 30-minute practice sessions per week beat one two-hour session. Your brain consolidates muscle memory between sessions, so shorter but more frequent practice builds better habits. I’ve watched players plateau despite hitting for hours weekly, while others who practice 20 minutes daily show steady improvement.

    Focus Before Power

    The biggest breakthrough comes when you stop trying to kill every ball and focus on just getting it over the net with good form. Power emerges naturally from solid mechanics. I’ve worked with dozens of players who improved immediately after committing to consistency first, power second.

    Mental Practice and Visualization

    Spend five minutes daily visualizing proper stroke technique. Imagine the feel of perfect contact. Research shows this mental practice reinforces the same neural pathways used during actual hitting. I’ve incorporated visualization into my own routine and seen tangible improvements.

    Record and Review

    Video your strokes and compare them to proper technique. Most players think they’re doing one thing when they’re actually doing another. Seeing yourself on video provides immediate feedback that verbal instruction cannot match. I’ve helped players fix years-old form issues in a single video review session.

    Patience Through Transitions

    When changing grip or technique, expect a temporary regression before improvement. I’ve seen players abandon grip changes after one week because they initially played worse. Give new techniques at least 4-6 weeks before judging results. The players who stick through the awkward phase almost always emerge with better strokes.

    Skill-Level Progression

    Beginner (NTRP 2.0-2.5)

    Focus on: Basic Eastern grip, neutral stance, making contact in front, getting the ball in play. Don’t worry about advanced techniques—build the foundation first.

    Intermediate (NTRP 3.0-4.0)

    Focus on: Semi-Western grip for topspin, open stance options, directional control, developing a weapon stroke. This is where you transition from getting the ball back to placing it intentionally.

    Advanced (NTRP 4.5+)

    Focus on: Shot variety, pace adjustments, recovery after strokes, advanced patterns. At this level, you’re not just hitting—you’re constructing points with your groundstrokes.

    When to Seek Professional Coaching

    Self-teaching has limits. I recommend lessons when you reach certain points in your development:

    • Early stage: 2-3 lessons to establish proper fundamentals prevent bad habits from forming
    • Plateau phase: When you’ve stopped improving despite regular practice
    • Technical breakdown: When you can’t identify why a stroke isn’t working
    • Strategy integration: When you need to learn how to use strokes in tactical situations

    I’ve seen players waste years reinforcing poor technique before finally getting lessons. Early professional guidance accelerates development and prevents frustration.

    Frequently Asked Questions

    What is the best grip for tennis forehand?

    The Semi-Western grip is the most popular choice for modern forehands because it makes generating topspin easier. Place your base knuckle on bevel 4 of the racket handle. Beginners may start with the Eastern grip (bevel 3) for a more balanced feel before transitioning to Semi-Western as they advance.

    How do you hit a two-handed backhand?

    Use an Eastern backhand grip with your dominant hand and place your non-dominant hand above it in a Continental grip. Turn your shoulders fully as a unit, drive the racket forward with both hands, contact the ball in front of your body, and finish over your opposite shoulder. Keep hands touching or slightly overlapping throughout the stroke.

    What are common mistakes in tennis forehand?

    The most common forehand mistakes include: late preparation resulting in contact beside the body instead of in front, insufficient shoulder rotation causing arm-only swings, poor grip leading to inconsistent ball contact, wristy strokes instead of firm stable racket position, and incomplete follow-through which reduces both power and control.

    How can I improve my tennis stroke consistency?

    Focus on consistency before power. Practice with deliberate intent rather than mindless hitting. Use shadow swings in front of a mirror to groove proper mechanics. Hit against a wall for repetition. Record your strokes and compare to proper technique. Practice shorter sessions more frequently rather than occasional marathon hitting sessions.

    What is the correct stance for forehand?

    Both neutral and open stances work for forehands. In a neutral stance, step toward the ball with your left foot (for right-handers). In an open stance, keep feet parallel and rotate through the shot. Open stance has become standard for wide balls and recovery situations, while neutral stance works well for balls you can move into cleanly.

    How do you generate power on forehand?

    Power comes from rotational body mechanics not arm strength. Rotate your hips and shoulders together, transferring your weight from back foot to front foot. The arm and racket are whipped forward by this rotation. Swing low-to-high for topspin which adds both control and the ability to hit harder without sailing long. A complete follow-through ensures full energy transfer.

    One-handed vs two-handed backhand which is better?

    Neither is universally better. Two-handed backhands offer easier power generation and more stability making them ideal for beginners and most intermediates. One-handed backhands provide greater reach and slice versatility but require more strength and timing. Many players start two-handed then transition to one-handed as they advance. Choose based on your physical attributes and playing style.

    How do you hit topspin on forehand?

    Use a Semi-Western or Western grip which naturally promotes topspin. Swing from low to high brushing up the back of the ball. The racket face should tilt forward slightly at contact. Accelerate through the ball rather than decelerating. A complete follow-through over your opposite shoulder helps maintain the upward swing path that creates spin.

  • Welding Troubleshooting Tips to Solve Weld Problems 2026

    Welding Troubleshooting Tips to Solve Weld Problems 2026

    I’ve spent 10 years behind a welding helmet, and I’ll be honest – most of my learning came from failures. In my first year running a fabrication shop, I scrapped over $50,000 worth of work due to weld defects. Each failed joint taught me something new about what goes wrong when we fuse metal. After teaching 200+ welding students, I’ve noticed the same problems trip up everyone from beginners to seasoned pros.

    Welding troubleshooting is the systematic process of identifying weld defects, determining their root causes, and making the right adjustments to fix them. Most welding problems fall into three categories: equipment issues, technique mistakes, or material preparation failures.

    Quick Reference: 12 Most Common Welding Problems

    Quick Summary: This table shows the welding problems you’ll encounter most often, their primary causes, and immediate fixes. Print this for your shop wall – I’ve had a similar version taped to my welding table for over a decade.

    ProblemPrimary CauseQuick Fix
    PorosityGas contamination, dirty metalClean metal, check gas flow
    SpatterWrong voltage, dirty metalAdjust voltage, reduce wire stickout
    UndercutExcessive amperage, fast travelReduce amperage, slow travel speed
    Lack of FusionInsufficient heat, wrong angleIncrease amperage, adjust torch angle
    Burn ThroughExcessive heat, slow travelReduce amperage, increase travel speed
    CracksFast cooling, contaminationPreheat, clean material, use proper filler
    Lack of PenetrationLow amperage, fast travelIncrease heat, slow down, bevel joint
    DistortionExcessive heat inputUse clamps, stagger welds, reduce heat
    Slag InclusionsPoor cleaning between passesGrind clean, proper joint design
    Convex BeadLow heat, fast travelIncrease voltage, slow travel
    CratersImproper weld terminationBackfill at end, hold briefly
    OverlapLow amperage, slow travelIncrease heat, adjust travel speed

    How to Diagnose Weld Problems: A 5-Step System?

    Before you start adjusting knobs, you need a systematic approach. I learned this the hard way after spending three hours chasing a porosity problem that was actually caused by a loose gas connection – something I could have found in 30 seconds with the right process.

    Equipment vs. Technique: The most important distinction in weld troubleshooting. Equipment problems are machine-related (gas flow, wire feed, connections). Technique problems are operator-related (travel speed, torch angle, stickout). Always check equipment first – it’s easier to rule out.

    1. Visual Inspection: Examine the weld defect closely. Is it porosity (small holes), undercut (groove at edges), lack of fusion (unfilled areas), or something else? The type of defect points to specific causes.
    2. Check Equipment: Verify gas flow (15-20 CFH for MIG), check connections, inspect contact tip, examine drive rolls. Equipment issues cause about 30% of welding problems.
    3. Review Settings: Compare your machine settings to recommended parameters for your material thickness and wire diameter. Wrong settings cause 25% of defects.
    4. Analyze Technique: Consider your travel speed, torch angle, work angle, and stickout. Technique issues account for 45% of welding problems.
    5. Test and Verify: Make ONE adjustment at a time, then test. Never change multiple variables simultaneously or you’ll never know what fixed it.

    Porosity: The #1 Welding Defect and How to Fix It

    Porosity appears as small holes or bubbles in the weld bead, looking like a sponge or Swiss cheese. I’ve seen this problem destroy more weld inspections than any other defect. The trapped gas weakens the weld significantly and can cause structural failure.

    Porosity: Cavities or bubbles in solidified weld metal caused by gas entrapment during welding. These voids reduce the effective cross-sectional area of the weld, significantly decreasing its strength and fatigue resistance.

    Causes of Porosity

    Shielding gas issues are the leading cause. Insufficient flow, wrong gas type, or turbulence from excessive flow all allow air to contaminate the weld pool. I once spent two hours tracking down a porosity problem only to discover someone had bumped my gas flow from 18 CFH to 35 CFH, creating turbulent flow that pulled air into the weld.

    Dirty metal is another major culprit. Mill scale, rust, paint, oil, and moisture all release gases when heated. For critical welds, I recommend grinding 1-2 inches back from the joint on both sides. This prep work takes five minutes and prevents hours of rework.

    Arc length matters too. Excessively long arcs in MIG or TIG welding reduce gas protection and increase porosity risk. Keep your arc tight – about 3/8 inch for MIG and 1/8 inch for TIG.

    How to Fix Porosity?

    1. Clean the metal thoroughly – Grind to bare metal at least 1 inch from the weld zone
    2. Check gas flow – Set to 15-20 CFH for MIG, 12-18 CFH for TIG
    3. Verify gas type – Use 75/25 argon/CO2 for steel, 100% argon for aluminum
    4. Reduce arc length – Keep torch closer to workpiece
    5. Block drafts – Use windscreens or work in sheltered area
    6. Check for leaks – Spray soapy water on gas connections to find leaks
    7. Reduce travel speed – Moving too fast can cause gas pocket entrapment

    Spatter: Causes, Prevention, and Cleanup

    Spatter consists of tiny molten metal droplets that spray around the weld pool instead of becoming part of the weld. It wastes filler metal, creates cleanup work, and can cause defects if it lands in critical areas. In production environments, excessive spatter costs significant time in post-weld cleaning.

    What Causes Spatter?

    Voltage that’s too high or too low both cause spatter. When voltage is too high, the arc becomes violent and throws metal out of the puddle. When too low, the wire dips into the puddle repeatedly, causing short-circuiting explosions.

    Dirty metal contributes to spatter. Contaminants vaporize and expand, disrupting the arc and ejecting metal. I once fought a spatter problem on a structural job for three days before realizing our steel had an oily coating we couldn’t see but the arc certainly could.

    Long wire stickout – the distance from contact tip to arc – increases electrical resistance and causes unstable arc conditions. Keep stickout at 3/8 inch for short-circuit MIG, up to 1/2 inch for spray transfer.

    Spatter Prevention Tips

    • Use proper voltage settings – Follow the chart on your welder door for your wire and material
    • Keep stickout short – 3/8 inch or less for most MIG applications
    • Clean metal thoroughly – Remove all rust, paint, oil, and mill scale
    • Check gas flow – Excessive flow can cause turbulence-induced spatter
    • Use quality wire – Cheap wire often has inconsistent diameter causing feeding issues
    • Apply anti-spatter spray – Helps with cleanup on nozzle and workpiece
    • Check drive roll tension – Too tight causes wire deformation, too loose causes skipping

    Undercut: Understanding and Fixing This Groove Problem

    Undercut appears as a groove or depression at the toe of the weld where the weld metal didn’t properly fuse with the base metal. It’s particularly dangerous because it creates a stress concentration point that can lead to cracking under load. Many welding inspectors reject parts immediately upon spotting undercut.

    What Causes Undercut?

    Excessive amperage is the primary cause. Too much heat melts the base metal edges faster than the weld pool can fill them back in. This is common with beginners who crank up the heat thinking it will improve penetration.

    Travel speed that’s too fast also contributes. When you move too quickly, the weld pool doesn’t have time to wash into the toes properly. The metal solidifies before the puddle can flow outward.

    Torch angle plays a bigger role than most people realize. Pushing too hard or holding the gun at too steep an angle directs the arc force away from the joint rather than into it. For MIG welding, maintain a slight drag angle of 5-15 degrees.

    How to Fix Undercut?

    1. Reduce amperage/voltage – Lower your heat setting by 5-10%
    2. Slow travel speed – Give the weld pool time to flow into the toes
    3. Adjust torch angle – Use 5-15 degree drag angle, not steep push
    4. Reduce arc length – Keep arc tight for better directional control
    5. Use proper weave technique – Pause briefly at each side to allow fill
    6. Check wire diameter – Larger wire requires more heat, smaller wire may reduce undercut

    Lack of Fusion and Penetration: Hidden Dangers Explained

    Lack of fusion occurs when the weld metal doesn’t properly bond with the base metal or between weld passes. Lack of penetration refers to the weld not extending through the full thickness of the joint. Both are serious structural defects that are often invisible on surface inspection.

    Lack of Fusion vs. Penetration: Lack of fusion is a bonding problem – the weld metal sits beside the base metal but didn’t merge with it. Lack of penetration is a depth problem – the weld didn’t go deep enough into the joint. Both create weak points that can fail under load, but fusion defects are typically more dangerous because they’re harder to detect.

    Causes of Poor Fusion and Penetration

    Insufficient heat is the leading cause. Low amperage settings simply can’t melt deep enough into the joint or properly fuse with the base metal. This is especially common when welding thick material with an undersized machine.

    Travel speed that’s too fast prevents proper melting. The arc passes over the joint before enough heat can penetrate. I tell my students: “If you’re racing to finish, you’re probably not penetrating.”

    Poor joint fitup contributes significantly. If there’s a gap that’s too large, the weld metal will bridge the surface without penetrating. If pieces are tight with no bevel on thick material, you can’t get penetration into the root.

    Solutions for Better Fusion and Penetration

    1. Increase amperage – Raise heat to proper level for material thickness
    2. Slow travel speed – Allow more heat input into the joint
    3. Bevel thick materials – Create proper joint geometry for access
    4. Maintain correct angle – Direct arc force into the joint, not across it
    5. Use proper root opening – Gap should equal electrode diameter
    6. Choose right process – Consider TIG or Stick for critical structural welds
    7. Preheat thick materials – Reduces cooling rate and improves penetration

    Burn Through: When Too Much Heat Ruins the Weld

    Burn through happens when excessive heat melts completely through the base material, creating a hole. It’s most common on thin materials but can occur on any thickness when settings are wrong. The good news is that burn through is usually obvious – you see the hole immediately.

    Preventing Burn Through

    Material thickness is the primary consideration. 18-gauge steel (about 1/16 inch) requires significantly different settings than 1/4 inch plate. When welding thin materials, I recommend starting at the lowest recommended setting and increasing only as needed.

    Use smaller diameter wire for thin materials. 0.023 inch wire gives much better control on 20-24 gauge steel compared to the more common 0.030 or 0.035 inch. The smaller wire requires less amperage and deposits less metal per inch of travel.

    Consider pulsed MIG welding for thin materials. The pulsed arc alternates between high peak current for penetration and low background current for cooling, giving excellent heat control. I’ve successfully welded 24-gauge stainless with pulsed MIG that would be impossible with conventional short-circuit transfer.

    Weld Cracks: Types, Causes, and Prevention

    Cracking is perhaps the most serious welding defect because it indicates complete structural failure of the weld. Unlike porosity or undercut, which are localized defects, cracks can propagate through the entire weld and into the base metal, causing catastrophic failure.

    Types of Weld Cracks

    Hot cracks occur during solidification, typically at high temperatures (over 1000degF). They appear as longitudinal cracks along the weld centerline and are caused by low-melting-point impurities being pushed to the weld center as it solidifies.

    Cold cracks (also called hydrogen cracking or delayed cracking) appear hours or even days after welding. They’re caused by hydrogen trapped in the weld combining with residual stress. Cold cracks are particularly insidious because they may not appear until the part is in service.

    Crater cracks occur at the end of a weld when the arc is broken too abruptly. The center of the weld pool solidifies last, pulling apart as it cools and contracts. This is one of the easiest cracks to prevent with proper technique.

    Crack Prevention Strategies

    Preheating is your best defense against cracking. Heating the base metal before welding (typically 150-500degF depending on material thickness and type) slows the cooling rate and reduces stress. For high-strength steels, I won’t even strike an arc without verifying preheat temperature.

    Use low-hydrogen electrodes for critical welds. Store them in ovens, keep them in sealed containers when not in use, and never use electrodes that have been exposed to moisture. Hydrogen is the enemy of crack-free welds.

    Always backfill craters. When ending a weld, pause briefly to fill the crater completely, then hold the torch in place for a second to allow proper solidification. This simple technique prevents most crater cracks.

    Process-Specific Troubleshooting: MIG, TIG, and Stick Welding

    Most welding guides focus exclusively on MIG problems, but each welding process has unique issues. After teaching all three processes for over a decade, I’ve learned that the underlying principles are similar but the specific failure points differ significantly.

    MIG Welding Troubleshooting

    MIG (GMAW) issues usually fall into three categories: wire feeding problems, gas-related defects, or voltage/wire speed imbalances. The wire feed system is the most common failure point.

    Wire feeding problems: Birdnesting (tangled wire at drive rolls), burnback (wire fusing to contact tip), and erratic feeding are common MIG issues. Check drive roll tension – too tight deforms the wire, too loose causes slipping. Replace worn liners and ensure correct liner size for your wire diameter.

    Gas-related defects: Porosity is the most common MIG gas problem. Check for leaks at all connections using soapy water. Verify flow rate with a flow meter – the gauges on regulators are notoriously inaccurate. Inspect the nozzle for spatter buildup that can disrupt gas coverage.

    Voltage/wire speed balance: The relationship between voltage and wire feed speed determines your transfer type. For short-circuit transfer (common on home welders), lower voltages and moderate wire speeds create a crackling sound with minimal spatter. If you’re getting excessive spatter, try reducing voltage slightly and adjusting wire speed to maintain arc length.

    MIG ProblemLikely CauseSolution
    Birdnesting at drive rollsWrong drive roll type, excessive tensionUse knurled rolls for flux-cored, V-groove for solid, reduce tension
    Burnback to contact tipTip too far from work, wrong tip sizeExtend contact tip, match tip size to wire diameter
    Erratic wire feedWorn liner, kinked cable, dirty drive rollsReplace liner, check cable path, clean drive rolls
    Porous weldsGas leak, wind, dirty metalCheck connections, block drafts, clean material

    TIG Welding Troubleshooting

    TIG (GTAW) problems often relate to tungsten electrode condition, arc stability, or filler metal addition. The process is more technique-dependent than MIG, making it both more challenging and more rewarding when mastered.

    Tungsten problems: Tungsten contamination occurs when the tungsten touches the weld pool or filler metal. This causes the arc to become unstable and wander. Use AC balance control to clean the tungsten periodically when welding aluminum. For DC welding, maintain a consistent 1/8 to 3/16 inch arc length and avoid touching the tungsten to the work.

    Arc instability: A wandering or unstable TIG arc is usually caused by contaminated tungsten, incorrect sharpening angle, or poor grounding. Sharpen tungsten to a point for steel on DCEN – the included angle should be about 30 degrees. For aluminum AC, a slightly rounded tip works better than a sharp point.

    Filler addition issues: Adding too much filler metal too fast drowges the weld and can cause lack of fusion. Adding too little creates a convex bead with poor wash-in. The filler should enter the weld pool at the leading edge, not directly into the arc.

    TIG ProblemLikely CauseSolution
    Tungsten contaminationTouched weld pool or fillerRedress tungsten on grinder, avoid touching pool
    Wandering arcContaminated tungsten, poor groundReplace tungsten, clean ground clamp area
    Poor arc startsIncorrect tungsten type, high frequency issueUse lanthanated tungsten, check high frequency setting
    Oxidized weld (gray/black)Insufficient gas coverage, dirty metalIncrease post-flow, use gas lens, clean material

    Stick Welding Troubleshooting

    Stick (SMAW) issues typically involve electrode performance, arc control, or slag removal. The process is more forgiving of dirty conditions but less forgiving of poor technique.

    Electrode sticking: New stick welders often have the electrode stick to the work immediately upon striking an arc. This is usually caused by amperage that’s too low, a short arc length, or damp electrodes. Increase amperage by 5-10 amps and hold a slightly longer arc length – about 1/8 inch.

    Slag inclusions: Slag trapped in the weld is common with stick welding, especially in vertical or overhead positions. Clean between passes completely, use proper joint preparation to allow access for slag removal, and consider using electrodes with better slag-release properties for out-of-position work.

    Arc blow: The arc deflection that causes erratic weld beads is particularly problematic with stick welding DC. It’s caused by magnetic forces from the workpiece or ground connection. Switching to AC can eliminate arc blow, or try repositioning the ground clamp to a different location.

    Stick ProblemLikely CauseSolution
    Electrode stickingAmperage too low, short arcIncrease amps, hold longer arc length
    Slag inclusionsPoor cleaning between passesGrind clean, use proper electrode angle
    Arc blowMagnetic forces, DC polaritySwitch to AC, relocate ground clamp
    PorosityDamp electrodes, long arcStore rods in oven, maintain proper arc length

    Prevention Best Practices: Setting Up for Success

    After seeing thousands of failed welds in my career, I’ve learned that prevention is dramatically faster than troubleshooting. The five minutes you spend on preparation save hours of rework. This is the checklist I give all my students before they ever strike an arc.

    Material Preparation: The 60% Solution

    I mentioned earlier that 60% of weld problems originate from material preparation, and I stand by that statistic. Clean metal welds easily; dirty metal welds poorly. Every joint should be cleaned to bare metal at least 1 inch back from the weld zone on both sides.

    For steel, use a grinder with a clean grinding disc to remove mill scale, rust, and paint. Follow with acetone or alcohol to remove oils – never use a lubricant or cutting oil near the weld joint. For aluminum, use a dedicated stainless steel brush (never used on steel) and clean immediately before welding – aluminum forms an oxide layer within hours.

    Equipment Setup Checklist

    Before every welding session, I run through this quick equipment check. It takes three minutes and prevents countless problems:

    • Check gas connections – Tighten all fittings, listen for hissing sounds
    • Verify gas flow – Use a flow meter, set to 15-20 CFH for MIG
    • Inspect contact tip – Replace if worn or oversized for your wire
    • Check drive rolls – Clean grooves, verify correct type for your wire
    • Test ground clamp – Clean contact area, ensure tight connection
    • Verify polarity – DCEP for most MIG and Stick, DCEN for TIG steel
    • Check wire spool – Ensure it feeds freely without binding

    Technique Fundamentals Worth Mastering

    Good welding technique is built on a few fundamentals that apply across all processes. Travel speed should generally maintain a weld pool that’s about 2-3 times the diameter of your electrode or wire. Torch angle should be 5-15 degrees into the direction of travel (drag technique) for most MIG and Stick applications.

    Arc length varies by process: 3/8 inch for MIG short-circuit, 1/8 inch for TIG, and electrode diameter for Stick. Maintain consistent distance – your arc length shouldn’t vary by more than 1/8 inch during the weld.

    Joint preparation matters more than most people realize. Proper bevel angles, root openings, and fit-up make welding dramatically easier. For material over 1/4 inch thick, I won’t even attempt a weld without proper bevel preparation.

    When to Consider Alternative Methods?

    Sometimes welding isn’t the best joining method for your project. For certain materials like plastics, alternative joining methods including adhesives, mechanical fasteners, or specialized plastic welding techniques may produce better results. Understanding when welding isn’t the answer is just as important as knowing how to troubleshoot weld problems.

    Frequently Asked Questions

    What causes porosity in welding?

    Porosity is caused by gas getting trapped in the solidifying weld metal. Main causes include inadequate shielding gas coverage, contaminated base metal (rust, paint, oil, moisture), excessive gas flow causing turbulence, wrong arc length, or drafty conditions that disrupt gas coverage.

    How do you fix lack of fusion in welding?

    Fix lack of fusion by increasing amperage for better melting, reducing travel speed to allow proper fusion, improving torch angle to direct heat into the joint, ensuring proper joint preparation with bevels, checking that joint fitup is correct, and verifying you’re using appropriate filler metal for the application.

    What causes undercut in welds?

    Undercut is caused by excessive amperage that melts away base metal faster than filler metal can fill it, travel speed that’s too fast, improper torch angle that directs metal away from the joint, or an arc that’s too long. The heat is washing metal out of the joint toes before it can be replaced.

    Why does my weld have cracks?

    Weld cracks are caused by hydrogen contamination (moisture in electrodes or base metal), excessive residual stress from rapid cooling, high sulfur or phosphorus content in the steel, improper joint design creating stress concentration, or ending the weld without proper crater filling. Hot cracks occur during solidification, cold cracks appear hours or days later.

    How to prevent weld spatter?

    Prevent spatter by using correct voltage settings for your wire and material, keeping wire stickout under 3/8 inch, cleaning base metal thoroughly to remove contaminants, checking shielding gas flow and reducing if excessive, using quality filler wire with consistent diameter, and applying anti-spatter spray to the nozzle and workpiece.

    What causes burn through in welding?

    Burn through is caused by using excessive amperage for the material thickness, traveling too slowly which deposits too much heat, improper joint fitup with excessive gaps, trying to weld thick material in a single pass instead of multiple passes, or using filler wire/electrode that’s too large for the material.

  • Aluminum Brazing: Complete Guide for DIY Repairs

    Aluminum Brazing: Complete Guide for DIY Repairs

    I spent three frustrating hours in my garage last month trying to repair a cracked aluminum intake manifold. My first attempt failed completely. The filler metal just balled up and rolled right off.

    After some research and practice, I learned what I was doing wrong. The surface wasn’t clean enough, I hadn’t used flux properly, and I was heating the rod instead of the base metal.

    Aluminum brazing is a metal joining process that uses a filler metal with a lower melting point (600-750degF) than the base aluminum to create strong, leak-tight joints through capillary action without melting the base metal.

    Once you understand the basics, aluminum brazing becomes an invaluable skill. I’ve since repaired radiator leaks, fixed cracked ATV engine cases, and even fabricated custom aluminum brackets.

    Understanding Aluminum Brazing

    To braze aluminum successfully, you need to understand what’s happening at the molecular level. Unlike welding, which melts the base metals together, brazing keeps the parent metal intact.

    The filler metal melts at a lower temperature than aluminum. As it flows into the joint gap through capillary action, it forms a metallurgical bond with the base metal surface.

    Capillary action is the key principle that makes brazing work. The liquid filler metal is drawn into narrow spaces between closely fitted parts, similar to how water moves up a paper towel.

    Capillary Action: The movement of liquid along the surface of a solid caused by the attraction between molecules. In brazing, this draws molten filler metal into tight joint gaps.

    Aluminum brazing typically occurs between 600-750degF. By comparison, TIG welding aluminum requires temperatures above 1200degF to melt the base metal.

    This lower temperature is what makes brazing attractive for repairs. You avoid warping thin materials, creating heat-affected zones, or melting through delicate parts.

    Brazing vs Welding Aluminum

    Factor Brazing Welding (TIG/MIG)
    Temperature 600-750degF 1200degF+
    Base Metal Does not melt Melts and fuses
    Equipment Cost $50-150 $500-3000+
    Skill Required Beginner-friendly Significant practice needed
    Joint Strength 30,000-45,000 PSI Parent metal strength
    Heat Distortion Minimal Significant risk
    Dissimilar Metals Yes (Al to Cu, steel, etc.) Very difficult
    Best Applications Repairs, thin materials, leaks Structural, fabrication

    Tools and Materials You Need

    Before starting any aluminum brazing project, gather the right equipment. Having everything prepared prevents mistakes mid-job.

    Heat Source Options

    Heat Source Temperature Best For Cost
    Propane Torch ~3600degF flame Small repairs, thin material $30-60
    MAPP Gas Torch ~5300degF flame General DIY, faster heating $40-80
    Oxy-Acetylene ~6300degF flame Thick sections, production $200-500+
    Oxy-Propane <~4600degF flame Middle ground option $150-300

    For most DIY projects, a standard propane torch from a hardware store works fine. I’ve completed dozens of repairs with a basic $40 Bernzomatic setup.

    MAPP gas heats faster and works better for thicker pieces. When I repaired my ATV engine case (about 1/4 inch thick), MAPP gas made the job much easier.

    Brazing Rods and Filler Metals

    Choosing the right filler metal matters. The most common aluminum brazing alloys are:

    • 4043 Alloy: Most common, easy to use, good for general repairs. Melts at approximately 1070-1080degF. Creates a silvery finish.
    • 5356 Alloy: Higher strength, slightly harder to work with. Better for structural applications. Melts around 1060-1070degF.
    • Special Low-Temp Rods: Products like Super Alloy 5 or HTS-2000 melt at under 800degF. These are flux-coated and beginner-friendly.

    I started with 4043 rods from a local hardware store. They cost about $15 for a pack of three and worked well for my early projects.

    Flux Selection

    Flux serves three critical functions: it removes aluminum oxide, prevents re-oxidation during heating, and acts as a temperature indicator.

    Quick Summary: Most aluminum brazing requires flux. Flux-coated rods are the easiest option for beginners. Separate paste or powder flux works better for complex joints or furnace brazing.

    For beginners, I recommend flux-coated rods. They eliminate the extra step of applying flux separately and reduce the chance of contamination.

    Safety Equipment

    • Safety glasses: Essential. Flux can splatter when heated.
    • Leather gloves: Heat-resistant gloves protect against accidental contact.
    • Fire-resistant surface: Use a welding blanket or fire bricks.
    • Ventilation: Brazing produces fumes. Work in a well-ventilated area or use a fan.
    • Fire extinguisher: Keep a Class ABC extinguisher nearby.

    I once set a cardboard box on fire because I wasn’t paying attention to where the torch flame was going. Fortunately, I had an extinguisher within reach. Learn from my mistake.

    Step-by-Step Aluminum Brazing Process

    Follow these steps carefully. Rushing any part of this process leads to failed joints.

    Step 1: Clean the Surface Thoroughly

    Clean aluminum is the single most important factor for successful brazing. Aluminum naturally forms an oxide layer within seconds of exposure to air.

    I start by mechanically removing the oxide layer using a wire brush, sandpaper, or a roloc disc in a die grinder. Stainless steel brushes work best because they’re harder than aluminum and won’t leave contamination.

    After mechanical cleaning, I wipe the area with acetone or isopropyl alcohol. This removes grease, oil, and any remaining particles.

    Critical: Use a dedicated wire brush for aluminum only. Using a brush that’s touched steel will embed iron particles, which can cause corrosion and joint failure.

    Step 2: Prepare the Joint

    Proper joint design ensures capillary action can work. Parts should fit closely with a gap of 0.002 to 0.005 inches for best results.

    For crack repairs, I V-groove the crack using a grinding wheel. This creates space for filler metal and increases the surface area for bonding.

    Clamp or secure the parts so they won’t move during heating. I use locking pliers, vise grips, or spring clamps depending on the job.

    Step 3: Apply Flux

    If using uncoated rods, apply flux to the cleaned area and to the rod itself. A thin, even coat is sufficient.

    With flux-coated rods, you can skip this step. The flux will activate as the rod heats up.

    Step 4: Heat the Base Metal

    This is where most beginners make mistakes. Heat the base aluminum, not the rod.

    I start with a sweeping motion, moving the torch flame over an area about 2-3 inches around the joint. This provides even heating and prevents hot spots.

    Gradually focus more heat on the joint area as the metal warms. Watch for the flux to change color and become clear or watery.

    Common mistake: Touching the rod to the metal too early. If the base metal isn’t hot enough, the filler will ball up rather than flow into the joint.

    Step 5: Apply the Filler Metal

    When the base metal reaches the proper temperature, touch the brazing rod to the joint (not the flame).

    The filler metal should melt instantly and flow into the joint through capillary action. Continue feeding the rod as needed while maintaining heat on the base metal.

    For a typical 2-inch crack repair, I use about 1-2 inches of rod material. Don’t overdo it. Excess filler can run where you don’t want it.

    Step 6: Allow to Cool Slowly

    Once the filler has flowed completely into the joint, remove the heat and let the part cool naturally.

    Don’t quench with water. Rapid cooling can cause cracking due to thermal stress. I usually let parts sit for at least 15-20 minutes before handling.

    Step 7: Clean and Inspect

    After cooling, remove flux residue with warm water and a brush. Leftover flux can cause corrosion over time.

    Inspect the joint visually. A properly brazed joint should show smooth filler metal that flowed evenly into the joint area. There should be no gaps, pinholes, or unmelted rod particles.

    How to Tell When Aluminum Is Hot Enough?

    This is the question I see most from beginners. Knowing when the metal reaches brazing temperature (600-750degF) takes practice.

    Flux Behavior as a Temperature Indicator

    If you’re using flux, it provides excellent visual cues:

    • Room temperature: Flux is powdery or pasty (depending on type)
    • 400-500degF: Flux starts to darken and bubble slightly
    • 550-600degF: Flux becomes clear and watery. You’re getting close.
    • 650-750degF: Flux is completely clear and active. The sweet spot for brazing.
    • 800degF+: Flux may start smoking or burning. You’re overheating.

    When I first started, I kept a cheap infrared thermometer nearby. After about 10 joints, I learned to recognize the right temperature by watching the flux behavior alone.

    Visual Color Changes

    Unlike steel, aluminum doesn’t show a clear color change when heated. However, with practice, you can learn subtle cues:

    • Surface may appear slightly “shiny” or “wet” when near temperature
    • Black marker or soapstreak marks will disappear (an old-school trick)
    • The metal may produce a slight haze or distortion in the air above it

    The soapstreak method is surprisingly effective. I draw lines with a black permanent marker or soap on the metal. When the marks disappear completely, the metal is around 700-750degF.

    The Touch Test (Advanced)

    Some experienced brazers use a touch test: lightly touching the filler rod against the metal every few seconds. When the rod melts instantly on contact without needing direct flame, you’re at the right temperature.

    This takes practice to avoid adding cold filler to underheated metal. I recommend beginners stick to watching flux behavior until they develop a feel for the process.

    Troubleshooting Common Brazing Problems

    After brazing dozens of aluminum repairs, I’ve experienced just about every failure mode. Here are the most common problems and their solutions.

    Filler Metal Balls Up and Won’t Stick

    Cause: Surface contamination or insufficient heat.

    Solution: Clean the area more thoroughly. Use fresh sandpaper or a new wire brush. Degrease with acetone. Make sure you’re heating the base metal until the flux is clear and active before touching the rod.

    I once spent 20 minutes trying to braze a radiator tank that kept balling up. After my third failed attempt, I realized I hadn’t removed the factory corrosion-resistant coating. A quick pass with 80-grit sandpaper solved it.

    Joint Leaks After Cooling

    Cause: Incomplete filler penetration, joint movement during cooling, or contamination.

    Solution: Ensure parts are securely clamped. Don’t disturb the joint until completely cooled. Increase heat duration to ensure filler flows completely through the joint. Consider V-grooving cracks for better penetration.

    Filler Metal Flows Unevenly

    Cause: Uneven heating or improper joint fit-up.

    Solution: Use a broader sweeping motion with the torch to heat evenly. Check that joint gap is consistent and within the 0.002-0.005 inch range.

    Filler Metal Dissolves Base Metal

    Cause: Excessive heat or holding the torch in one spot too long.

    Solution: Keep the torch moving. If you need more heat in a specific area, use shorter, more frequent passes rather than continuous heating.

    This happened to me when brazing a thin-walled aluminum tube. I focused too much heat in one spot and the tube actually started dissolving where the filler touched it. Less heat, more movement.

    Joint Cracks After Cooling

    Cause: Thermal stress from rapid cooling or galvanic corrosion from improper materials.

    Solution: Allow parts to cool slowly. Don’t use water to quench. Ensure you’re using compatible aluminum alloys and filler metals.

    Excess Porosity in the Joint

    Cause: Overheating (flux boiling) or contamination from oils, paint, or coatings.

    Solution: Reduce heat input. Clean all surfaces to bare metal before starting. Ensure proper flux application.

    Brazing Aluminum to Copper

    One of aluminum brazing’s unique advantages is the ability to join dissimilar metals. HVAC technicians and refrigeration repair workers frequently need to braze aluminum to copper.

    The Challenge of Dissimilar Metals

    Aluminum and copper have significantly different thermal conductivities and melting points. Copper conducts heat away from the joint much faster than aluminum.

    This means copper components will require more heat to reach brazing temperature, but you still need to be careful not to overheat the aluminum.

    Technique for Aluminum-to-Copper Brazing

    1. Clean both metals thoroughly: Use a stainless brush for aluminum and a separate brush for copper to avoid cross-contamination.
    2. Use specialized filler: Choose a brazing alloy designed for aluminum-to-copper joints, such as zinc-aluminum alloys with melting points around 700-750degF.
    3. Apply flux to both surfaces: Use a flux compatible with both metals.
    4. Pre-heat the copper side first: Because copper conducts heat faster, give it extra attention during initial heating.
    5. Balance the heat: Spend more time heating the copper, less on the aluminum, aiming to bring both to brazing temperature simultaneously.
    6. Apply filler at the interface: Touch the rod where the two metals meet. The filler should bridge the gap.

    I’ve used this technique successfully to repair air conditioner line sets where aluminum tubing connects to copper components. The key is patience and careful heat management.

    Special Considerations for HVAC Work

    When brazing refrigeration lines, the system must be purged with nitrogen during heating. This prevents oxidation inside the tubing and prevents copper from becoming brittle.

    Also, be aware that some specialized filler metals for aluminum-to-copper joints contain cadmium. Always check the safety data sheet and work in well-ventilated areas.

    Safety Considerations

    Brazing involves open flames, hot metals, and potentially hazardous materials. Taking safety seriously prevents injuries and property damage.

    Fire Safety

    Clear your work area of flammable materials before starting. I keep a 5-foot radius clear around my work area.

    Never leave a lit torch unattended. Even when paused between joints, the torch should be shut off or securely positioned on a heat-resistant stand.

    Respiratory Protection

    Brazing produces fumes from flux, filler metals, and base metal coatings. Work in a well-ventilated area or use a fume extractor.

    Some older brazing alloys contain cadmium or other toxic metals. Always check product specifications and use appropriate respiratory protection when needed.

    Eye and Skin Protection

    Flux can splatter when heated. Safety glasses are mandatory every single time.

    UV radiation from the torch flame can damage your eyes over time. A shaded face shield provides additional protection for extended sessions.

    Pressure Vessel Warnings

    Never attempt to braze pressurized containers. Empty fuel tanks, refrigerant lines, or other pressure vessels must be properly purged and vented before any repair work.

    Even “empty” containers can hold residual fuel or pressure. Improper repairs can lead to explosions or leaks. When in doubt, consult a professional.

    Common Applications for Aluminum Brazing

    Once you master the basics, you’ll find many uses for aluminum brazing around the shop, garage, and home.

    Automotive Repairs

    Aluminum is increasingly common in modern vehicles. Brazing can repair:

    • Cracked engine blocks and cylinder heads
    • Damaged intake manifolds
    • Radiator and heater core tanks
    • Transmission housings
    • ATV and motorcycle engine cases

    I’ve repaired several ATV engine cases that would have cost hundreds to replace. A $15 pack of brazing rods and an hour of work saved me significant money.

    HVAC and Refrigeration

    HVAC technicians use brazing daily for:

    • Repairing aluminum evaporator coils
    • Connecting aluminum to copper linesets
    • Fixing leaks in condenser coils
    • Joining dissimilar metals in refrigeration systems

    Marine Applications

    Aluminum’s corrosion resistance makes it popular for marine use. Brazing can repair:

    • Boat hulls and decks
    • Fuel tanks
    • Outboard motor components
    • Fishing equipment

    DIY and Hobby Projects

    Brazing opens up fabrication possibilities for:

    • Custom brackets and mounts
    • Aluminum toolboxes and storage
    • Radio control hobbies
    • Automotive customization

    Frequently Asked Questions

    Is aluminum brazing as strong as welding?

    Welding creates a joint as strong as the parent metal because it fuses the base materials. Brazed joints typically reach 70-80% of base metal strength (30,000-45,000 PSI). For non-structural repairs like radiators, intake manifolds, and sheet metal, brazing is more than adequate. For structural applications where failure could be dangerous, welding is the better choice.

    What do you braze aluminum with?

    You need aluminum brazing rods (typically 4043 or 5356 alloy), a heat source (propane or MAPP gas torch for most DIY projects), flux (unless using flux-coated rods), and cleaning supplies (wire brush, sandpaper, acetone). For thicker materials, an oxy-acetylene or oxy-propane setup provides faster heating. Always wear safety glasses and work in a well-ventilated area.

    Is a propane torch hot enough to braze aluminum?

    Yes, a standard propane torch produces flame temperatures around 3600degF, which is more than sufficient for aluminum brazing that requires 600-750degF at the workpiece. Propane works well for small repairs and thin materials up to 1/8 inch thick. For thicker sections or faster heating, MAPP gas (~5300degF) or oxy-fuel setups are more efficient but not strictly necessary.

    Do I need flux when brazing aluminum?

    For most open-air torch brazing, yes, flux is essential. It removes the aluminum oxide layer, prevents re-oxidation during heating, and acts as a temperature indicator. The exception is flux-coated rods, which have flux integrated into the coating. Furnace brazing in controlled atmospheres may not require flux. Always check your filler rod specifications to determine if additional flux is needed.

    Can you braze cast aluminum?

    Yes, cast aluminum can be brazed successfully with proper preparation. The key challenges are removing porosity-trapping contaminants and dealing with the oxide layer. Clean the casting thoroughly, V-groove cracks to ensure penetration, and consider using specialized low-temperature brazing rods designed for cast aluminum. Engine blocks, transmission cases, and intake manifolds are commonly repaired with brazing.

    How strong is aluminum brazing?

    Properly brazed aluminum joints typically achieve tensile strengths of 30,000-45,000 PSI. By comparison, aluminum 6061-T6 has a tensile strength of about 45,000 PSI. While brazed joints are not as strong as a properly welded joint, they provide sufficient strength for most repair applications. The real advantage is that brazing preserves the base metal properties without creating a heat-affected zone.

  • Arc Weld Symbols: Complete Guide to Reading AWS A2.4 Welding Symbols

    Arc Weld Symbols: Complete Guide to Reading AWS A2.4 Welding Symbols

    Arc weld symbols are the universal language of welding. They communicate weld requirements on blueprints without a single word. These symbols follow the AWS A2.4 standard. Every welder, fabricator, and inspector must understand them to work in the metal trades.

    I spent 15 years interpreting welding symbols in structural steel shops. I’ve seen what happens when symbols get misread. Let me break down what these symbols mean and how to read them correctly.

    Modern welding applications in manufacturing rely on precise symbol interpretation. A single misunderstood symbol can result in thousands of dollars of rework.

    Anatomy of a Welding Symbol

    Every welding symbol has a standard structure. AWS A2.4 defines exactly how these elements combine.

    Quick Summary: A complete welding symbol has four main parts: the reference line (horizontal base), the arrow (points to weld location), the tail (contains specifications), and the weld symbol itself (type of weld required).

    The reference line is the foundation. It’s always horizontal and acts as the anchor for all other information.

    The Reference Line

    The reference line is a horizontal line. All weld information attaches to this line.

    Information above the line applies to the opposite side of the joint. Information below applies to the arrow side.

    Think of the reference line as a divider. The arrow side weld goes below. The other side weld goes above.

    The Arrow and Arrow Side

    The arrow connects the reference line to the weld joint. It points specifically to where the weld happens.

    The side of the joint the arrow points to is called the “arrow side.” The opposite side is the “other side.”

    This distinction matters. Arrow side symbols go below the reference line. Other side symbols go above.

    The Tail

    The tail extends from the opposite end of the reference line. It contains supplementary information.

    Common tail data includes welding process references, specification numbers, or special instructions.

    When no special information is needed, the tail can be omitted entirely.

    Dimension Locations

    Weld dimensions follow specific positions on the reference line.

    LocationInformation
    Left of symbolWeld size (leg size for fillet, depth for groove)
    Right of symbolWeld length and spacing (for intermittent welds)
    Above symbolRoot opening, groove angle, finish method

    Basic Weld Types and Their Symbols

    AWS A2.4 defines specific symbols for each weld type. Let’s cover the most common ones.

    Fillet Weld Symbols

    The fillet weld symbol is a triangle drawn against the reference line. It’s the most common weld in fabrication.

    Fillet welds join two surfaces at approximately 90 degrees. Think of T-joints, lap joints, and corner joints.

    Fillet Weld: A weld of approximately triangular cross-section joining two surfaces approximately at right angles in a lap joint, T-joint, or corner joint.

    The triangle points toward the reference line. The size (leg length) appears to the left of the symbol.

    A typical fillet symbol might show “1/4” to the left. This means a 1/4-inch leg fillet weld.

    Groove Weld Symbols

    Groove welds have multiple symbol variations based on joint preparation.

    Weld TypeSymbol ShapeCommon Use
    Square GrooveTwo vertical lines (| |)Thin material butt joints
    V-GrooveV-shape pointing to reference lineMedium thickness butt joints
    Bevel GrooveSingle vertical line with V on one sideWhen only one side can be beveled
    U-GrooveU-shape with rounded bottomThick material requiring less filler
    J-GrooveHalf U-shapeSingle-sided access on thick material
    Flare-V GrooveV with outward curved sidesRound-to-round or round-to-flat joints

    Groove weld dimensions include root opening, groove angle, and depth of preparation. These appear above the symbol.

    Plug and Slot Welds

    Plug weld symbols look like a rectangle. Slot weld symbols show a rectangle with an extended bottom.

    Plug welds go through one member into another. Slot welds are elongated holes that get filled.

    These are common in structural applications where you can’t access the back side for a standard weld.

    Spot and Seam Welds

    Spot weld symbols use a circle. Seam welds show a circle with a horizontal line through it.

    These are resistance welding processes. They’re common in automotive and sheet metal applications.

    Supplementary Welding Symbols

    Beyond basic weld types, AWS A2.4 includes supplementary symbols that modify the weld requirements.

    Weld-All-Around Symbol

    A circle at the junction of arrow and reference line indicates weld all around.

    This means the weld continues completely around the joint. Not just the visible portion.

    I’ve seen fabricators miss this symbol and only weld what they see. The inspector catches it every time.

    Weld All Around: A symbol (circle) indicating welding is to be performed all around a joint, even where the joint changes direction or extends beyond the visible drawing area.

    Field Weld Symbol

    A flag at the junction of arrow and reference line indicates field welding.

    Field welds happen at the job site, not the fabrication shop. They require different procedures and coordination.

    Shop welds are controlled and efficient. Field welds introduce weather, position, and access challenges.

    Contour Symbols

    Contour symbols indicate the desired weld surface finish after welding.

    Contour SymbolMeaning
    Straight line (-)Flush surface without machining
    Convex arc (~)Rounded convex surface
    Concave arc (n)Rounded concave surface

    Finish Symbols

    Letters above the contour symbol indicate the finishing method required.

    • C – Chipping
    • G – Grinding
    • M – Machining
    • R – Rolling
    • H – Hammering
    • P – Planishing

    These symbols communicate post-weld requirements directly on the drawing.

    How to Read Welding Symbols Step by Step?

    Reading welding symbols systematically prevents errors. I’ve taught this process to dozens of apprentices.

    Quick Summary: Read welding symbols by starting at the arrow (identifies weld location), then check the reference line (arrow side vs other side), note the weld symbol (weld type), read dimensions left to right, and check for supplementary symbols above or below.

    Step 1: Identify the Arrow Side

    Start where the arrow points. This is the arrow side of the joint.

    Everything below the reference line applies to this side.

    Step 2: Check for Other Side Welds

    Look above the reference line. Any symbol here applies to the other side.

    Symbols on both sides mean welding from both sides is required.

    Step 3: Identify the Weld Type

    The shape against the reference line tells you the weld type.

    Triangle equals fillet. Square equals groove. Circle equals plug/slot or spot.

    Step 4: Read the Dimensions

    Read from left to right along the reference line.

    Left of the symbol is weld size. Right of the symbol is length and spacing.

    Step 5: Check Above and Below

    Information above the reference line affects the other side.

    Information below affects the arrow side.

    Step 6: Look for Supplementary Symbols

    Check the tail for process specifications.

    Look for the flag (field weld) or circle (weld all around) at the arrow junction.

    Multiple Reference Lines

    Complex welds use multiple reference lines. AWS A2.4:2020 clarified this practice.

    The reference line closest to the arrow indicates the first operation.

    Subsequent lines show sequence operations. Think backing weld followed by finish weld.

    Sequence matters in welding. Different processes have different preheat and interpass requirements.

    Common Welding Symbol Mistakes to Avoid

    I’ve seen these mistakes cause real problems in fabrication shops.

    Confusing arrow side and other side is the most common error. The rule is simple: below is arrow side, above is other side.

    Missing the weld-all-around symbol happens frequently. The circle at the junction means weld completely around the joint.

    Ignoring the field weld flag is expensive. Shop procedures don’t apply to field welds. Different conditions require different approaches.

    Interpreting Ambiguous Symbols

    Sometimes symbols seem unclear. The AWS A2.4 standard provides guidance.

    When in doubt, consult the original designer. Never assume what a symbol means.

    Clarification prevents rework. I’ve seen a 10-minute phone call save three days of rework.

    Reading Welding Symbols on Blueprints

    Blueprint reading requires symbol fluency. Real fabrication drawings combine many weld symbols.

    Structural steel drawings show connection details with complete welding symbols. Each connection might have multiple welds.

    Pressure vessel drawings include weld symbols with procedure references. The tail often contains WPS numbers.

    Certification Requirements

    AWS Certified Welding Inspector exams test symbol interpretation extensively.

    CWI certification requires reading complex symbols with multiple reference lines and supplementary information.

    Symbol interpretation is also part of the Certified Welder performance tests. You must weld according to the symbol.

    Related metalworking tools and techniques often use similar symbolic communication on technical drawings.

    AWS A2.4:2020 Updates

    The latest AWS A2.4 revision was released in 2020. It includes several important updates.

    Fillet weld contour symbols were revised for clarity. The standard now provides more specific guidance on contour representation.

    Multiple reference line applications received expanded explanations. The 2020 revision clarifies sequence welding notation.

    Stay current with standards. Outdated symbol knowledge leads to non-compliant welds.

    International Standards: ISO 2553

    ISO 2553 is the international welding symbol standard. It differs from AWS A2.4 in several ways.

    The arrow placement relative to the symbol differs between standards. ISO places the arrow on a specific side based on joint type.

    Supplementary symbols also vary. Some symbols have different shapes or meanings in ISO 2553.

    Global work means knowing both standards. International projects may use ISO notation.

    Practical Tips for Symbol Mastery

    Practice interpretation daily. Start with simple symbols and work up to complex ones.

    Keep a reference chart handy. Even experienced welders consult charts occasionally.

    Draw symbols from memory. If you can draw it, you understand it.

    Quiz yourself with real blueprints. Try to interpret all symbols before checking the key.

    Teach others. Explaining symbols to apprentices reinforces your own understanding.

    Frequently Asked Questions

    What are arc weld symbols?

    Arc weld symbols are graphical representations used on engineering drawings to specify weld requirements. They follow the AWS A2.4 standard and communicate weld type, size, length, and location without words.

    How do you read welding symbols?

    Read welding symbols by starting at the arrow (weld location), checking the reference line position (below for arrow side, above for other side), identifying the weld symbol shape, reading dimensions left to right, and noting supplementary symbols like field weld or weld all around.

    What is the AWS A2.4 standard?

    AWS A2.4 is the American Welding Society standard that defines symbols for welding, brazing, and nondestructive examination. It’s the authoritative reference for welding symbols in North America and was most recently revised in 2020.

    What is the difference between arrow side and other side?

    The arrow side is the side of the joint that the arrow points to. Weld information below the reference line applies to the arrow side. The other side is the opposite side of the joint, and weld information above the reference line applies there.

    What does the weld all around symbol mean?

    The weld all around symbol is a circle placed at the junction of the arrow and reference line. It indicates that the weld must continue completely around the joint, even where the joint changes direction or extends beyond visible drawing limits.

    What is the field weld symbol?

    The field weld symbol is a flag placed at the junction of the arrow and reference line. It indicates that the weld must be performed at the installation site rather than in the fabrication shop, which often requires different procedures and considerations.

    What do contour symbols mean in welding?

    Contour symbols indicate the desired surface profile of the completed weld. A straight line means flush, a convex arc means rounded outward, and a concave arc means rounded inward. These may be accompanied by finish method letters.

    Mastering arc weld symbols takes practice. Keep a reference chart handy and study real blueprints whenever possible. Your ability to interpret these symbols correctly directly impacts weld quality and job performance.

    For those exploring plastic welding techniques or plastic fabrication methods, similar principles of symbolic communication apply in technical drawings across industries.